
Food Vacuum Packaging Machine | Reliable Packaging Solutions
Engineered for ultimate freshness, maximum barrier integrity, and extended shelf-life. Ludyway provides high-precision industrial food vacuum packaging equipment, automated sealing systems, and turnkey preservation lines compliant with international sanitary standards.
Advanced Food Vacuum Packaging Systems for Modern Food Processing
In today’s fast-paced commercial food production, maintaining product freshness while optimizing distribution logistics is critical. A food vacuum packaging machine is vital for removing atmospheric oxygen from airtight pouches or containers before hermetic sealing. By drastically lowering residual oxygen levels to below 0.5%, aerobic microorganisms like bacteria and mold are inhibited, enzyme activity is suppressed, and lipid oxidation is virtually eliminated.
At Ludyway, we combine over three decades of mechanical innovation with cutting-edge microcomputer PLC control systems. Our industrial vacuum sealing machinery caters to meat processing plants, seafood distributors, dried fruit producers, dairy packers, and central kitchens requiring continuous, leak-proof packaging solutions.
Why Vacuum Packaging Matters for Commercial Food Brands
Eliminating air minimizes freezer burn, preserves natural aromatics, prevents moisture migration, and provides a sleek visual appearance that enhances consumer trust on retail shelves.
Beyond standard single and double-chamber systems, Ludyway designs high-speed multi-lane continuous vacuum packaging lines and form-fill-seal (FFS) systems integrated with Modified Atmosphere Packaging (MAP). This allows manufacturers to inject precise nitrogen (N2) or carbon dioxide (CO2) mixtures after deep vacuuming, protecting delicate food structures such as freeze-dried snacks, roasted coffee beans, and crisped vegetables.
Constructed completely from food-grade SUS304/SUS316 stainless steel with IP65-rated washdown capabilities, our machinery guarantees compliance with FDA, CE, and global HACCP hygiene regulations, assuring reliable, uninterrupted 24/7 industrial performance.
Intelligent Automation & High-Precision Vacuum Control
Micro-Sensor Vacuum Regulators
High-sensitivity digital vacuum sensors continuously monitor chamber pressure in real-time. Operators can adjust vacuum levels from 0.01 kPa to deep industrial levels for soft solids, powders, or rigid meats.
Multi-Temperature Pulse Sealing
Independent PID thermal controllers ensure accurate heating across aluminum foil, multi-layer co-extruded films, PA/PE, and biodegradable vacuum pouches without burnt edges or cold seal pinholes.
High-Capacity Busch Vacuum Pumps
Fitted with robust, energy-efficient rotary vane vacuum pumps engineered for 24-hour non-stop industrial cycles, low operating noise, minimal maintenance, and instant exhaust air filtration.
Siemens / Omron PLC Controls
Multi-language color touchscreens store up to 99 customized packaging presets, enabling rapid product changeovers between granular powders, liquids, solid cuts, and fresh marinated items.
SUS304 Sanitary Washdown Body
Seamless welded construction with sloping surfaces allows quick drainage and full IP65 washdown sanitization, meeting strict food hygiene and anti-corrosion production environments.
Inert Gas Flushing Module
Optional gas-flushing valves inject high-purity Nitrogen or Carbon Dioxide in exact proportions, ideal for delicate snack goods, powdered dairy blends, and fresh pasta prone to crushing.
High-Performance Food Vacuum & Preservation Machinery
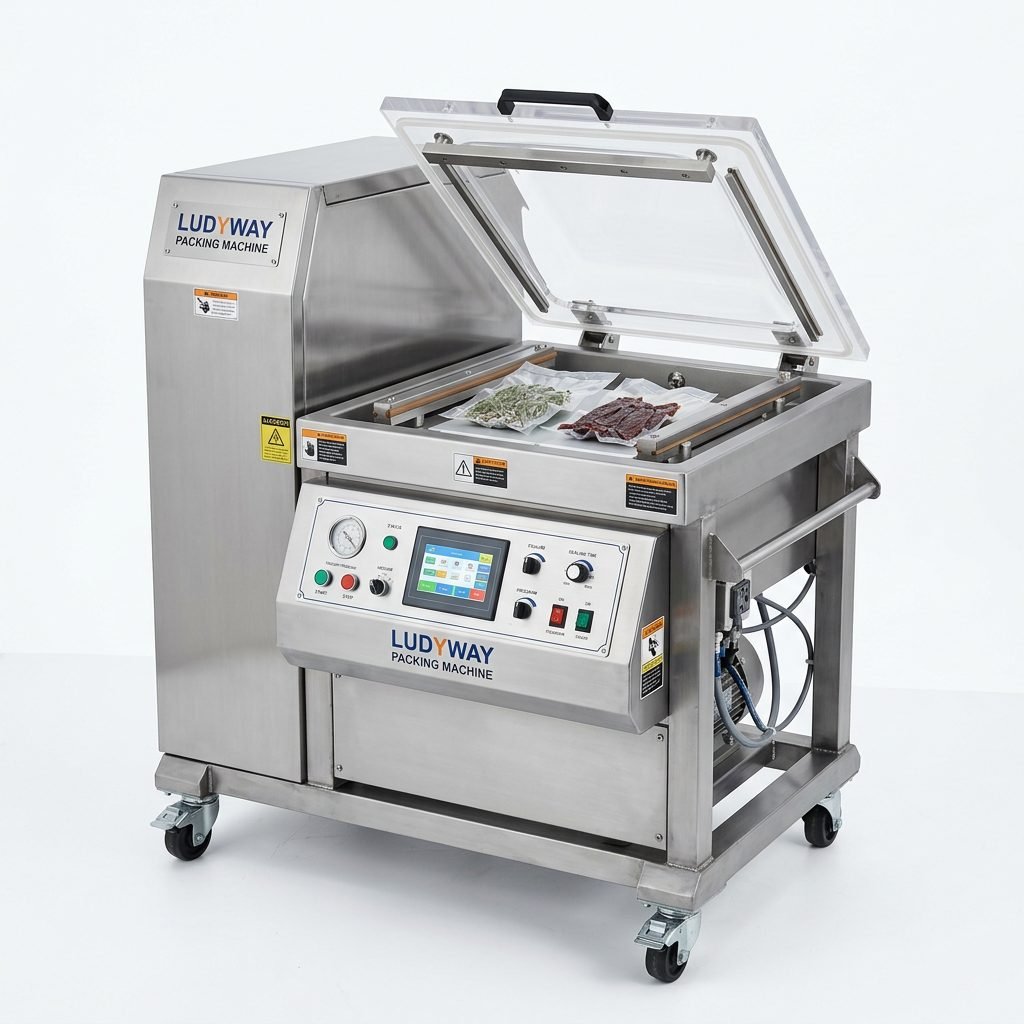
Industrial Vacuum Packaging Machine for Food Products
Heavy-duty chamber vacuum packing system designed for bulk food processing, block cheeses, and fresh cuts.
View Specifications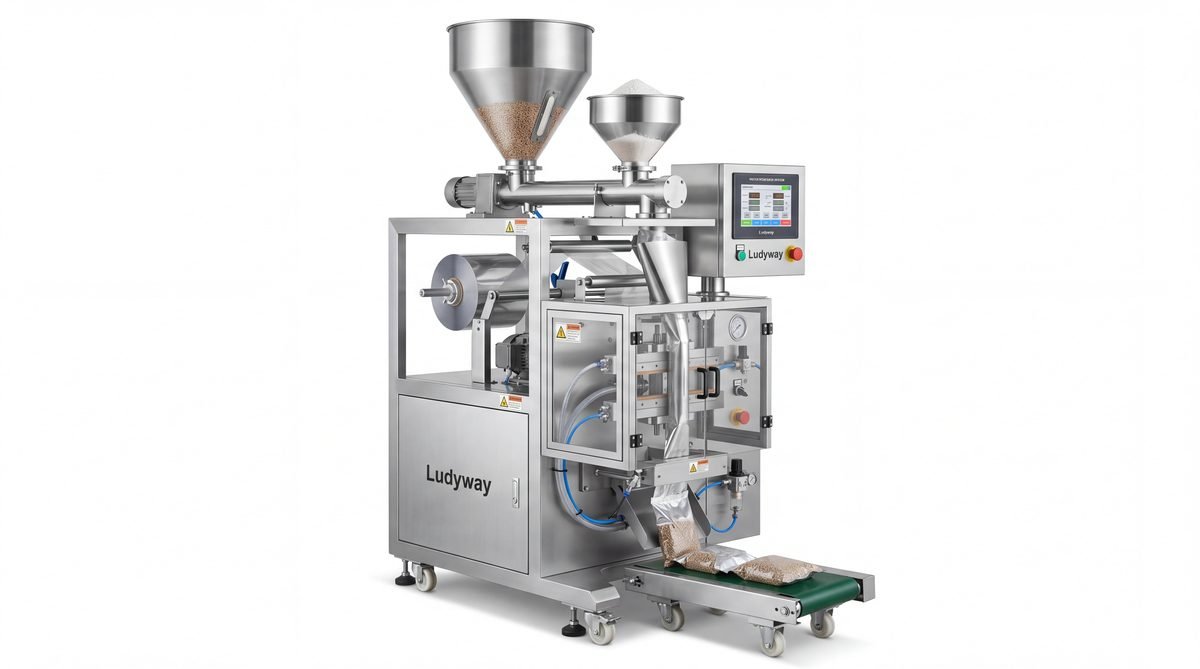
Industrial Vacuum Packaging Machine for Food Powders
Equipped with anti-dust filters and gentle de-aeration for vacuuming functional food powders and spices.
View Specifications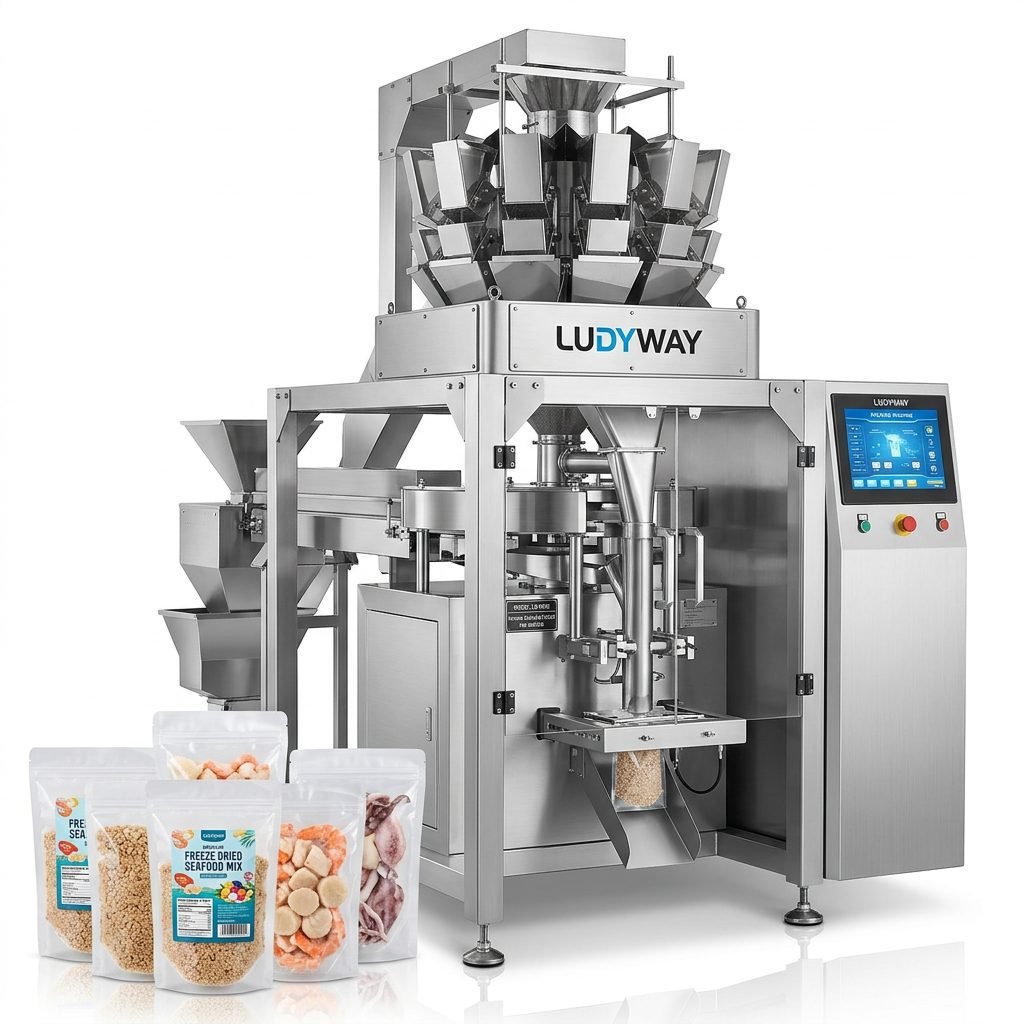
Freeze Dried Seafood Vacuum Sealing Machine
Precision vacuum sealing for delicate shrimp, dried squid, and fish granules without product breakage.
View Specifications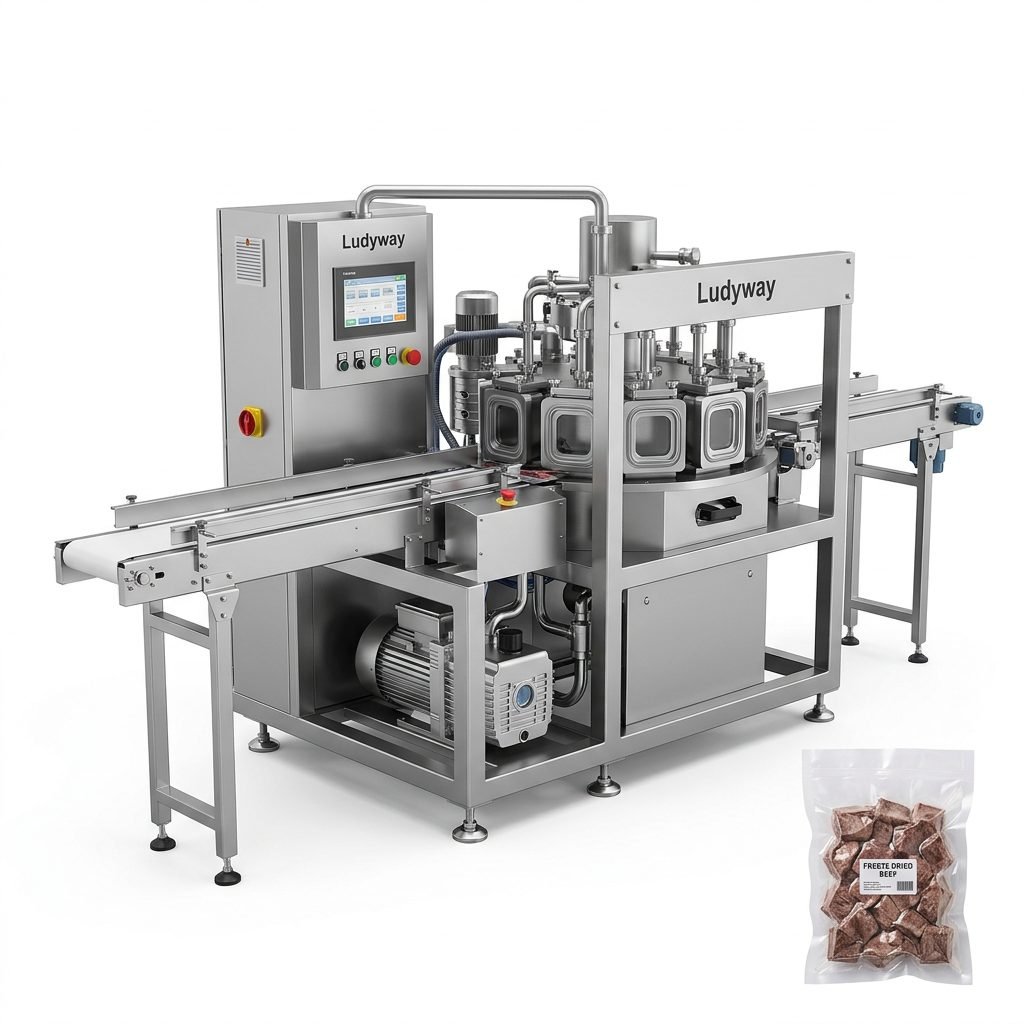
Freeze Dried Beef Vacuum Packaging System
High-speed commercial vacuum and sealing line engineered for beef jerky, cured steaks, and pet delicacies.
View Specifications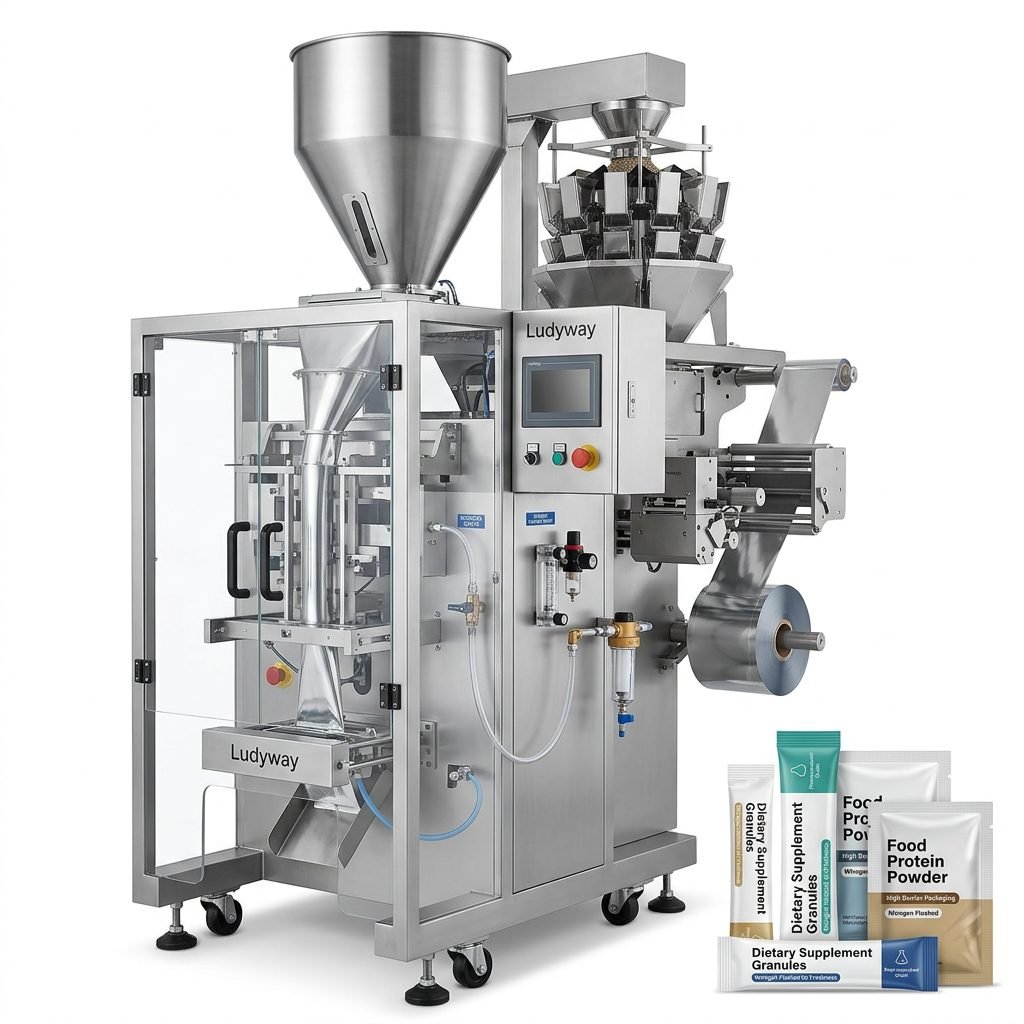
Nitrogen Flushing Vacuum Packaging System
Automated vacuum gas replacement system creating an inert environment for delicate snack crisps and infant formula.
View Specifications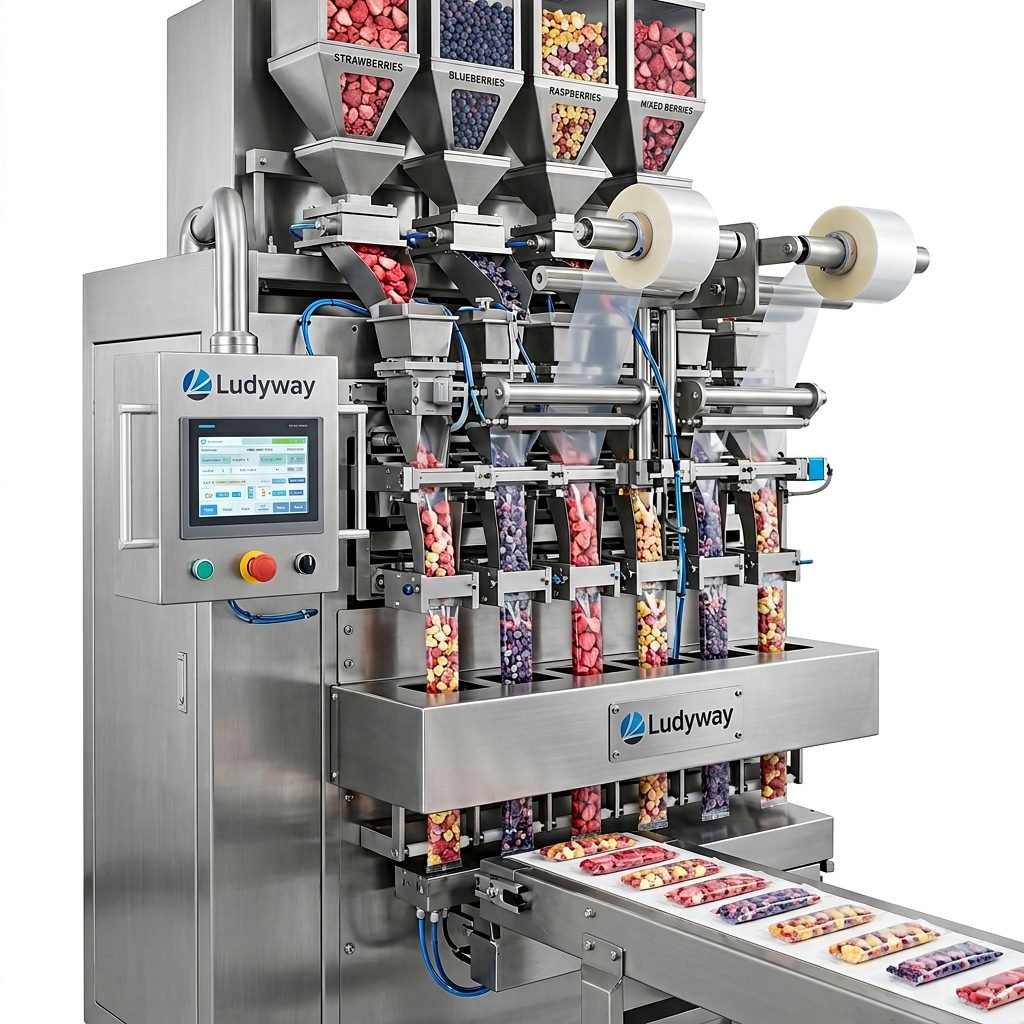
Freeze-Dried Fruit Multi-Lane Packing Line
Multi-lane high-speed portion packaging with vacuum gas flushing for freeze-dried fruit chunks and slices.
View Specifications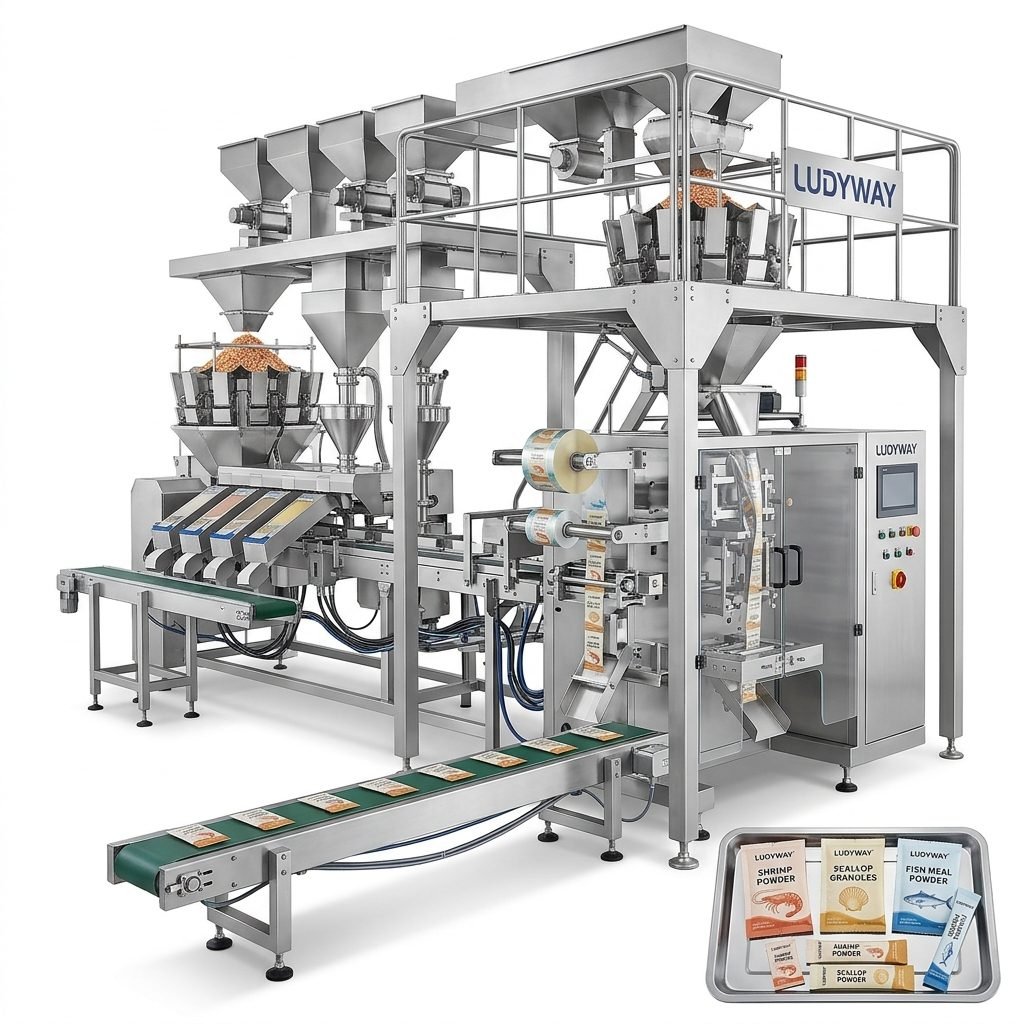
Automated Dried Seafood Packaging Line
Multi-lane vacuum sealing unit built with anti-saline stainless steel for fish powder, shrimp, and marine snacks.
View Specifications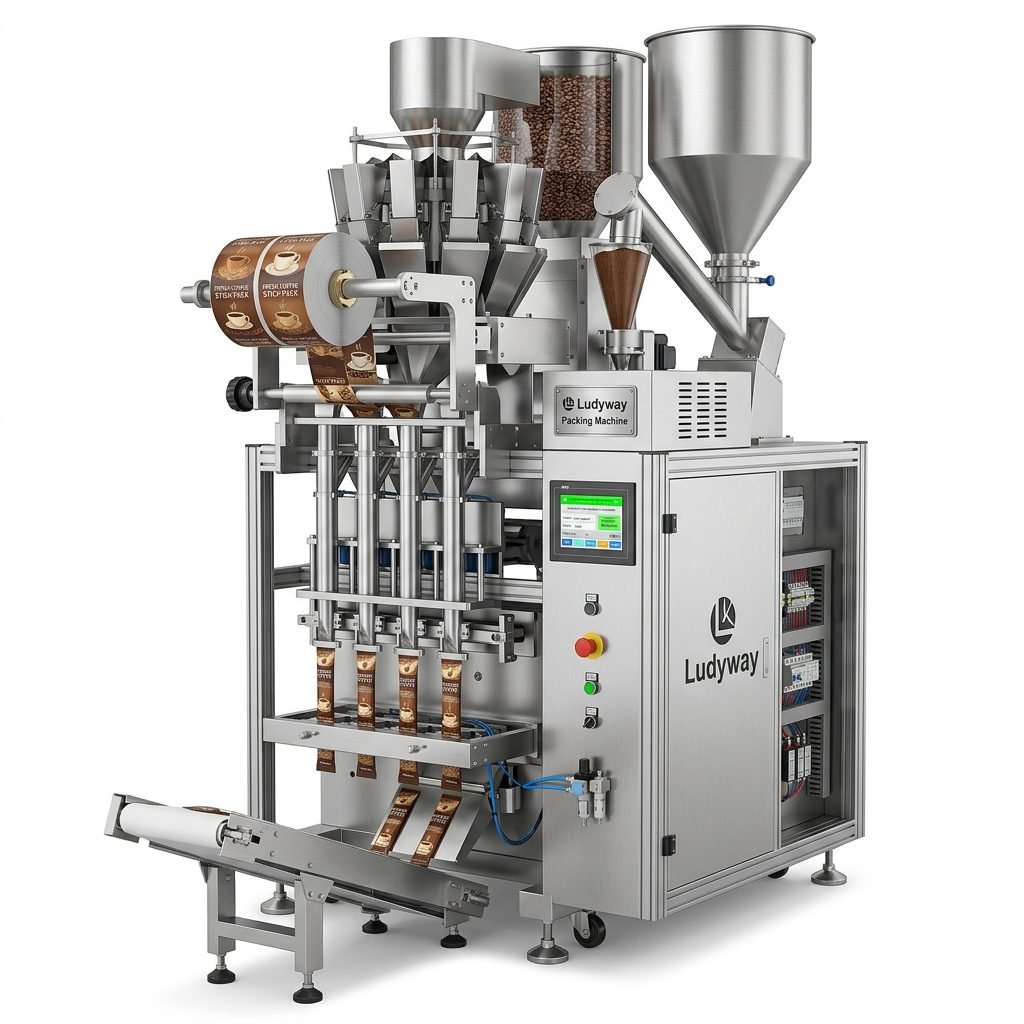
Automatic Multi-Lane Coffee Bean Packing Line
Aroma-retaining vacuum and one-way degassing valve integration for specialty whole-bean and ground coffee.
View SpecificationsComprehensive Vacuum Solutions Across Food Sectors
Fresh & Cured Meat Products
Removes air around bone-in cuts, steaks, bacon, and sausages using heavy-duty puncture-resistant barrier pouches. Extends refrigerated shelf life from days to weeks while preventing oxidation browning and fluid purge.
Seafood & Marine Delicacies
Essential for salmon fillets, frozen shrimp, mussels, and freeze-dried seafood. Inhibits psychrotrophic bacterial proliferation and prevents lipid oxidation in high-omega-3 fatty marine fish.
Freeze-Dried Fruits & Veggies
Highly hygroscopic freeze-dried berries, apple slices, and soup vegetables require deep moisture-barrier vacuum packaging or nitrogen backflush to preserve crispy cellular structure and vibrant coloration.
Coffee, Teas & Spices
Volatile aromatic compounds deteriorate rapidly in the presence of oxygen. Vacuum sealing lock-in natural essential oils, roasting freshness, and freshness terpenes in coffee beans and herbal tea leaves.
Cheese & Dairy Specialties
From cheddar blocks to grated parmesan, vacuum sealing retards surface mold growth, maintains optimal internal moisture ratios, and simplifies cold-chain supermarket warehousing.
Grains, Seeds & Dry Mixes
High-volume vacuum bagging creates compact, rigid brick-shaped pouches for rice, quinoa, chia seeds, and flour. Eliminates weevil insect infestation and cuts carton space utilization by 25%.
Technical Comparison: Vacuum System Configurations
Review specifications across machine classes to match your daily production capacity, product format, and shelf-life objectives.
| Machine Model Class | Target Food Commodity | Vacuum Efficiency | Cycle Speed | Pouch Compatibility | Gas Flush Option |
|---|---|---|---|---|---|
| Single-Chamber Vacuum Packer | Batch Meats, Cheese, Specialty Items | ≤ 0.1 kPa | 1 – 3 cycles / min | PA/PE, Multi-layer Barrier | Optional (N2 / CO2) |
| Double-Chamber Industrial Packer | Seafood, Poultry, Cured Hams | ≤ 0.08 kPa | 3 – 6 cycles / min | Co-extruded, Aluminum Foil | Included |
| Continuous Belt Vacuum System | High-Volume Fresh Produce & Jerky | ≤ 0.05 kPa | 6 – 12 cycles / min | Thermoforming film, Premade bags | Included |
| Multi-Lane Vacuum SFFS / Sachet | Coffee Powder, Spices, Freeze-Dried | ≤ 0.2 kPa | 40 – 150 packs / min | Laminated Foil, Retort film | High-Speed MAP |
| Thermoforming Vacuum Packaging | Bacon, Ready Meals, Sausages | ≤ 0.05 kPa | 10 – 25 cycles / min | Flexible & Rigid Rollstock | Full MAP System |
Maximizing Return on Investment with Automated Vacuum Sealing
3X to 5X Shelf Life Multiplication
Vacuum sealing mitigates aerobic spoilage pathways, extending cold storage shelf-life for fresh meats from 3 days to over 21 days, and dry products from 6 months to 24+ months, opening long-distance export corridors.
Drastic Reduction in Food Spoilage
Supermarkets and supply chain partners experience up to a 60% reduction in inventory waste caused by oxidation, mold spotting, freezer drying, and pouch seal leaks during logistics transit.
Freight & Warehouse Compression
Extracting excess air dramatically decreases pouch volume. Tightly packed rectangular or vacuum-conformed packages reduce master carton dimensions, optimizing pallet density and ocean container freight costs.
Total Quality Assurance in Food Processing
Every Ludyway vacuum packaging machine features integrated seal inspection checkpoints, digital heating control loops, and optional date-coding systems. Whether packaging organic grains or sterile medical foods, our systems guarantee hermetic seal integrity that passes dye penetration and bubble emission tests.
State-of-the-Art Production & Global Engineering Footprint
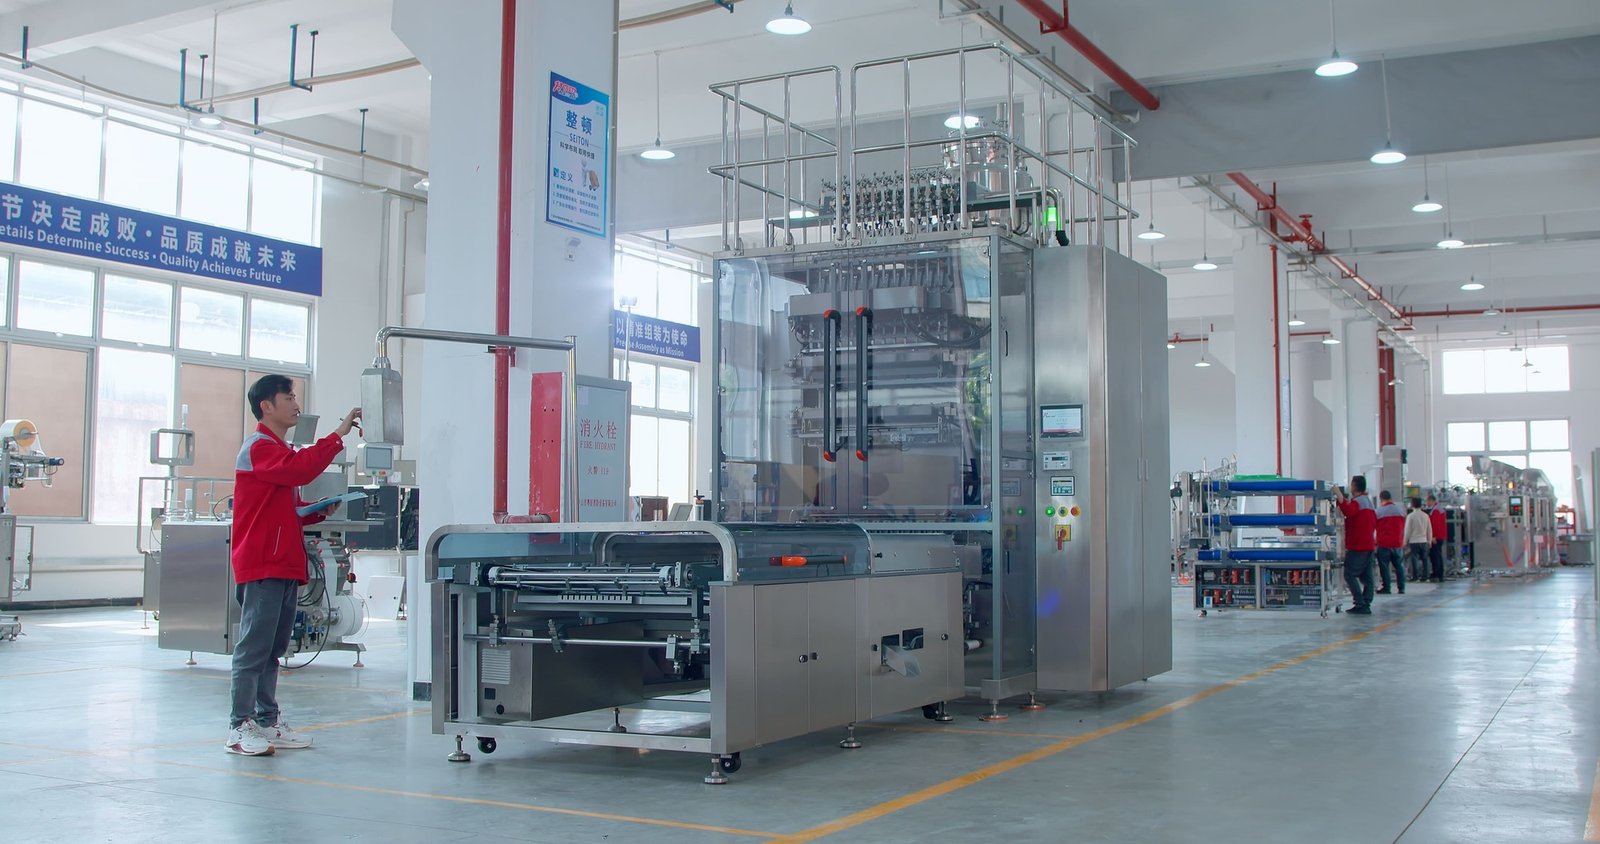
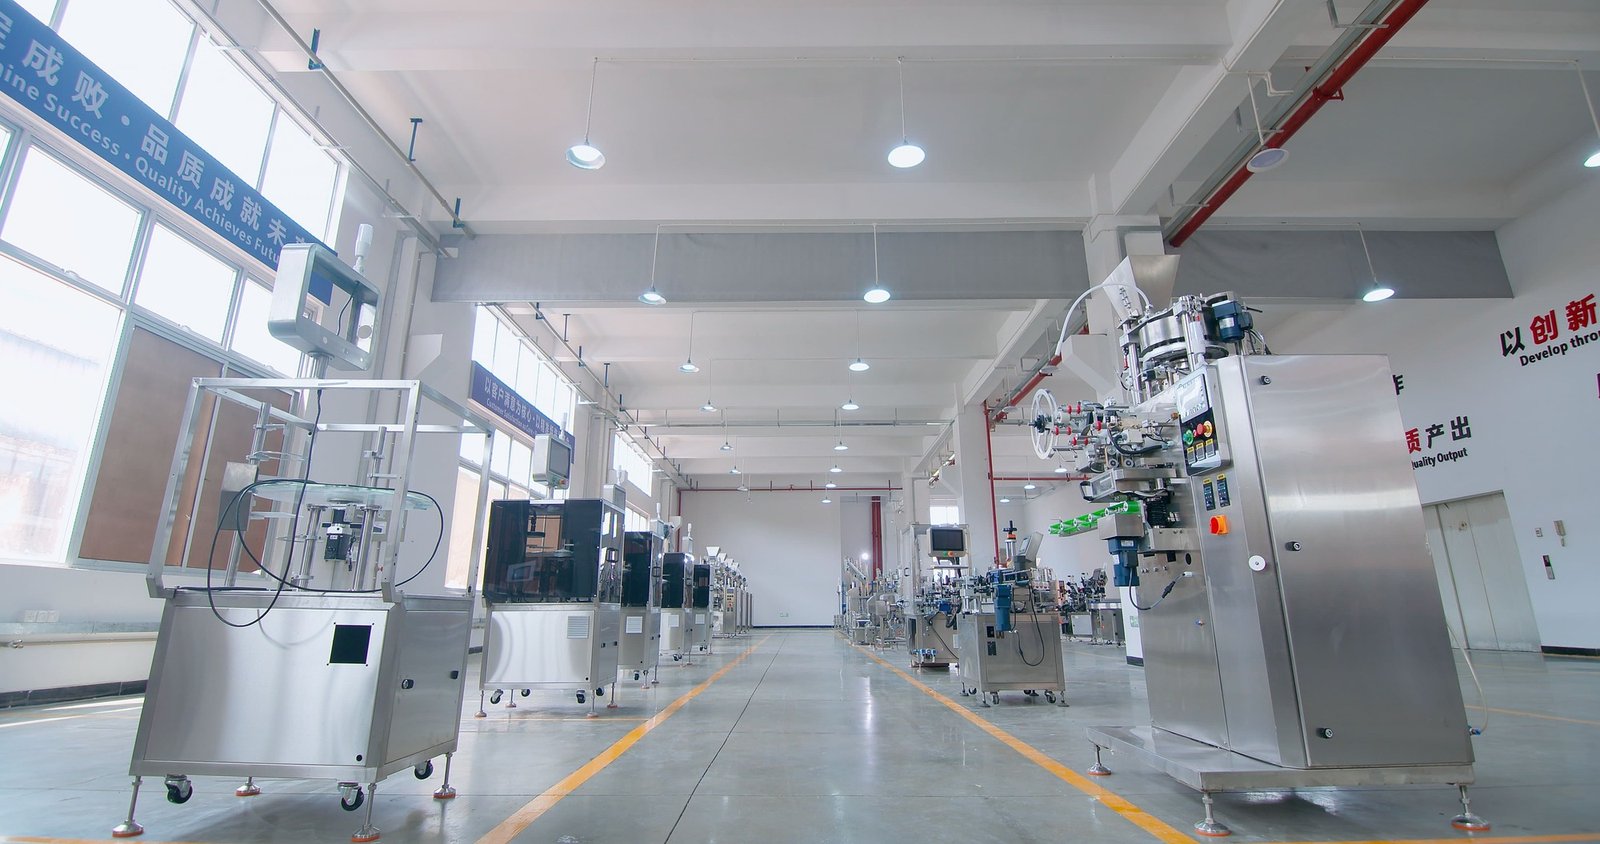
20,000㎡ Smart Machinery Workshop
Equipped with CNC laser cutting, automated 5-axis machining centers, and ultrasonic welding units, Ludyway fabricates over 200 units of advanced packaging equipment monthly. Every machine undergoes 72 hours of continuous dry-run testing before international container loading.
Our global service team provides remote commissioning, on-site installation, operator training, and comprehensive spare parts supply across North America, Europe, Southeast Asia, and South America.
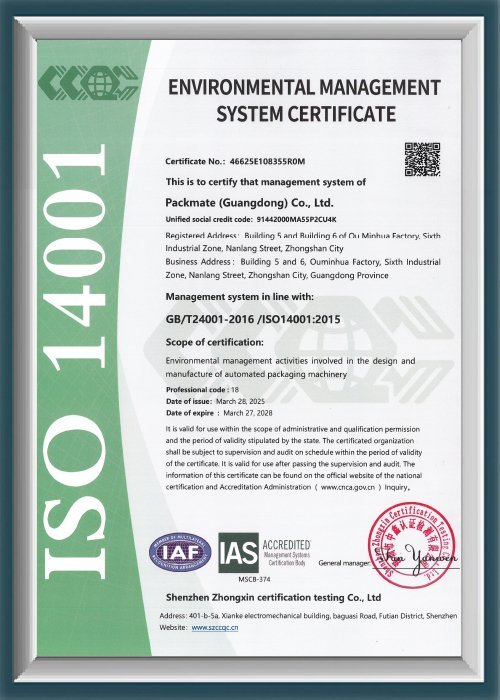
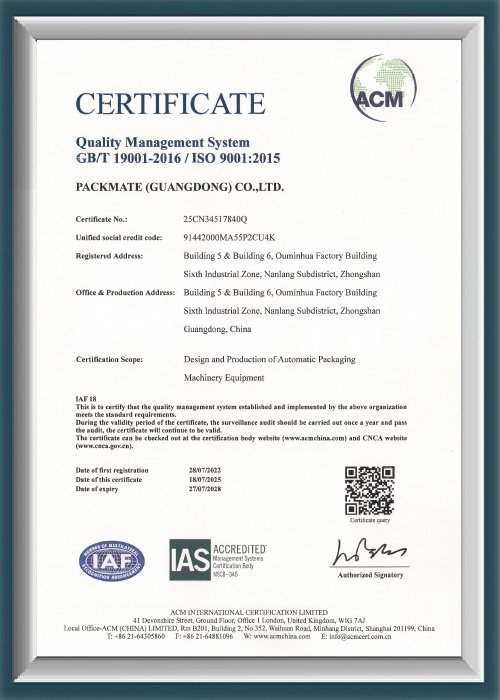
Trusted by Multinational Food & Pharmaceutical Brands
How to Select the Right Food Vacuum Packaging Machine
1. Food Texture & Physical State
Liquids and semi-liquids (sauces, curries) require slanted chamber plates or specialized liquid vacuum sealing algorithms to avoid boil-over under negative pressure. Powders require specialized exhaust deceleration valves, whereas bone-in meats need puncture-tested seal jaws.
2. Production Volume & Daily Throughput
Calculate required packages per minute (PPM). Small batch processors thrive on tabletop or double-chamber units (500–2,000 packs/shift). Continuous high-volume facilities need automated conveyorized belt machines or multi-lane continuous rotary form-fill-seal units (10,000+ packs/shift).
3. Barrier Film & Pouch Structure
Ensure thermal seal jaw heating elements match your film chemistry. Standard PA/PE vacuum bags seal easily; heavy aluminum laminates or high-barrier EVOH shrink films require elevated, precisely calibrated sealing pressure and rapid water-cooled jaw cycles.
4. Plant Sanitation & Washdown Protocols
Food processing environments handling raw meat, dairy, or seafood demand IP65/IP67 rated electrical enclosures, seamless stainless steel laser-welded frames, and quick-release conveyor belts for daily chlorine or high-pressure chemical washdowns.
Food Vacuum Packaging Machines: Frequently Asked Questions
What is the difference between standard vacuum packing and MAP (Modified Atmosphere Packaging)?
Standard vacuum packaging evacuates virtually all atmospheric air from the pouch, causing the packaging film to collapse tightly around the food product. Modified Atmosphere Packaging (MAP) first creates a deep vacuum and then back-flushes an engineered gas blend (typically 70% N2 + 30% CO2 or pure Nitrogen) into the bag before sealing. MAP protects fragile snacks from crushing while preventing anaerobic microbial growth.
How do Ludyway vacuum packaging machines handle liquid or high-moisture foods?
Under vacuum pressure, the boiling point of water drops significantly. Ludyway packaging machines feature smart liquid sensors and rapid-seal cutoff parameters. When moisture is detected or preset liquid parameters are triggered, the machine instantly executes the sealing pulse before liquid can froth out of the pouch, ensuring clean, strong, leak-proof hermetic seals.
Which packaging pouch materials can be used with your food vacuum machinery?
Our machines support all common industrial food-grade barrier films, including Polyamide/Polyethylene (PA/PE), Oriented Polypropylene (BOPP), Aluminum Foil (AL) multi-layer structures, EVOH high-barrier laminates, retort pouches, and emerging certified compostable/biodegradable vacuum films.
What maintenance is required for commercial vacuum pumps?
Standard preventive maintenance involves regularly checking the pump oil sight glass, replacing vacuum pump oil and exhaust oil mist filters every 500 to 1,000 operational hours (depending on moisture load), and cleaning the chamber silicone sealing gaskets. Ludyway machines include automated maintenance alert prompts on the touchscreen interface.
Can Ludyway customize vacuum packing lines to integrate into existing production conveyors?
Yes. As a full-service machinery manufacturer with a 20,000㎡ plant, we engineer turnkey custom solutions. We integrate automatic checkweighers, multi-head weighers, metal detectors, bucket elevators, robotic arm loaders, and carton packing systems into continuous automated lines.
What warranty and after-sales support does Ludyway provide for international clients?
We provide a comprehensive 12 to 24-month warranty on structural components, Siemens/Omron PLCs, and vacuum pump assemblies. Our engineering team provides 24/7 video technical support, rapid air delivery of modular spare parts, and on-site field installation and engineer training upon request worldwide.
Accelerate Your Food Packaging Line with Ludyway Automation
Whether you need a dedicated industrial vacuum packaging machine, a multi-lane stick pack system, or a complete turnkey food processing line, our senior packaging engineers are ready to tailor an optimal solution for your plant.
