Best Vacuum Packaging Machine for Food Packaging
Engineered for absolute hermetic seal integrity, maximum shelf-life extension, and high-throughput automated food processing. Experience high-efficiency vacuum degassing, MAP gas flushing, and micro-precision chamber control.
Why Modern Food Processors Require Advanced Vacuum Degassing
In modern food manufacturing, selecting the best vacuum packaging machine transcends simple pouch sealing. It dictates biochemical preservation kinetics, microbial barrier thresholds, and product stability across the global cold chain.
Inhibition of Aerobic Spoilage
Atmospheric oxygen (approx. 20.9% O₂) is the primary catalyst for enzymatic browning, lipid rancidity, and the proliferation of aerobic microbes like Pseudomonas and molds. High-vacuum extraction draws pressure down to < 5 mbar, virtually eliminating free oxygen.
Shelf-Life Boost Increases standard refrigerated shelf life by 300% to 500% compared to atmospheric containment.
Freeze-Burn & Moisture Control
For frozen foods and freeze-dried delicacies, sublimated moisture migration leads to dry, oxidized surfaces. Skin-tight vacuum pouches form an impenetrable micro-barrier, arresting moisture loss and cryo-damage during sub-zero storage.
Weight Retention Eliminates surface desiccation and preserves exact target batch weight throughout logistical cycles.
Volumetric & Shipping Efficiency
Eliminating head-space gas collapses package volume by up to 45%. This enables ultra-dense tertiary carton packing, optimizes container payload utilization, and drops maritime and freight emissions per kilogram of food delivered.
Logistics ROI Cuts cold chain pallet freight costs substantially across domestic and cross-border distribution.
Featured Industrial Vacuum & Food Packaging Machines
Select from our precision-engineered machinery lineup built with food-grade SUS304/SUS316 stainless steel, heavy-duty rotary vane vacuum pumps, and intelligent digital sealing controls.
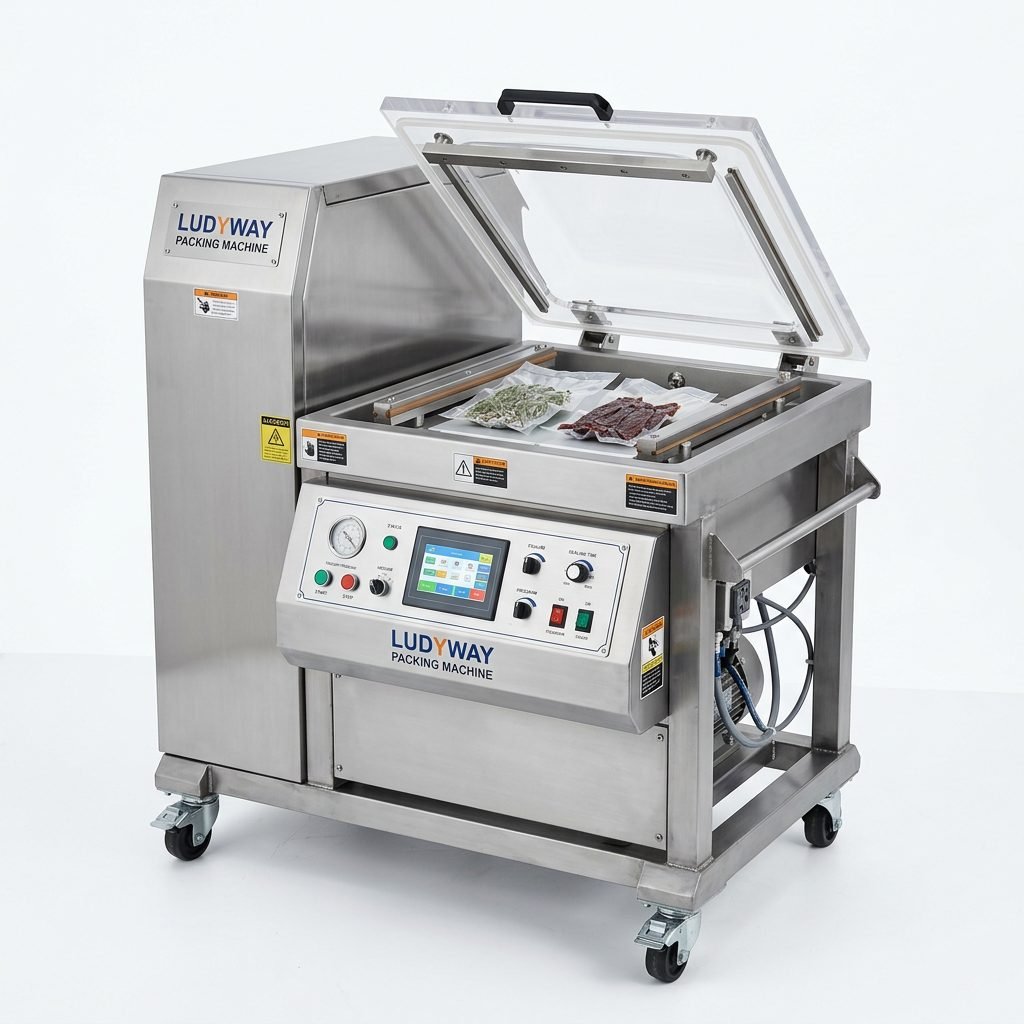
Industrial Vacuum Packaging Machine for Food & Pharma
- Heavy-duty Busch vacuum pump integration
- Ultimate vacuum: ≤ 0.1 KPa pressure
- Digital cycle timing with auto chamber lift
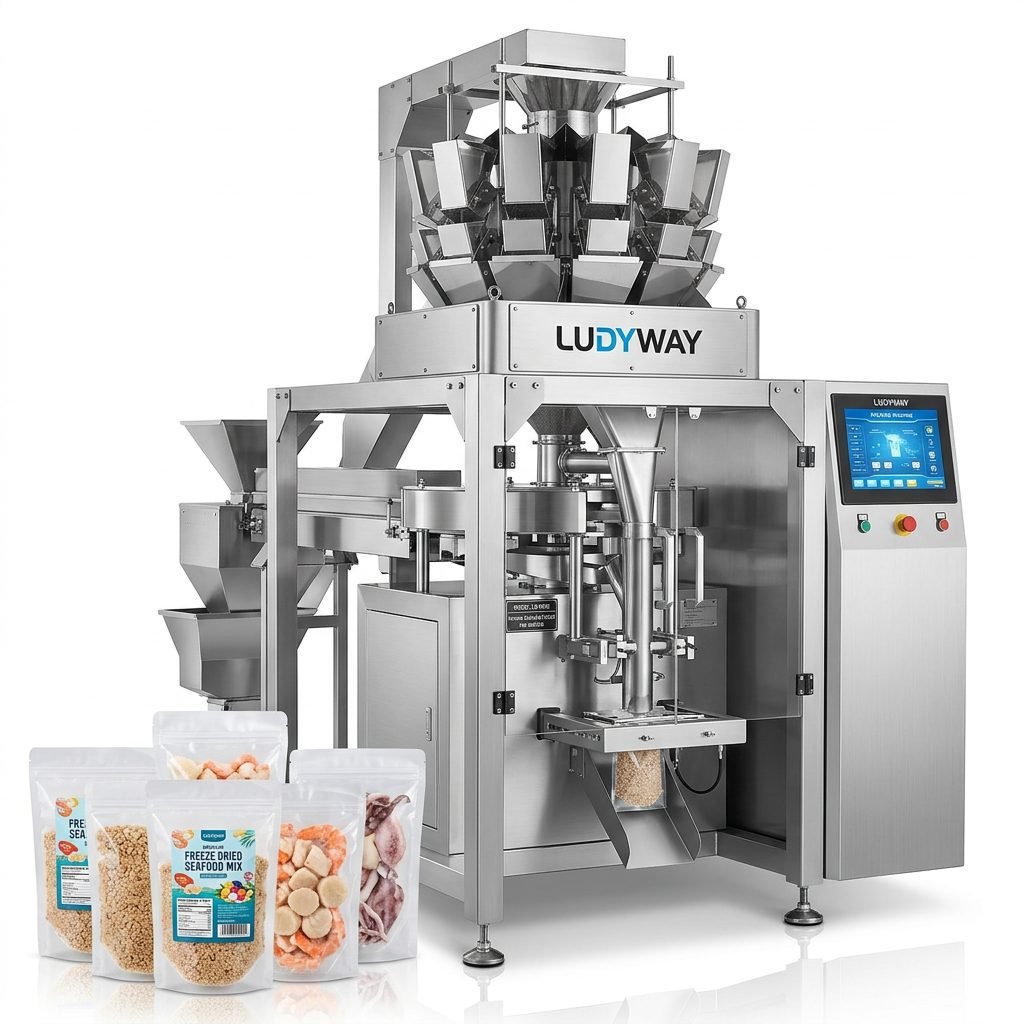
Freeze Dried Seafood Vacuum Sealing Machine
- Zero-crush micro-atmosphere evacuation
- Double impulse sealing bar protection
- Washdown IP65 sanitary stainless housing
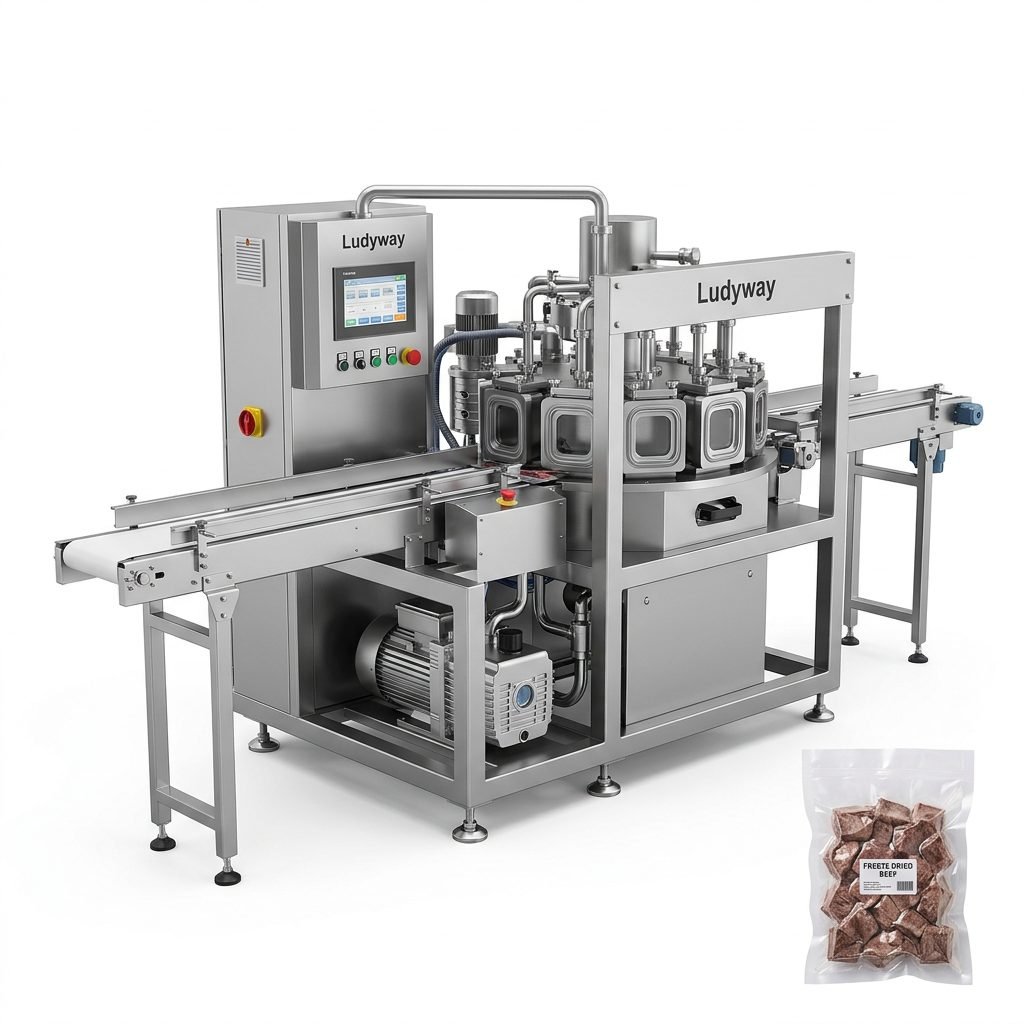
Freeze Dried Beef Vacuum Packaging System
- Continuous conveyor feeding integration
- High-speed multi-cycle sealing capability
- Puncture-resistant vacuum pouch handling
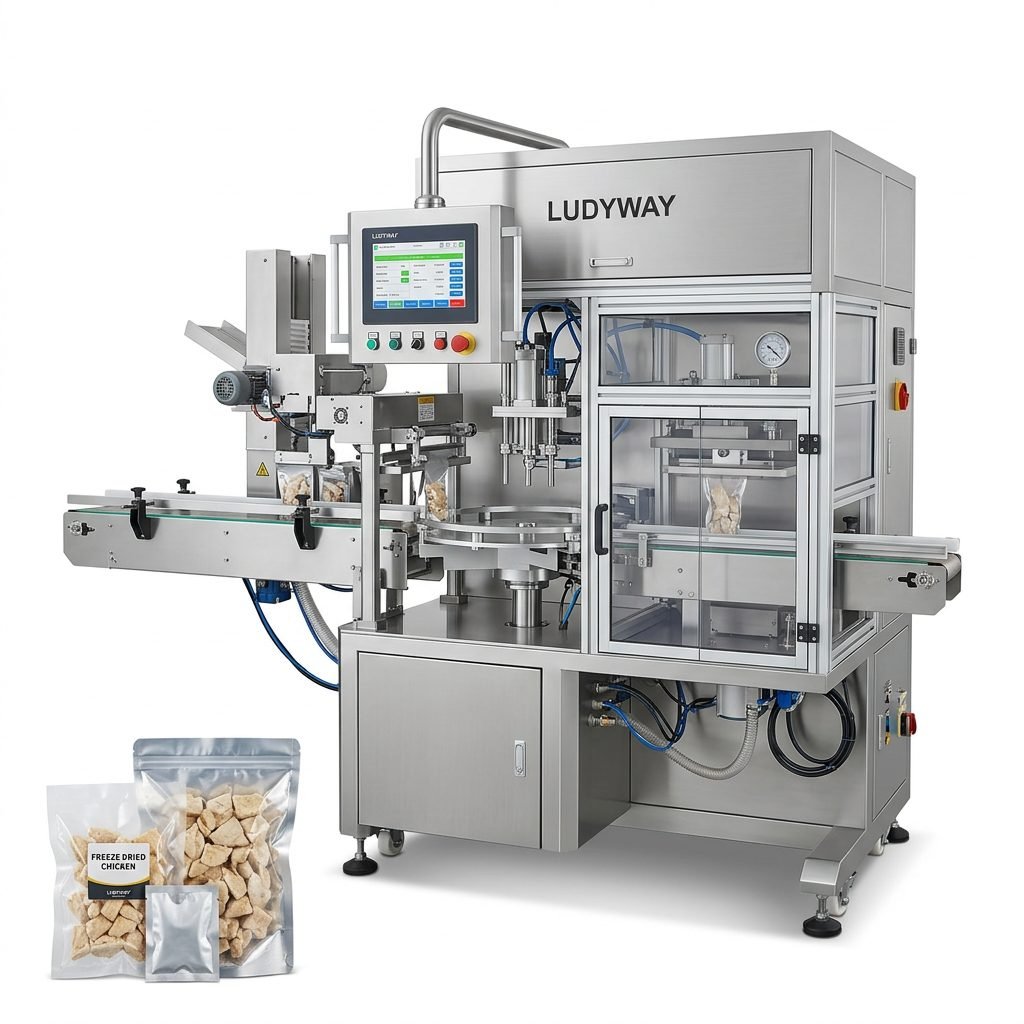
Freeze Dried Chicken Vacuum Packaging Machine
- Custom pouch/sachet format adaptability
- Precision pneumatic pressure calibration
- Residual oxygen reduction below 0.1%
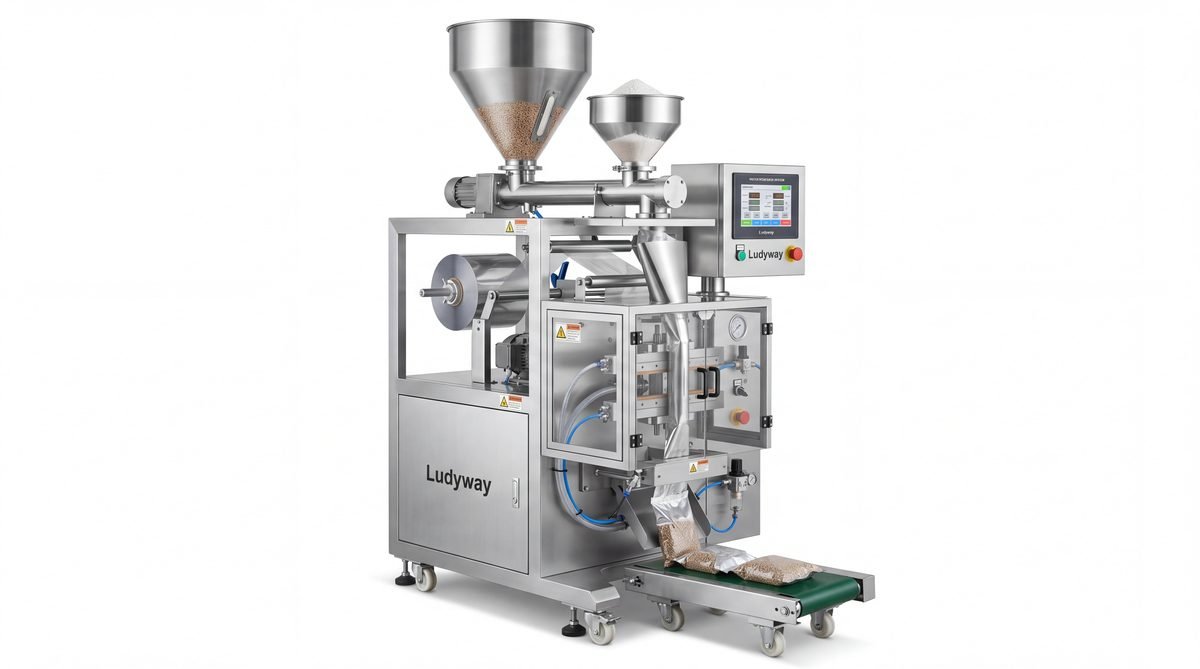
Vacuum Packaging Machine for Granule & Powder
- Anti-dust aspiration filter mechanisms
- Compact footprint with heavy-duty castors
- Multi-recipe storage via Siemens HMI touch
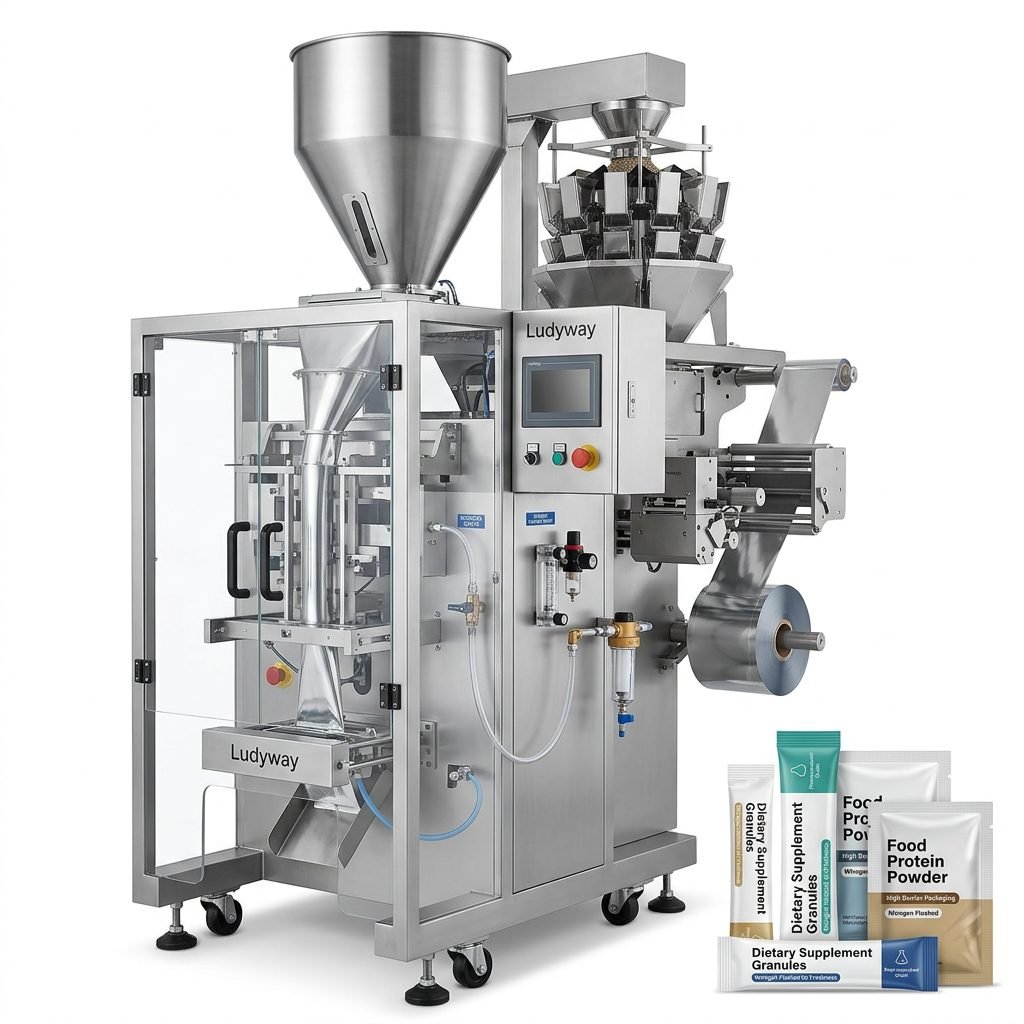
Nitrogen Flushing Packaging System (MAP)
- Combined deep vacuum & N₂ back-flush
- Cushion packaging for fragile snack items
- Gas mixing accuracy within ± 0.5% tolerance
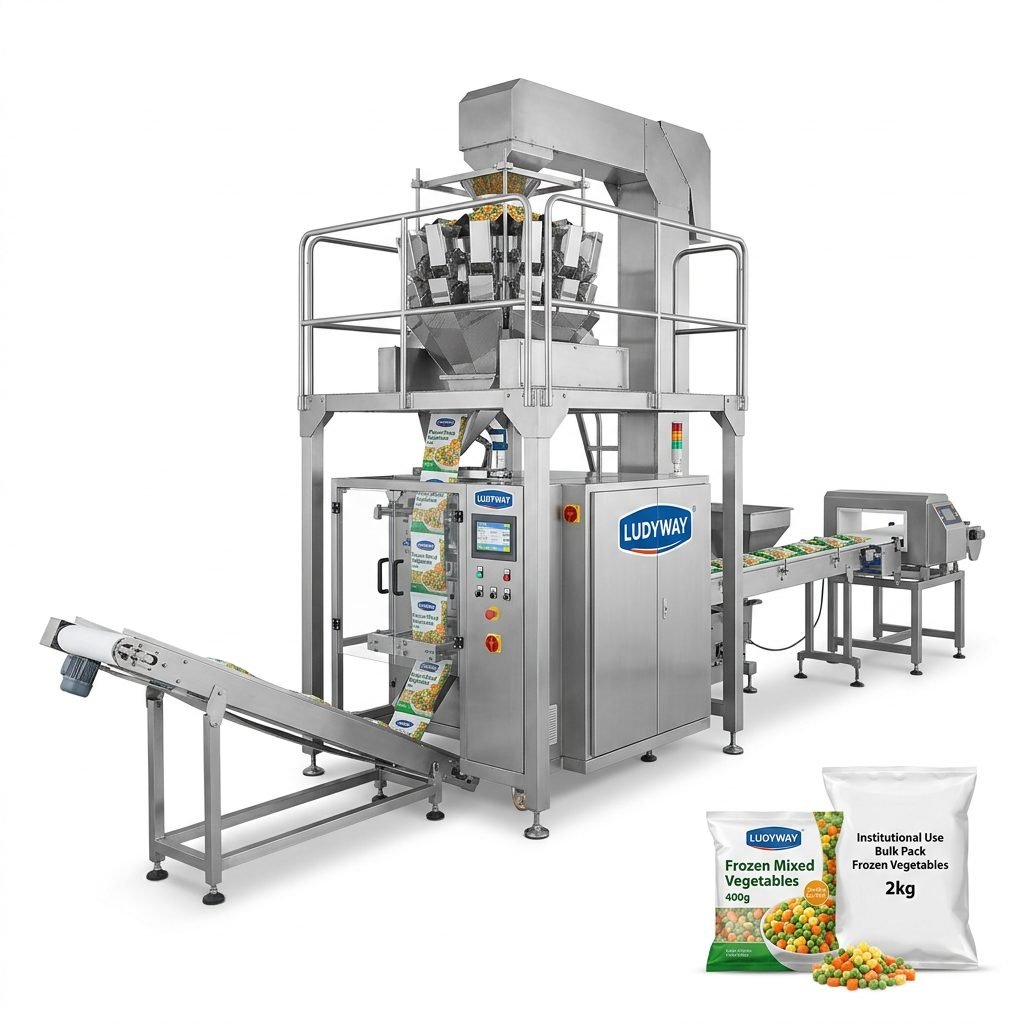
High-Speed Frozen Food Packaging Lines
- Automated portion control multi-head scale
- Cold-resistant pneumatic and electrical lines
- Continuous high-volume production output
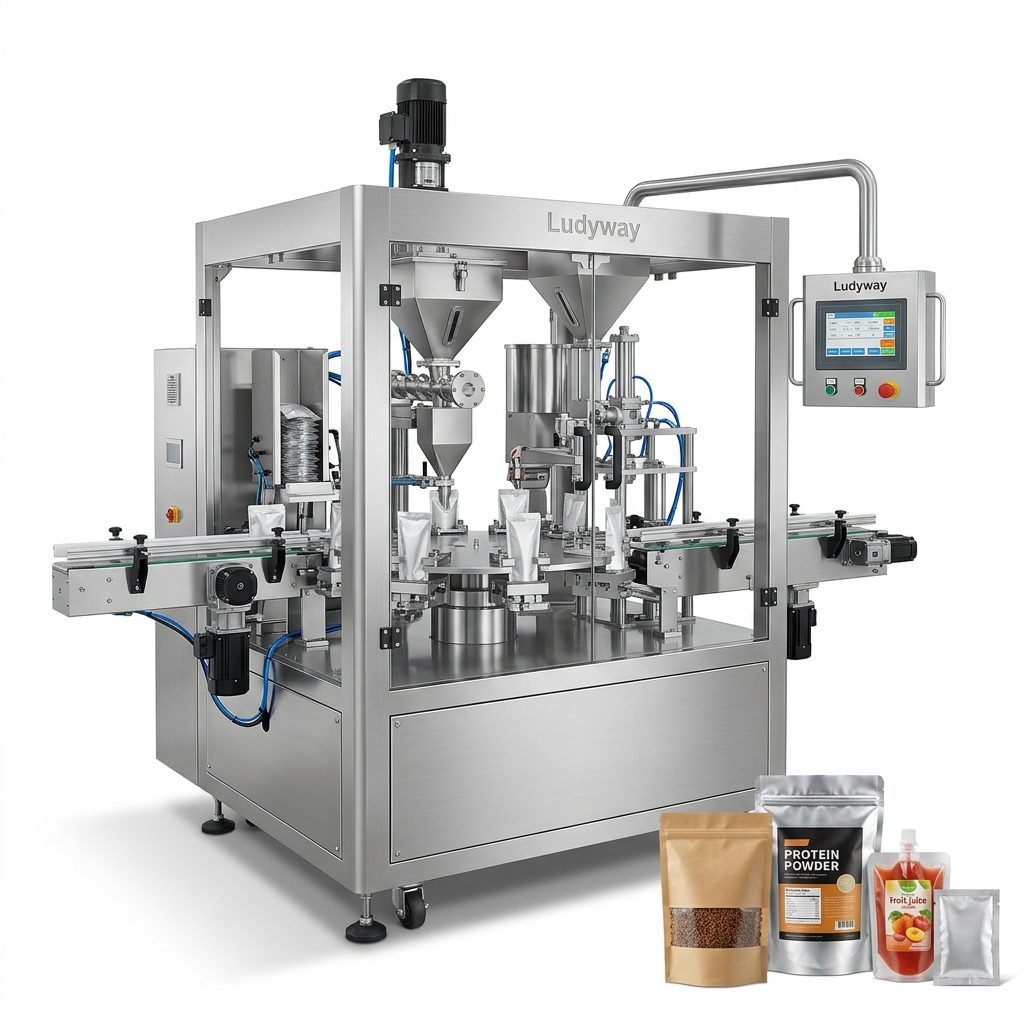
Premade Rotary Vacuum Pouch Machine
- Rotary 8-station high-speed vacuum indexing
- Handles stand-up, zip-lock, and retort bags
- Automatic pouch pick, open, fill, vacuum & seal
How to Select the Best Vacuum Packaging Machine for Food
To maximize operational equipment effectiveness (OEE) and prevent packaging line bottlenecks, evaluating machinery requires understanding chamber physics, pump throughput, and thermodynamic sealing controls.
| Machine Category | Primary Food Applications | Evacuation Speed | Throughput Capacity | Key Technical Strength |
|---|---|---|---|---|
| Single Chamber Tabletop/Floor | Artisan cheeses, charcuterie, pilot labs | 15–30 sec/cycle | 2–6 bags/min | Low footprint, quick tool-less changeover |
| Double Chamber Heavy-Duty | Fresh primal meats, frozen poultry, wholesale seafood | 12–25 sec/cycle | 12–30 bags/min | Non-stop oscillating chamber efficiency |
| Continuous Automatic Belt | High-volume cured bacon, block cheeses, retort packs | 8–15 sec/cycle | 30–60 bags/min | Automated belt infeed & discharge line integration |
| Rotary Premade Pouch Vacuum | Ready-to-eat (RTE) meals, nuts, pet food kibble | Continuous rotary | 40–80 bags/min | Zero manual bag loading, full PLC automated line |
| Thermoforming Vacuum/Skin (VSP) | Premium steaks, fresh fish fillets, sliced deli meats | Continuous rollstock | 60–120 packs/min | Lowest material cost/pack, stunning retail presentation |
1. Vacuum Pump Volumetric Flow (m³/h)
The heart of any packaging system is its rotary vane vacuum pump. Industrial lines require oil-lubricated high-capacity pumps (e.g., Busch 63 m³/h to 300 m³/h). Inadequate flow leads to long cycle lags, high oxygen residuals, and incomplete bag contraction.
2. Temperature & Impulse Sealing Controls
Multi-layer barrier bags (PA/PE, EVOH, Aluminum foil) require uniform heat dissipation. Ludyway integrates bi-active impulse sealing with water-cooled or aluminum-backed seal jaws to ensure zero burn-through and 100% airtight seams.
3. Sanitary Washdown Design (IP65/IP69K)
Food hygiene regulations demand rigorous caustic sanitation. Ensure the chassis features sloping drainage surfaces, 304/316 grade stainless steel construction, and completely sealed electrical cabinets to withstand daily high-pressure washdown.
Smart Sensor Feedback & Quality Assurance Systems
Achieve absolute consistency across millions of packaging cycles with intelligent process automation, real-time pressure diagnostics, and machine learning calibration.
Absolute Pressure Sensor Monitoring vs. Simple Timers
Traditional entry-level sealers use rudimentary timing loops, which fail to compensate for altitude shifts, pouch humidity, or volume variances. Ludyway food vacuum systems feature high-precision piezoresistive digital vacuum sensors that dynamically sense boiling points and stop evacuation precisely at the threshold of moisture evaporation, safeguarding product moisture while hitting <0.1% O₂.
Multi-Stage Modified Atmosphere Packaging (MAP) Injection
For delicate products such as fresh berry medleys, chips, or fragile freeze-dried proteins, simple hard vacuum causes product crushing. Our systems execute a programmable multi-step sequence: deep vacuum evacuation followed by precision inert gas back-flushing (N₂ / CO₂ / O₂ blends) to provide structural cushion and bacteriostatic protection.
Predictive Maintenance & OEE Line Telemetry
Equipped with industrial Siemens PLC controls and IoT cloud gateways, our packaging lines track cycle speed, pump oil breakdown indices, heating ribbon degradation, and seal pressure deviations in real time. Maintenance alerts prevent unexpected line downtime, ensuring uninterrupted output across 24/7 food processing facilities.
Tailored Food Packaging Solutions by Product Type
From red meat processing slaughterhouses to high-speed snack packaging factories, our packaging machinery is custom-tooled for specific physical and biological food properties.
Meat, Poultry & Charcuterie
Heavy cuts of bone-in beef, whole poultry, sausages, and cured bacon require puncture-resistant barrier pouches and high-tensile sealing. Our double-chamber and continuous belt machines evacuate air rapidly without drawing blood purge into the sealing track, maintaining pristine seal aesthetics.
Seafood & Aquaculture
Seafood fats oxidize rapidly, causing pungent off-odors and discolored meat. With specialized high-vacuum degas cycles and liquid-trap filtration, our machinery seals fresh salmon fillets, frozen shrimp, and freeze-dried seafood with zero water weight migration or vacuum seal failure.
Snacks, Nuts, Coffee & Dry Granules
Roasted nuts and whole bean coffee contain volatile aromatic oils vulnerable to staling. Our multi-lane stick pack and premade vacuum systems integrate inert gas flushing, locking in volatile aromas and crisp textures while preventing fragile nuts from crushing.
Bulk Ingredients & Food Powders
Packaging fine starch, flour, milk powder, or seasonings under vacuum presents dusting challenges. Ludyway installs specialized multi-cyclone dust extraction and pulse back-flush valves to ensure no airborne powder contaminates the sealing bar or enters the vacuum chamber pump.
About Ludyway Packaging Machinery
Your trusted global manufacturing partner for high-efficiency packaging lines and automated turnkey plant solutions.
Over 30 Years of Advanced Packaging Engineering
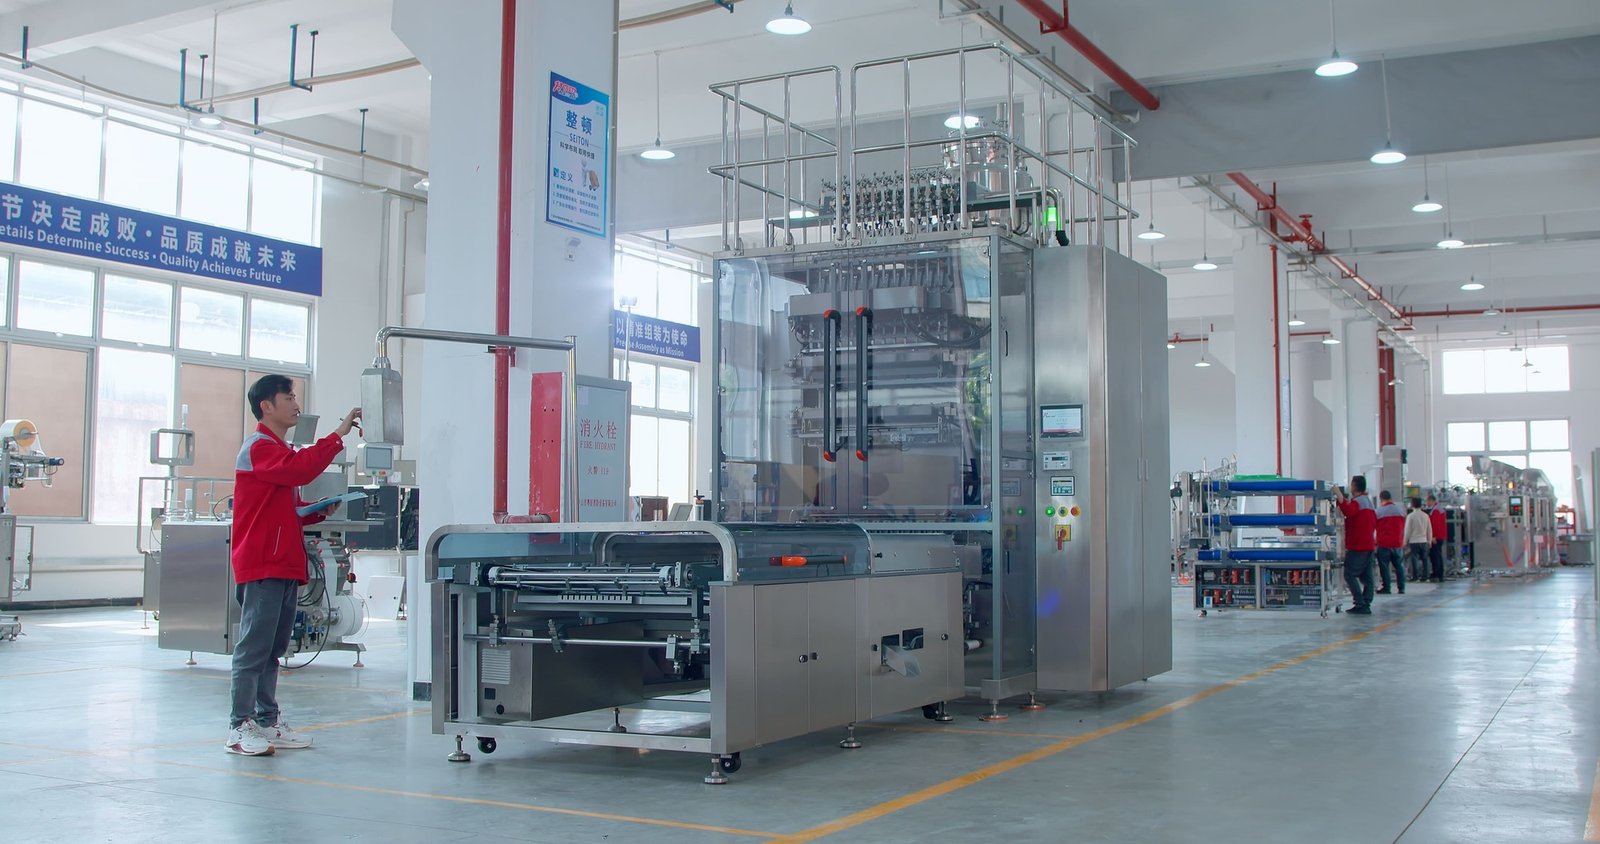
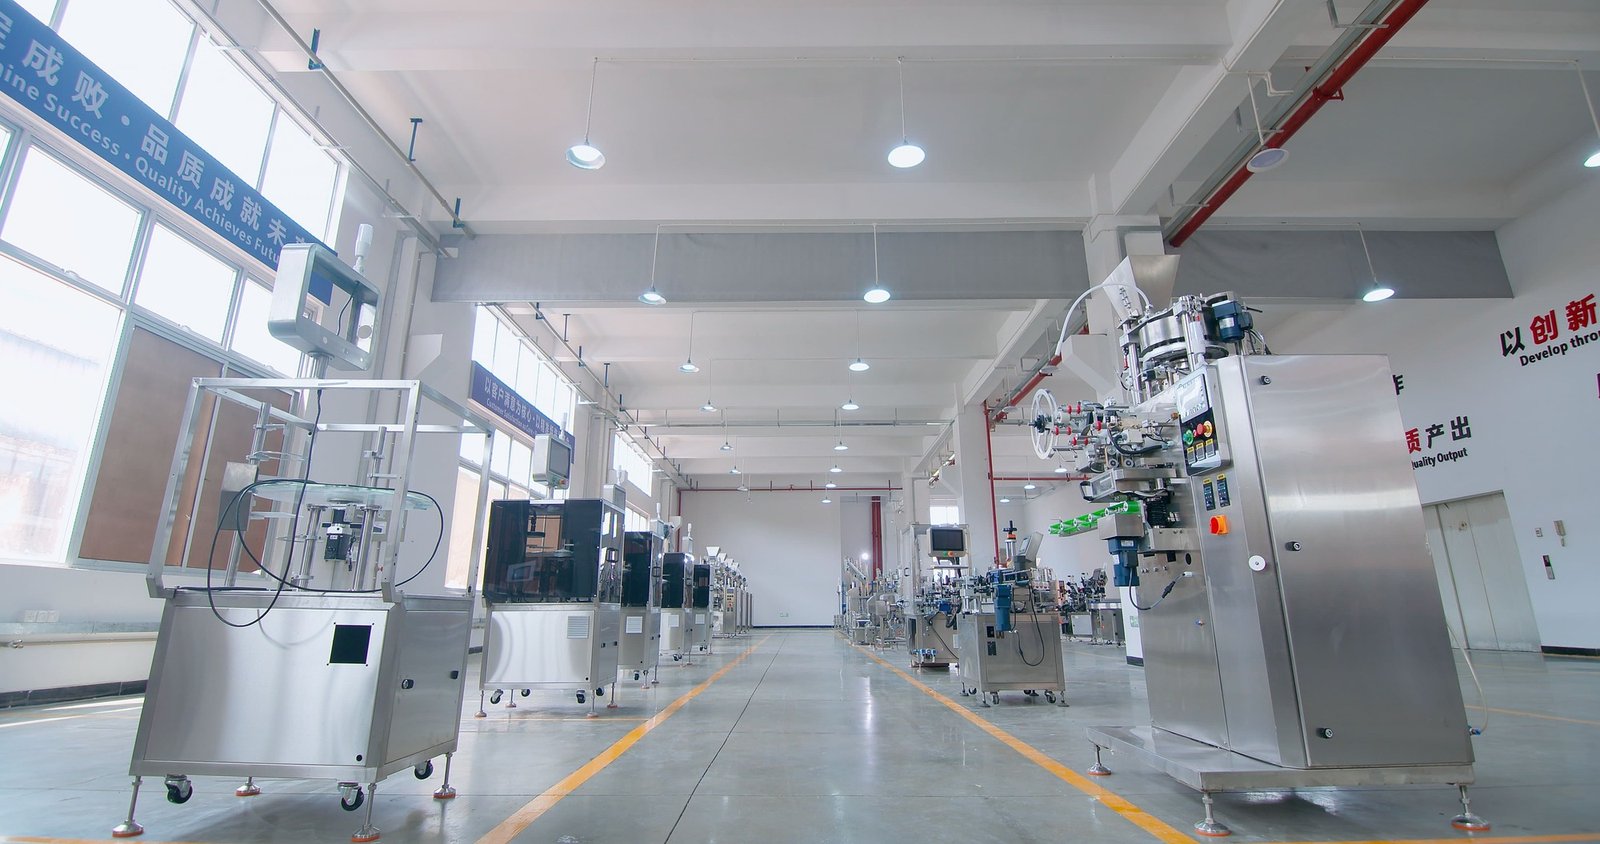
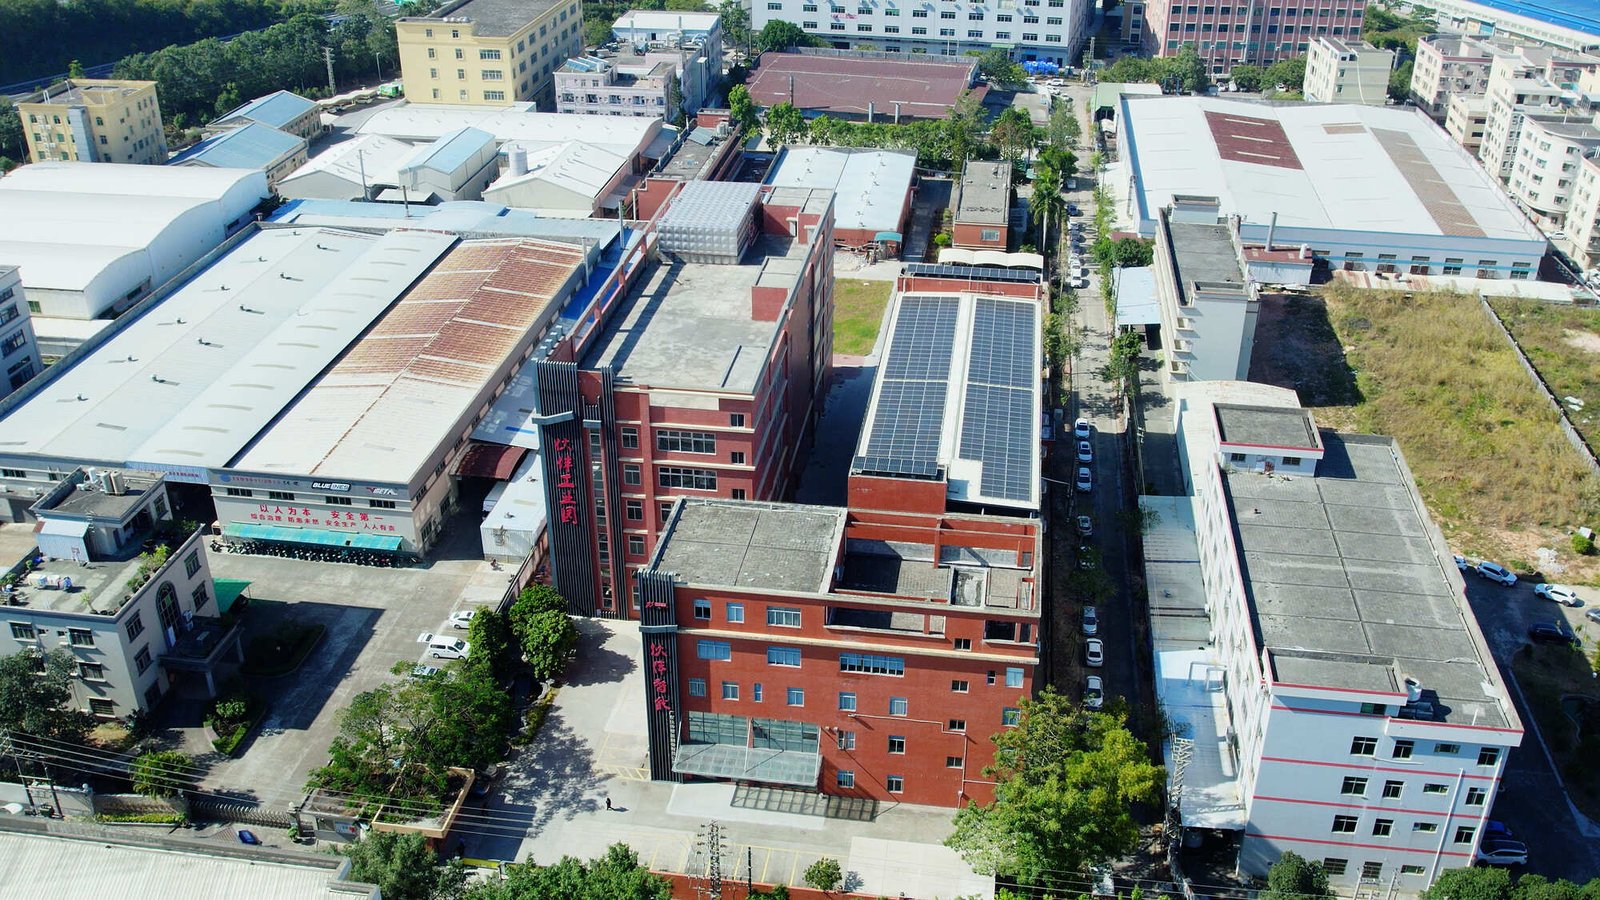
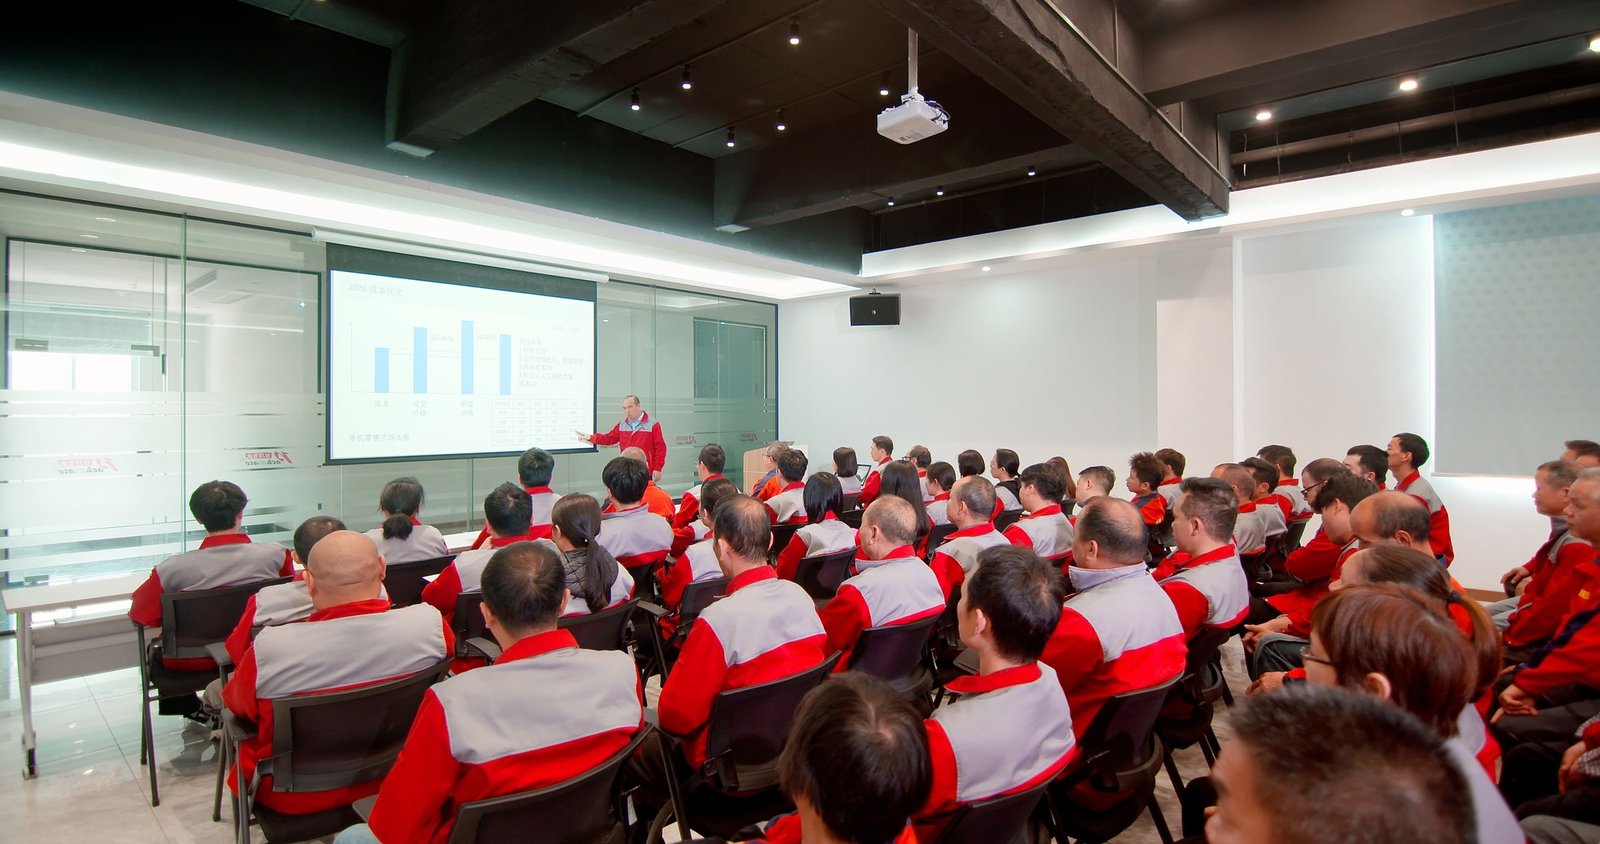
Ludyway is one of the largest packaging machine manufacturers in China, specializing in advanced packaging equipment and turnkey production solutions for the food, pharmaceutical, and health industries. Supported by a modern 20,000㎡ manufacturing facility and a team of 130+ professional packaging experts, Ludyway manufactures more than 50 intelligent packaging machine models.
Serving customers in over 100 countries and regions, we provide multi-lane stick pack, sachet, continuous rotary, and high-vacuum sealing systems tailored to elevate product shelf-life, production throughput, and brand prestige.
Certified Quality & Worldwide Presence
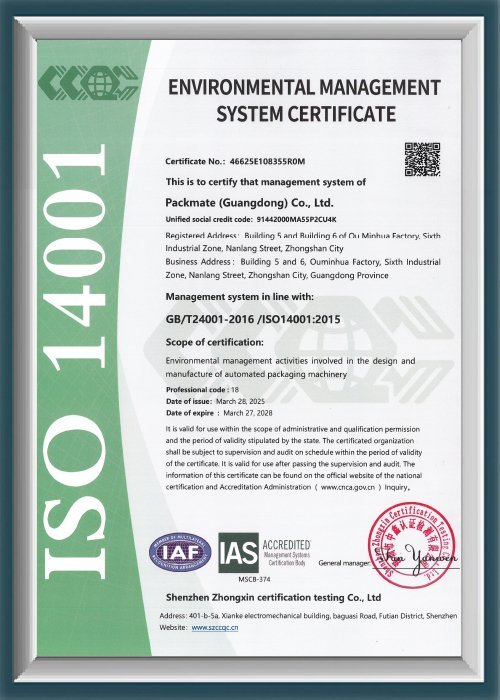
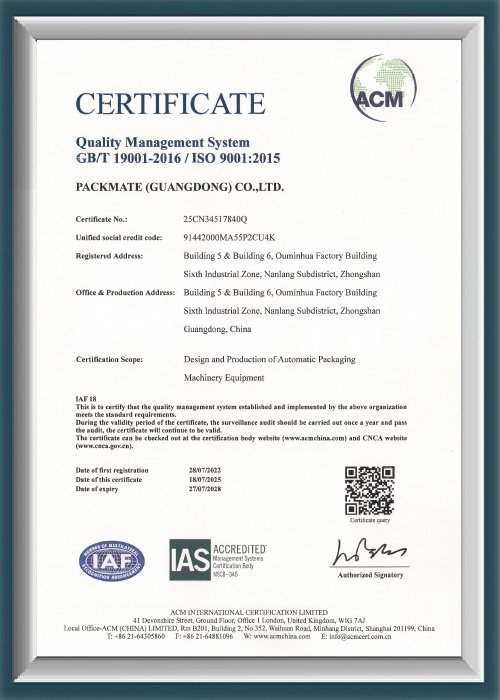
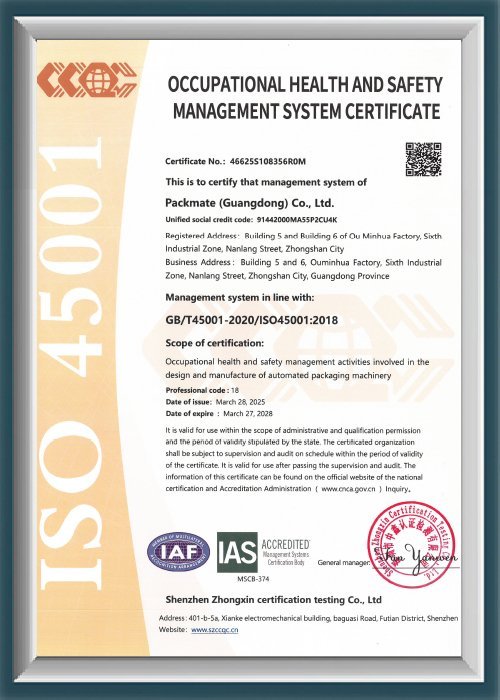
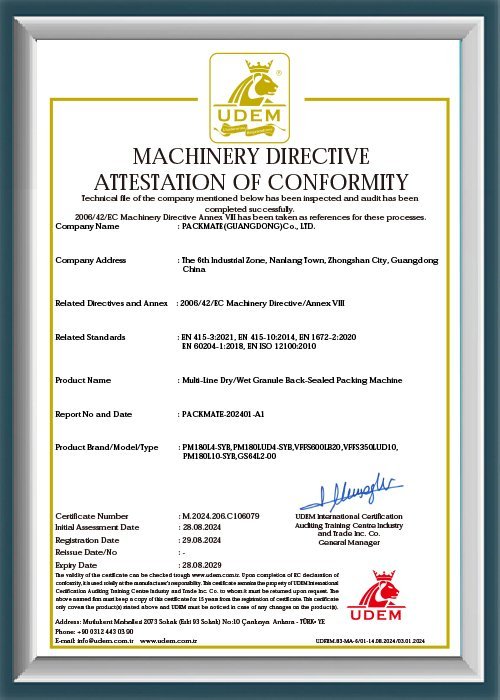
Fully certified under international CE, ISO9001, and sanitary food contact machinery directives, Ludyway equipment powers leading packaging plants across Europe, the Americas, Asia, and the Middle East.
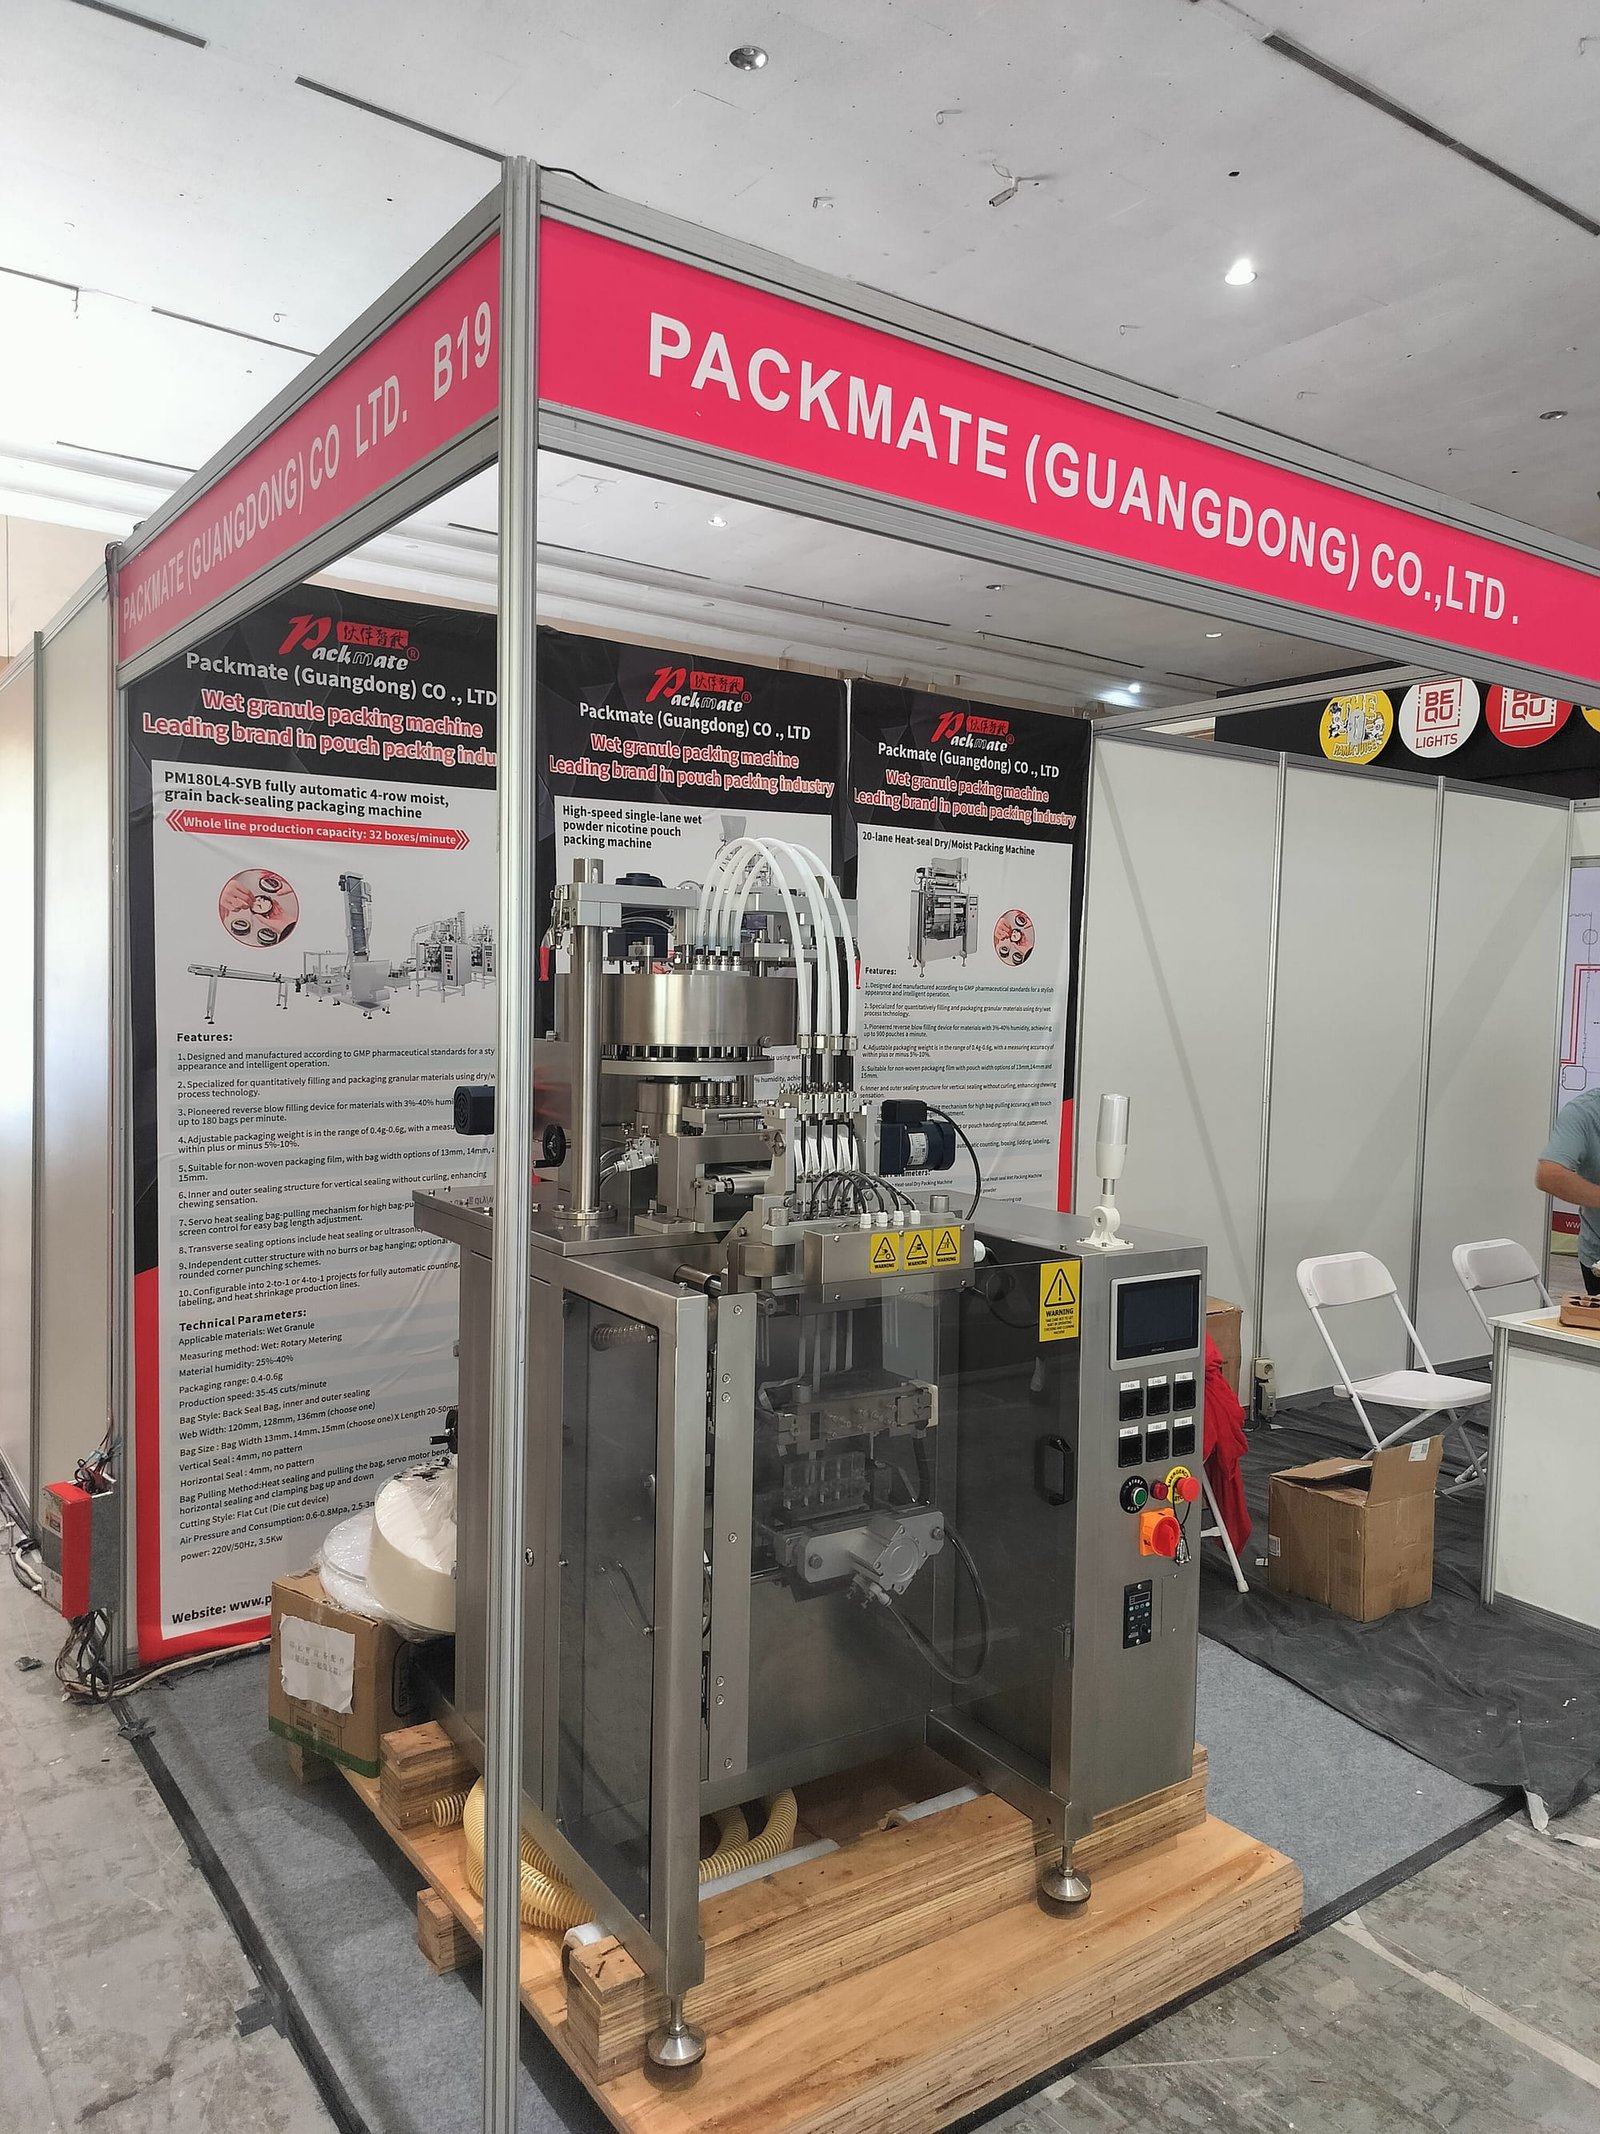
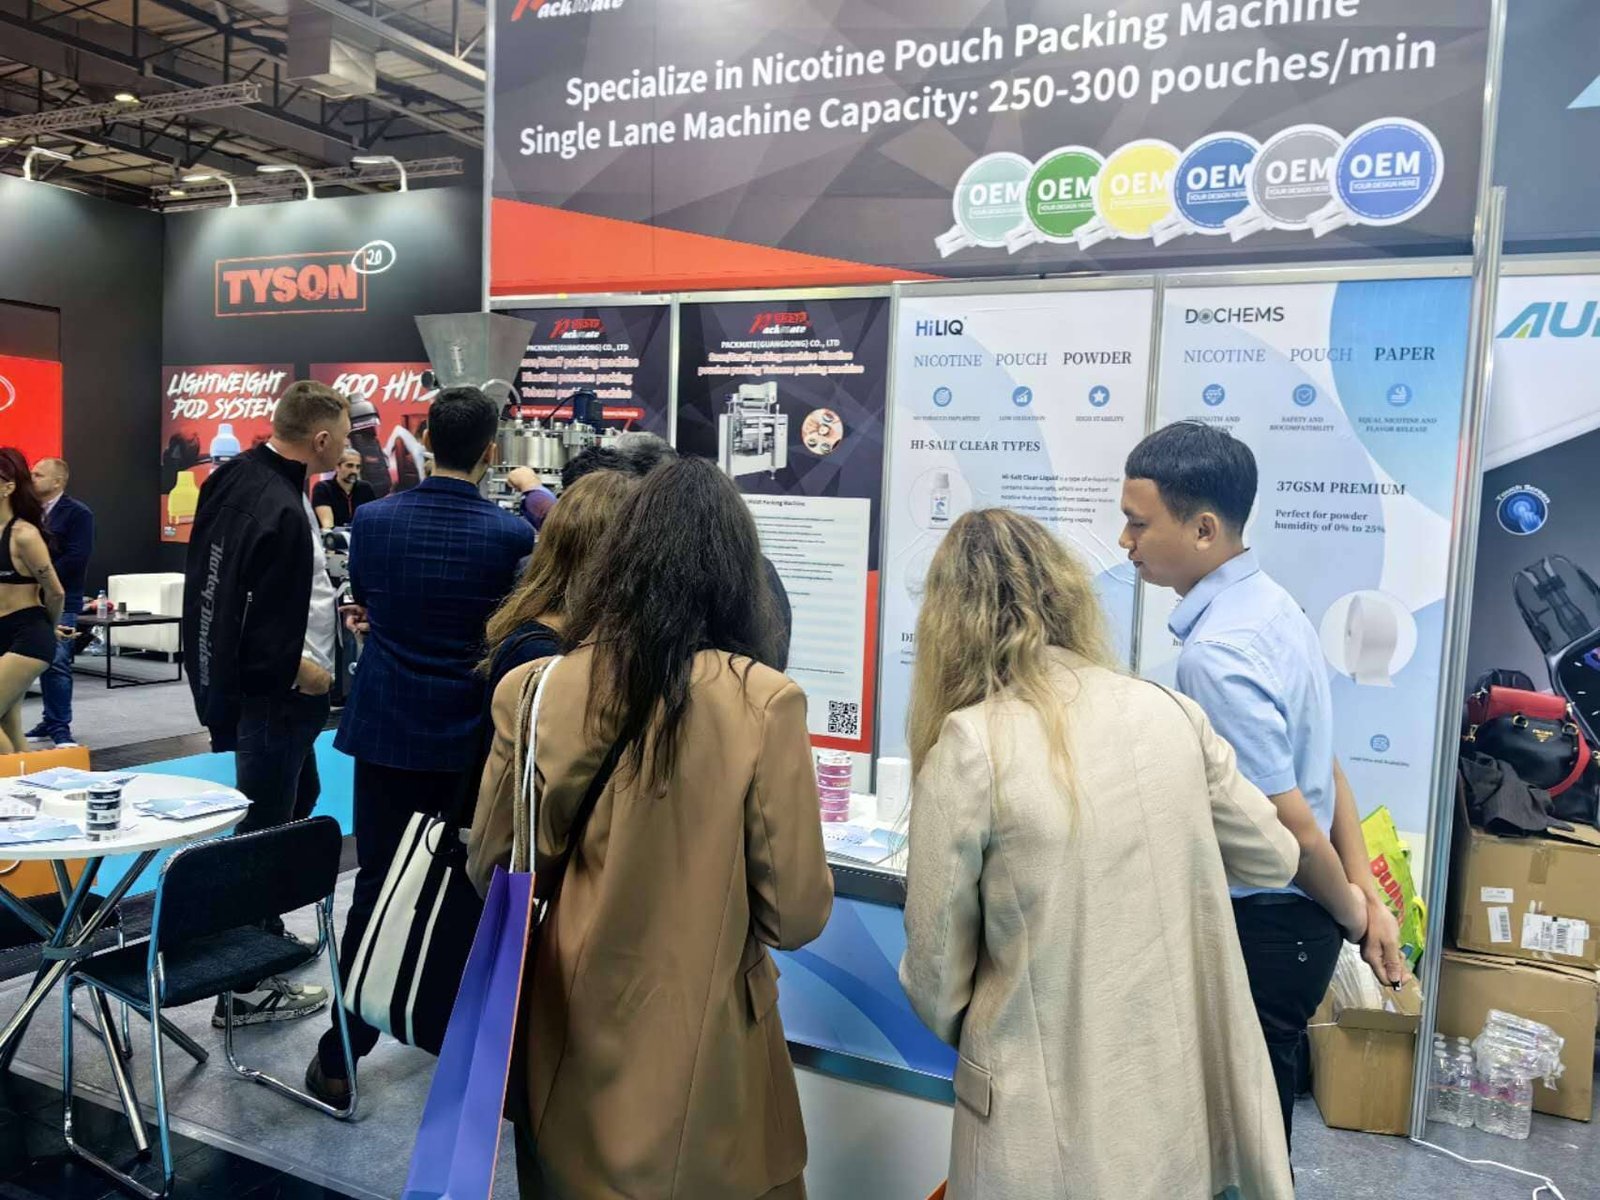
Exhibiting Worldwide at Premier Packaging Expos
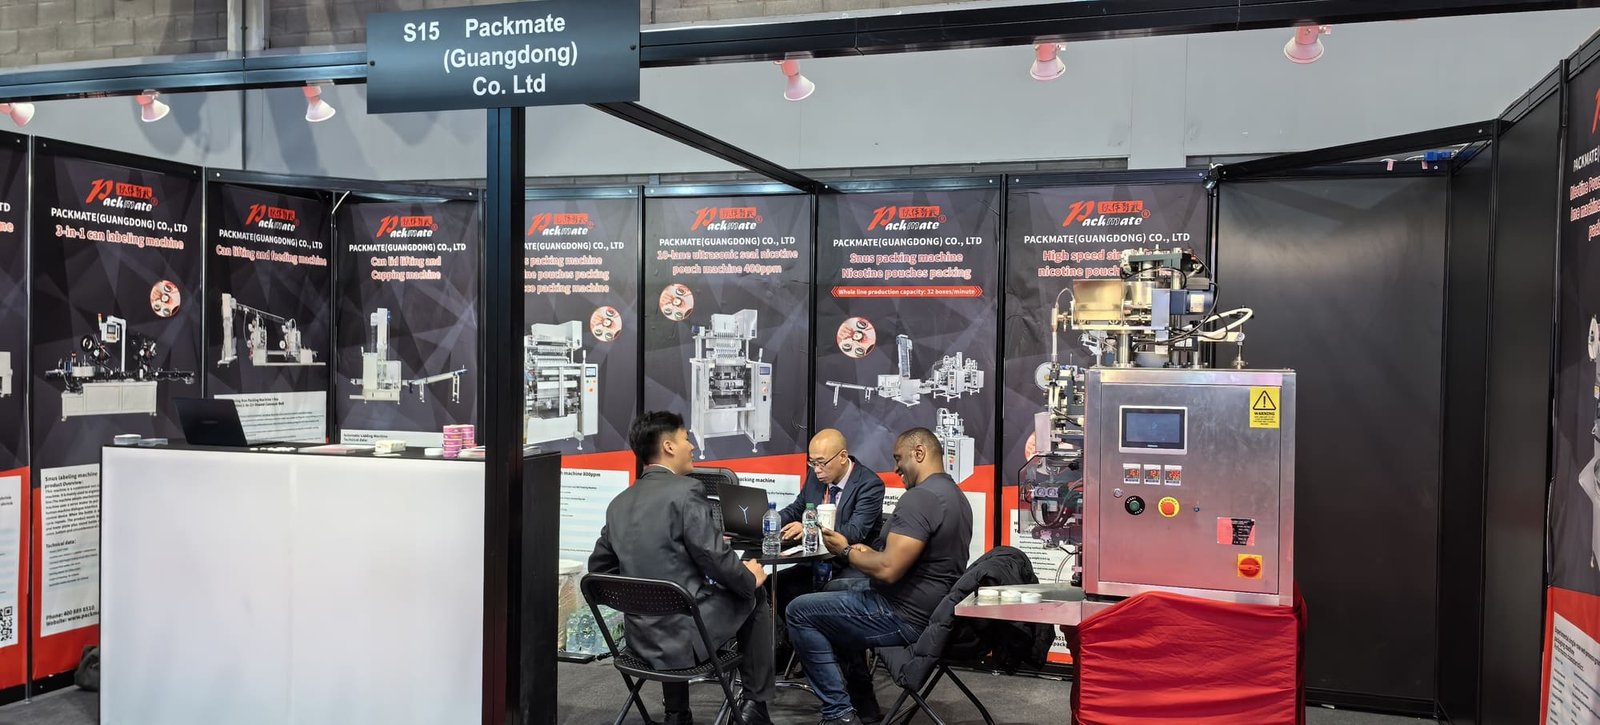
From Interpack Germany to ProPak Asia and Pack Expo USA, meet our technical team live on site.
Food Vacuum Packaging Machine FAQs
Clear, engineering-focused answers to help you size, configure, and optimize your commercial food packaging line.
1. What is the difference between chamber vacuum packaging and external suction sealers?
Chamber vacuum machines place the entire pouch inside an airtight vessel, evacuating air equally inside and outside the pouch. This allows liquid, sauce, and high-moisture foods to be sealed without suction pull. External sealers clamp only the bag neck and cannot handle liquids or deliver true industrial vacuum levels (<10 mbar).
2. Which pouch materials are compatible with industrial vacuum sealers?
Industrial machines typically run co-extruded multi-layer pouches including PA/PE (Polyamide/Polyethylene), EVOH high-barrier films, aluminum-metalized barrier laminates, and retortable CPP pouches with thicknesses ranging from 60 to 180 microns.
3. How does Modified Atmosphere Packaging (MAP) differ from pure vacuum?
Pure vacuum removes ambient atmosphere until the pouch clings tightly to the product. MAP first pulls a deep vacuum and then back-flushes a specialized gas mix (such as 70% N₂ + 30% CO₂). This preserves shape, prevents crushing fragile chips or salads, and inhibits anaerobic bacterial growth.
4. How often does a commercial vacuum pump require oil maintenance?
For rotary vane vacuum pumps (e.g., Busch/Becker), oil changes are typically required every 500 to 1,000 operational hours, or immediately if moisture contamination causes milkiness in the oil sight glass. Regular oil changes ensure pump longevity and consistent evacuation speed.
5. Can Ludyway vacuum packaging machines integrate into automated conveyor lines?
Yes. Our continuous belt vacuum machines and rotary premade pouch packaging systems are engineered for full integration with multi-head weighers, automated pick-and-place robots, metal detectors, checkweighers, and automatic case cartoning lines.
6. How is seal integrity validated for strict food safety compliance (HACCP/FDA)?
Ludyway machines provide digital seal parameter logging (temperature, dwell time, sealing pressure). In-line non-destructive seal inspection sensors and external methylene blue vacuum dye immersion tanks can be utilized to guarantee hermetic compliance with zero pinhole leaks.
Ready to Upgrade Your Food Vacuum Packaging Performance?
Connect with our senior packaging engineers today for customized chamber drawings, cycle speed calculations, and tailored factory turnkey solutions.