
High-Performance Vacuum Packaging Machine Technologies for Global Industry
In modern industrial packaging, preserving product freshness, preventing microbiological decay, and shielding sensitive goods from atmospheric humidity and oxidation are absolute imperatives. A high-efficiency vacuum sealer packaging machine extracts ambient oxygen before applying a thermal hermetic seal, significantly extending shelf life and eliminating physical transit damages.
Ludyway engineering combines cutting-edge high-vacuum extraction systems with precision micro-step heat-sealing controls. Designed for flexible pouch formats, bulk barrier bags, and continuous form-fill-seal operations, our vacuum sealing equipment accommodates complex production profiles spanning dry granules, fine powders, raw protein portions, and precision electronic assemblies.
Intelligent Sensor-Driven De-aeration
Equipped with advanced digital piezoresistive pressure gauges, Ludyway vacuum systems automatically optimize chamber evacuation down to ≤0.1 KPa, ensuring uniform barrier film contact without rupturing delicate product structures.
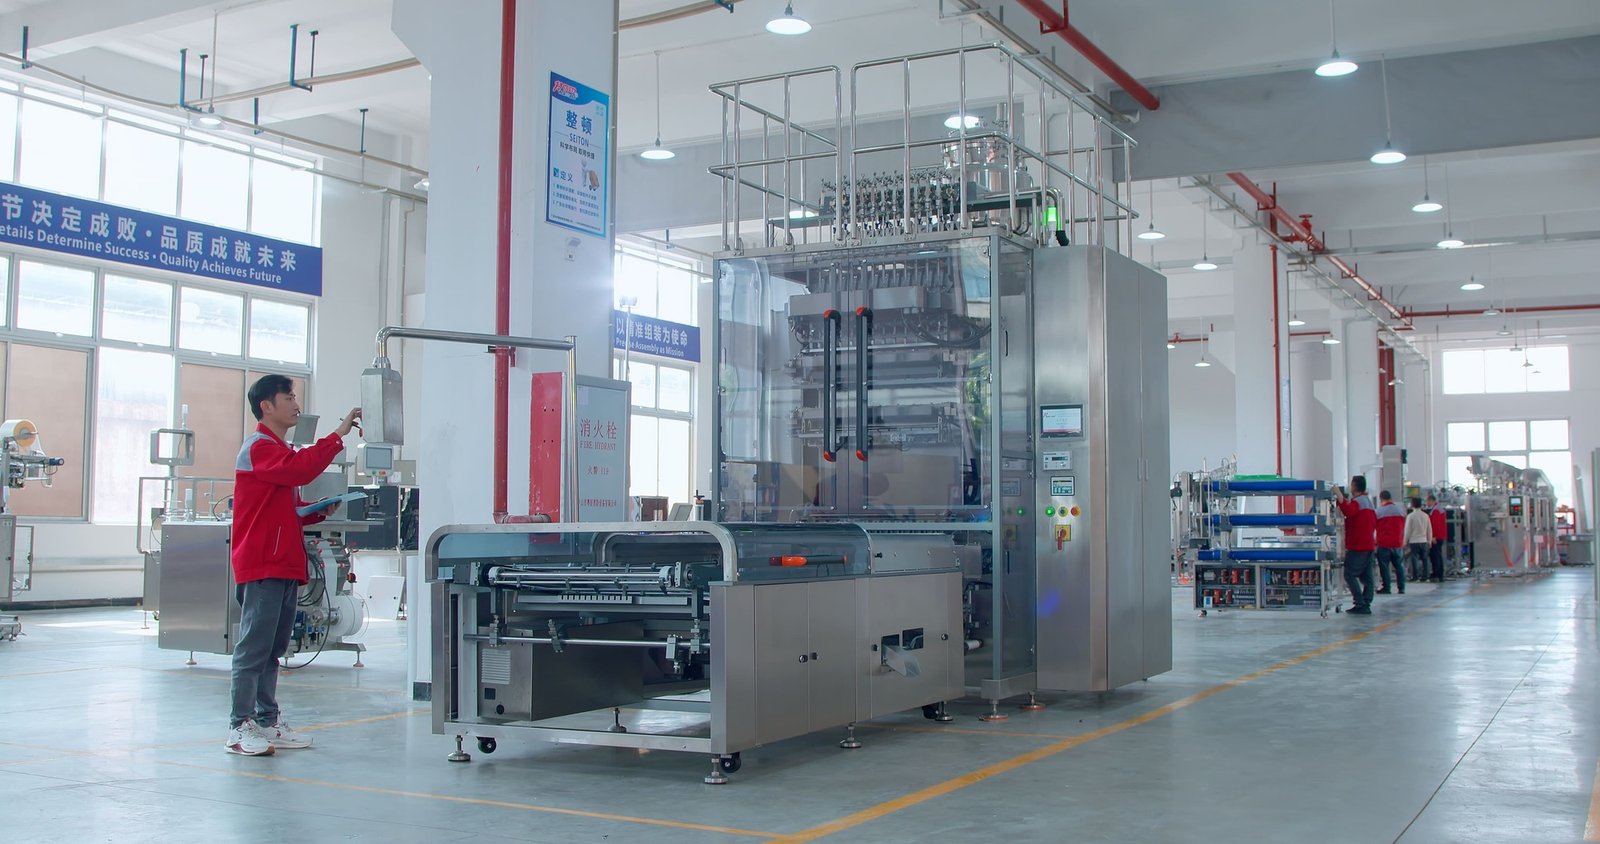
Why Modern Production Relies on Automated Vacuum Sealing
Extended Shelf Life
By lowering residual O2 concentration below 0.5%, aerobic bacterial multiplication and oxidative rancidity in food and nutritional active ingredients are completely suppressed.
Volume Reduction & Cargo Savings
Eliminating internal pouch air volume optimizes freight density by up to 40%, drastically trimming maritime and overland shipping overhead for global distributors.
Moisture & Contamination Barrier
Hermetically sealed high-barrier films prevent environmental moisture absorption, protecting hygroscopic powders, chemicals, and medical devices from degradation.
Gas Flush & MAP Integration
Easily synchronize nitrogen (N2) or carbon dioxide (CO2) flushing modules to cushion fragile freeze-dried snacks and retain delicate produce textures.
High-Speed Continuous Duty
Heavy-duty industrial vacuum pumps and water-cooled heat-sealing bars permit nonstop 24/7 manufacturing without thermal drift or sealing degradation.
Traceable Digital Control
Equipped with Siemens PLC touch interfaces, providing multiparameter recipe management, automated vacuum diagnostics, and full compliance logging.
High-Efficiency Vacuum & Multi-Lane Packaging Systems
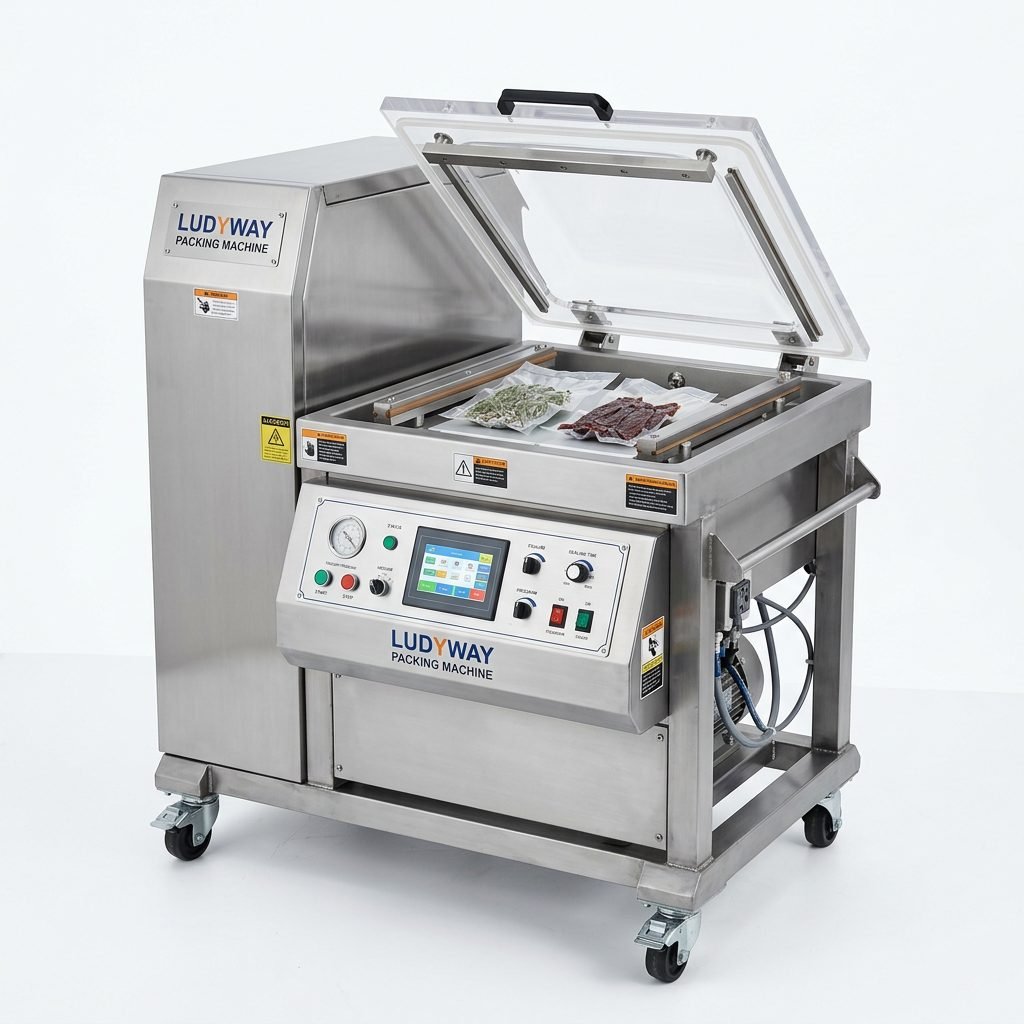
Industrial Vacuum Packaging Machine for Food & Pharma
View System Specs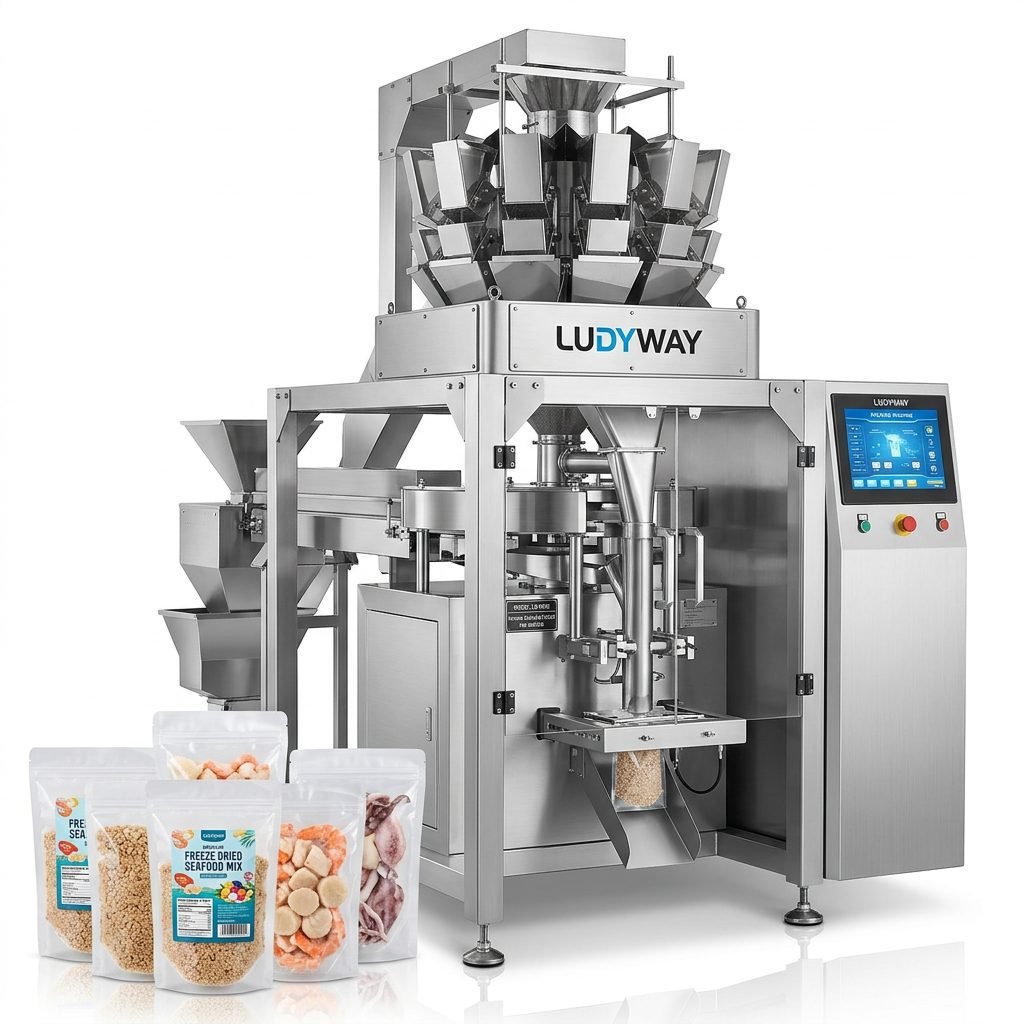
Freeze Dried Seafood Vacuum Sealing Machine
View System Specs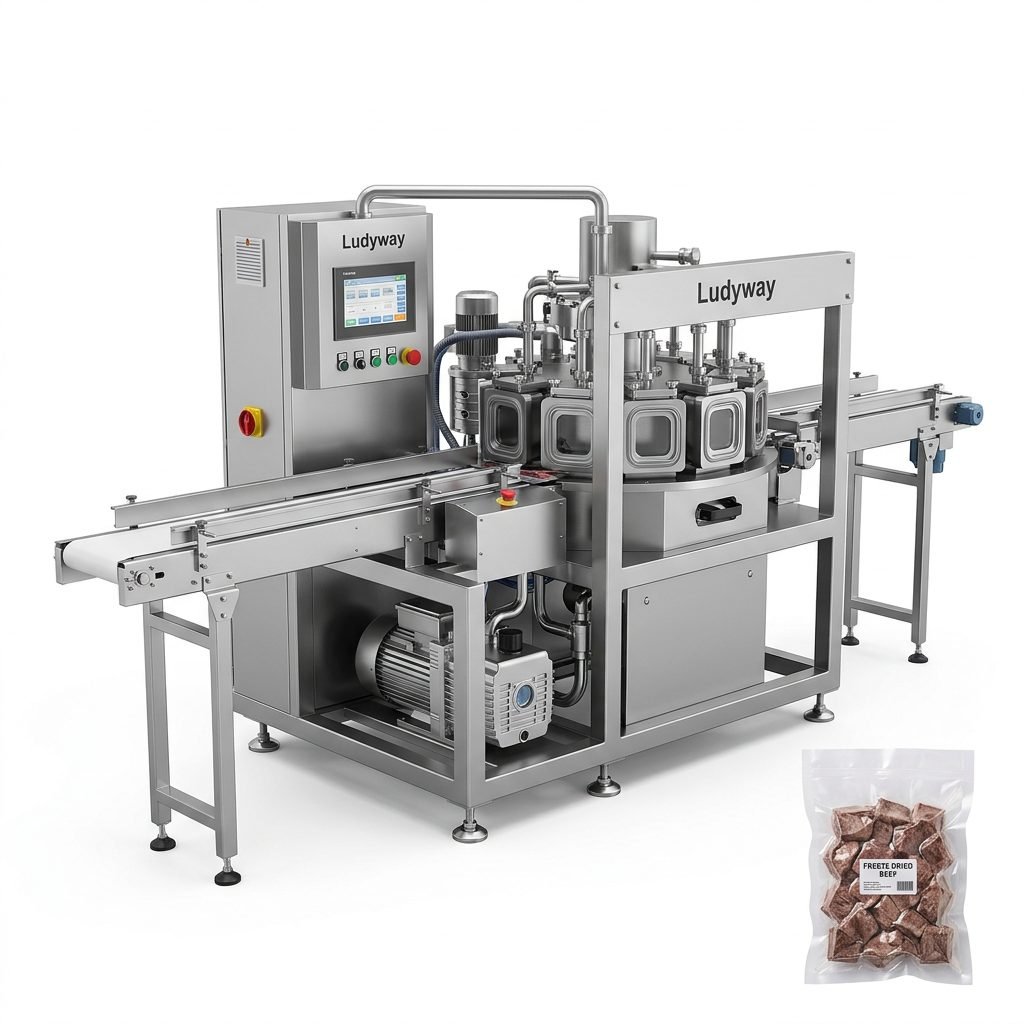
Freeze Dried Beef Vacuum Packaging System
View System Specs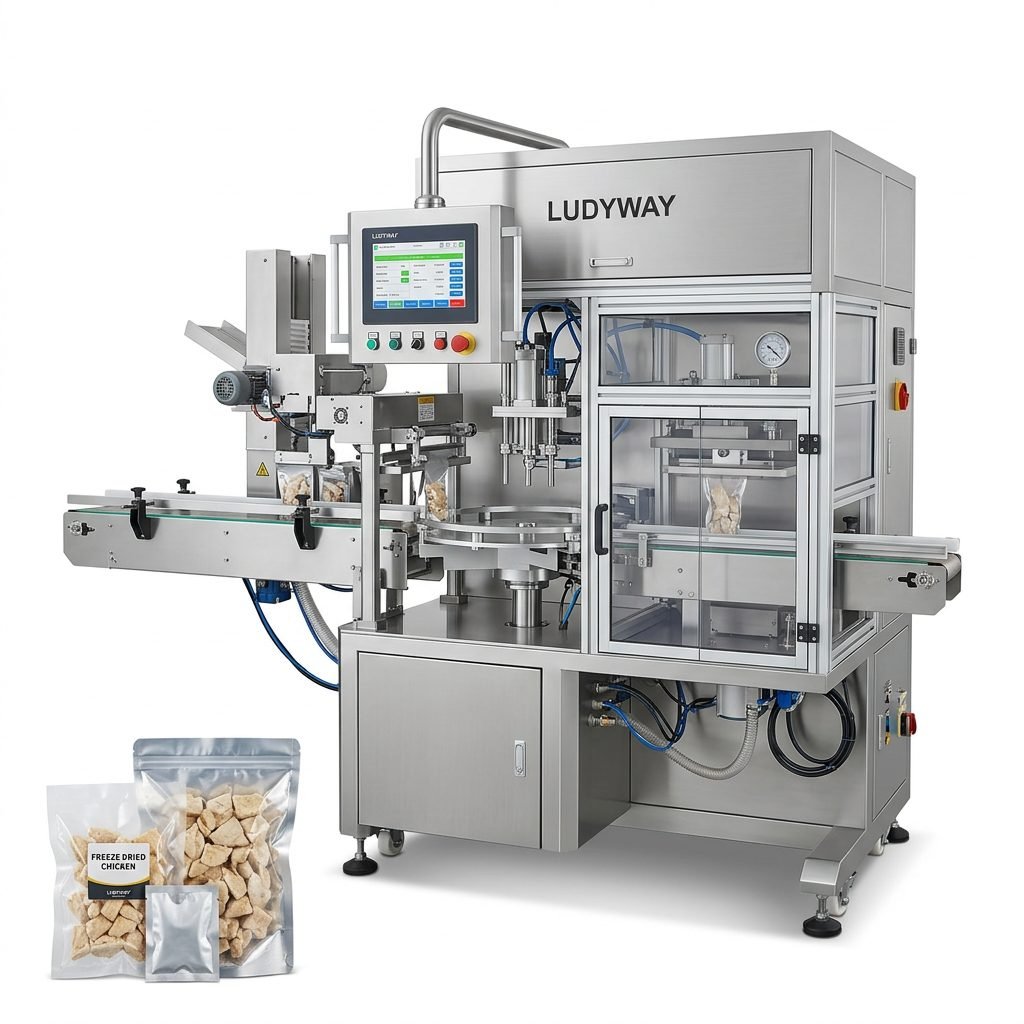
Freeze Dried Meat Vacuum Packaging Machine
View System Specs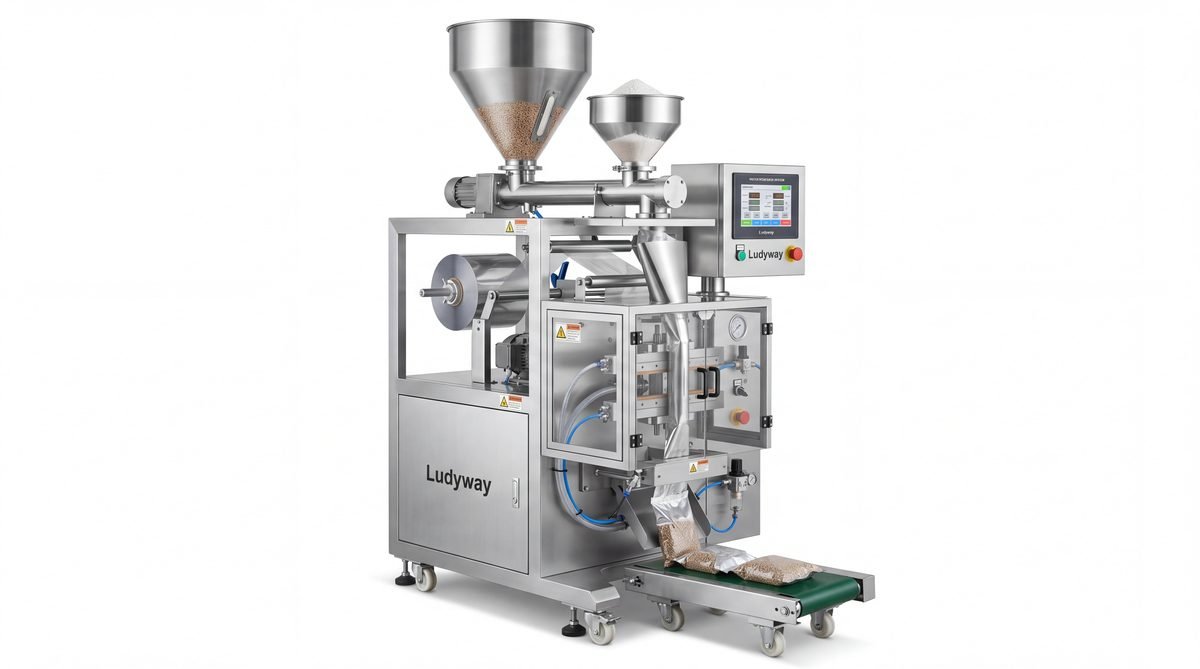
Vacuum Packaging Line for Bulk Granules & Powders
View System Specs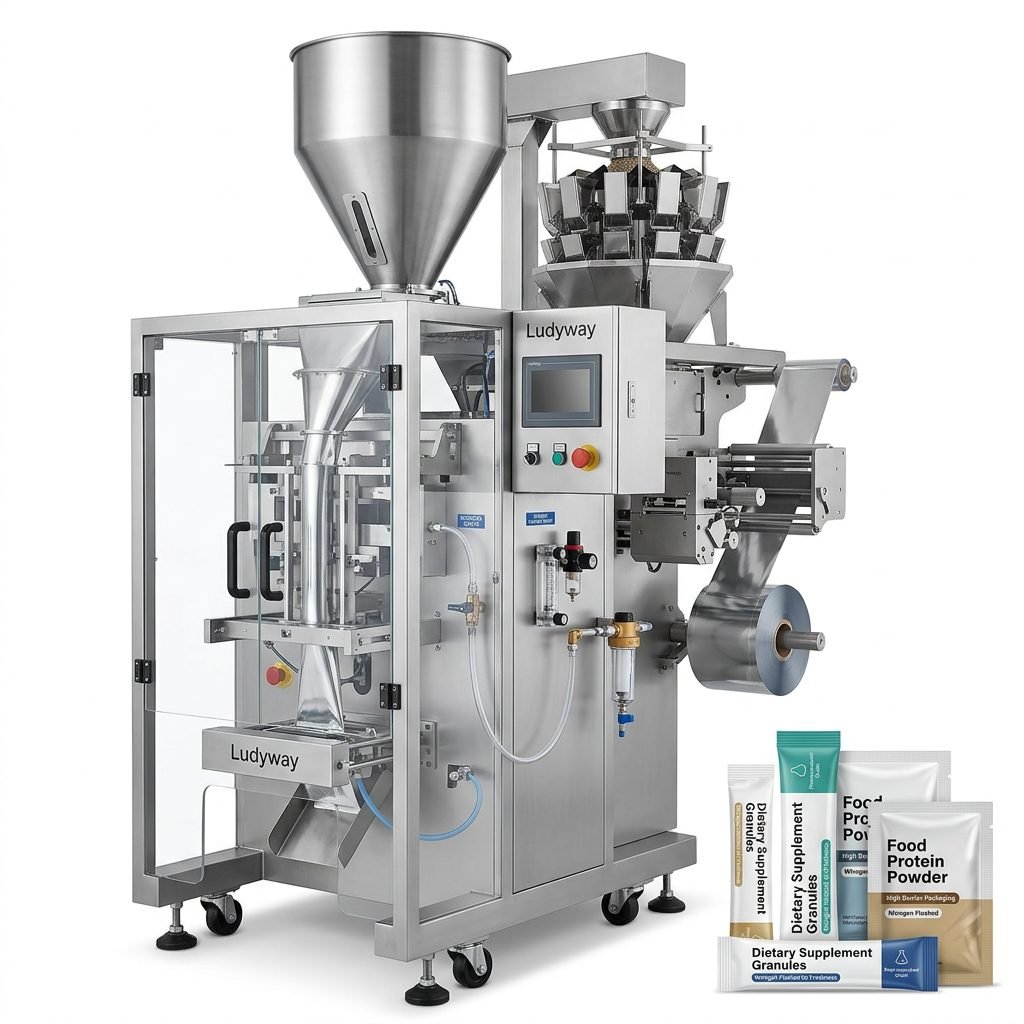
Nitrogen Flushing Packaging System
View System Specs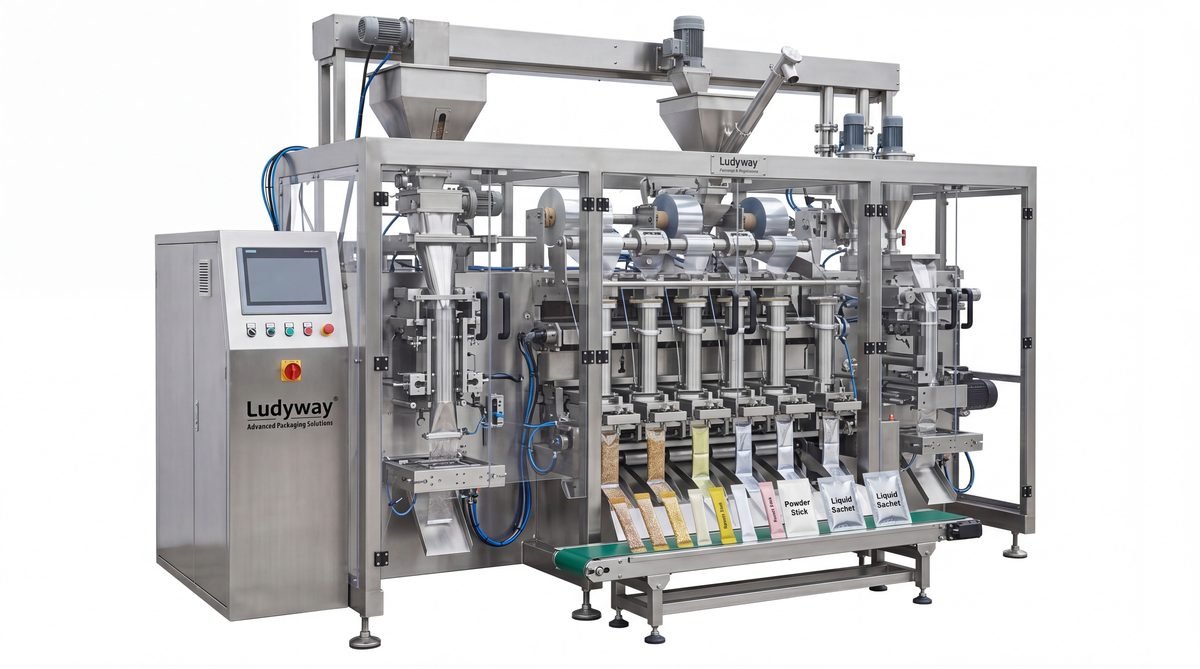
Multi-Lane Stick Pack & Sachet Machine
View System Specs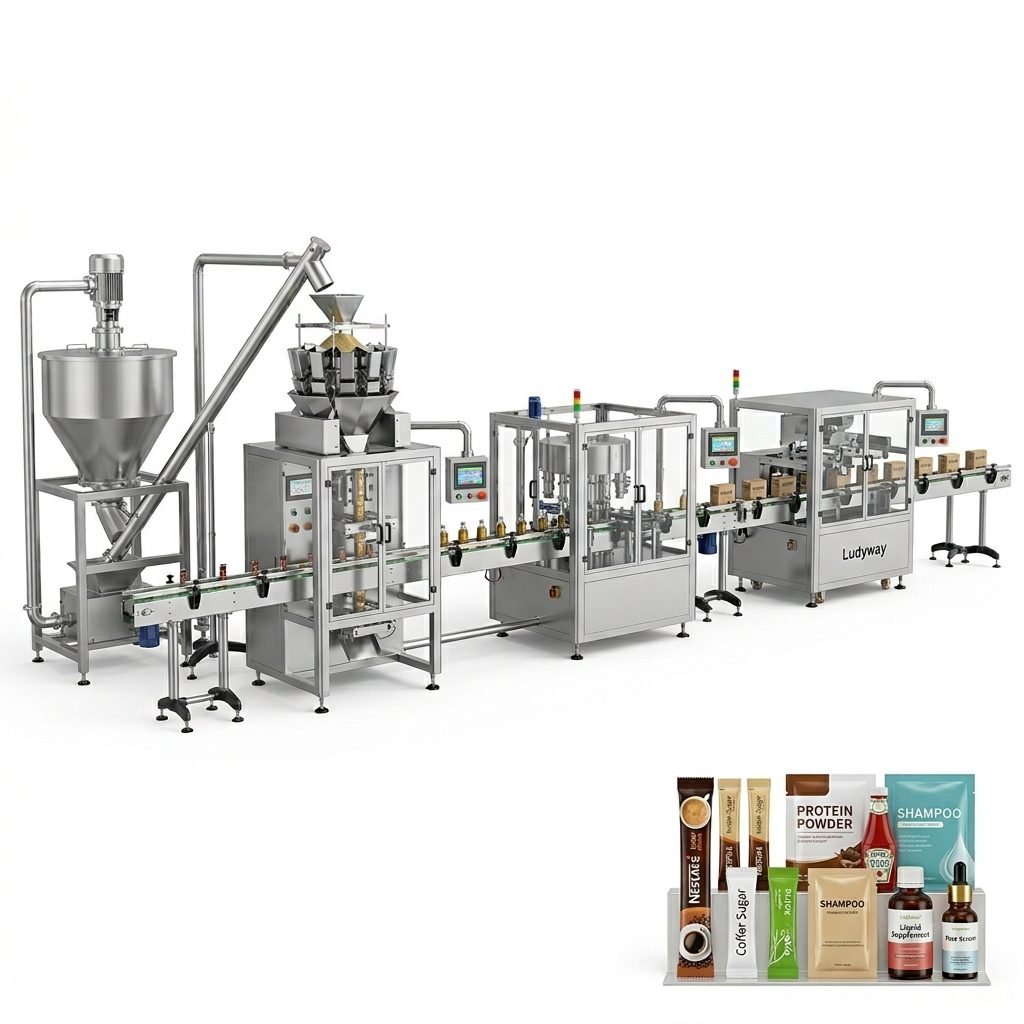
Turnkey Automated Packaging Line Solution
View System SpecsTechnical Comparison: Industrial Vacuum Sealing Systems
| System Parameter | Single-Chamber Vacuum Model | Double-Chamber Continuous Model | Rotary Vacuum Pouch Packaging Line |
|---|---|---|---|
| Production Capacity | 1 – 4 cycles / min | 3 – 8 cycles / min | 30 – 60 pouches / min (Automated) |
| Ultimate Vacuum Pressure | ≤ 0.1 KPa | ≤ 0.1 KPa | ≤ 0.08 KPa |
| Pouch Size Range | Up to 400 x 500 mm | Up to 600 x 700 mm | Width: 100-250mm, Length: 150-350mm |
| Sealing Bar Length | 400 mm / 500 mm (Single/Dual) | 600 mm / 800 mm (Dual per chamber) | Custom Rotary Heat Sealing Jaw |
| Frame Construction | AISI 304 Stainless Steel | Heavy-Duty AISI 304 Stainless Steel | Sanitary SUS304 / SUS316 Contact Parts |
| Gas Flushing Option | Available (N2 / MAP) | Available (Multi-gas blending) | Integrated Inline Multi-Nozzle MAP |
| Control Architecture | Microcontroller / Digital UI | PLC + Color Touch Screen | Advanced Siemens PLC & Servo Drive |
Four-Stage Precision Hermetic Packaging Architecture
Automated Infeed & Dosing
Product is accurately fed via multi-head weighers, augers, or liquid peristaltic pumps into premade barrier pouches or thermoformed pockets.
Chamber Evacuation
High-displacement vacuum pumps rapidly extract internal chamber atmospheric gases down to pre-set millibar values measured by digital transducers.
MAP Flush & Thermal Seal
Optional inert gas flushing stabilizes internal pressure before impulse heating bars fuse the multilayer polymer jaws under controlled pneumatic force.
Discharge & Inspection
Pneumatically transferred sealed packs proceed to inline checkweighers, X-ray foreign body detectors, and downstream automated cartoning machinery.
Comprehensive Industry Application Scenarios
1. Food Processing & Freeze-Dried Logistics: Critical for preserved meats, freeze-dried fruit chunks, roasted nuts, seafood fillets, and ready-to-eat rations. Vacuum sealing maintains color preservation, suppresses lipid oxidation, and prevents the loss of crisp volatile aromas.
2. Pharmaceuticals & Medical Consumables: Creates absolute sterile barrier protection for disposable medical kits, wound dressings, sterile surgical masks, and hygroscopic active pharmaceutical powders requiring tamper-evident hermetic packaging.
3. Specialty Chemical & High-Tech Manufacturing: Shields sensitive electronic PCB modules, semiconductor dies, automotive adhesives, and catalyst additives against static discharge and ambient humidity degradation.
International Certifications & Compliances
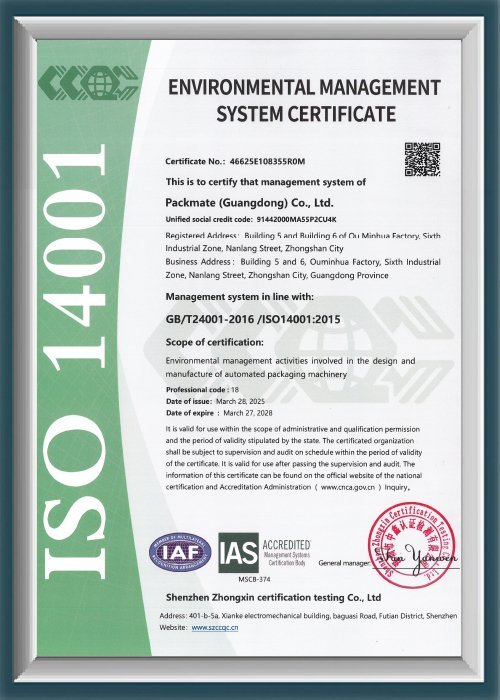 CE Safety Compliance
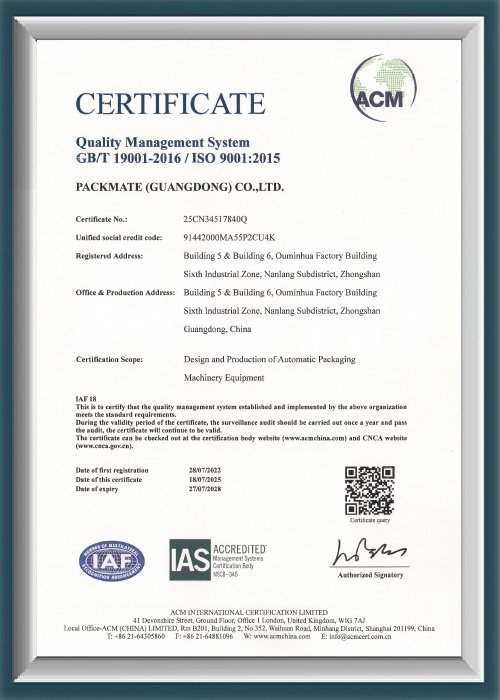 ISO9001 Quality System
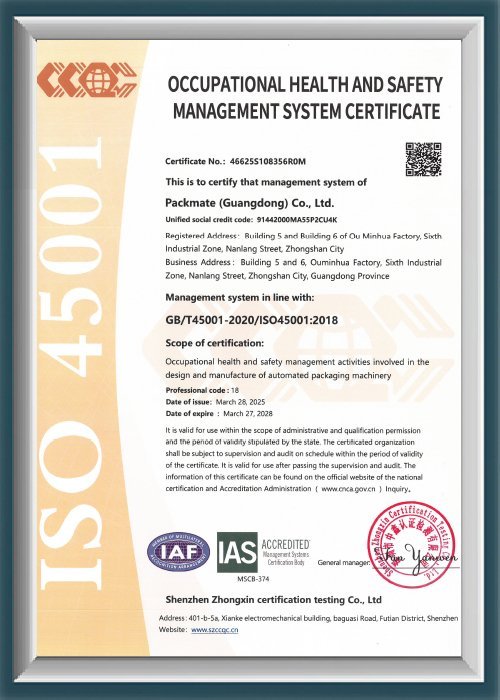 Sanitary GMP Compliance
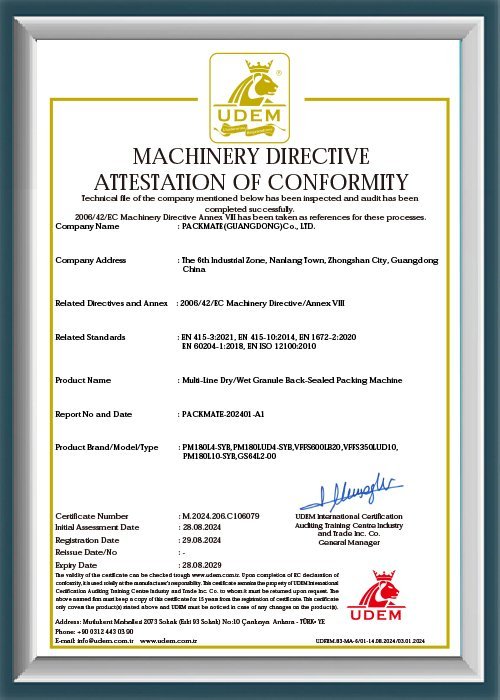 Global Export Conformity
Trusted by Global Brand Leaders Worldwide
Frequently Asked Questions on Vacuum Sealer Machinery
What packaging film materials are compatible with industrial vacuum sealers?
Our vacuum packaging machinery supports a broad array of multilayer high-barrier films, including PA/PE (nylon laminate), PET/AL/PE (aluminum foil laminates), EVOH high-barrier films, and recyclable mono-PE co-extrusions designed for modern eco-packaging requirements.
Can vacuum sealer machines package liquids or high-moisture paste products?
Yes. We configure specialized vacuum machines with inclined sealing trays and progressive chamber evacuation logic that prevents liquid boiling and foaming under depressurization, ensuring 100% leak-proof hermetic seals for sauces, marinades, and medical serums.
What is the difference between standard vacuum sealing and Modified Atmosphere Packaging (MAP)?
Standard vacuum sealing eliminates virtually all ambient air to collapse the pouch tightly around the item. Modified Atmosphere Packaging (MAP) first evacuates ambient oxygen and then flushes the pouch with a precise mixture of inert gases (such as N2 or CO2) to preserve product shape, prevent crushing, and protect delicate cell walls.
How does Ludyway guarantee after-sales technical support and spare parts availability?
Ludyway supports clients across 100+ countries with dedicated remote PLC diagnostics, on-site commissioning engineers, comprehensive video training protocols, and immediate global dispatch of wear components directly from our modern 20,000㎡ manufacturing hub.
Upgrade Your Production Efficiency with Ludyway Turnkey Packaging Automation
Connect with our packaging engineering specialists today for complete technical consultations, custom footprint layouts, and comprehensive machinery proposals.
