How Modern Vacuum Sealer Packaging Machines Inhibit Food Spoilage
Biological decay, enzymatic browning, and lipid auto-oxidation are primarily catalyzed by ambient oxygen and moisture. Ludyway vacuum packaging machines deploy multi-stage evacuation cycles to establish an ultra-low oxygen barrier that stabilizes perishable integrity.
At an industrial scale, a vacuum sealer packaging machine for food preservation operates beyond simple air extraction. Our state-of-the-art machines utilize precision rotary-vane and high-capacity digital vacuum sensors to extract up to 99.5% of ambient atmosphere from multi-layer pouches, sachets, and vacuum barrier bags before hermetically sealing the thermoplastic film.
By creating an anaerobic enclosure, our machinery halts the aerobic proliferation of mold, fungal spores, and bacteria like Pseudomonas. Simultaneously, it prevents the moisture migration that leads to freezer burn in raw meats or staleness in moisture-sensitive freeze-dried foods, seeds, and roasted coffee beans.
- Oxygen Evacuation Precision: Digital pressure control down to ≤ 10 mbar residual pressure.
- Modified Atmosphere Option (MAP): Integrated high-speed nitrogen flushing for fragile freeze-dried snacks and leafy produce.
- Thermal Impulse Sealing: Multi-zone PID temperature controls ensuring zero pinholes or channel leaks along the seal perimeter.
Engineered for Every Processing Capacity & Food Medium
Whether packing delicate freeze-dried fruit powders, fresh seafood, or bulk dry grain ingredients, Ludyway fabricates customized vacuum architectures tailored to line speed and sanitary standards.
Rotary Chamber Vacuum Machines
Engineered for high-output meat processing, poultry packaging, and cheese block preservation. Features multi-station continuous rotary tables that synchronize pouch loading, deep vacuum evacuation, thermal sealing, and automated discharge.
Multi-Lane Stick & Pouch Vacuum Lines
Equipped with multi-head vibratory and auger dosing systems. Delivers integrated vacuuming and nitrogen flushing specifically designed for powdered baby foods, functional supplements, seasonings, and coffee ground pouches.
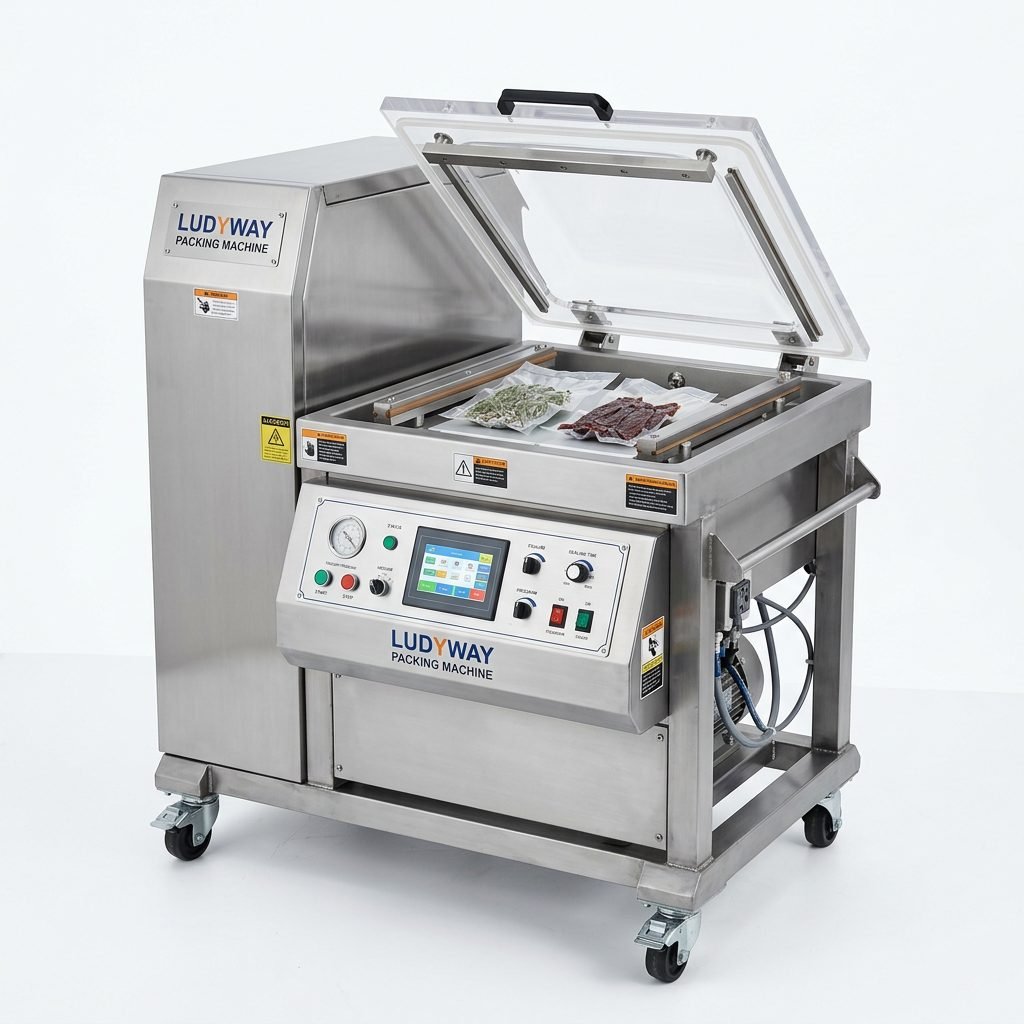
Double-Chamber Industrial Sealers
Built for bulk food processors packaging bulk grains, marinated seafood, nuts, and primal cuts. The dual-chamber layout allows operators to unload and reload one station while the opposing chamber completes deep air evacuation.
Conventional Atmospheric Packaging vs. Ludyway Vacuum Automation
Upgrading to automated industrial vacuum sealing extends food product viability by 300% to 500%, reducing post-production spoilage losses and expanding commercial distribution horizons.
| Food Category | Ambient / Conventional Shelf Life | Ludyway Vacuum Sealed Viability | Primary Preservation Mechanism |
|---|---|---|---|
| Freeze-Dried Fruits & Vegetables | 1–3 Months (Moisture absorption risk) | 18–36 Months | Complete elimination of ambient relative humidity & vapor migration. |
| Fresh Primal Meat & Poultry | 3–5 Days (Refrigerated) | 21–28 Days (Refrigerated) | Suppression of aerobic spoilage bacteria & meat myoglobin stabilization. |
| Seafood & Marinated Fish | 2–4 Days (Refrigerated) | 14–21 Days | Inhibition of oxidative rancidity and enzyme-driven protein breakdown. |
| Roasted Coffee Beans & Grounds | 2–4 Weeks (Volatile degassing decay) | 12–24 Months | Prevention of aroma oil auto-oxidation with optional one-way degassing valves. |
| Nuts, Seeds & Dried Grains | 3–6 Months (Fat rancidity & weevil risk) | 24–36 Months | Zero-oxygen environment eliminates insect infestation and fatty-acid decay. |
| Seasoning Powders & Broth Mixes | 4–6 Months (Clumping & caking) | 24+ Months | Hermetic seal prevents ambient moisture entrapment and aroma loss. |
Why Leading Food Processors Integrate Ludyway Packaging Machinery
With over three decades of manufacturing experience, Ludyway builds turnkey packaging lines combining AI-driven dosing, automated film tracking, and ultra-durable vacuum chambers.
Hygienic 316/304 Stainless Steel Construction
Constructed specifically for FDA, CE, and cGMP compliance. Our food packaging machines feature rounded, seamless interior chambers that eliminate crevices, enabling aggressive high-pressure sanitation washdowns without risking electrical ingress or bacterial harborage.
Smart PLC Integration & Real-Time Parameter Telemetry
Equipped with intuitive touchscreen HMIs capable of storing over 50 product recipes. Monitor real-time vacuum depth, sealing bar temperature curves, nitrogen purge ratios, and cycle speed with single-touch calibration.
Optimized Energy Consumption & Rapid Cycle Rates
High-performance direct-drive vacuum pumps and pneumatic assist mechanisms minimize electrical and pneumatic consumption per pack, delivering cycle times as swift as 12 to 25 cycles per minute per chamber.
Pinhole-Free Hermetic Sealing Jaws
Custom bi-active heating bars with specialized cooling profiles guarantee that even thick laminated foils, EVOH high-barrier films, and co-extruded barrier pouches remain completely sealed under rough shipping logistics.
Featured Vacuum & Food Packaging Systems
Select from Ludyway’s specialized packaging lineup to match your exact product viscosity, granulate bulk density, and shelf-life preservation mandates.
Industrial Vacuum Packaging Machine for Food & Pharmaceutical Products
Explore Specifications →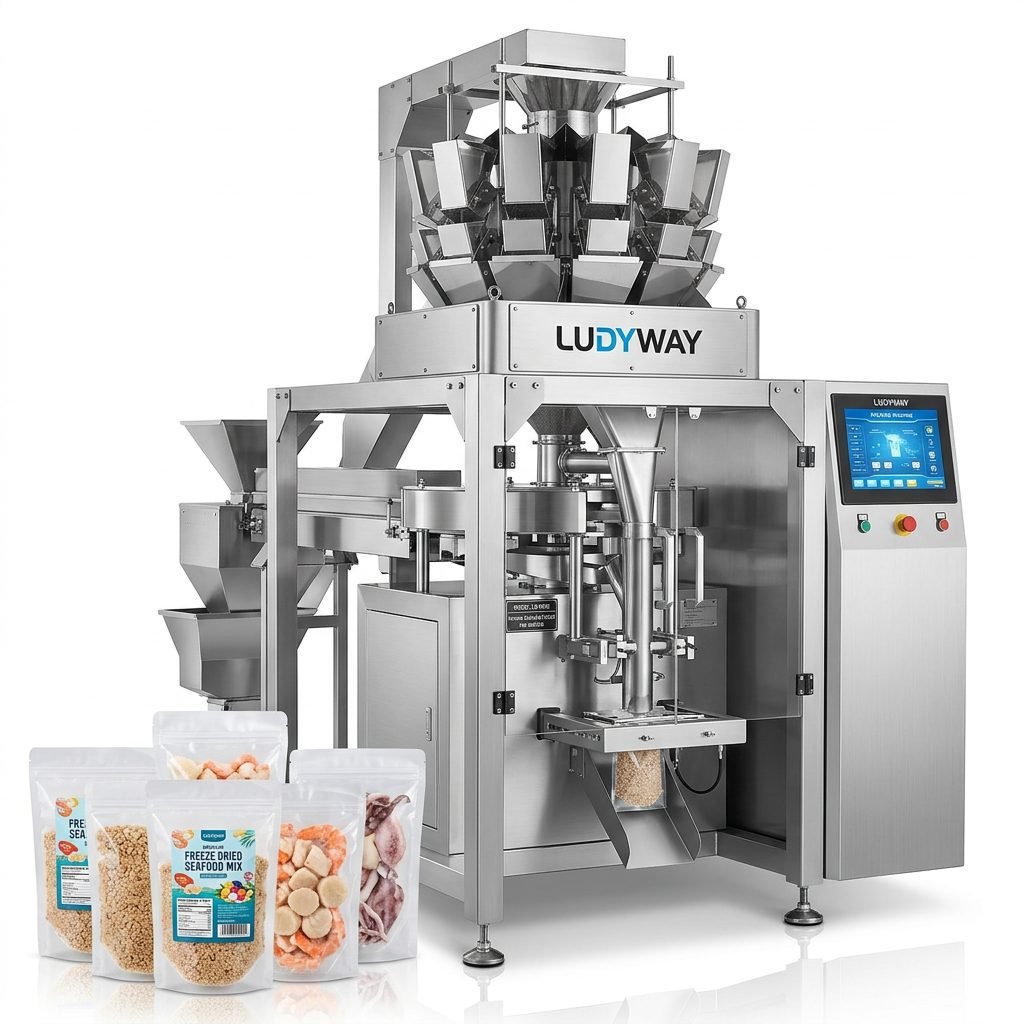
Freeze Dried Seafood Vacuum Sealing Machine for Granule Packaging
Explore Specifications →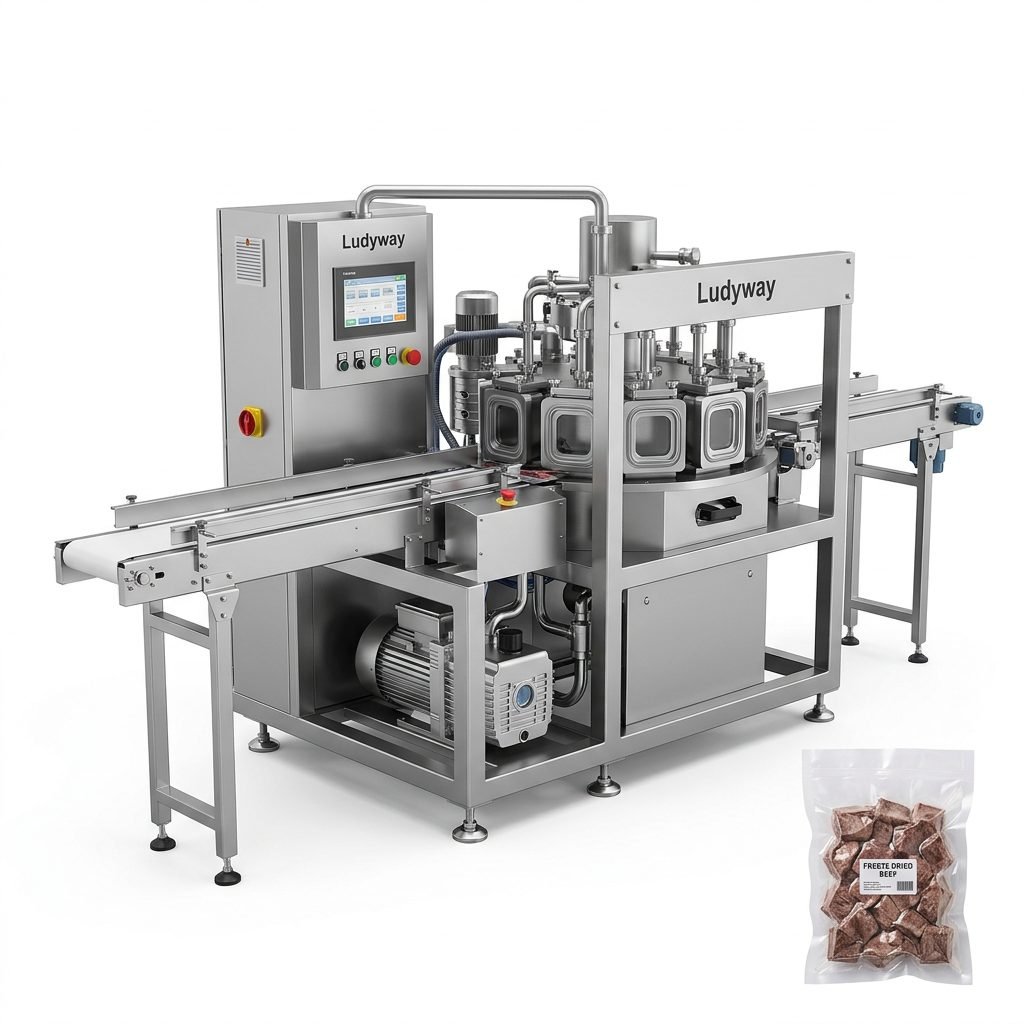
Freeze Dried Beef Vacuum Packaging System for Industrial Production
Explore Specifications →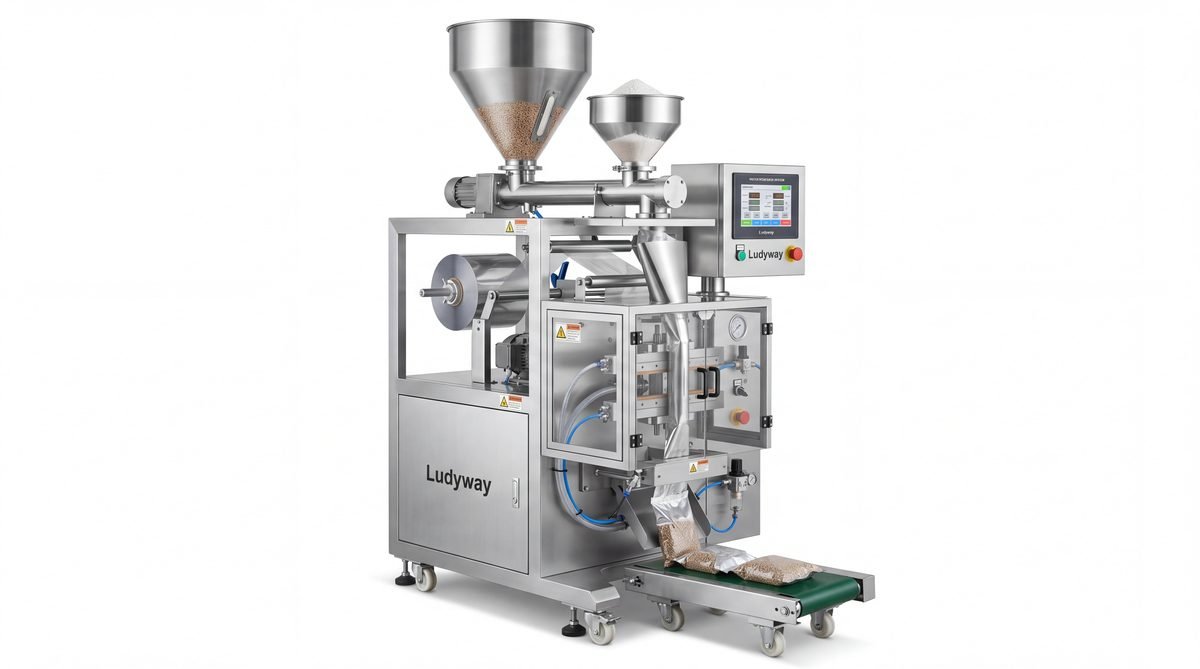
Industrial Vacuum Packaging Machine for Food & Pharma Granule Powder
Explore Specifications →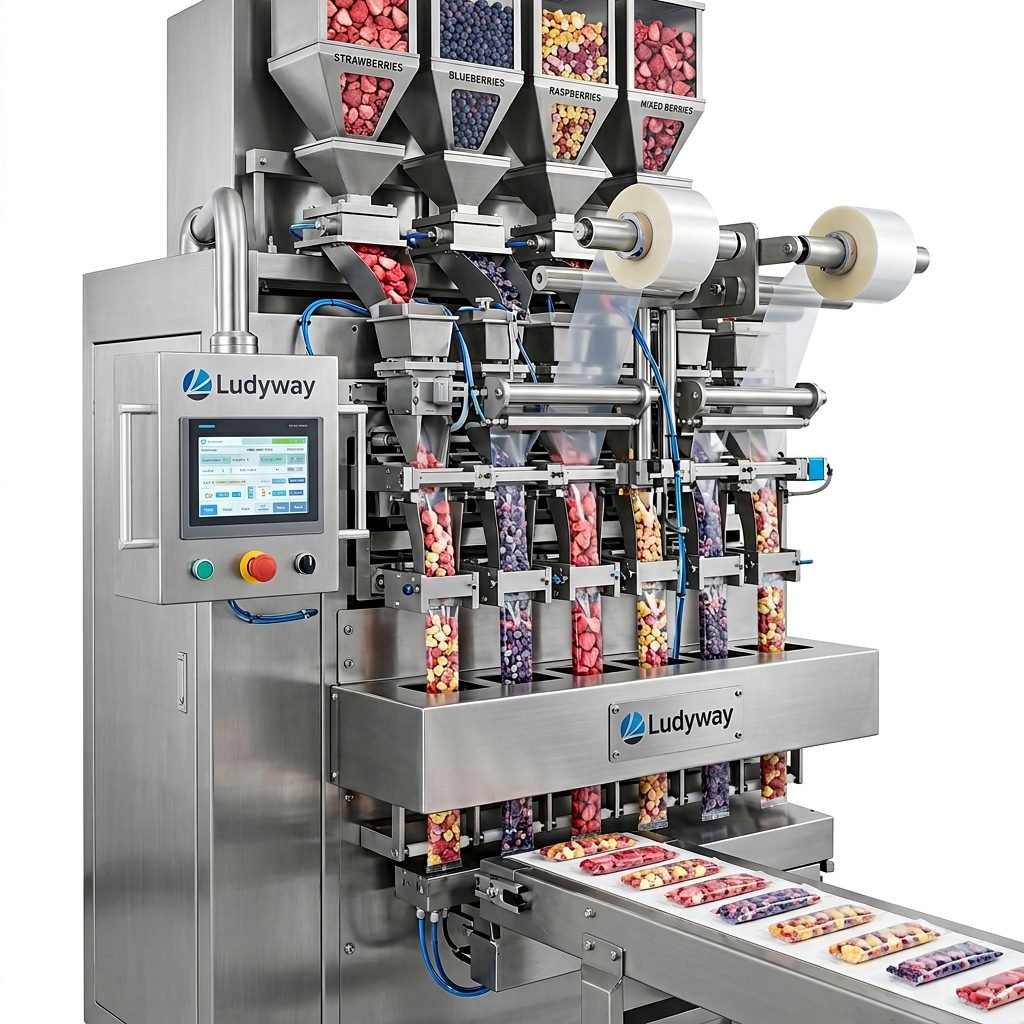
Freeze-Dried Fruit Stick Pack Machine for Granule Packaging Multi-Lane
Explore Specifications →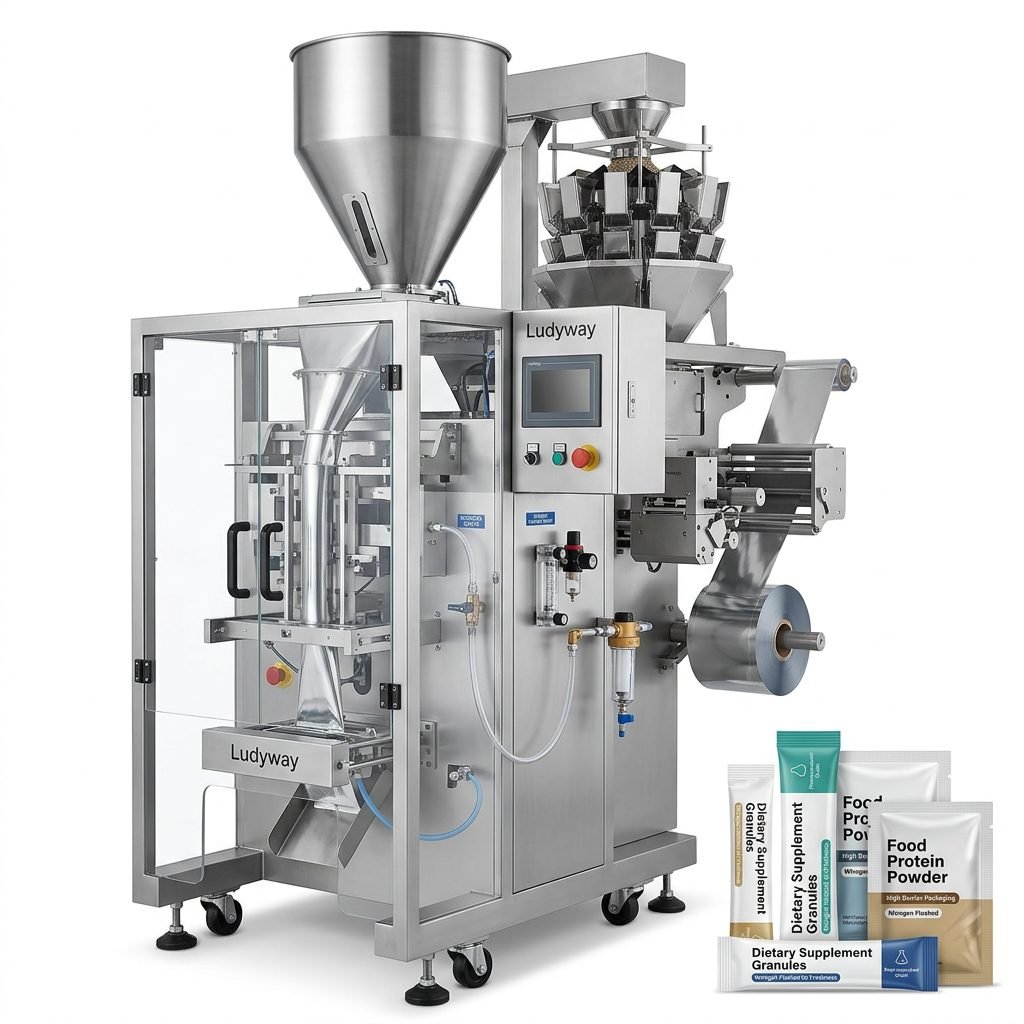
Nitrogen Flushing Packaging System for Granule & Powder Preservation
Explore Specifications →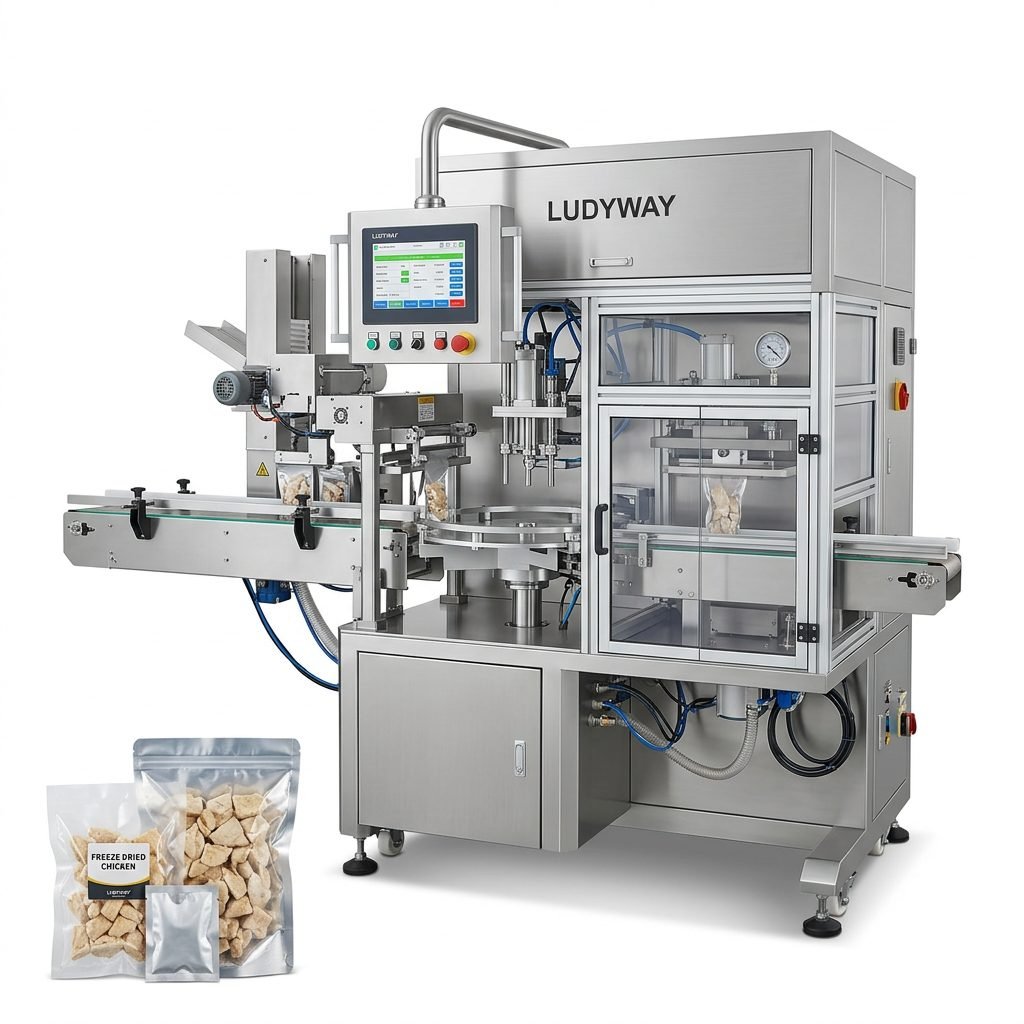
Freeze Dried Chicken Vacuum Packaging Machine for Pouches & Sachets
Explore Specifications →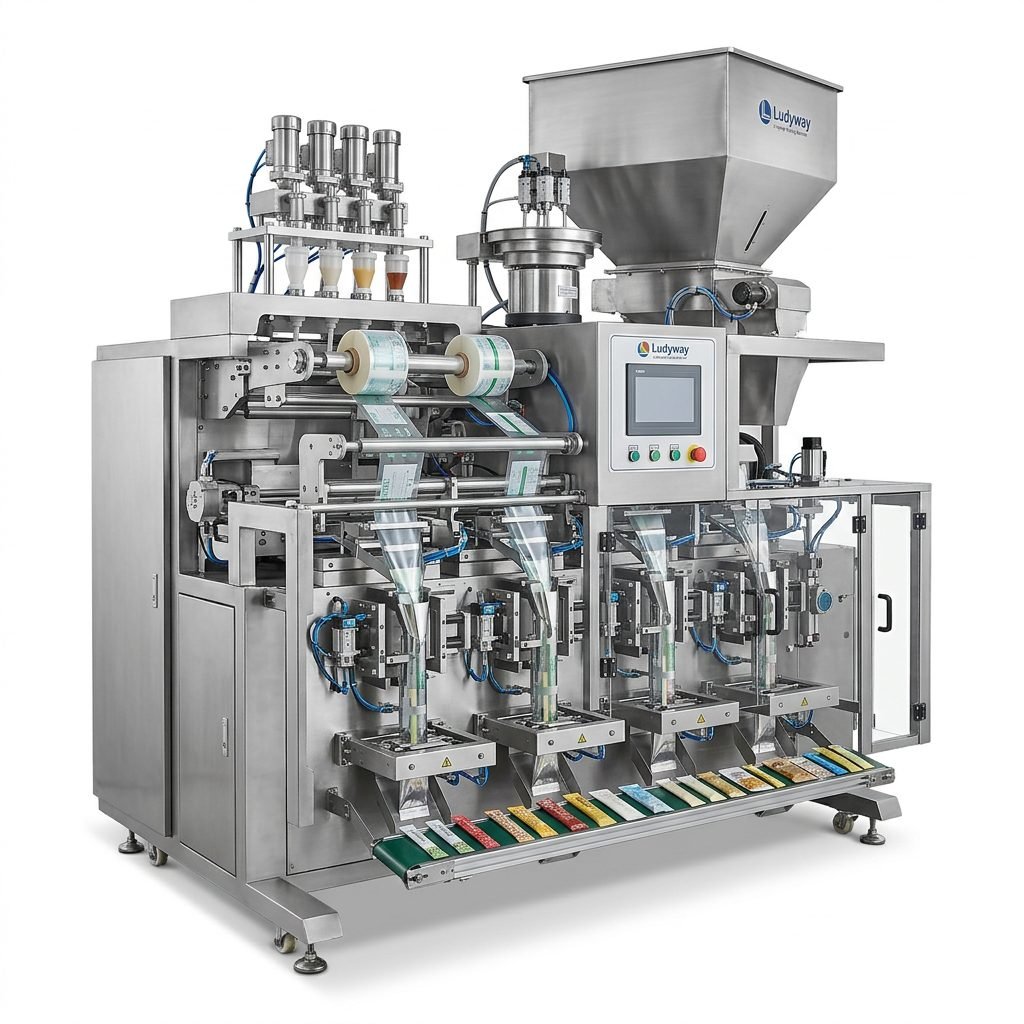
Multi-Lane Frozen Food Packaging Machine for Sachet & Stick Pack
Explore Specifications →Global Pioneer in Turnkey Packaging & Vacuum Automation Solutions
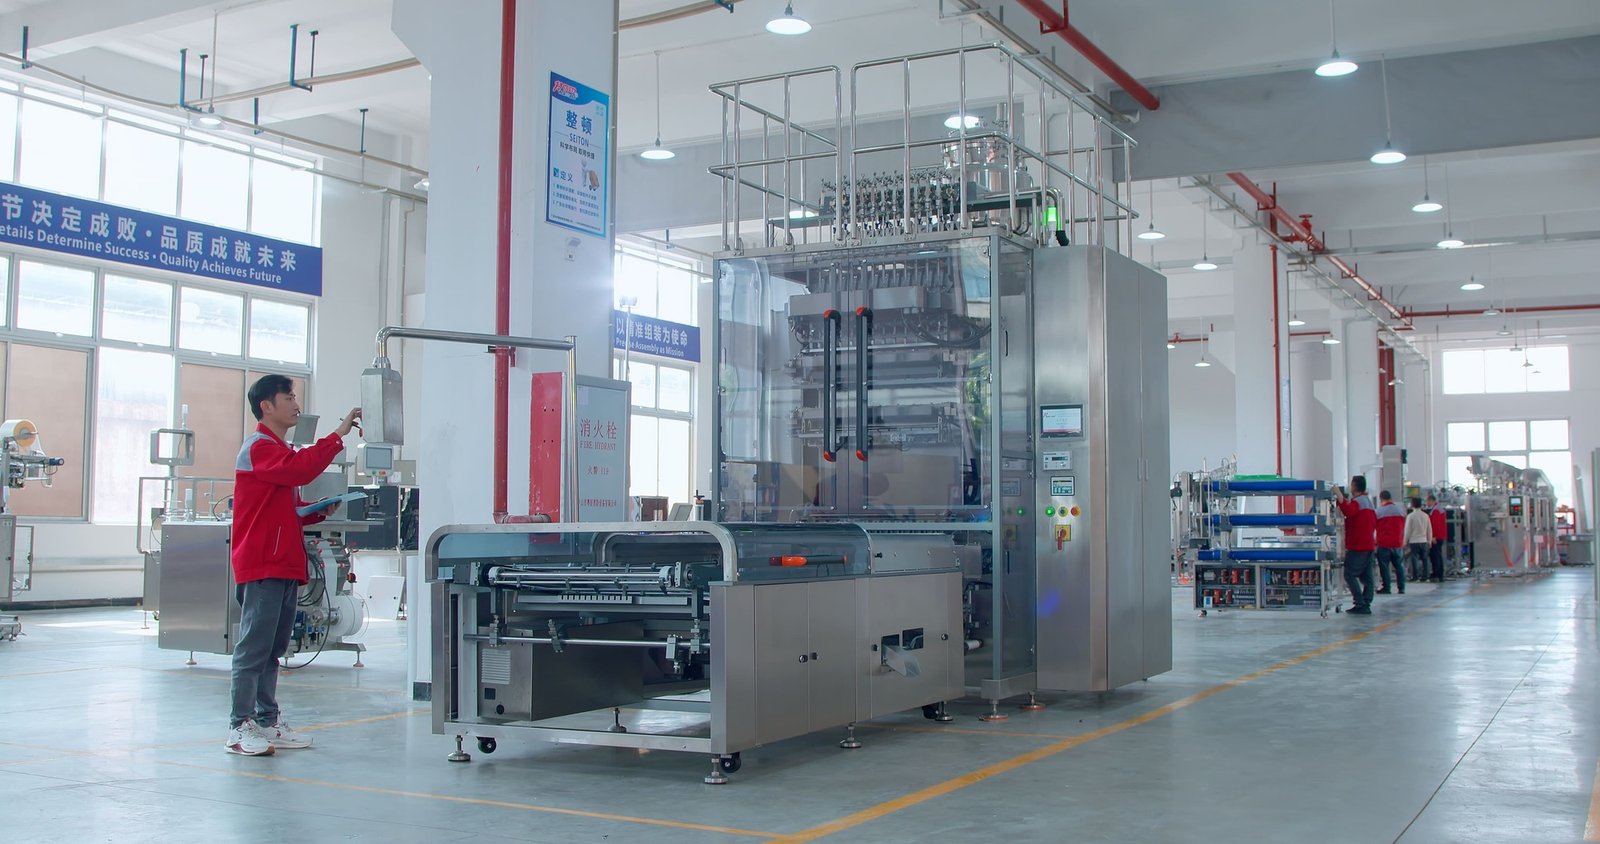
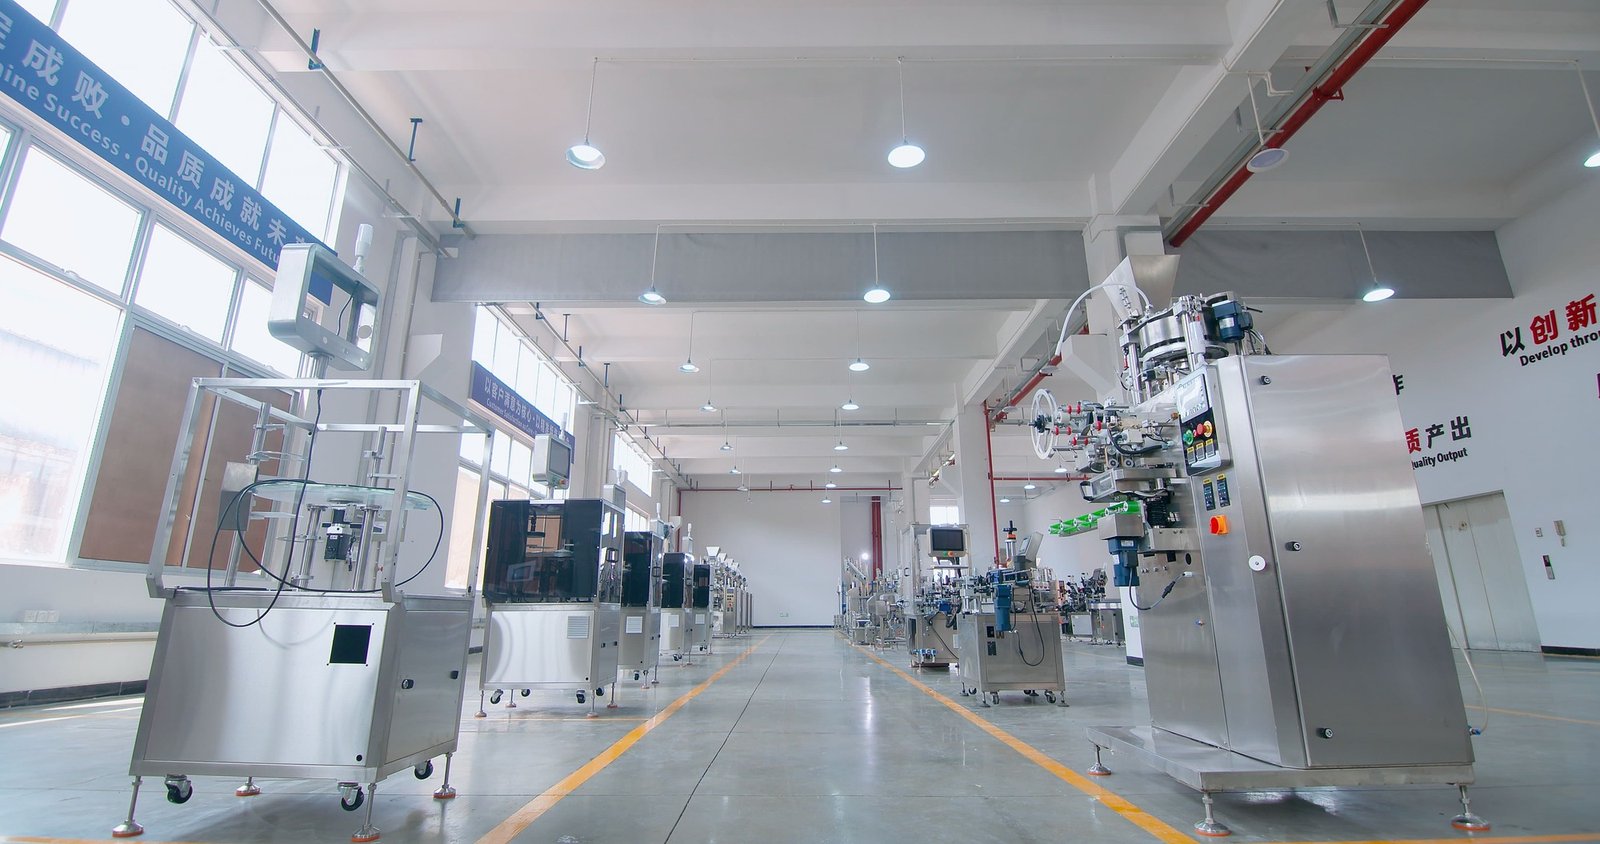
Founded on principles of engineering excellence and technological innovation, Ludyway has evolved into one of China’s premier manufacturers of intelligent packaging equipment and turnkey packaging lines. Spanning over 30 years of accumulated industry mastery, we engineer tailored preservation machinery for the food, pharmaceutical, cosmetic, and chemical sectors.
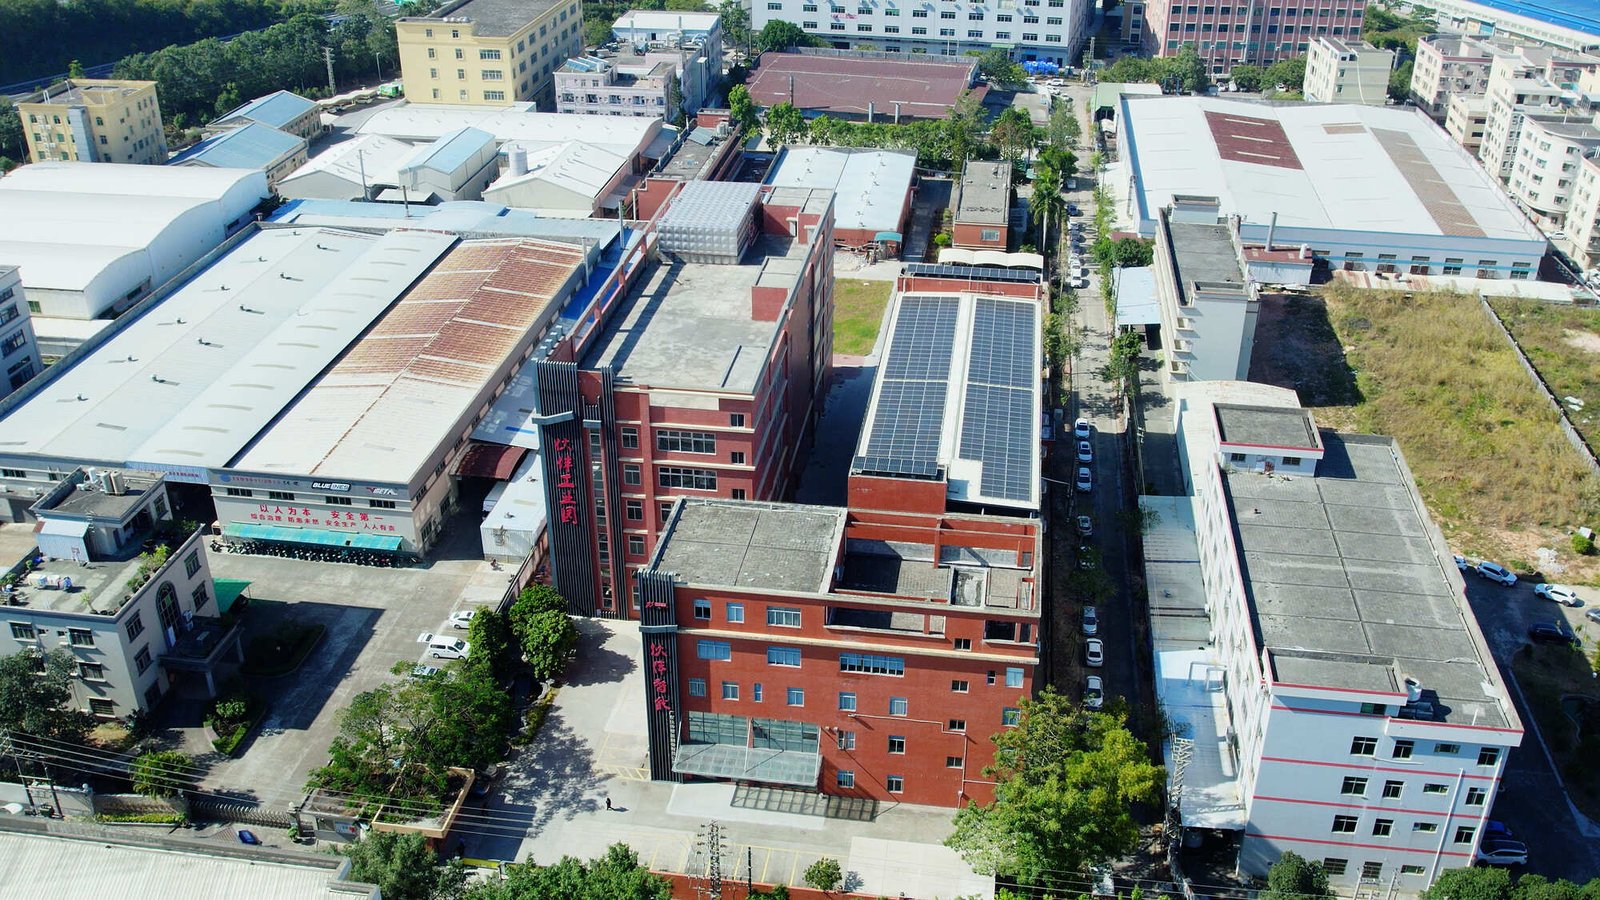
Headquartered within a state-of-the-art 20,000㎡ modern manufacturing facility, our operations are powered by 130+ dedicated packaging specialists and an arsenal of 200+ precision manufacturing units. We offer over 50 intelligent machinery models, including multi-lane stick pack systems, high-speed sachet form-fill-seal machines, and fully integrated vacuum sealer packaging lines.
From fresh produce preservation in North America to freeze-dried food handling across Europe and Asia, Ludyway serves manufacturing clients in more than 100 countries, delivering cost-effective, high-throughput, and durable solutions that maximize operational uptime.
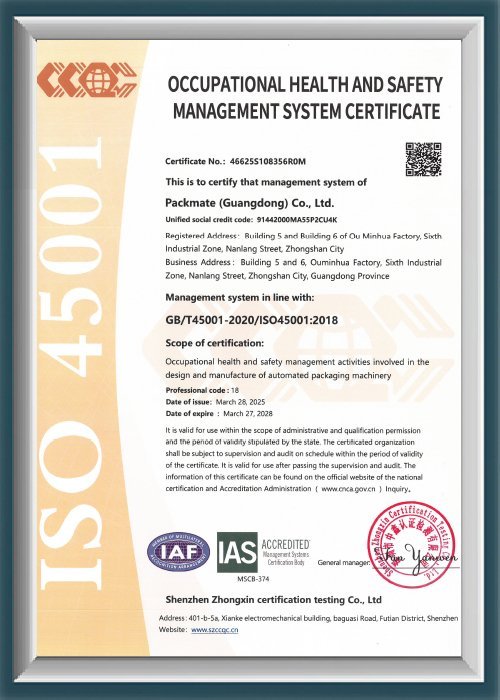
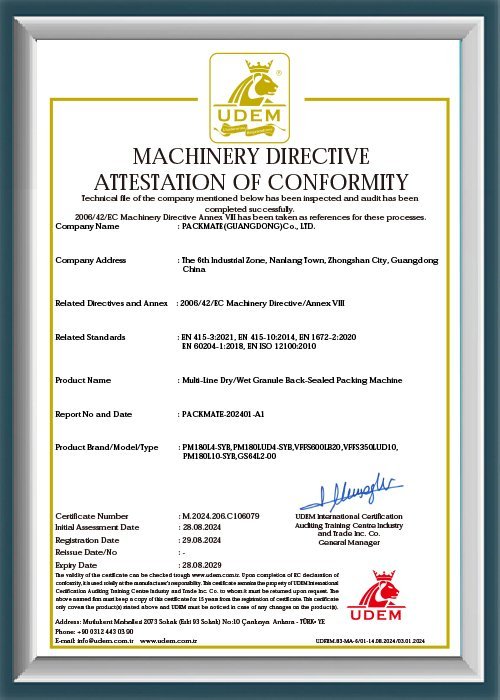
Certified International Manufacturing Standards
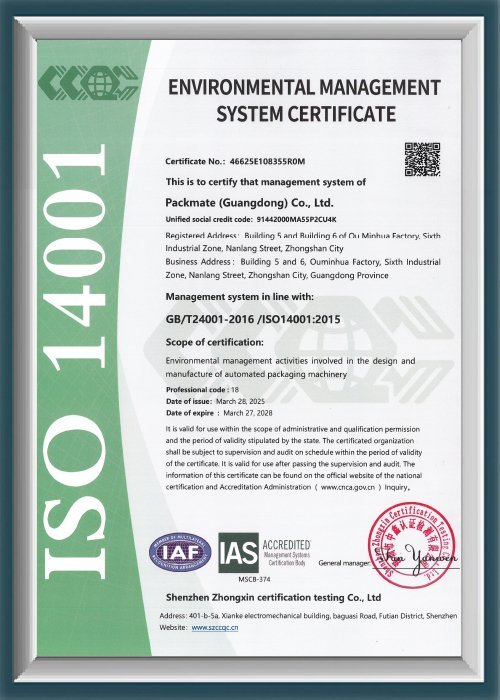
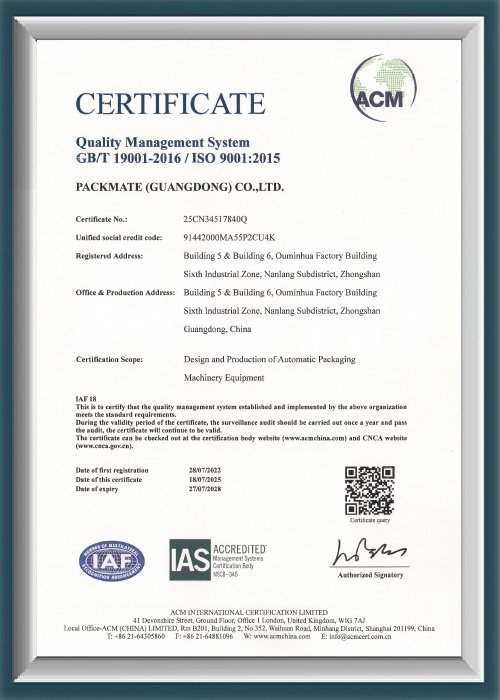
All Ludyway food preservation and vacuum packaging systems strictly comply with global food safety, CE electromagnetic compatibility, and ISO9001 management protocols.
Trusted by Worldwide Food Processing Enterprises
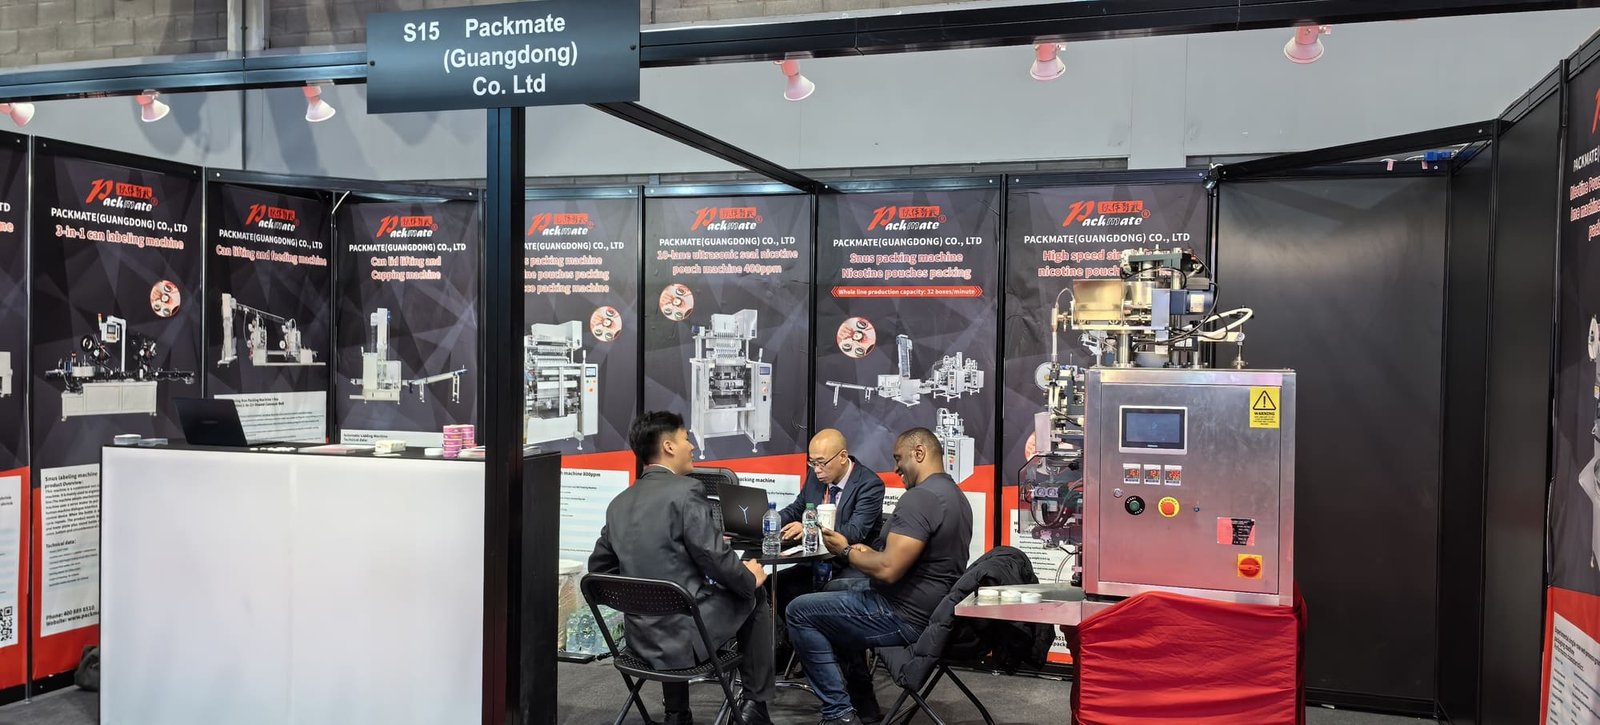
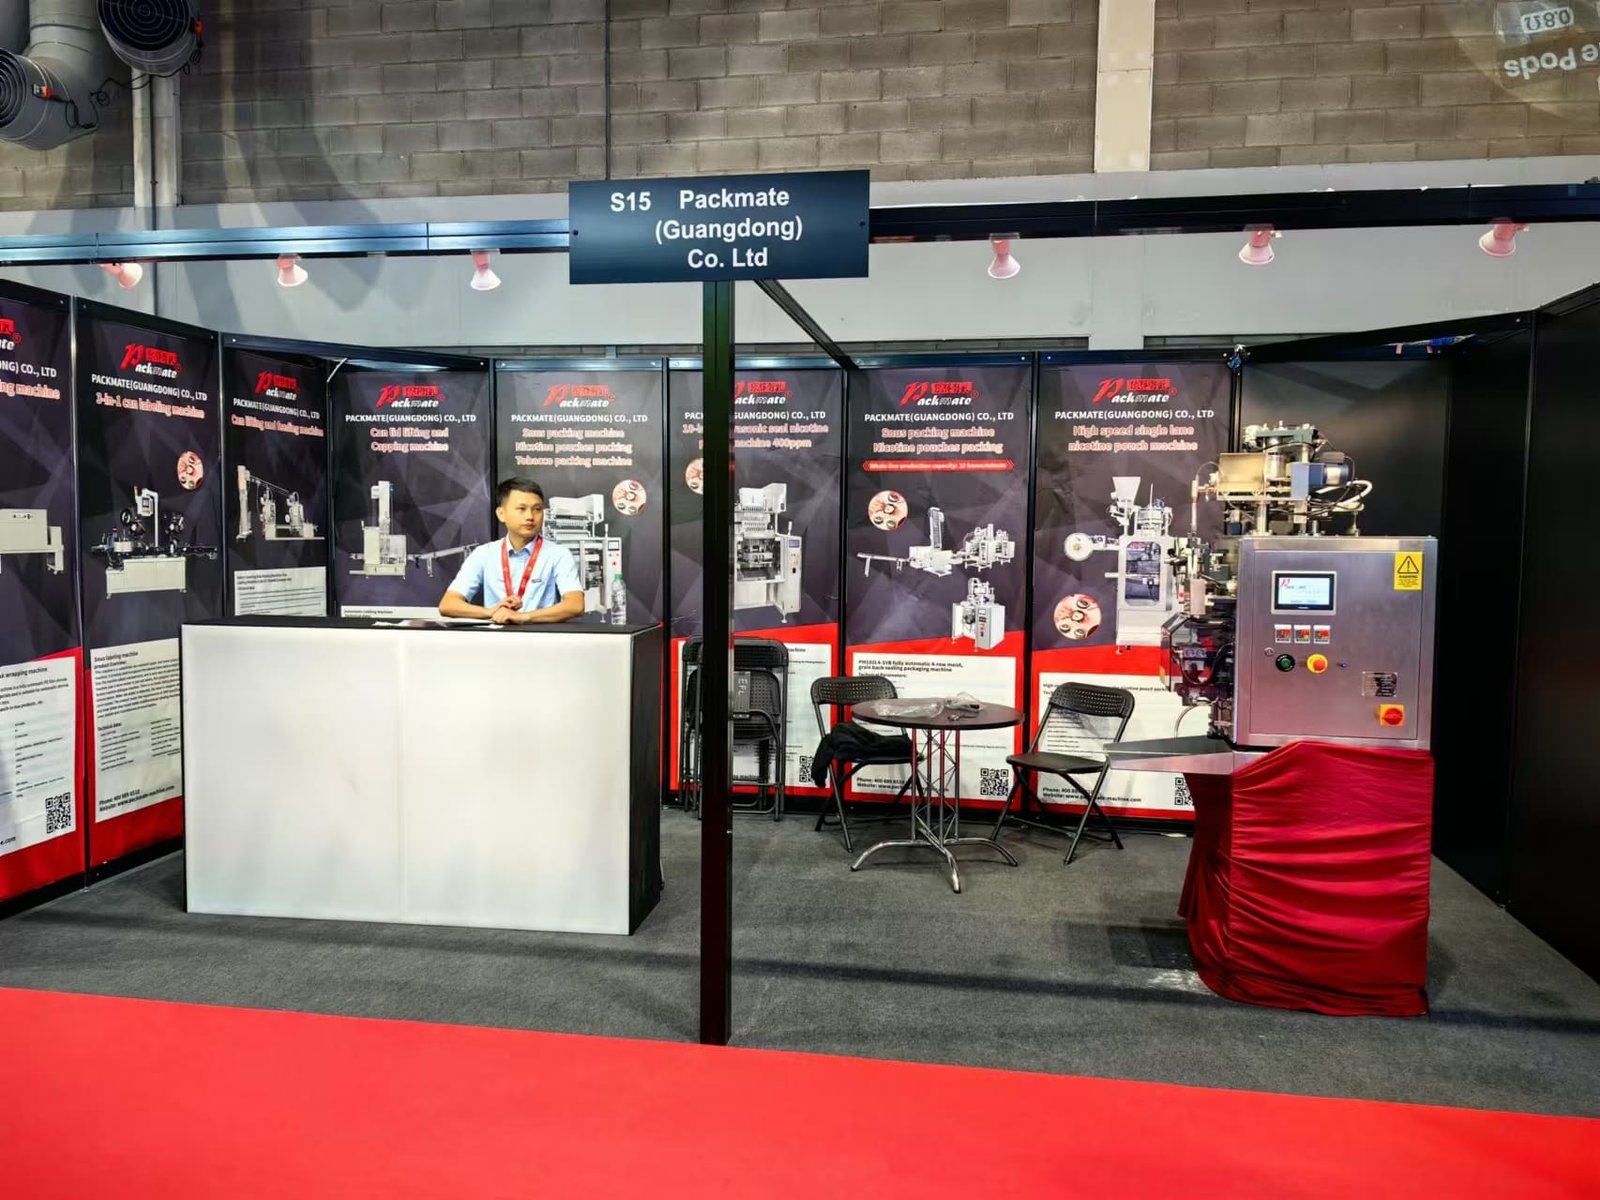
We collaborate with leading international brands and regularly present automated packaging innovations across premier industrial trade fairs worldwide.
Frequently Asked Questions: Food Preservation Vacuum Machinery
Explore critical engineering parameters, film compatibilities, and integration requirements for commercial food packaging lines.
What packaging materials are compatible with Ludyway vacuum sealing machinery?
Our vacuum packaging equipment is compatible with all commercial multi-layer co-extruded barrier films, including PA/PE (Polyamide/Polyethylene), PET/AL/PE (Aluminum Foil Laminates), EVOH high-barrier films, recyclable mono-PE films, and shrinkable vacuum barrier pouches. Temperature profiles can be calibrated specifically to your film thickness (from 50 to 200+ microns).
How does Ludyway handle fine food powders during high-vacuum cycles?
Fine powders (such as protein powders, starch, or spice extracts) can become entrained in vacuum suction lines. Ludyway integrates patented multi-stage particulate cyclone filters, specialized vacuum deceleration chambers, and anti-dust impulse sealing jaws to ensure absolute seal integrity without powder bridging.
Can Ludyway packaging machines combine vacuum sealing with nitrogen flushing (MAP)?
Yes. Our Modified Atmosphere Packaging (MAP) option first pulls an intense vacuum (≤ 5 mbar) to evacuate ambient oxygen, followed by an immediate micro-filtered Nitrogen (N2) or Carbon Dioxide (CO2) backflush. This cushions fragile items (e.g., potato chips, freeze-dried fruits) against crush damage while keeping residual oxygen below 0.5%.
What after-sales support and spare parts availability does Ludyway offer globally?
Ludyway provides 24/7 remote diagnostic support, complete English PLC interface manuals, modular spare parts kits (including genuine heating elements, Teflon strips, vacuum pump gaskets), and on-site engineer dispatch for commissioning and factory training worldwide.
Optimize Your Food Preservation Packaging Line Today
Partner with Ludyway Machinery to deploy high-efficiency vacuum sealer packaging systems built for superior seal reliability, extended food shelf life, and maximized production uptime.