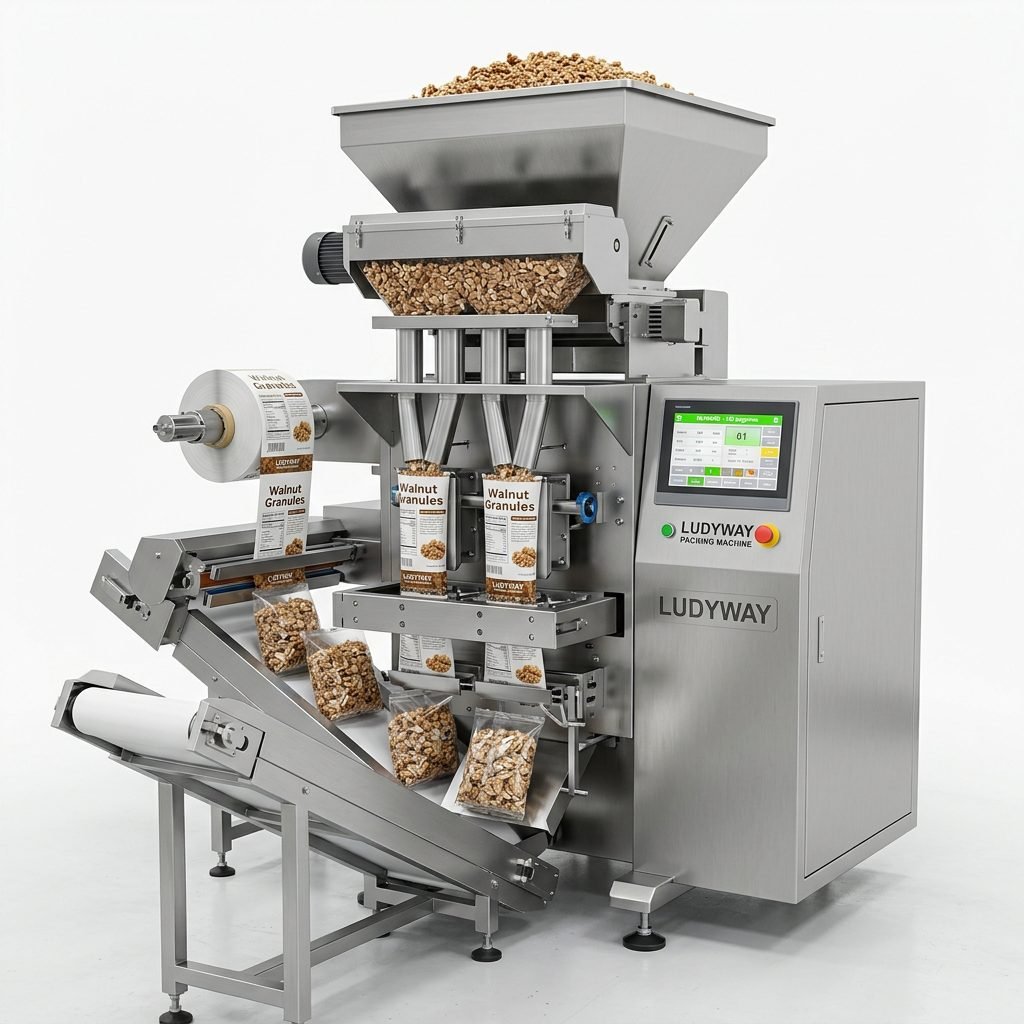
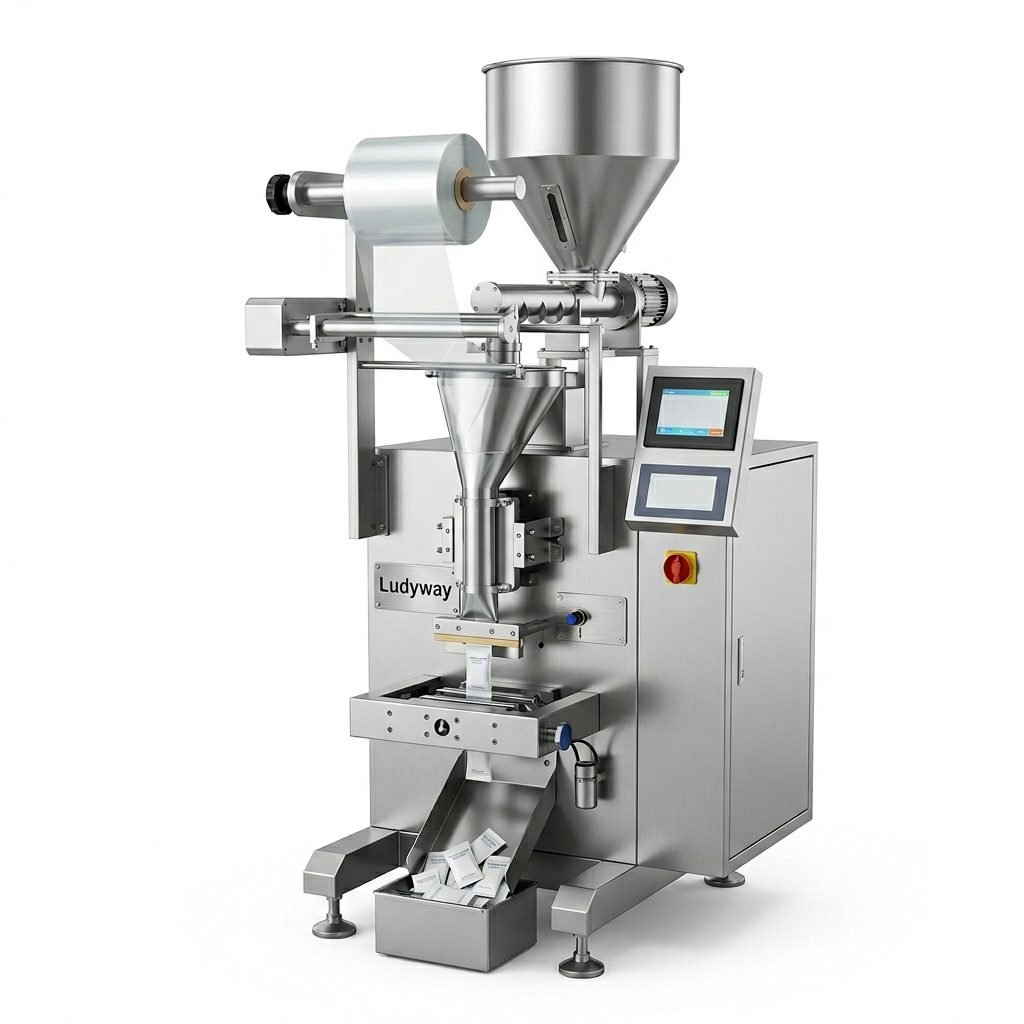
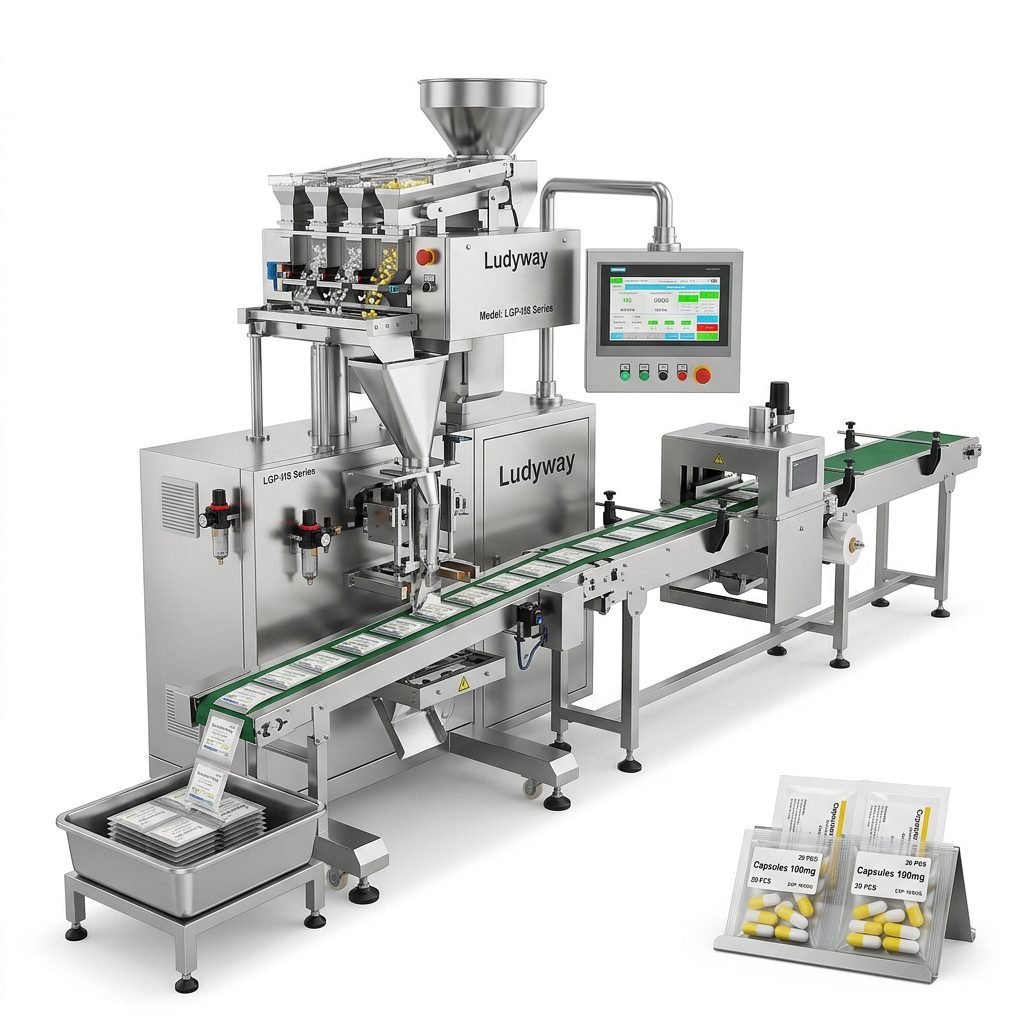
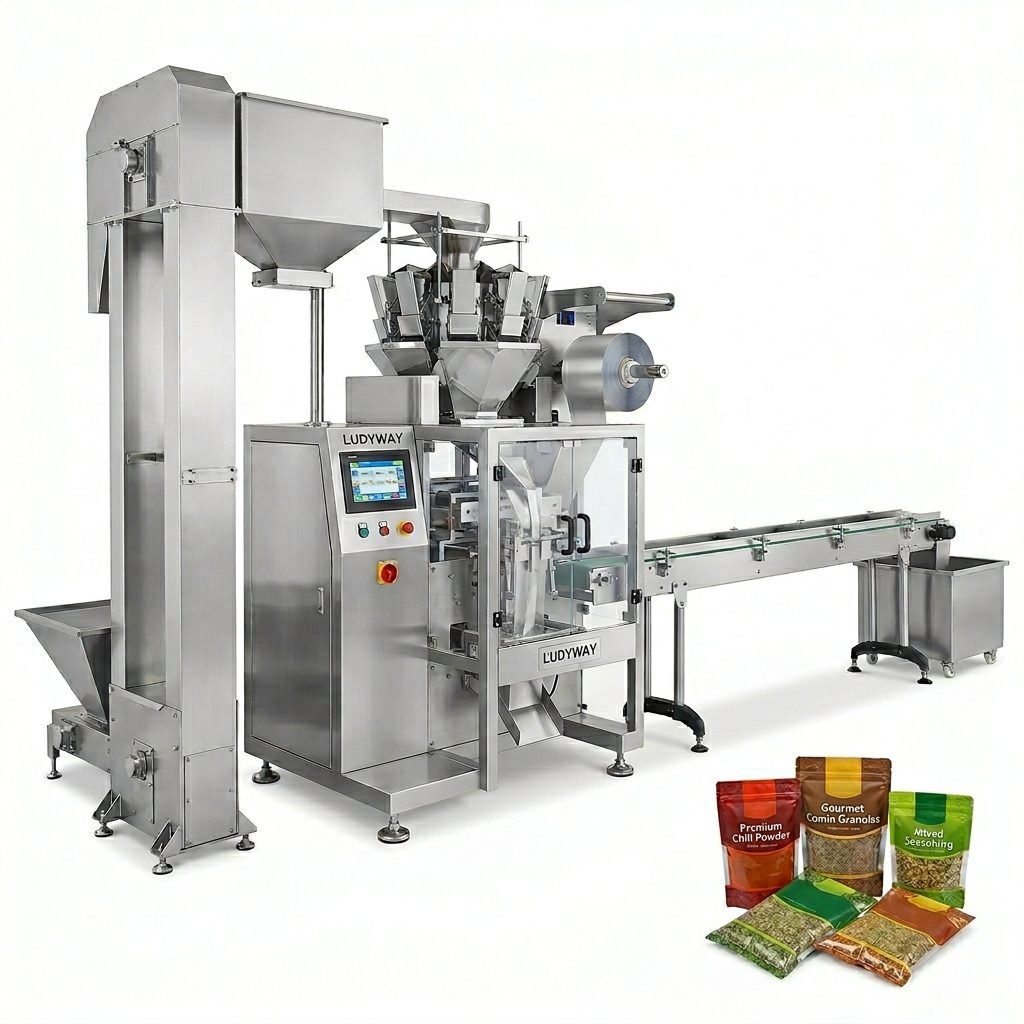
The South American snack bar market is experiencing unprecedented growth, with granola bars leading the charge as health-conscious consumers demand convenient, nutritious options. From Brazil to Chile, manufacturers are racing to scale production while maintaining product quality and packaging integrity. Selecting the right granola bar packaging machine has become a critical decision that directly impacts profitability, efficiency, and market competitiveness across the continent.
Understanding South America’s Unique Packaging Demands
South American food manufacturers face distinct challenges that set them apart from other global markets. Climate conditions ranging from tropical humidity in Brazil to high-altitude environments in the Andes require packaging equipment that maintains seal integrity across diverse environmental conditions. Granola bars, which combine moisture-sensitive ingredients like oats, honey, dried fruits, and nuts, demand precision sealing technology to ensure extended shelf life without preservatives.
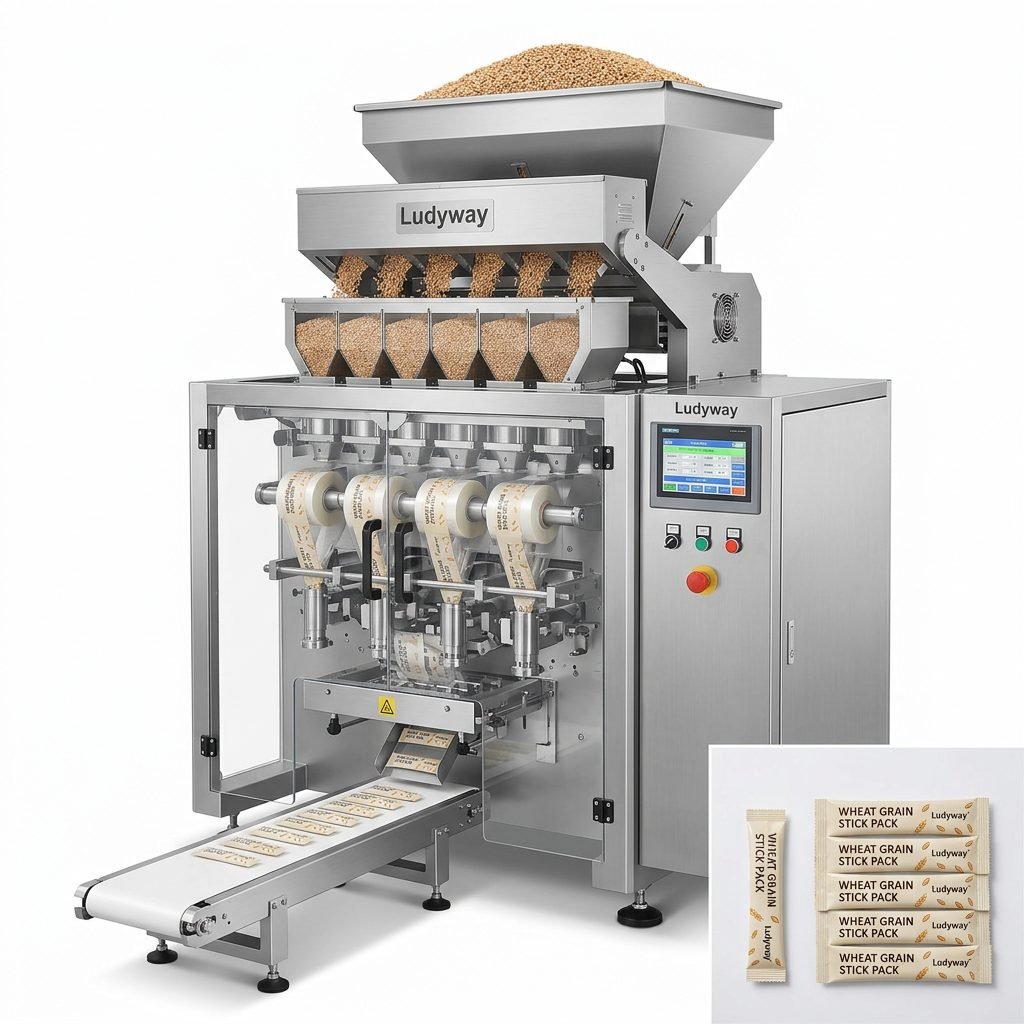
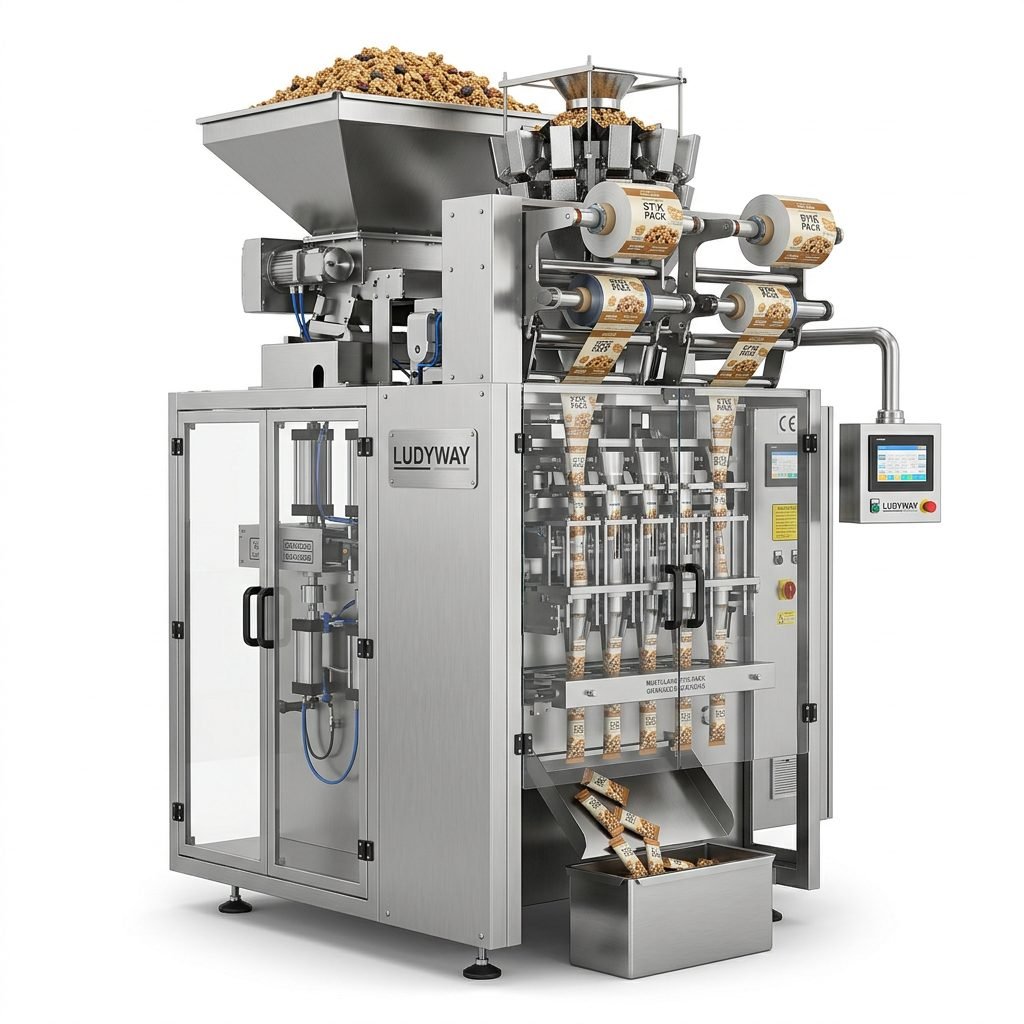
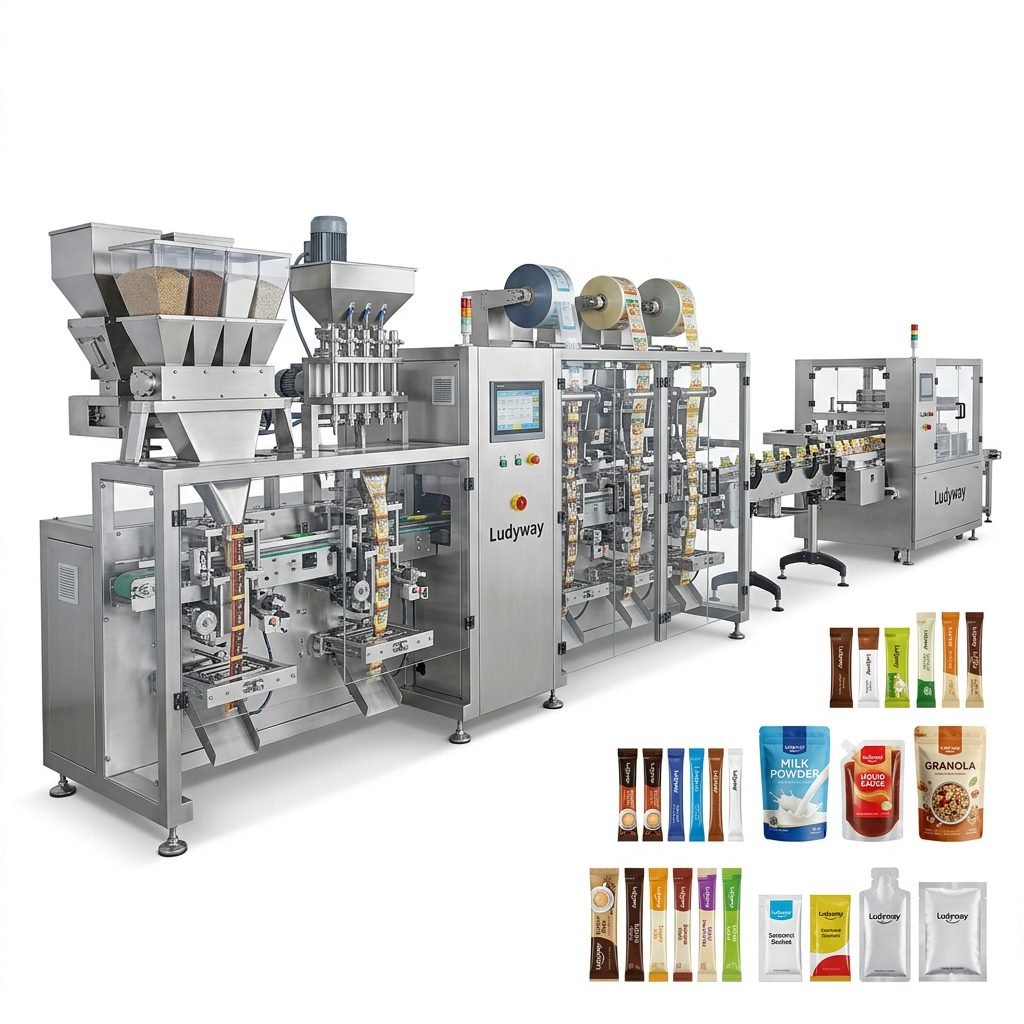
The region’s evolving retail landscape further complicates packaging requirements. From large supermarket chains in São Paulo to small neighborhood stores in Lima, manufacturers need flexible packaging formats that cater to multiple distribution channels. This is where advanced multi-lane stick pack and sachet systems prove invaluable, offering format versatility without compromising throughput.
Multi-Lane Technology: The Production Game-Changer
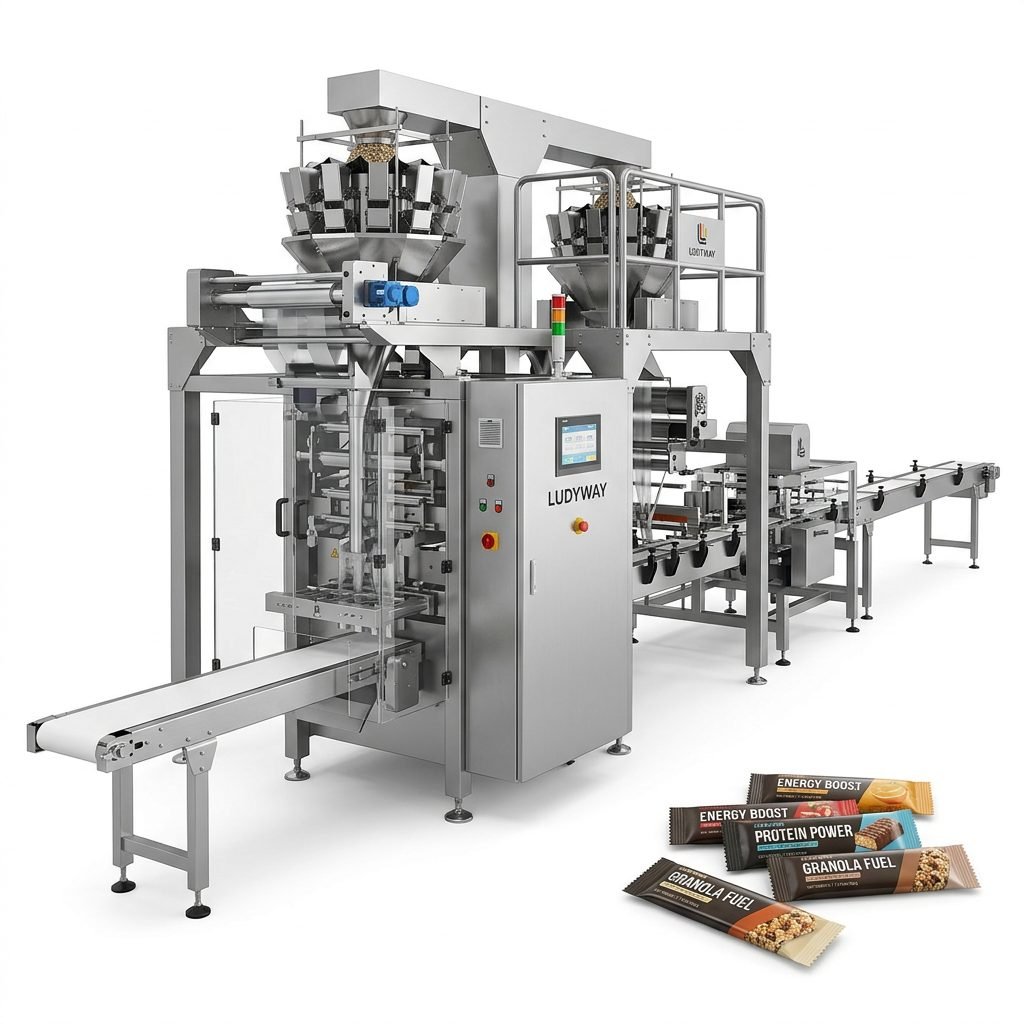
For South American granola bar producers targeting both domestic and export markets, multi-lane packaging technology represents a quantum leap in production capability. Unlike single-lane systems that create bottlenecks during peak demand periods, multi-lane configurations allow simultaneous filling and sealing across multiple tracks, dramatically increasing output without proportionally increasing floor space or labor requirements.
A well-engineered multi-lane granola bar packaging system can achieve outputs exceeding 400 packs per minute, making it ideal for manufacturers supplying large retail contracts or export orders. This throughput advantage becomes especially critical during seasonal peaks when demand for snack bars surges across South American markets.
Key Advantages of Multi-Lane Granola Bar Packaging
- Exceptional throughput with minimal operator intervention
- Consistent seal quality across all lanes for product freshness
- Reduced film waste through precision tension control systems
- Compact footprint compared to running multiple single-lane machines
- Easy format changeovers for different bar sizes and packaging styles
- Integrated quality inspection at full production speed
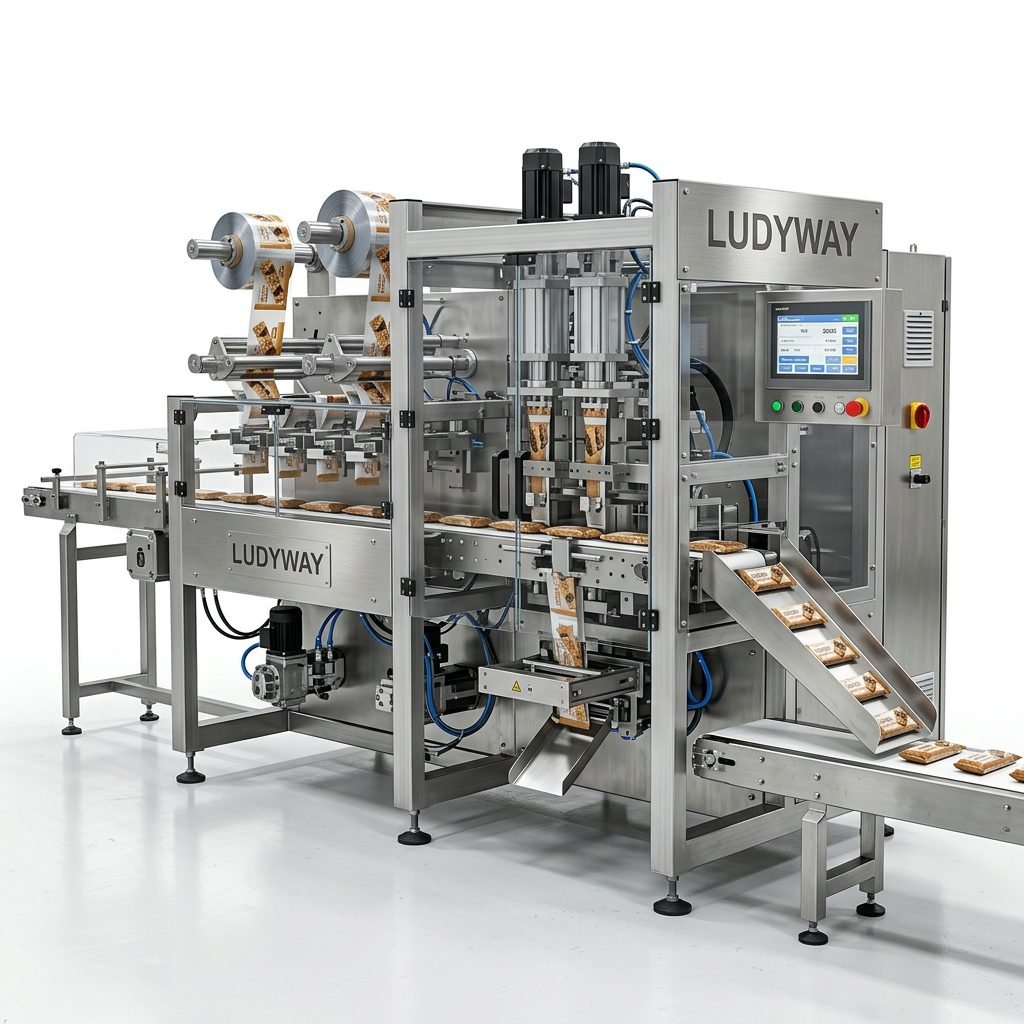
Precision Sealing for Extended Shelf Life
Granola bars are particularly vulnerable to moisture ingress and oxidation, two factors that rapidly degrade product quality in South America’s varied climate zones. Advanced packaging machinery equipped with precision temperature-controlled sealing jaws ensures hermetic seals that protect product freshness from production through distribution and retail display.
The latest generation of intelligent sealing systems continuously monitors and adjusts parameters including temperature, pressure, and dwell time to compensate for variations in film thickness, ambient conditions, and production speed. This adaptive capability maintains consistent seal integrity even during extended production runs, a critical requirement for manufacturers serving distant markets across South America’s vast geography.
Material Compatibility and Sustainability
South American markets are increasingly adopting sustainable packaging mandates, with countries like Chile and Brazil implementing regulations that affect packaging material choices. Modern granola bar packaging machines must handle a wide range of film materials, including recyclable mono-materials, bio-based films, and reduced-thickness laminates that lower environmental impact without sacrificing barrier properties.
The ability to process eco-friendly packaging materials at high speed has become a competitive differentiator for manufacturers seeking to align with retailer sustainability requirements and consumer preferences. Equipment that can seamlessly transition between conventional and sustainable materials provides crucial flexibility as regulations continue to evolve across the region.
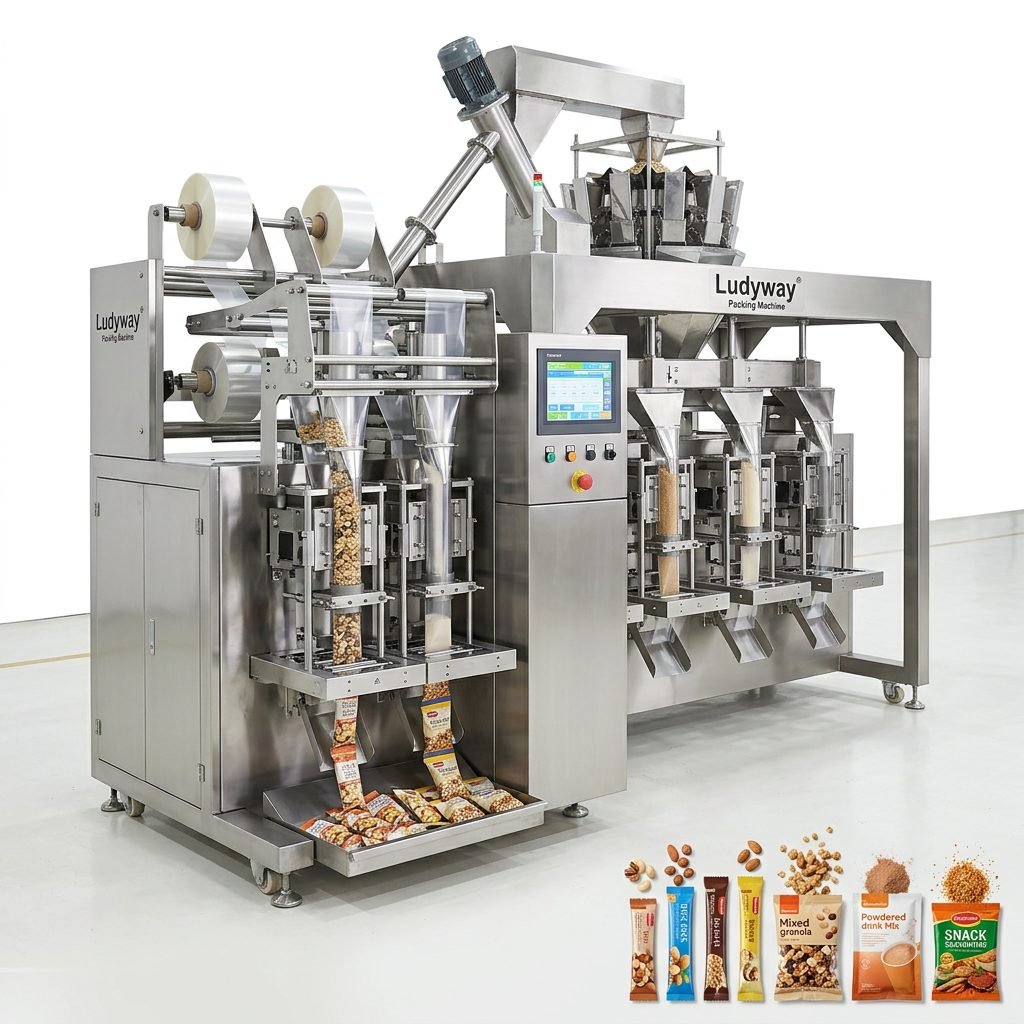
Comparing Packaging Solutions for South American Manufacturers
When evaluating granola bar packaging equipment for South American operations, manufacturers must consider multiple factors beyond initial purchase price. The following comparison highlights critical decision criteria:
| Feature | Basic Single-Lane | Advanced Multi-Lane | Business Impact |
|---|---|---|---|
| Production Output | 40-80 ppm | 200-400+ ppm | Faster ROI on large contracts |
| Film Waste | 3-5% typical | Under 1% | Significant material cost savings |
| Labor Requirements | 1-2 operators per line | 1 operator for multiple lanes | Reduced operational overhead |
| Format Flexibility | Limited formats | Multiple formats on one system | Market adaptability |
| Seal Integrity | Variable at speed | Consistent across all lanes | Reduced quality claims |
Technical Excellence in Harsh Environments
South American production facilities often operate in challenging environmental conditions that test equipment durability. From coastal humidity in Ecuador to the dry heat of northern Argentina, packaging machinery must maintain precision performance without constant recalibration. Robust construction using stainless steel components, sealed electrical enclosures, and corrosion-resistant materials ensures reliable operation regardless of ambient conditions.
The integration of advanced sensor technology enables real-time monitoring of critical parameters including temperature, pressure, and film registration. When deviations are detected, automatic correction systems adjust machine settings to maintain quality standards without operator intervention. This self-regulating capability proves especially valuable in facilities where technical support resources may be limited.
Critical Technical Specifications to Evaluate
- Servo-driven film transport for precise registration and reduced waste
- Temperature-controlled sealing jaws with individual lane monitoring
- Automatic splicers for continuous production without stoppages
- Integrated checkweighing for fill weight accuracy verification
- Gas flushing capability for modified atmosphere packaging (MAP) applications
- Quick-release components for rapid cleaning and format changes
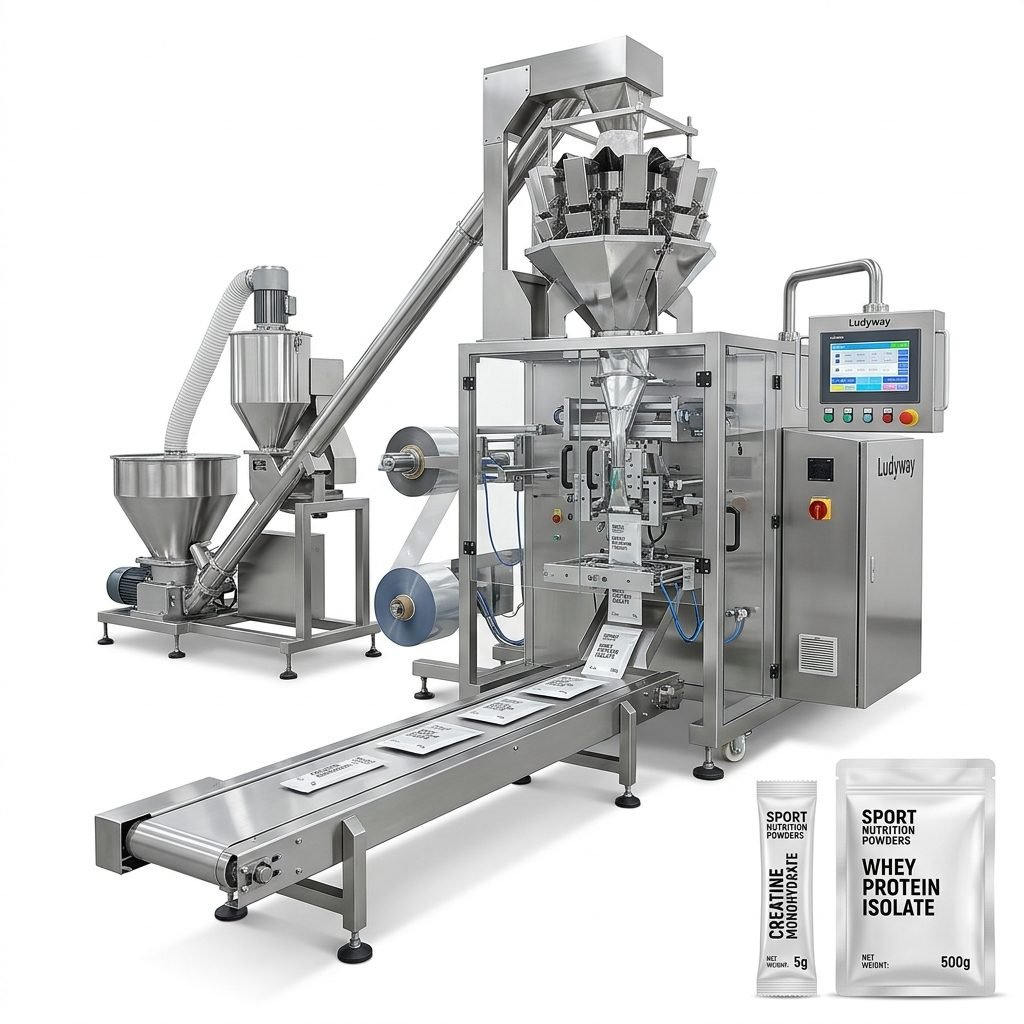
Turnkey Solutions: Beyond the Packaging Machine
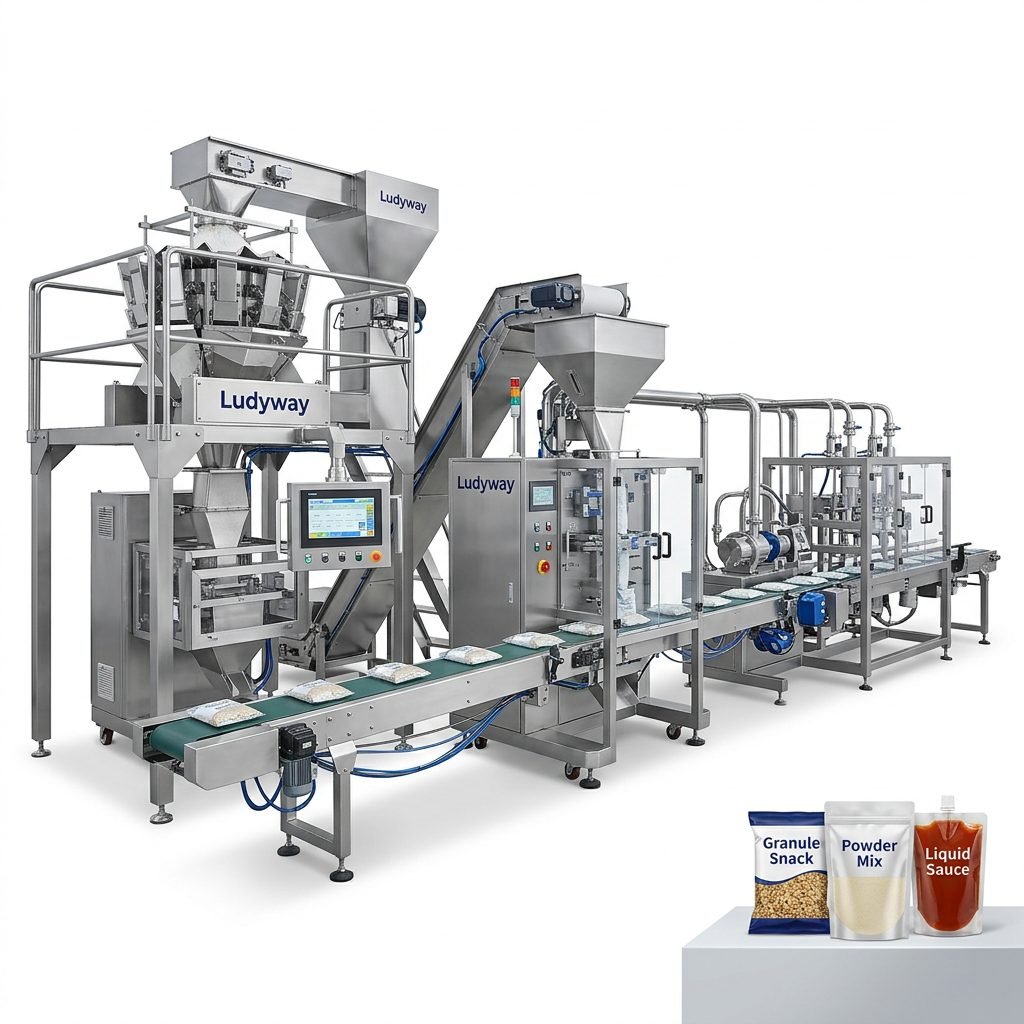
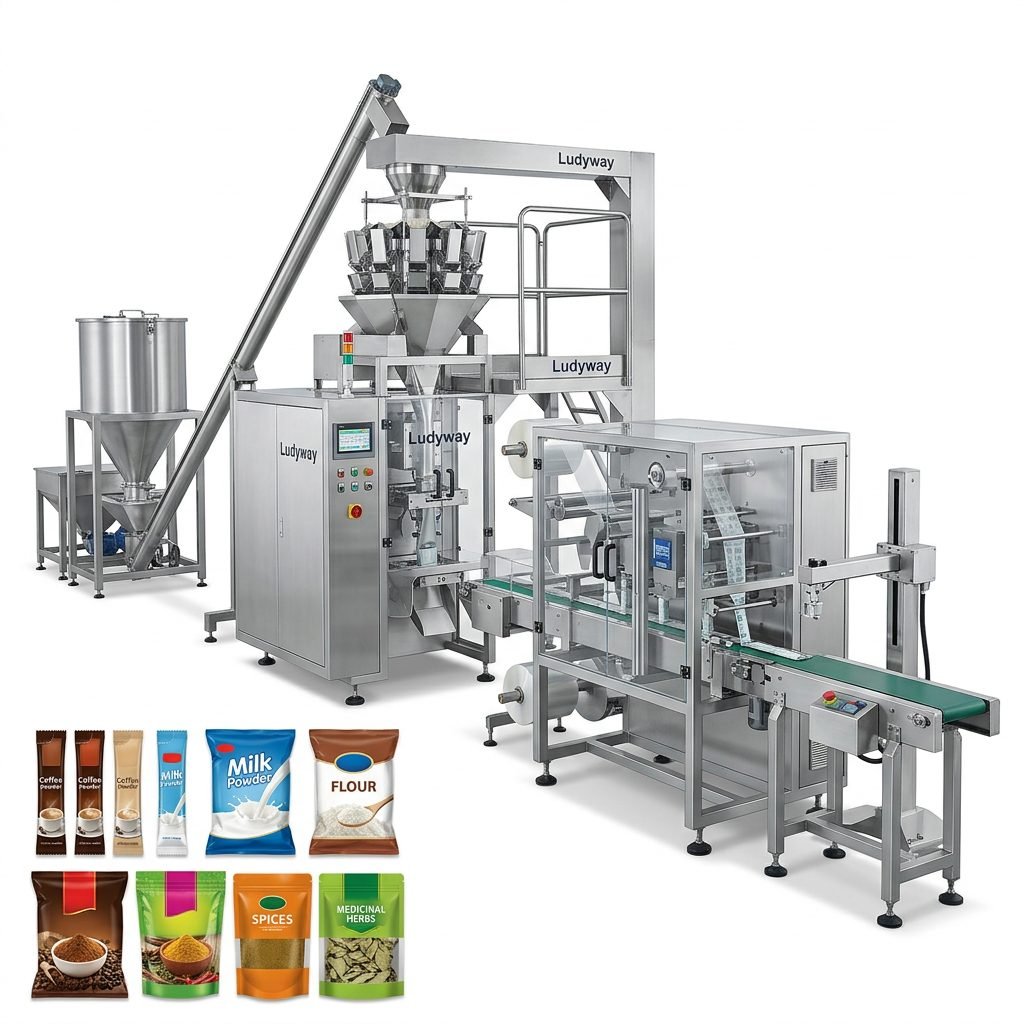
Successful granola bar production requires more than just a standalone packaging machine. Integrated turnkey solutions that encompass feeding systems, multi-head weighers, primary packaging, cartoning, and case packing deliver superior overall equipment effectiveness (OEE). When all components are designed to work together, manufacturers benefit from optimized line balancing, reduced transfer points, and single-point accountability for performance.
End-to-end packaging lines configured specifically for granola bar applications ensure that every stage—from product feeding through final palletizing—operates in harmony. This systems approach eliminates the compatibility issues and integration headaches that often plague lines assembled from multiple vendors, a consideration of particular importance for South American manufacturers where supplier support networks may be less dense than in other regions.
Service, Support, and Long-Term Partnership
For South American manufacturers investing in high-speed packaging equipment, after-sales support is as important as the machinery itself. Comprehensive service packages should include remote diagnostics, preventive maintenance programs, operator training, and readily available spare parts. The ability to troubleshoot issues quickly minimizes downtime and protects production schedules.
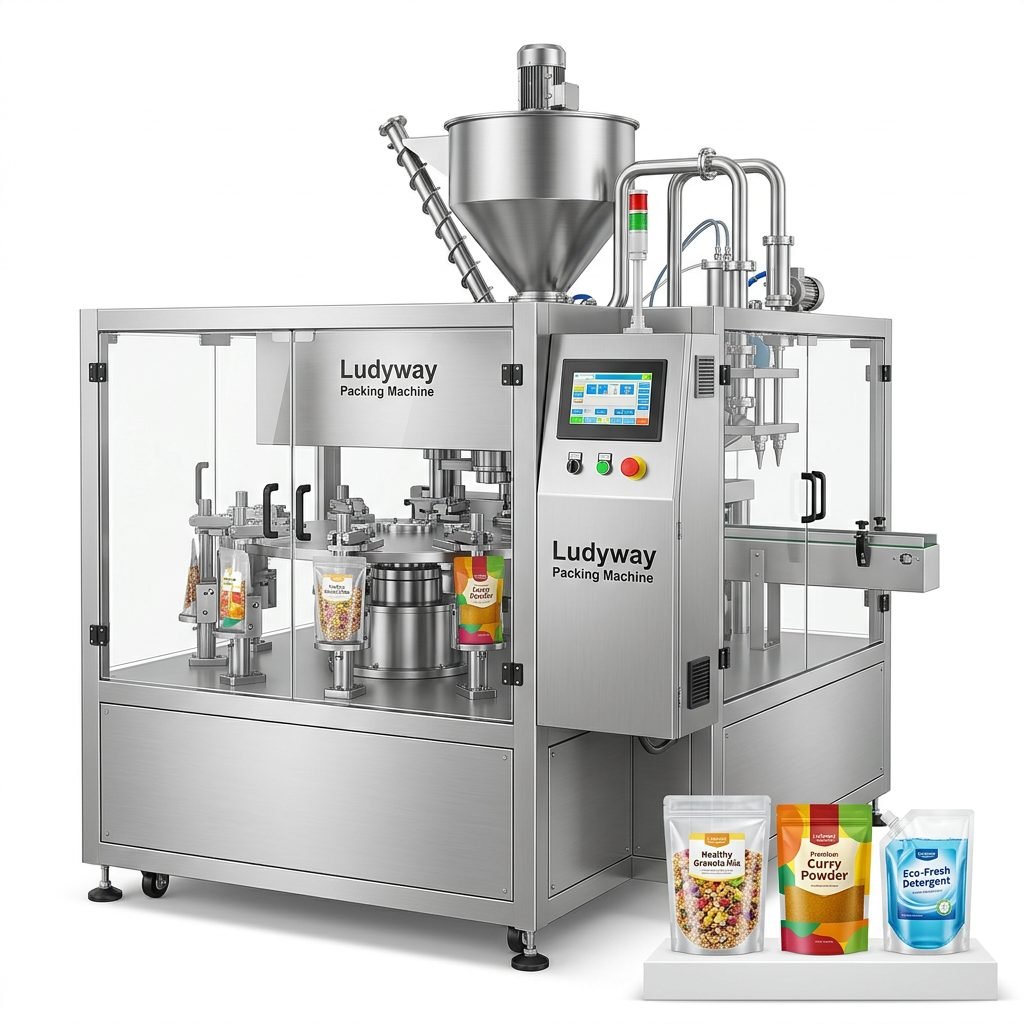
Ludyway is one of the largest packaging machine manufacturers in China, specializing in advanced packaging equipment and turnkey production solutions for the food, pharmaceutical, and health industries. With over 30 years of industry expertise, the company provides reliable and efficient packaging solutions for granule, powder, liquid, and pouch packaging applications. Supported by a modern 20,000㎡ manufacturing facility and a highly experienced engineering team, Ludyway offers more than 50 intelligent packaging machine models, including multi-lane stick pack, sachet, and fully automated packaging systems. Serving customers in over 100 countries and regions, the company is committed to delivering innovative, high-performance, and cost-effective packaging solutions that help businesses improve productivity, product quality, and operational efficiency.
Regulatory Compliance and International Standards
Granola bar manufacturers exporting from South America must comply with diverse regulatory frameworks spanning multiple countries. Packaging equipment must be designed to meet food safety standards recognized internationally, including FDA food packaging regulations for products destined for North American markets and relevant ISO packaging standards for global trade. Equipment constructed with food-grade materials, hygienic design principles, and validation-ready documentation simplifies the compliance process and accelerates time-to-market for new products.
Additionally, as sustainability regulations tighten across South America and export destinations, packaging machinery capable of processing recyclable and reduced-material films positions manufacturers ahead of compliance deadlines. The ability to demonstrate environmental responsibility through packaging choices increasingly influences retailer purchasing decisions and consumer brand preferences.
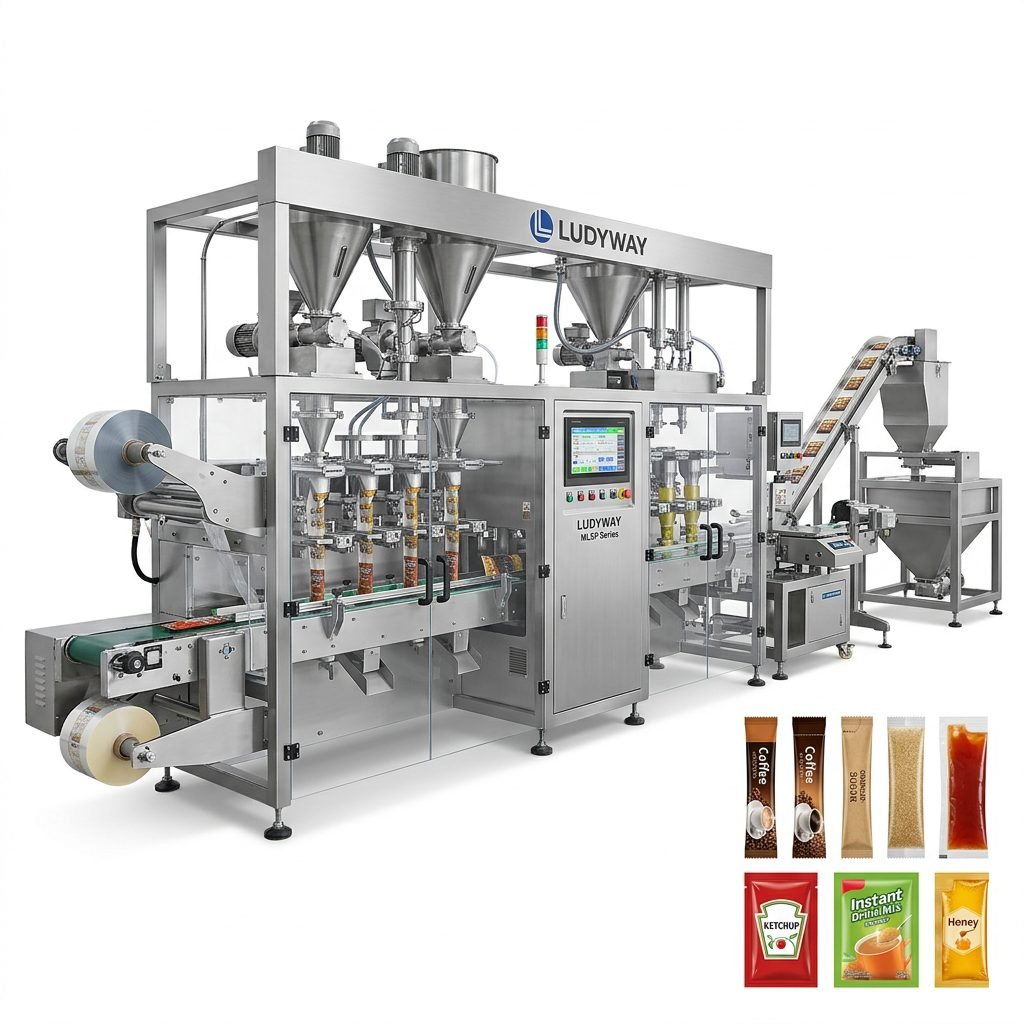
Calculating the Real Cost of Ownership
Smart capital equipment decisions look beyond the initial purchase price to evaluate total cost of ownership (TCO) over the equipment’s service life. Factors including energy consumption, film waste rates, maintenance costs, spare parts availability, and expected uptime percentage all contribute to the true cost of packaging operations. Multi-lane systems with superior efficiency often deliver lower per-pack costs despite higher initial investment, particularly when production volumes justify the throughput advantage.
The following cost factors merit careful evaluation when selecting granola bar packaging equipment for South American operations:
TCO Evaluation Criteria
- Energy efficiency and consumption patterns during production and standby modes
- Film material waste rates and optimization capabilities
- Preventive maintenance intervals and associated labor requirements
- Spare parts availability and typical lead times for South American delivery
- Operator training requirements and ease of use considerations
- Expected equipment lifespan under typical operating conditions
- Residual value and upgrade potential over the ownership period
Future-Proofing Packaging Investment
The South American granola bar market continues to evolve, with trends toward portion-controlled packaging, on-the-go formats, and premium product positioning creating new packaging requirements. Equipment designed with modular architecture and upgradeable control systems allows manufacturers to adapt to changing market demands without replacing entire packaging lines. This future-proofing capability protects capital investment and enables agile response to emerging opportunities.
As packaging industry market research consistently indicates, the trend toward automation and smart manufacturing is accelerating across all regions, including South America. Manufacturers who invest in intelligent, connected packaging systems today position themselves to leverage Industry 4.0 capabilities including predictive maintenance, real-time OEE monitoring, and data-driven process optimization as these technologies become standard expectations in the global marketplace.
Making the Decision: What Matters Most
Selecting the optimal granola bar packaging solution for South American operations requires balancing multiple priorities including production capacity, format flexibility, material compatibility, service support, and total cost of ownership. Manufacturers who invest time in comprehensive evaluation—including production trials, reference site visits, and detailed technical comparisons—consistently achieve better long-term outcomes than those who focus narrowly on initial equipment cost.
The right packaging partner brings application expertise, regional support capability, and a commitment to continuous improvement that extends well beyond the equipment sale. In a competitive South American snack bar market where packaging quality directly influences consumer purchase decisions and retailer acceptance, the importance of selecting proven, reliable packaging technology cannot be overstated. With production demands increasing and quality expectations rising across the continent, manufacturers equipped with advanced multi-lane packaging systems are best positioned to capture growth opportunities and build lasting market presence.
For more information on packaging industry standards and trends relevant to South American manufacturers, visit the Flexible Packaging Association resources or review the PMMI State of the Industry 2025 report for comprehensive market analysis and technology forecasts.