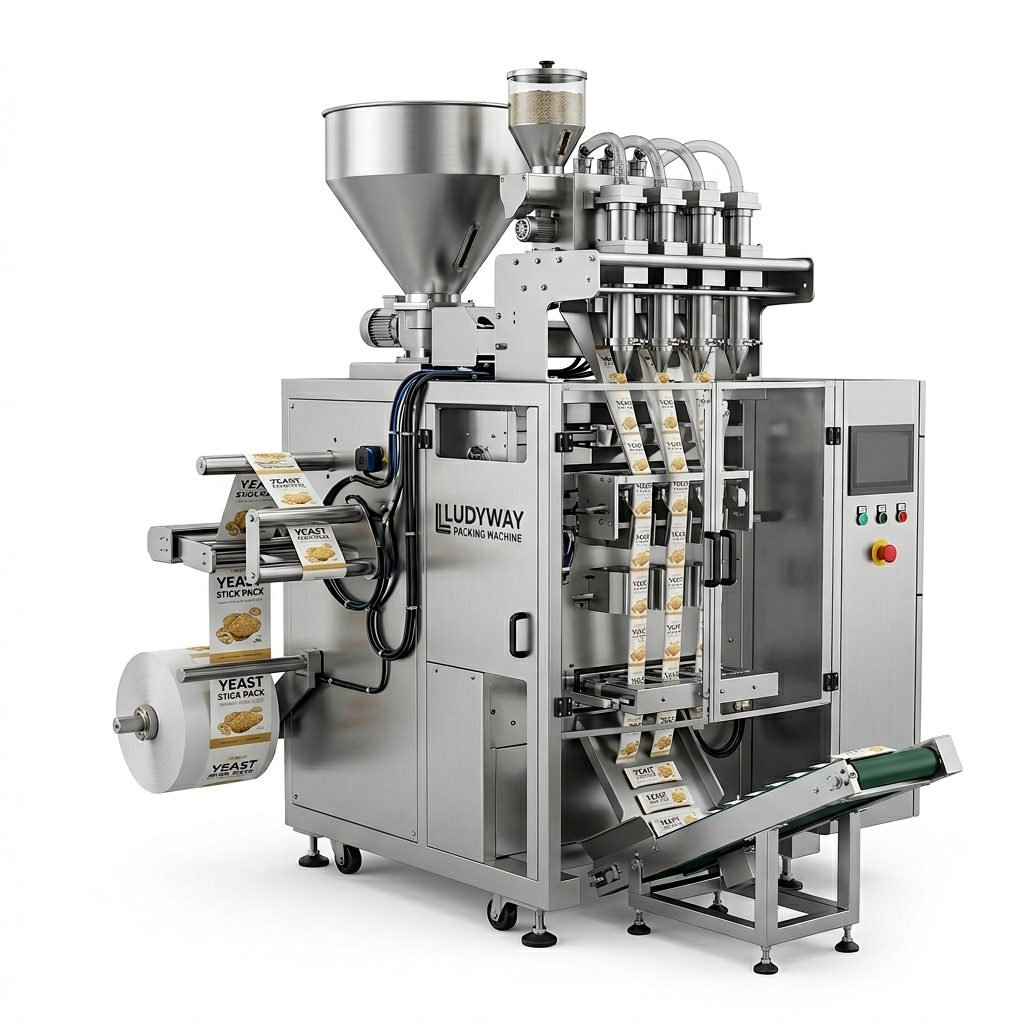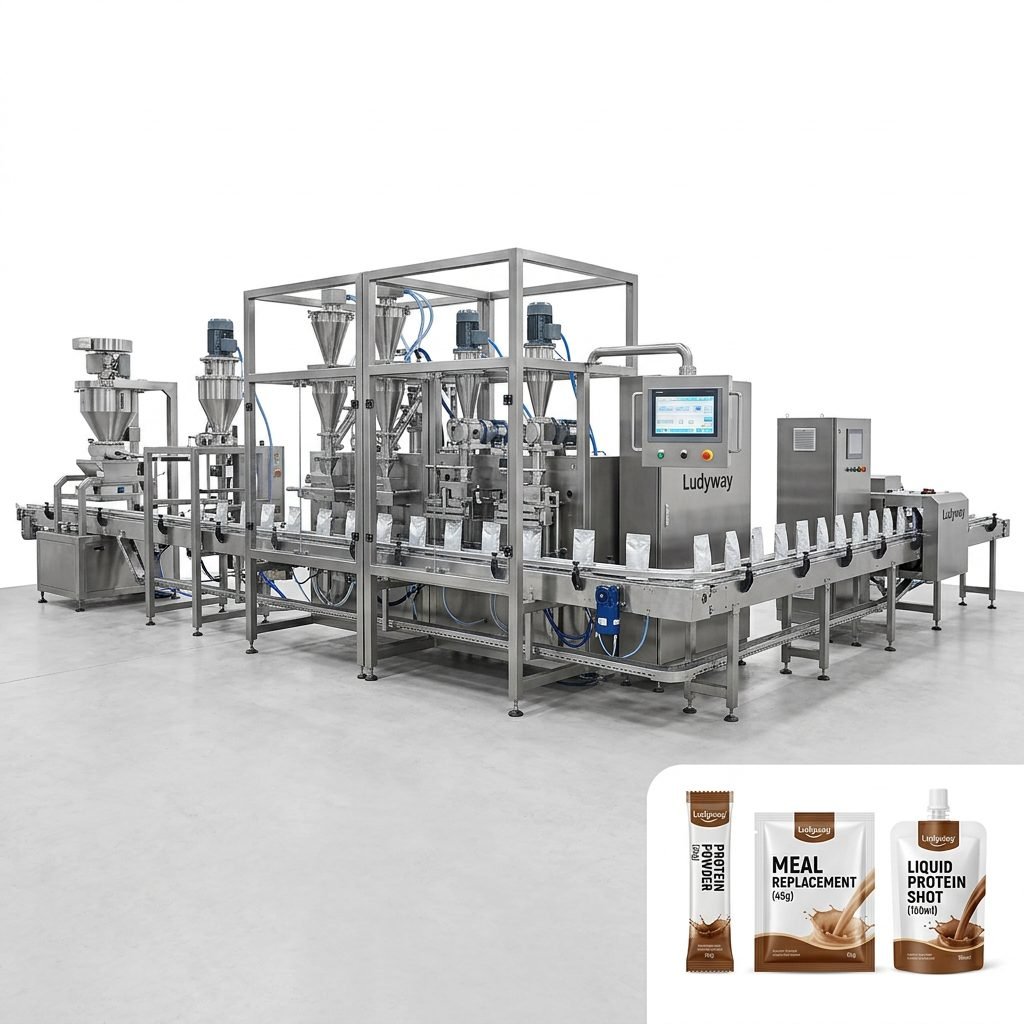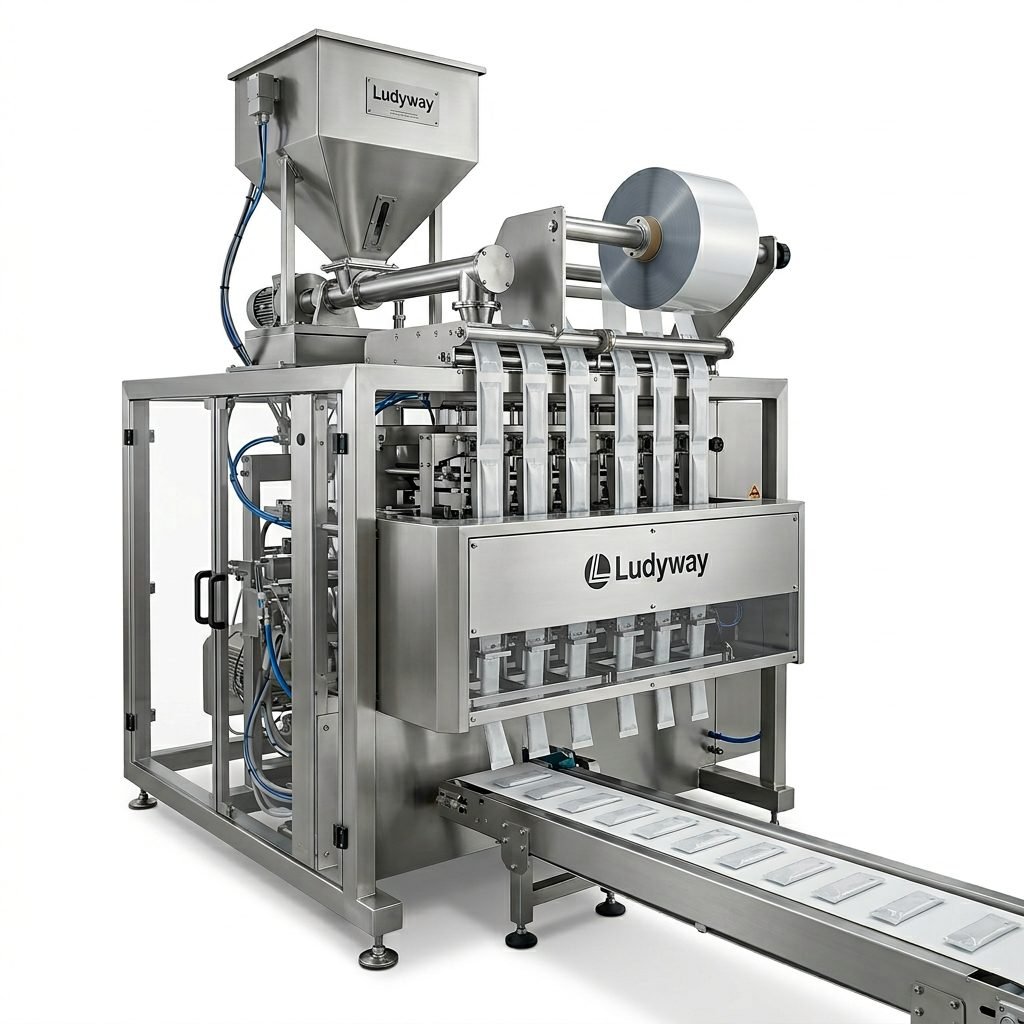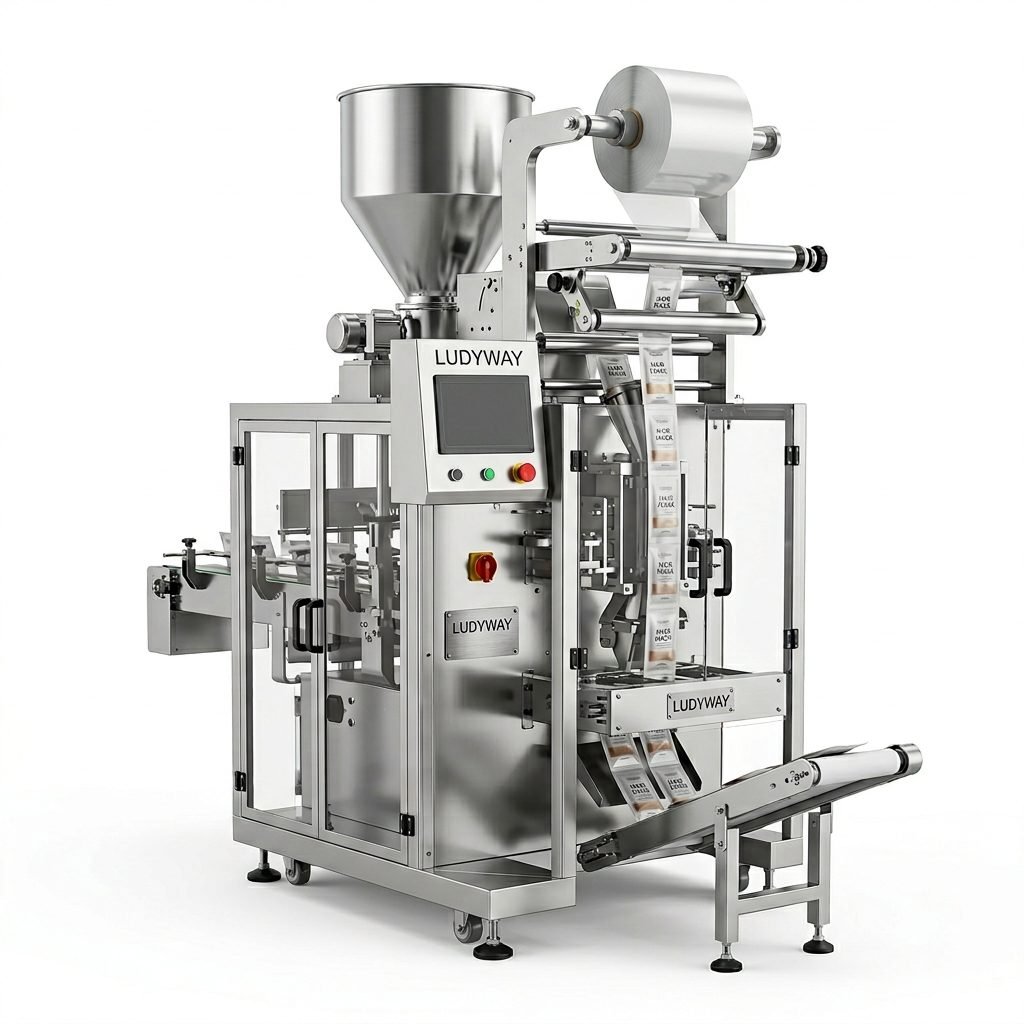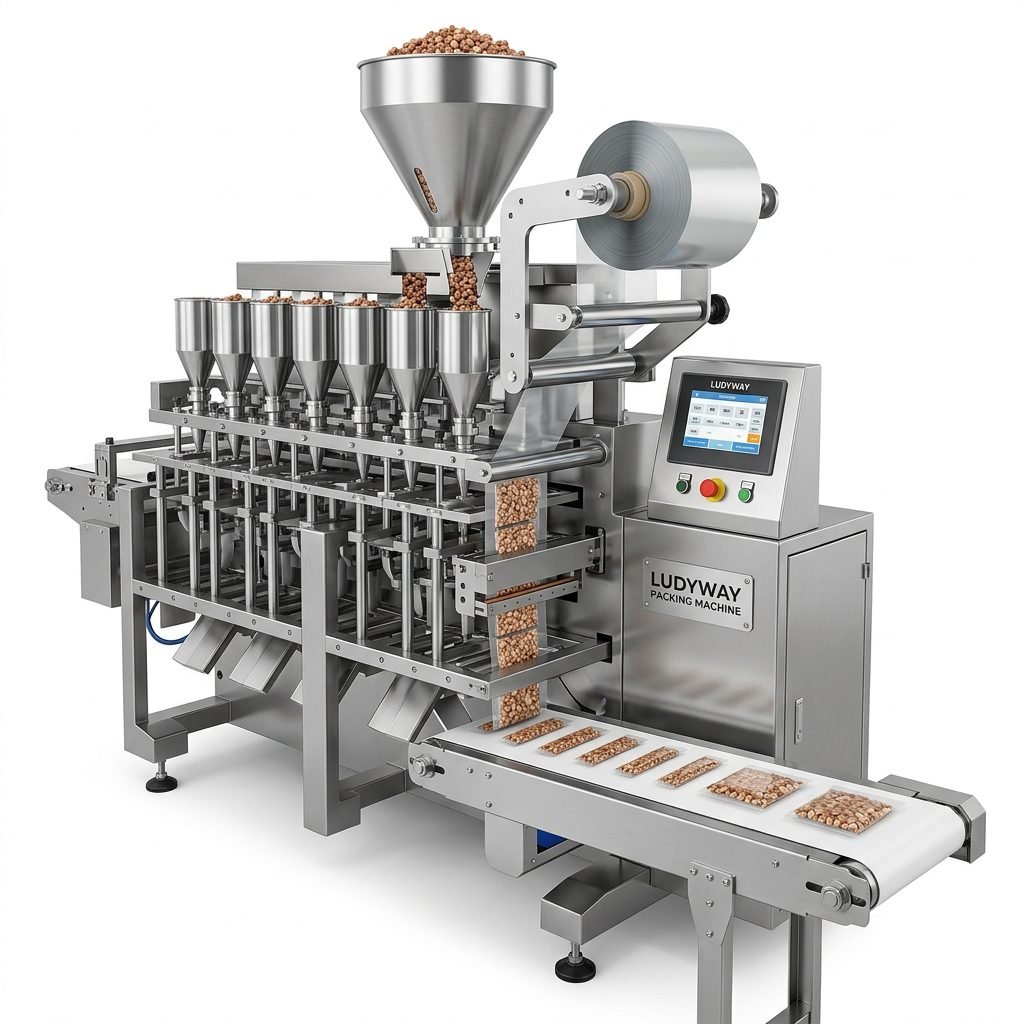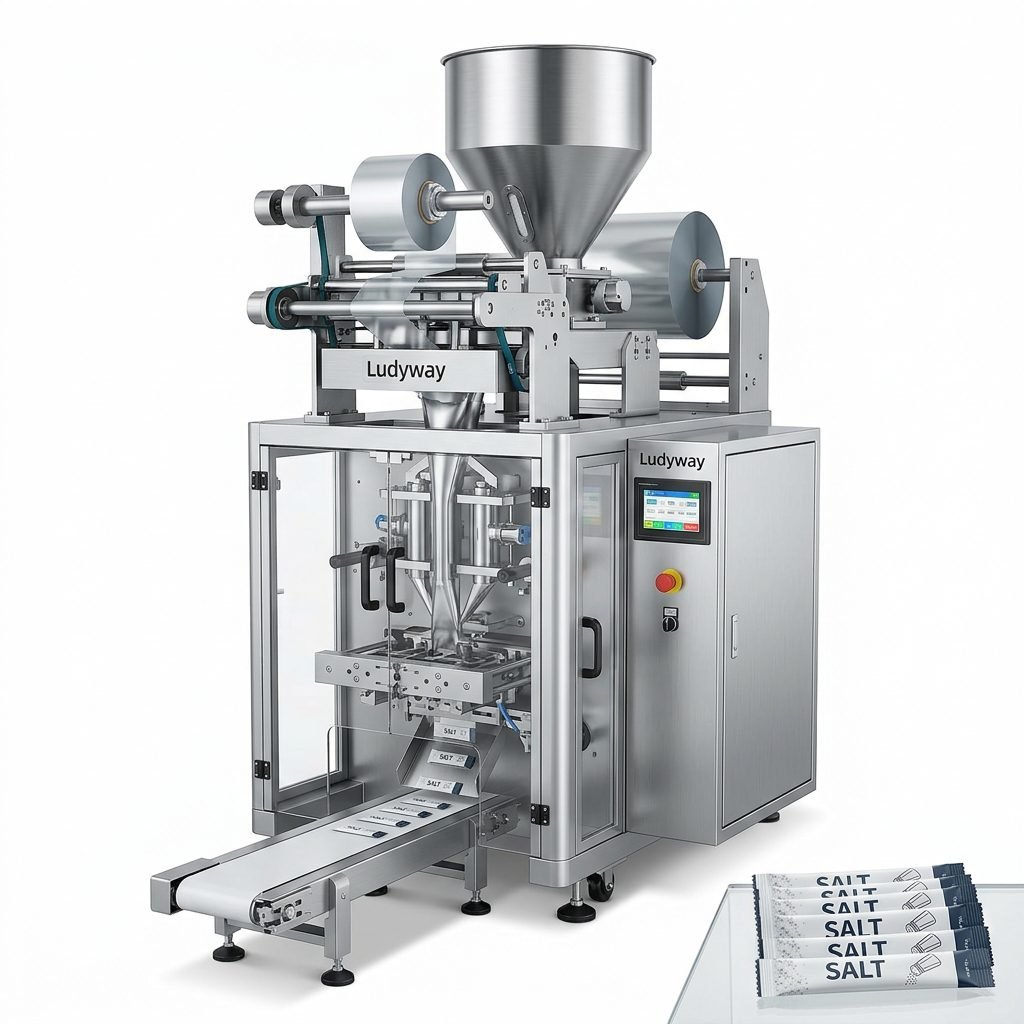
The North American frozen novelty market continues to expand rapidly, driving unprecedented demand for high-performance popsicle packaging machinery. Whether you’re producing water-based ice pops, cream-filled frozen treats, or yogurt-dipped bars, selecting the right packaging automation equipment directly impacts your production efficiency, product shelf life, and bottom line.
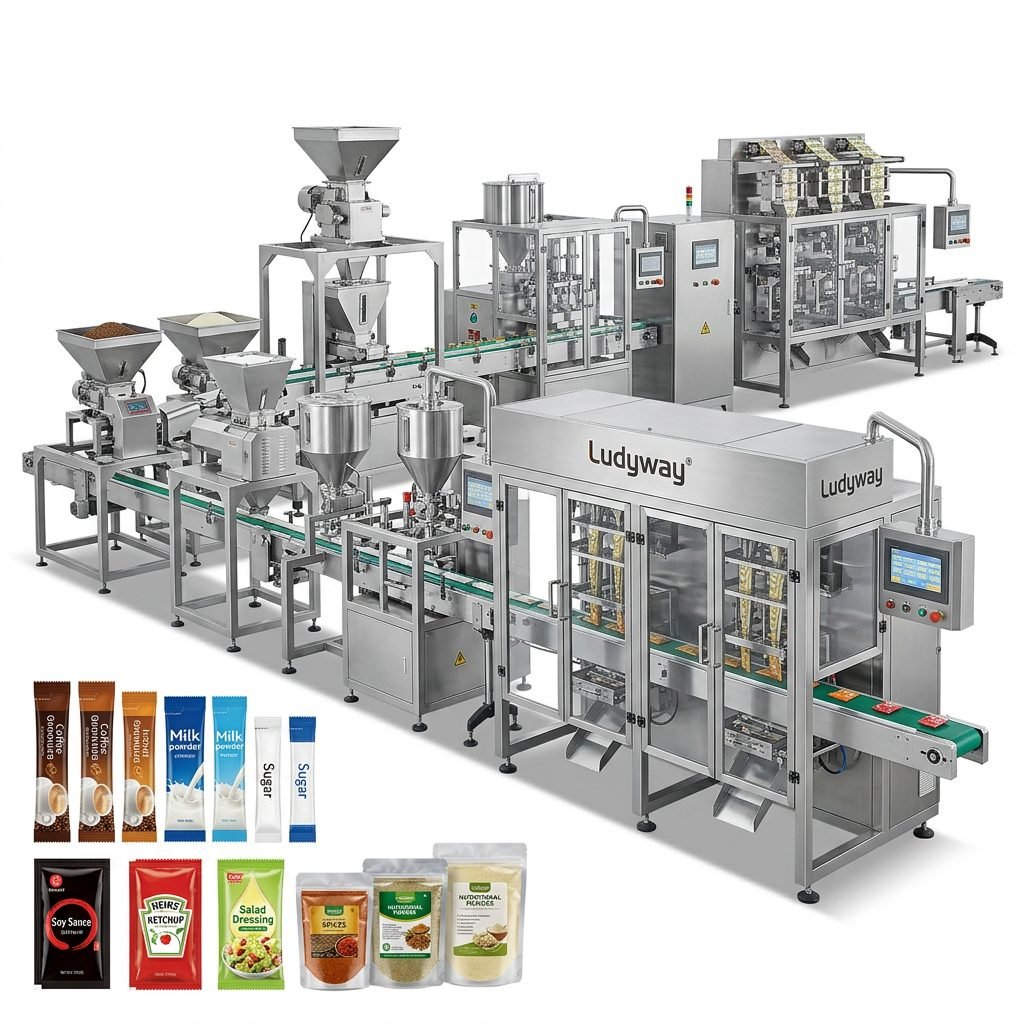
Understanding the Popsicle Packaging Challenge
Packaging frozen novelties presents unique technical challenges that standard packaging machines simply cannot handle. Temperature fluctuations, condensation, stick insertion accuracy, and high-speed wrapping requirements all demand specialized engineering. A purpose-built popsicle packaging machine must deliver:
- Cold-temperature tolerance – Reliable operation in sub-zero production environments
- Precision stick handling – Accurate placement without product damage at high speeds
- Moisture-resistant sealing – Hermetic seals that prevent freezer burn and contamination
- Multi-format flexibility – Quick changeover between single-serve and multi-pack configurations
- Hygienic design compliance – Meeting FDA food packaging standards
Key Features to Look For in a Popsicle Packaging System
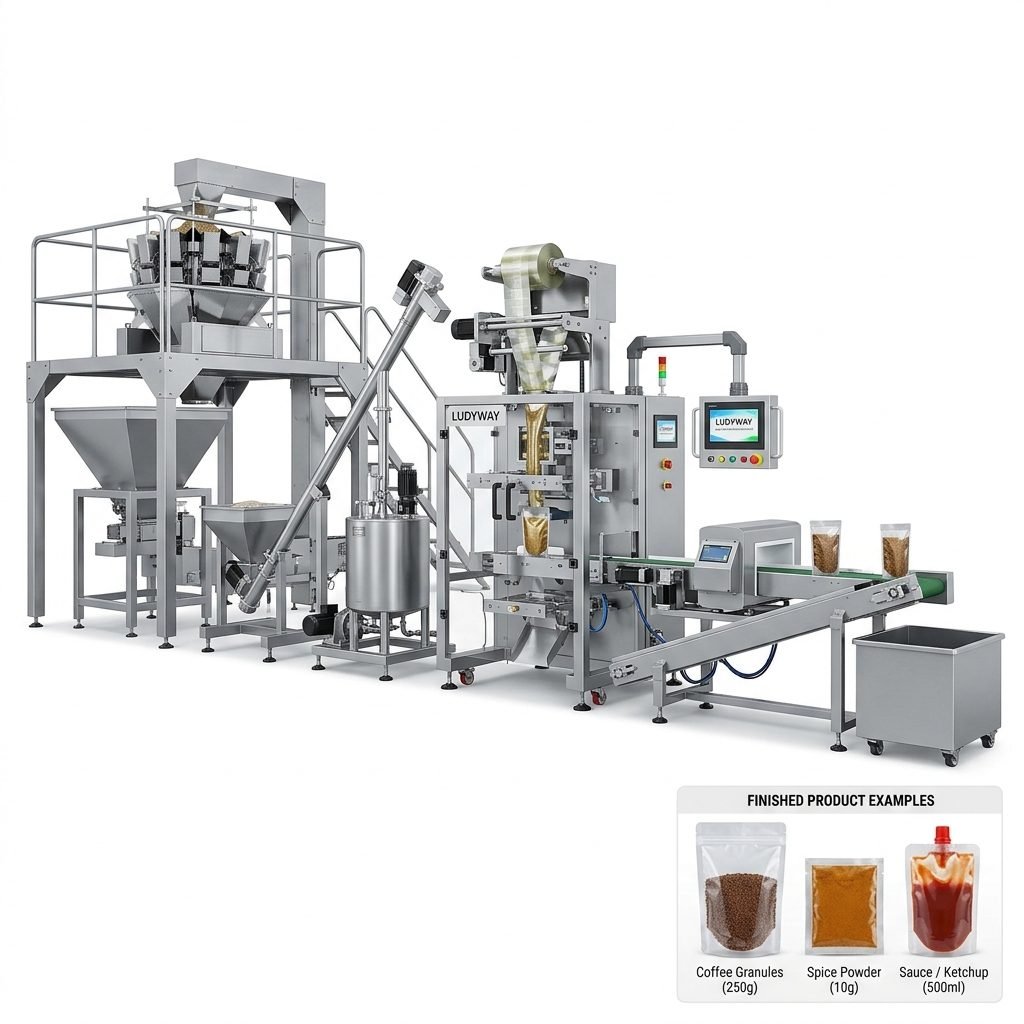
When evaluating equipment for frozen novelty packaging, manufacturers should prioritize systems that integrate seamlessly with existing production infrastructure. The most advanced solutions on the market combine multi-lane wrapping technology with intelligent monitoring systems that minimize waste and maximize throughput.
Critical Performance Specifications
Modern popsicle packaging lines must consistently deliver speeds of 150-300 units per minute while maintaining precise film registration and seal integrity. Servo-driven film transport systems have largely replaced mechanical drives, offering superior accuracy and reduced maintenance requirements.
Comparing Packaging Machine Technologies
Not all packaging equipment is created equal. The table below illustrates key differences between standard and specialized frozen novelty packaging systems:
| Feature | Standard Machines | Specialized Popsicle Systems |
|---|---|---|
| Temperature Range | Ambient only | Down to -30°C continuous operation |
| Stick Insertion | Not available | Automated precision placement ±0.5mm |
| Film Compatibility | Limited cold-seal options | Multi-layer barrier films optimized for frozen |
| Cleaning Protocol | Standard washdown | IP65-rated hygienic design with CIP capability |
| Speed Capacity | 60-120 ppm typical | 150-300+ ppm sustained |
Why North American Manufacturers Choose Turnkey Solutions
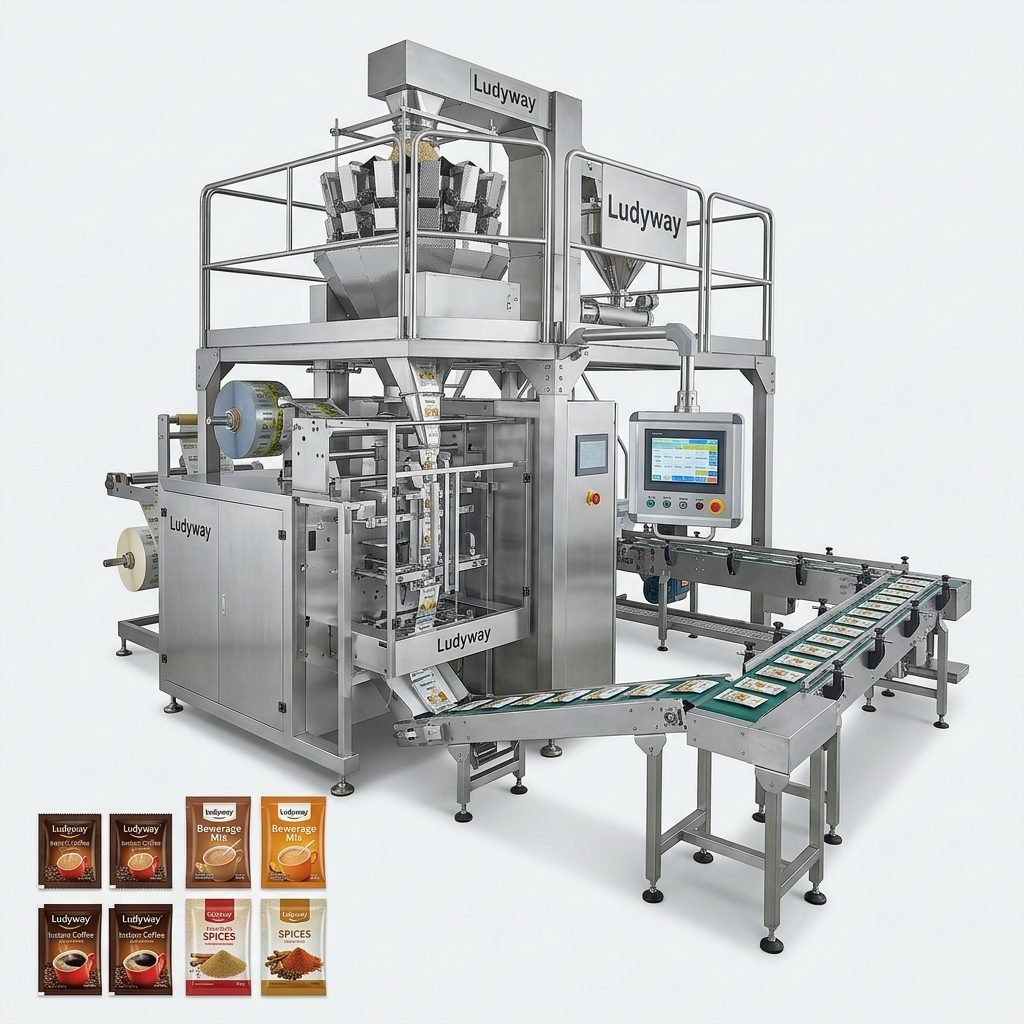
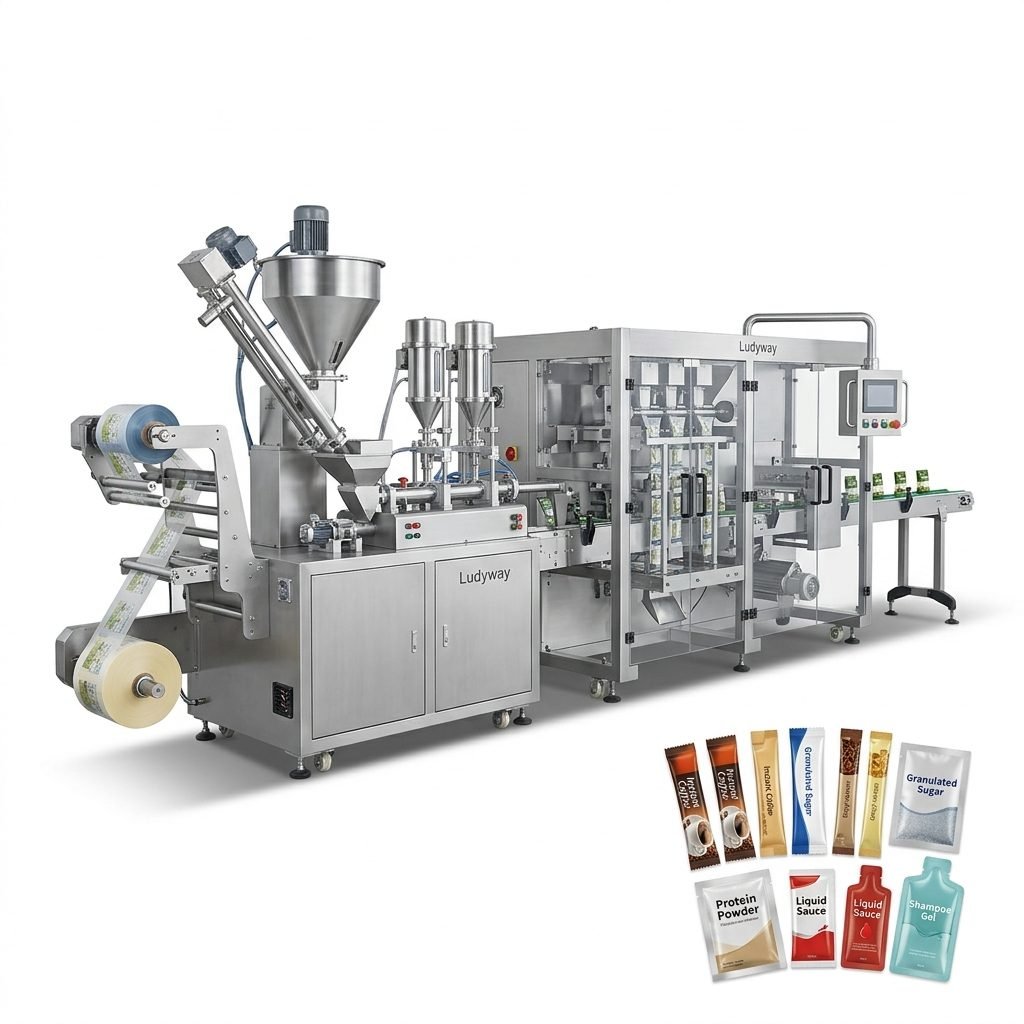
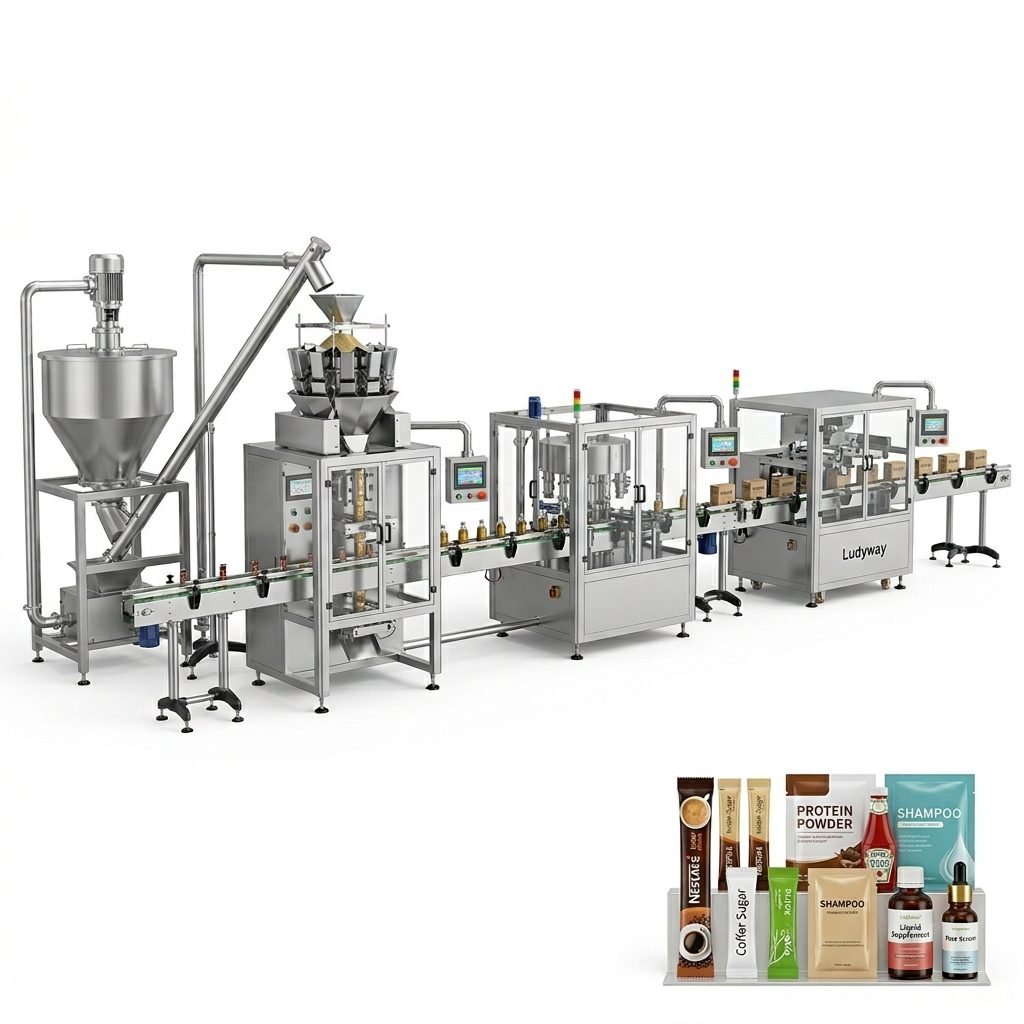
The shift toward integrated packaging systems reflects the growing complexity of frozen novelty production. Rather than piecing together equipment from multiple suppliers, manufacturers increasingly opt for turnkey packaging lines that include everything from PACK EXPO verified filling and wrapping to cartoning and palletizing.
Benefits of an Integrated Approach
- Single-source accountability – One partner for design, installation, and support
- Optimized throughput – Synchronized speeds across all line components
- Reduced footprint – Compact layouts designed for maximum efficiency
- Faster ROI – Streamlined commissioning and ramp-up to full production
- Simplified training – Unified control interfaces reduce operator learning curves
Material Handling Considerations for Frozen Production
The cold chain demands special attention to material compatibility. Popsicle packaging films must maintain seal strength at temperatures as low as -40°F while resisting brittleness that leads to micro-leaks. Advanced multi-layer polyethylene and polypropylene laminates with cold-seal adhesives have become the industry standard, offering excellent clarity for product visibility while providing robust barrier properties.
Regulatory Compliance and Food Safety
Any popsicle packaging machine deployed in North America must comply with a comprehensive framework of regulations. Equipment should be designed in accordance with ISO packaging standards and meet the requirements of 21 CFR Part 110 for food manufacturing facilities. Stainless steel construction, accessible clean-in-place systems, and validated sanitation protocols are non-negotiable features.
Essential Certifications
- UL/CSA electrical certification for North American installations
- 3-A Sanitary Standards compliance for dairy-based products
- HACCP-ready design with full traceability documentation
- CE marking with equivalent ANSI/PMMI safety standards
The Ludyway Advantage in Popsicle Packaging
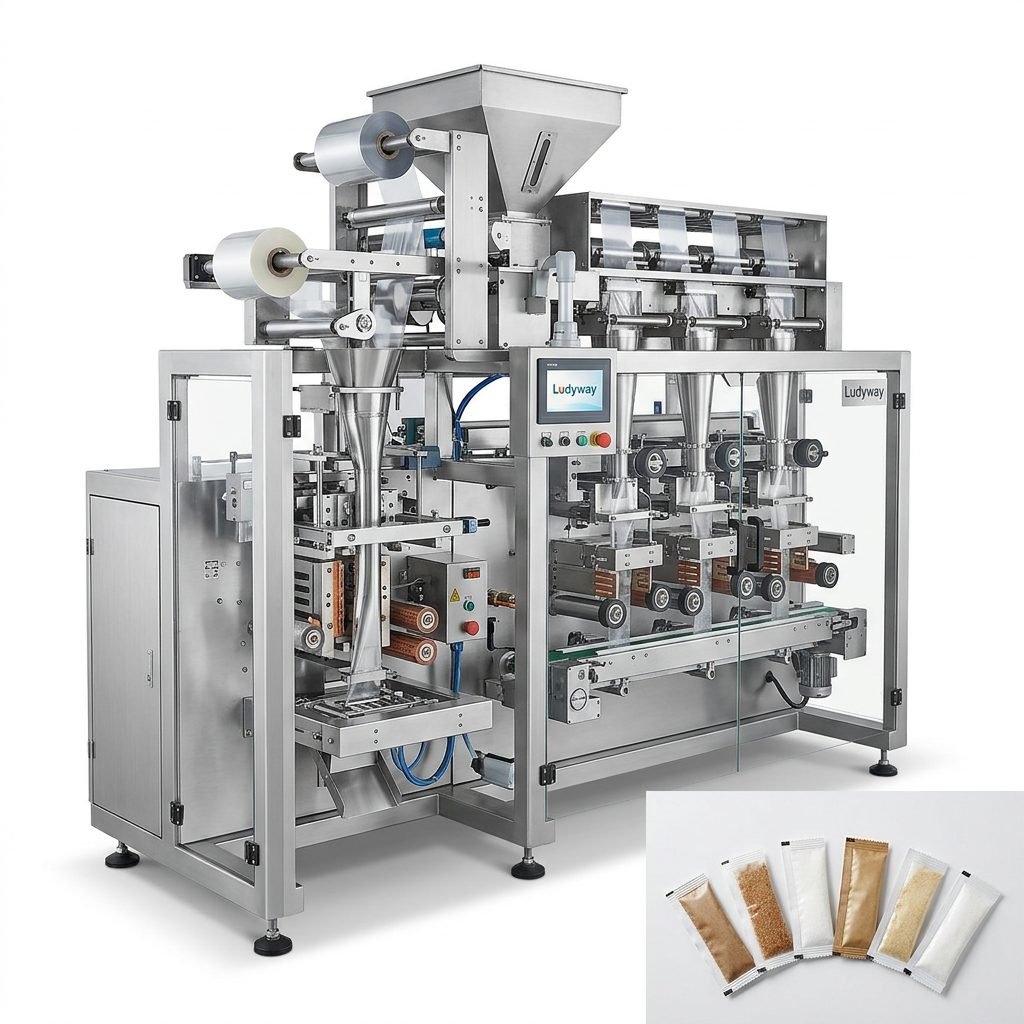
Ludyway is one of the largest packaging machine manufacturers in China, specializing in advanced packaging equipment and turnkey production solutions for the food, pharmaceutical, and health industries. With over 30 years of industry expertise and a state-of-the-art 20,000㎡ manufacturing facility, the company delivers reliable, high-speed popsicle packaging systems tailored to North American market requirements.
Why Industry Leaders Trust These Solutions
- 50+ machine models – Extensive range covering every frozen novelty format
- 200+ manufacturing equipment units – Scaled production capacity for timely delivery
- 130+ packaging experts – Dedicated engineering and service support teams
- Presence in 100+ countries – Global logistics and local service networks
Return on Investment Analysis
Upgrading to a modern automated popsicle packaging system typically delivers measurable financial returns within 18-24 months. Key drivers include labor reduction of 40-60%, film waste decreases of 15-25%, and throughput increases that can double output without adding shifts. When evaluating equipment, consider the total cost of ownership over a minimum 10-year service life rather than focusing solely on initial purchase price.
| ROI Factor | Impact Range | Typical Payback Period |
|---|---|---|
| Labor Savings | 40-60% reduction in direct labor | 8-12 months |
| Film Waste Reduction | 15-25% less material consumption | 4-8 months |
| Throughput Increase | Up to 100% capacity gain | 6-14 months |
| Maintenance Reduction | 30-50% lower service costs | Ongoing annual savings |
Future-Proofing Your Packaging Investment
The North American frozen novelty sector continues to evolve, driven by consumer demand for clean-label ingredients, sustainable packaging, and innovative formats. Selecting a flexible packaging equipment platform that accommodates future market shifts protects your capital investment and positions your operation for sustained growth.
Sustainability Considerations
Leading popsicle packaging systems now offer compatibility with recyclable mono-material films and paper-based wrappers that meet growing retailer and consumer expectations. Equipment designed with servo-driven tension controls can handle thinner gauge materials without compromising seal quality, reducing plastic consumption by up to 20% while maintaining production speeds.
Making the Right Choice for Your Facility
Selecting the best popsicle packaging machine requires careful evaluation of your specific production requirements, facility constraints, and growth projections. Prioritize suppliers with proven experience in frozen applications, comprehensive after-sales support, and a commitment to innovation that keeps pace with packaging industry trends.
With the right equipment partner, your popsicle packaging operation can achieve the speed, reliability, and quality that defines category-leading brands. Focus on proven performance, North American compliance, and responsive technical support to ensure your investment delivers long-term competitive advantage in this dynamic market segment.
For detailed specifications, ROI projections, or to arrange a virtual factory tour, reach out to discuss your specific frozen novelty packaging requirements with an experienced application specialist. The right solution turns your packaging line from a bottleneck into a competitive advantage.