Automated Bagging System | Intelligent High-Efficiency Packaging Solutions
Revolutionize your high-throughput packaging operations with smart multi-lane dosing, precision sealing, and turnkey automated bagging systems tailored for food, pharmaceutical, and chemical bulk manufacturing.
Next-Generation Automated Bagging Systems for Modern Manufacturing
Transitioning from conventional manual packaging to an intelligent, end-to-end automated bagging system is the cornerstone of optimizing batch cycle times, reducing overhead, and adhering to rigorous international hygienic standards.
In modern industrial facilities, manual bag handling and weighing inconsistencies cause severe production bottlenecks, excessive material loss, and high labor turnover. An automated bagging system integrates synchronized infeed conveyors, multi-head or auger dosing units, dynamic bag feeding, and high-integrity sealing stations into a single connected workflow.
Whether packing bulk powdered raw materials, granular foods, animal feeds, or pharmaceuticals, Ludyway’s automation architectures deliver precision down to ±0.2% dosing variance. Utilizing industrial-grade PLC microprocessors and intuitive multi-language HMI interfaces, operators maintain full diagnostic control while achieving non-stop packaging speeds exceeding 120 cycles per minute.
- Multi-Format Flexibility: Compatible with open-mouth bags, valve bags, stick packs, and quad-seal pouches.
- High Precision Dosing: Servo-driven augers and multi-head combination scales prevent overfill and giveaway.
- Hygienic Construction: Full SUS304/SUS316L stainless steel engineering adhering to cGMP and FDA directives.
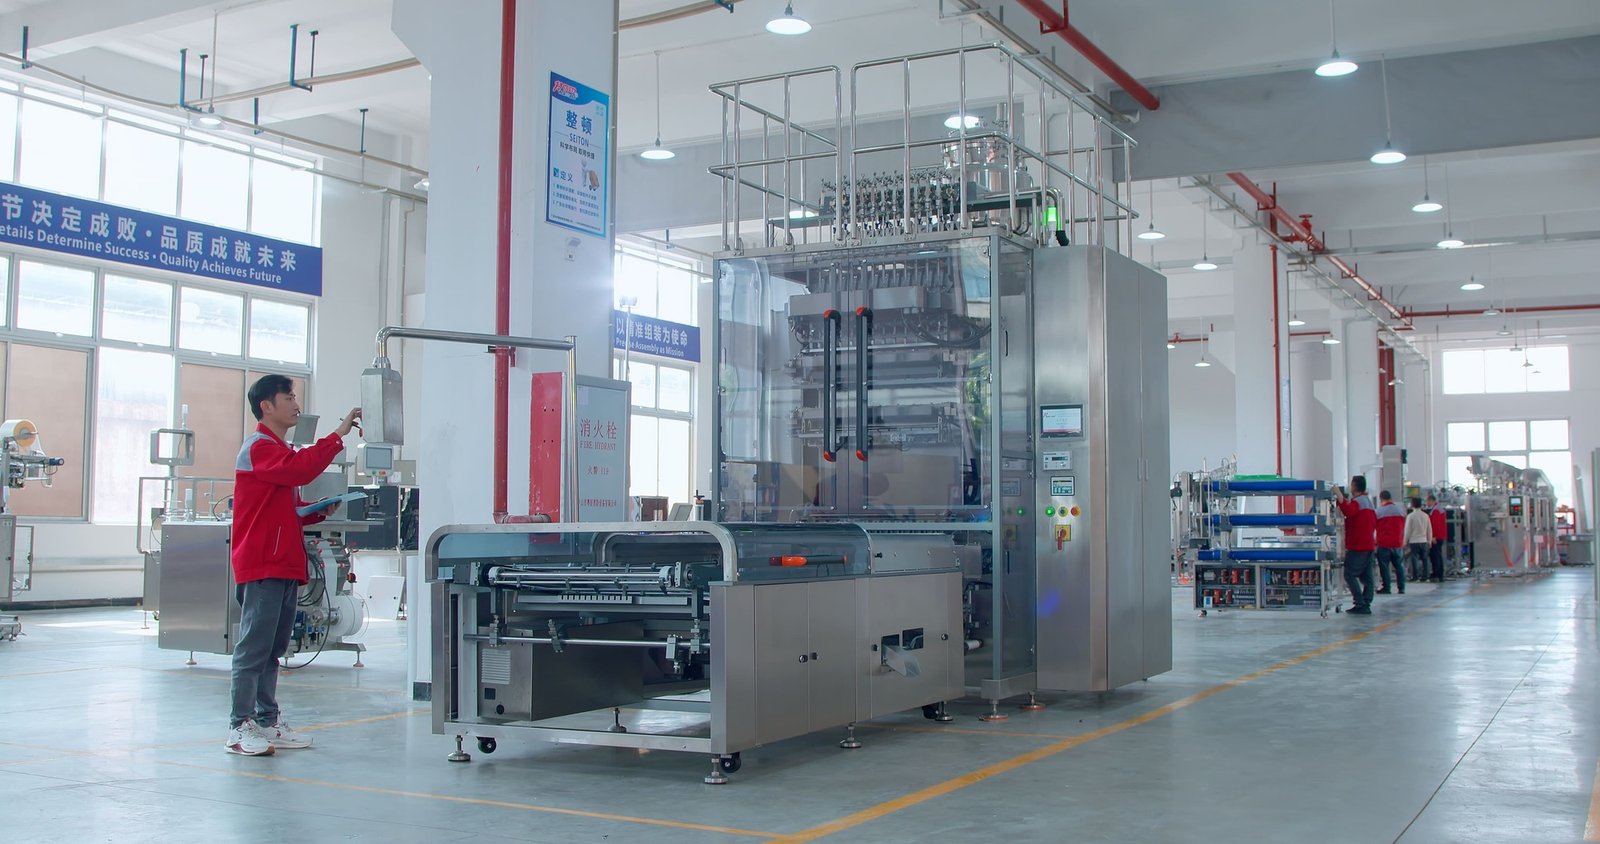
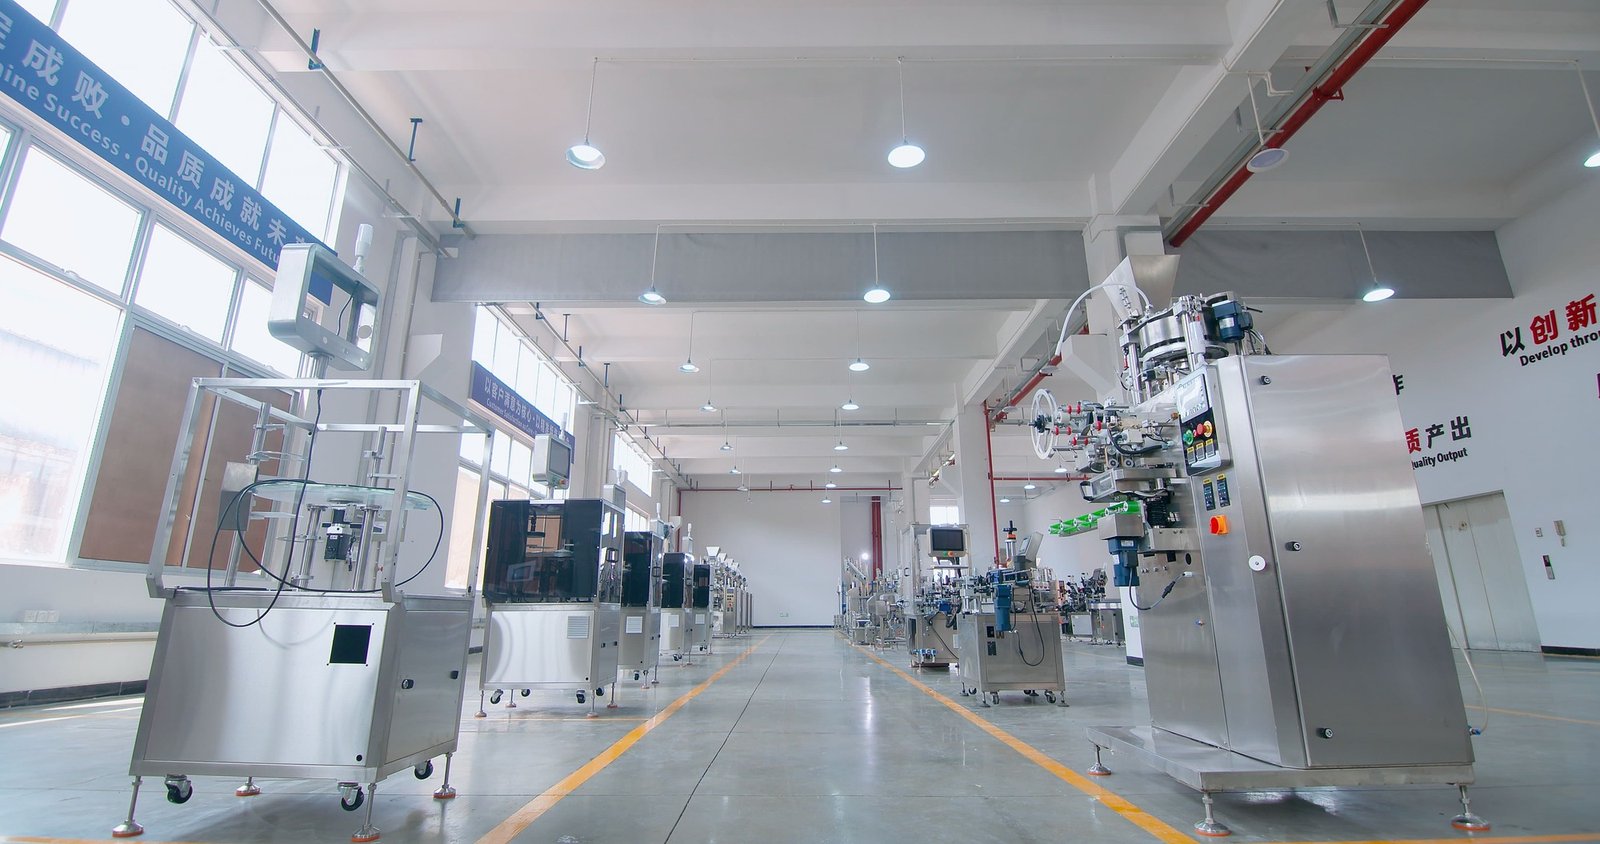
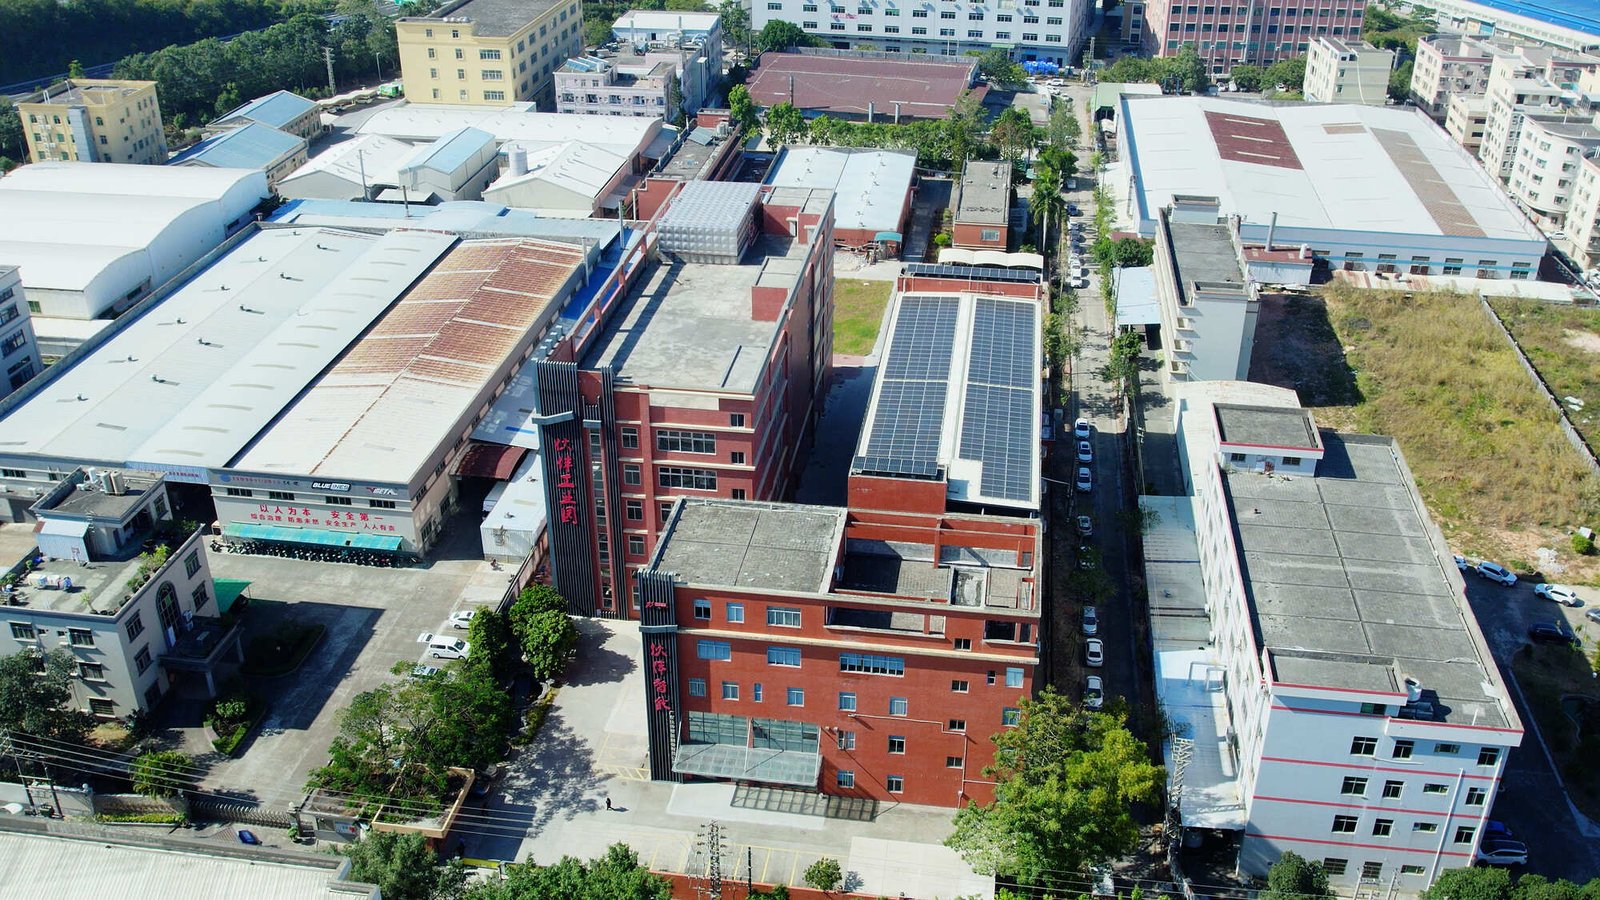
Intelligent Machinery Assembly Plant
Over 20,000㎡ precision manufacturing facility dedicated to turnkey packaging innovation.
Technical Architecture & Engineering Specifications
Designed with industrial AI sensor arrays and adaptive dynamic servo actuators for unmatched stability across high-speed packaging cycles.
High-Speed Weighing Core
Combines multi-head dynamic load cells and ultra-fast AD converters to sample bulk weights at millisecond intervals, eliminating underfill and batch giveaway.
Adaptive Bag Positioning
Pneumatic robotic arms and vacuum duckbill grips synchronize to open, position, clamp, and stabilize bags effortlessly across continuous high-cycle operations.
Smart Thermal & Ultrasonic Sealing
PID-controlled temperature bars and high-frequency ultrasonic sealing heads ensure hermetic seam closures on laminated films, heavy foil, and woven polybags.
| System Parameter | Standard Multi-Lane Sachet / Stick | Heavy-Duty Bulk Bagging Line | Pharmaceutical Cleanroom Spec |
|---|---|---|---|
| Packaging Speed | 40 – 120 cycles/min per lane | 10 – 35 bags/min (10kg – 50kg) | 50 – 160 cycles/min |
| Dosing Accuracy | ≤ ±0.5% – ±1.0% | ≤ ±0.2% (Dynamic Load Cell) | ≤ ±0.15% (Micro-Auger) |
| Bag Materials | PET/AL/PE, Paper/PE, Composite | Kraft Paper, PP Woven, Heavy PE | Medical Aluminum, Barrier Foil |
| Control Interface | 7″ / 10″ Siemens HMI Color Touch | 12″ Industrial PC + Remote IoT | 21 CFR Part 11 Compliant HMI |
| Compressed Air Supply | 0.6 – 0.8 MPa, 0.4 m³/min | 0.6 – 0.8 MPa, 0.9 m³/min | 0.6 MPa (Oil-free filtered) |
Featured Packaging & Dosing Systems
Discover our core line of automated packaging machines engineered for high throughput, minimal downtime, and flexible bag format conversion.
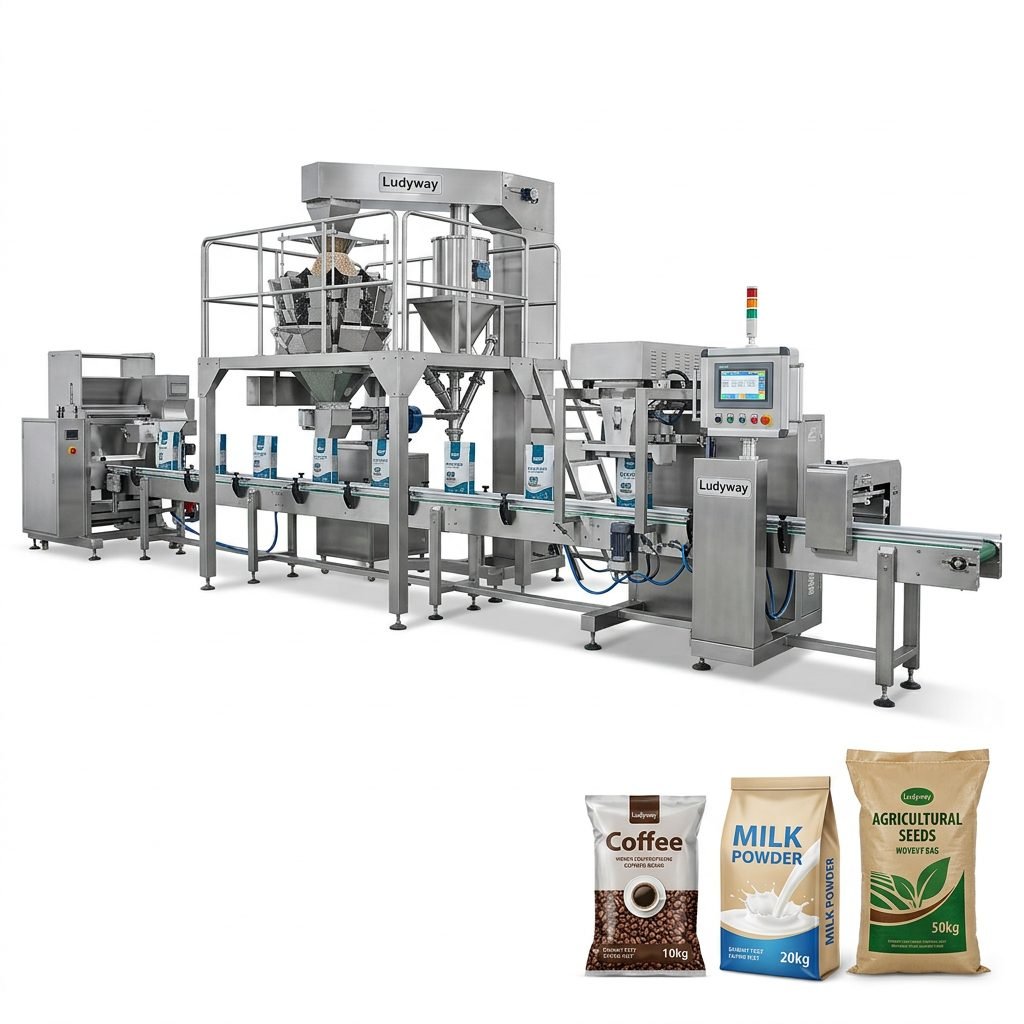
Open Mouth Bag Packaging Lines for Granule & Powder
Automated heavy-duty bag feeding, dust-tight filling spout, and robotic bag sealing system for industrial bulk applications.
View Equipment Details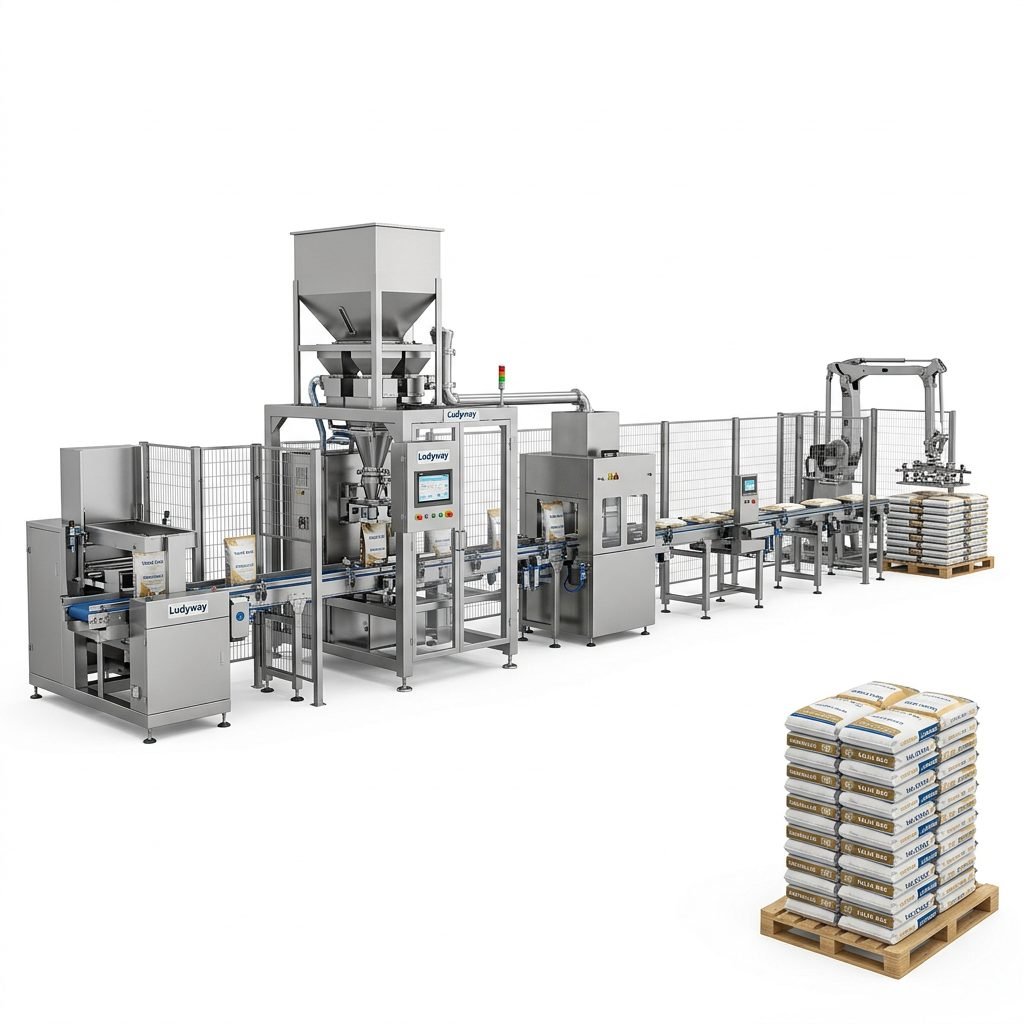
Valve Bag Packaging Lines for Granules & Powders
Ultrasonic valve sealing technology integrated with automated bag placers for clean, spillage-free chemical processing.
View Equipment Details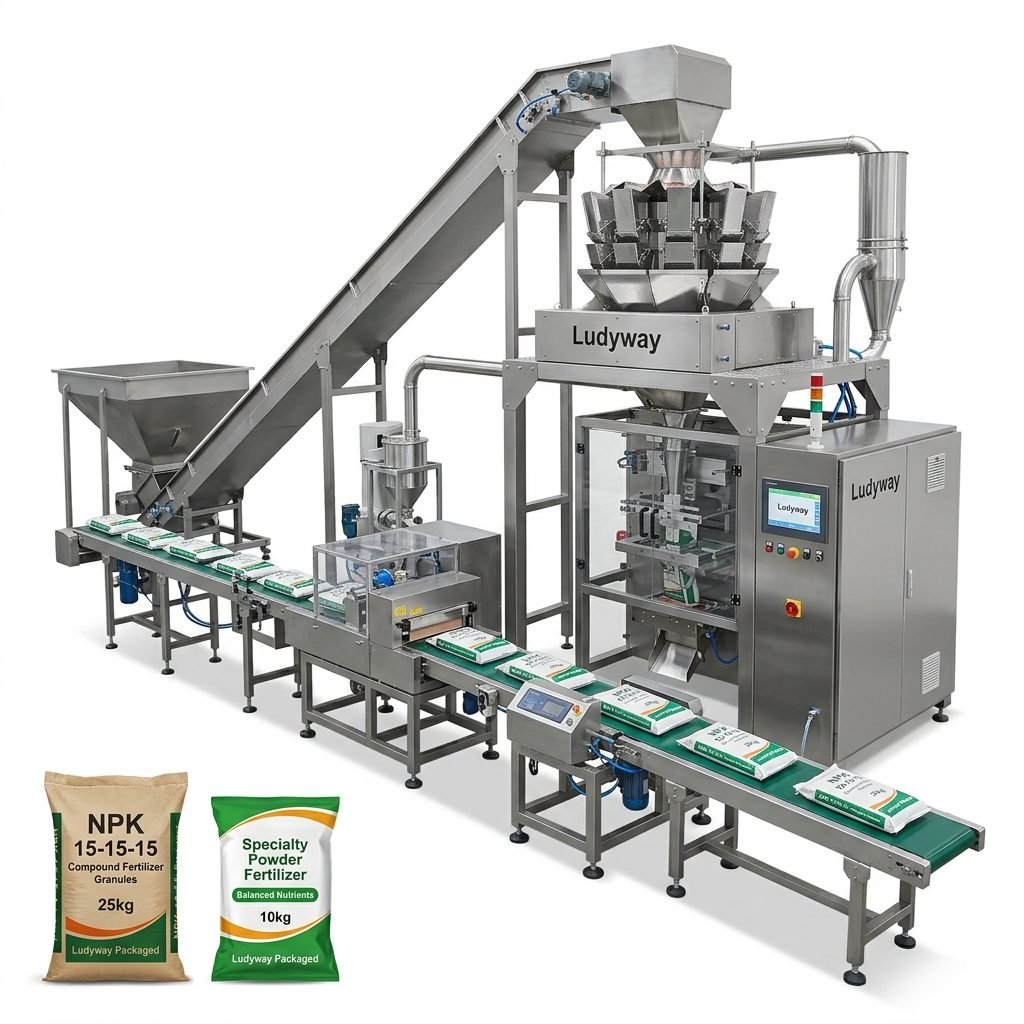
Compound Fertilizer Automated Bagging Line
Corrosion-resistant construction engineered for corrosive agricultural chemicals, bulk fertilizers, and soil additives.
View Equipment Details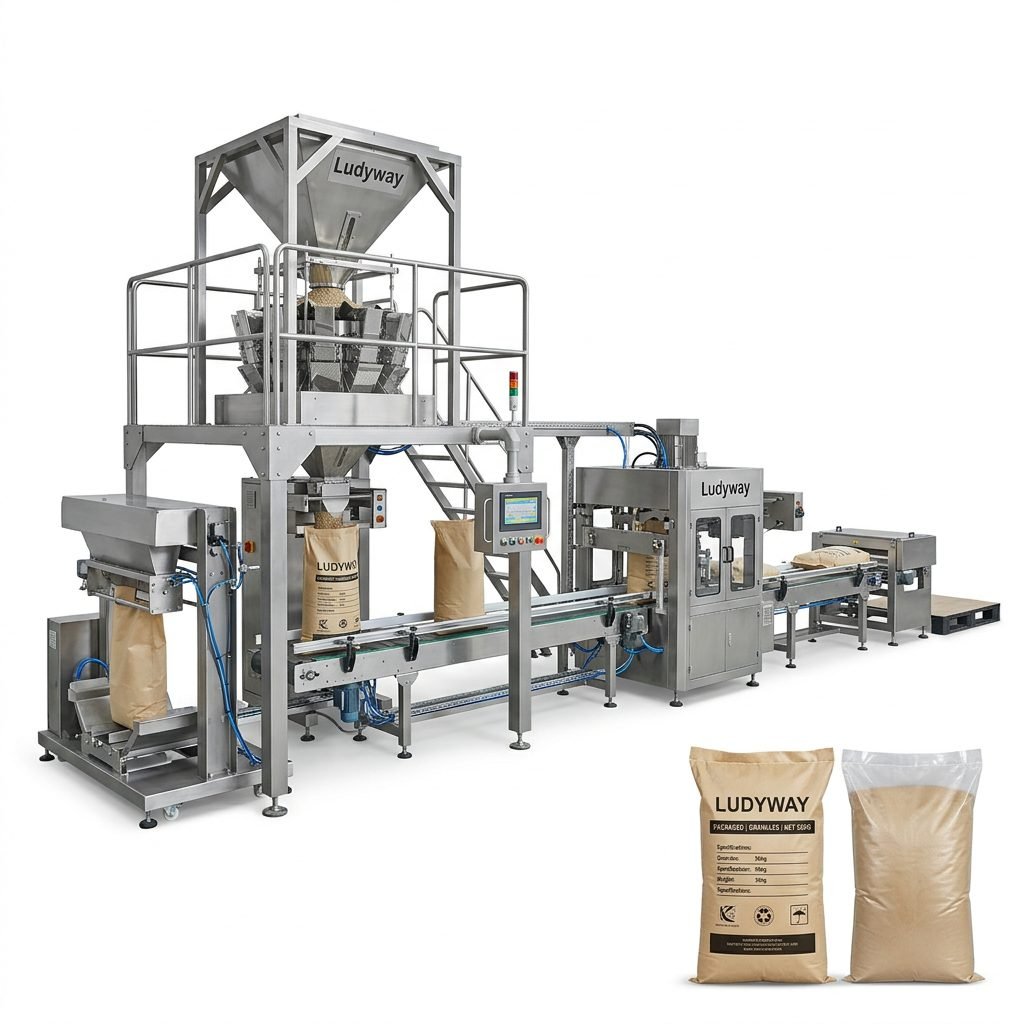
50kg Bag Packaging Line for Granules & Powders
High-capacity automated filling system with motorized conveyor belts, dynamic checkweighing, and automated bag sewing.
View Equipment Details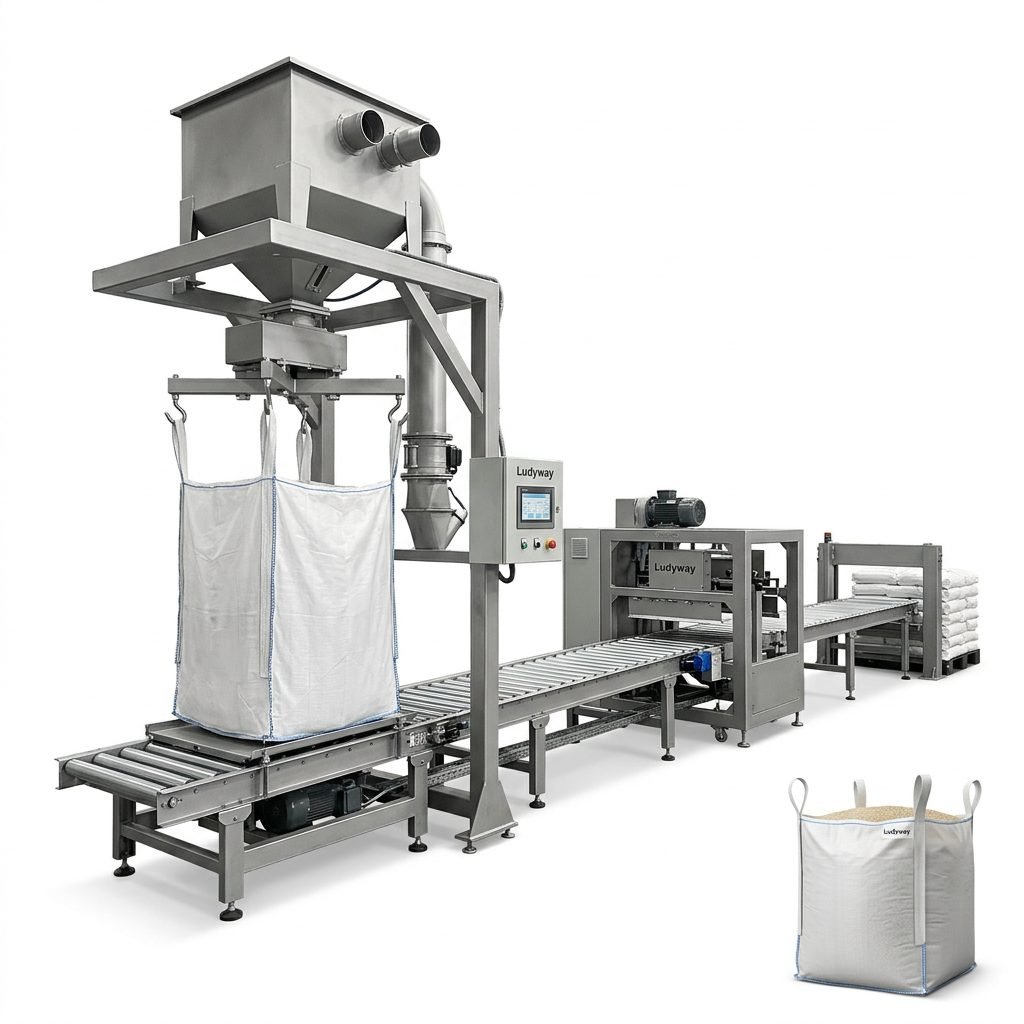
Heavy-Duty Big Bag Weighing & Packaging Lines
Bulk jumbo bag handling and precision weigh-filling line designed for continuous non-stop mining, grain, and chemical plants.
View Equipment Details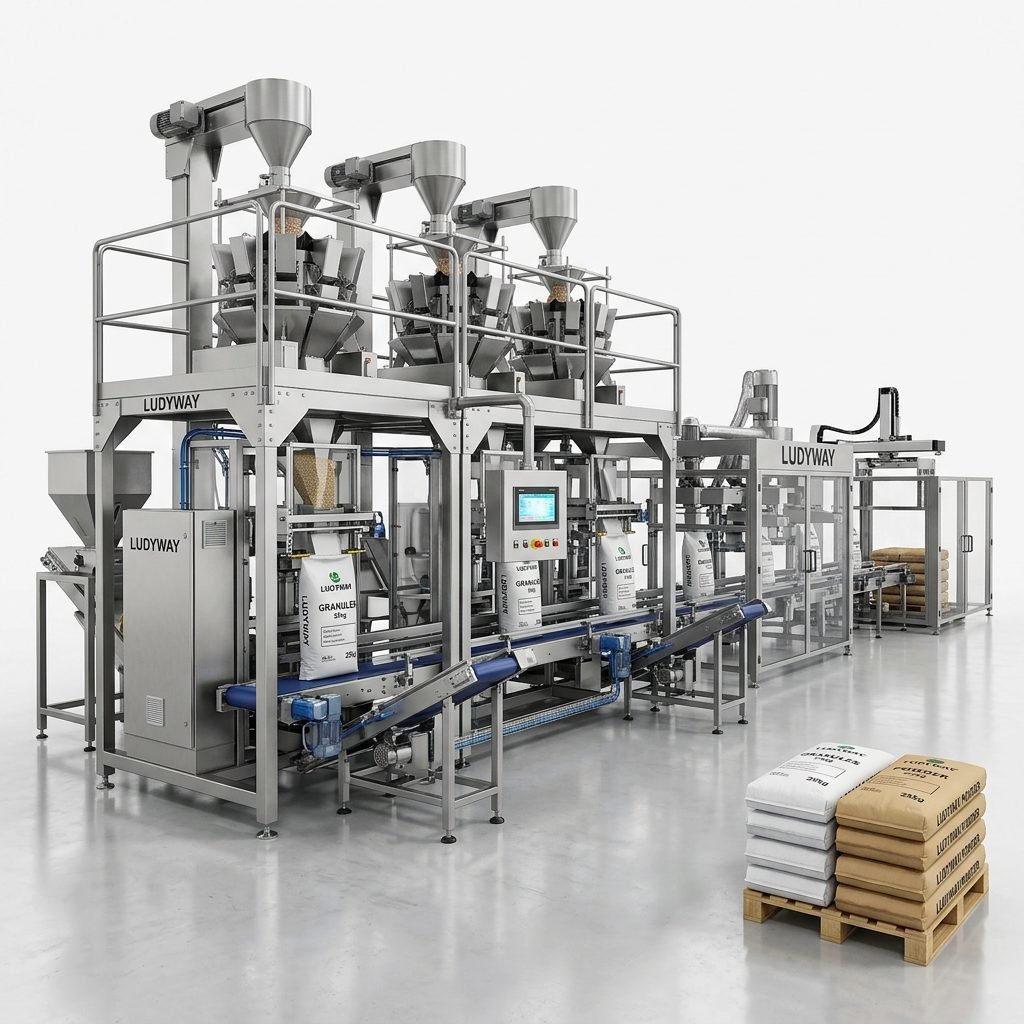
25kg Bag Multi-Lane Packaging Automation Lines
High-speed dual station bag feeding mechanism delivering rapid output for plastic resins, food flour, and mineral powders.
View Equipment Details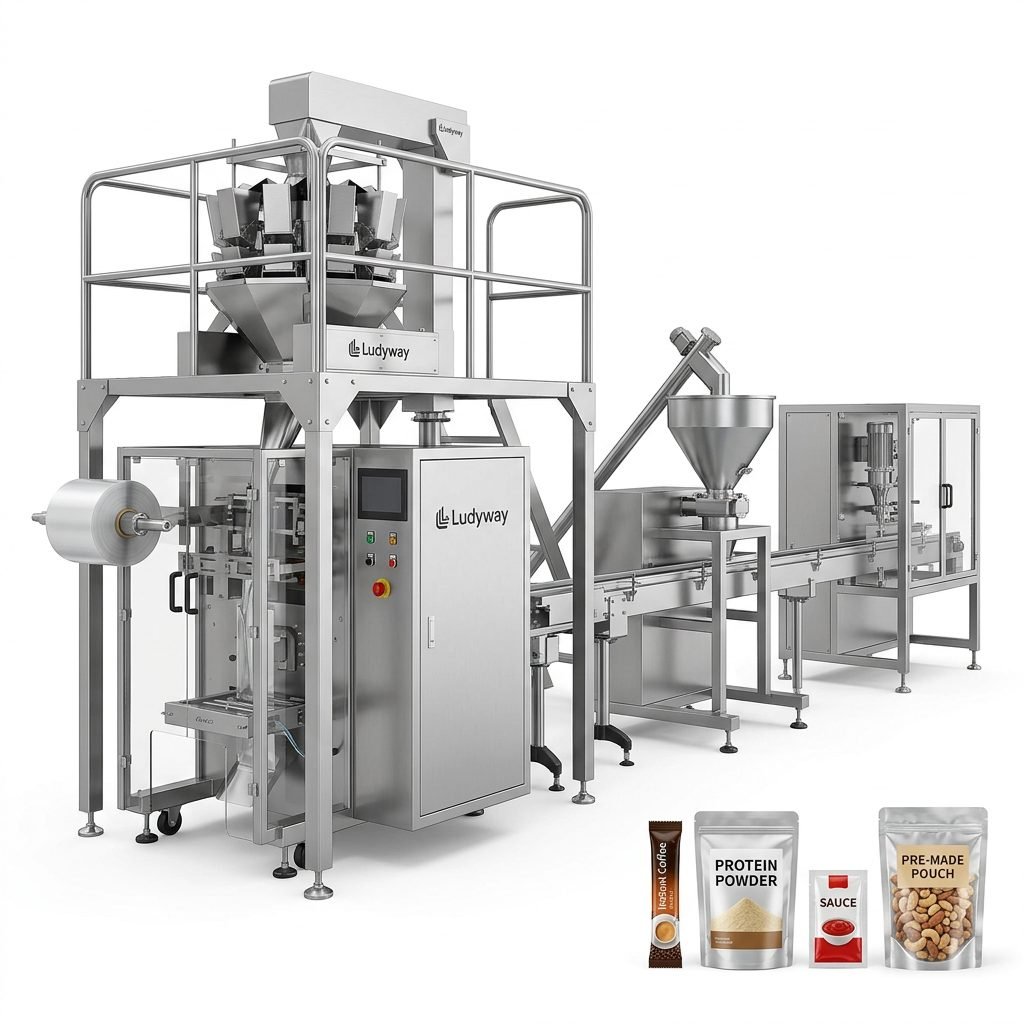
Automated Multi-Lane Sachet & Pouch Packaging
Versatile multi-lane vertical form fill seal machinery engineered for high-precision portion packaging of powders and liquids.
View Equipment Details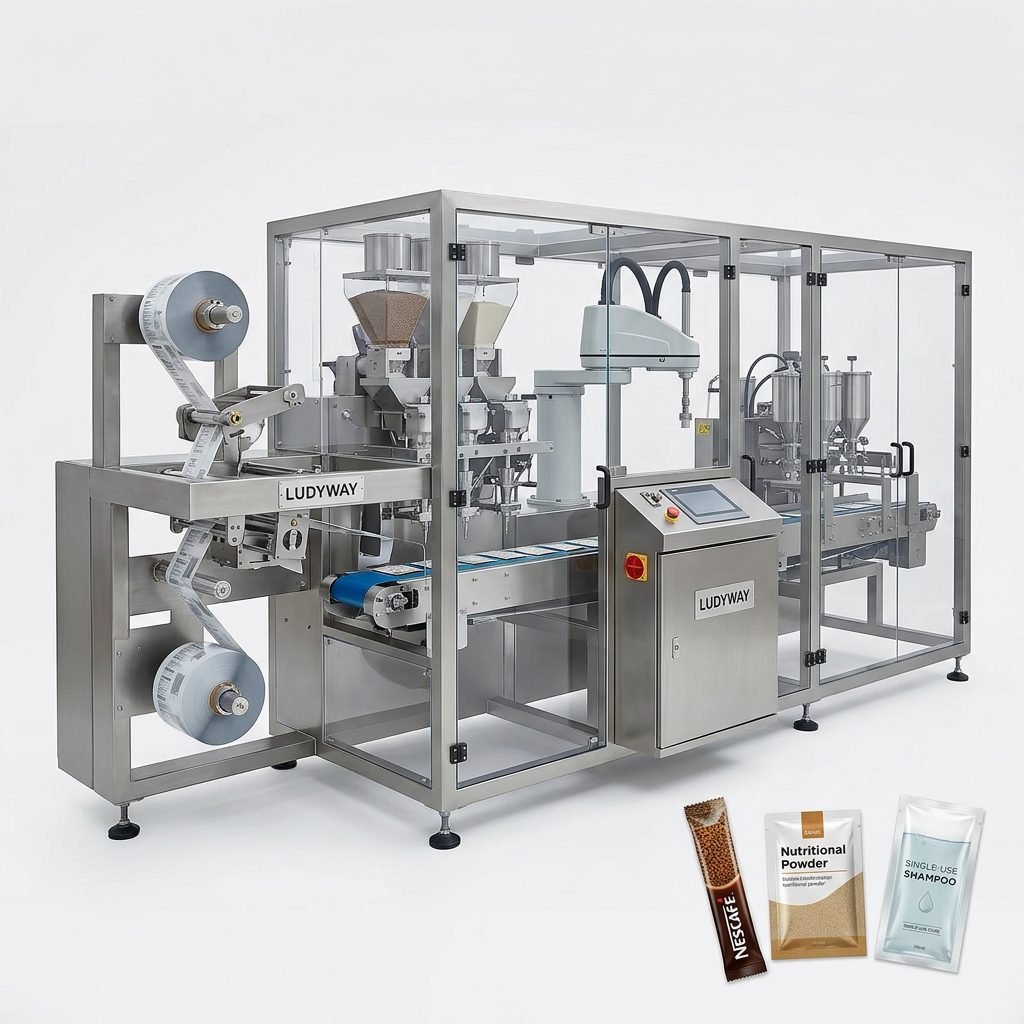
Robotic Automated Packaging & Palletizing Line
Complete turnkey integration including smart visual inspection, dynamic carton packing, and robotic end-of-line palletizing.
View Equipment DetailsTailored Turnkey Solutions Across Core Sectors
Engineered to comply with stringent regulatory standards and diverse physical bulk product characteristics.
Food & Beverage Processing
From fine powdered milk, spices, and flours to granular grains, dried fruit, and snacks. Incorporates nitrogen flushing systems for shelf-life extension.
Explore Food Packaging Machines →Pharmaceuticals & Health
GMP-grade automated bagging and sachet packaging solutions with complete batch trackability, laminar flow integration, and high cleanability.
Explore Pharma Packaging Systems →Chemicals & Industrial Minerals
Heavy-duty dust containment, anti-static engineering, and vacuum compaction for building adhesives, plastic resins, carbon black, and pigments.
Explore Chemical Machinery →Animal Nutrition & Pet Feeds
High-volume automatic bagging lines for pet kibble, livestock mash, feed premixes, and bird seeds featuring reinforced heavy-gauge bag drop arms.
Explore Feed Packaging Solutions →Cosmetics & Personal Care
High-speed portion packaging for facial powders, hair treatments, and personal care solutions with precision liquid-tight or powder-sealed sachet boundaries.
Explore Cosmetic Packaging Lines →Nicotine & Modern Portion Pouches
Specialized high-speed pouch counting, can filling, cartoning, and automatic sealing machines engineered for tobacco-free oral nicotine production.
Explore Nicotine Pouch Automation →Certified Manufacturing Excellence & Trusted Global Partnerships
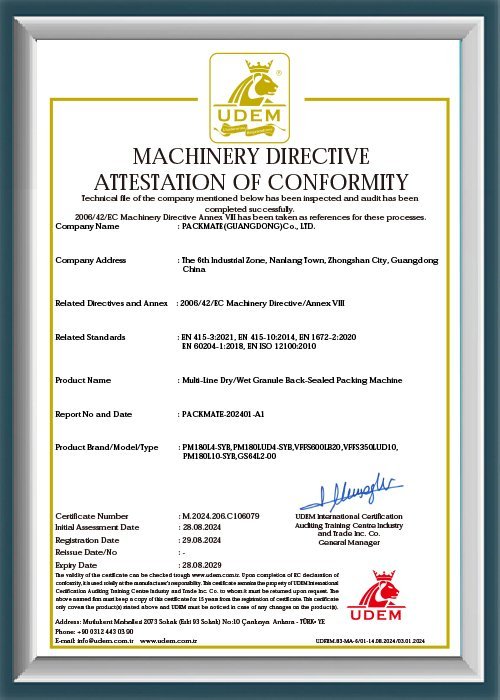
All Ludyway automated bagging systems are engineered in accordance with ISO9001 quality management, CE directives, and GMP clean-design benchmarks.
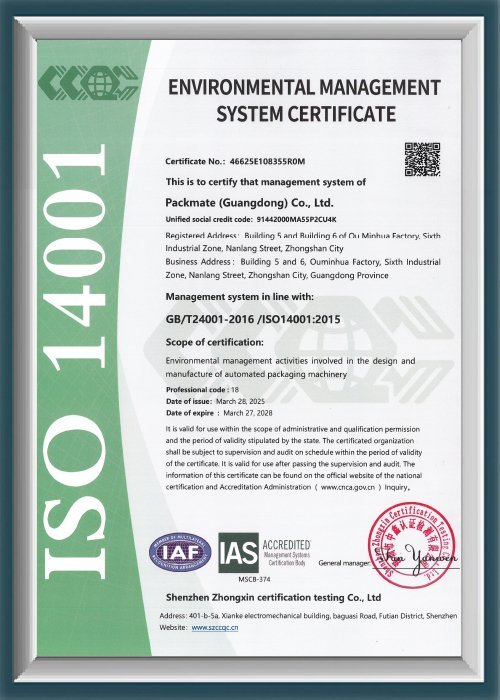
CE Safety Conformity
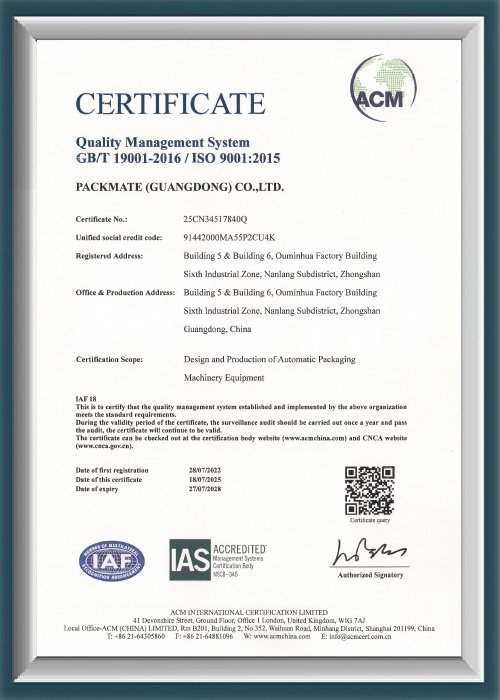
ISO9001 Quality Standard
Sanitary Food Grade Verification
UL & CSA Electrical Safety
Trusted by Industry Leaders Worldwide
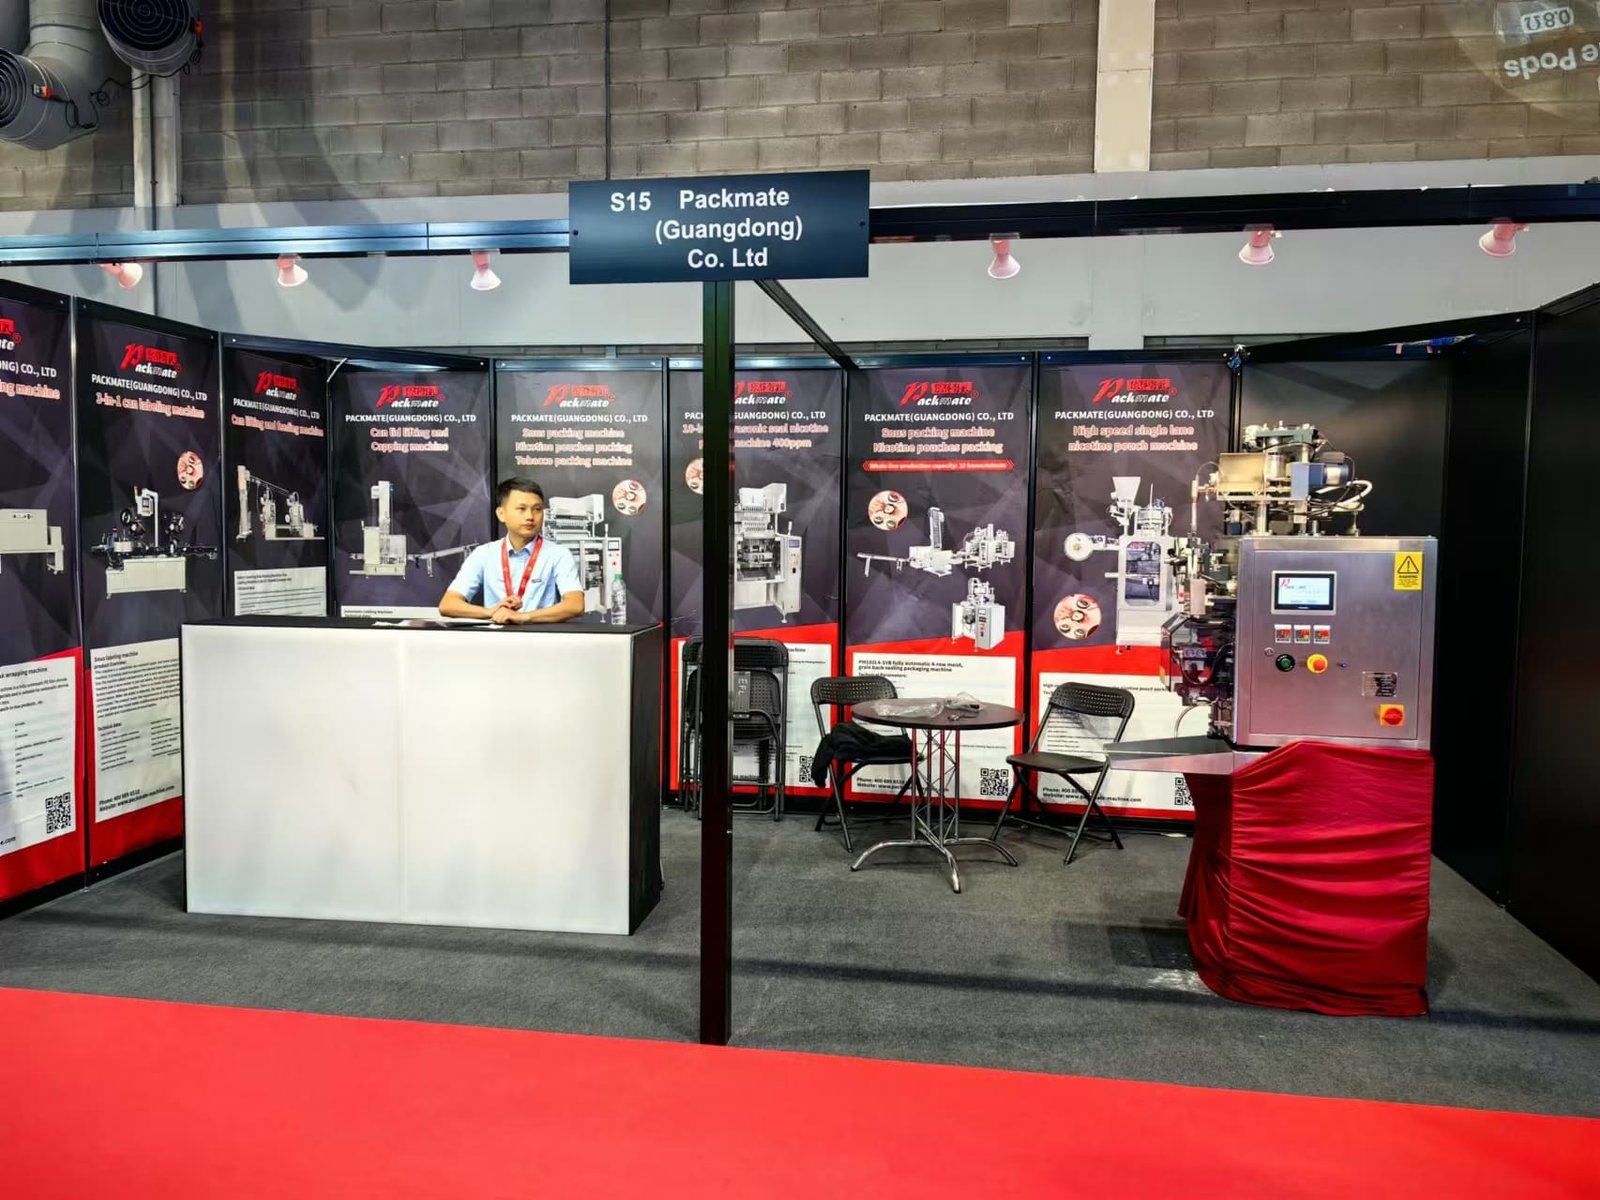
International Exhibitions & World-Class Facilities
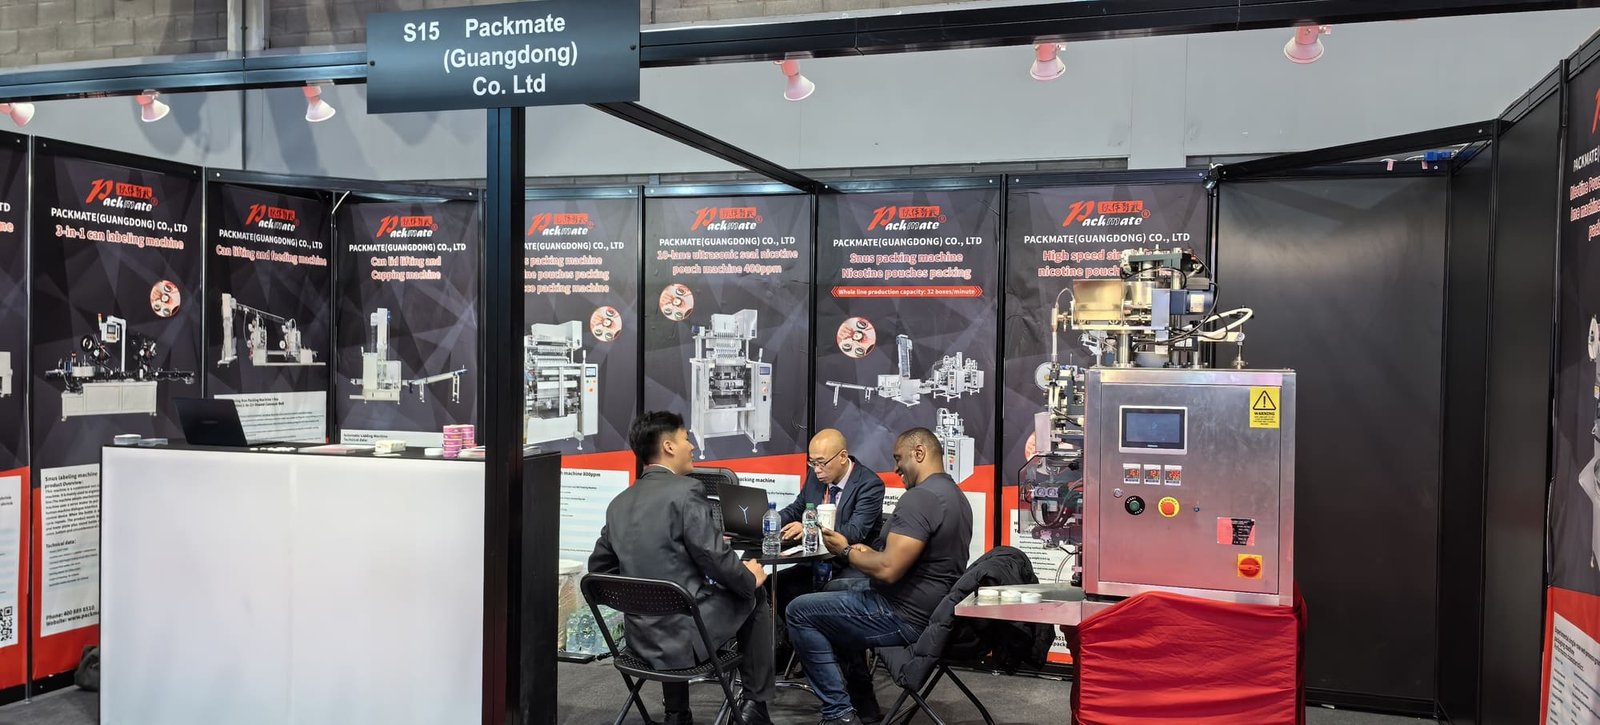
Connecting with industrial manufacturing clients across major packaging expos in Europe, North America, Asia, and the Middle East.
How to Choose & Optimize an Automated Bagging System
A comprehensive technical guide for factory engineers, plant managers, and procurement leaders.
1. Material Flow Properties & Dosing Mechanism Selection
The primary consideration when deploying an automated bagging line is the physical behavior of your bulk product. Non-free-flowing powders (such as baby milk powder, fine starch, titanium dioxide, or organic cocoa) require servo-driven vertical auger fillers fitted with anti-bridging agitators and vacuum de-aeration systems to prevent powder swirling and uneven bag fills. Conversely, free-flowing granules (like coffee beans, fertilizer pellets, dry animal feeds, and plastic chips) excel when coupled with multi-head weighers or linear vibratory feeders that utilize gravity feeds without material degradation.
2. Bag Construction, Sealing Integrity, and Shelf-Life Protection
Modern packaging environments demand total protection against oxygen ingress, moisture absorption, and mechanical puncture. Heavy-duty polywoven bags used in the chemical and agricultural sectors require synchronized folding guide bars and high-tension sewing or thermal band sealers. For retail food and high-potency pharmaceuticals, laminated foil pouches utilize multi-stage heating bars with continuous thermocouple monitoring, followed by immediate chilled cooling bars to ensure clean, wrinkle-free, leak-proof barrier seals.
3. Integration with Secondary End-of-Line Packaging Automation
A standalone bagging unit achieves its full ROI potential when integrated into a unified line. Connecting downstream checkweighers, inline industrial metal detectors, dynamic X-ray inspection modules, automatic case cartoners, and robotic palletizers creates a lights-out manufacturing environment. Real-time SCADA or MES communication protocols (EtherNet/IP, Profinet, Modbus TCP) allow remote diagnostics, instant recipe recall, and predictive maintenance tracking.
What is the expected ROI period for an automated bagging system?
Most mid-to-large scale processing plants recover their initial investment within 8 to 14 months through eliminated manual labor overhead, precise weight giveaway reduction (saving 1-3% raw material), and 30-50% higher continuous line output.
How fast can bag sizes and recipe parameters be changed on the HMI?
Ludyway machines feature quick-release forming tubes, motorized width adjustment guides, and pre-saved digital recipe profiles on the touch screen, allowing complete size changeovers within 10 to 15 minutes without specialized hand tools.
Are Ludyway bagging systems suitable for hazardous or dusty chemical environments?
Yes. We engineer ATEX/explosion-proof certified motors, fully enclosed dust-extraction spouts with negative pressure vacuums, and NEMA 4X / IP65 rated electrical enclosures for harsh mineral, chemical, and flour environments.
Ready to Upgrade Your Packaging Line with Automated Precision?
Consult with our senior packaging engineers today to design a fully customized, high-speed automated bagging system optimized for your product parameters.