Vacuum Sealed Packaging Machine | Reliable Packaging Solutions
Empower high-efficiency manufacturing with advanced industrial vacuum sealed packaging systems. Designed for airtight barrier protection, extended shelf preservation, and high-speed precision across food, chemical, medical, and nutraceutical processing lines.
State-of-the-Art Vacuum Sealed Packaging Machine Systems
Modern production environments demand uncompromising barrier integrity, rapid cycle times, and minimal product degradation. A professional vacuum sealed packaging machine eliminates residual atmospheric oxygen from pouches, rigid packs, and specialty containers, preventing oxidation, enzymatic decay, and microbial contamination.
Deep Vacuum De-Oxygenation
High-throughput rotary vane and dry vacuum pumps evacuate air down to critical millibar levels, securing freshness and stabilizing sensitive ingredients.
Hermetic Thermal Sealing
Precision PID temperature controllers coupled with pneumatic sealing jaws ensure fail-safe barrier bonding across laminated foils, EVOH, and co-extruded films.
Intelligent Automation Control
Integrated PLC interfaces enable real-time recipe management, dynamic vacuum monitoring, automatic fault diagnostics, and rapid changeovers.
Engineered Vacuum & High-Speed Packaging Machinery
Discover tailored solutions engineered for high-integrity sealing, automated material conveyance, and vacuum preservation.
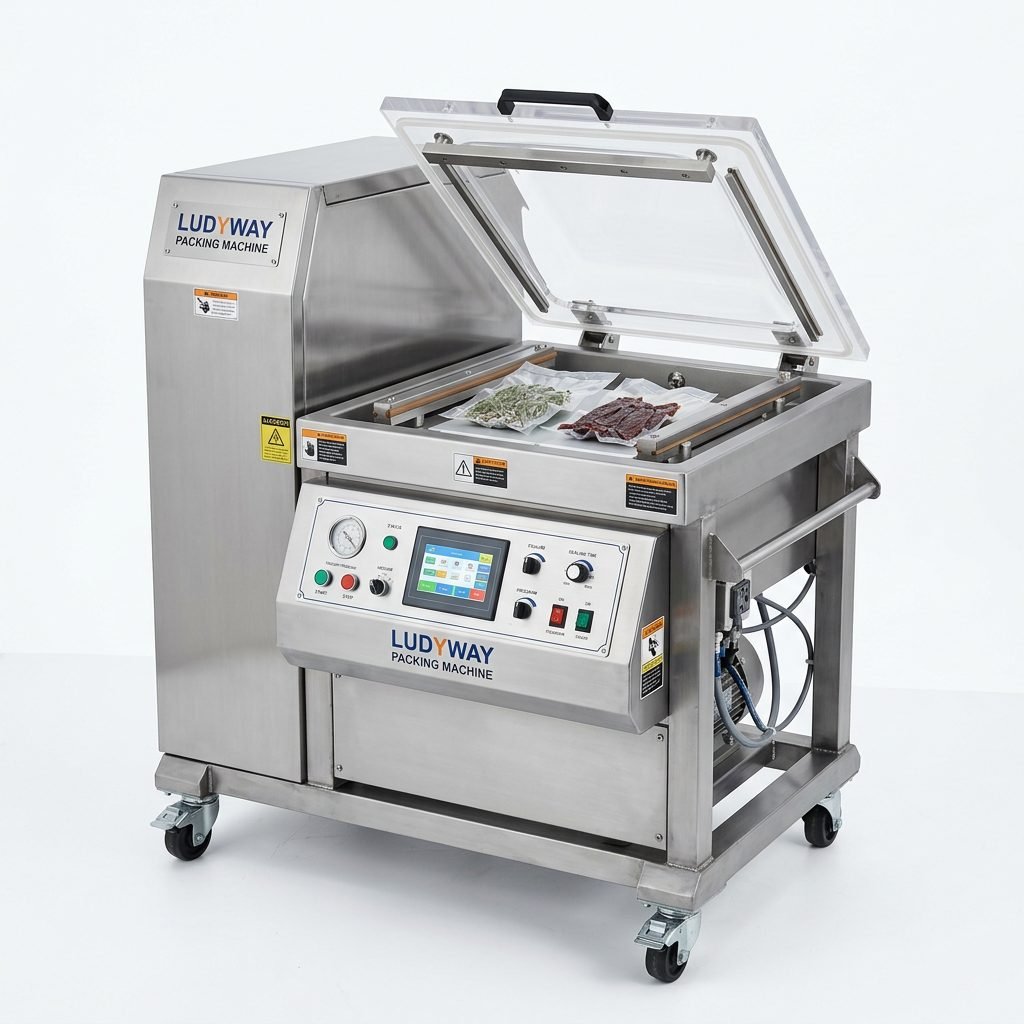
Industrial Vacuum Packaging Machine for Food & Pharma
View Equipment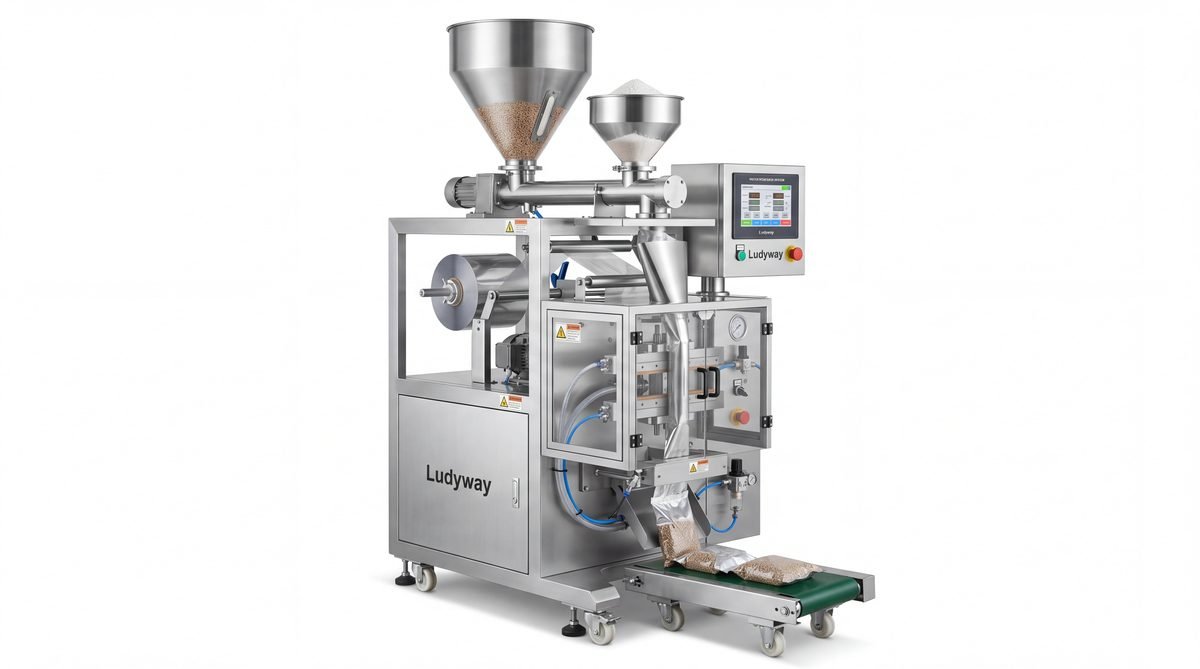
Industrial Vacuum Machine for Granule & Powder
View Equipment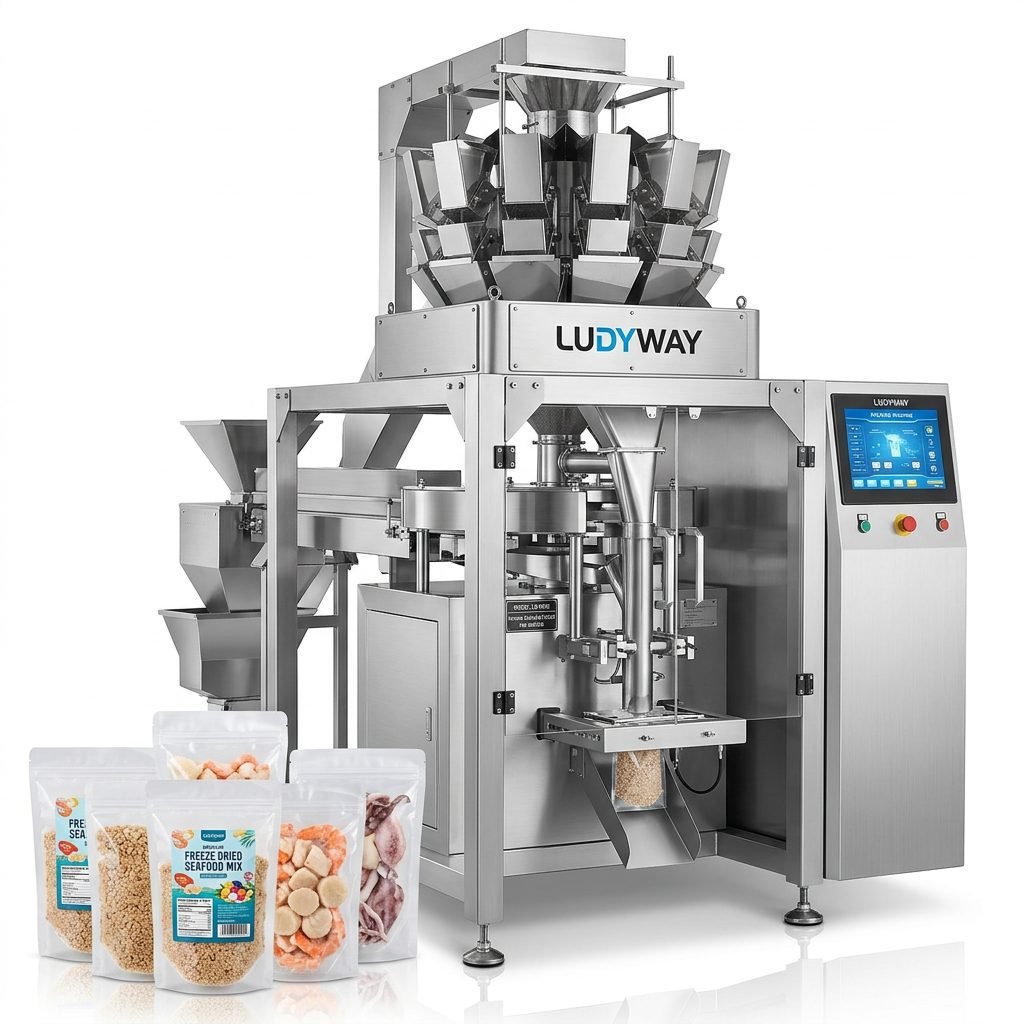
Freeze Dried Seafood Vacuum Sealing Machine
View Equipment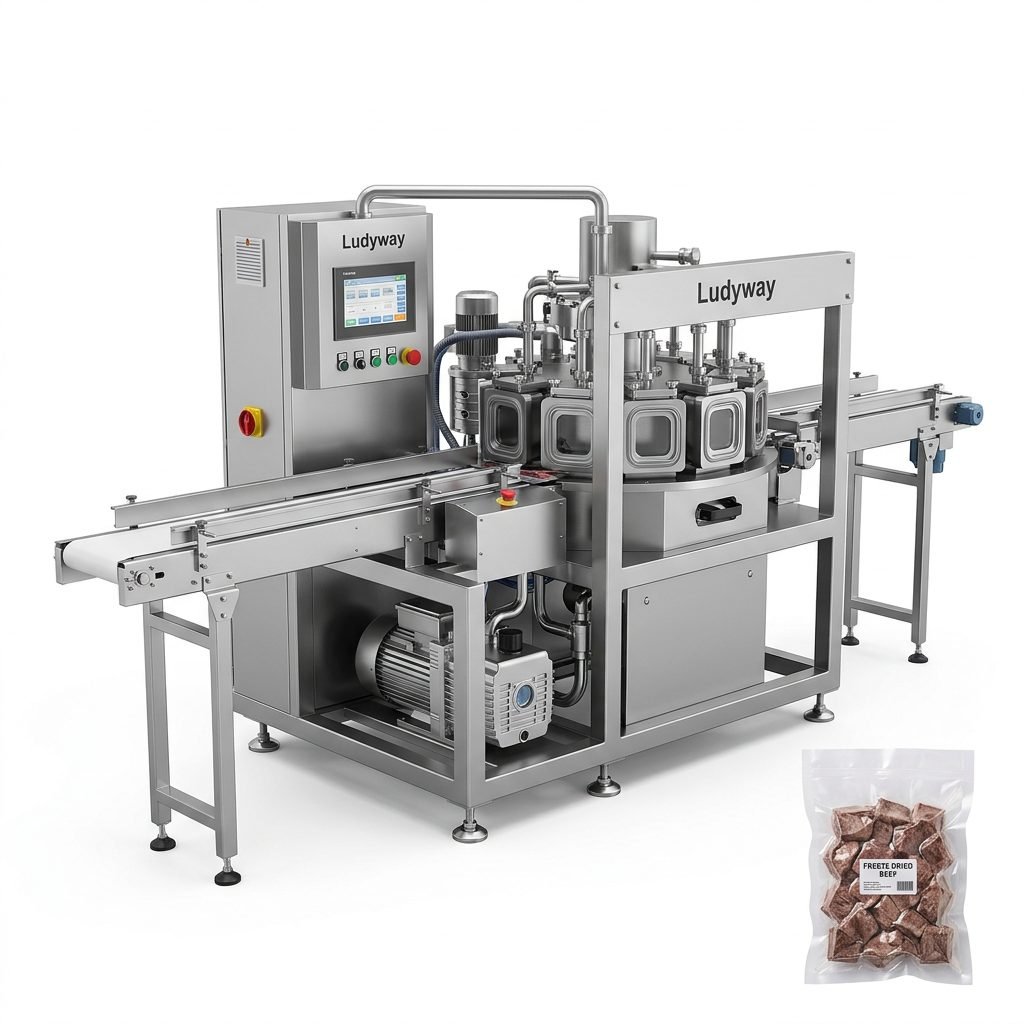
Freeze Dried Beef Vacuum Packaging System
View Equipment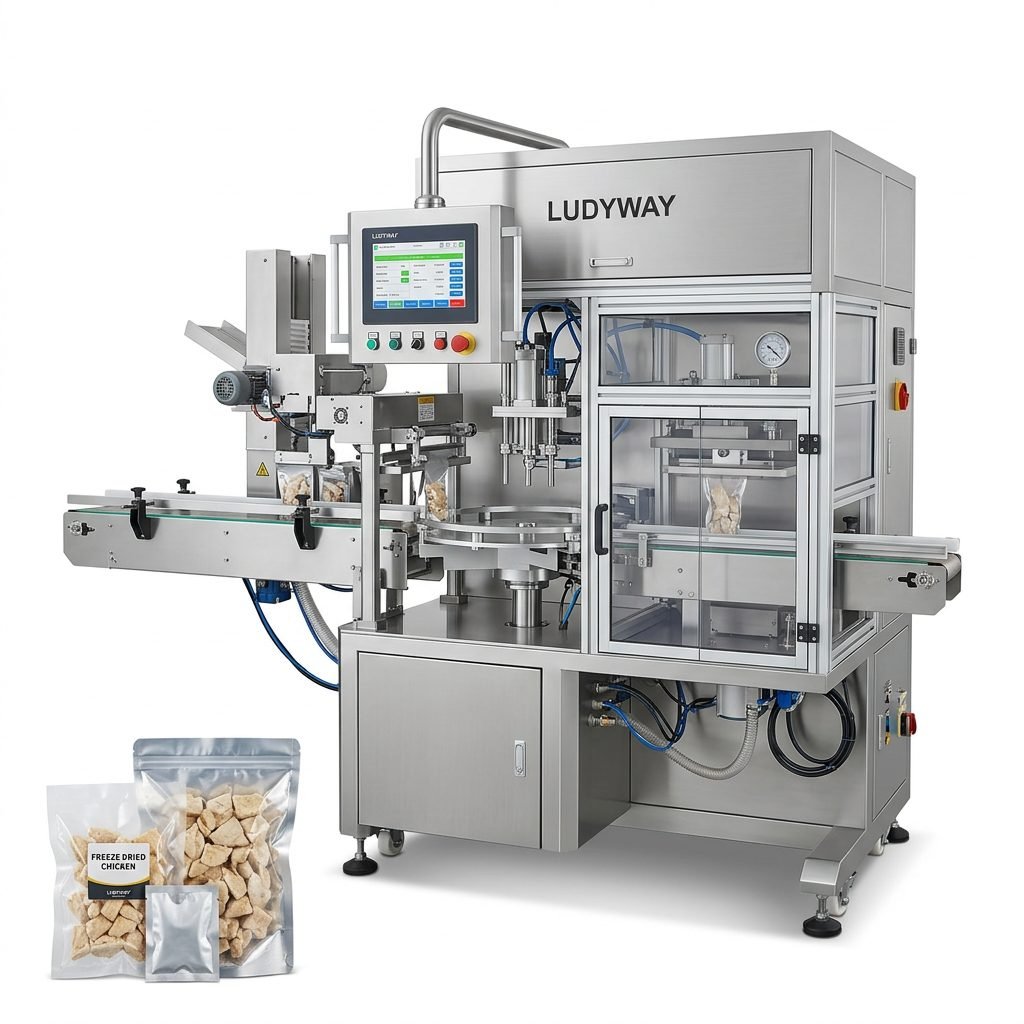
Freeze Dried Chicken Vacuum Packaging Machine
View Equipment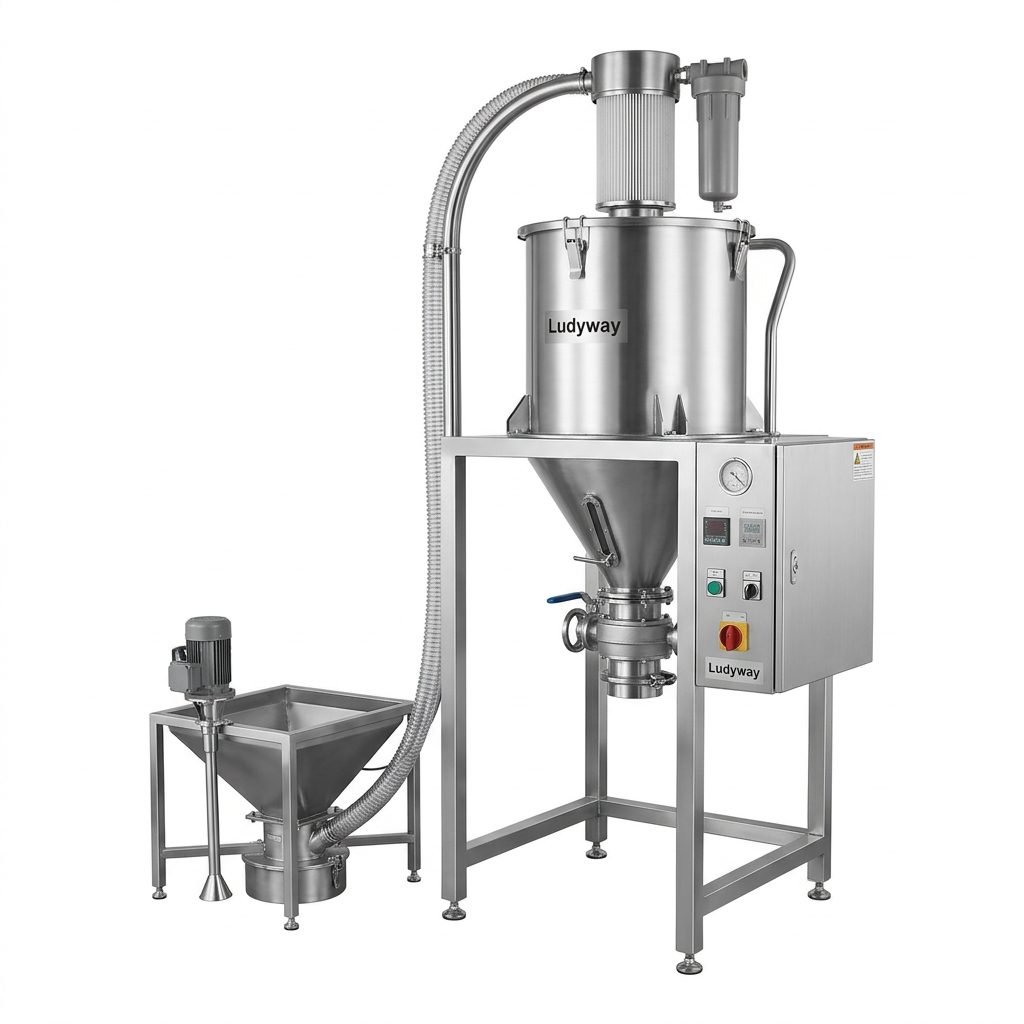
Automatic Vacuum Feeder Conveying System
View Equipment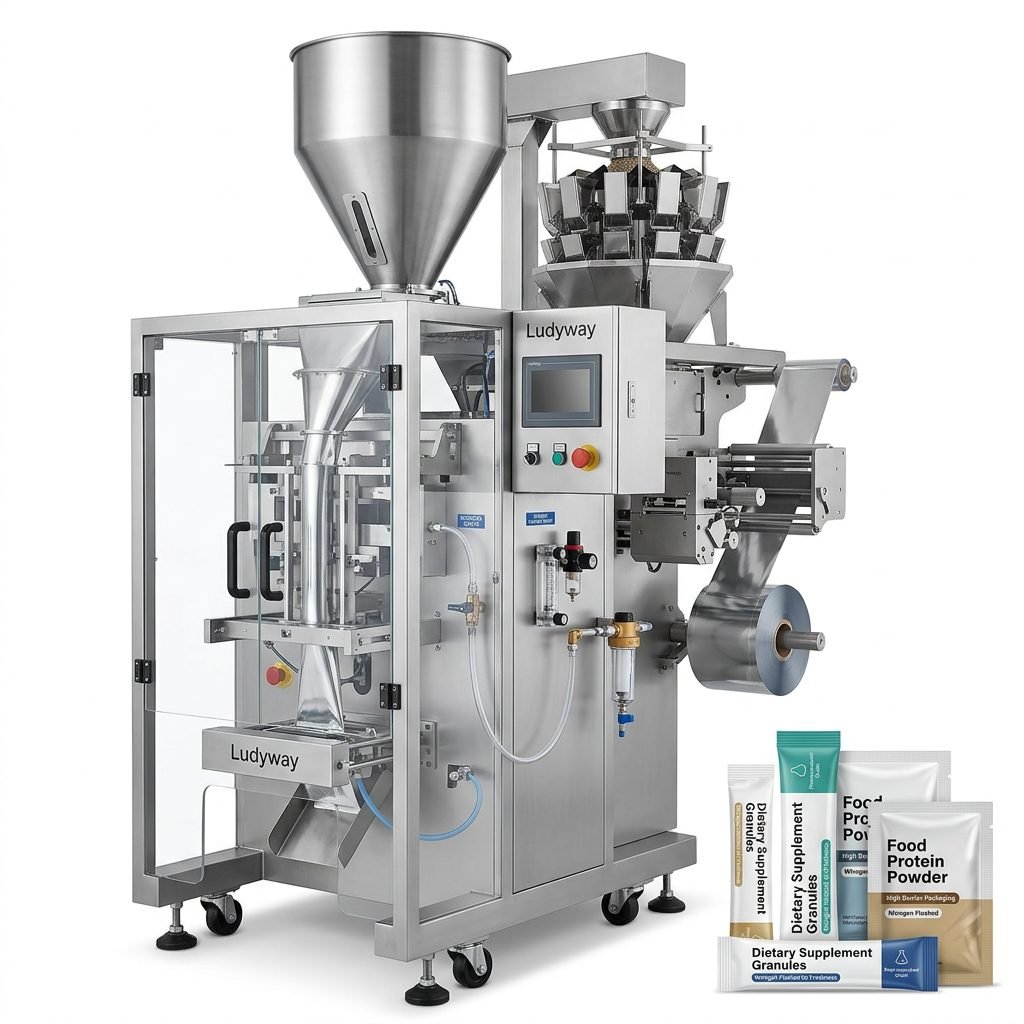
Nitrogen Flushing Gas Replacement System
View Equipment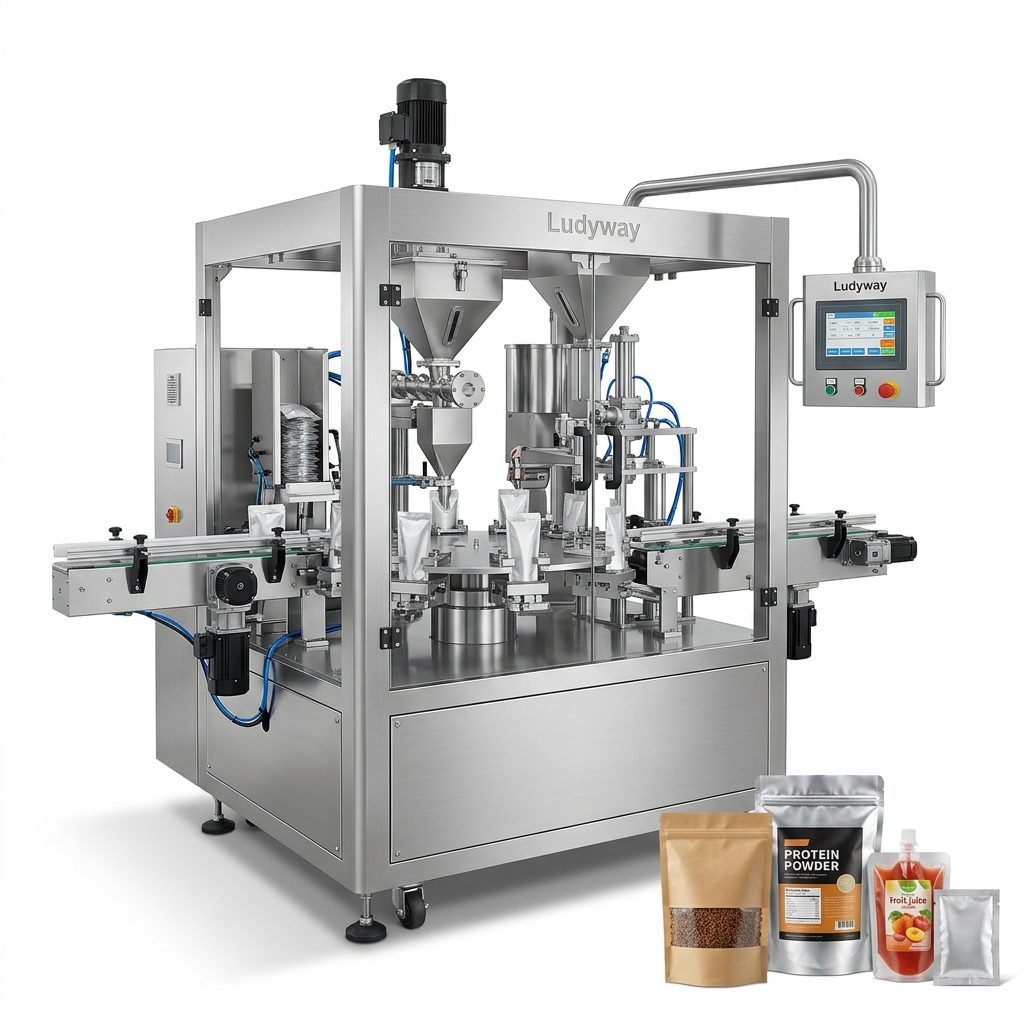
Premade Pouch Rotary Vacuum & Sealing Line
View EquipmentTechnical Specifications & Working Parameters
Review the structural and pneumatic operational data engineered into our industrial vacuum sealing series.
| Parameter | Chamber Vacuum Systems | Rotary Continuous Vacuum Lines | Modified Atmosphere (MAP) Integration |
|---|---|---|---|
| Evacuation Rate | Up to 99.8% Vacuum Level | High-speed dynamic degassing | Controlled Gas Replacement (<0.5% O2) |
| Production Output | 10 – 35 cycles/min | 40 – 90 pouches/min | 30 – 60 packs/min |
| Sealing Length / Width | 400mm – 1000mm (Double bar) | 120mm – 320mm rotary stations | Customized tooling per tray/pouch |
| Film Compatibility | PA/PE, PET/AL/PE, Barrier Nylons | Multi-layer laminated rollstock/pouches | High-barrier EVOH, Anti-fog laminates |
| Pneumatic & Power | 0.6 – 0.8 MPa | 380V / 220V 50/60Hz | 0.6 – 0.8 MPa | 3-Phase 380V | 0.6 – 0.8 MPa | 3-Phase 380V |
| Frame Construction | SUS304 Stainless Steel (Washdown) | SUS304 / SUS316 Pharma Grade | IP65 Hygienic Food Contact Design |
Why Vacuum Sealed Packaging Is Essential in Modern Automation
An engineering breakdown of barrier dynamics, shelf-life extension, and automated production efficiency.
1. Scientific Principles of Vacuum Barrier Preservation
Aerobic microorganisms, including molds and bacteria, require oxygen to metabolize and reproduce. When fresh produce, dried powders, freeze-dried meats, or perishable foods are packed under conventional atmospheric conditions, residual oxygen accelerates lipid oxidation, color degradation, and nutrient breakdown. By utilizing an industrial vacuum sealed packaging machine, the atmospheric pressure inside the package is reduced to under 10 mbar, effectively eliminating the gaseous reactant necessary for spoilage.
Furthermore, vacuum packaging removes moisture-laden air, protecting hygroscopic powders—such as milk formulas, chemical additives, and effervescent nutraceuticals—from caking, hydrolytic degradation, and loss of potency.
A vacuum package is only as reliable as its boundary seal. Micro-leaks caused by inconsistent temperature profiles or contaminated seal areas allow gradual air ingress. Ludyway packaging machines utilize dual-zone thermal impulse bars and pneumatic seal equalizers to guarantee leak-free hermetic seals even when dealing with fine powders or oily food residues.
2. Versatility Across Diverse Product Categories
While commonly associated with frozen and fresh meats, advanced vacuum packaging systems are critical across numerous manufacturing sectors:
- Freeze-Dried Foods & Seafood: Freeze-dried items have extremely porous cellular matrices. Vacuum sealing protects them from atmospheric re-hydration and preserves crispness over multi-year storage cycles.
- Fine Chemical & Pharmaceutical Powders: Active pharmaceutical ingredients (APIs) and reactive chemical compounds require hermetic containment to prevent volatilization, airborne moisture absorption, or worker exposure.
- Specialty Electronics & Precision Components: Sensitive semiconductors, optical sensors, and medical devices benefit from vacuum packaging to mitigate surface oxidation, particulate contamination, and electrostatic risk during global freight.
- Pet Treats & Animal Nutrition: High-protein dehydrated pet chews and kibbles retain their lipid stability and aroma without artificial preservatives when packaged in high-barrier vacuum envelopes.
3. Seamless Integration with Downstream Turnkey Packaging Lines
A stand-alone sealing unit often creates a bottleneck in modern high-speed operations. Ludyway designs complete modular systems where vacuum units integrate directly with upstream packaging auxiliary equipment (such as vacuum feeders, multi-head weighers, and conveyor systems) as well as downstream automated cartooning, batch coding, and case packing systems.
This holistic integration minimizes manual human intervention, meets stringent HACCP and GMP sanitary standards, and elevates overall line productivity (OEE) beyond 95%.
About Ludyway Machinery
Over 30 years of engineering pedigree delivering global packaging solutions across more than 100 countries.
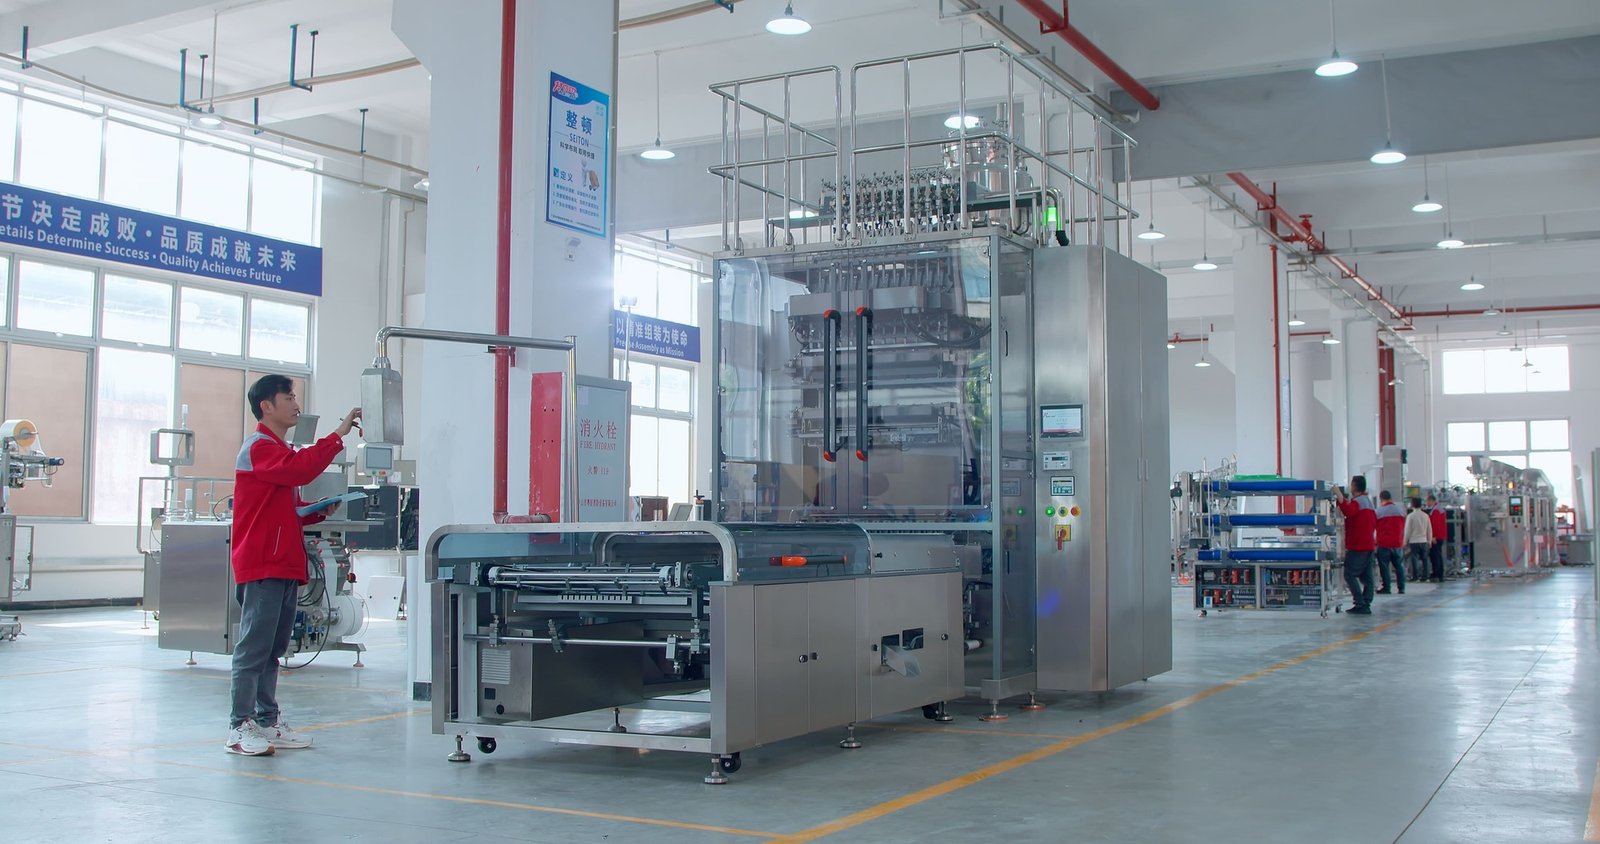
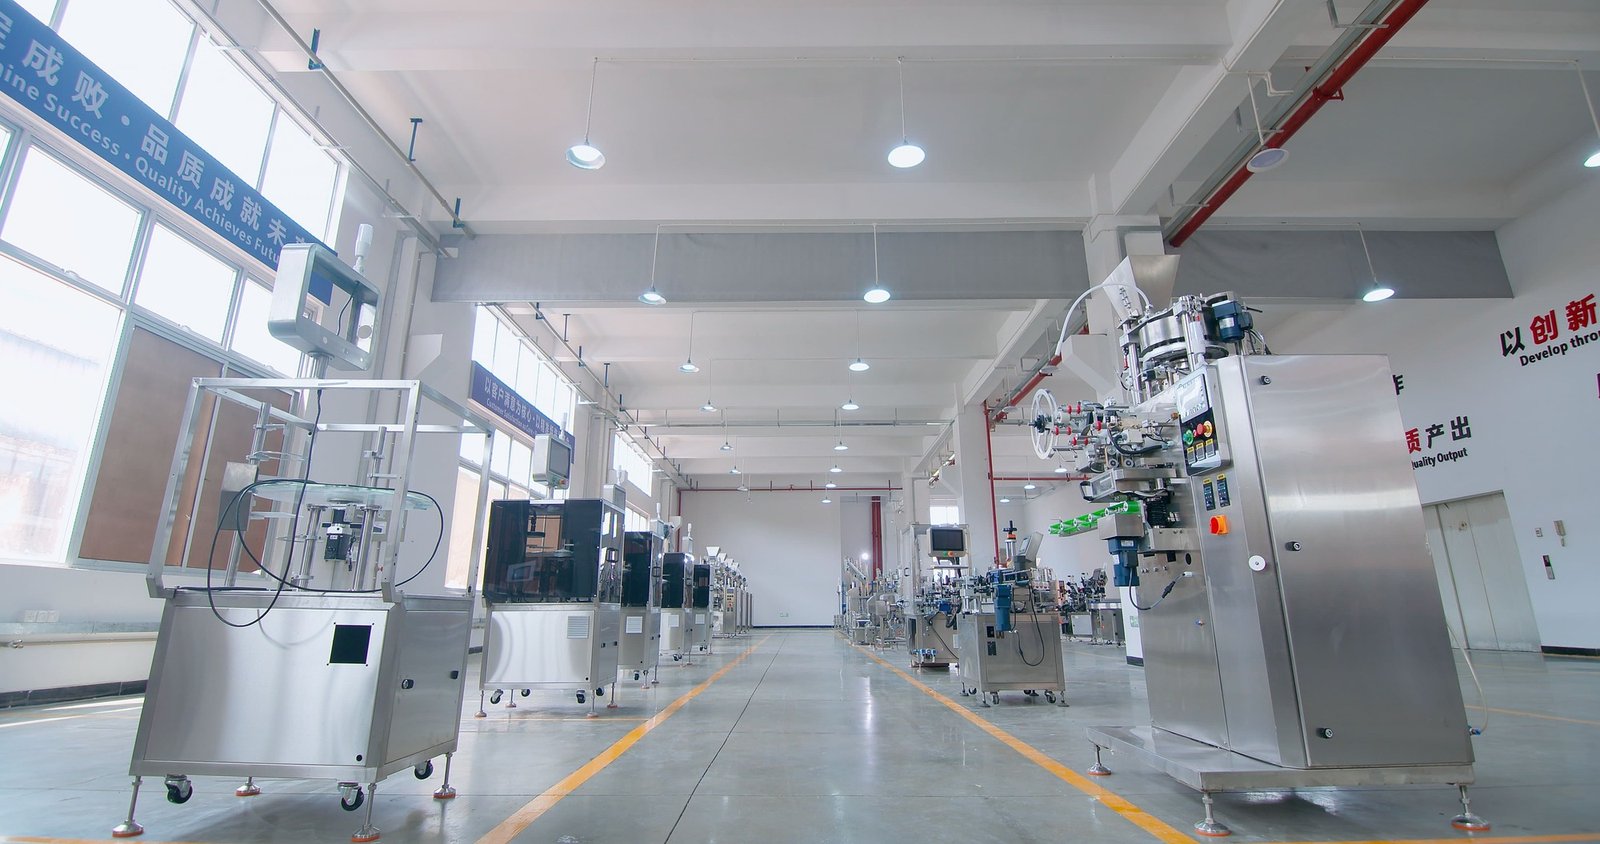
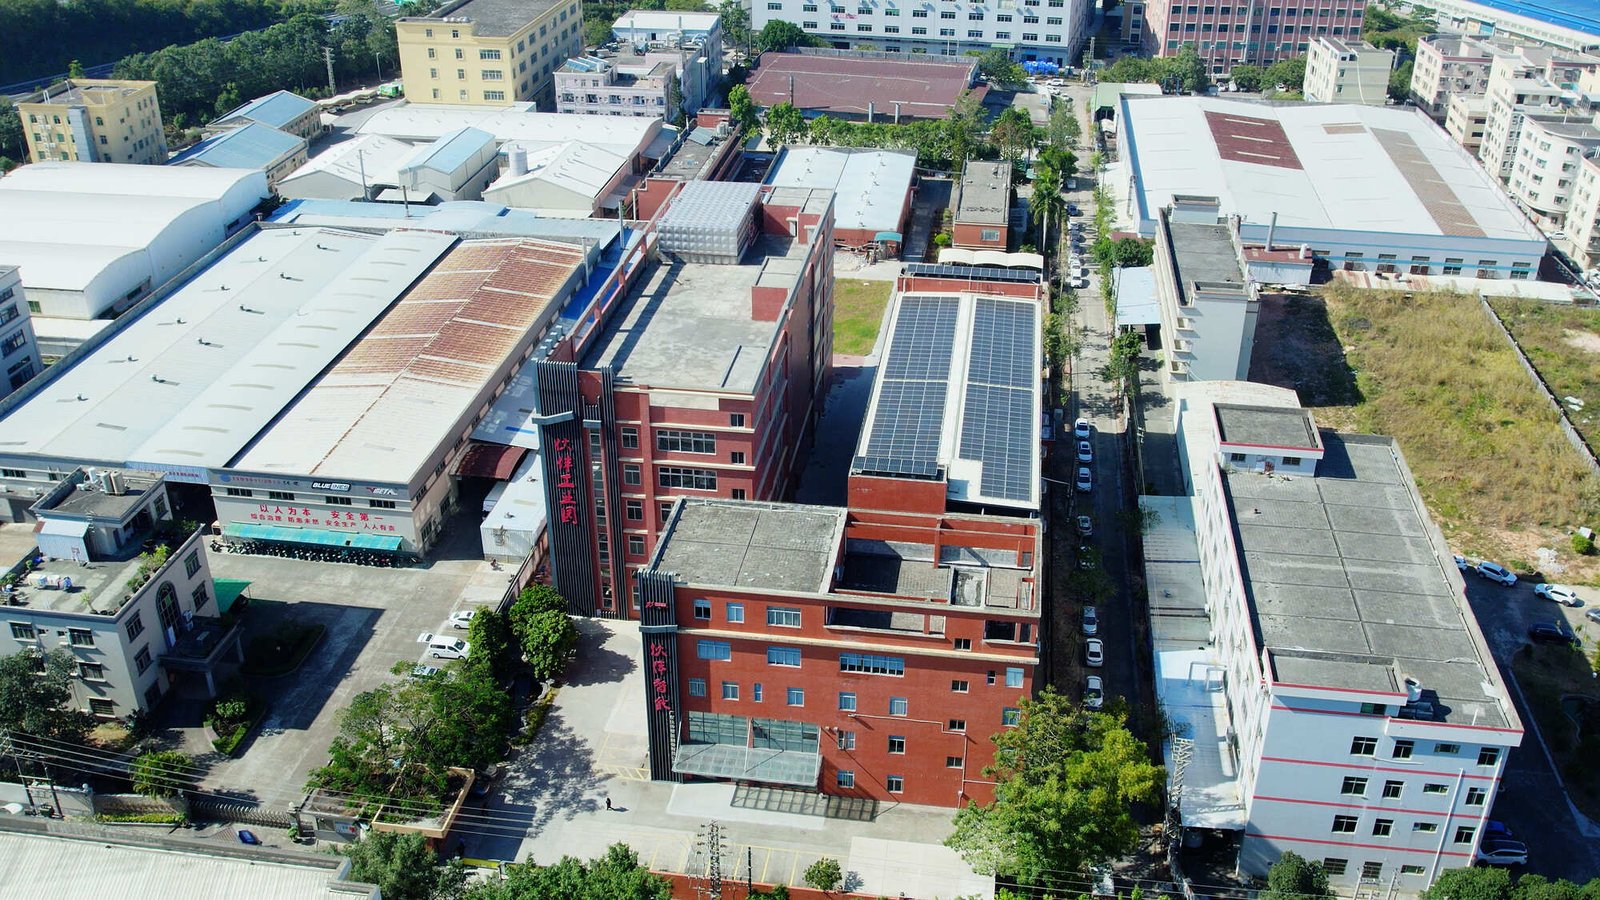
Ludyway is recognized as one of China’s premier packaging machine manufacturers, specializing in advanced packaging machinery and turnkey production line integration for the food, pharmaceutical, chemical, and health industries. Operating from a modern 20,000㎡ manufacturing facility equipped with over 200 precision manufacturing units, our 130+ engineering and packaging specialists engineer solutions tailored to your unique throughput and barrier requirements.
From stick packs and multi-lane sachet form-fill-seal equipment to high-speed industrial vacuum sealed packaging systems, we deliver durable, intelligent, and cost-effective automation designed for maximum uptime.
International Certifications & Global Presence
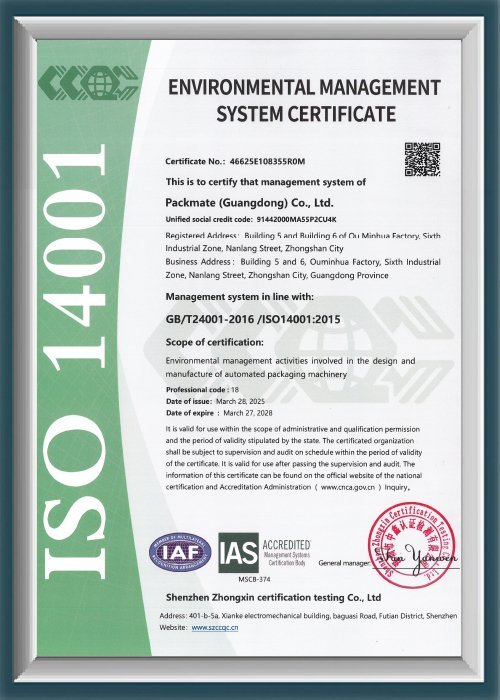
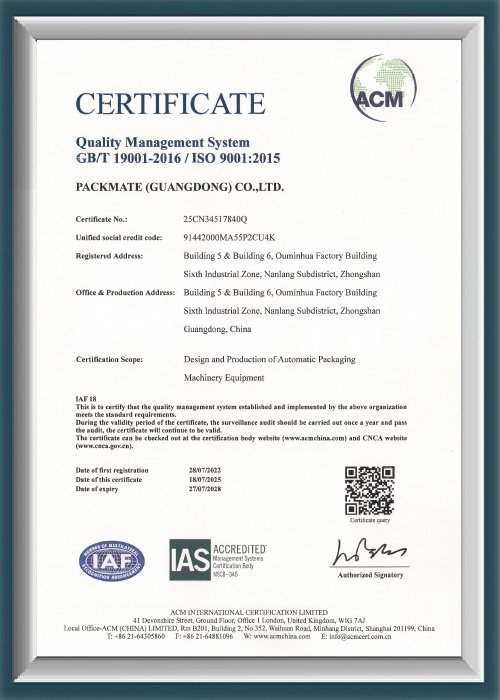
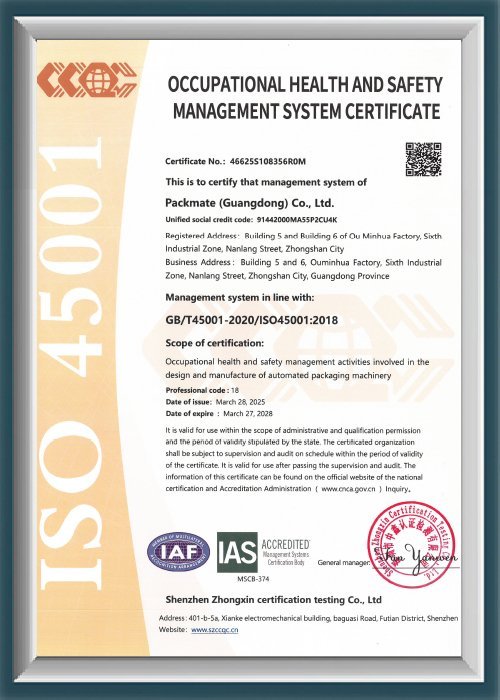
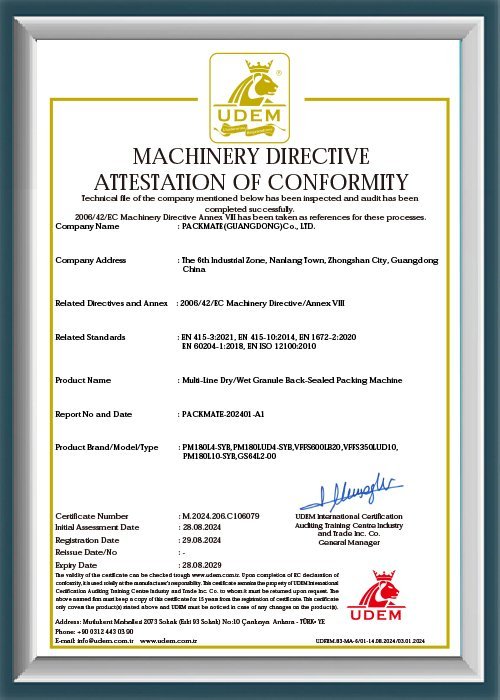
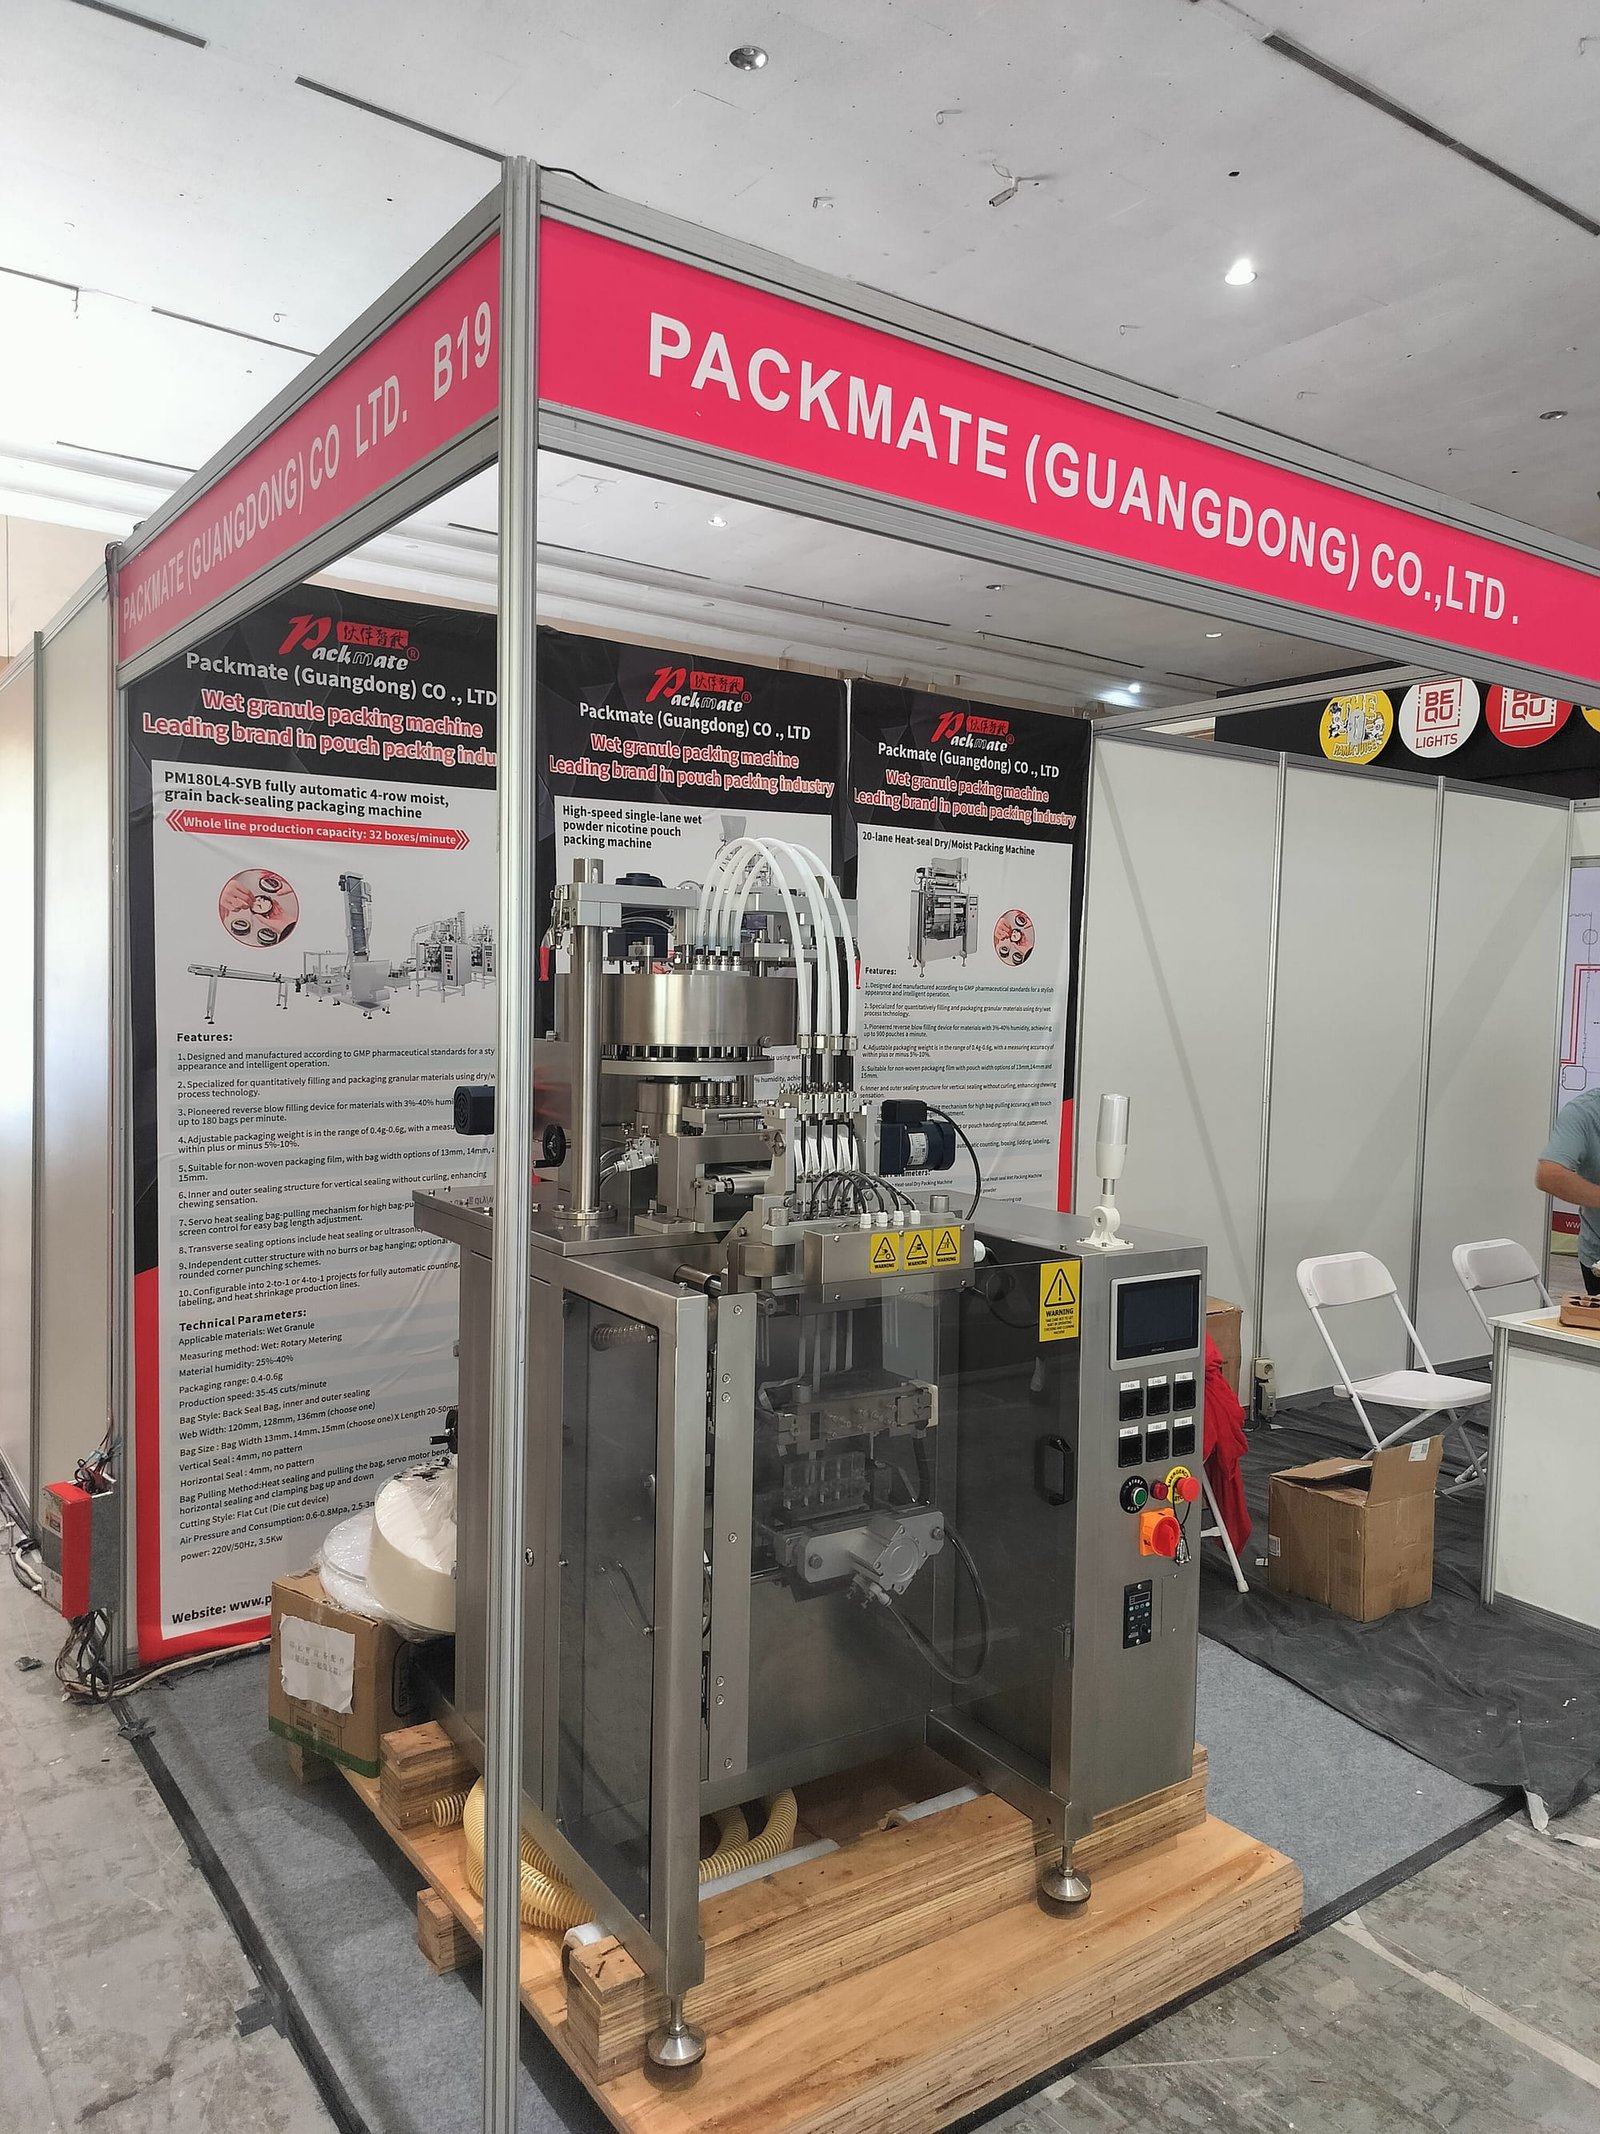
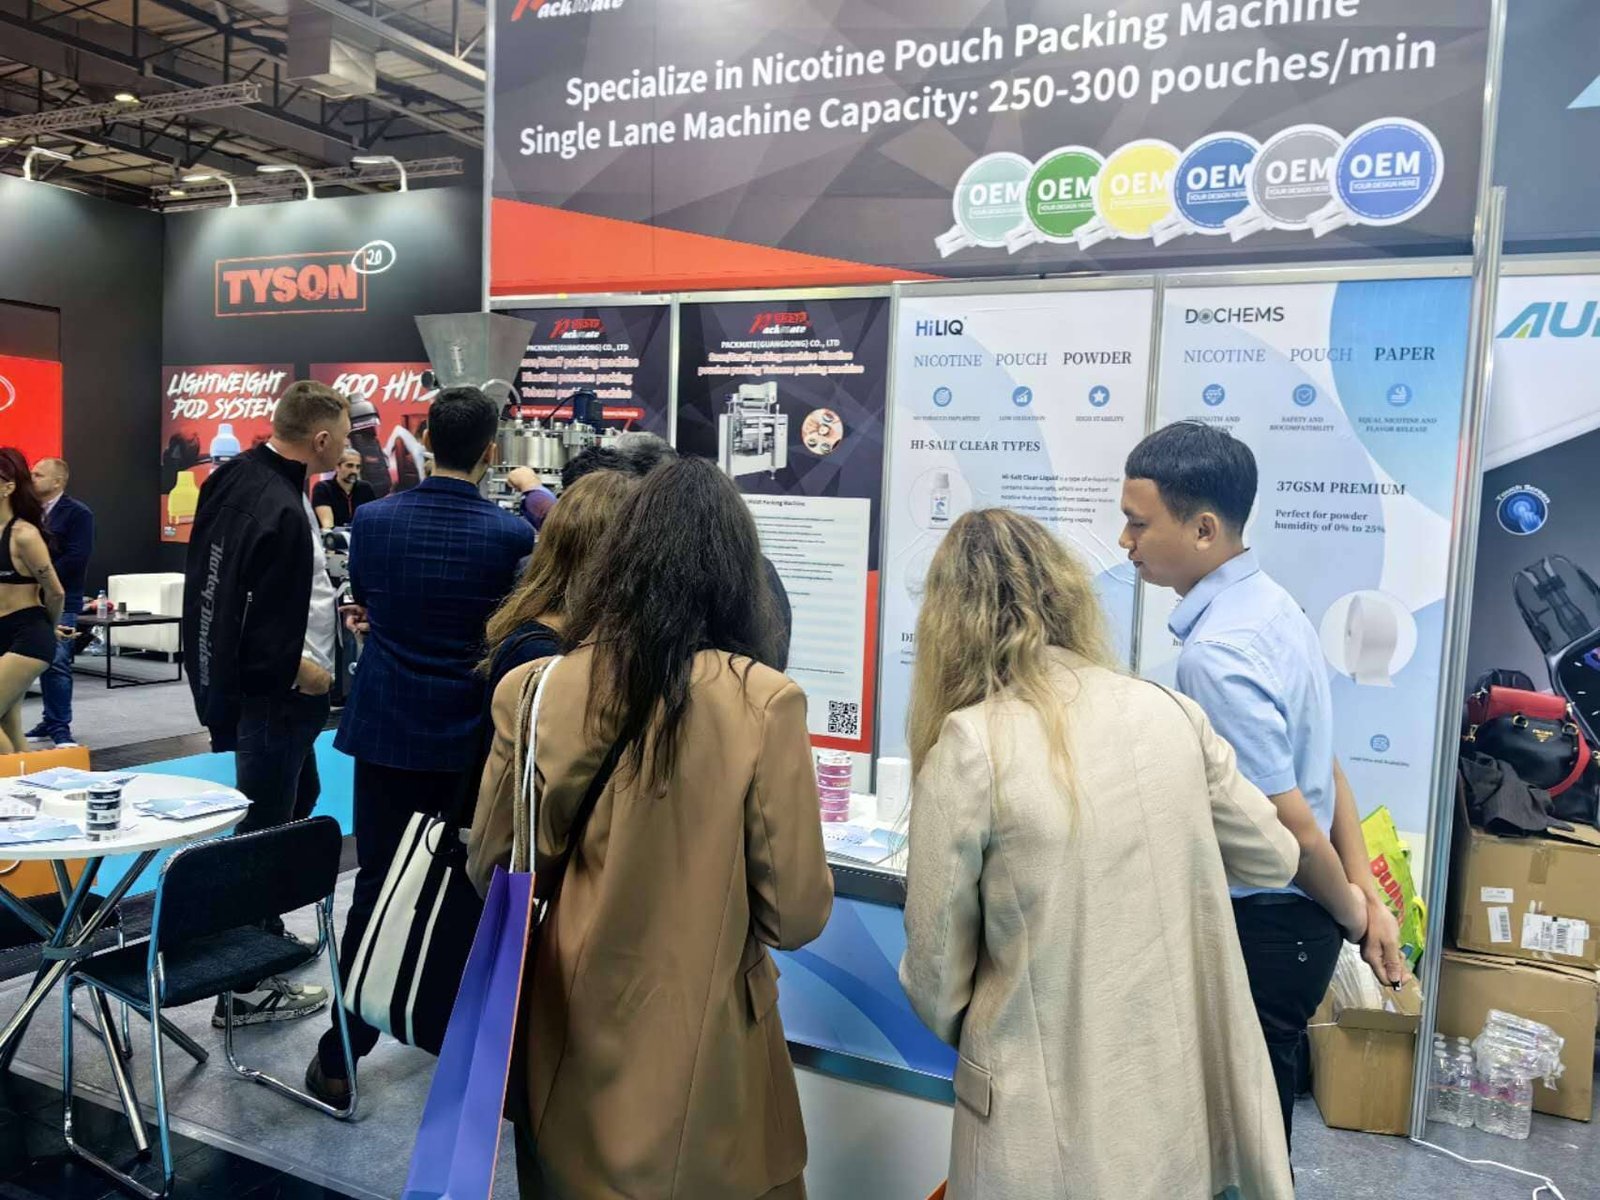
Our packaging equipment is manufactured in compliance with international CE, ISO9001, and cGMP standards, showcased regularly at leading industry expos worldwide.
Trusted by Leading Global Brands
We partner with premier material and component suppliers across the globe to assure unmatched machine reliability.
Frequently Asked Questions
Get immediate answers regarding machine selection, maintenance, and integration capabilities.
Standard vacuum sealing draws out ambient air, causing the pouch to collapse tightly around the product. This is optimal for dense solids, freeze-dried meats, and hardware. For fragile products (such as potato chips or brittle baked goods) or items where physical compression causes crushing, a Nitrogen Flushing Packaging System replaces oxygen with inert nitrogen gas to prevent oxidation without compressing the item.
Our equipment accommodates a broad spectrum of high-barrier materials, including Nylon/PE (PA/PE), PET/AL/PE, EVOH high-barrier films, laminated Kraft paper barrier composites, and recyclable mono-material films. Sealing temperature, cooling time, and pneumatic pressure are finely adjustable via the digital HMI screen.
Yes. Ludyway provides custom engineering designs to match cleanroom footprints, conveyor heights, and regional industrial power supplies (such as 380V 3-phase 50Hz, 220V 60Hz, or 480V systems). Full turnkey engineering services are available to configure end-to-end lines.
Ready to Upgrade Your Packaging Line Efficiency?
Contact our technical engineers today for customized machinery configurations, free product sample testing, and complete turnkey production proposals.