Food Vacuum Packaging Machine | Reliable Packaging Solutions
Empowering commercial food manufacturers, processing facilities, and high-capacity packagers with intelligent, airtight preservation technology engineered for extended shelf life, zero flavor degradation, and ultimate microbial safety.
Why Industrial Food Vacuum Packaging Outperforms Standard Packaging
In modern food manufacturing, preventing oxidative degradation and aerobic microbial proliferation is essential. An industrial-grade food vacuum packaging machine removes ambient atmospheric oxygen from hermetic barriers, significantly delaying rancidity, maintaining natural organoleptic qualities, and mitigating freezer burn across perishable and non-perishable commodities.
Oxygen Depletion & Microbial Barrier
By drawing chamber pressure below 10 mbar, Ludyway systems eliminate aerobic bacterial colonies, mildew growth, and enzymatic browning, increasing typical product shelf lives by 3x to 5x without chemical preservatives.
Moisture Retention & Weight Integrity
High-integrity thermal sealing bars create an impervious barrier against hygroscopic moisture exchange. Fresh meats, marinated proteins, and freeze-dried items maintain total net weight, juicy texture, and essential nutrients.
Puncture Resistance & Logistics Safety
Reinforced vacuum envelopes stabilize fragile goods, preventing internal movement during global distribution. High-strength barrier seals withstand deep-freeze thermal shifts, mechanical handling, and long-distance maritime shipping.
Featured Food Vacuum Packaging Machinery
Discover our cutting-edge series of automated vacuum sealing systems, modified atmosphere packaging (MAP) units, and high-speed rotary pouch machines built for granular, solid, and dehydrated food lines.
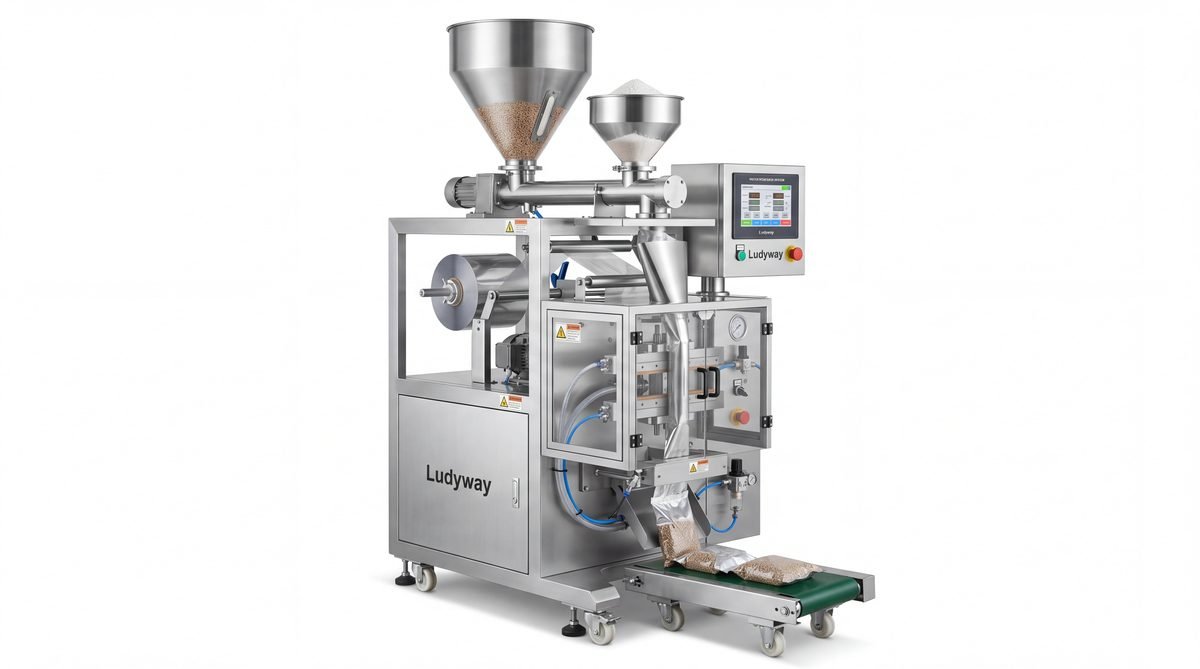
Industrial Food & Pharma Vacuum Machine
High-capacity chamber evacuation system engineered for delicate powders, bulk food staples, and fine ingredients requiring ultra-low residual O2 levels.
View Specifications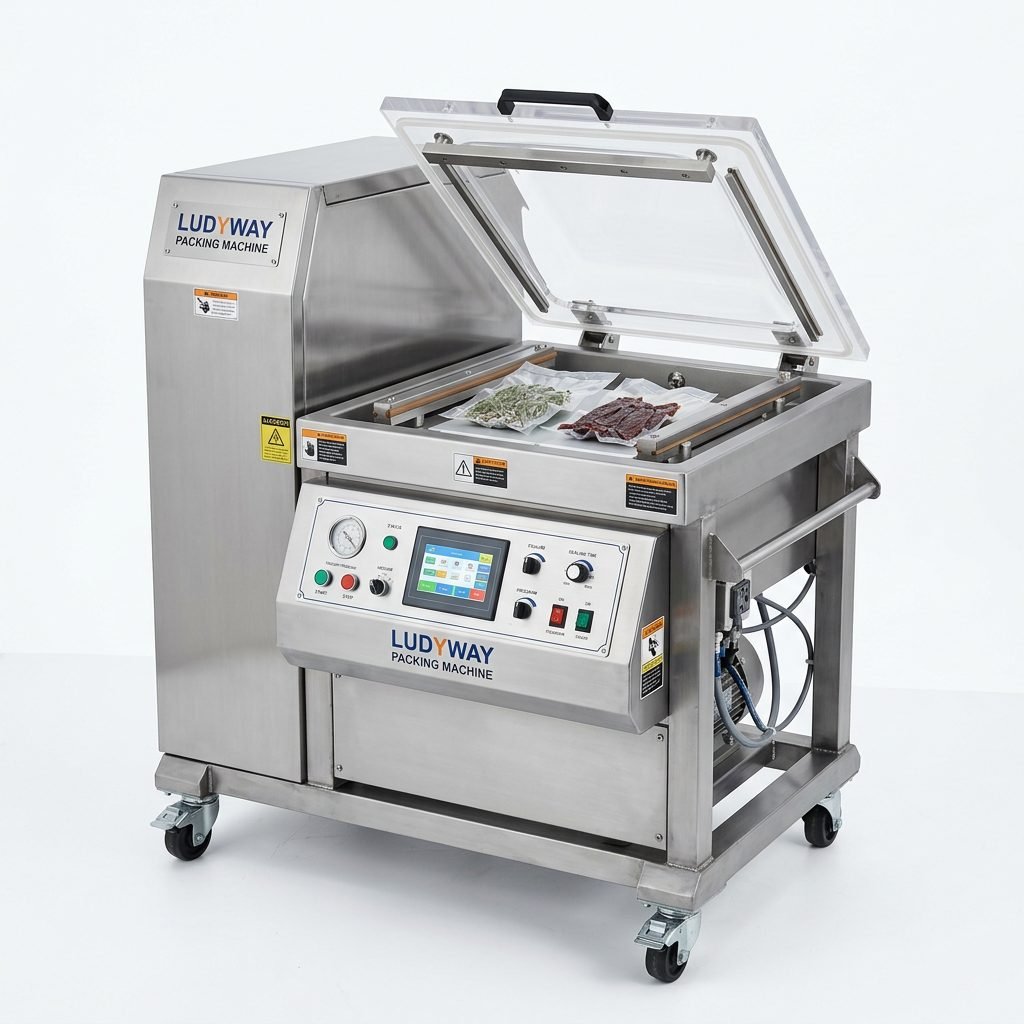
Heavy-Duty Chamber Vacuum Machine
Robust stainless steel SUS304 construction with digital vacuum sensors, dual sealing bars, and rapid cycle timing for high-throughput food packaging.
View Specifications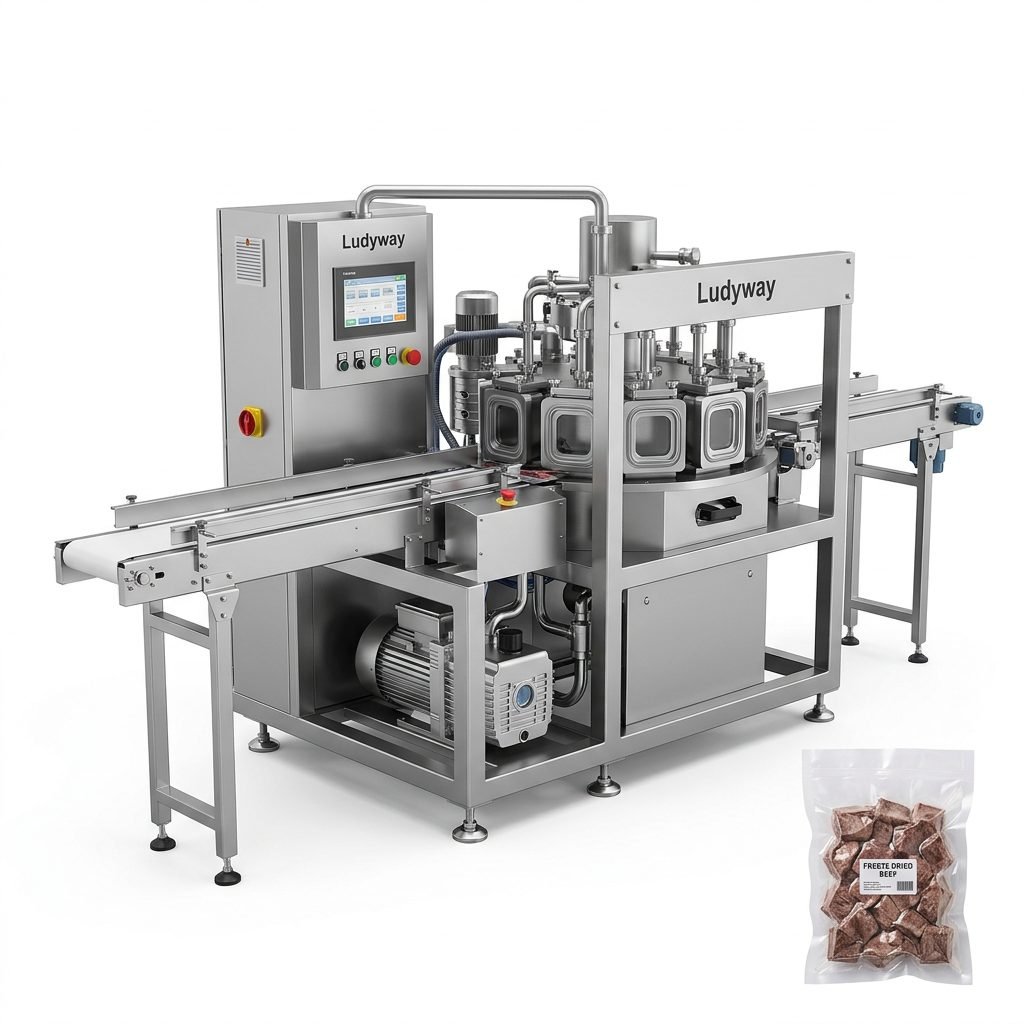
Freeze-Dried Beef Vacuum Packaging System
Specialized deoxygenation and vacuum sealing mechanism protecting dehydrated meats from atmospheric moisture and lipid oxidation.
View Specifications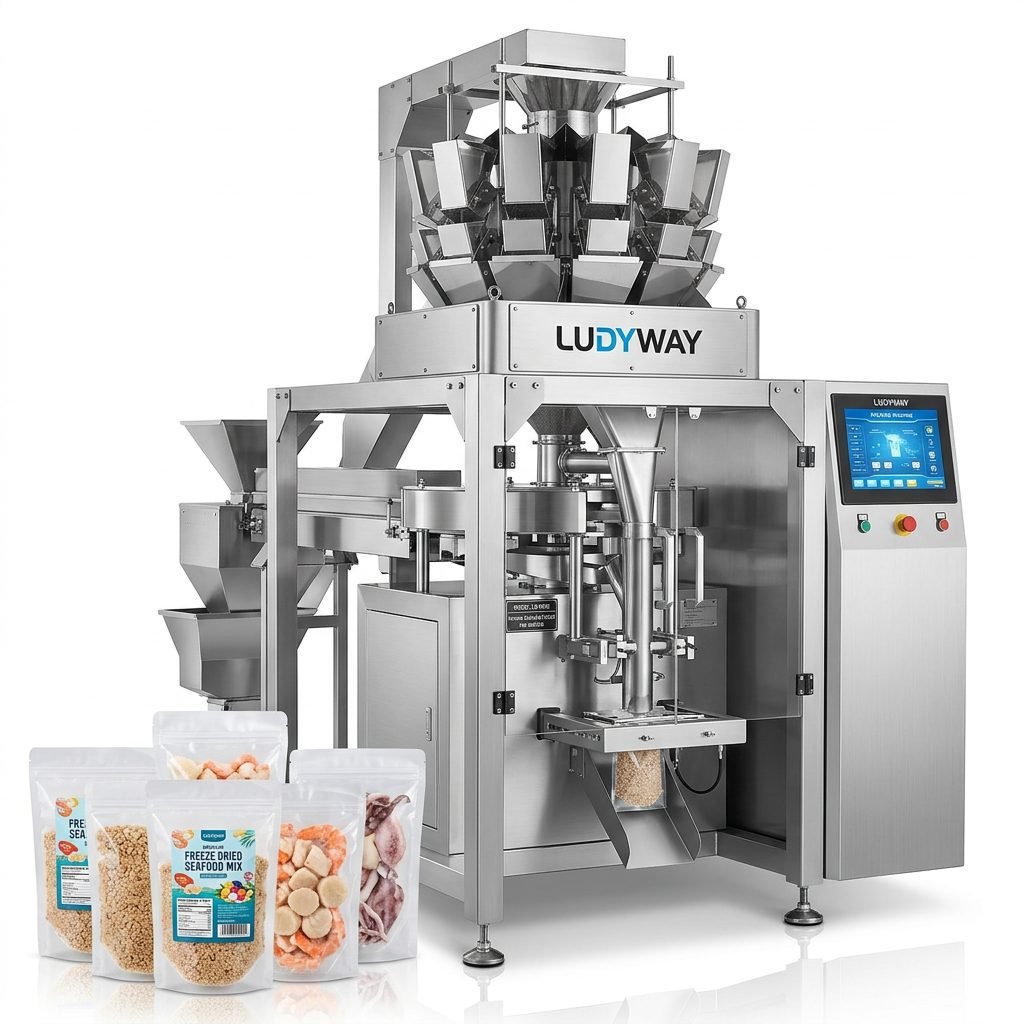
Freeze-Dried Seafood Vacuum Sealer
Optimized sealing geometry for irregular seafood pieces, maintaining rigid hermetic seals that prevent micro-leakage during long-term storage.
View Specifications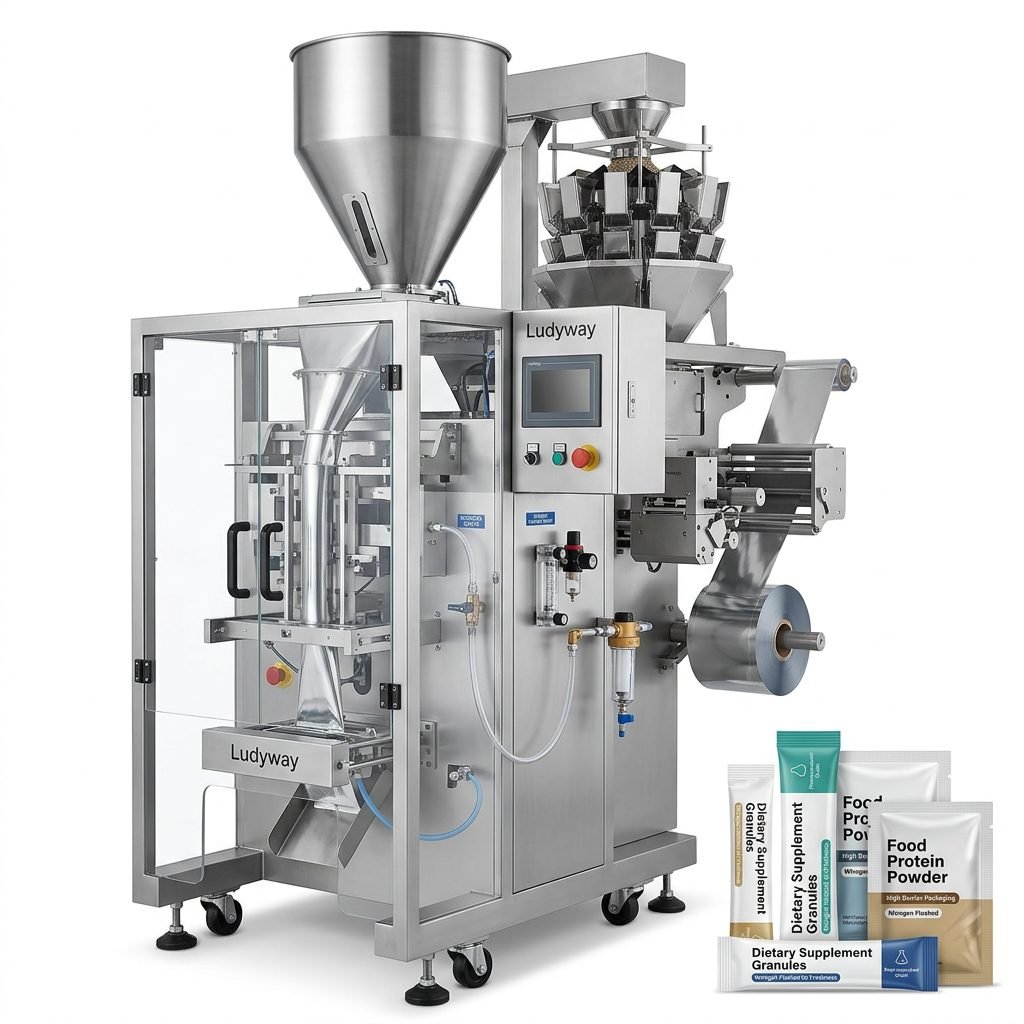
Nitrogen Flushing Vacuum MAP System
Dual-stage vacuum evacuation with inert nitrogen gas flushing for pressure-sensitive snacks, nuts, and crisp food items prone to crushing.
View Specifications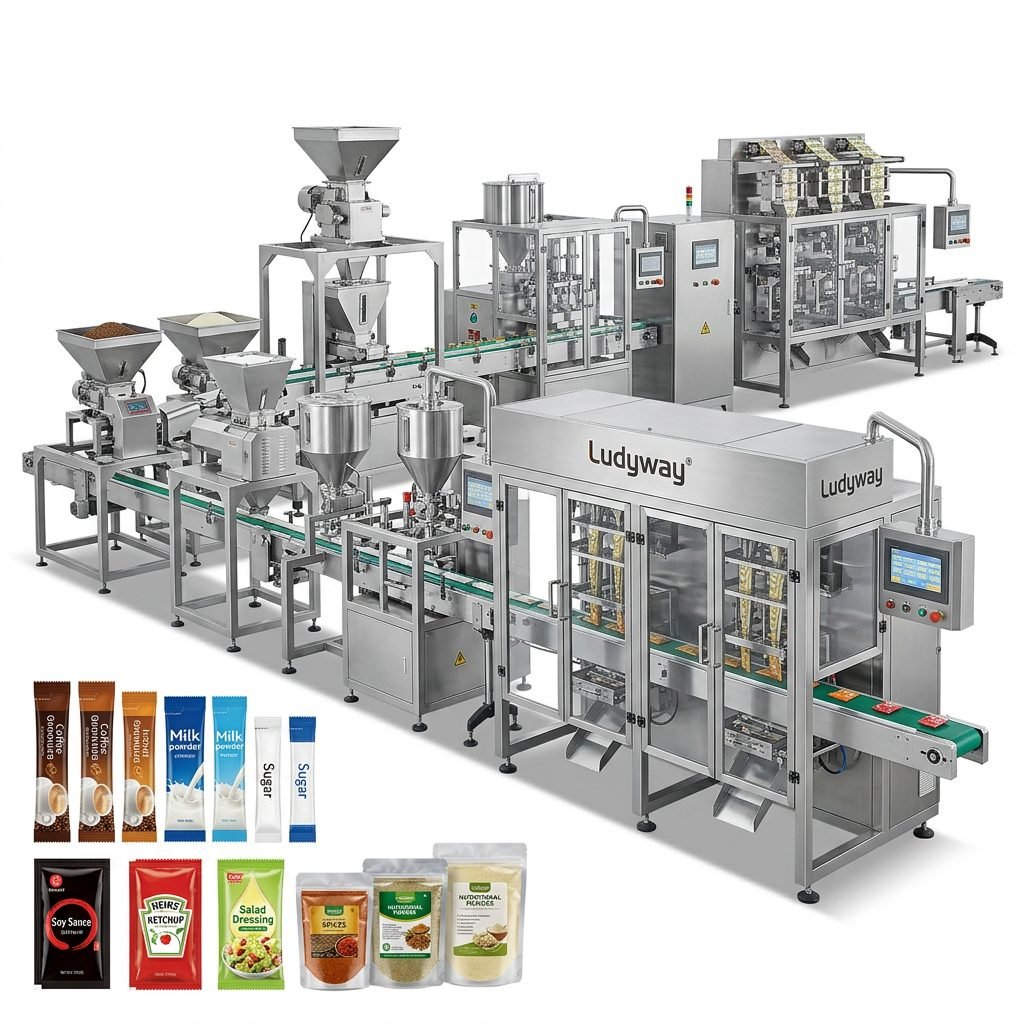
High-Speed Automated Food Packaging Line
Integrated multi-stage filling, vacuum sealing, and discharge conveyor system designed for high-throughput commercial packing plants.
View Specifications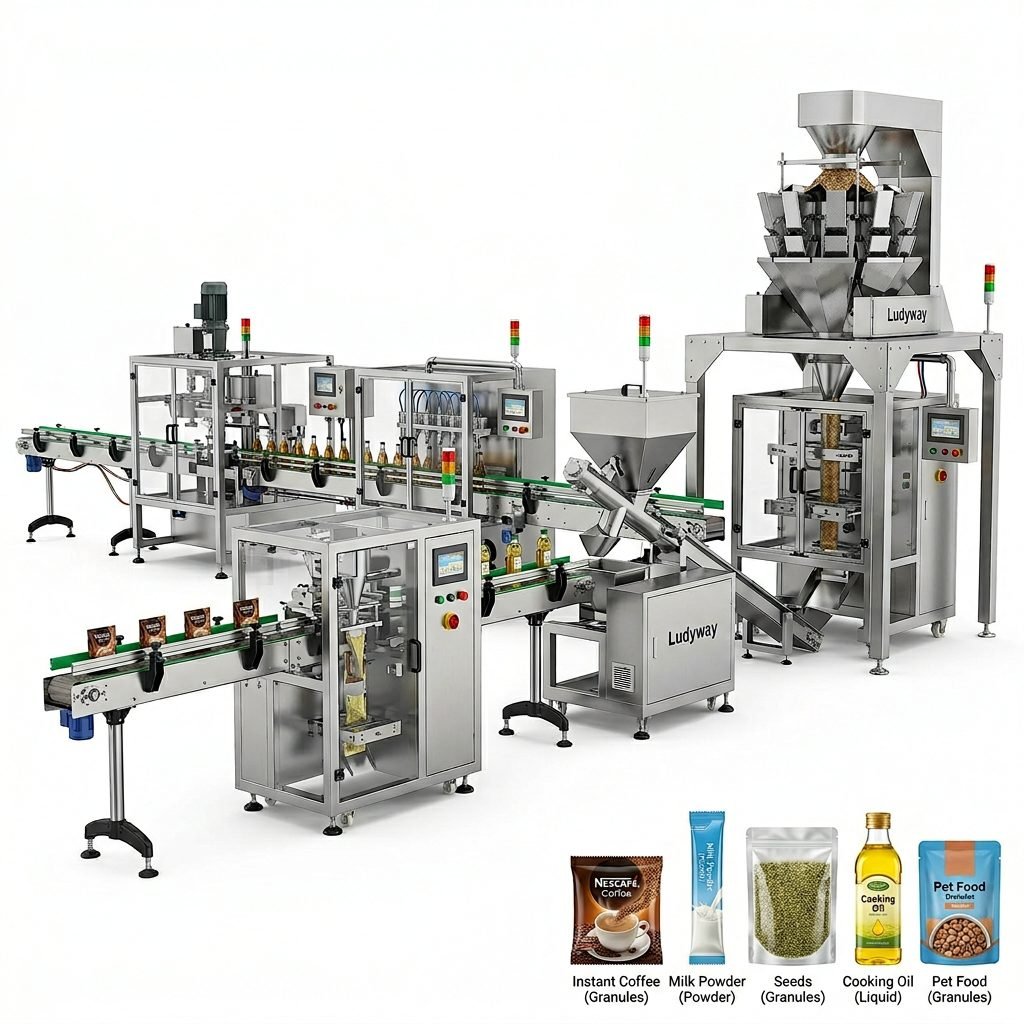
Integrated Multi-Product Food Packaging Line
Flexible PLC-controlled automated line supporting rapid changeovers across granular, solid, and multi-format vacuum pouch formats.
View Specifications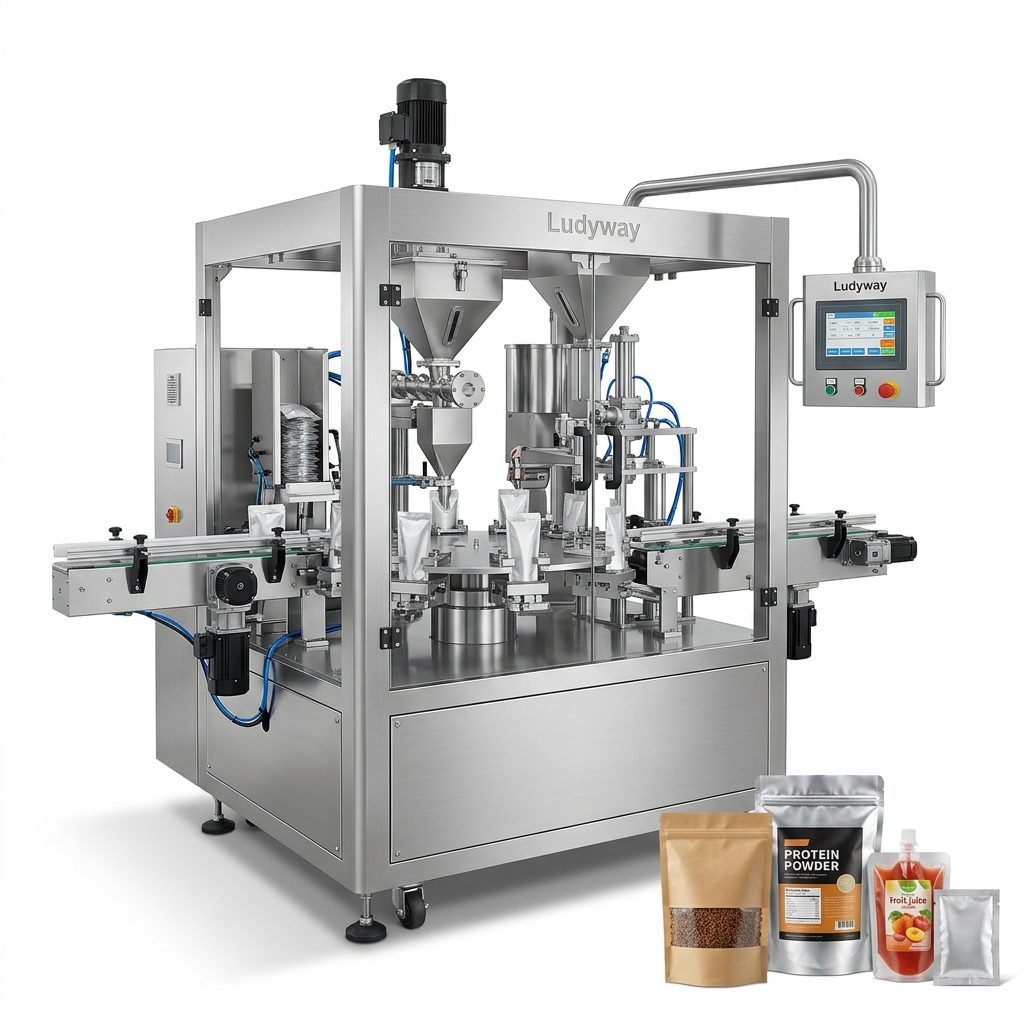
Premade Rotary Pouch Vacuum Machine
Rotary 8-station pouch pick-fill-vacuum-seal unit optimized for stand-up pouches, zipper barrier bags, and custom commercial food shapes.
View SpecificationsIndustrial Food Vacuum Machine Series Comparison
Review our core vacuum and modified atmosphere machine configurations. All models feature full stainless steel sanitary construction, Siemens or Mitsubishi PLC interfaces, and Busch vacuum pump integrations.
| Machine Architecture | Chamber / Station Mode | Vacuum Capacity | Cycle Speed | Gas Flushing (MAP) | Primary Food Application |
|---|---|---|---|---|---|
| Single Chamber Series | Batch Manual / Semi-Auto | ≤ 10 mbar (≤ 0.5% O2) | 2 – 4 cycles/min | Optional | Specialty meats, artisan cheeses, pilot production |
| Double Chamber Heavy-Duty | Dual Alternating Chamber | ≤ 5 mbar (≤ 0.2% O2) | 4 – 7 cycles/min | Included | Fresh poultry, seafood blocks, bulk institutional foods |
| Continuous Belt Vacuum Line | Automatic Conveyor Vacuum | ≤ 2 mbar (≤ 0.1% O2) | 6 – 12 cycles/min | Optional | High-volume smoked sausages, jerky, processed bacon |
| Rotary Premade Pouch Vacuum | 8 – 10 Station Rotary Index | ≤ 5 mbar (≤ 0.2% O2) | 35 – 60 pouches/min | Integrated Dual MAP | Freeze-dried fruits, nuts, ready meals, sauces |
| Thermoforming Skin / MAP Line | Continuous Rollstock Form-Fill-Seal | ≤ 1 mbar (≤ 0.05% O2) | 8 – 18 cycles/min | Multi-Gas Blend System | Fresh steaks, portioned fish fillets, deli cold cuts |
Comprehensive Commercial Food Processing Solutions
From perishable animal proteins to fragile dehydrated produce, our custom vacuum and gas replacement packaging architectures integrate directly into your food production line.
Raw & Cured Meats / Poultry
- Beef & Pork Cuts: Prevents myoglobin oxidation and surface discoloration under refrigerated shipping.
- Processed Bacon & Sausages: Eliminates aerobic bacteria and halts fat rancidity.
- Poultry Portions: Retains core juiciness without moisture loss or package ballooning.
Seafood & Aquaculture
- Whole Fish & Fillets: Suppresses histamine production and psychrotrophic bacterial growth.
- Frozen Shellfish: High-puncture multi-layer films protect shells from piercing the vacuum barrier.
- Smoked Fish Delicacies: Locks in delicate smoky aromas and volatile flavor compounds.
Dry Goods, Nuts & Freeze-Dried
- Freeze-Dried Produce: Prevents ambient air rehydration, retaining extreme crispness.
- Nuts & Seeds: Eliminates oil oxidation, preventing rancid odor and staleness.
- Specialty Grains & Rice: Controls moisture and prevents weevil infestations during long-term storage.
About Ludyway Packaging Machinery
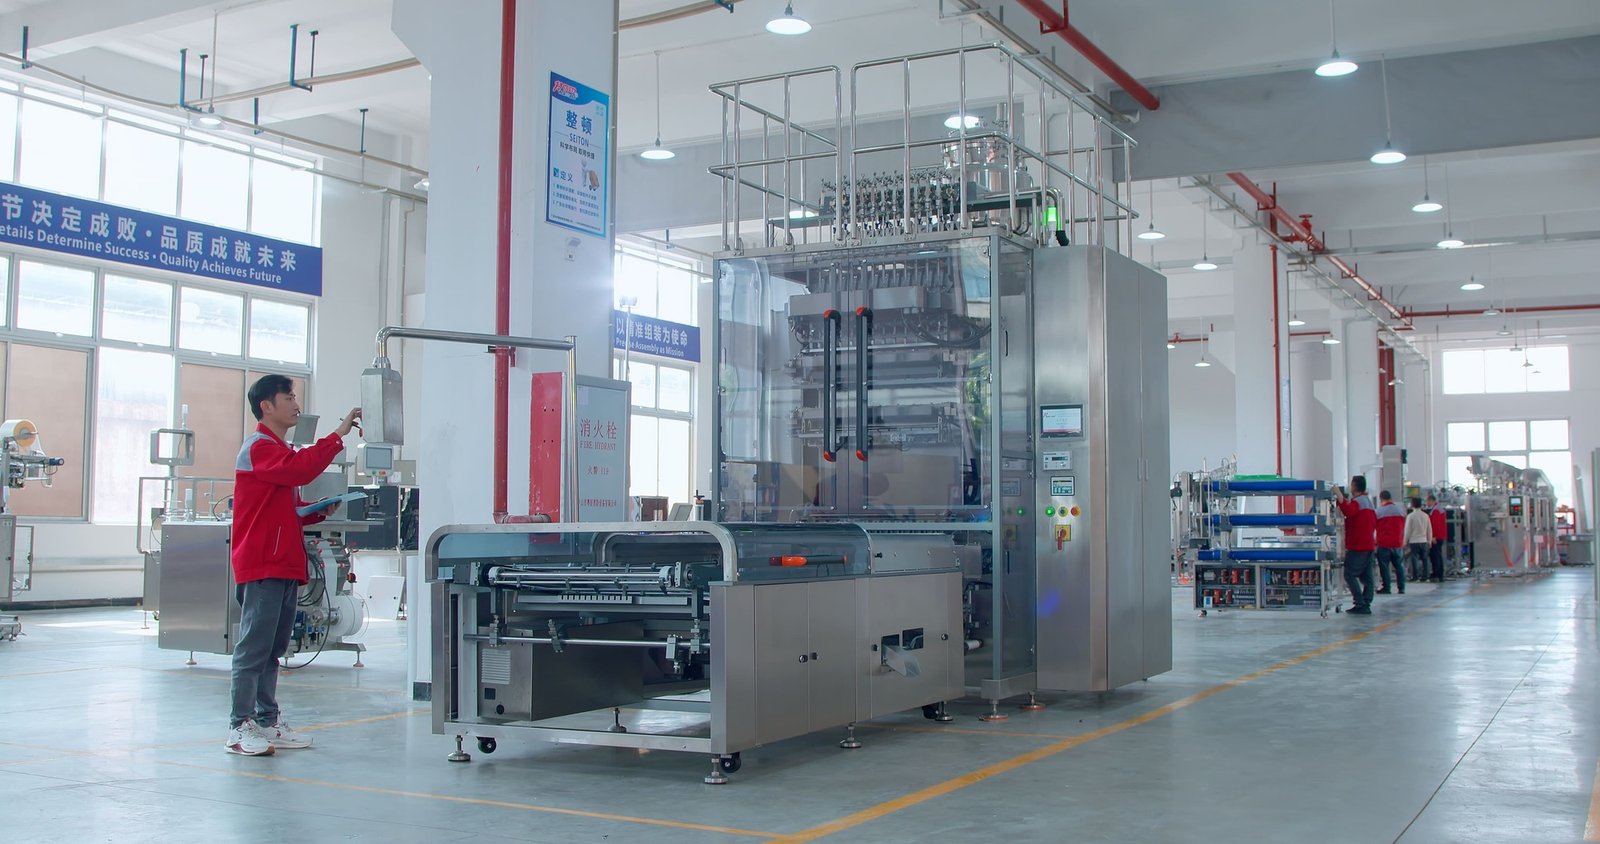
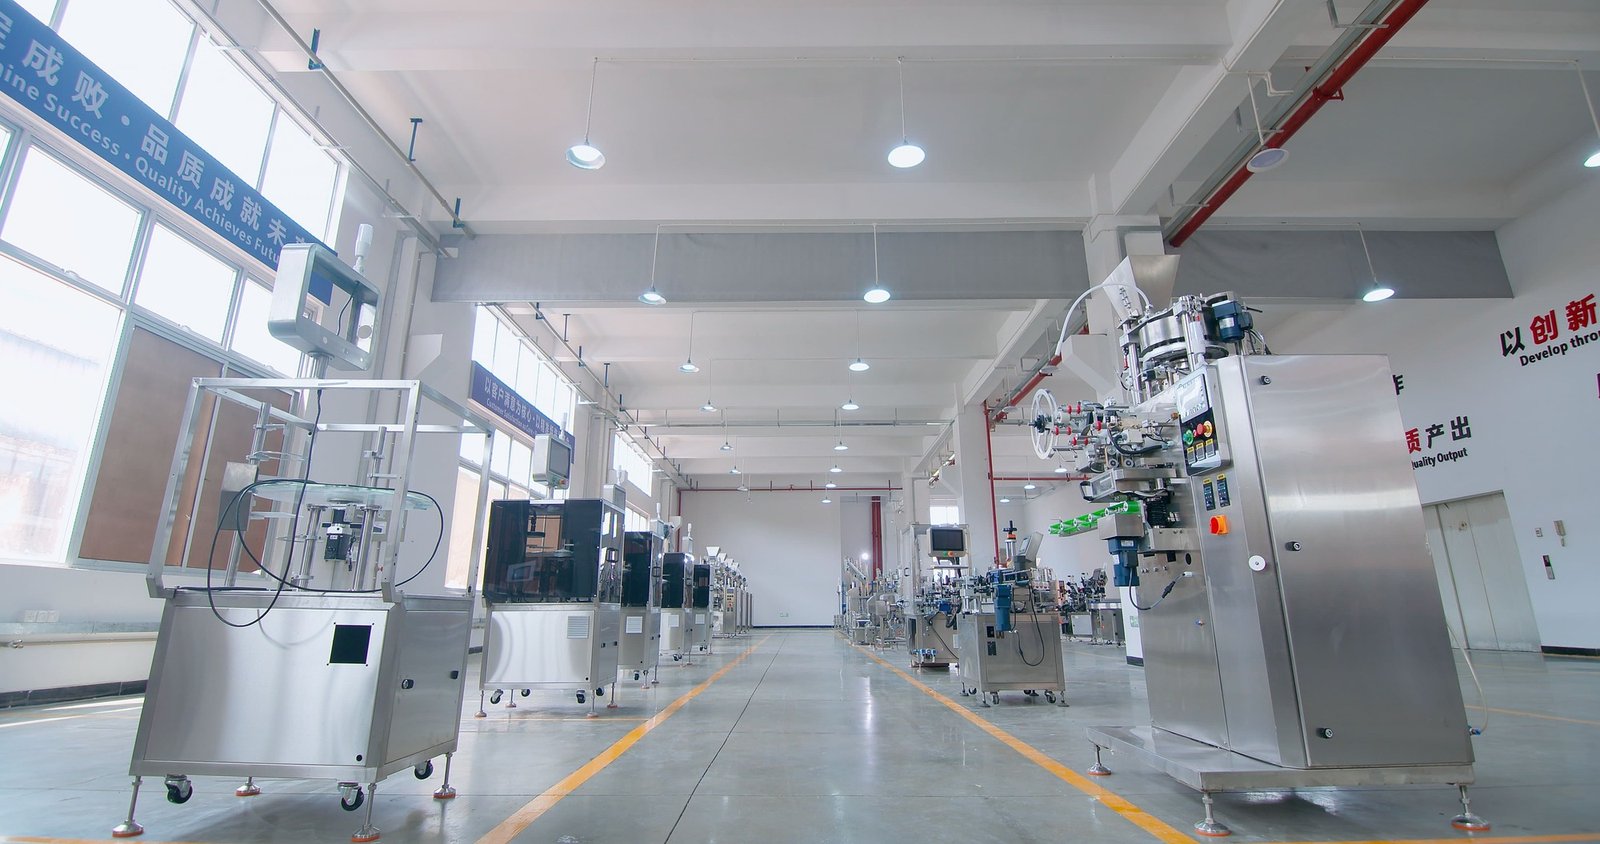
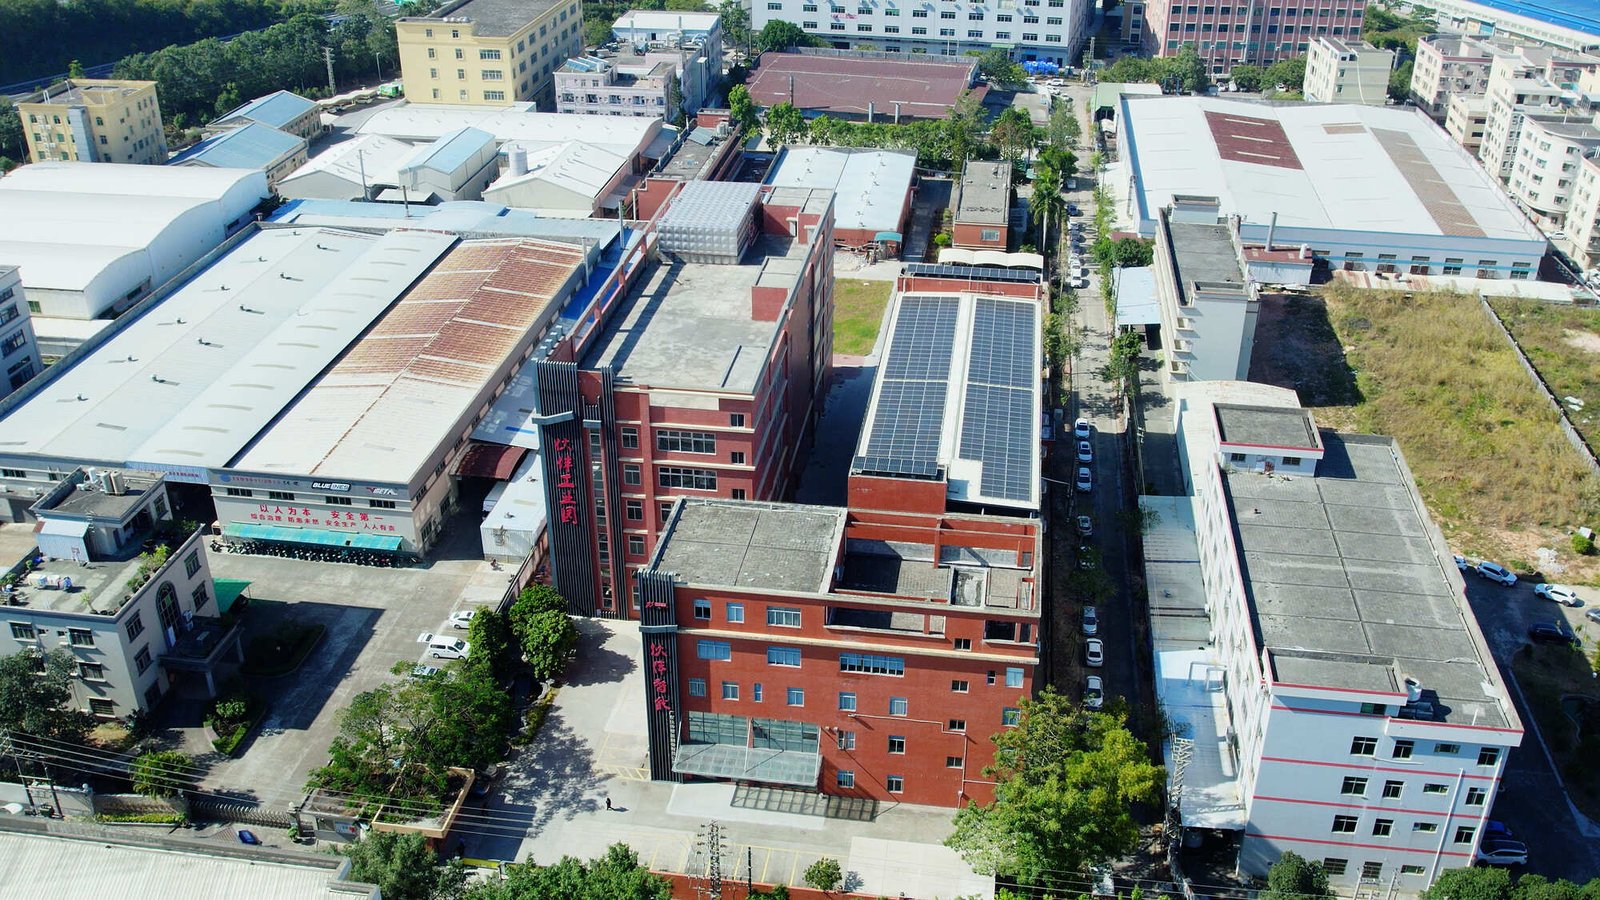
Ludyway is one of China’s premier packaging machine manufacturers, delivering turnkey automation and advanced preservation packaging equipment for the global food, dairy, pharmaceutical, and health industries. Backed by 30+ years of technical experience, we operate a 20,000㎡ modern manufacturing facility equipped with over 200 precision machining and testing units.
Our engineering roster of 130+ technical experts continuously develops high-performance machinery across 50+ intelligent packaging models. From custom modified atmosphere vacuum sealers to multi-lane sachet packaging and high-speed rotary bagging, Ludyway equipment powers production in more than 100 countries and regions worldwide.
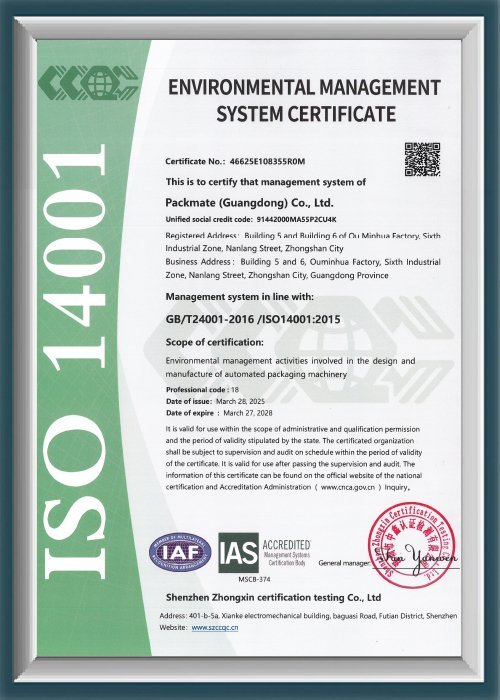
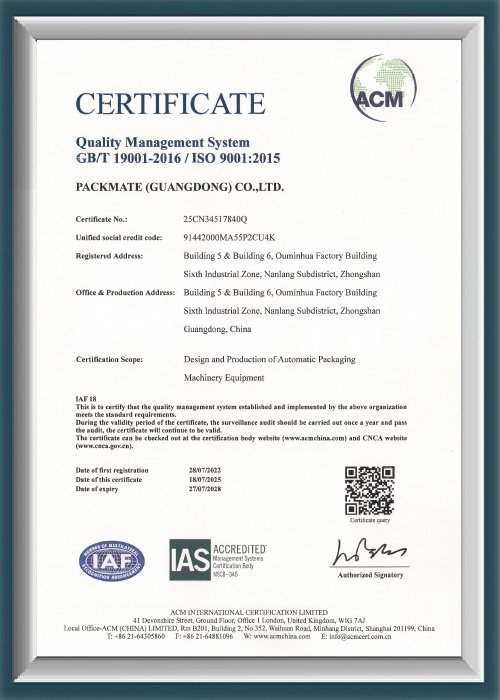
Certified Manufacturing & Global Exhibitions
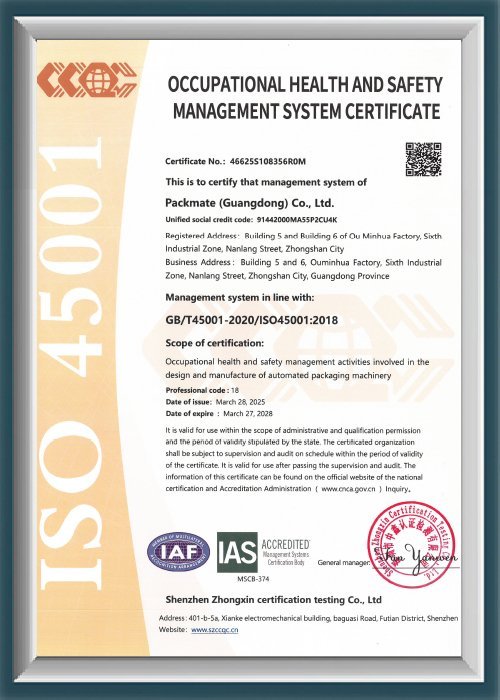
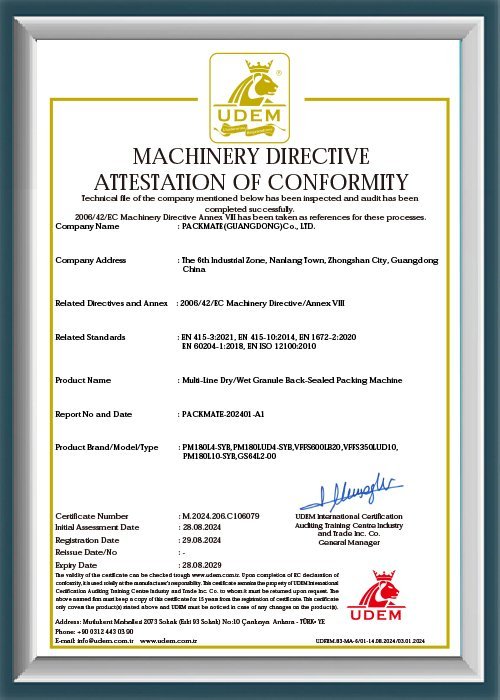
Ludyway packaging machines comply strictly with European CE directives, ISO9001 quality management benchmarks, and cGMP sanitary standards for food safety and cleanroom operation.
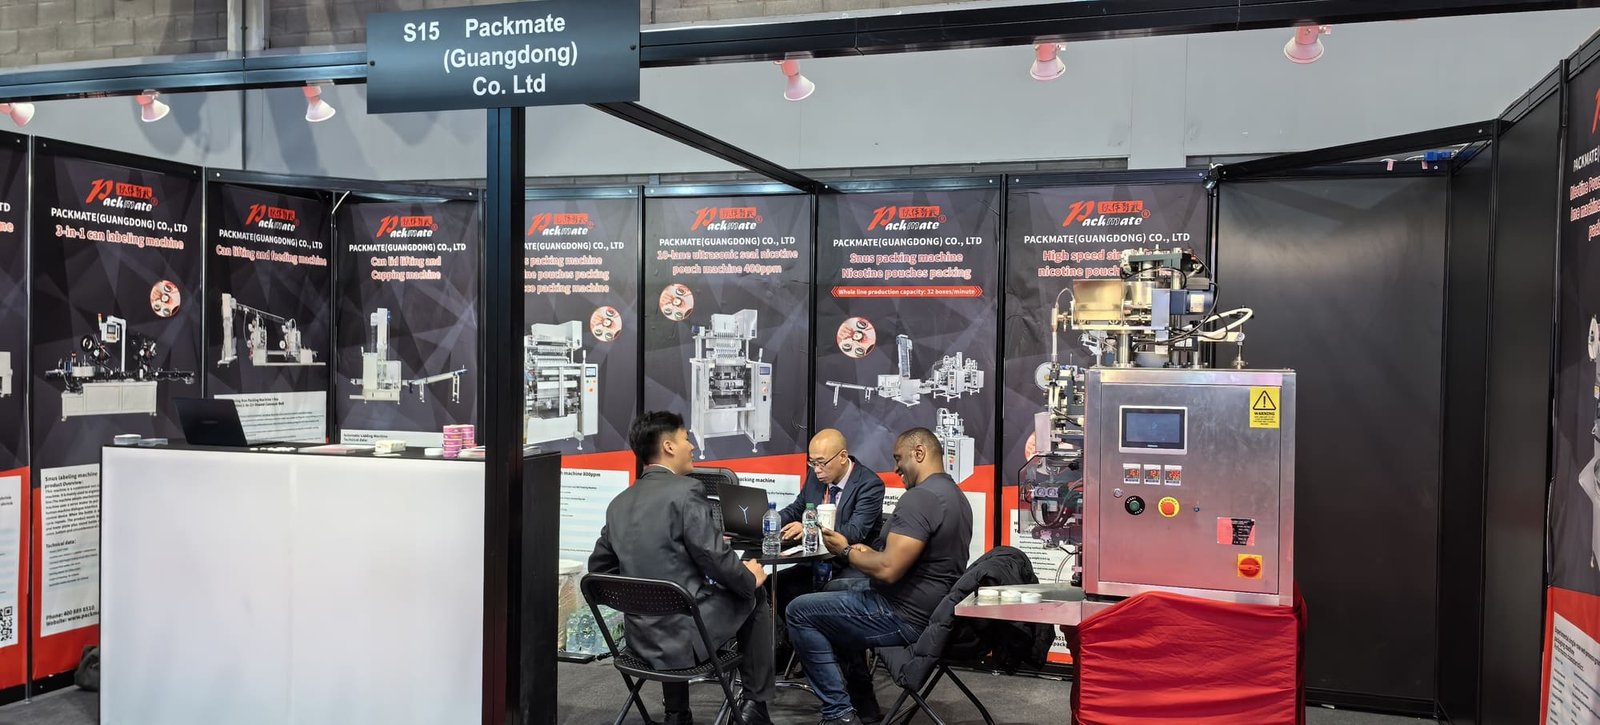
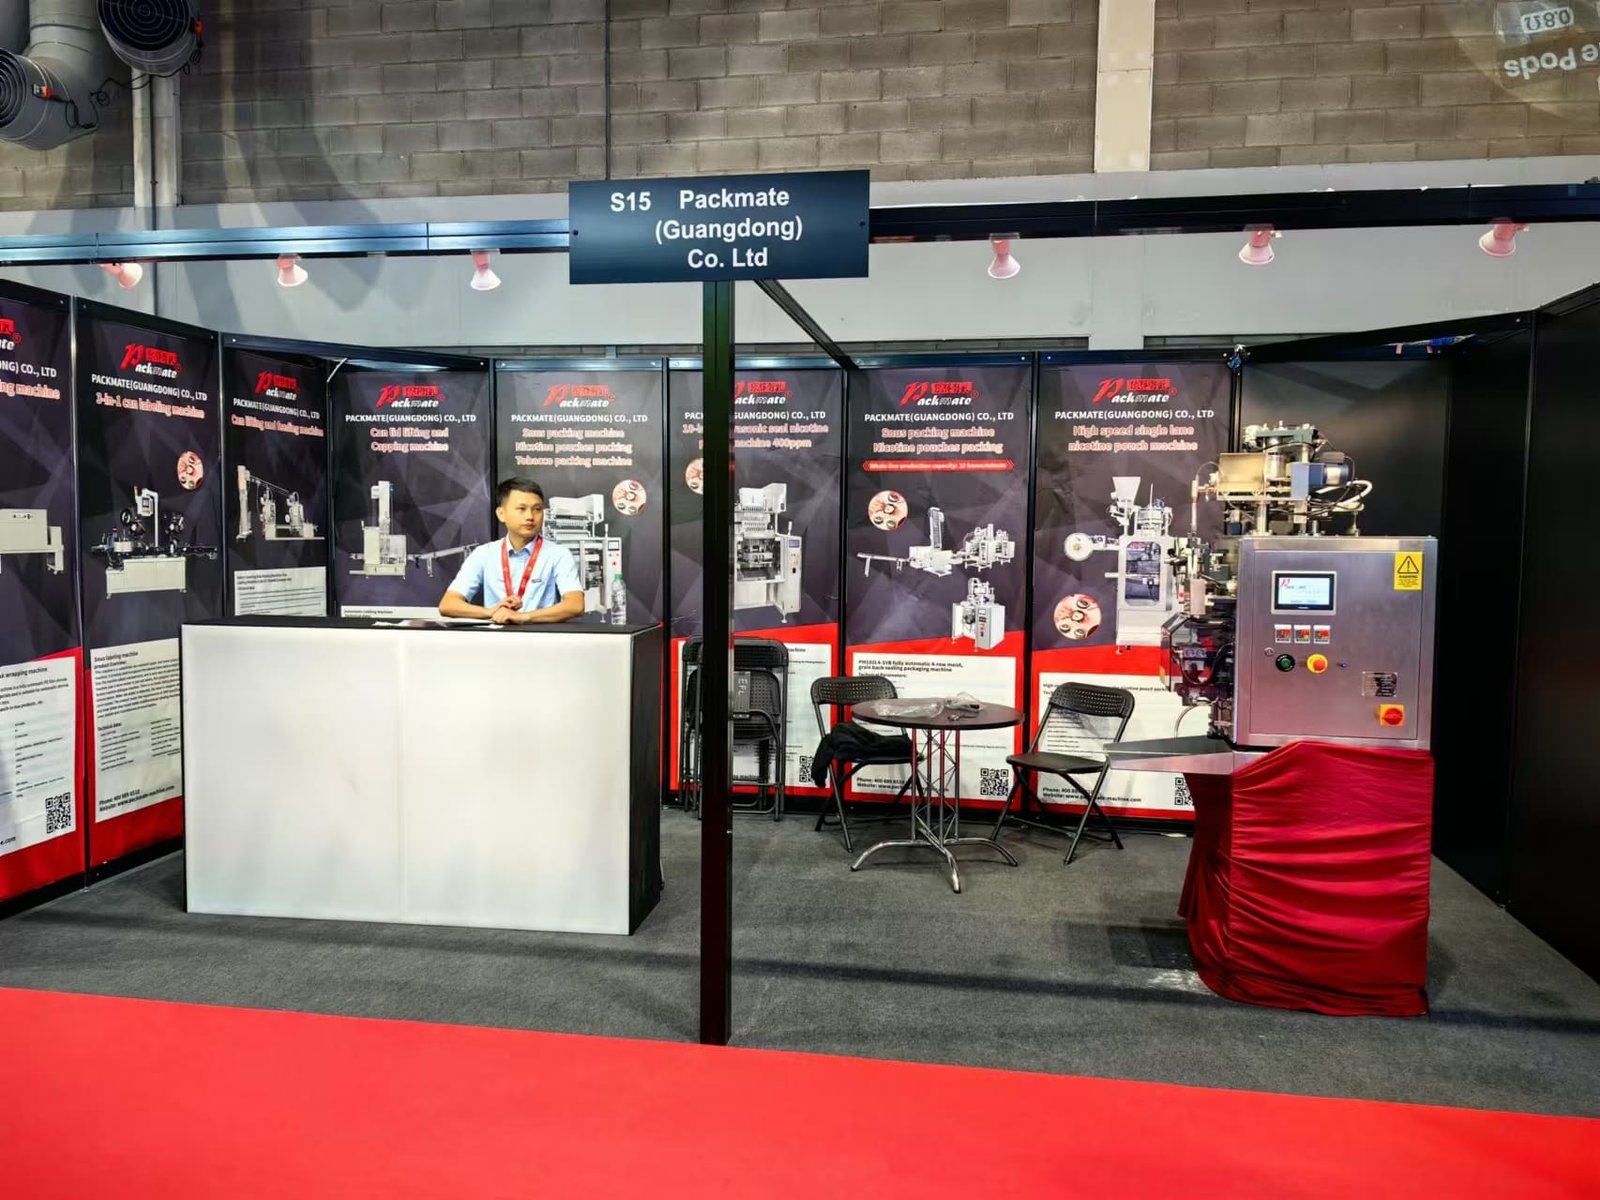
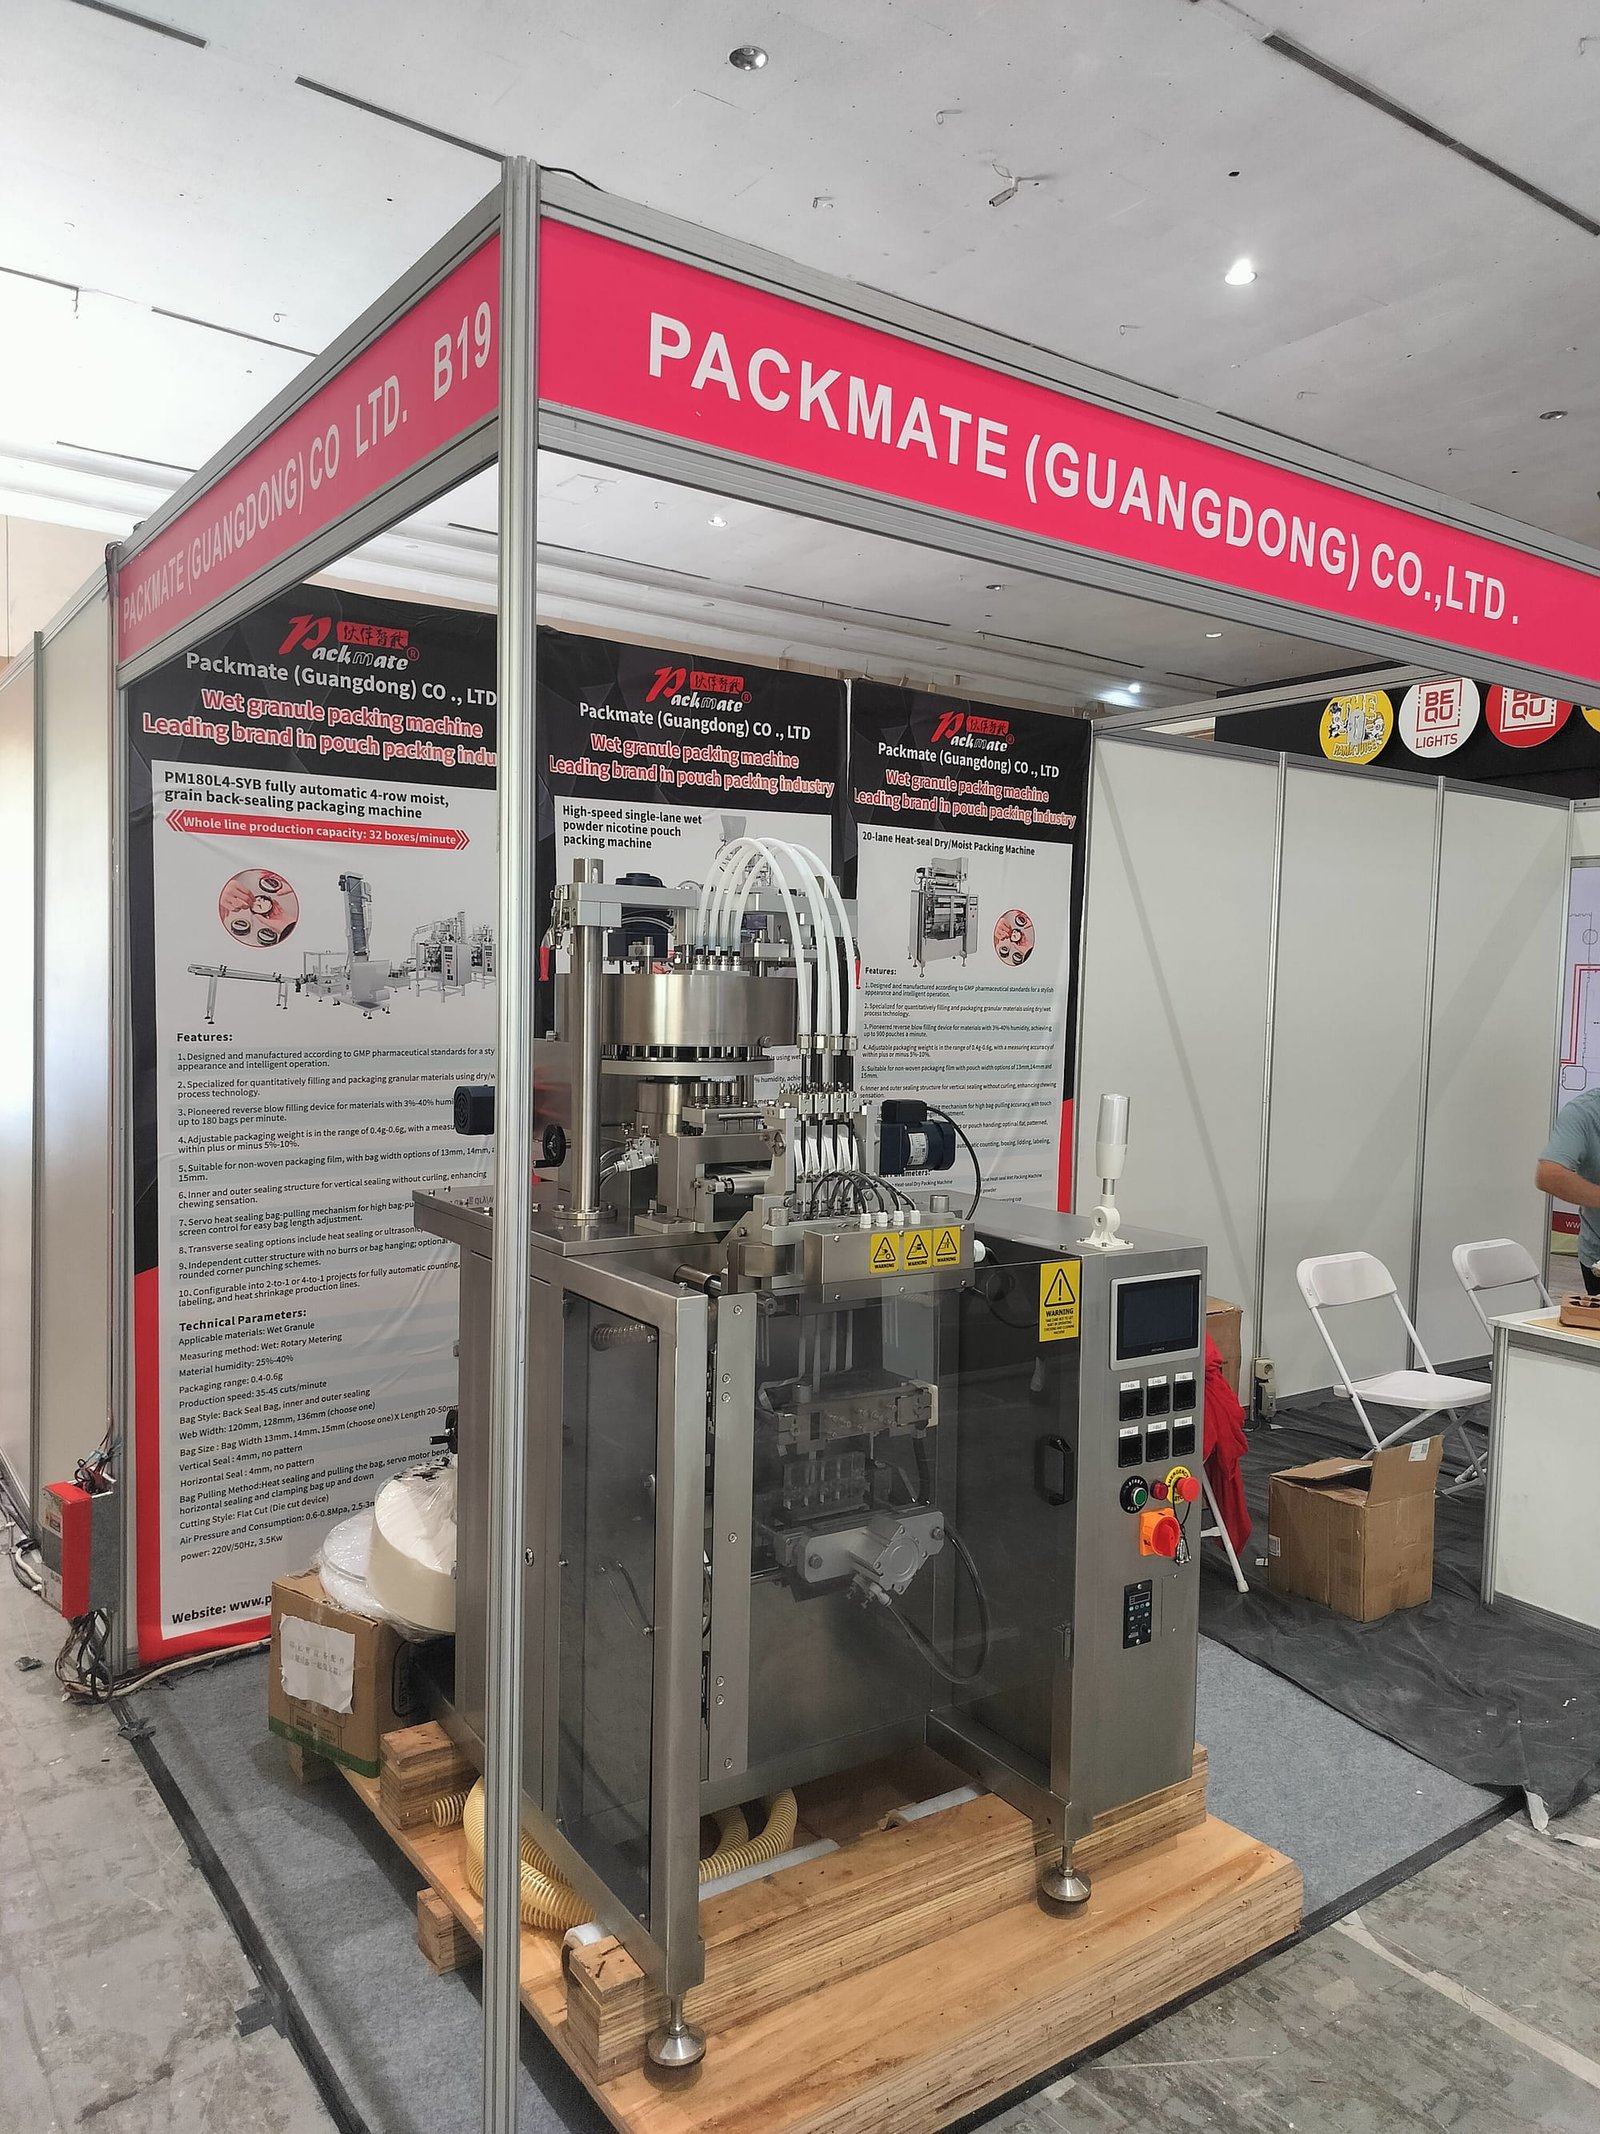
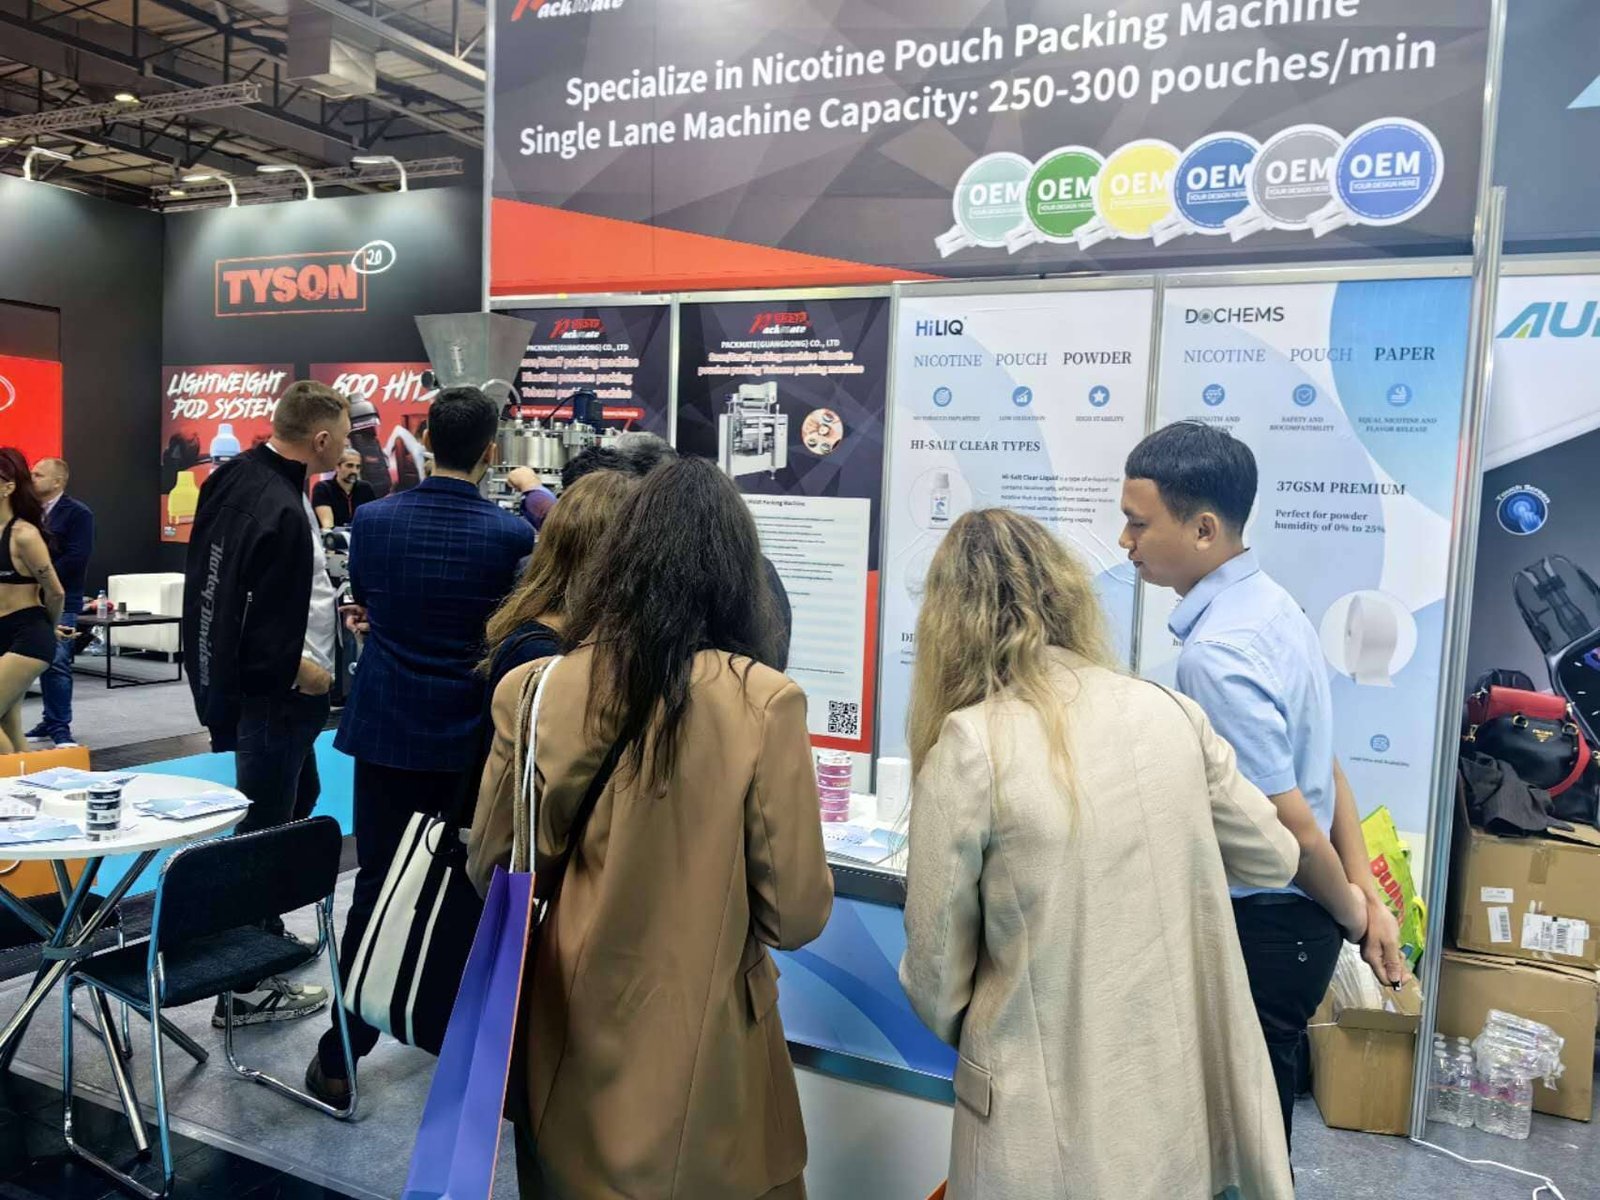
Global Presence Across International Expos
Meeting partners and showcasing high-performance food packaging technology around the world.
Frequently Asked Questions: Food Vacuum Packaging
Get technical answers to common queries regarding vacuum levels, modified atmosphere packaging integration, film selections, and line maintenance.
What vacuum level is required for commercial food preservation?
For fresh meat, seafood, and dairy, commercial standards require residual oxygen levels below 0.5% and chamber pressure under 10 mbar. Ludyway heavy-duty vacuum machines achieve ultimate vacuum levels down to 1 to 2 mbar, virtually eliminating aerobic microbial activity.
How does Modified Atmosphere Packaging (MAP) differ from pure vacuum sealing?
While standard vacuum draws all air out, creating a skin-tight envelope, MAP introduces a customized gas blend (typically Nitrogen N2, Carbon Dioxide CO2, and Oxygen O2) after vacuum evacuation. This prevents fragile foods (like chips or fresh berries) from crushing while still preventing bacterial spoilage.
What film materials are compatible with Ludyway vacuum equipment?
Our equipment seals all major commercial barrier films including PA/PE (Nylon/Polyethylene), PET/AL/PE (Aluminum foil laminates), EVOH high-barrier coextrusions, and eco-friendly recyclable barrier materials with reliable heat sealing profiles.
Can your machines handle food products containing liquids or oils?
Yes. We incorporate liquid-stop filters, inclined chamber deck inserts, and digital boiling-point detection algorithms that prevent liquid boil-over during rapid chamber depressurization, ensuring clean, leak-proof seal areas.
What routine maintenance is required for long-term machine life?
Key maintenance tasks include periodic vacuum pump oil changes (every 500 operating hours), daily inspection of silicone sealing gaskets, cleaning of heating wire PTFE tapes, and checking pneumatic air filters for moisture accumulation.
How does Ludyway support global installation and technical service?
We provide complete turnkey support: on-site installation, plant operator training, 24/7 remote diagnostic assistance via PLC cloud modules, and express courier dispatch of original spare parts worldwide.
Ready to Upgrade Your Food Packaging Efficiency?
Connect with our senior engineering team today for technical line audits, custom vacuum chamber blueprints, and turnkey production pricing tailored to your factory capacity.