In the modern food industry, extending shelf life while preserving freshness, flavor, and nutritional value is a constant challenge. A small vacuum packaging machine offers an efficient, cost-effective solution for businesses of all sizes. Whether you run a small deli, a gourmet coffee roastery, or a growing meal-prep operation, investing in the right equipment can transform your workflow and product quality.
What Makes a Small Vacuum Packaging Machine Essential?
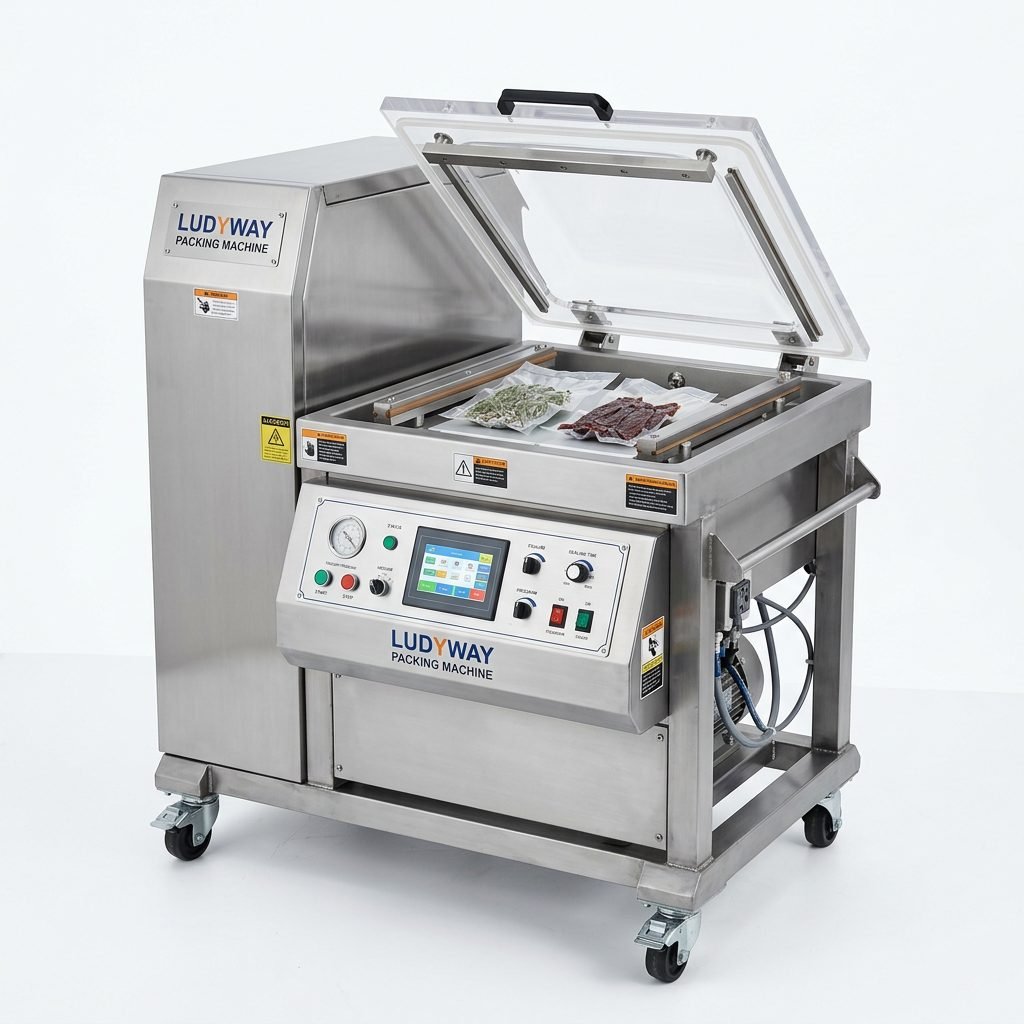
Vacuum packaging removes oxygen from the package before sealing, drastically slowing down the oxidation process that causes food to spoil. For small to medium-sized enterprises, a compact vacuum sealer is not just a luxury—it’s a strategic investment. It reduces food waste, enhances hygiene, and allows for precise portion control. Unlike massive industrial lines, a small vacuum packaging machine fits seamlessly into limited spaces without compromising on performance.
Key Features to Look For in a Compact Vacuum Sealer
Not all vacuum machines are created equal. When selecting a model for your business, consider the following critical features that directly impact efficiency and reliability.
- Consistent Sealing Power: Look for machines with robust heating elements that ensure airtight seals even under continuous operation.
- Adjustable Vacuum Pressure: Delicate items like berries or pastries require gentle suction, while dense meats need high vacuum levels.
- Stainless Steel Construction: Food-grade stainless steel chambers are essential for hygiene, durability, and easy cleaning.
- Digital Control Panel: Precise microprocessor controls allow operators to save presets, reducing human error and standardizing output.
- Versatile Bag Compatibility: A quality machine should handle various bag sizes and textures, from flat pouches to embossed vacuum bags.
Comparing Chamber vs. External Vacuum Sealers
Understanding the difference between chamber vacuum sealers and external suction models is crucial for making the right choice. The table below breaks down the distinctions based on common business needs.
| Feature | Chamber Vacuum Machine | External Suction Machine |
|---|---|---|
| Seal Quality | Excellent, high consistency | Good, but may vary with bag type |
| Liquid Packaging | Handles liquids and marinated items easily | Struggles with liquids, often requiring special bags |
| Duty Cycle | Designed for continuous professional use | Best for intermittent, lighter workloads |
| Maintenance | Low maintenance with durable pump systems | Higher wear on sealing gaskets and heat strips |
| Footprint | Moderate, but available in compact designs | Very small, easily portable |
Why Chamber Machines Lead in Professional Kitchens
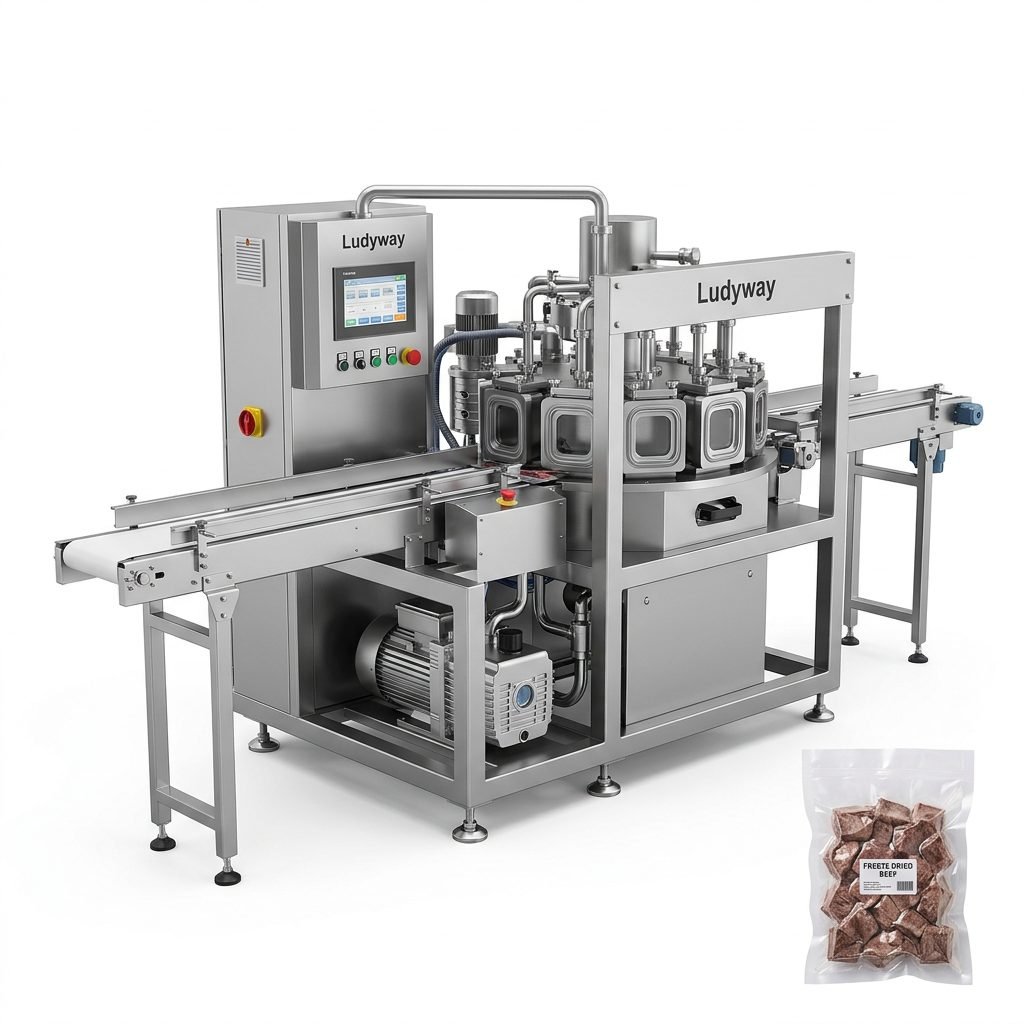
For efficiency-driven food packaging, chamber systems are the gold standard. They evacuate air from the entire chamber, meaning the pressure inside and outside the bag equalizes, preventing crushing and ensuring a perfect seal every time.
Optimizing Workflow with Automated Vacuum Systems
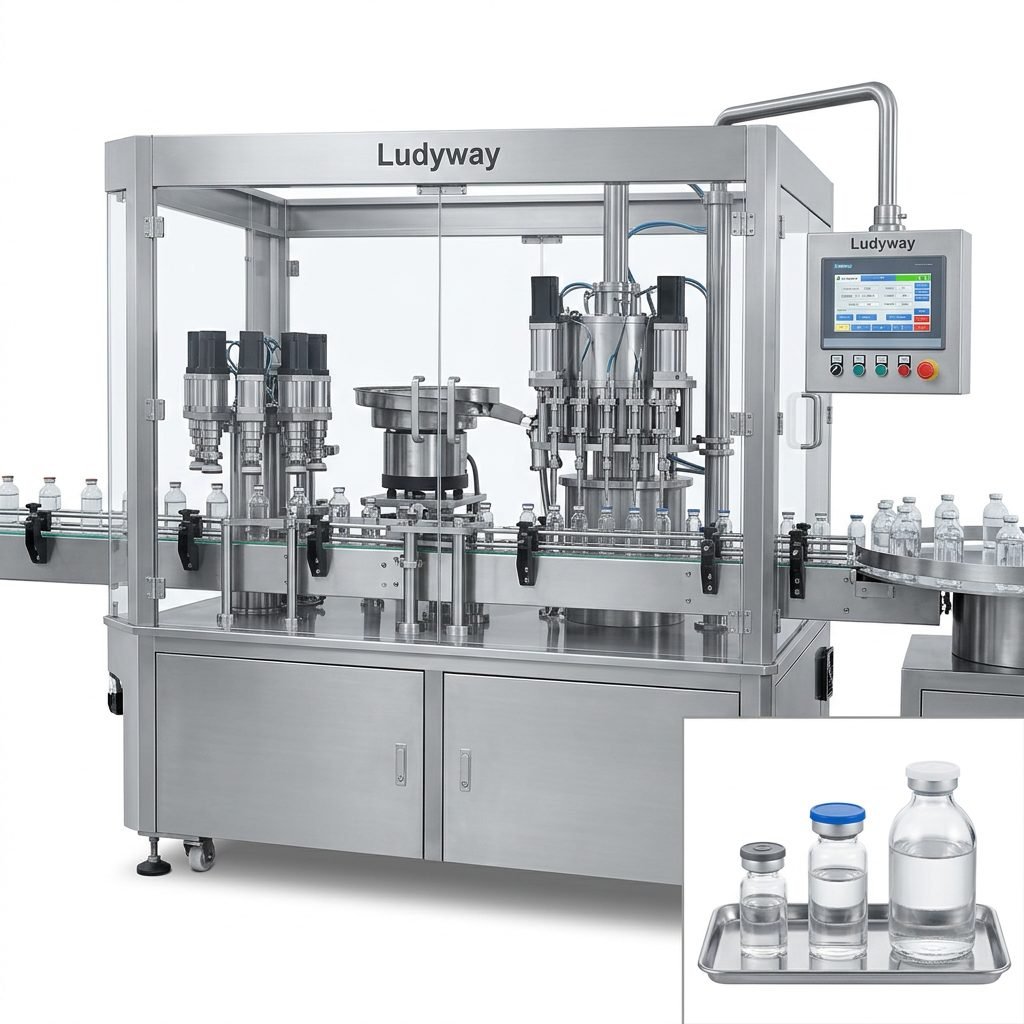
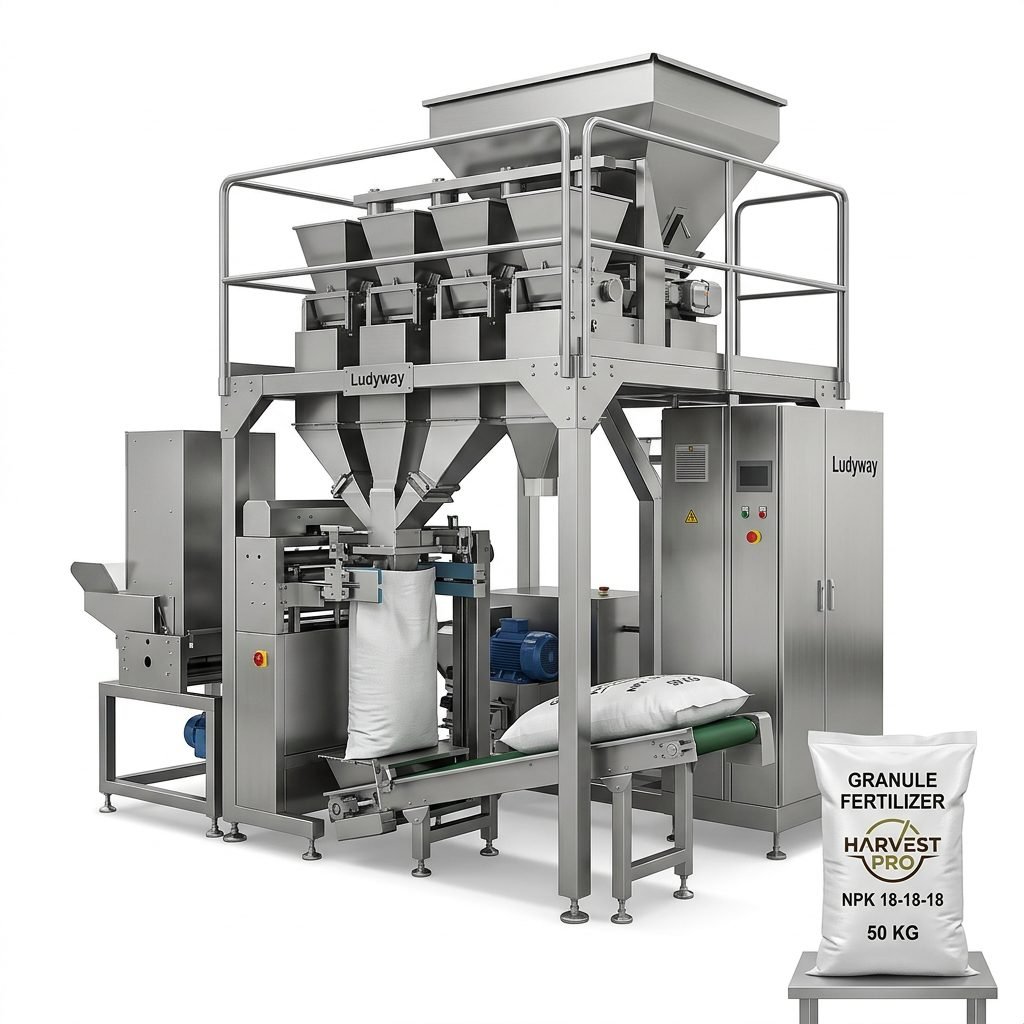
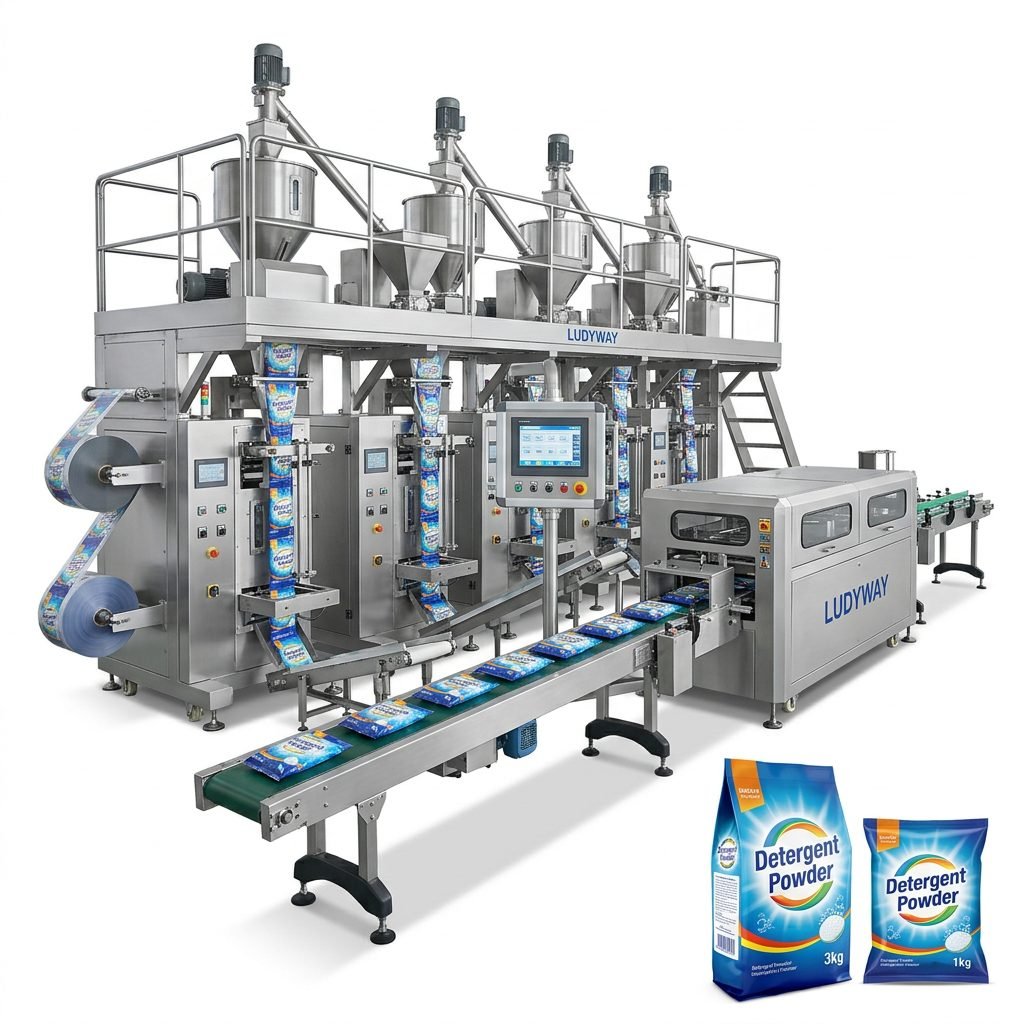
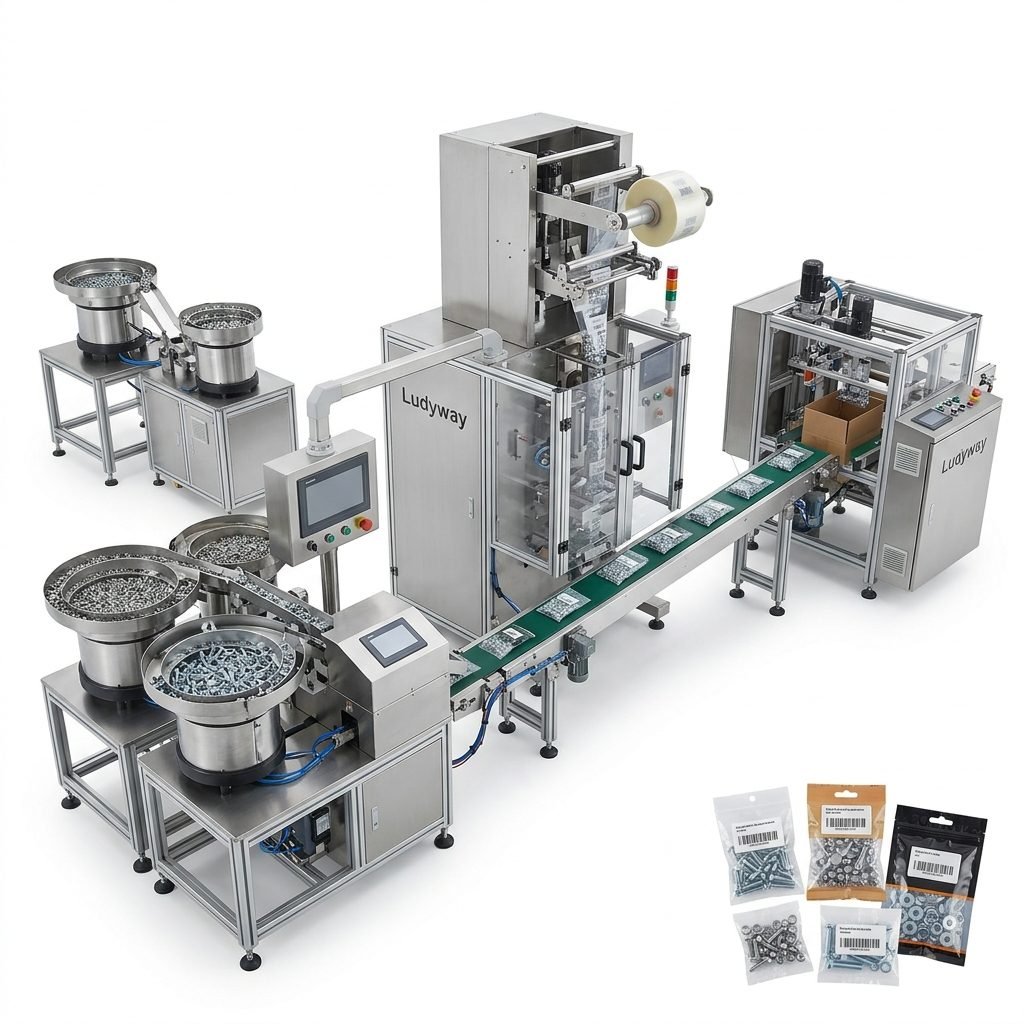
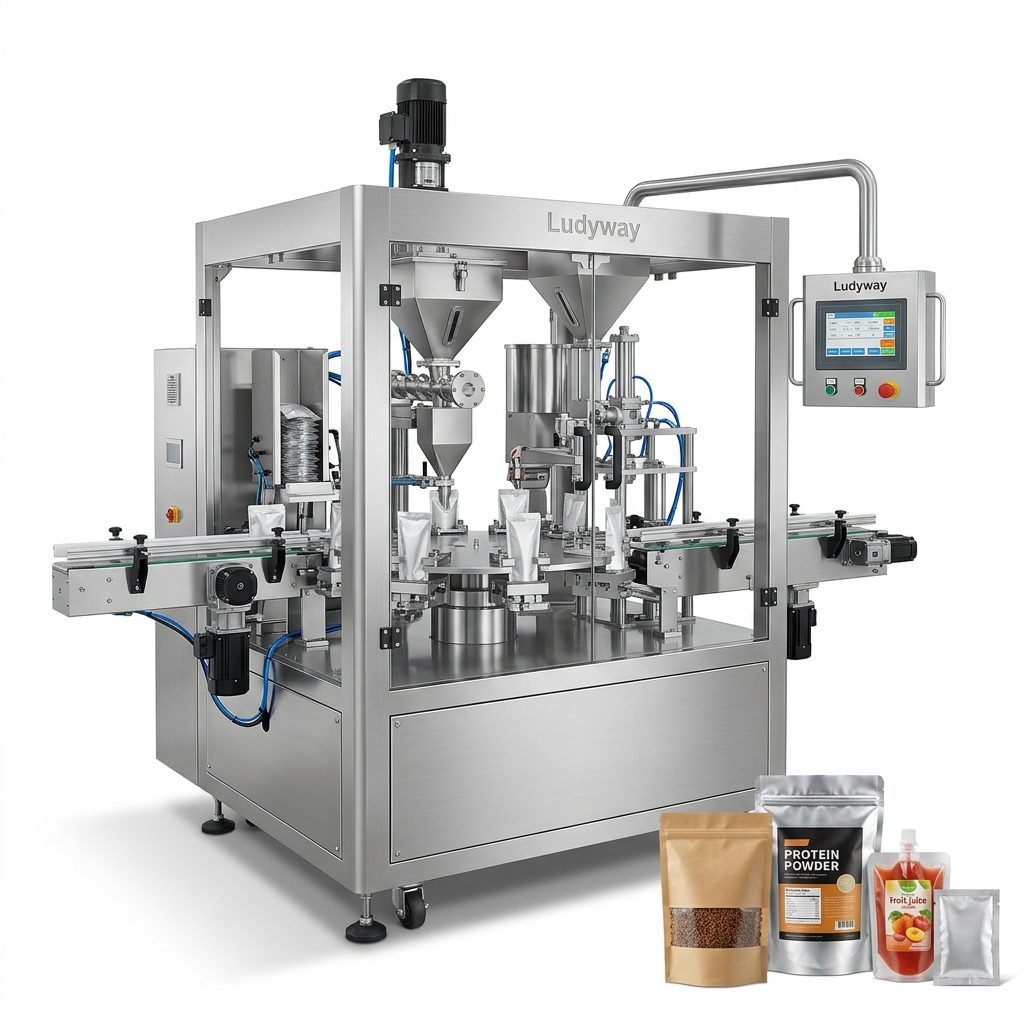
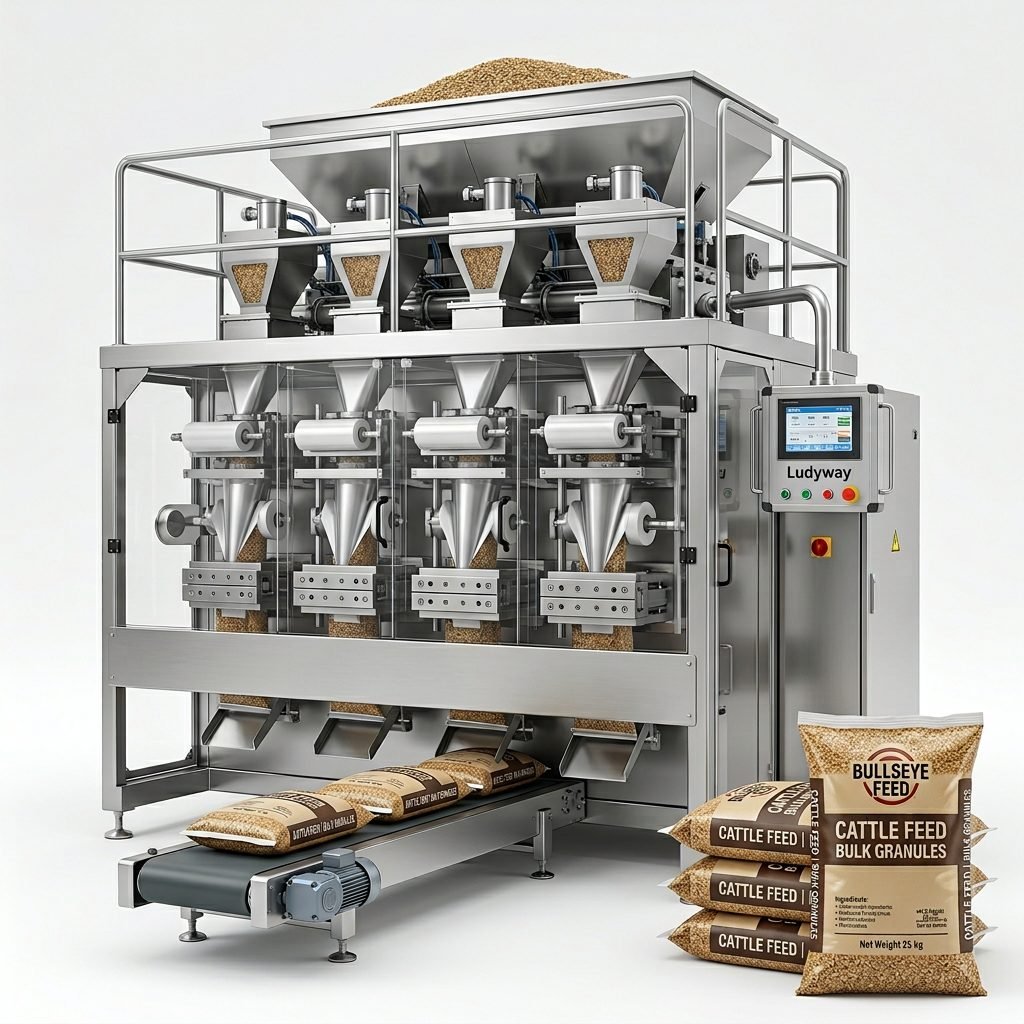
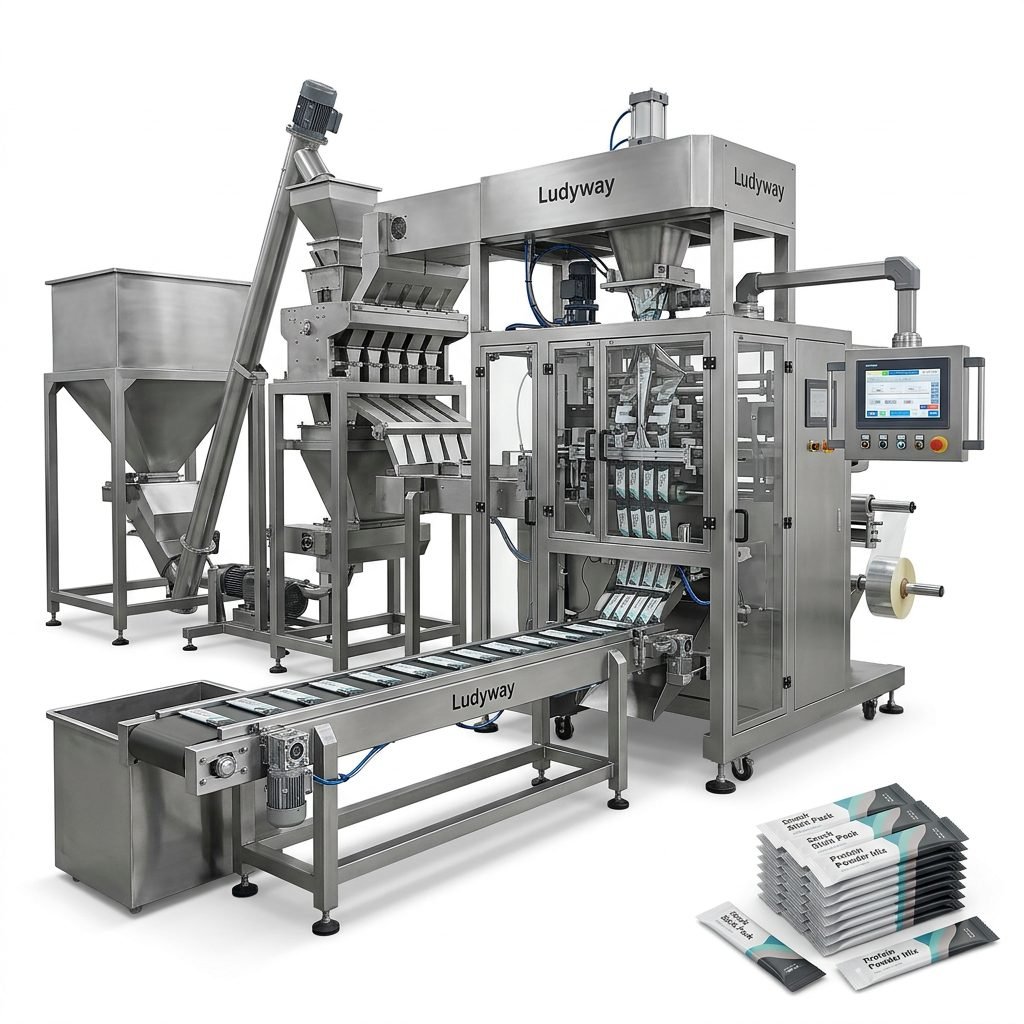
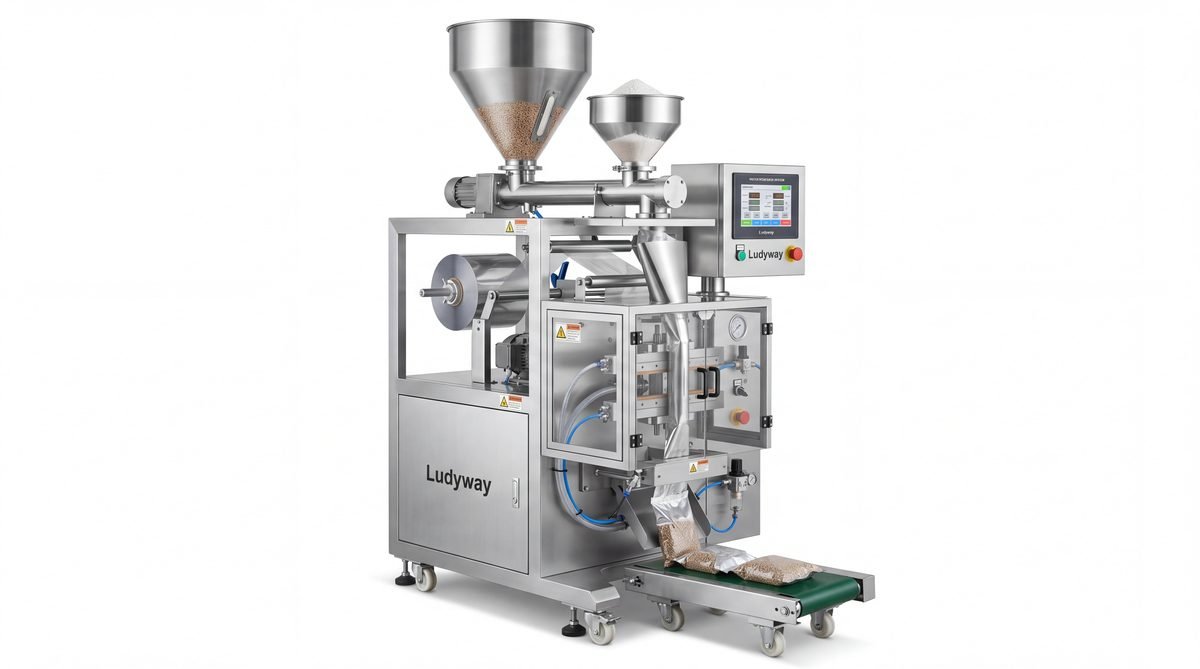
Modern small vacuum packaging machines are designed to integrate into broader automated packaging lines. By combining vacuum sealing with weighing, labeling, and cartoning systems, producers can achieve remarkable throughput. This is particularly relevant for manufacturers dealing with granules, powders, and liquids who require precise portioning before sealing.
Application Scenarios: From Coffee to Medical Supplies
The versatility of a compact vacuum machine extends far beyond basic food storage. Here are several sectors where this technology proves indispensable:
- Coffee Roasters: Preserving volatile aromatic compounds in freshly roasted beans or ground coffee requires immediate oxygen removal. A coffee packaging machine with a nitrogen flush option keeps the product fresh for months.
- Meat and Seafood: Preventing freezer burn and extending the cold chain are critical. Vacuum packaging inhibits bacterial growth and maintains texture.
- Pharmaceuticals and Nutraceuticals: From probiotic powders to sensitive medical devices, vacuum sealing protects against moisture and contamination.
- Pet Food Producers: Maintaining the freshness of high-value pet treats and supplements without artificial preservatives is a major market trend.
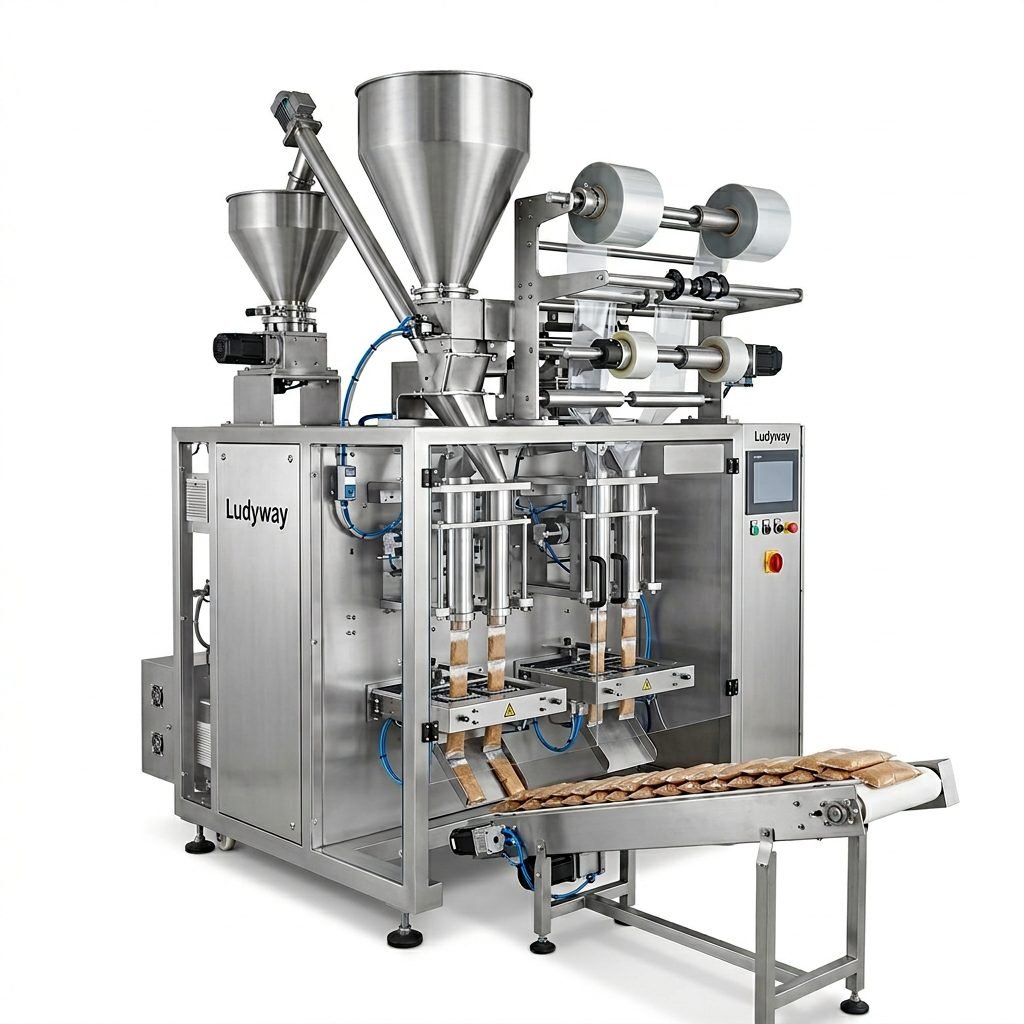
Integrating Multi-Lane and Stick Pack Systems
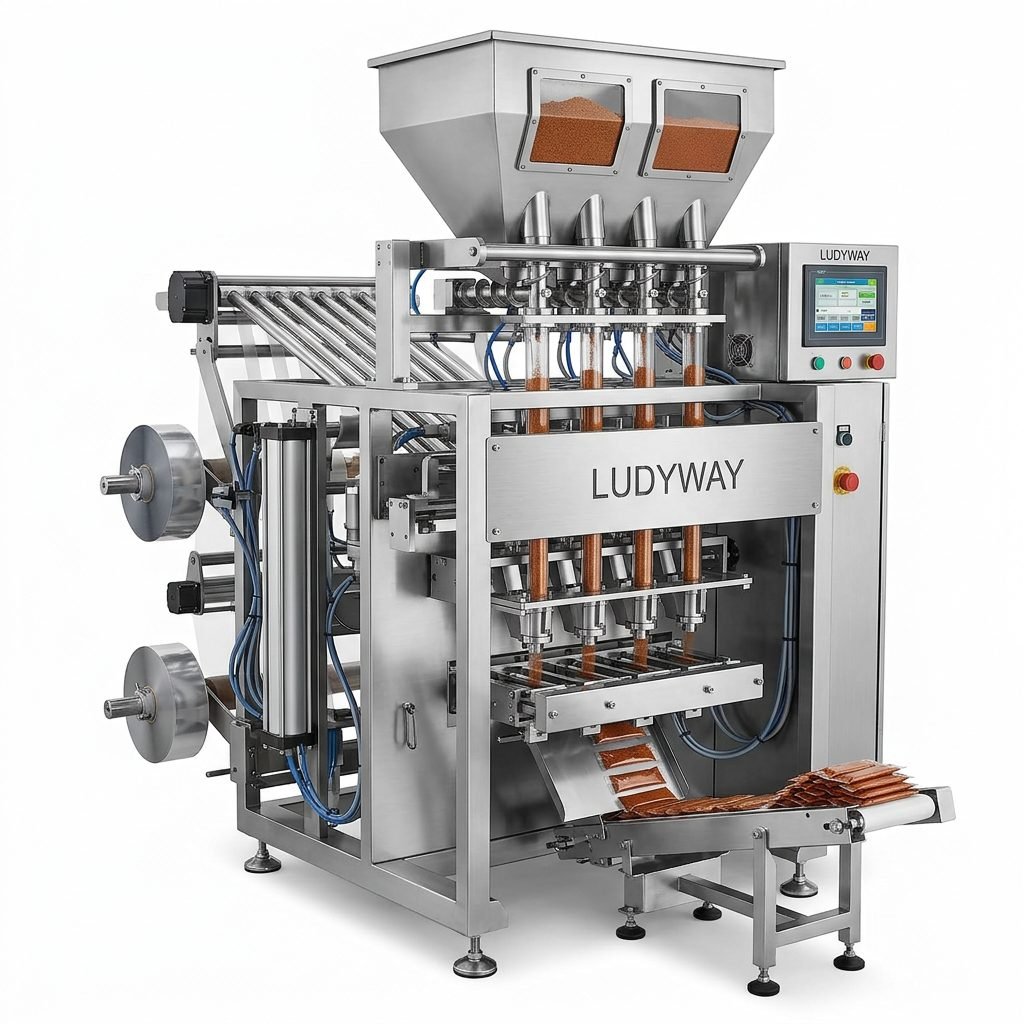
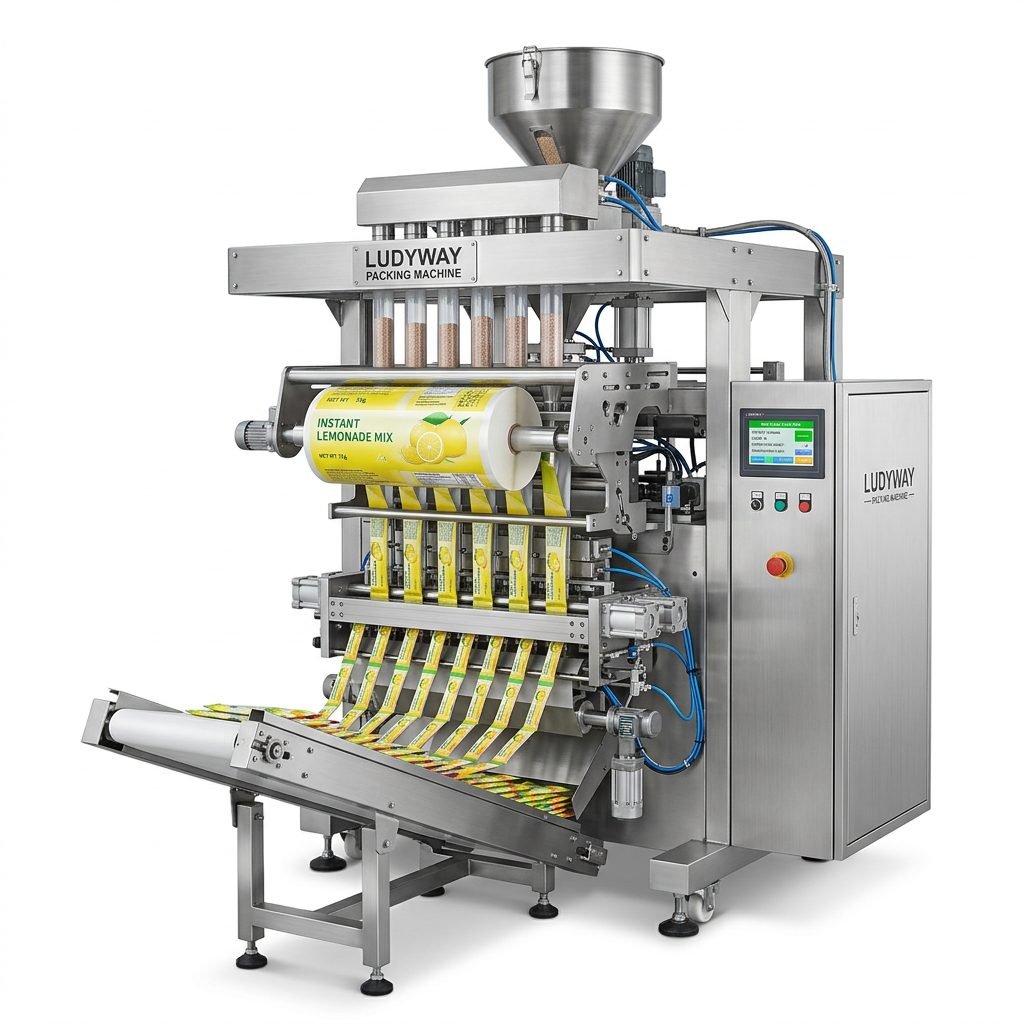
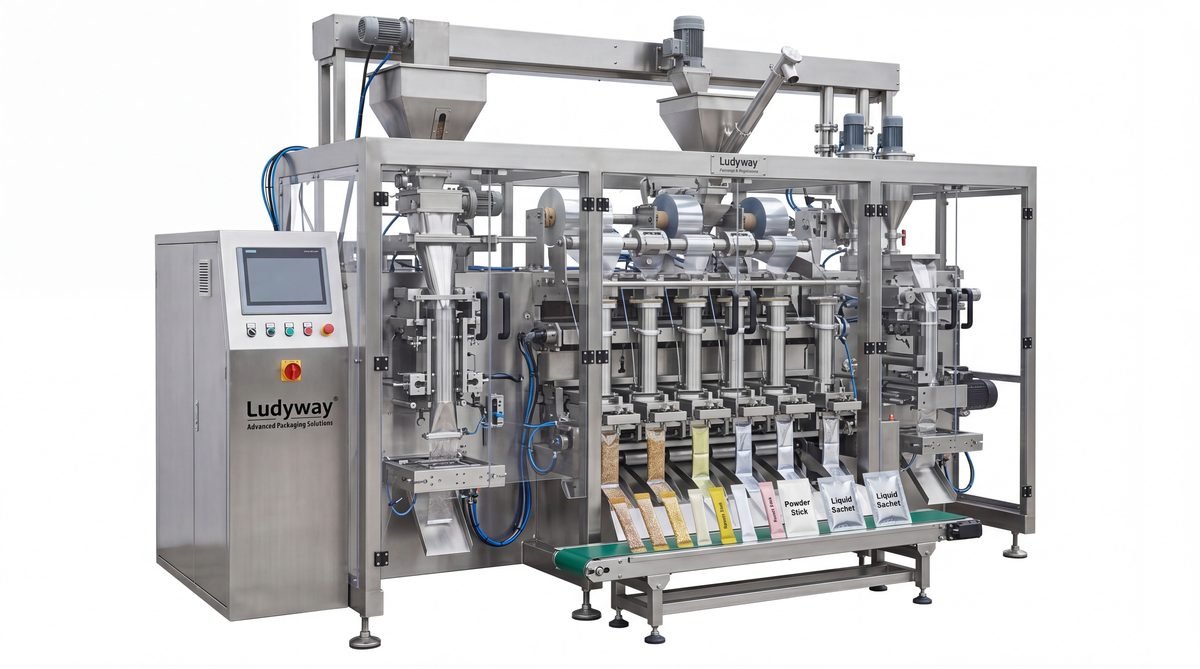
For businesses scaling up production, pairing vacuum capabilities with multi-lane stick pack or sachet machinery is a logical next step. This combination allows for high-speed packaging of single-serve portions while ensuring each unit is hermetically sealed for maximum shelf life. Leading equipment manufacturers now offer fully integrated turnkey packaging solutions that handle everything from filling to case packing.
Technical Specifications That Impact Performance
When evaluating a machine, look beyond marketing claims and examine the technical details. A high-efficiency vacuum pump with a flow rate of at least 20 m³/h is recommended for professional use. The chamber dimensions should accommodate your largest product, and the sealing bar length determines how many smaller packages you can process simultaneously.
Another critical factor is the duty cycle. A machine built for industrial applications should operate reliably for hours without overheating. This is where the engineering expertise behind brands like Ludyway becomes apparent. Ludyway is a major packaging machine manufacturer with over 30 years of industry experience, offering more than 50 intelligent models from a modern 20,000㎡ facility. Their systems are designed for continuous, high-performance operation across food, pharmaceutical, and health industries.
Common Mistakes to Avoid When Vacuum Packaging
Even the best equipment will underperform if used incorrectly. Avoid these frequent pitfalls:
- Overfilling Bags: Always leave at least 2-3 inches of headspace above the product for a clean seal. Product residue in the sealing area will cause leaks.
- Ignoring Maintenance: Vacuum pumps require regular oil changes (for oil-based systems) and filter replacements. A neglected pump loses suction power rapidly.
- Using Incorrect Film: Not all films are created equal. For long-term storage, use high-barrier films with low oxygen transmission rates.
- Skipping Cool-Down Cycles: Sealing bars need time to cool between cycles. Overworking the bar can damage heating elements and compromise seal integrity.
Return on Investment: Calculating Efficiency Gains
Switching to a dedicated small vacuum packaging machine delivers measurable ROI. Reduced product spoilage alone often justifies the capital outlay within 6 to 12 months. Added benefits include extended market reach through longer shelf life, reduced preservative use (appealing to clean-label consumers), and the ability to sell pre-portioned, value-added products at premium price points.
A turnkey packaging line that integrates vacuum sealing can further reduce labor costs by automating repetitive tasks. For businesses handling diverse product categories—from freeze-dried fruits to liquid seasonings—configurable systems offer the flexibility to switch between applications with minimal downtime.
Sustainability and Waste Reduction
Vacuum packaging also supports sustainability goals. By extending product freshness, it directly fights food waste. Many modern film materials are now recyclable or made from renewable sources, aligning with evolving regulatory standards and consumer demand for eco-friendly packaging.
Choosing a Partner for Long-Term Success
The quality of the machine is only part of the equation. Reliable after-sales support, spare parts availability, and technical consultation are essential for minimizing downtime. Look for companies that possess ISO certifications, a global service network, and a documented track record in your specific industry. A partner that understands packaging industry standards and participates in international exhibitions signals long-term stability and innovation commitment.
Conclusion: Invest in Reliable Vacuum Technology
A small vacuum packaging machine is more than a tool—it’s a gateway to improved product quality, operational efficiency, and business growth. Prioritize machines with robust construction, digital controls, and proven sealing performance. Whether you are packaging delicate powders, marinated meats, or premium coffee, the right vacuum system will safeguard your product’s integrity from production to consumption. For tailored guidance and advanced equipment, exploring comprehensive packaging lines from experienced manufacturers is the smartest next step toward achieving your production goals.