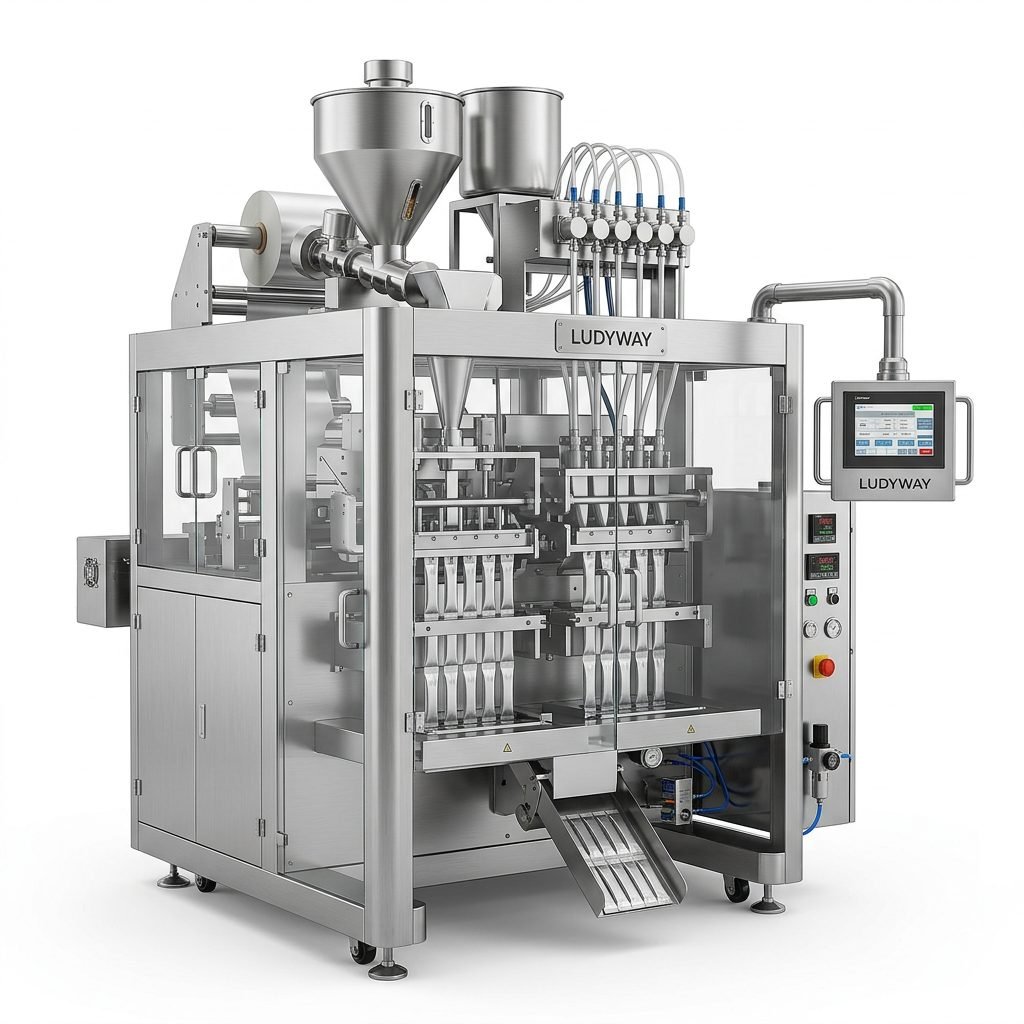
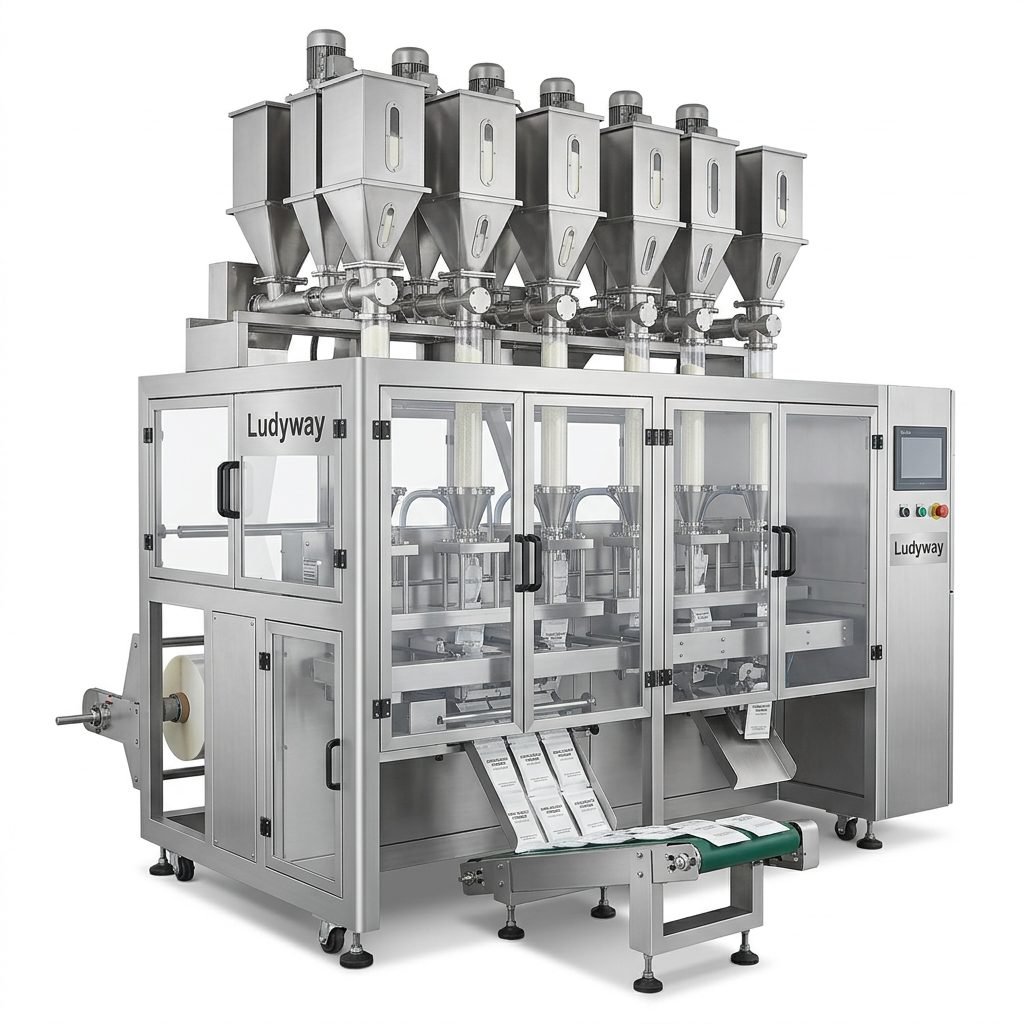
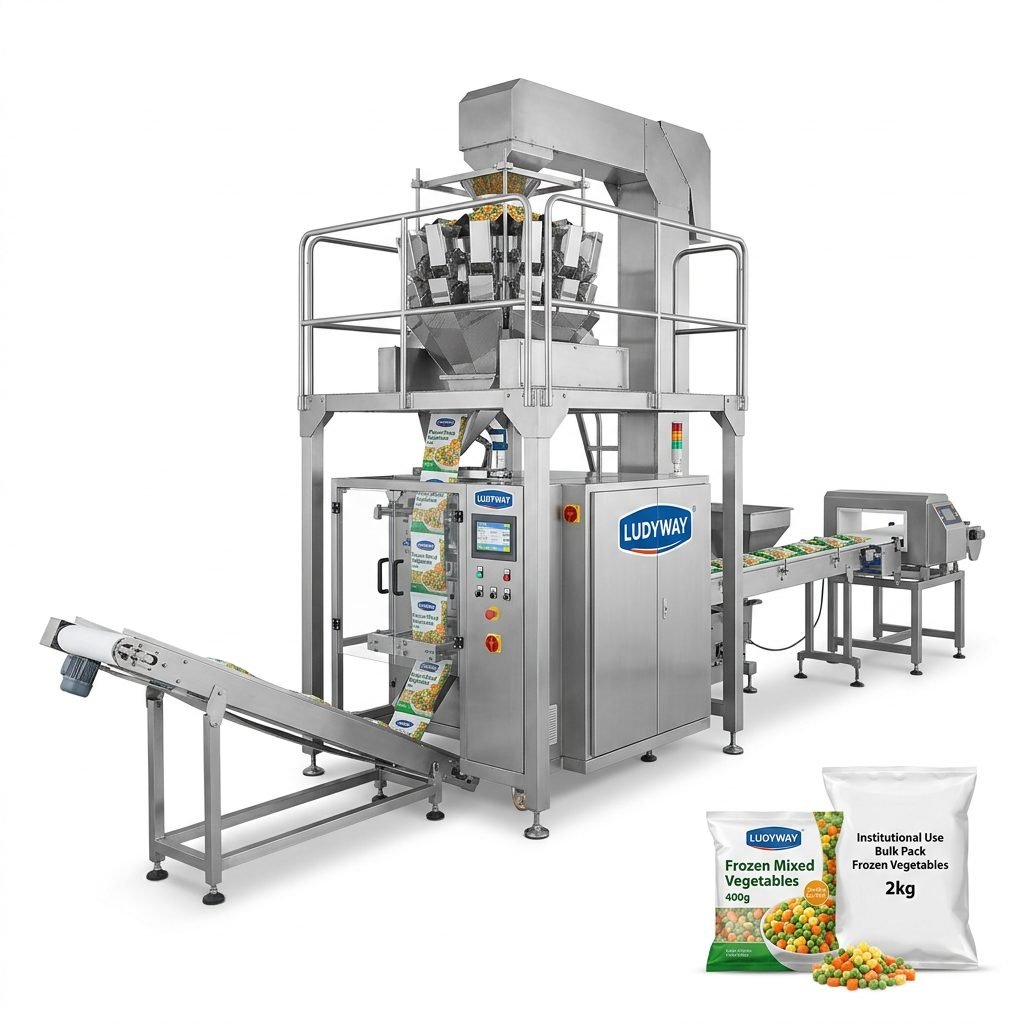
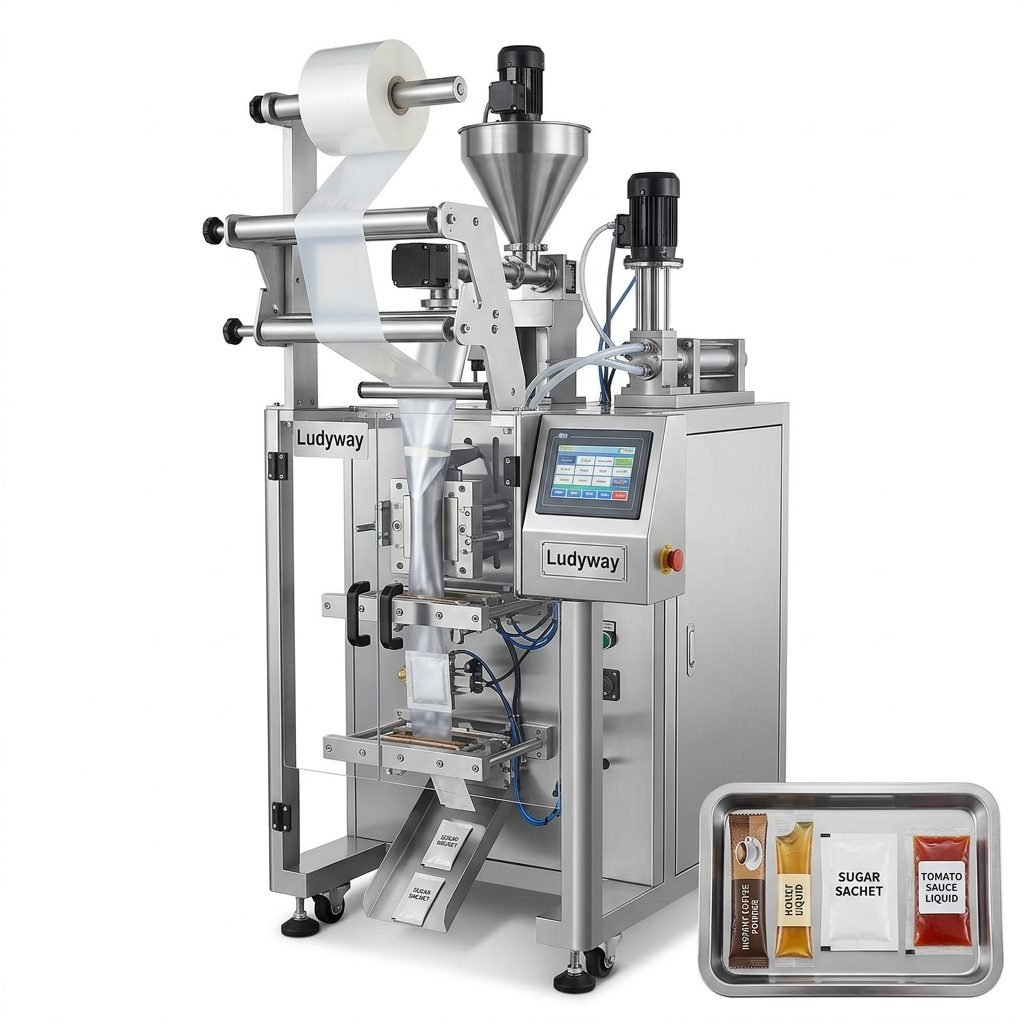
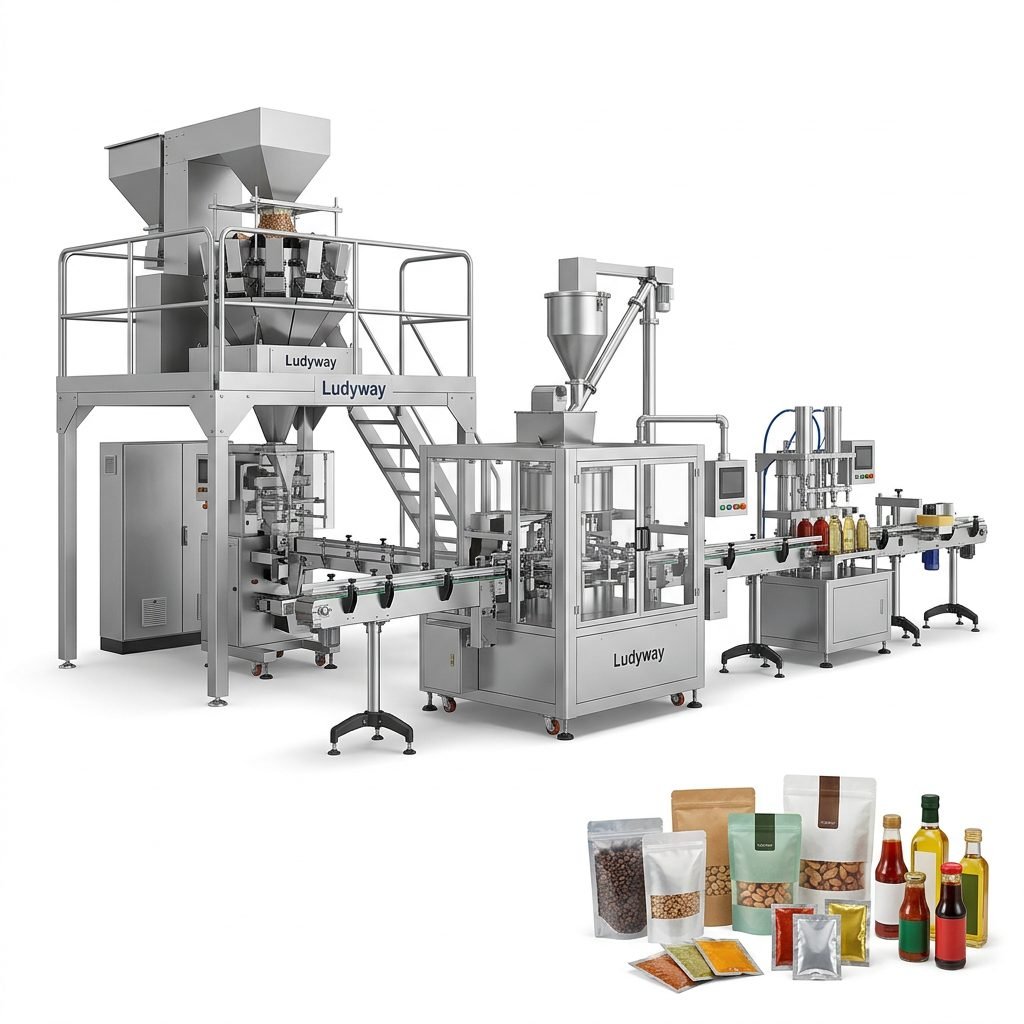
Investing in a vacuum packaging machine is a critical decision for manufacturers looking to extend product shelf life, maintain hygiene standards, and optimize packaging workflows. Whether you operate in the food, pharmaceutical, or industrial sector, selecting the right Sevana vacuum packaging machine requires a clear understanding of your production requirements, product characteristics, and long-term operational goals.
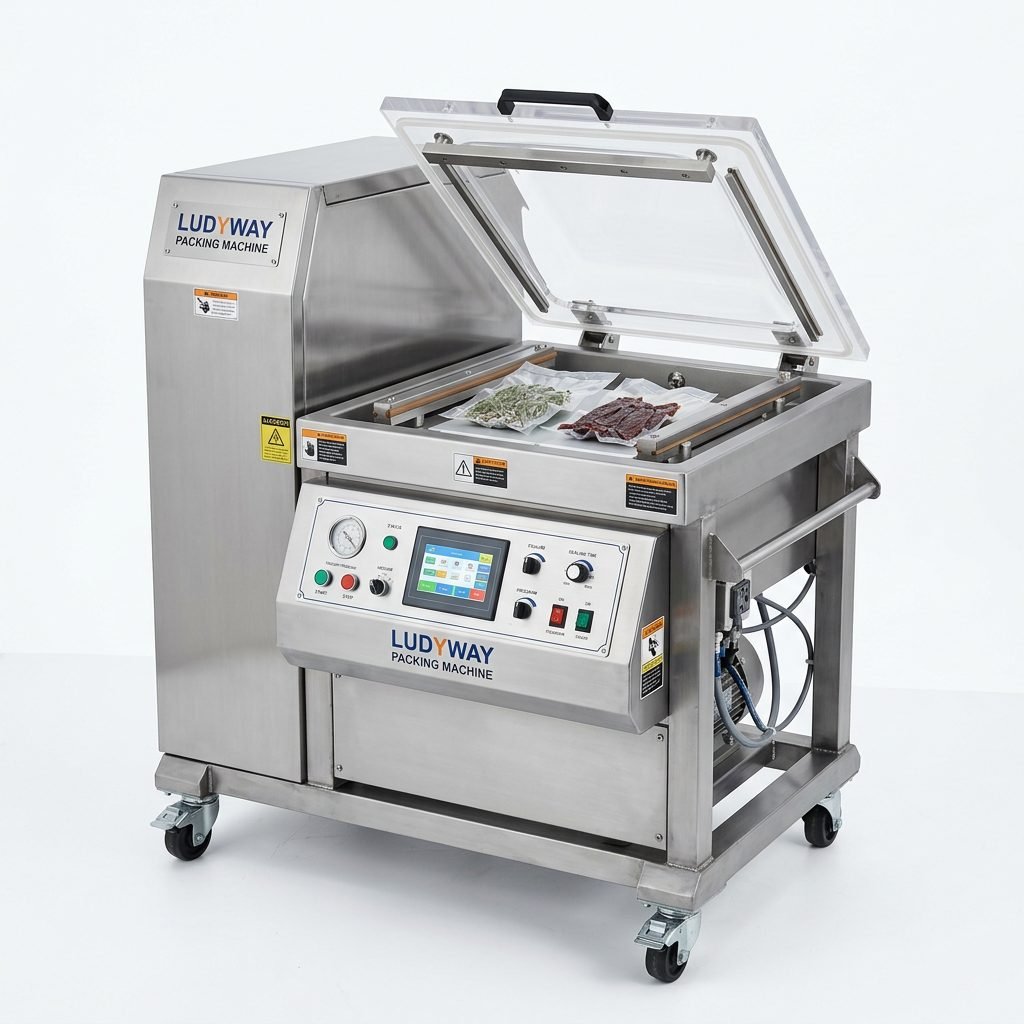
1. Understanding Vacuum Packaging Technology
Vacuum packaging removes air from the package prior to sealing, creating an oxygen-reduced environment that significantly slows product degradation. Modern vacuum packaging systems go beyond simple air extraction — they integrate gas flushing (MAP — Modified Atmosphere Packaging), precision sealing controls, and automated cycle management. When evaluating a Sevana vacuum packaging machine, look for models that offer adjustable vacuum levels, multiple sealing modes, and compatibility with various bag materials including laminated films, aluminum foil pouches, and high-barrier structures.
Key Vacuum Packaging Benefits
- Extended shelf life — reduces oxidation and microbial growth
- Product protection — prevents freezer burn, moisture loss, and contamination
- Improved logistics — compact packaging reduces storage and shipping costs
- Enhanced presentation — tight, professional packaging appearance
2. Types of Vacuum Packaging Machines
Not all vacuum packaging equipment serves the same purpose. The right machine type depends on your production volume, product format, and packaging material. Below is a comparison of the most common configurations available in the Sevana vacuum packaging machine range and similar industrial systems.
| Machine Type | Best For | Production Level | Key Advantage |
|---|---|---|---|
| Single Chamber | Small batches, solids | Low to medium | Precise control, versatile |
| Double Chamber | Medium batches, alternating cycles | Medium to high | Continuous operation capability |
| External / Nozzle Type | Liquids, powders, delicate items | Low to medium | No product compression |
| Belt / Conveyor System | High-volume production lines | High to very high | Automation-ready integration |
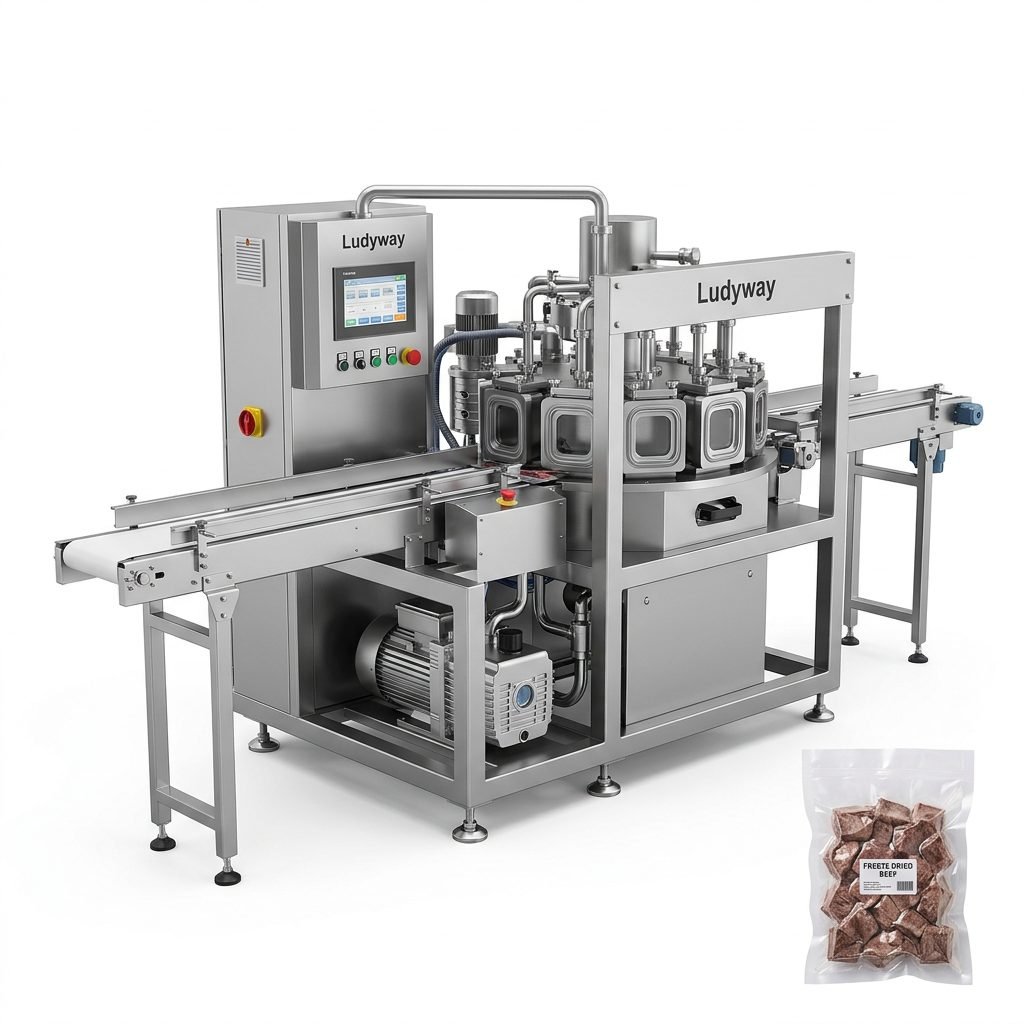
3. Critical Factors to Evaluate
Choosing a vacuum packaging machine involves more than comparing technical specifications. The following factors directly affect machine performance, operational efficiency, and return on investment.
3.1 Product Characteristics
The physical properties of your product — solid, granular, powder, or liquid — determine the appropriate vacuum chamber design and sealing configuration. Liquid products require external nozzle machines or inclined chamber designs to prevent spillage during air extraction. Powders benefit from machines with gentle vacuum ramp-up to avoid dust dispersion. Sharp or irregular solids may require reinforced bag materials and wider seal bars.
3.2 Production Speed and Cycle Time
Cycle time includes loading, vacuum draw, sealing, and unloading. For manufacturers scaling up operations, investing in a Sevana vacuum packaging machine with automated loading and conveyor feeding can substantially increase throughput. Belt-driven systems capable of 4-8 cycles per minute are commonly used in medium to high-volume packaging operations.
3.3 Seal Integrity and Consistency
Seal quality is the most critical performance indicator of any vacuum packaging system. Look for machines with independent temperature control zones on the seal bar, adjustable sealing time, and consistent pressure distribution. Double-seal configurations provide an extra layer of security for extended shelf-life applications, especially in FDA-regulated food packaging environments.
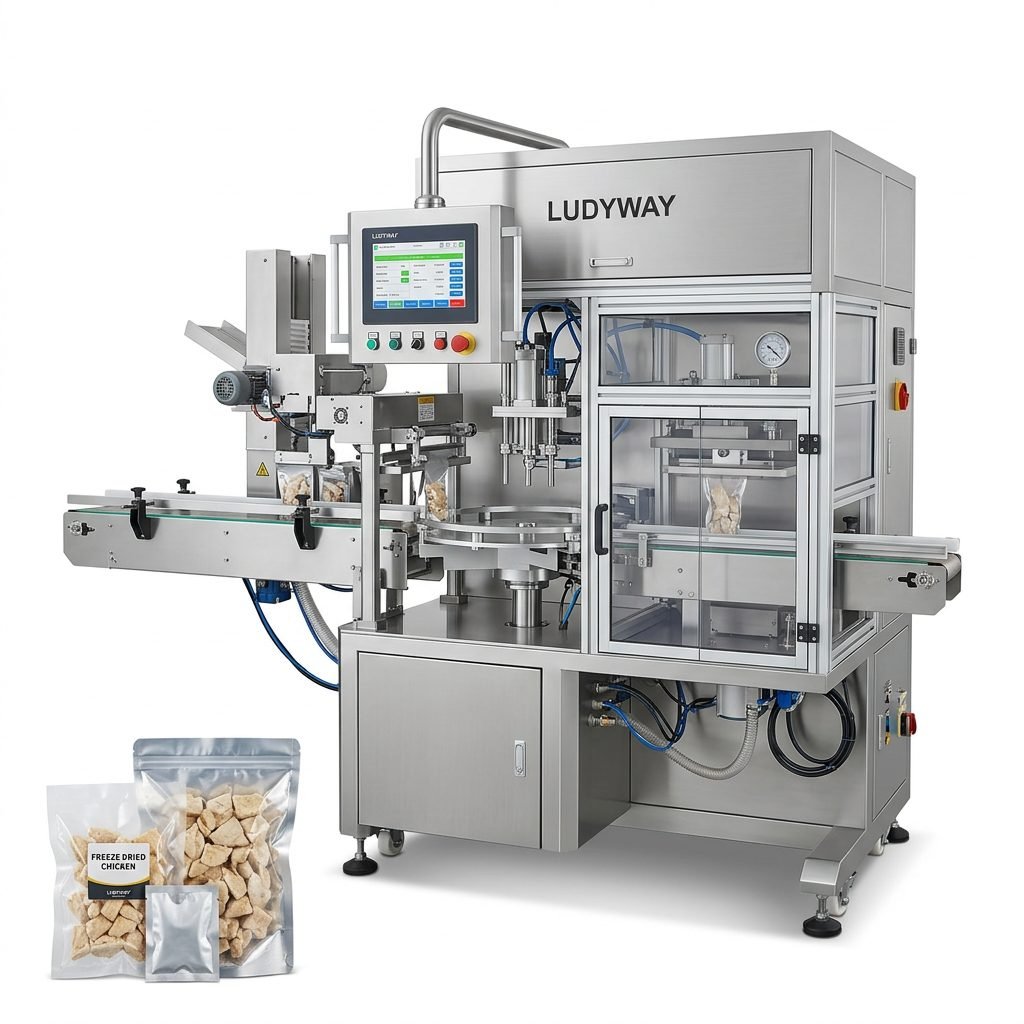
4. Material Compatibility and Flexibility
Modern packaging lines must accommodate diverse bag materials and formats. A well-designed vacuum packaging machine should handle polyethylene (PE), polyamide (PA), aluminum-laminated films, and high-barrier co-extruded materials. Check the maximum bag width and length specifications, as well as the machine’s ability to switch between different bag sizes with minimal changeover time. Some machines support both flat pouches and gusseted bags, offering greater packaging flexibility.
Bag Format Compatibility Checklist
- Flat vacuum pouches — standard sizes
- Gusseted bags — for bulk or irregular products
- Shrink bags — for tight product conformity
- Re-sealable zipper pouches — consumer convenience
- Pre-made pouches with spouts — liquid products
5. Automation and Integration Capabilities
For manufacturers moving toward Industry 4.0 and smart factory environments, vacuum packaging equipment should integrate seamlessly with upstream and downstream systems. Advanced Sevana vacuum packaging machine configurations support automated product feeding, weighing, labeling, coding, metal detection, and cartoning — all connected through centralized PLC control systems with HMI touchscreen interfaces. This integration reduces manual handling, minimizes errors, and provides real-time production data.
When planning a complete packaging line, consider how the vacuum sealing station will connect with industry-standard packaging line equipment, including checkweighers, X-ray inspection systems, and robotic palletizing cells.
6. Hygiene, Cleaning, and Maintenance
Hygienic design is non-negotiable for food and pharmaceutical applications. Key features to look for include:
- Stainless steel construction — SUS304 or SUS316L for corrosion resistance
- IP65 or higher-rated electrical enclosures — protection during washdown
- Tool-free disassembly — facilitates quick cleaning and product changeover
- Sloped surfaces and drainage — prevents liquid pooling
- Accessible vacuum pump and filter systems — simplifies routine maintenance
7. Vacuum Pump Technology
The vacuum pump is the heart of the system. Two primary pump types are used in industrial vacuum packaging:
| Pump Type | Vacuum Level | Maintenance | Typical Application |
|---|---|---|---|
| Oil-Lubricated Rotary Vane | High (below 1 mbar) | Regular oil changes | General industrial, solids |
| Dry Scroll / Claw Pump | Medium to high | Low maintenance | Food, pharma — contamination-sensitive |
Dry vacuum pumps are increasingly preferred in food and pharmaceutical settings because they eliminate oil-related contamination risks and comply with stricter ISO packaging standards for cleanroom and hygienic production environments.
8. Energy Efficiency and Operating Costs
Beyond the initial purchase price, factor in total cost of ownership (TCO) including energy consumption, consumables, maintenance schedules, and expected service life. Machines equipped with variable-speed drives and energy-efficient motors can reduce power usage by 20-30% compared to older fixed-speed designs. Additionally, consider spare parts availability and technical support responsiveness when selecting a vacuum packaging machine supplier for long-term partnerships.
9. Global Standards and Certifications
For manufacturers exporting to international markets, machine compliance with recognized standards is essential. A properly configured Sevana vacuum packaging machine should meet relevant requirements for:
- CE marking — European Economic Area compliance
- FDA food contact material regulations — for U.S. food packaging
- ISO 11607 — packaging for terminally sterilized medical devices
- GFSI-recognized hygienic design principles — food safety compliance
Always request documentation confirming machine certifications before procurement.
10. Evaluating Supplier Capabilities
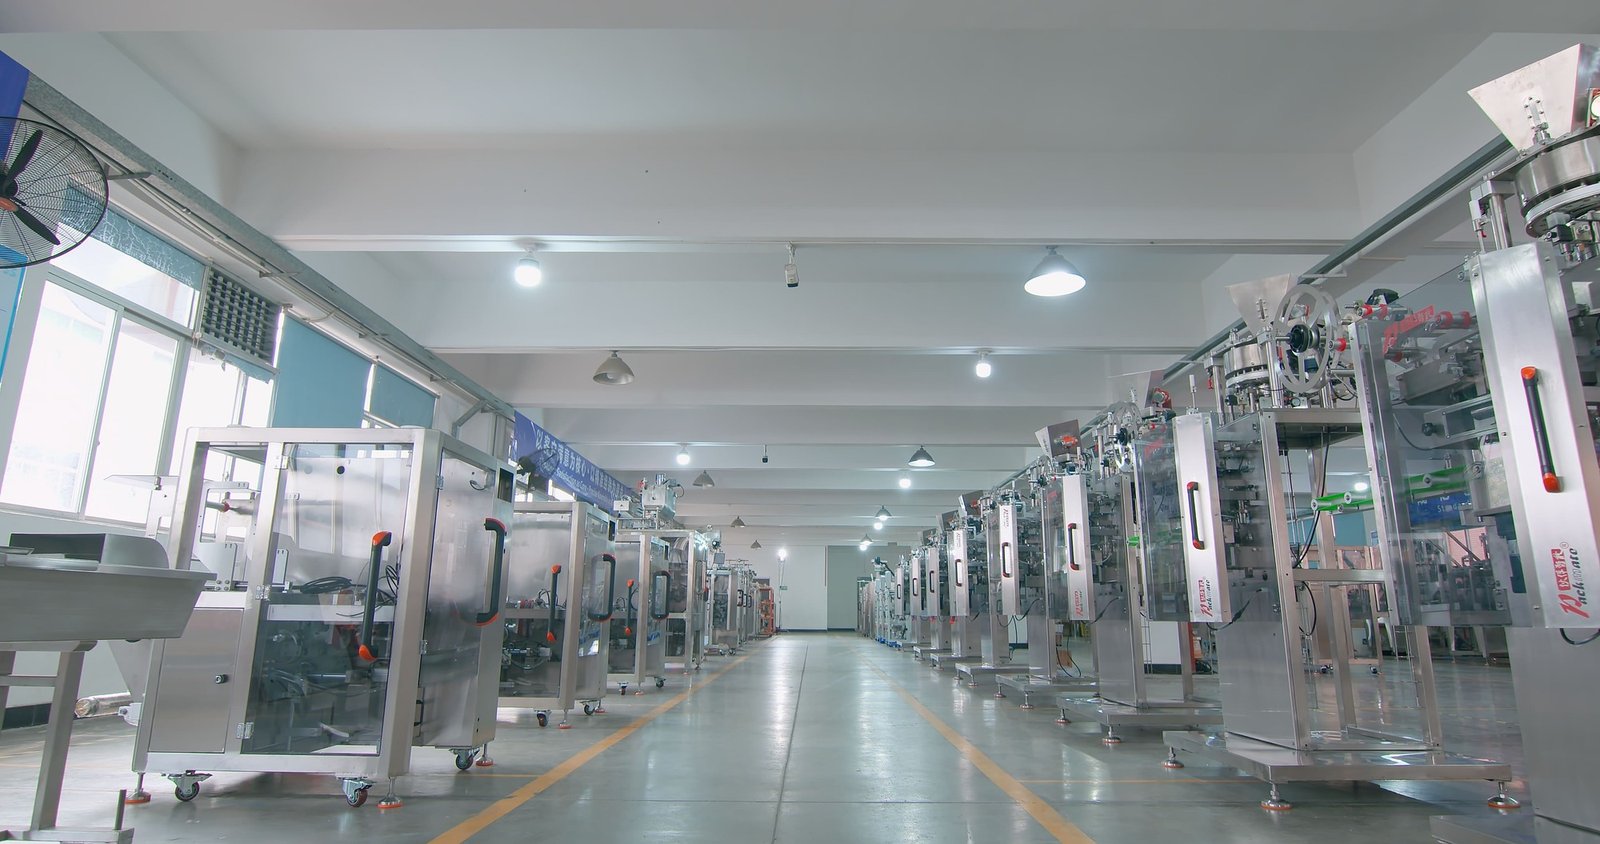
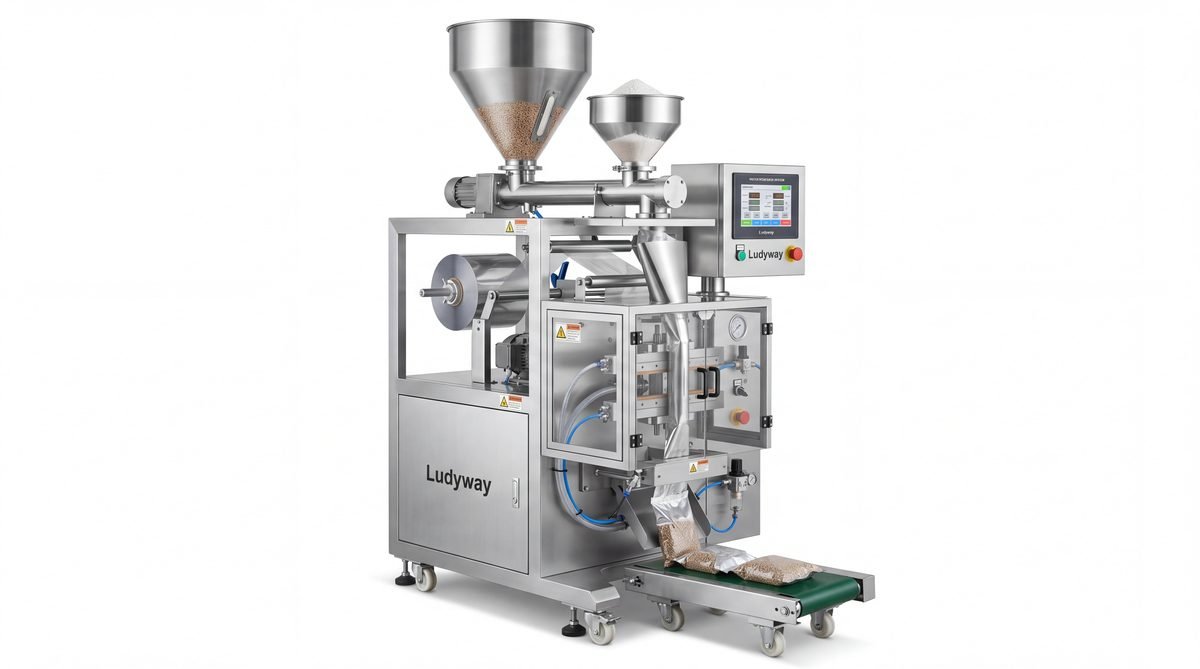
Purchasing a vacuum packaging machine is a strategic investment. Beyond the equipment itself, assess the manufacturer’s engineering expertise, customization capabilities, and after-sales support infrastructure. Ludyway Machinery, a China-based packaging machinery manufacturer with more than 30 years of industry experience, operates a 20,000-square-meter manufacturing facility and serves customers in over 100 countries. The company is projected to achieve export revenue exceeding RMB 500 million (approximately US$69 million) in 2025, with plans to surpass RMB 1 billion (approximately US$138 million) in 2026. Such scale indicates robust manufacturing capacity and global service capability — factors that contribute to reliable equipment supply and long-term technical support.
When reviewing potential partners, consider their track record in international packaging exhibitions and industry engagement through organizations such as the PMMI — Association for Packaging and Processing Technologies.
11. Customization: One Size Does Not Fit All
Standardized machines work well for common applications, but many manufacturers require tailored configurations. A supplier offering customized vacuum packaging solutions can adapt chamber dimensions, conveyor layouts, sealing bar configurations, and control logic to match specific product and production requirements. This approach is particularly beneficial for flexible packaging applications where bag sizes, materials, and throughput demands vary significantly.
12. Preparing for Future Growth
Select a vacuum packaging machine that accommodates your projected growth over the next 3-5 years. Modular designs that support lane expansions, faster cycle speeds, and additional automation modules — such as automatic bag loading, coding, and case packing — protect your initial investment and reduce the cost of future upgrades.
Key Takeaways
- Match machine type to your product format and production volume
- Prioritize seal integrity and vacuum consistency over maximum speed
- Verify material compatibility across your full range of packaging films
- Choose suppliers with proven global service networks and engineering depth
- Plan for automation integration from day one, even if phased in later
A well-chosen Sevana vacuum packaging machine delivers consistent product quality, reduces waste, and supports scalable production growth. By evaluating technical specifications alongside supplier capabilities and long-term support infrastructure, manufacturers can make informed purchasing decisions that align with both current needs and future ambitions.