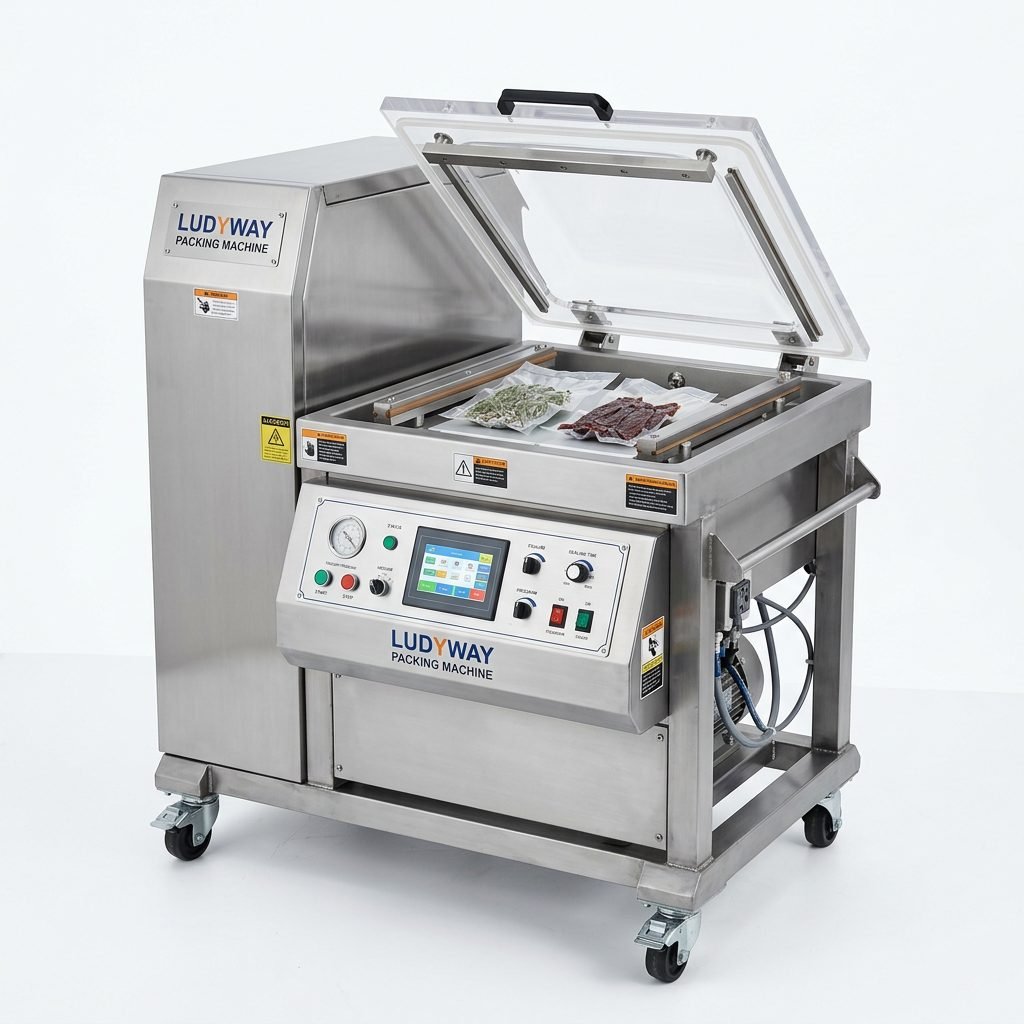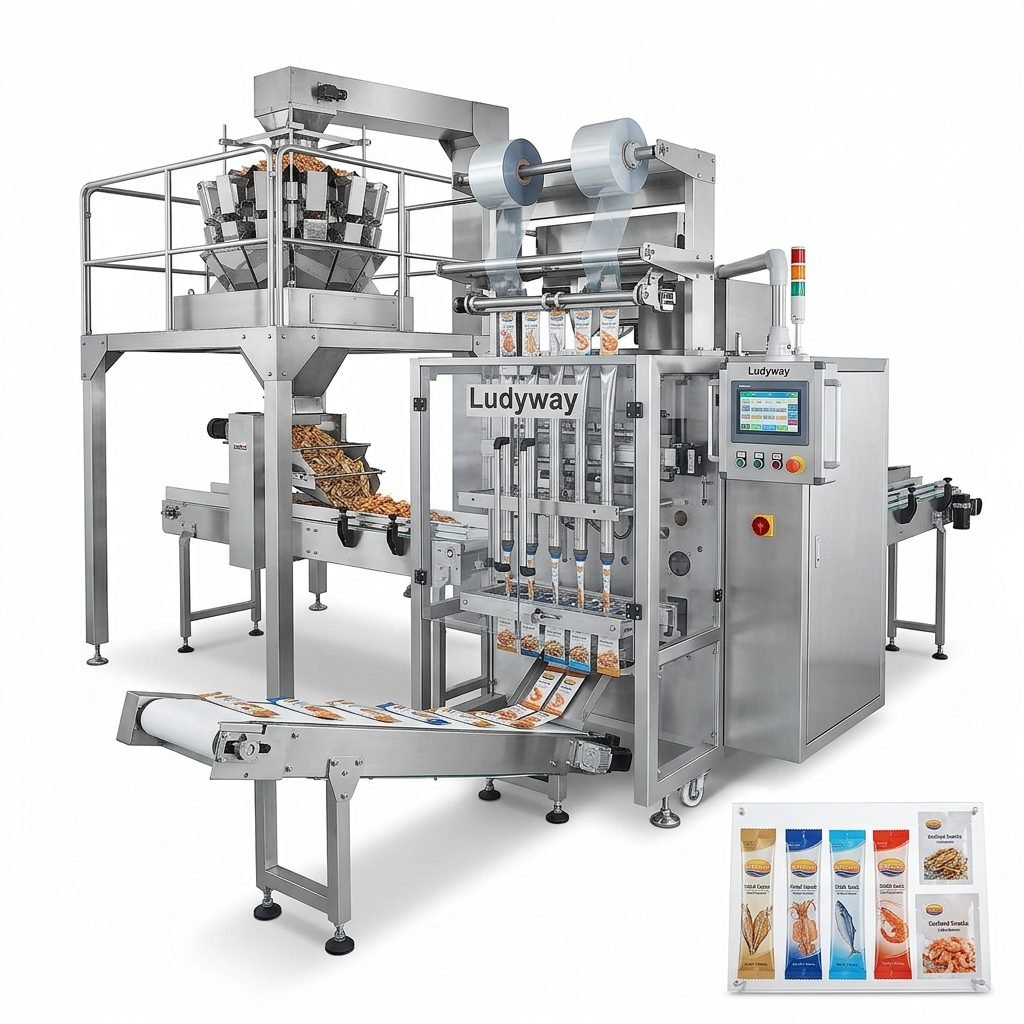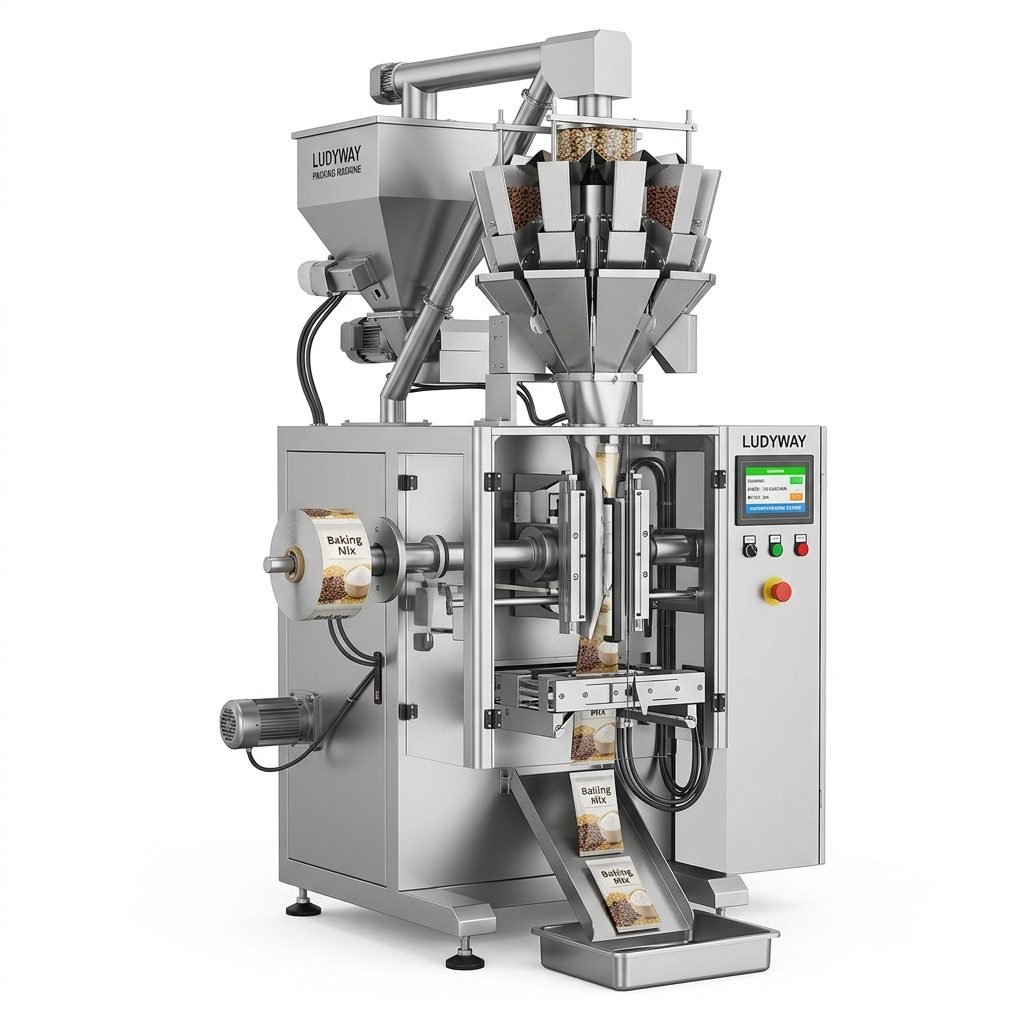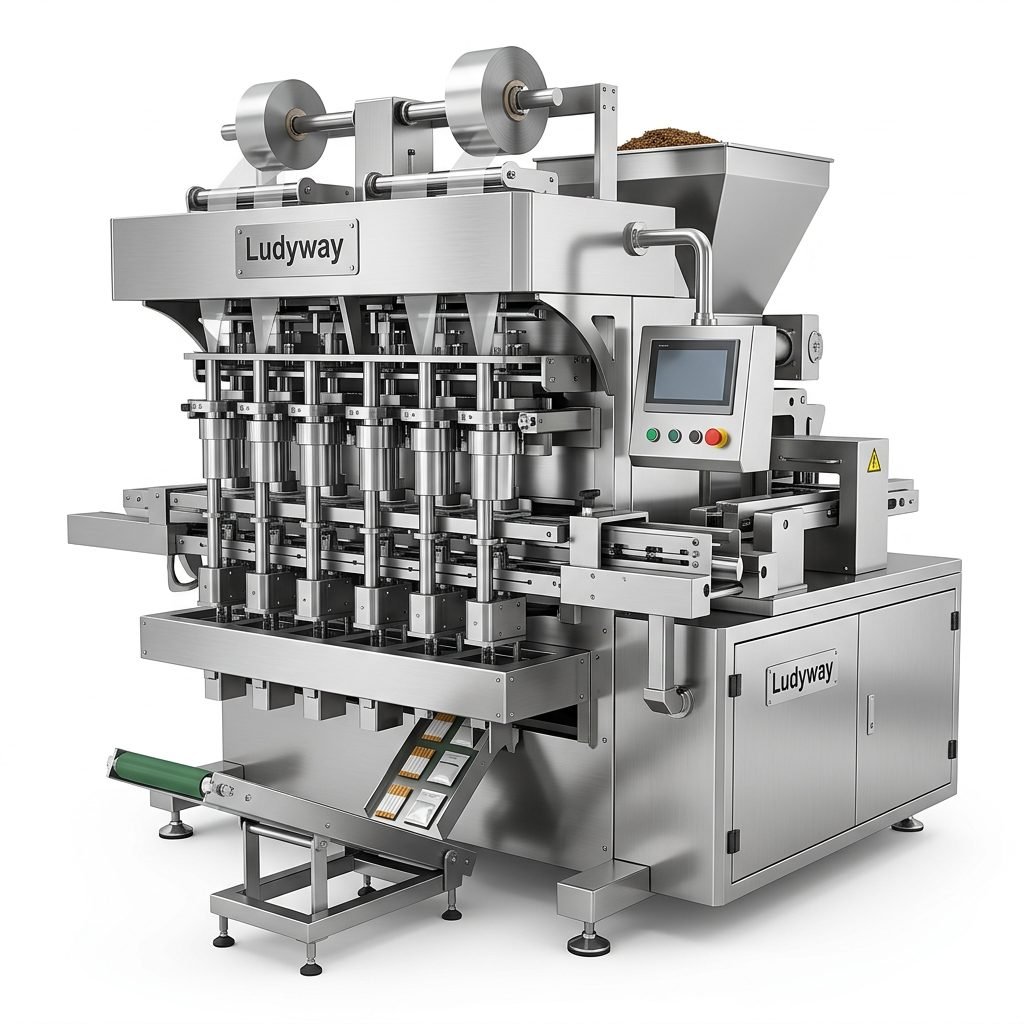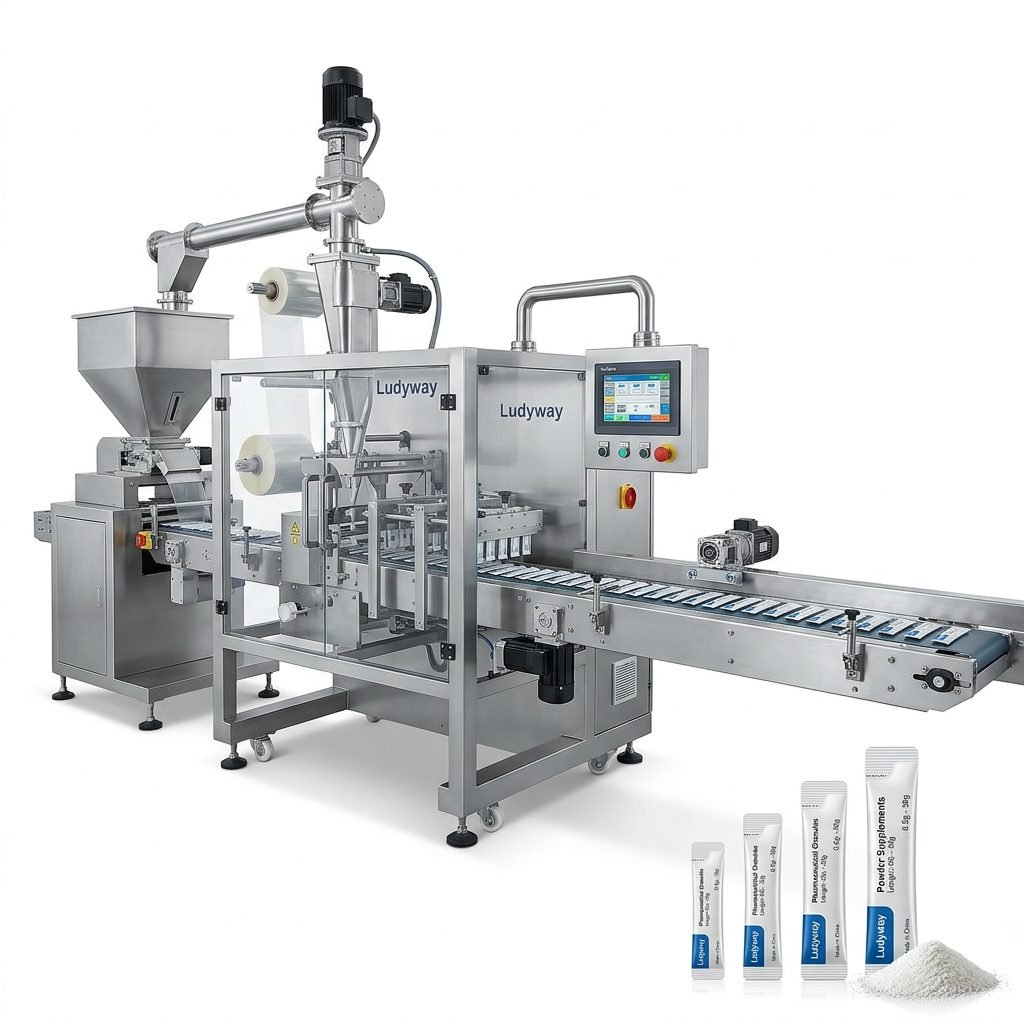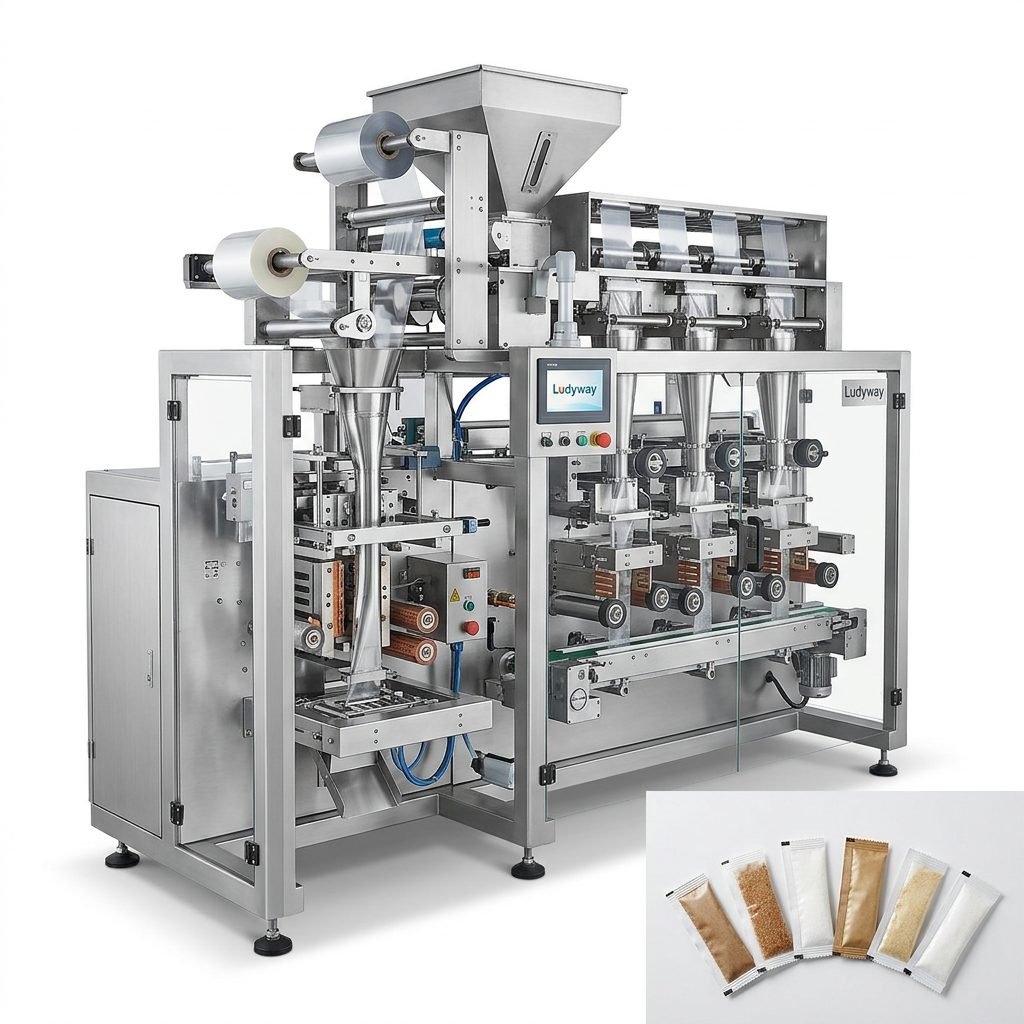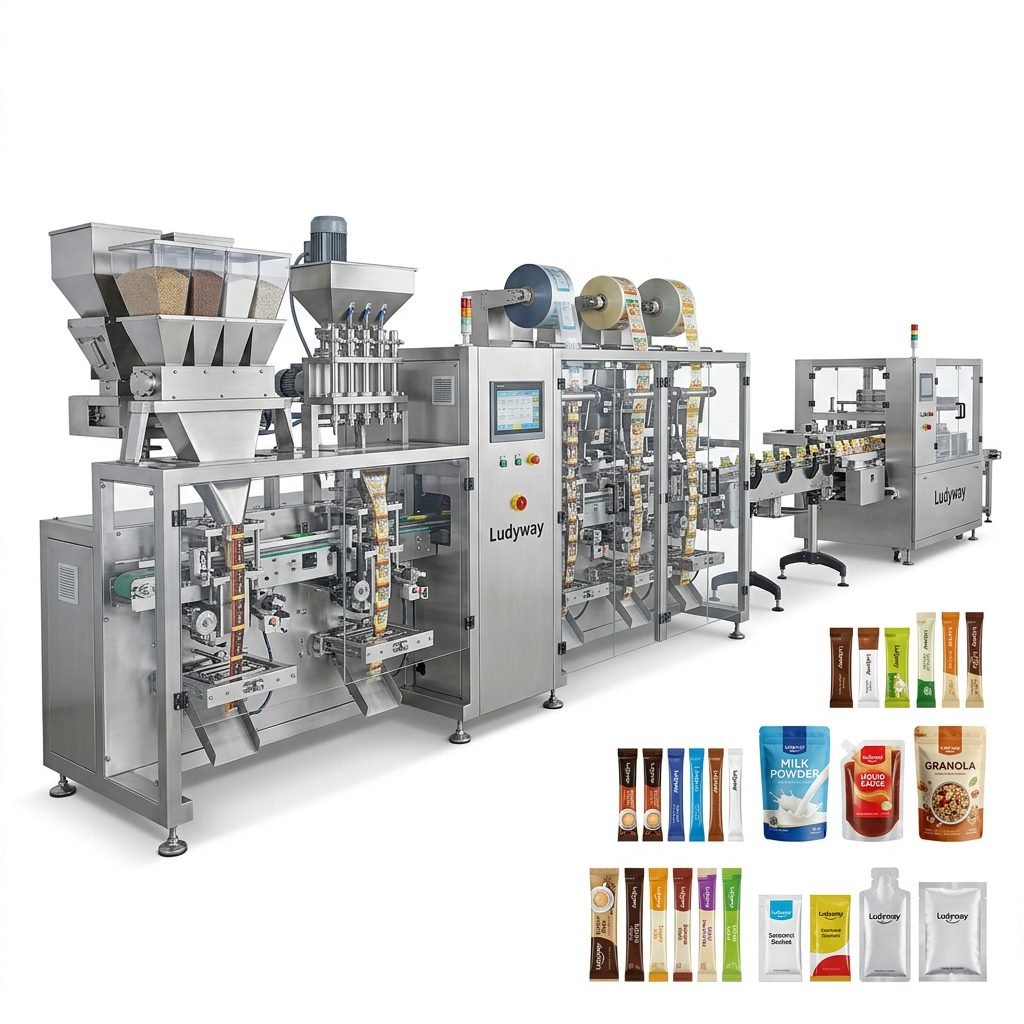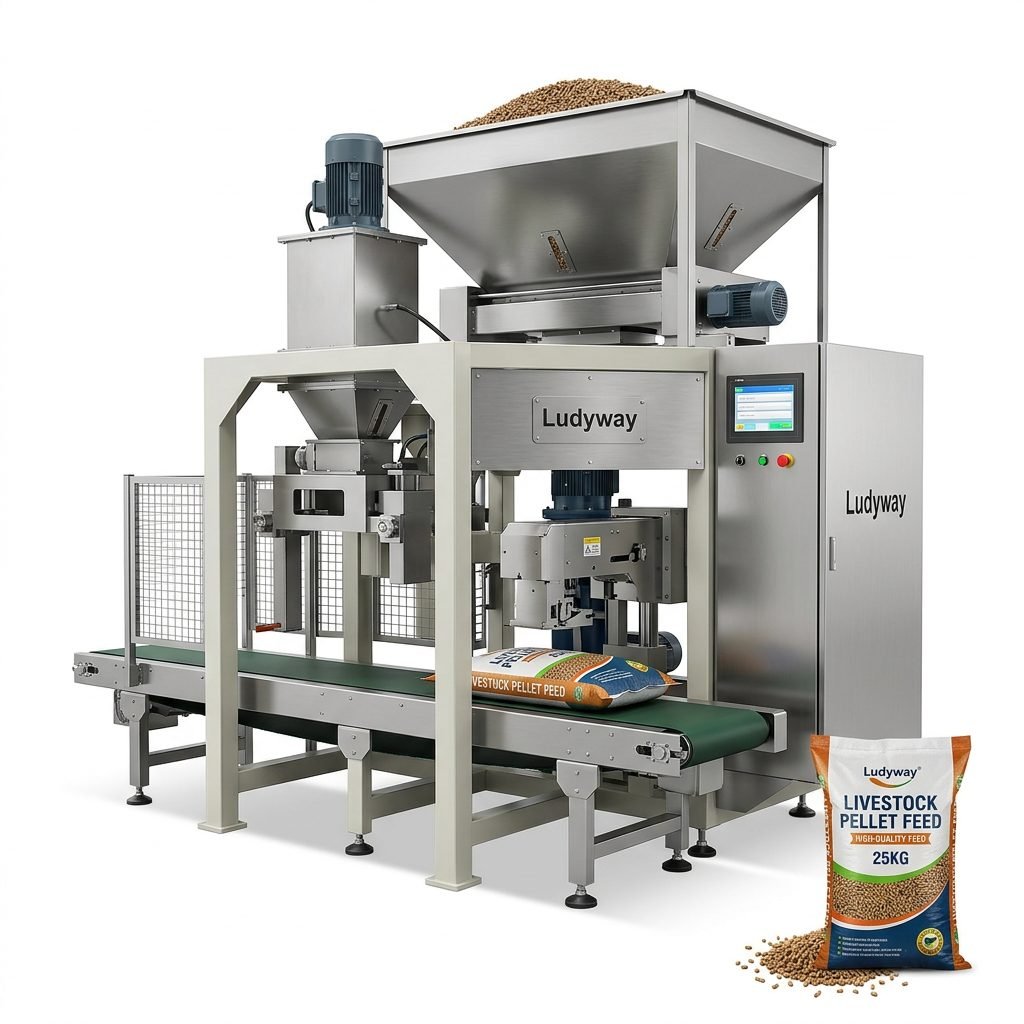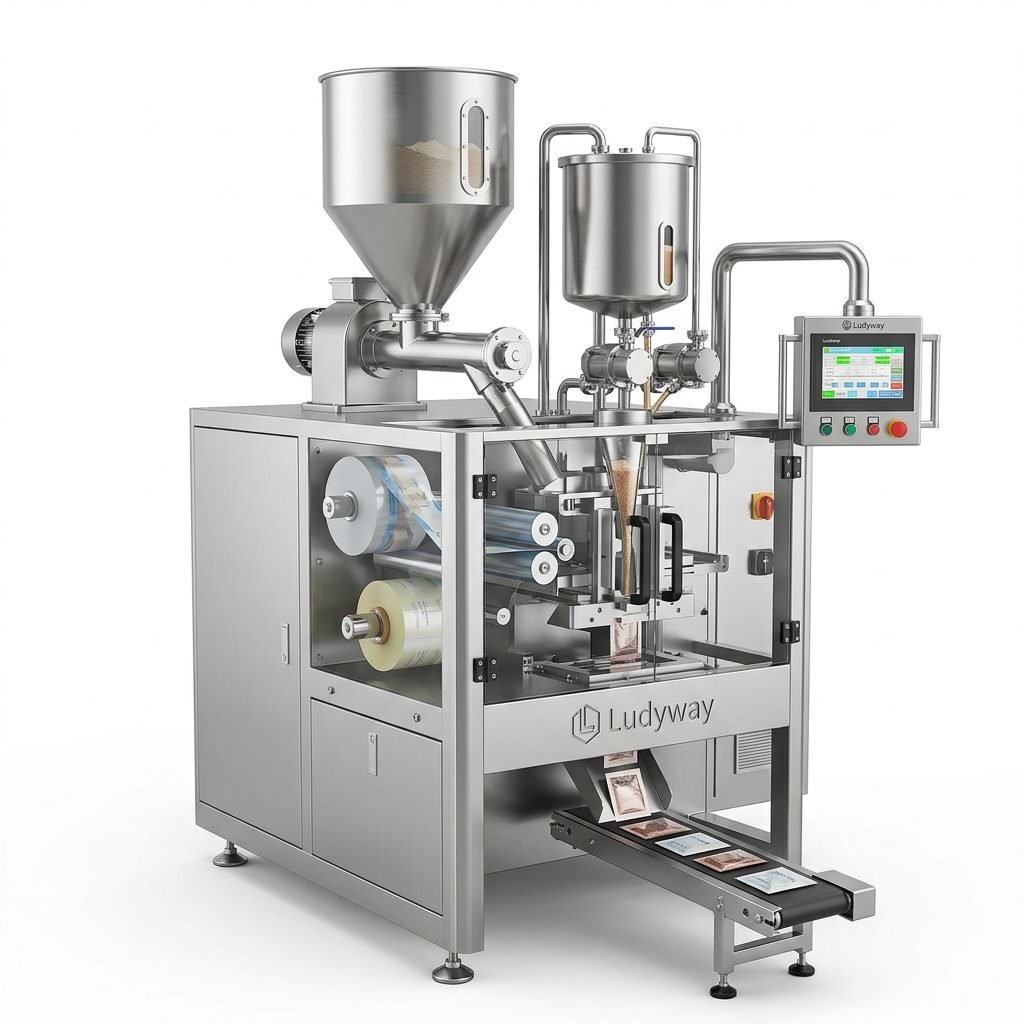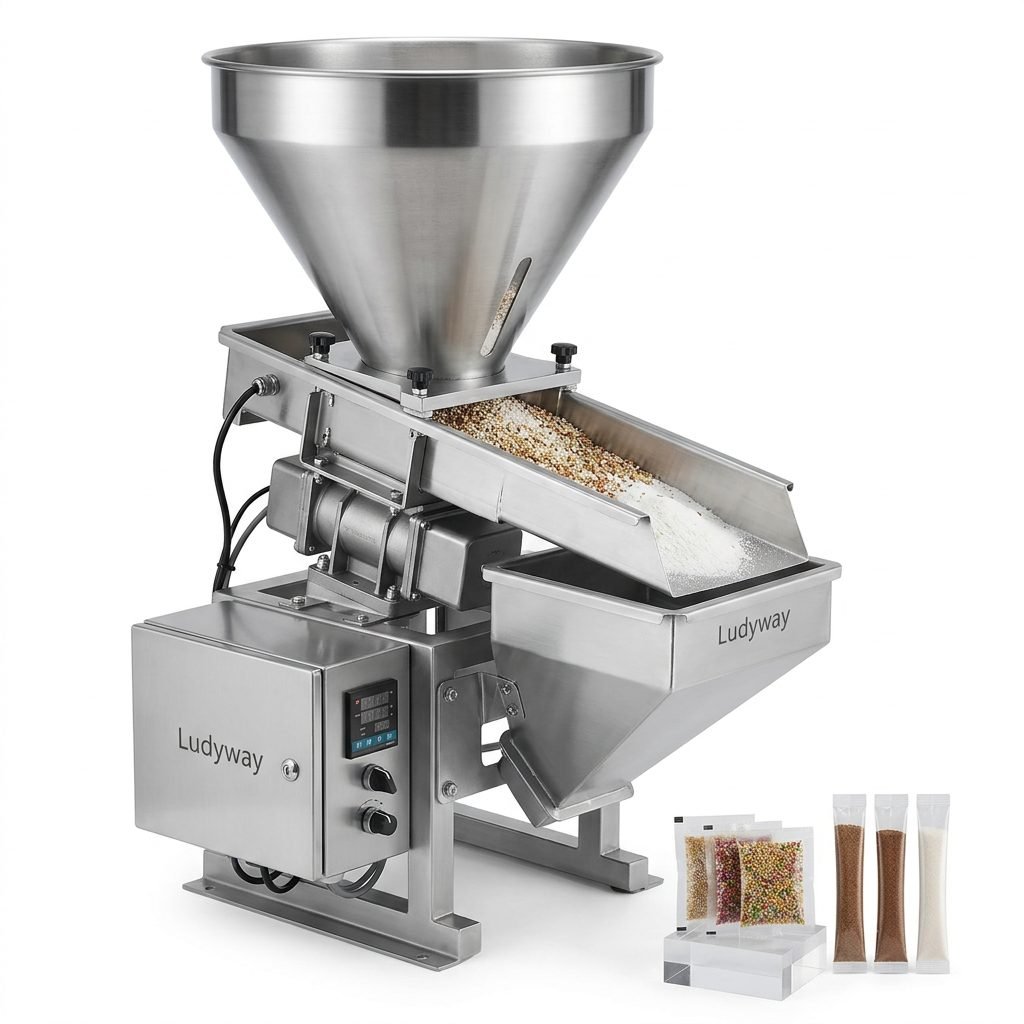
North American food manufacturers face increasing pressure to extend product shelf life, maintain freshness, and comply with stringent FDA food packaging regulations while optimizing operational costs. Vacuum packaging technology has emerged as the definitive solution for preserving food quality, reducing waste, and meeting consumer demand for minimally processed products. Selecting the right vacuum packaging machine partner can significantly impact your production efficiency and bottom line.
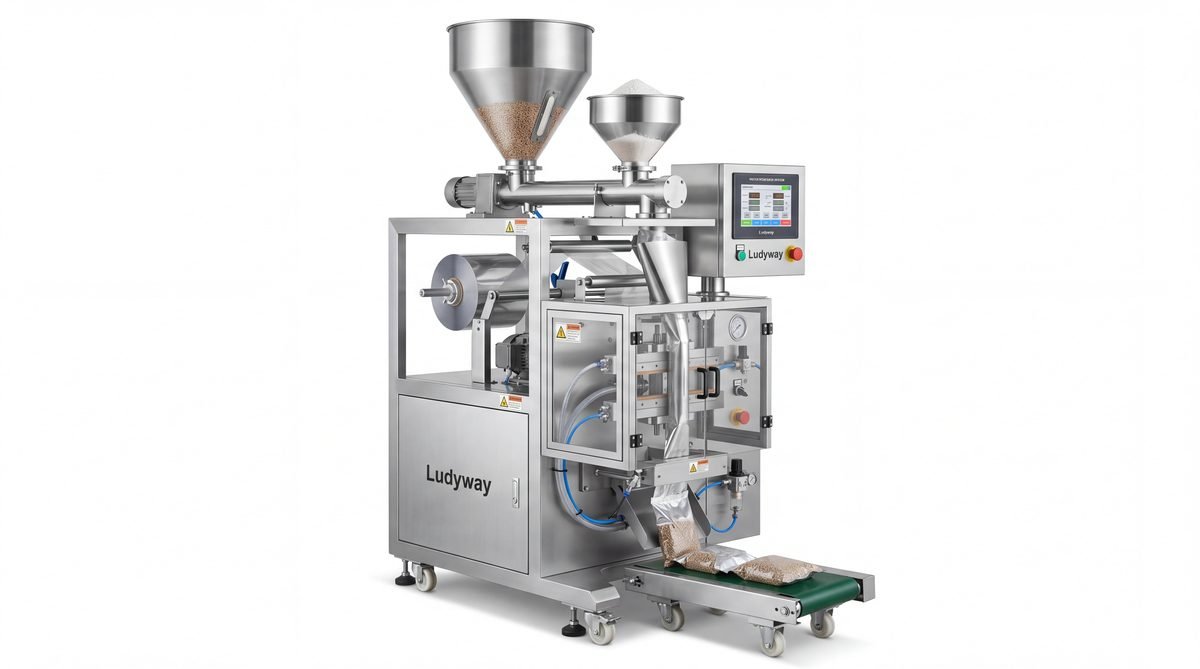
Critical Factors for Vacuum Packaging in North America
North American food processors require equipment that meets rigorous safety standards and delivers consistent performance. Key considerations include compliance with ISO packaging standards, compatibility with diverse food types, and seamless integration into existing production lines. The PMMI reports that North American food packaging machinery demand continues to grow year over year, driven by automation and food safety requirements.
| Feature | Benefit for North American Manufacturers |
|---|---|
| High-Speed Multi-Lane Systems | Maximize throughput while reducing per-unit packaging costs |
| Precision Vacuum Sealing | Extended product shelf life and superior freshness retention |
| Stainless Steel Construction | Full compliance with USDA and FDA sanitary requirements |
| Intelligent Control Systems | Reduced operator training time and minimized human error |
| Turnkey Integration | Single-source solution from filling to final packaging |
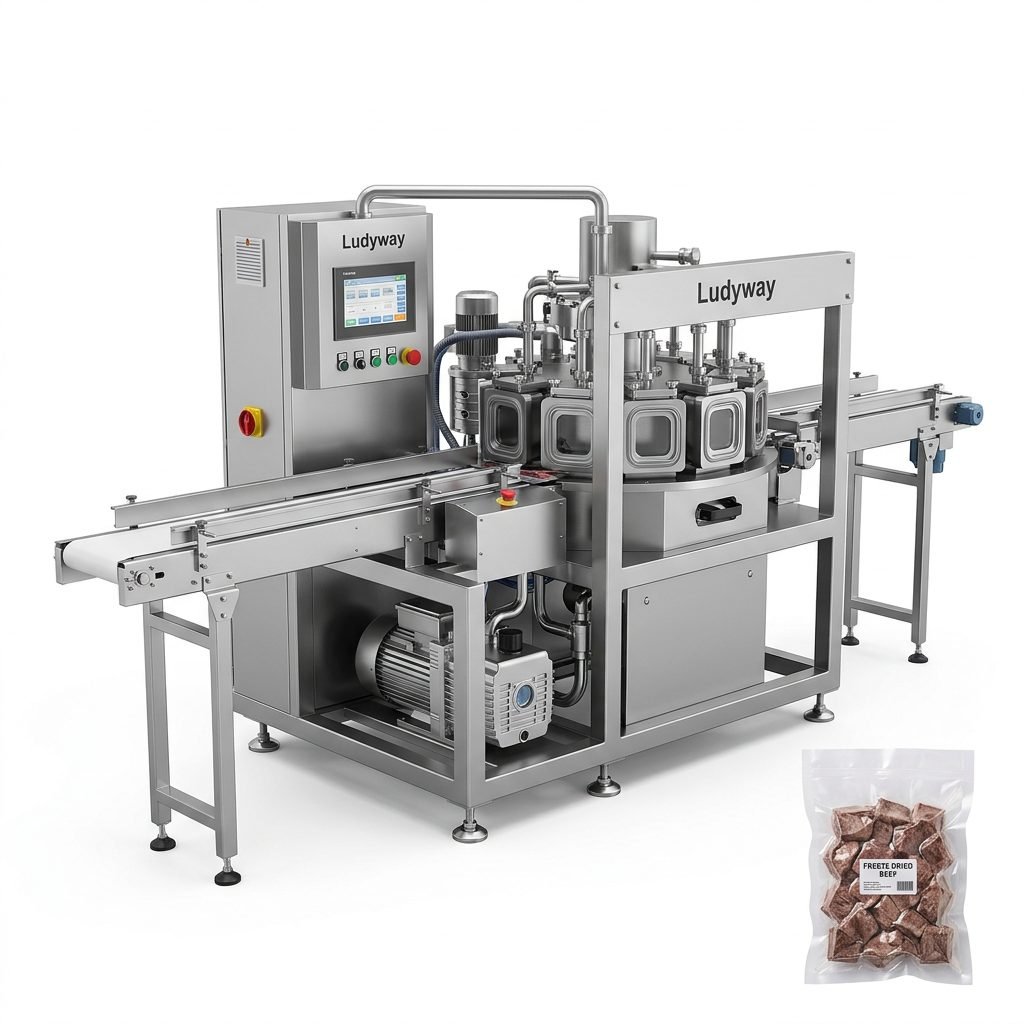
Applications Across the Food Industry
Modern vacuum packaging machines serve an extensive range of food categories. From freeze-dried fruits and vegetables to meat products, seafood, dairy, and ready-to-eat meals, the versatility of advanced vacuum systems enables processors to package diverse product lines with a single equipment platform.
- Freeze-dried foods — preserves texture and nutritional value
- Fresh and processed meats — prevents oxidation and discoloration
- Seafood products — maintains moisture and prevents freezer burn
- Dairy and cheese — extends shelf life without preservatives
- Snack foods and nuts — protects against rancidity and staleness
- Pet food and treats — ensures freshness in premium product lines
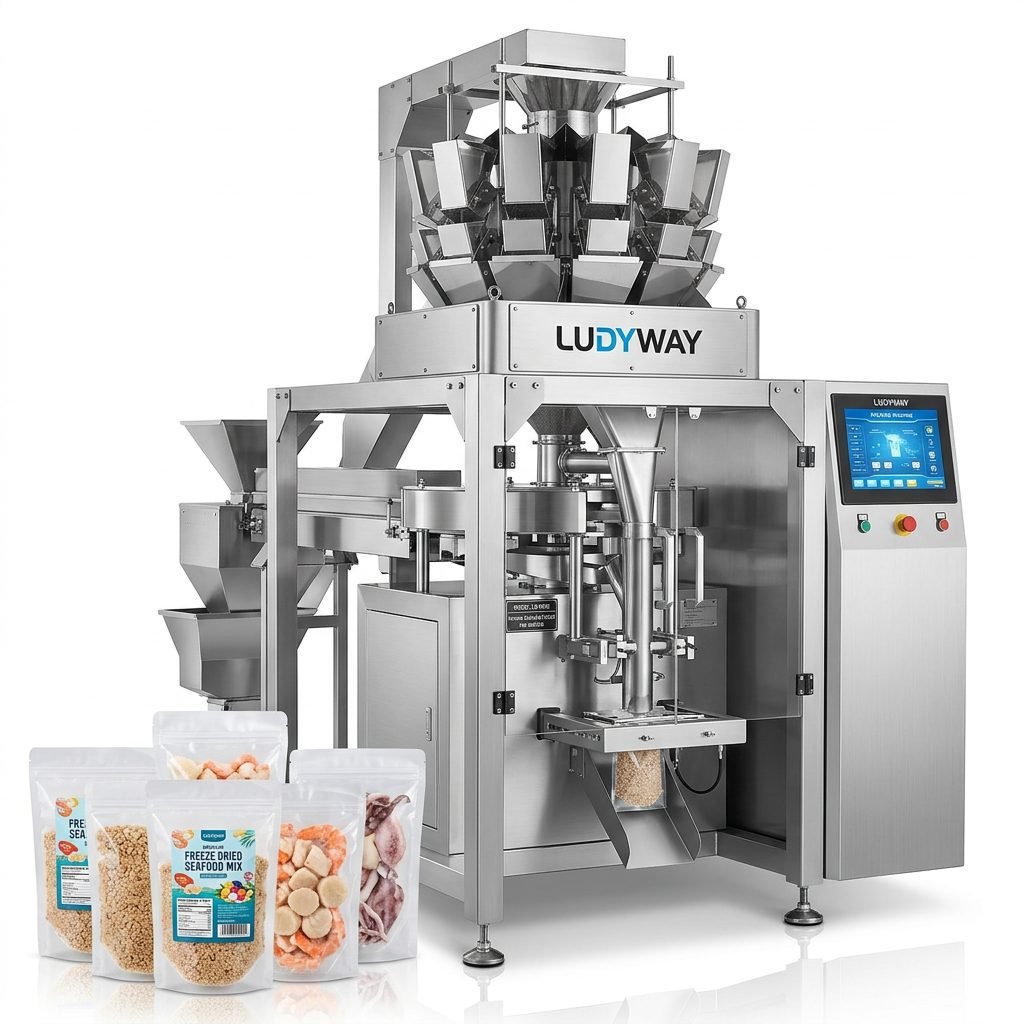
Technology and Engineering Excellence
Advanced food vacuum packaging machines incorporate multiple technologies that set them apart in the North American market. Multi-lane configurations dramatically increase output while precision dosing systems ensure exact portion control — a critical requirement for regulated food products. Nitrogen flushing capabilities further enhance product preservation by displacing oxygen before sealing, which is particularly valuable for sensitive ingredients and extended distribution channels.
Key Technical Specifications to Evaluate
- Vacuum pressure range and consistency
- Sealing temperature precision and dwell time control
- Compatible film materials and thickness range
- Production speed across different package formats
- Changeover time between product types
- Integration with upstream and downstream equipment
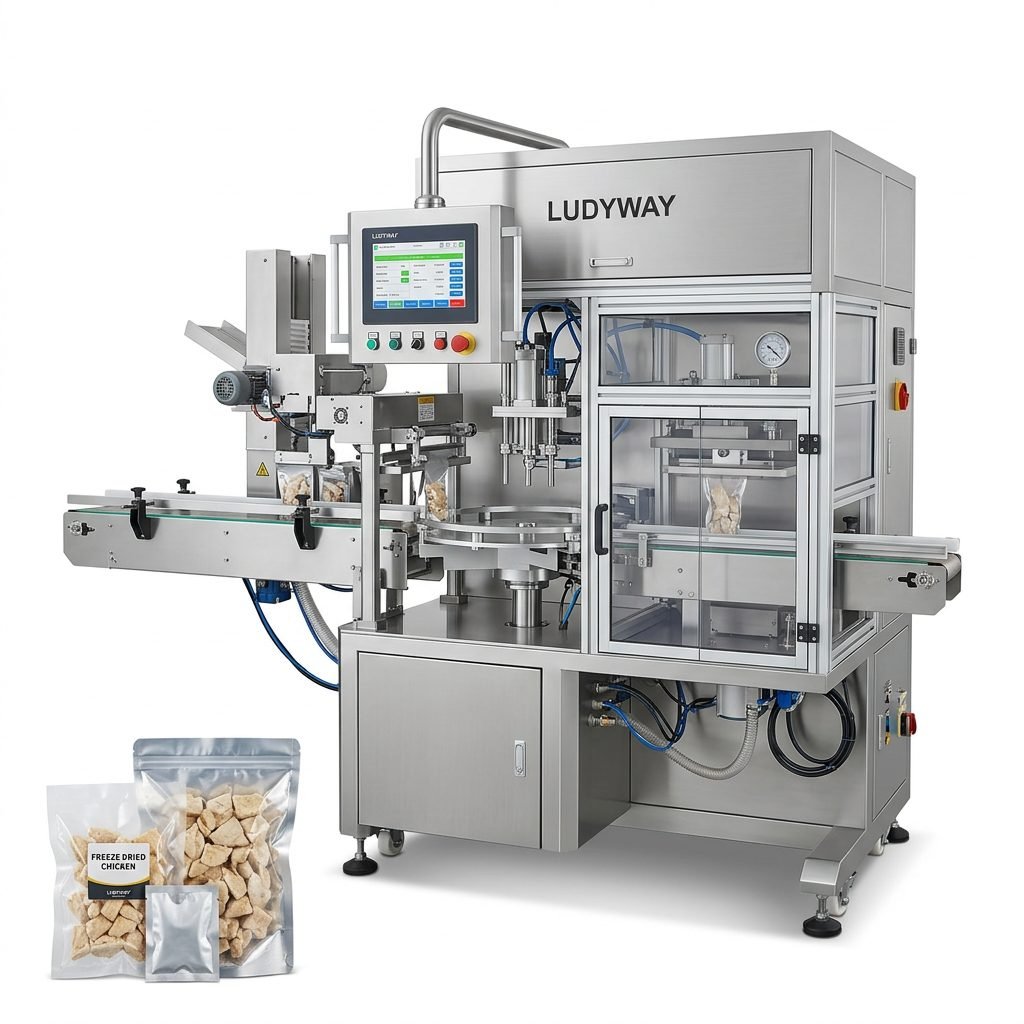
Why North American Processors Are Making the Switch
The flexible packaging industry in North America continues to expand, and food manufacturers need reliable equipment partners who understand both regulatory requirements and production realities. Ludyway, one of the largest packaging machine manufacturers in China, operates a modern 20,000㎡ manufacturing facility and offers more than 50 intelligent packaging machine models, serving customers in over 100 countries with advanced vacuum packaging solutions for the food, pharmaceutical, and health industries.
| Industry Standard | Relevance to Vacuum Packaging |
|---|---|
| FDA 21 CFR | Food contact substance compliance for all packaging materials |
| ISO 11607 | Validated sealing and packaging integrity standards |
| HACCP Principles | Critical control points for food safety in packaging |
| USDA Requirements | Sanitary design and material traceability mandates |
Return on Investment Considerations
Investing in high-quality vacuum packaging equipment delivers measurable returns. Reduced product spoilage, lower packaging material waste, faster production speeds, and decreased labor requirements all contribute to a rapid payback period. Additionally, superior package quality enhances brand perception and can support premium pricing strategies in competitive North American retail environments.
Operational Benefits at a Glance
- Up to 40% reduction in product spoilage and returns
- Significant decrease in packaging film consumption
- Labor savings through automated multi-lane operation
- Extended distribution reach with longer shelf life products
Making the Right Choice for Your Facility
Selecting a vacuum packaging machine supplier requires evaluating technical capabilities, industry experience, after-sales support, and long-term reliability. For more information on how advanced vacuum packaging technology can transform your food production operations, explore the complete range of packaging solutions designed specifically for the North American market. You can also review the latest packaging industry state-of-the-industry reports from PMMI for comprehensive market insights.