In the specialty coffee industry, preserving the delicate aromas, volatile oils, and complex flavor profiles of freshly roasted beans is a relentless battle against oxygen, moisture, and time. For roasters, distributors, and large-scale coffee producers, investing in a high-performance coffee vacuum packaging machine is not just an operational upgrade—it is the definitive line between delivering a premium sensory experience and a stale, flat cup. As the global demand for specialty and single-origin coffee surges, understanding how advanced packaging technology locks in peak freshness becomes a critical competitive advantage.
The Science of Coffee Degassing and Staleness
To appreciate the value of vacuum sealing, one must first understand the enemy. Freshly roasted coffee beans undergo a process called degassing, releasing carbon dioxide (CO2) while simultaneously being vulnerable to oxidation. Oxygen is the primary catalyst for staling, causing lipids to go rancid and aromatic compounds to evaporate. While one-way valve bags allow CO2 to escape without letting oxygen in, they still leave beans in contact with residual oxygen. A vacuum packaging machine for coffee physically removes this atmosphere, drastically decelerating the oxidation process and preserving the coffee’s intrinsic organoleptic properties for months, not weeks.
Why Standard Packaging Fails Premium Coffee
Many producers rely on basic heat-sealing or nitrogen-flushing alone. While nitrogen flushing displaces oxygen, it is rarely 100% efficient, often leaving residual oxygen levels of 2% to 5% inside the package. For ground coffee—which has an exponentially larger surface area than whole beans—this residual oxygen rapidly degrades quality. A dedicated external vacuum system extracts air before sealing, ensuring the bag tightly conforms to the product. This not only minimizes oxygen but also prevents moisture ingress and creates a rigid, brick-like package that protects fragile whole beans from physical damage during transit and storage.
Key Features of an Industrial Coffee Vacuum Sealer
Not all vacuum machines are created equal. When selecting equipment for high-throughput coffee packaging, several engineering factors stand out:
- Adjustable Vacuum Levels: The ability to fine-tune the vacuum strength is crucial. Too much vacuum on delicate whole beans can crush them; a precision gauge allows operators to find the perfect balance.
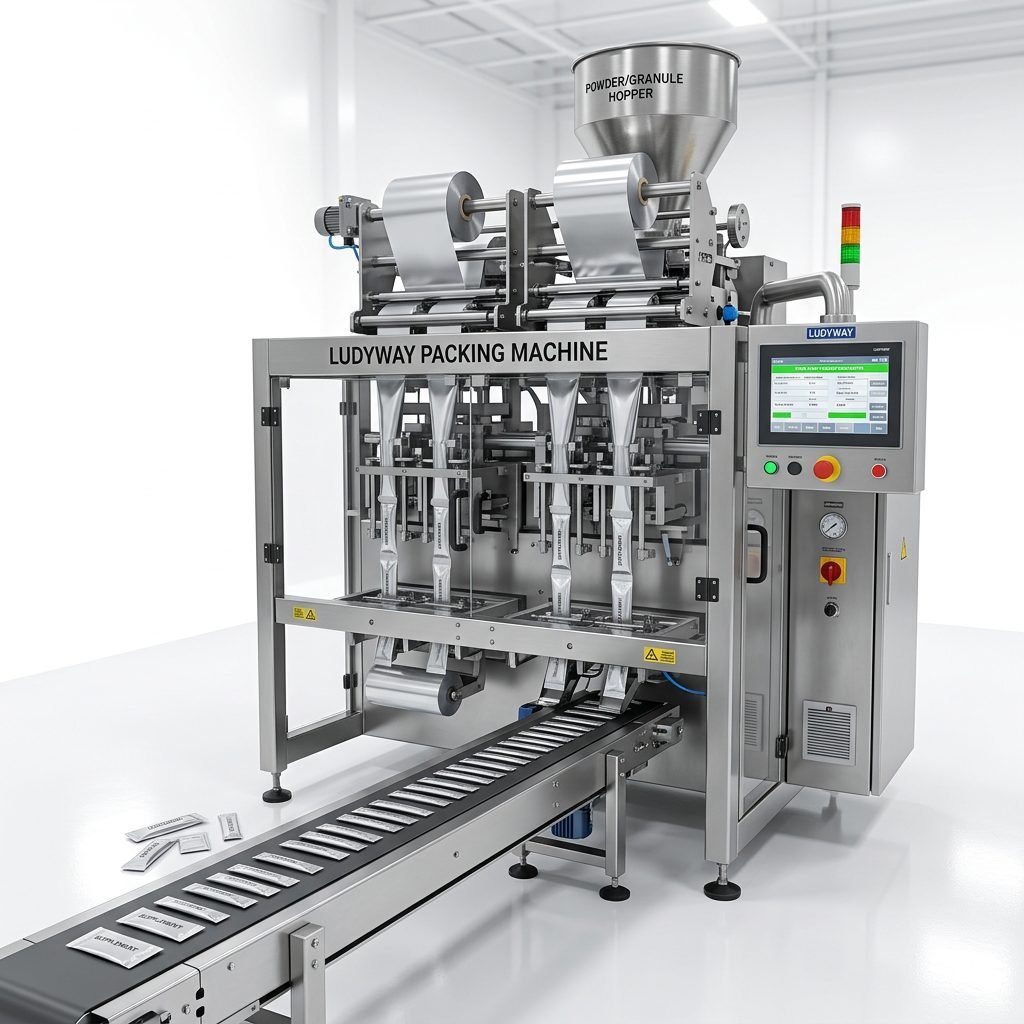
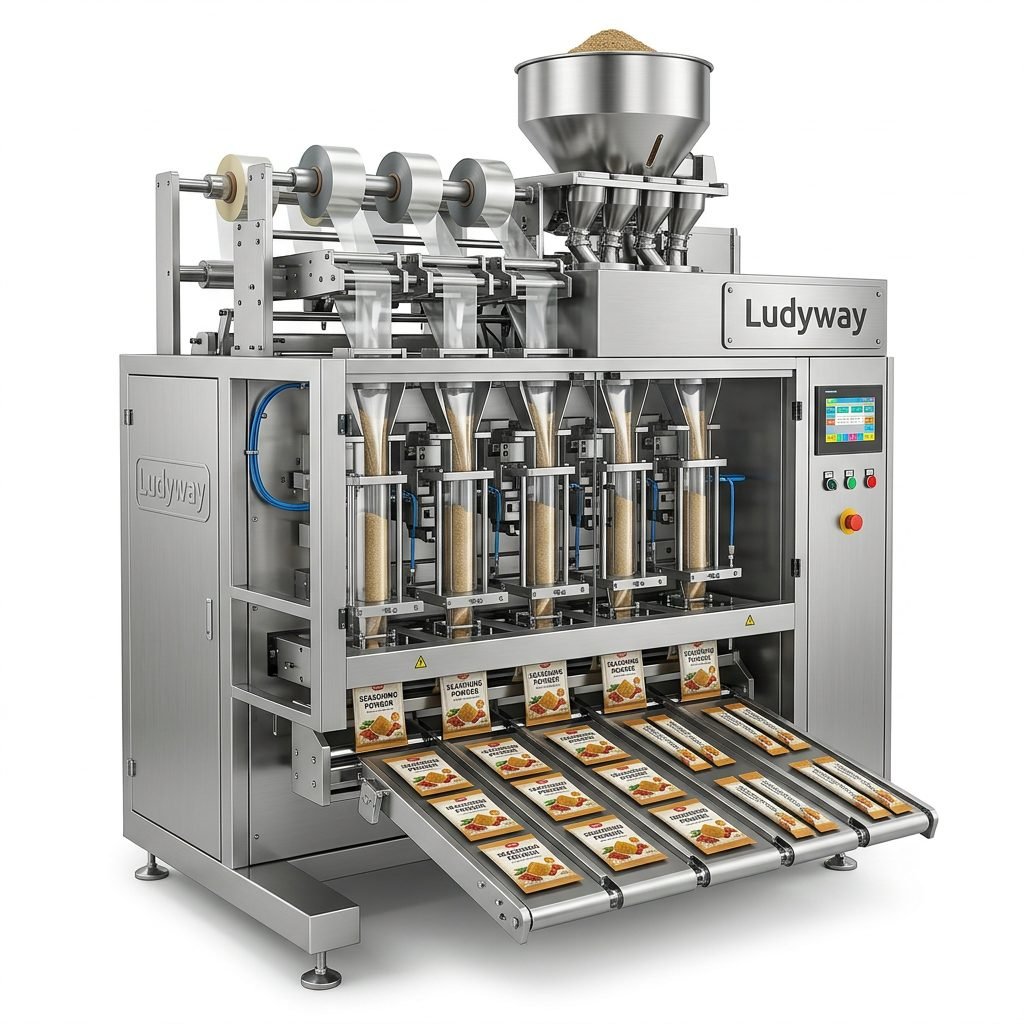
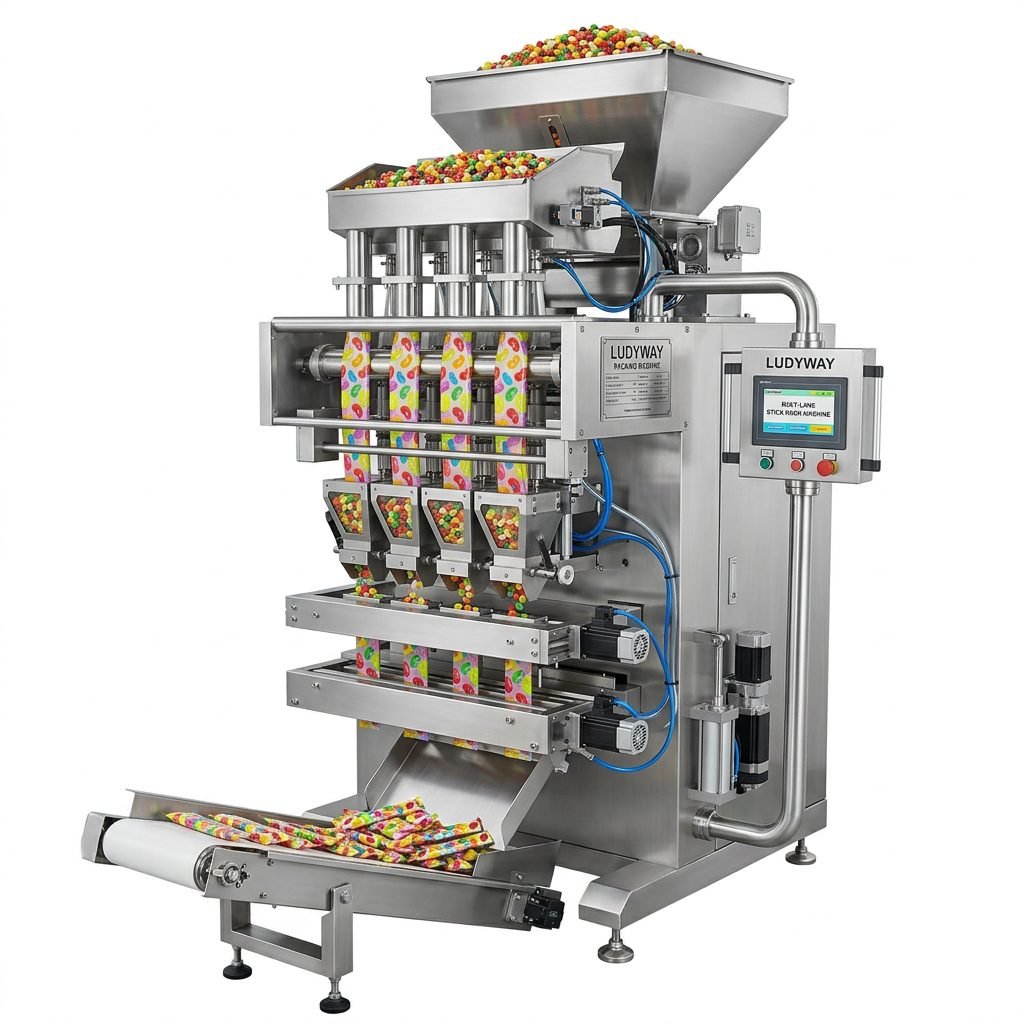
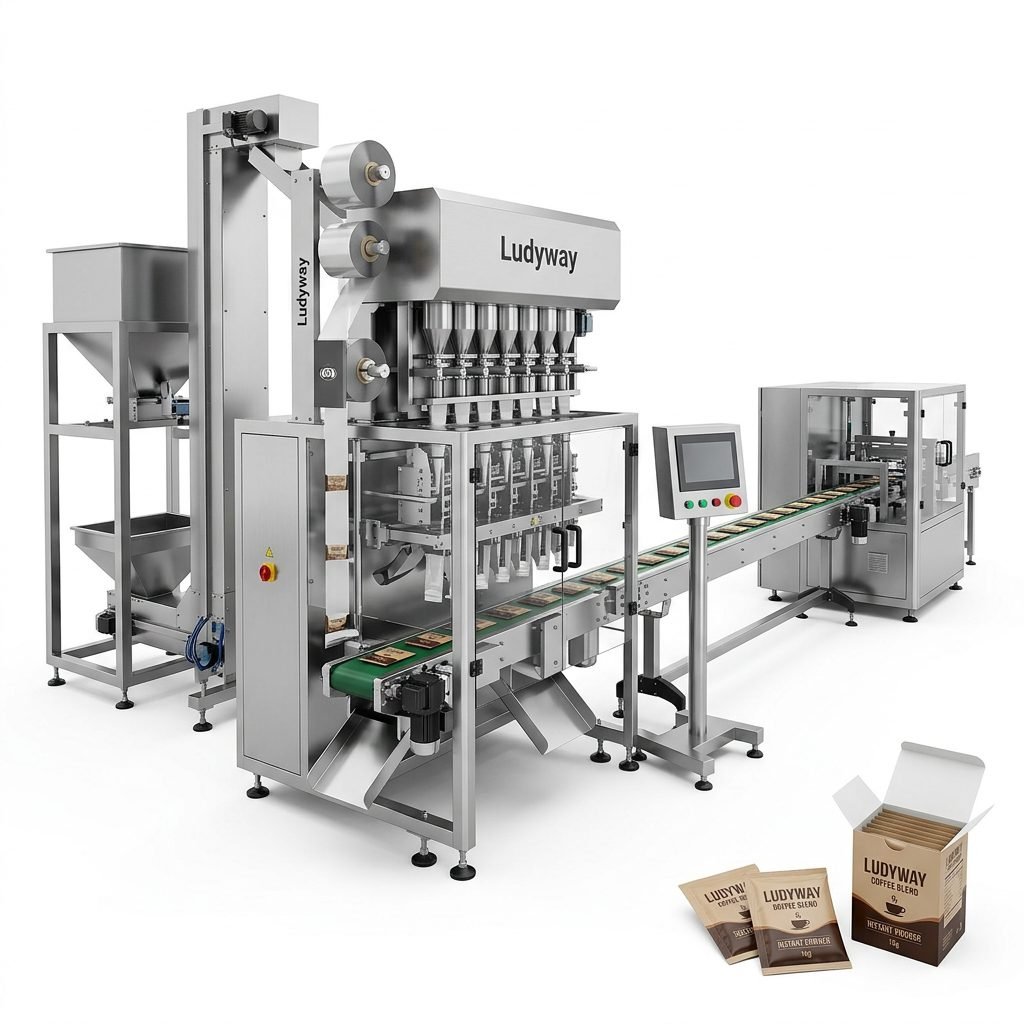
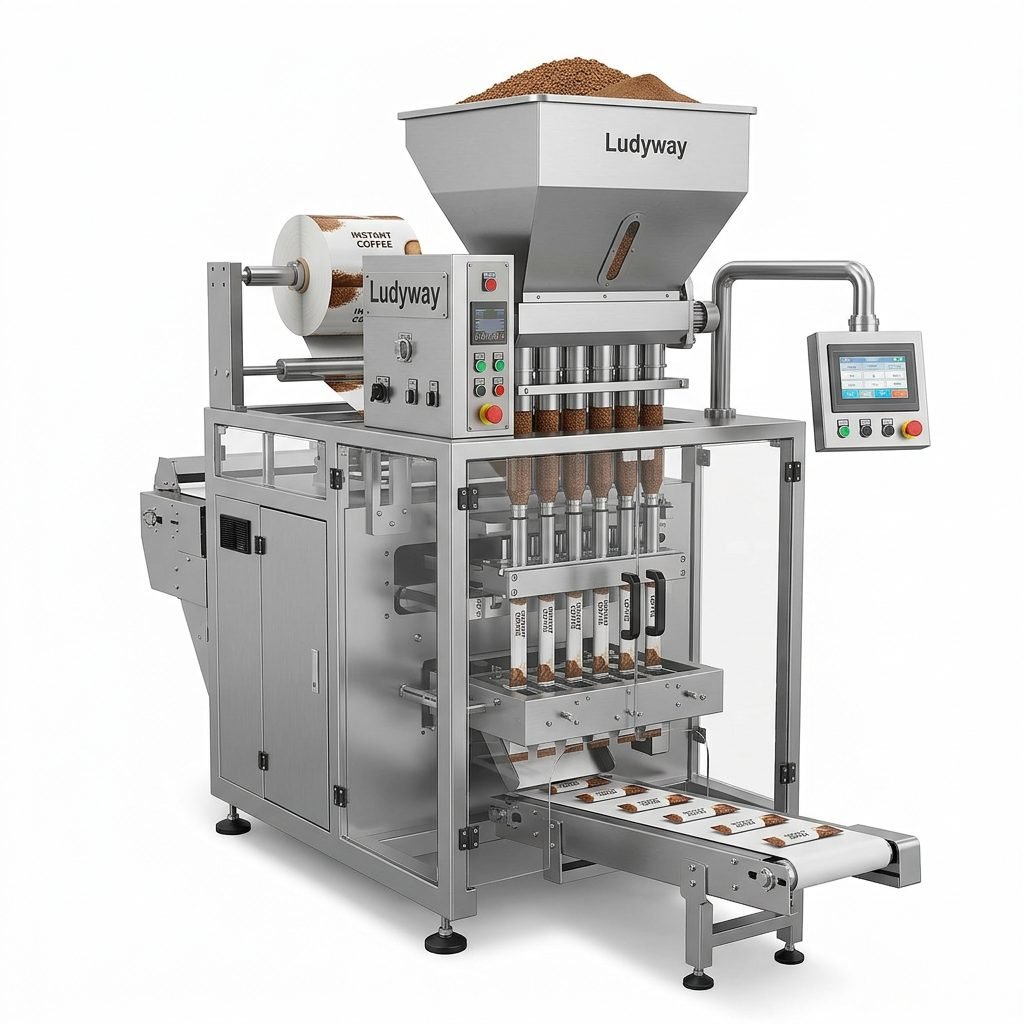
- Multi-Lane Configuration: For ground coffee and stick pack formats, multi-lane sachet vacuum machines maximize throughput without sacrificing seal integrity.
- Dual-Sealing Systems: A secondary sealing bar provides a fail-safe, preventing air leakage that could compromise seal quality.
- Compatible Film Handling: The machine must flawlessly handle metallic and high-barrier laminated films essential for aroma retention.
The Ludyway Approach to Vacuum Packaging Engineering
Ludyway is one of the largest packaging machine manufacturers in China, specializing in advanced packaging equipment and turnkey production solutions. Our engineering focus on vacuum-seal integrity integrates high-precision sensors and modular design, allowing roasters to vacuum-pack everything from light-roast single origins to dark-roast espresso blends. By combining a nitrogen-flushing infrastructure with a final vacuum pull, the system achieves oxygen residue levels often below 0.5%, significantly extending the shelf life compared to conventional methods.
| Feature | Standard Packaging | Coffee Vacuum Packaging Machine |
|---|---|---|
| Residual Oxygen | 2% – 5% | < 0.5% |
| Shelf Life (Ground) | 2-4 Weeks | 6-12 Months |
| Bean Integrity | Loose Movement | Compressed & Protected |
| Aroma Lock | Moderate | High (Volatile Oils Preserved) |
Optimizing the Supply Chain with Vacuum Technology
The benefits of vacuum packing extend far beyond the roastery. For e-commerce and global export, vacuum-packed coffee bricks are logistically superior. They occupy less volume, reduce shipping costs, and are impervious to pressure changes during air freight. Furthermore, when paired with a multi-lane stick pack machine, coffee producers can offer single-serve vacuum pods or sticks that guarantee a fresh cup every time, directly catering to the convenience market forecasted in the recent PMMI 2025 State of the Industry analysis.
Vacuum Sealing for Ground Coffee vs. Whole Beans
- Whole Beans: Vacuum pressure must be controlled to prevent crushing. The machine should draw air to a precise set point and hold it for a programmable dwell time to ensure the air is completely evacuated from the irregular voids between beans.
- Ground Coffee: Requires a dust-resistant vacuum pump. Fine coffee particles can easily be sucked into the pump mechanism, causing premature wear. Advanced systems utilize dust traps and filters to maintain performance consistency.
- Pre-Tamped Pucks: For the growing ready-to-brew market, vacuum sealing ensures the puck remains compact and the coffee stays fresh until the moment water hits it.
Integrating Vacuum Lines into Turnkey Solutions
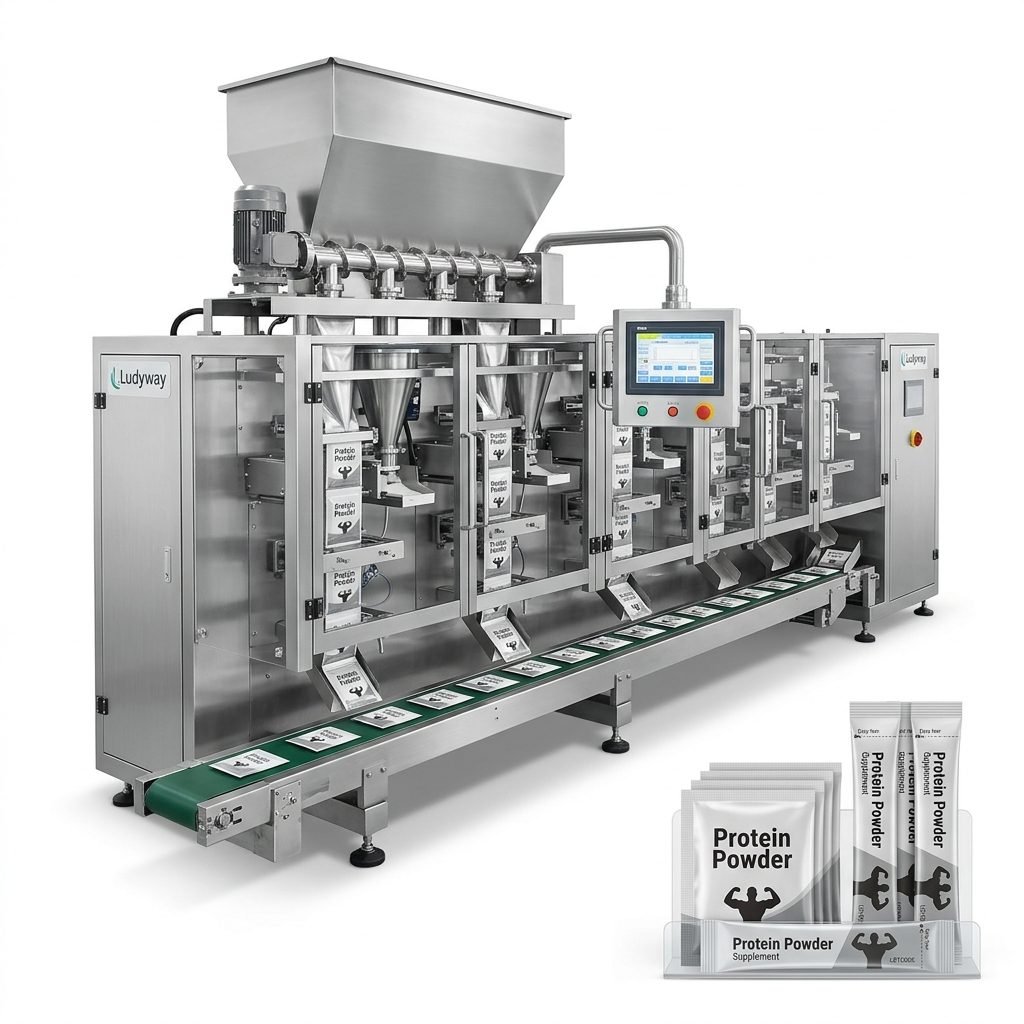
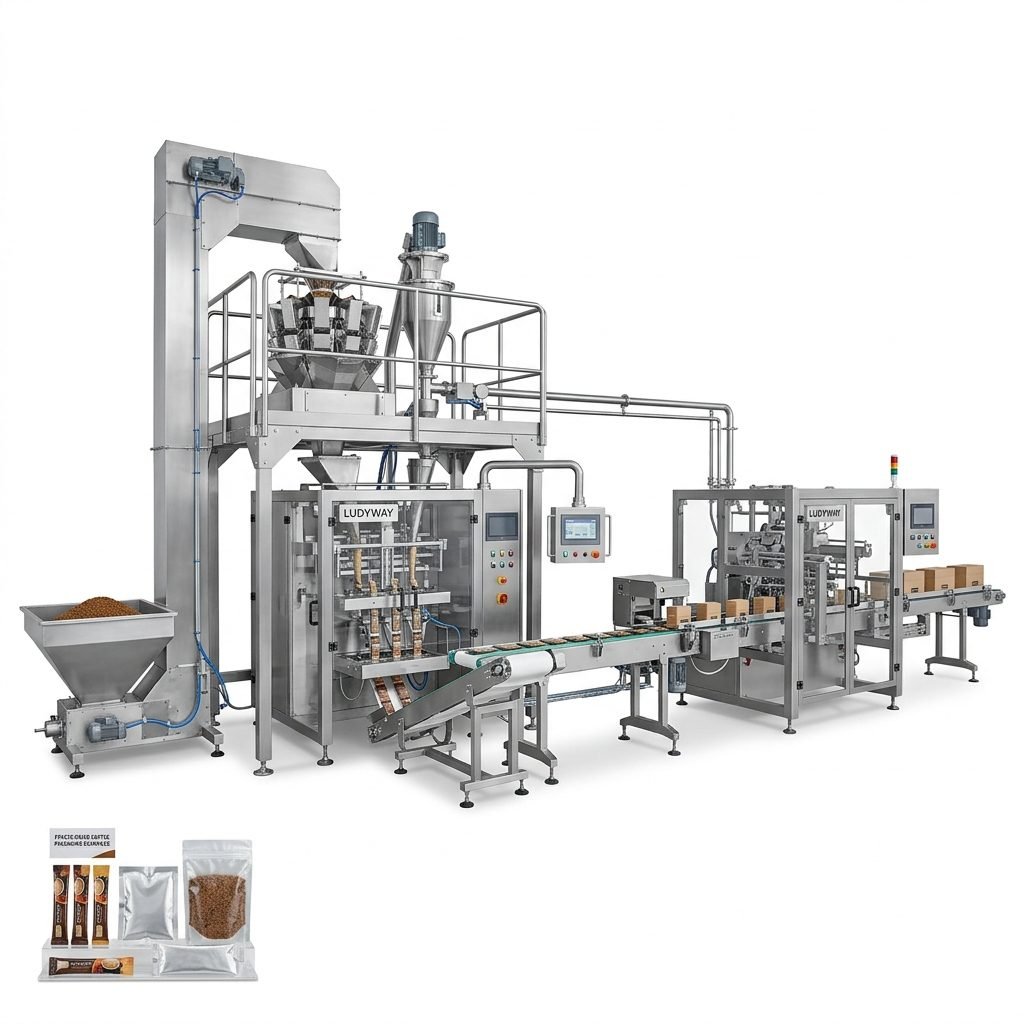
Modern coffee facilities often seek integrated turnkey packaging lines that combine weighing, grinding, filling, vacuum sealing, and cartoning. By synchronizing the vacuum packaging machine with automated weigher fillers, producers can achieve remarkable throughput. The compact, brick-like shape produced by vacuum sealing is ideal for automated cartoning robots, reducing manual labor and boosting end-of-line efficiency.
Maintaining Freshness Beyond the Factory Floor
Consumer perception of quality is heavily influenced by packaging. A professionally vacuum-sealed coffee bag signals freshness, quality control, and attention to detail. It eliminates the “guesswork” for the barista or home brewer. When the vacuum seal is finally broken, the immediate burst of aroma proves that the packaging integrity has faithfully preserved the roast. This tangible proof of quality fosters brand loyalty and justifies a premium price point in a crowded market.
Common Applications for Coffee Vacuum Machines
- Whole Bean Coffee
- Ground Coffee (Espresso & Filter)
- Instant Coffee Powder
- Freeze-Dried Coffee Granules
- Single-Serve Coffee Pods & Sticks
Conclusion
Choosing the right coffee vacuum packaging machine transcends simple bagging; it is a comprehensive quality preservation strategy. From extending shelf life and reducing oxygen residue to enabling efficient supply chains and protecting precious volatile aromas, vacuum technology is indispensable for serious coffee brands. By investing in precision-engineered, modular vacuum sealing solutions designed for the rigors of continuous production, your business can ensure that every bag of coffee reaches the consumer as fresh as the moment it was sealed.