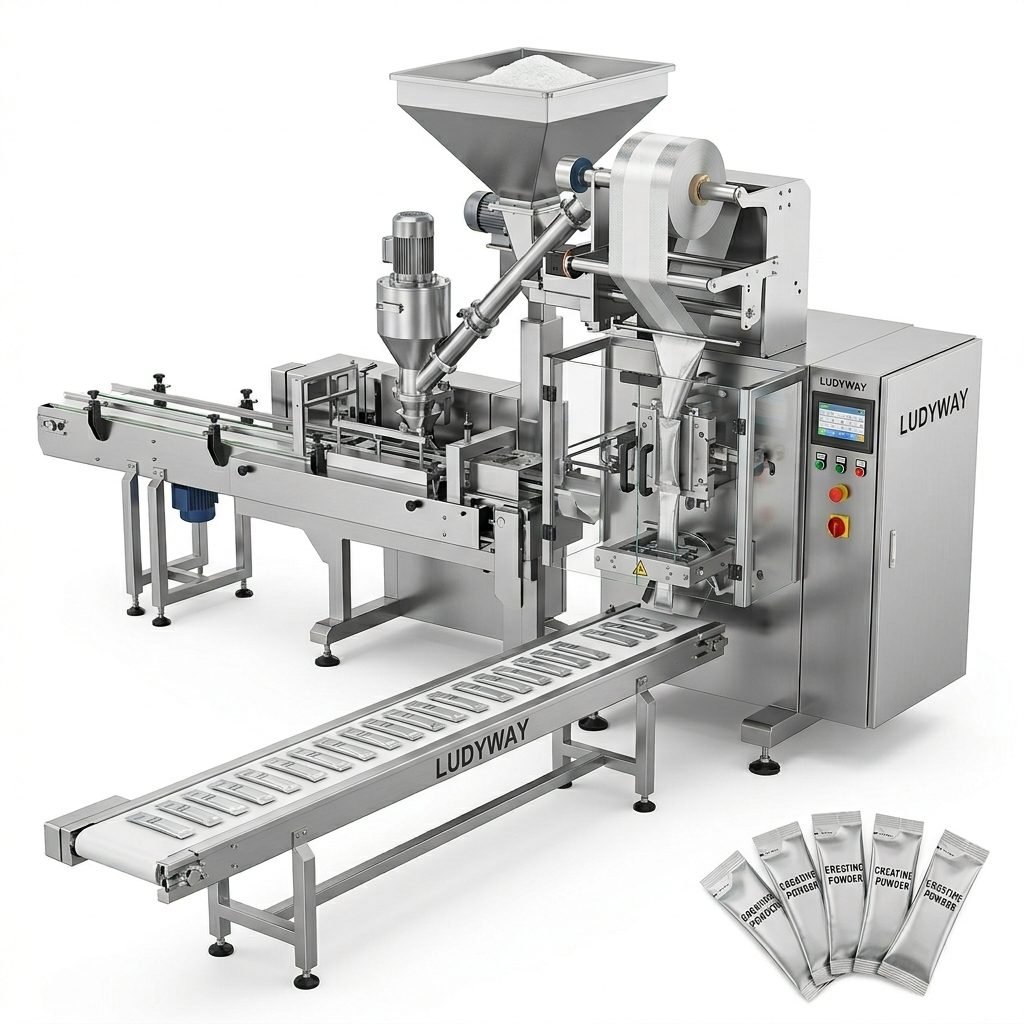
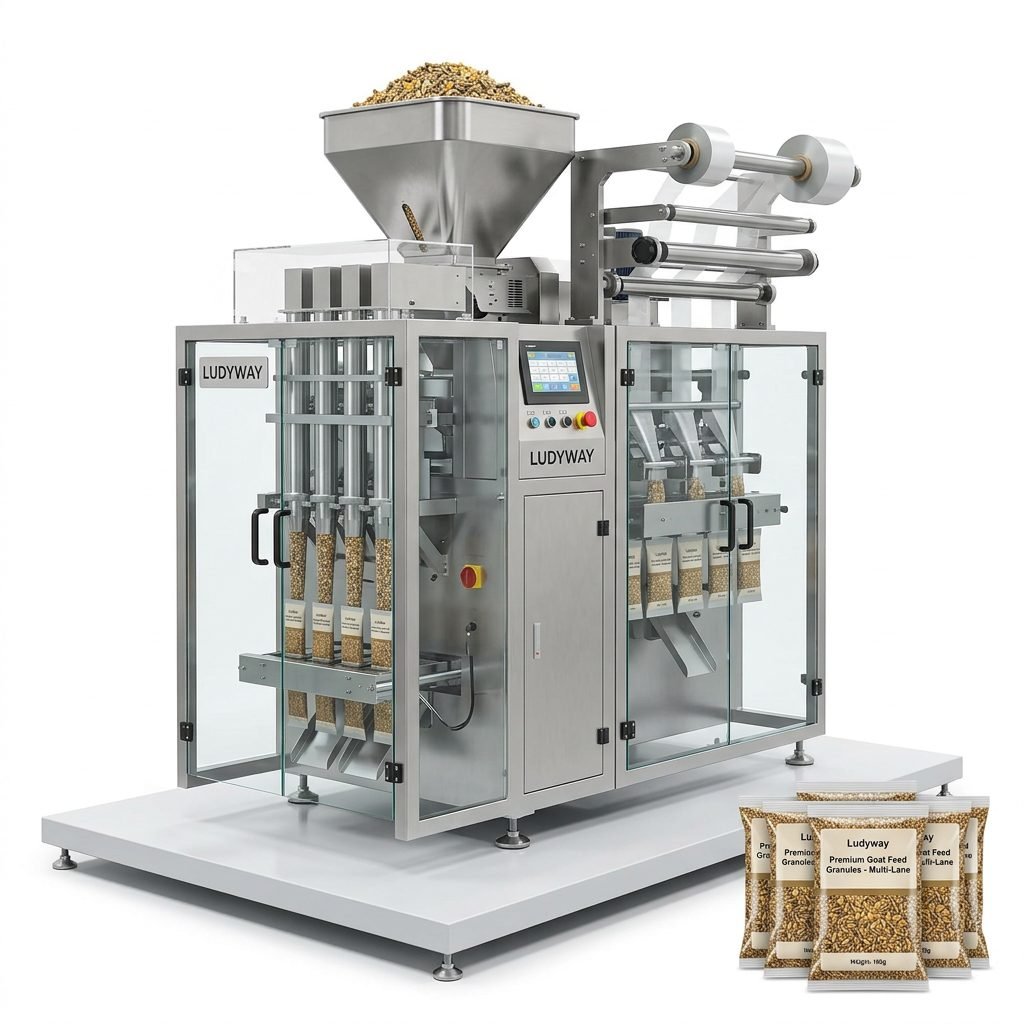
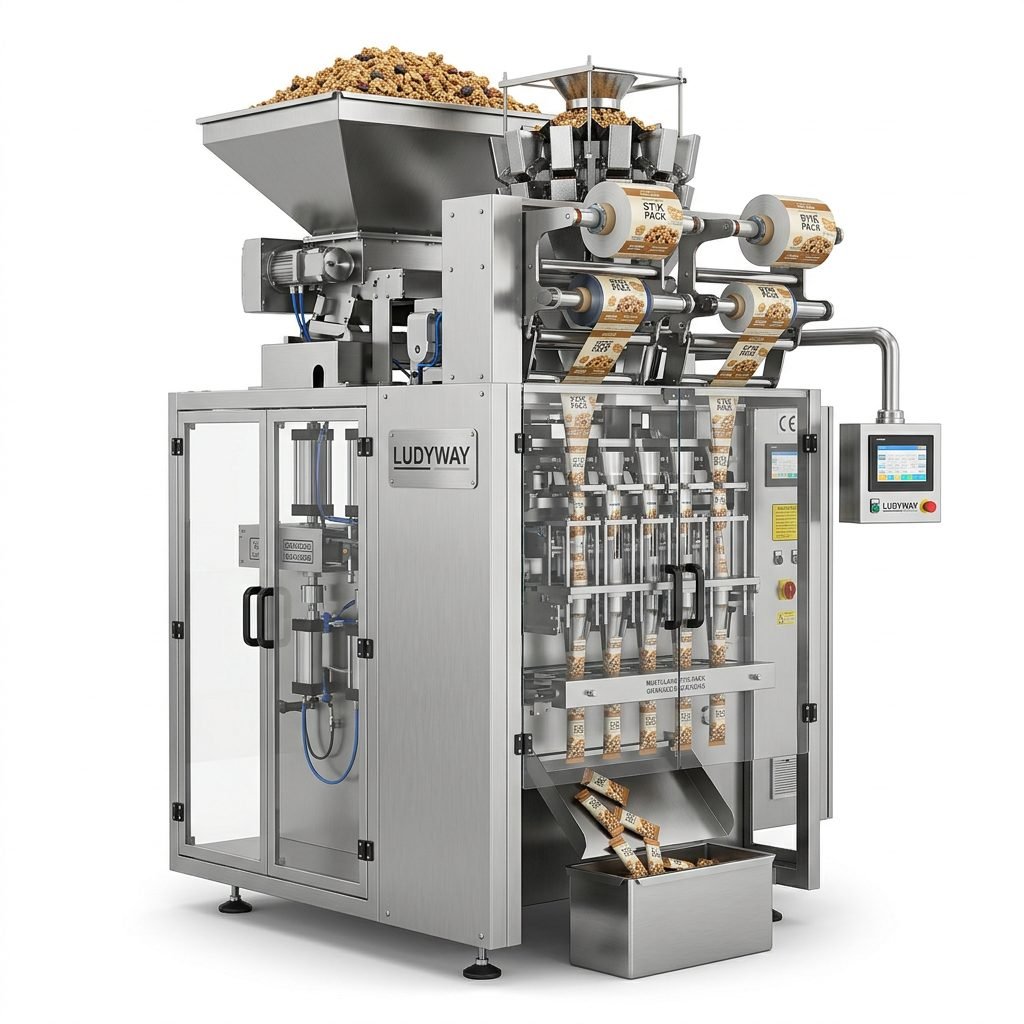
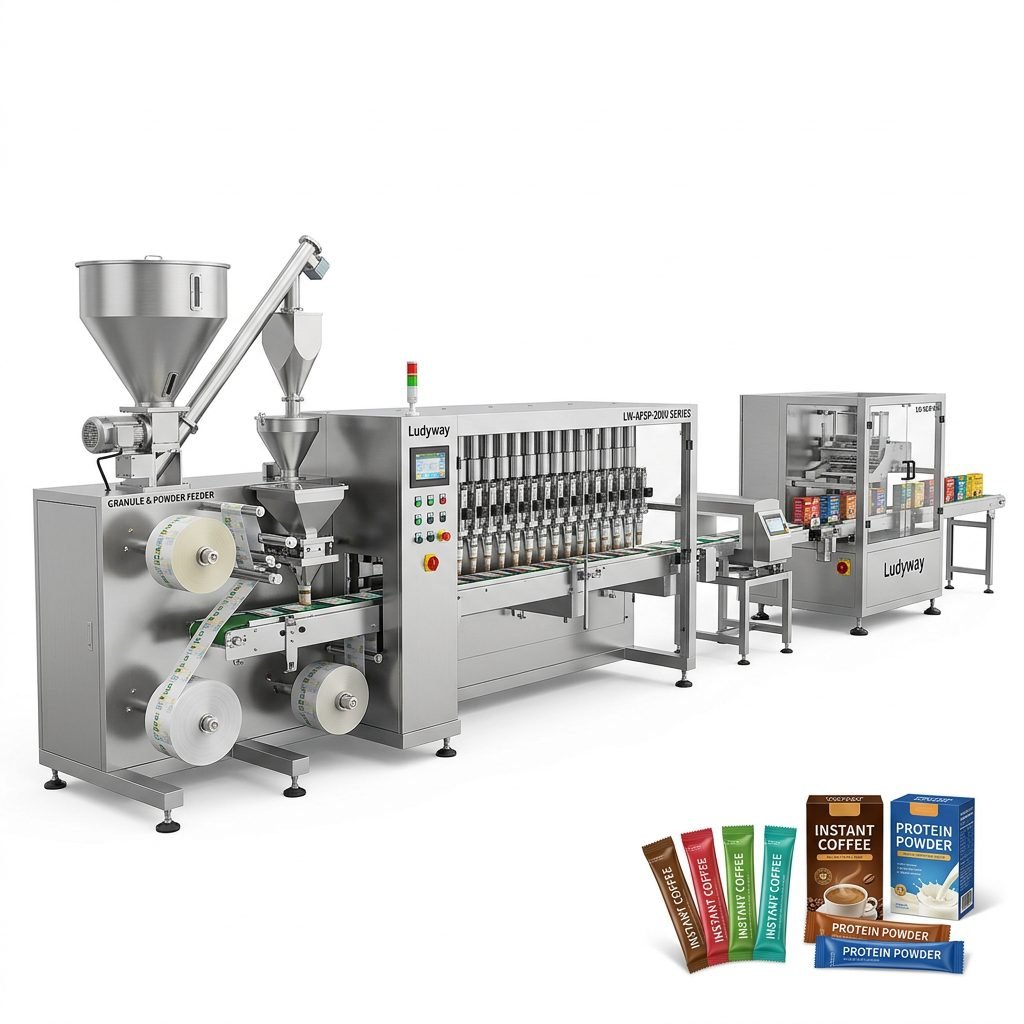
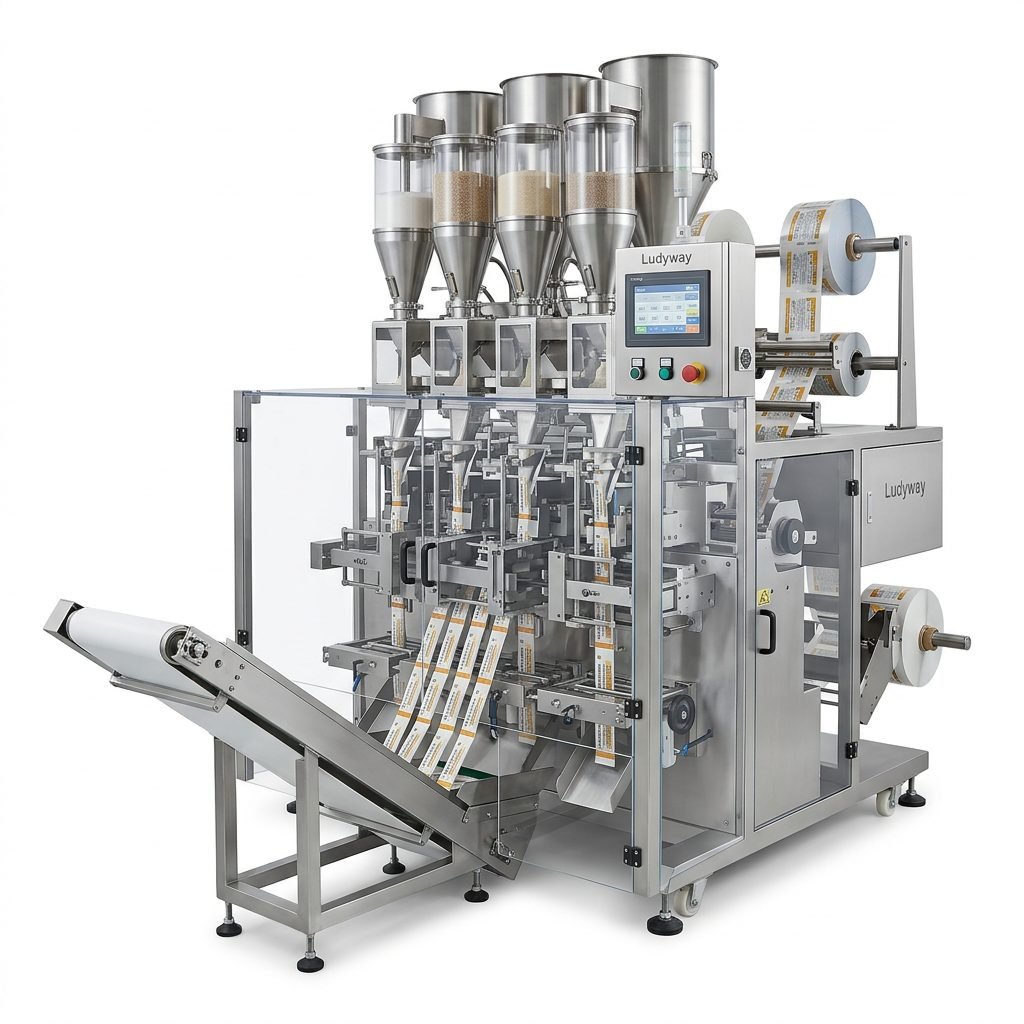
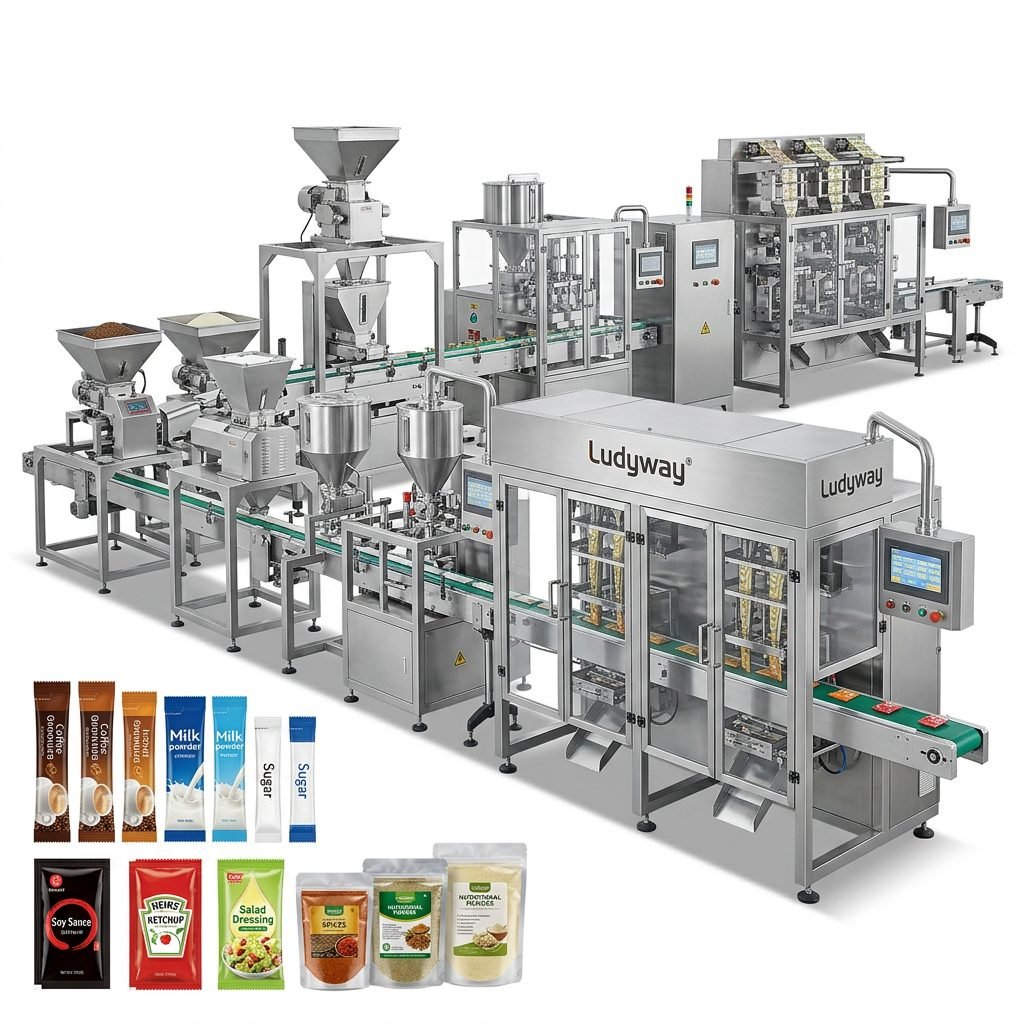
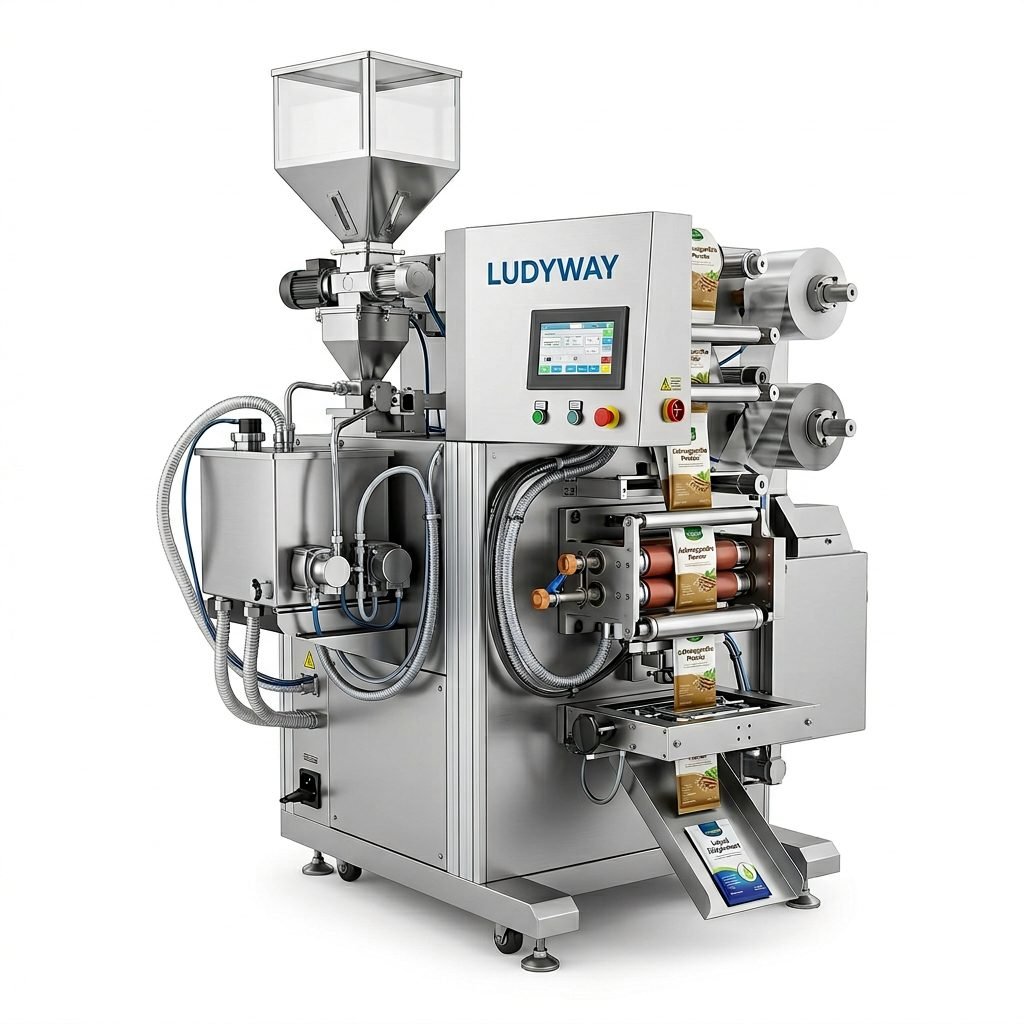
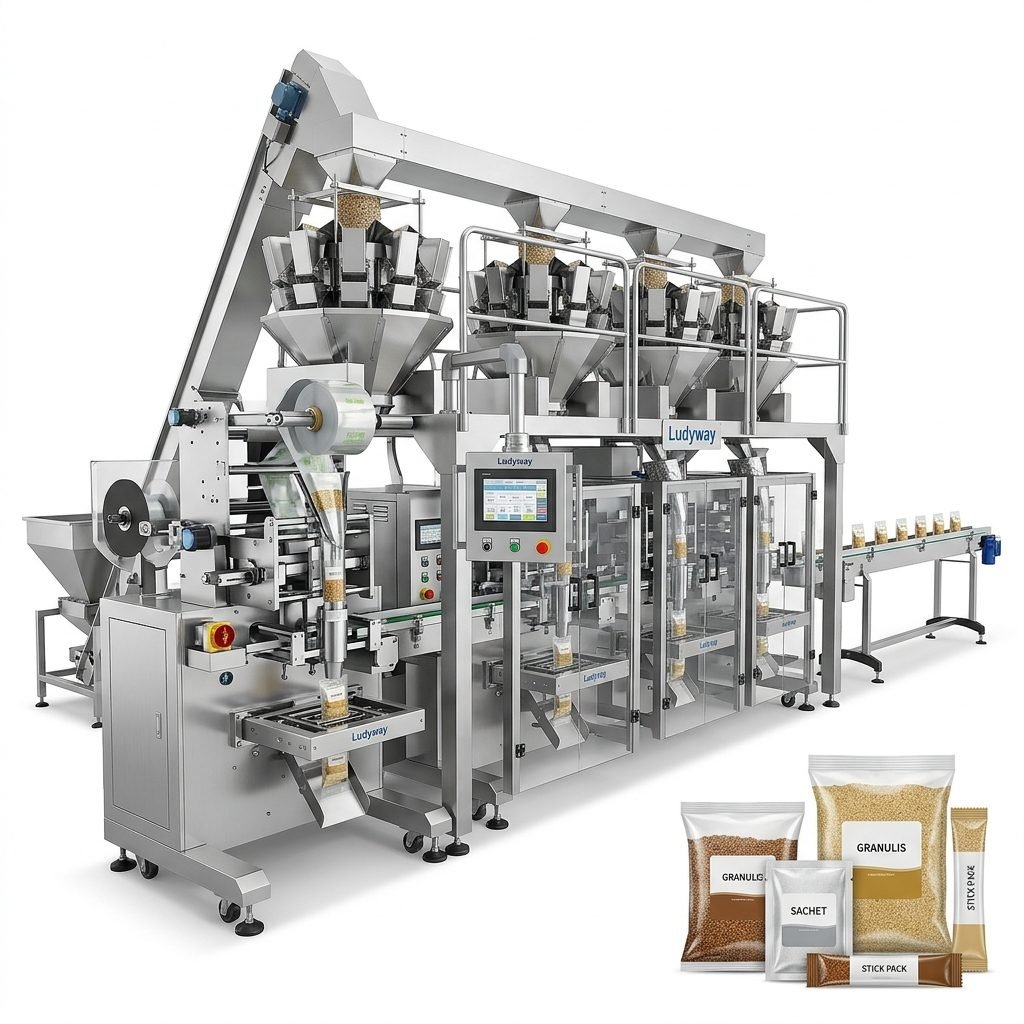
The African coffee industry is experiencing unprecedented growth. From the highlands of Ethiopia to the plantations of Kenya and Uganda, coffee producers are seeking advanced solutions to preserve freshness and extend shelf life. A high-performance coffee vacuum packaging machine is no longer a luxury—it is a necessity for any serious exporter or roaster aiming to compete in global markets.
Why Vacuum Packaging Matters for African Coffee
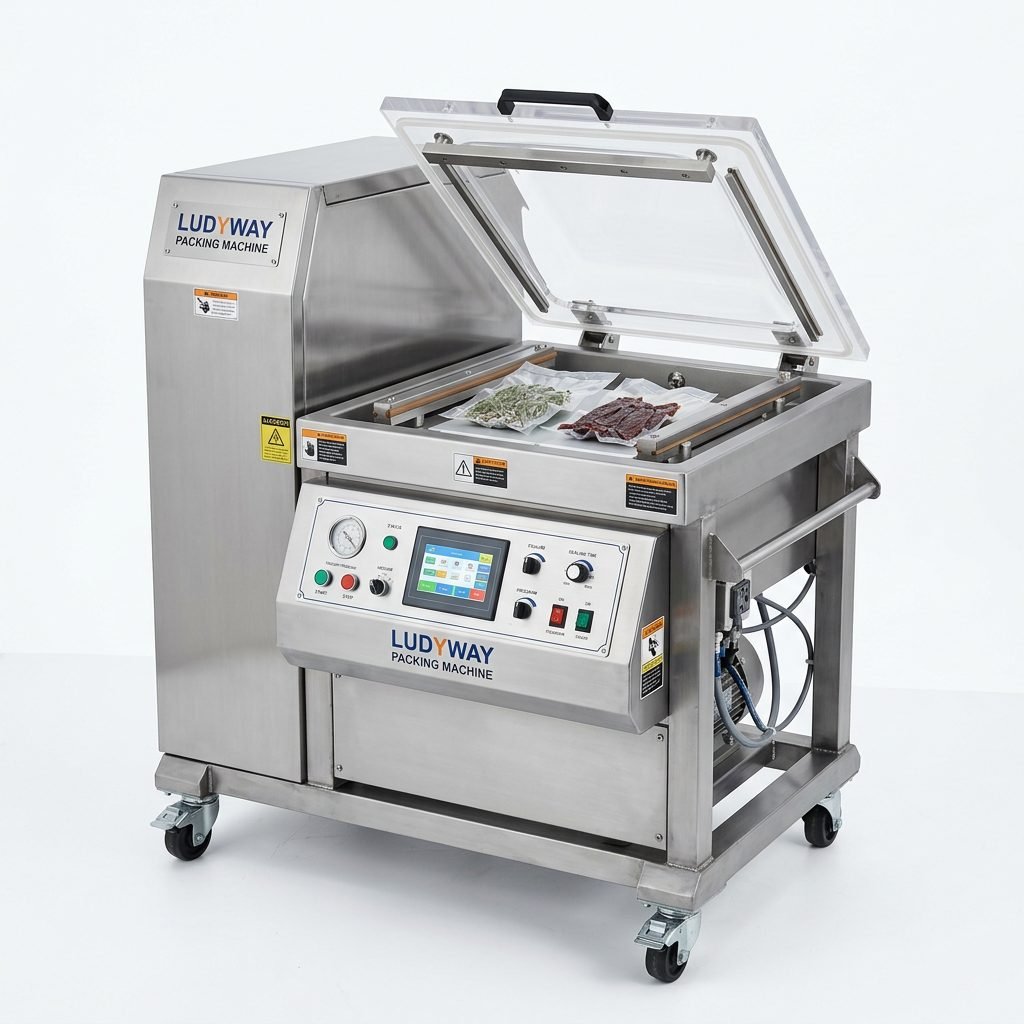
Coffee beans and ground coffee are highly sensitive to oxygen, moisture, and light. Without proper vacuum sealing, roasted coffee can lose its aroma and flavor within days. For African producers exporting to Europe, the Middle East, and beyond, a reliable vacuum packaging machine ensures that every bag arrives at its destination as fresh as the day it was packed. Vacuum technology removes oxygen from the package, dramatically slowing oxidation and preserving the volatile aromatic compounds that define premium coffee.
Key Benefits of Vacuum Sealing Coffee
- Extended Shelf Life — Vacuum-sealed coffee stays fresh for up to 12 months or longer, reducing waste and returns.
- Preserved Aroma and Flavor — Oxygen is the enemy of roasted coffee; vacuum packaging locks in the rich, complex notes African coffees are famous for.
- Enhanced Export Readiness — International buyers demand properly sealed packaging that meets stringent quality standards.
- Protection Against Contaminants — A sealed vacuum bag prevents moisture ingress, mold growth, and pest contamination during transit.
- Improved Brand Perception — Premium packaging reflects premium quality, helping African brands command higher prices.
What to Look for in the Best Coffee Vacuum Packaging Machine
Selecting the right equipment is critical for consistent results. Here are the factors that separate an average machine from an industrial-grade coffee vacuum packaging solution:
| Feature | Why It Matters for Coffee |
|---|---|
| Vacuum Strength & Consistency | Achieves deep vacuum levels to eliminate residual oxygen inside the package. |
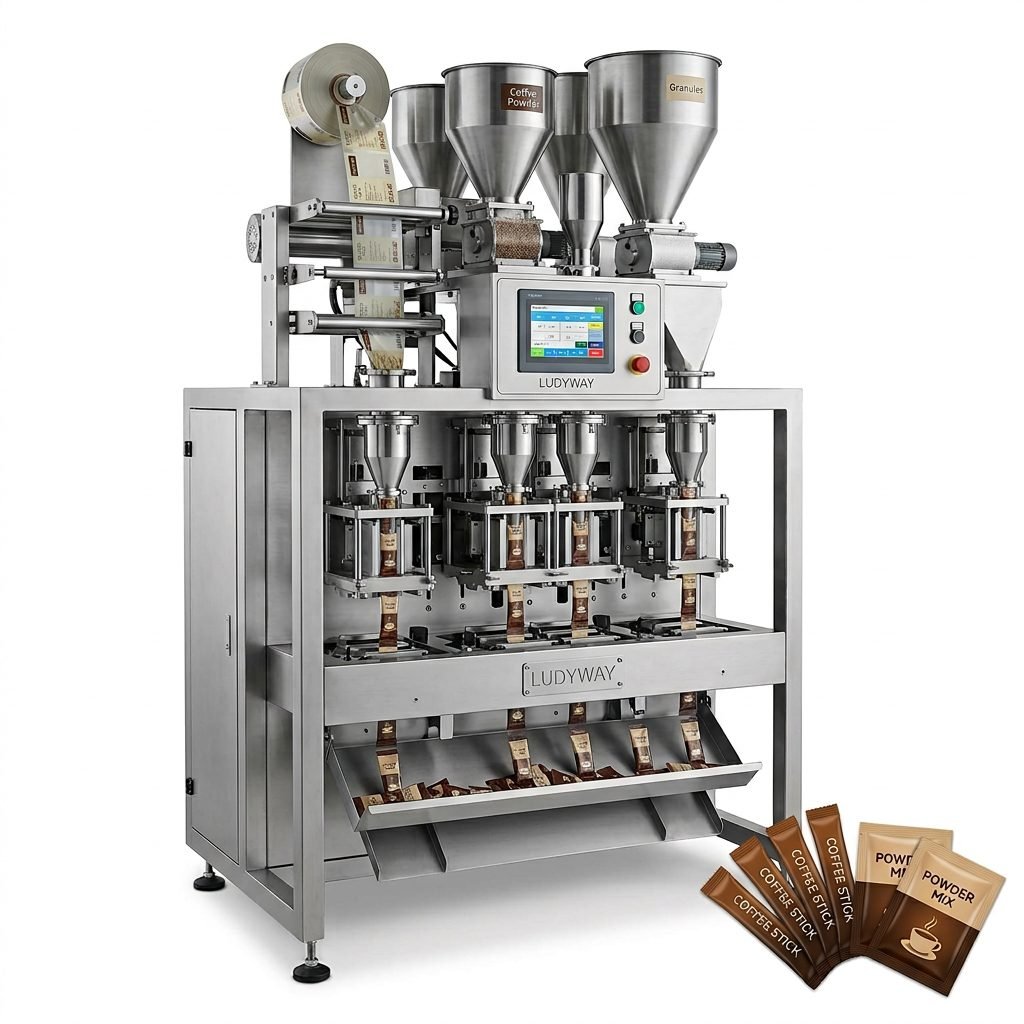
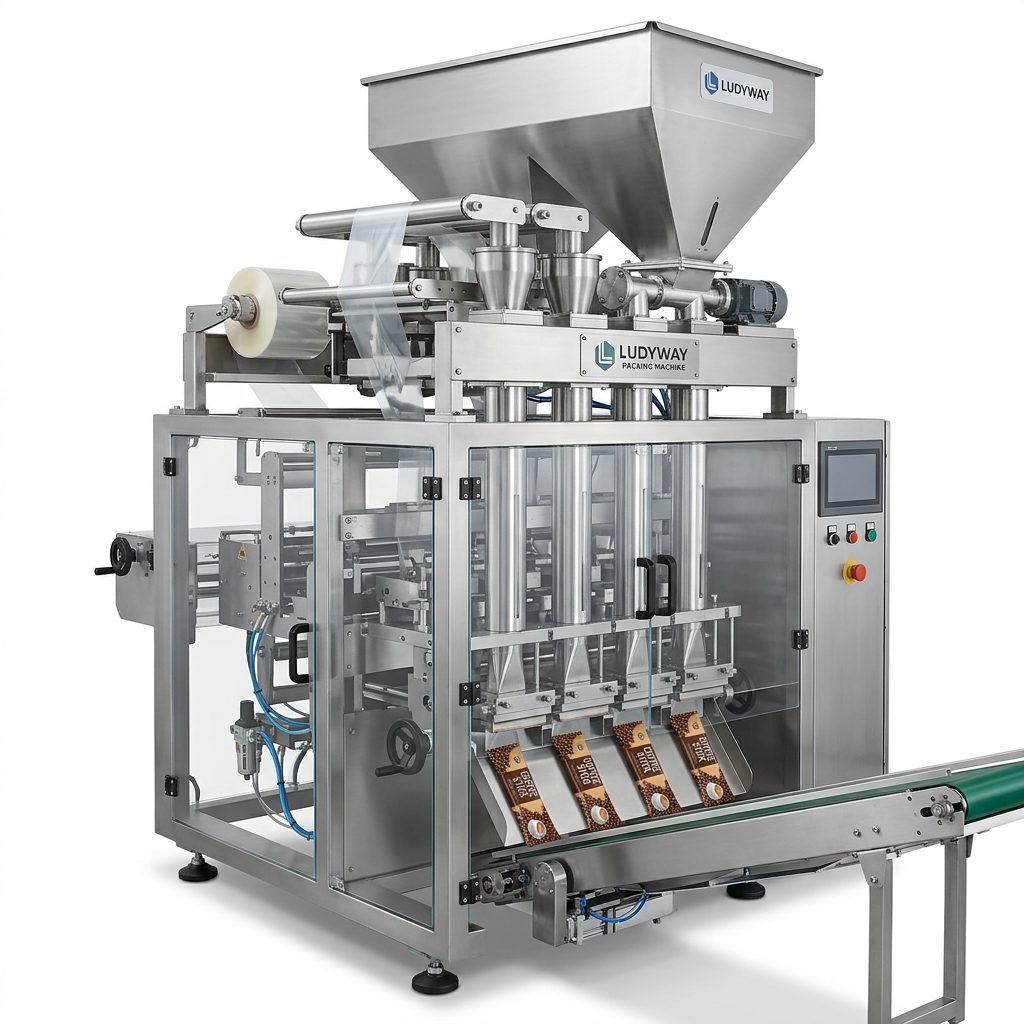
| Multi-Lane Capability | Increases throughput for high-volume African producers packing stick packs and sachets. |
| Adjustable Sealing Parameters | Accommodates different bag materials and thicknesses without compromising seal integrity. |
| Nitrogen Flushing Option | Combines vacuum with inert gas injection for maximum freshness protection. |
| Stainless Steel Construction | Ensures food-grade hygiene and durability in humid or demanding environments. |
| User-Friendly Control Interface | Simplifies operation and reduces training time for production staff. |
Why Choose Ludyway for Coffee Vacuum Packaging in Africa
When investing in packaging machinery, African coffee businesses need a partner that combines engineering excellence with practical affordability. Ludyway has emerged as a preferred choice for producers across the continent. As one of the largest packaging machine manufacturers in China, Ludyway brings over 30 years of industry expertise to every project. The company’s multi-lane packaging systems are engineered for reliability, speed, and long-term performance under demanding production conditions.
Proven Performance Across Africa
African coffee producers face unique challenges—from variable power supply to humid processing environments. Ludyway’s vacuum packaging machines are designed with robust electrical systems and corrosion-resistant components that thrive in these conditions. With installations in over 100 countries and regions, including growing adoption across East and West Africa, the track record speaks for itself.
Comprehensive Turnkey Solutions
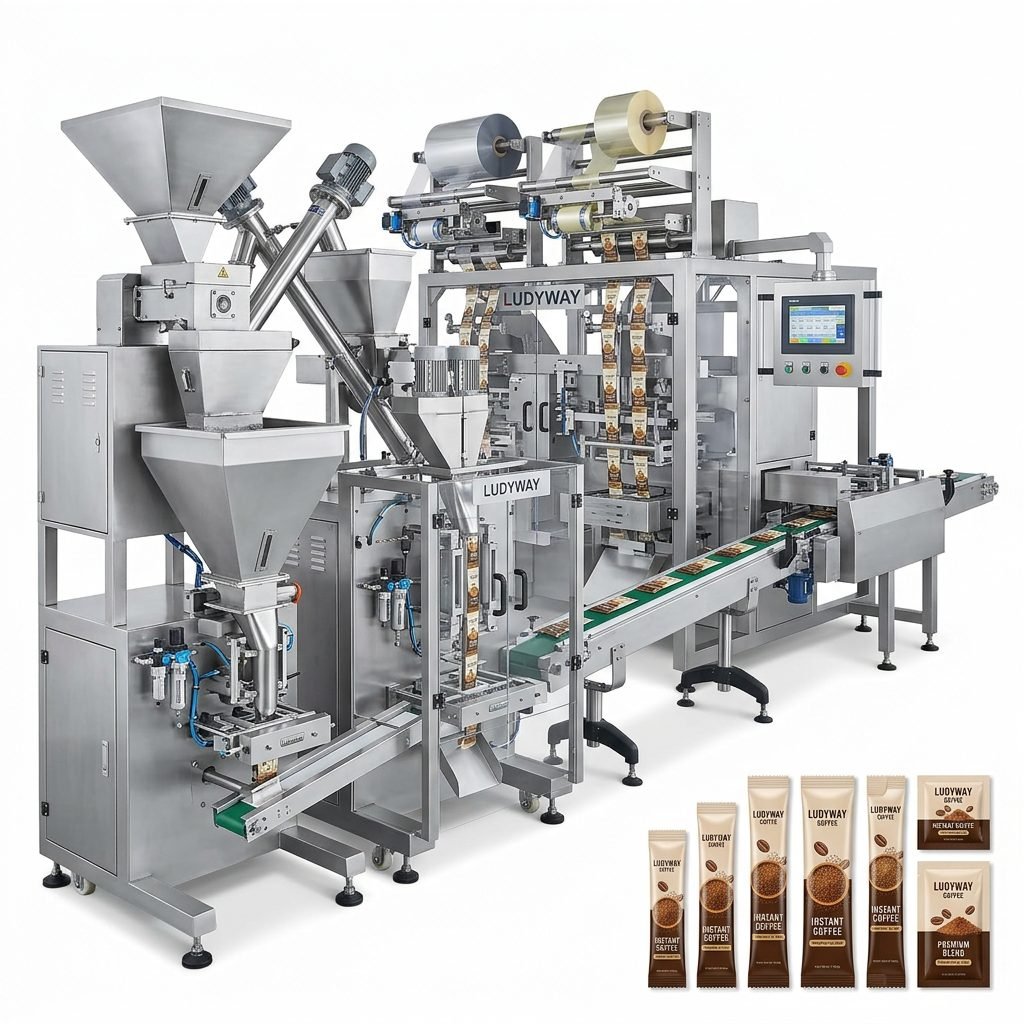
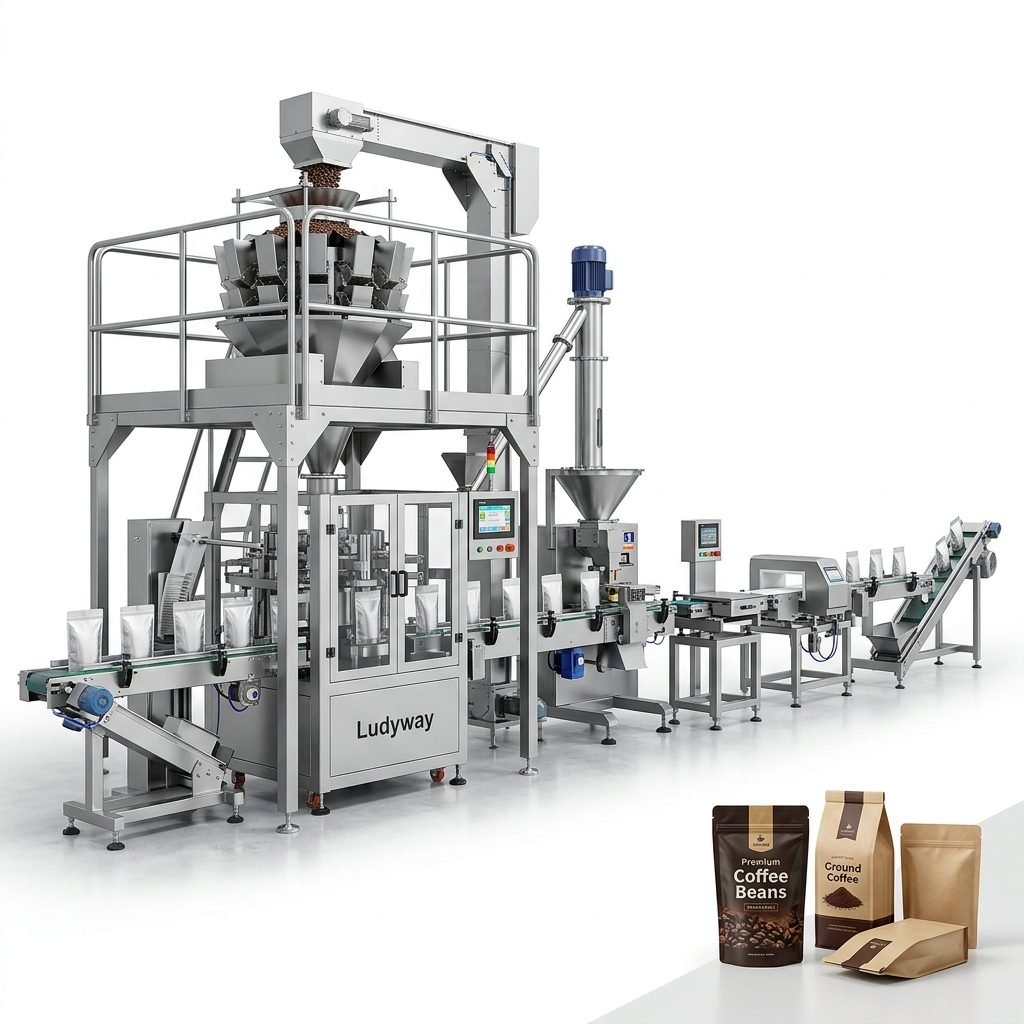
Beyond the vacuum sealer itself, Ludyway delivers complete packaging lines that integrate weighing, filling, sealing, coding, and cartoning into a seamless workflow. This turnkey approach reduces complexity for African buyers who want a single point of responsibility for their entire packaging operation. Learn more about integrated packaging line solutions that cover everything from granule and powder handling to final palletizing.
Comparing Packaging Formats for Coffee
Different market segments demand different packaging formats. Here is how vacuum technology adapts to various coffee product types:
| Coffee Product Type | Recommended Packaging Format | Vacuum Benefit |
|---|---|---|
| Whole Bean Coffee (Export) | Vacuum-sealed foil bags, 250g to 5kg | Prevents oxidation during long sea freight |
| Ground Coffee (Retail) | Vacuum stick packs and sachets | Single-serve freshness with extended shelf appeal |
| Instant Coffee Powder | Multi-lane vacuum sachet packaging | Moisture barrier protection for hygroscopic powder |
| Coffee Capsules | Individual vacuum-sealed pods | Airtight seal preserves volatile aromatics |
| Bulk Green Coffee Beans | Large-format vacuum bags, 20kg to 60kg | Controls moisture and prevents mold during storage |
Technical Excellence That Drives Results
Modern coffee vacuum packaging equipment integrates advanced features that directly impact product quality and operational efficiency. Key technical specifications to prioritize include:
- High-precision vacuum sensors that maintain consistent pressure levels across every cycle
- Multi-stage vacuum programs configurable for different bag sizes and coffee types
- Gas flushing integration allowing nitrogen backfill after vacuum for added protection
- Servo-driven sealing jaws ensuring uniform heat distribution and tamper-evident closures
- Quick-change tooling that enables fast transitions between packaging formats
Cost-Effectiveness for African Operations
Capital expenditure is a significant consideration for any African agribusiness. Investing in a high-quality vacuum packaging machine yields measurable returns through reduced product spoilage, lower return rates, and access to premium markets that demand vacuum-sealed packaging. The long-term operational savings often outweigh the initial equipment cost within the first year of operation. For businesses seeking guidance, industry resources such as the PMMI business intelligence reports provide valuable market data and packaging trends relevant to African producers.
Maintenance and After-Sales Support
Remote technical support, readily available spare parts, and clear maintenance documentation are essential for African facilities that may not have immediate access to specialized technicians. Effective after-sales infrastructure ensures maximum machine uptime and production continuity. Packaging standards and regulatory guidance are equally important—refer to ISO packaging standards for international compliance requirements, and consult FDA food packaging guidelines for markets requiring U.S. regulatory alignment.
Future-Proofing Your Coffee Packaging Line
As the African coffee sector continues its upward trajectory—driven by growing specialty coffee demand and increasing intra-African trade under the AfCFTA agreement—forward-thinking producers are upgrading their packaging capabilities now. A versatile coffee vacuum packaging machine that handles multiple formats and adapts to changing market requirements is a strategic asset that positions businesses for sustainable growth.
Whether you are a cooperative in Rwanda seeking to export single-origin specialty coffee, a roaster in Nigeria supplying the domestic retail market, or a large-scale producer in Ethiopia servicing international buyers, the right vacuum packaging technology transforms your product’s marketability and shelf presence. Explore the full range of granule and powder packaging machines designed for the unique demands of the coffee industry.
—— Equip your coffee brand with packaging that preserves quality from origin to cup ——