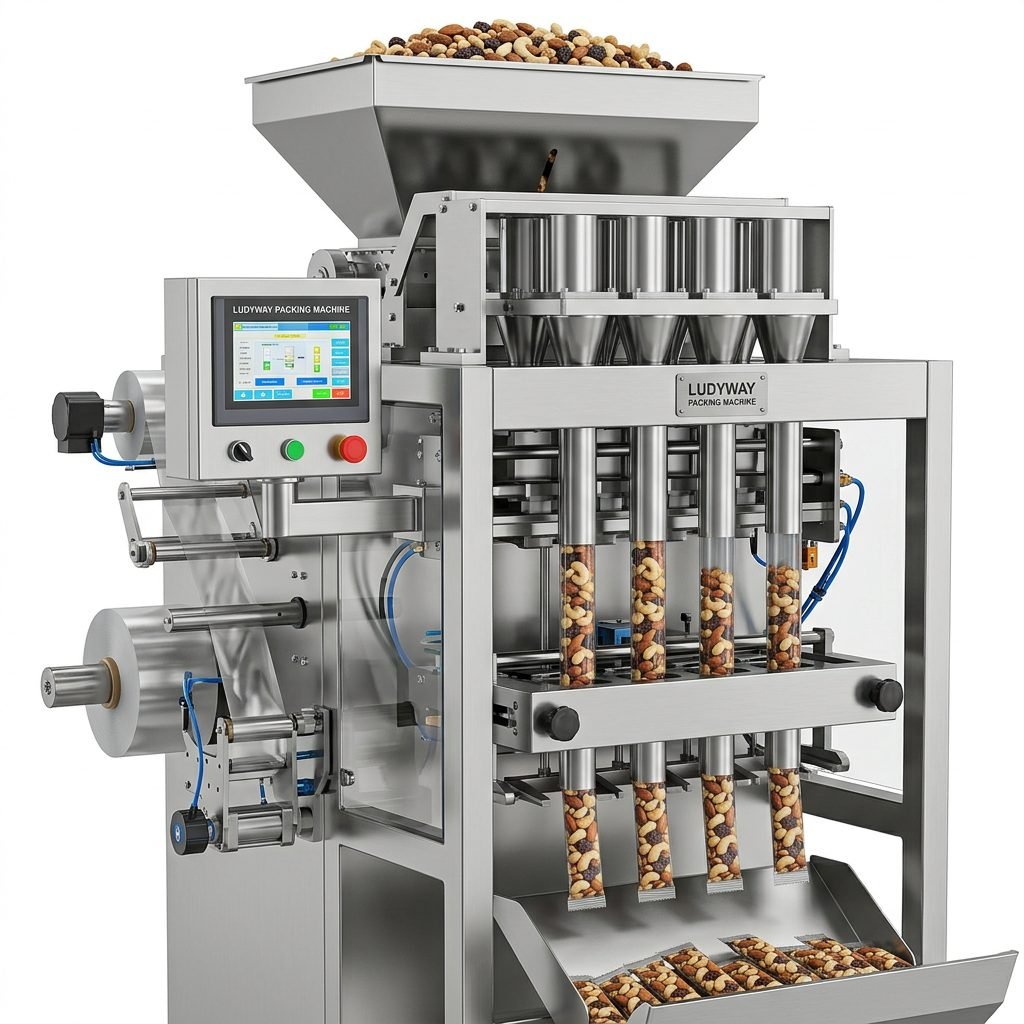
Expanding a confectionery brand into global markets requires more than just an excellent recipe. The packaging production line you choose directly impacts product shelf life, regulatory compliance, and operational efficiency across multiple regions. Setting up a confectionery packaging machine production line that meets international standards demands careful planning, from equipment selection to layout design and quality assurance protocols. This guide walks you through the essential steps to build a production line ready for worldwide distribution.
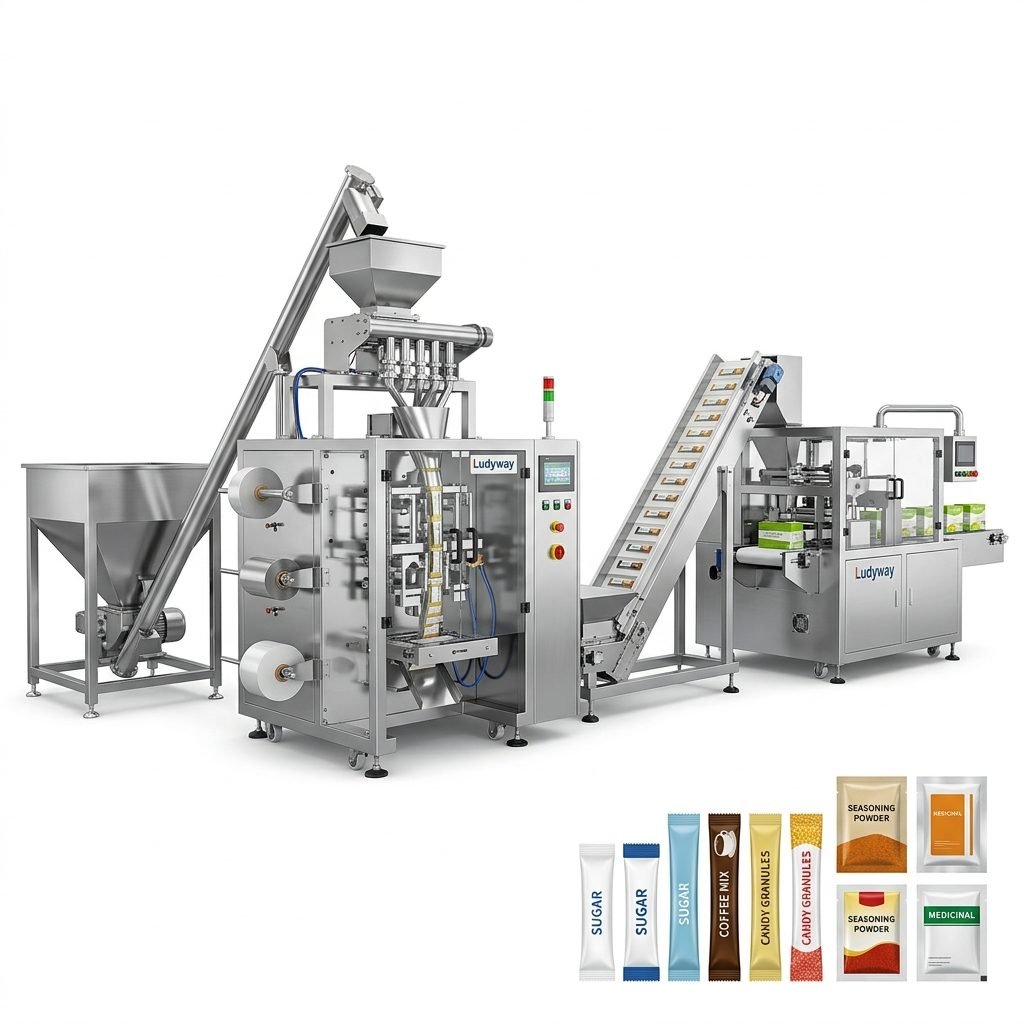
Understanding Global Market Requirements
Before purchasing any equipment, you must evaluate the specific needs of your target regions. Different markets impose distinct regulatory frameworks that influence packaging material choices, labeling requirements, and machine certifications. The FDA food contact substance regulations in North America differ significantly from European packaging waste directives, and both require careful attention during line configuration.
Key factors to assess include:
- Product format variations — stick packs, sachets, pouches, or flow-wrapped pieces for different regional preferences
- Shelf-life expectations — barrier film requirements, nitrogen flushing, or vacuum sealing capabilities
- Labeling compliance — multi-language printing, allergen declarations, and nutritional fact formats
- Sustainability mandates — recyclable or compostable material compatibility mandated by certain regions
- Production volume targets — whether you need a single high-speed line or multiple parallel systems
Key Equipment for a Confectionery Packaging Line
A high-performance confectionery packaging line typically integrates several specialized machines that work in synchronized sequence. Selecting the right combination of equipment determines your throughput capacity and product consistency.
Multi-Lane Stick Pack and Sachet Machines
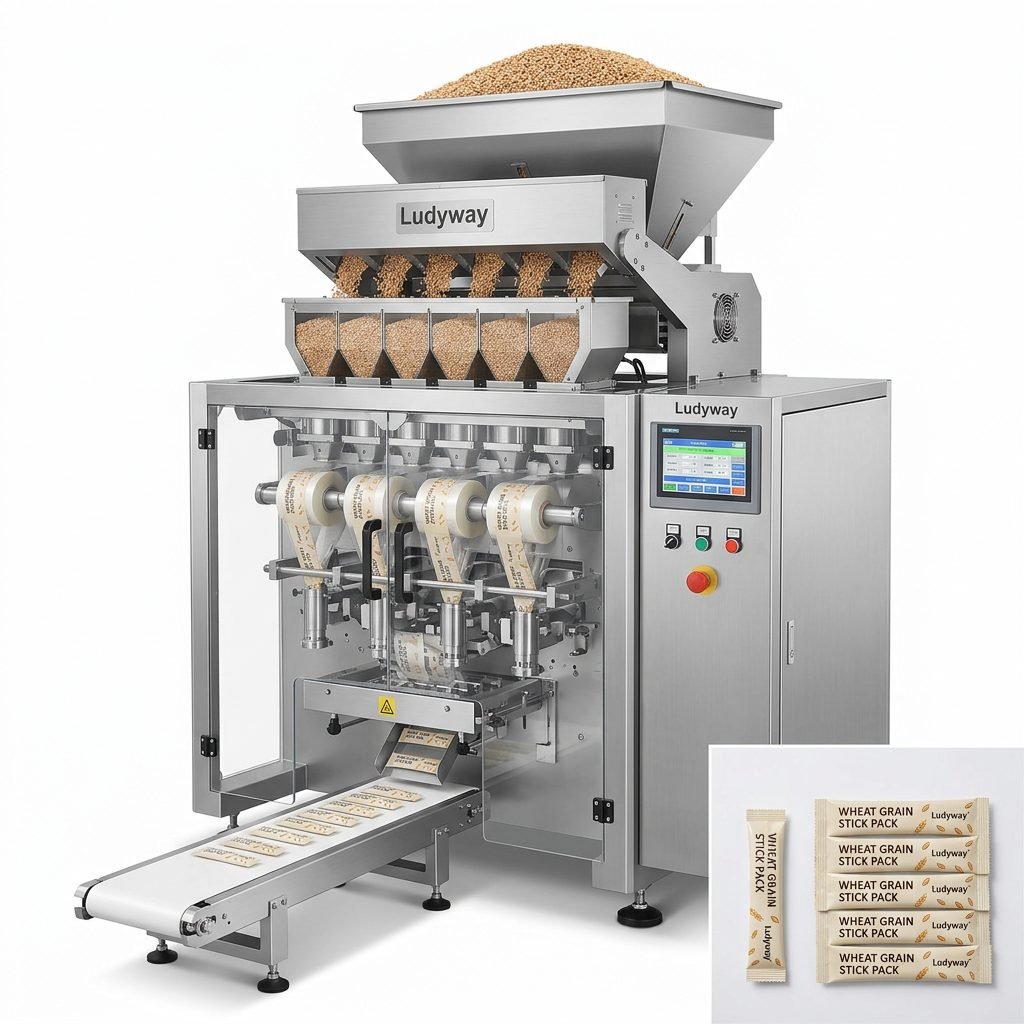
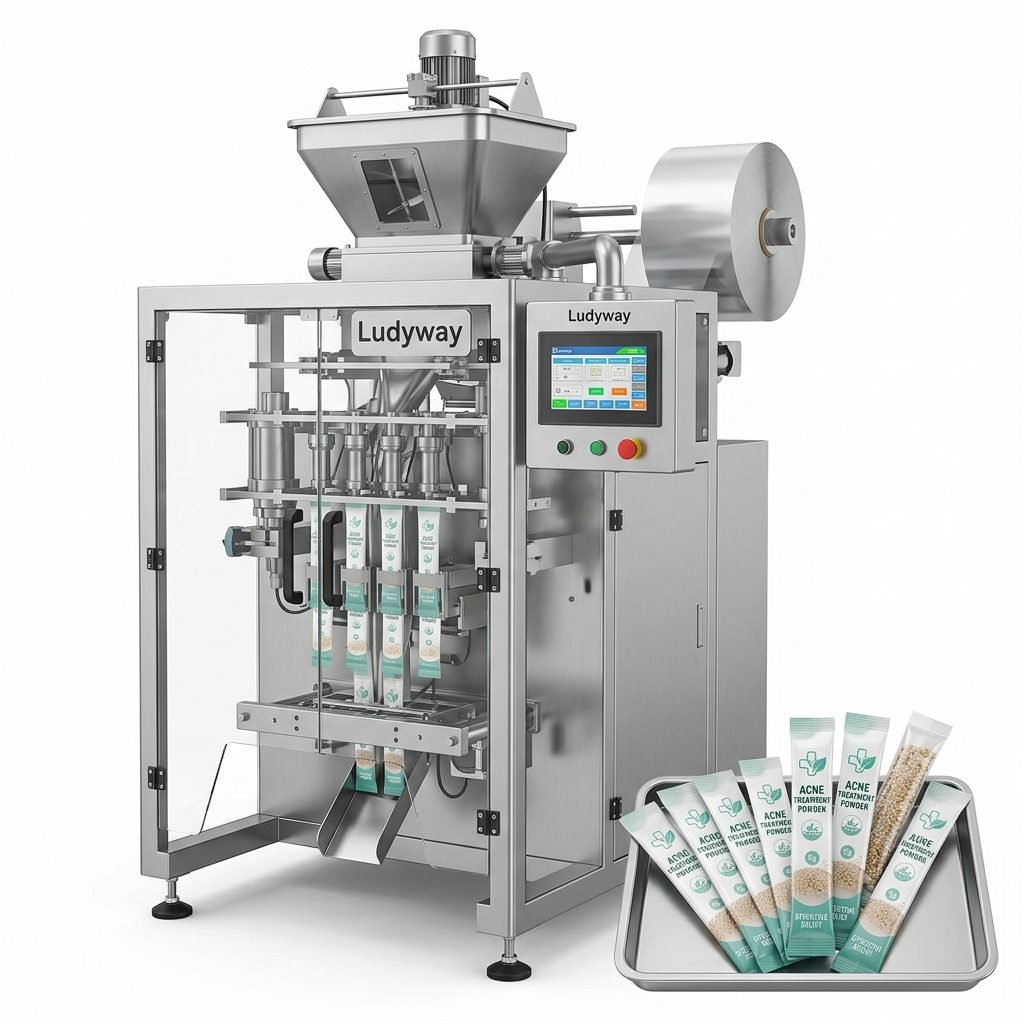
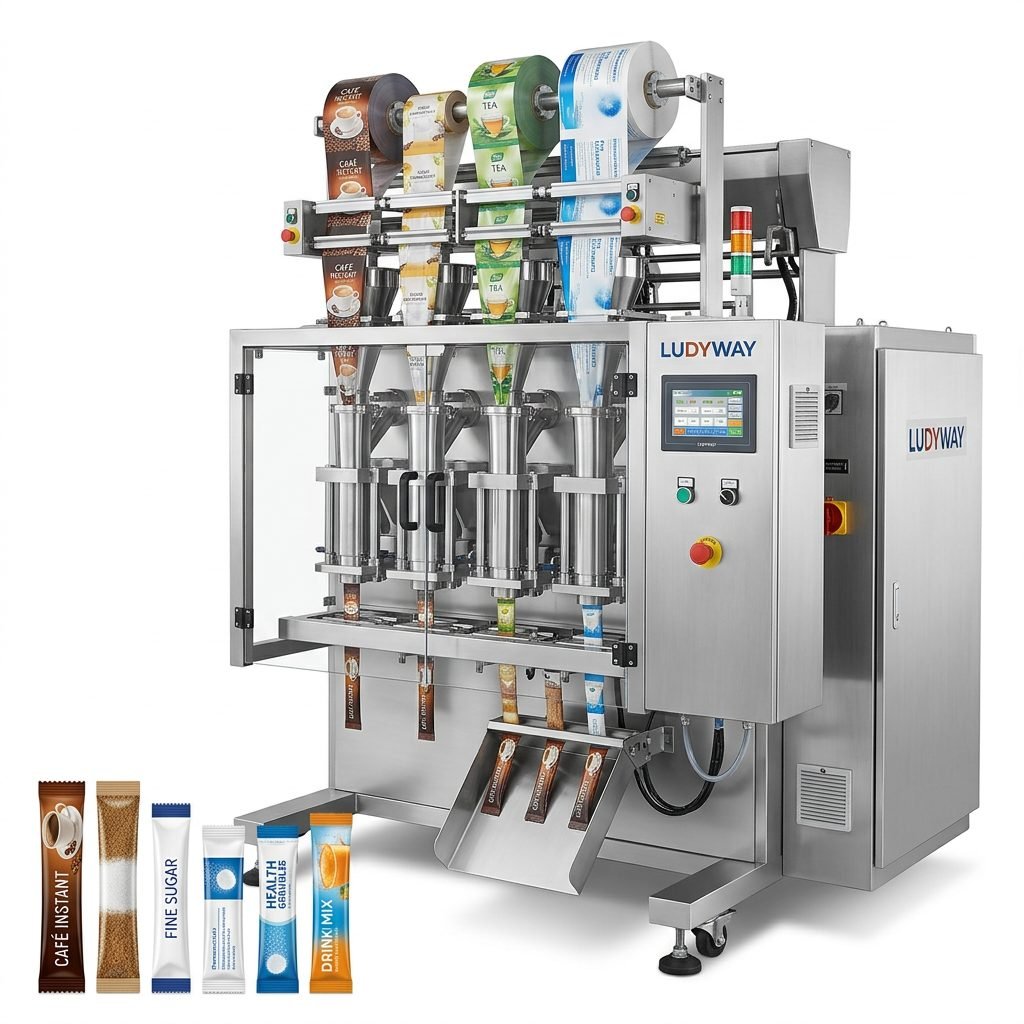
For powdered drink mixes, granulated sugar confections, and single-serve candy portions, multi-lane stick pack machines offer unmatched efficiency. These systems can run 4 to 12 lanes simultaneously, dramatically increasing output while maintaining precise fill weights. Look for models with servo-driven sealing jaws and automatic film tracking to minimize waste during format changes.
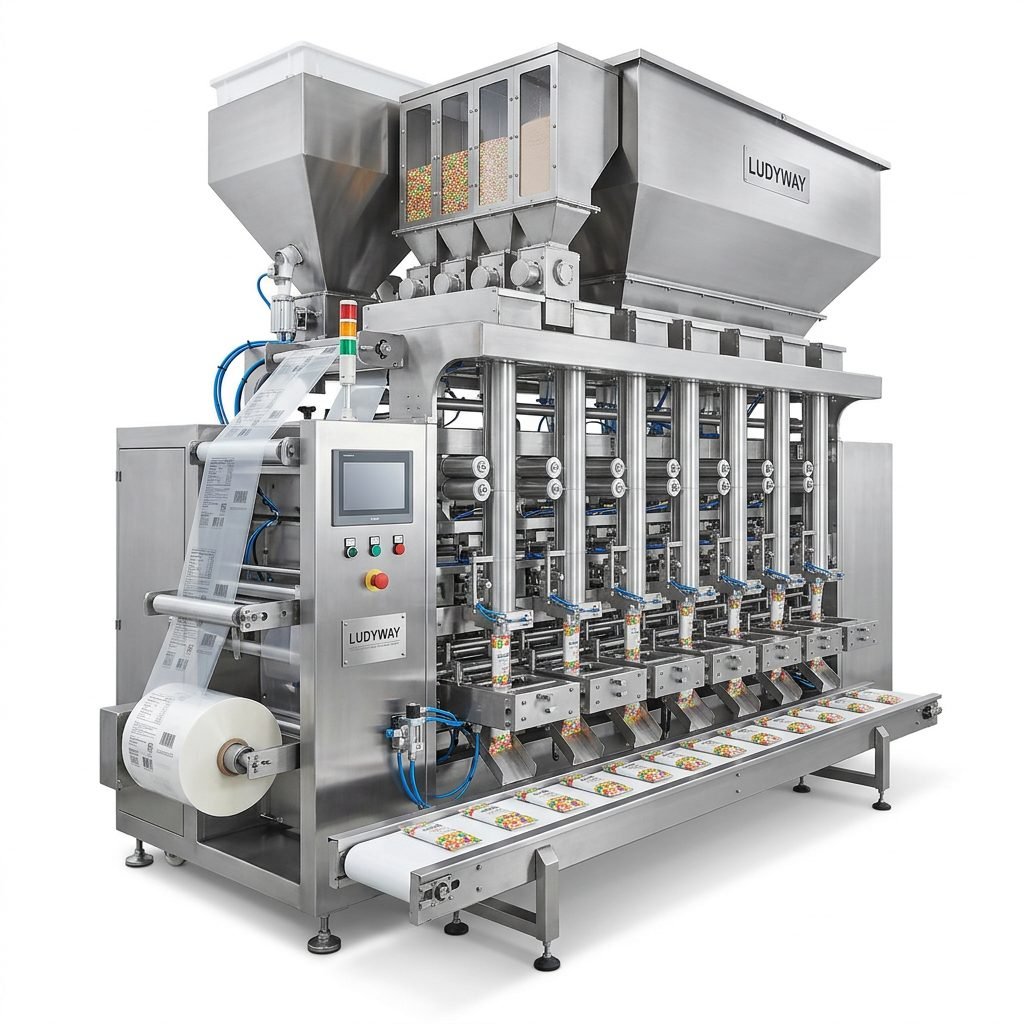
Automated Weighing and Filling Systems
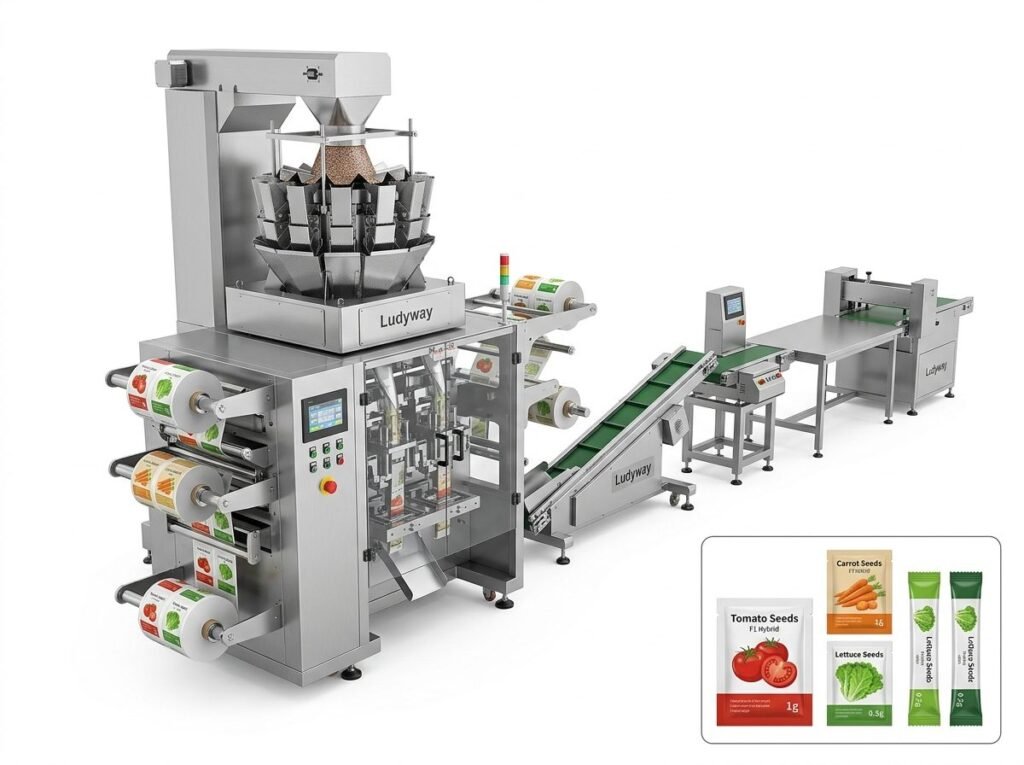
Accurate portioning is critical for cost control and regulatory compliance. Multi-head weighers with precision load cells can handle various confectionery products — from gummy candies and hard-boiled sweets to chocolate-coated nuts. Combination weighers calculate the optimal weight combination in milliseconds, ensuring each package meets the declared net weight with minimal giveaway.
Flow Wrapping and Pouch Packaging
For bars, blocks, and individually wrapped pieces, horizontal flow wrappers provide hermetic seals that extend shelf life. When combined with automatic feeding systems, these machines can achieve speeds exceeding 800 packs per minute. Pouch packaging machines with zipper applicators or resealable features add consumer convenience increasingly demanded in premium global markets.
Ensuring Compliance with International Standards
Global packaging operations must adhere to recognized ISO packaging standards and regional certification requirements. The table below summarizes key standards that affect confectionery packaging line setup:
| Standard | Scope | Applicable Regions |
|---|---|---|
| ISO 22000 | Food safety management systems | Global |
| FDA 21 CFR Part 110 | Current Good Manufacturing Practice | United States |
| EU Regulation 1935/2004 | Materials intended for food contact | European Union |
| BRCGS Packaging | Packaging materials safety and quality | Global (retailer recognized) |
| ISO 11607 | Packaging validation for sterile products | Global |
Production Line Layout and Workflow Optimization
An efficient confectionery production floor layout minimizes material handling distances and reduces contamination risks. The ideal arrangement follows a logical flow from raw material receiving to finished goods dispatch. Consider these layout principles when designing your line:
- Zoning by hygiene level — separate raw ingredient handling areas from finished product zones to prevent cross-contamination
- Linear material flow — arrange equipment so products move in one direction without backtracking, reducing labor and forklift traffic
- Utility access planning — position machines with easy access to compressed air, electrical connections, and dust extraction systems
- Ergonomic operator stations — design inspection points and manual packing stations at comfortable working heights with adequate lighting
- Future expansion space — reserve floor area for additional lanes or downstream equipment as production scales
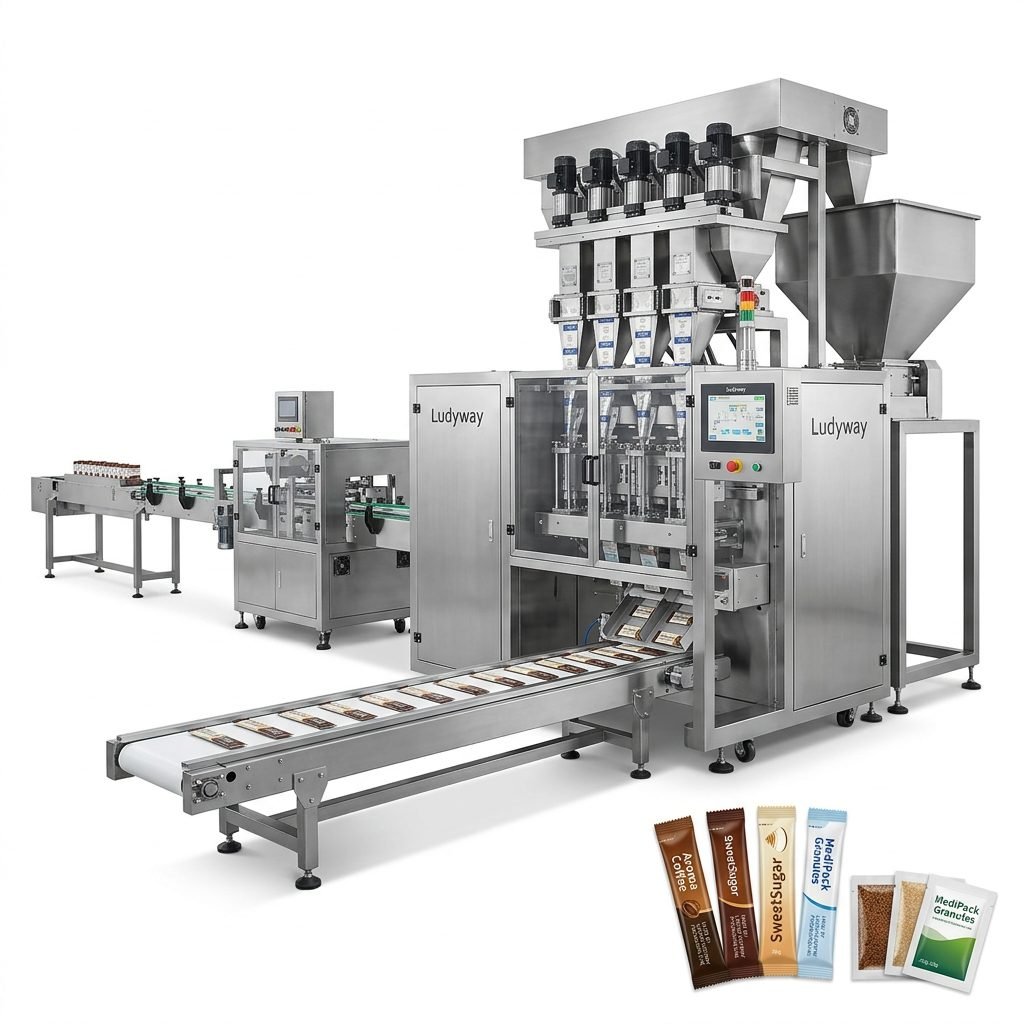
Integration and Automation Technologies
Modern confectionery packaging lines leverage Industry 4.0 technologies to enhance productivity and traceability. Integrating real-time monitoring systems allows plant managers to track Overall Equipment Effectiveness (OEE), detect anomalies early, and schedule predictive maintenance. Automated changeover systems reduce downtime between product runs — a critical capability for manufacturers serving diverse international markets with varying SKU requirements.
Advanced features worth evaluating include:
- Vision inspection systems for seal integrity verification and label placement accuracy
- Serialization and track-and-trace capabilities for markets requiring unit-level traceability
- Remote diagnostic access enabling OEM support teams to troubleshoot without on-site visits
- IoT-enabled sensors that feed production data into centralized ERP and MES platforms
Quality Control and Testing Protocols
A robust quality assurance program is non-negotiable for global market access. Implement inline checkweighers to reject underweight or overweight packages in real time. Metal detectors and X-ray inspection systems should be positioned after the filling station to catch physical contaminants before products reach secondary packaging. Leak testing equipment — particularly for modified atmosphere packaging — ensures seal integrity throughout the distribution chain.
Documentation of quality procedures is equally important. Maintain detailed records of machine calibration, cleaning schedules, and batch testing results to satisfy auditor requirements under industry best practices and regulatory frameworks.
Training, Maintenance, and After-Sales Support
Even the most advanced packaging line will underperform without proper operator training and maintenance procedures. Invest in comprehensive training programs covering machine operation, troubleshooting, and changeover procedures. Establish a preventive maintenance schedule based on manufacturer recommendations and actual usage hours. Partnering with an experienced packaging equipment manufacturer that offers responsive after-sales support — including spare parts availability, remote technical assistance, and on-site service — significantly reduces costly downtime.
When evaluating suppliers, inquire about their international service network. A manufacturer with a global presence can dispatch technicians quickly to your facility regardless of location. Ludyway, with its extensive international operations and commitment to customer success across more than 100 countries, exemplifies the type of partner that helps confectionery brands scale globally with confidence.
Preparing Your Line for Launch
Before commencing full-scale production, conduct Factory Acceptance Testing (FAT) at the equipment manufacturer’s facility, followed by Site Acceptance Testing (SAT) after installation. Run production trials using actual packaging materials and representative products to validate speed, accuracy, and seal quality. Address any deviations before committing to commercial orders destined for international customers.
Setting up a confectionery packaging machine production line for global markets is a significant investment, but one that pays dividends through expanded market access, reduced per-unit costs, and superior product presentation. By carefully evaluating equipment options, ensuring regulatory compliance, optimizing layout, and integrating smart technologies, you position your brand to compete effectively on the world stage.