
Home / Products / Packaging Machine / Packaging Auxiliary Equipment / Vertical Bucket Elevator for Granules & Powders – High Capacity Conveying System
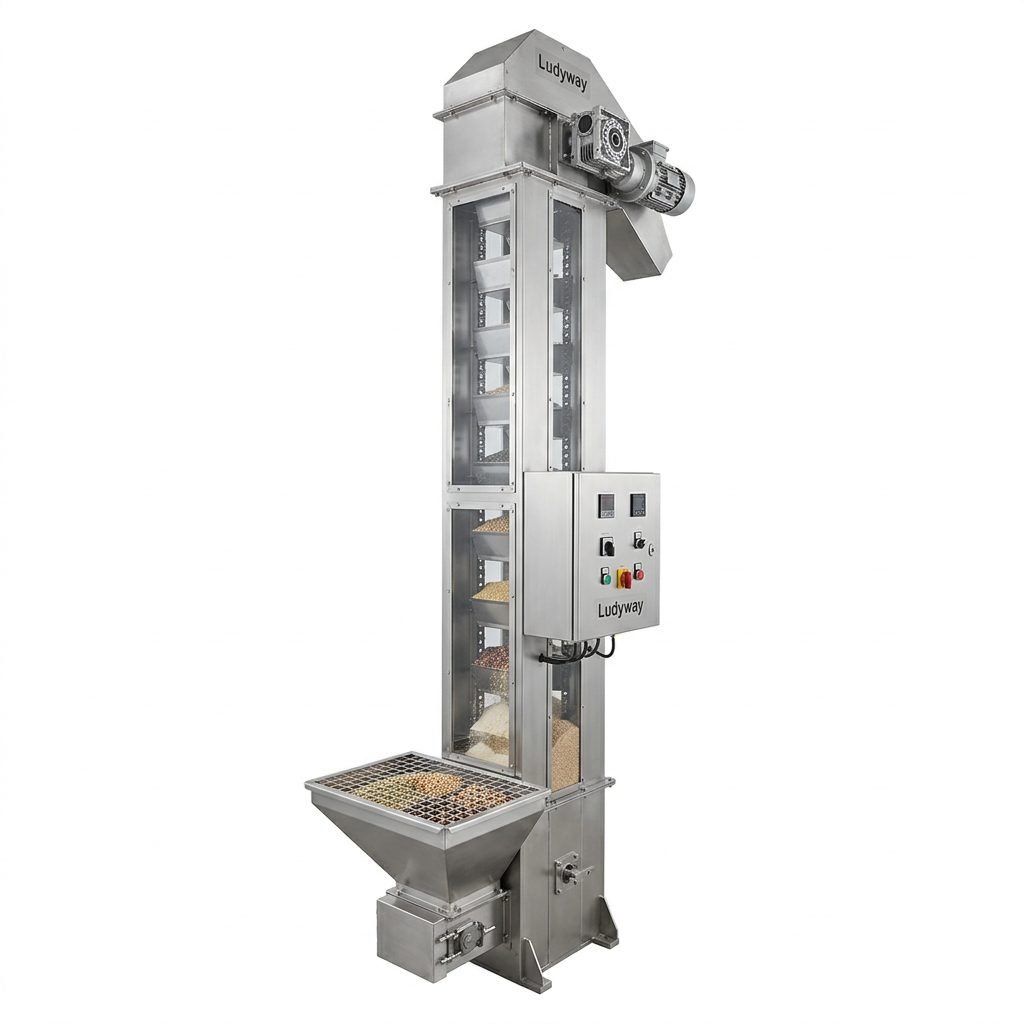
Our Vertical Bucket Elevator is a robust and highly efficient material handling solution engineered for the continuous vertical lifting of bulk materials such as granules, powders, pellets, and small aggregates. Designed for industrial applications where floor space is at a premium, this system excels in moving materials between different process levels with minimal footprint and maximum reliability. It is the cornerstone of a streamlined production line, ensuring a consistent and controlled flow of materials to silos, mixers, packaging machines, or other processing stages. Built with durability and low maintenance in mind, this elevator is an essential investment for industries seeking to optimize their conveying operations for both productivity and long-term operational cost savings.
The Vertical Bucket Elevator stands out due to its superior engineering and user-centric design. Key features include:
The following table outlines the standard technical parameters for our Vertical Bucket Elevator series. Custom specifications are available upon request to meet unique application needs.
| Parameter | Specification |
|---|---|
| Model Series | VBE-200, VBE-300, VBE-500, VBE-800 |
| Conveying Capacity | Up to 100 cubic meters per hour |
| Lifting Height | 5 to 30 meters (Custom heights available) |
| Bucket Material | Mild Steel, Stainless Steel 304/316, Polyethylene |
| Drive Power | 3 kW to 22 kW (Depending on model & capacity) |
| Operating Speed | 0.8 – 1.6 m/s |
| Inlet & Outlet Options | Customizable flanges to match your process equipment |
| Control System | Standard manual control; Optional PLC-based automation with sensors |
This versatile Vertical Bucket Elevator is indispensable across a wide spectrum of industries that require reliable vertical transport of bulk solids.
Tag: Filling Machine, Granule Packing Machine, Industrial Packing Machine, Packaging Machine, Powder Packing Machine
Our experts are ready to help you choose the right machine.

A liquid unit dose packaging machine is designed to form, fill, and seal single-use portions of liquid products into compact, hygienic packs such as sachets,
Short answer: The best vacuum packaging machine suppliers for commercial and industrial use are those that combine stable sealing performance, food-grade or pharmaceutical-grade build quality,
In modern food, pharmaceutical, nutraceutical, and chemical production, a powder sachet packaging machine plays a critical role in delivering fast output, precise dosing, and dependable

Our experts are available 24/7 to support you. Whatever packaging solution you need, we can design and manufacture it to meet your exact requirements.
Our specialists will get back to you within 10 minutes.
Ludyway
Packaging Machine
Hello!
How can we help you? Our sales team is available 24/7 to assist you!