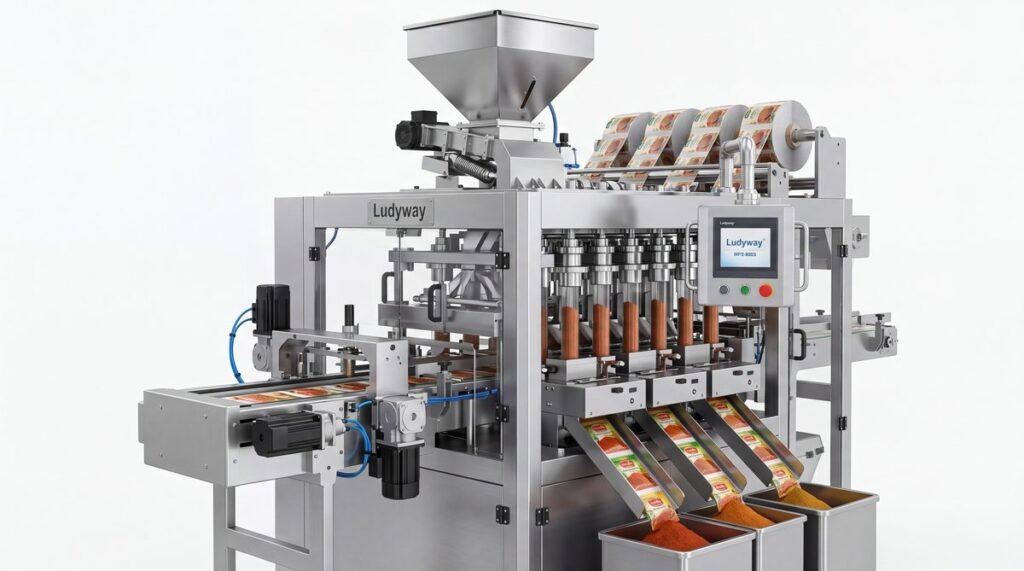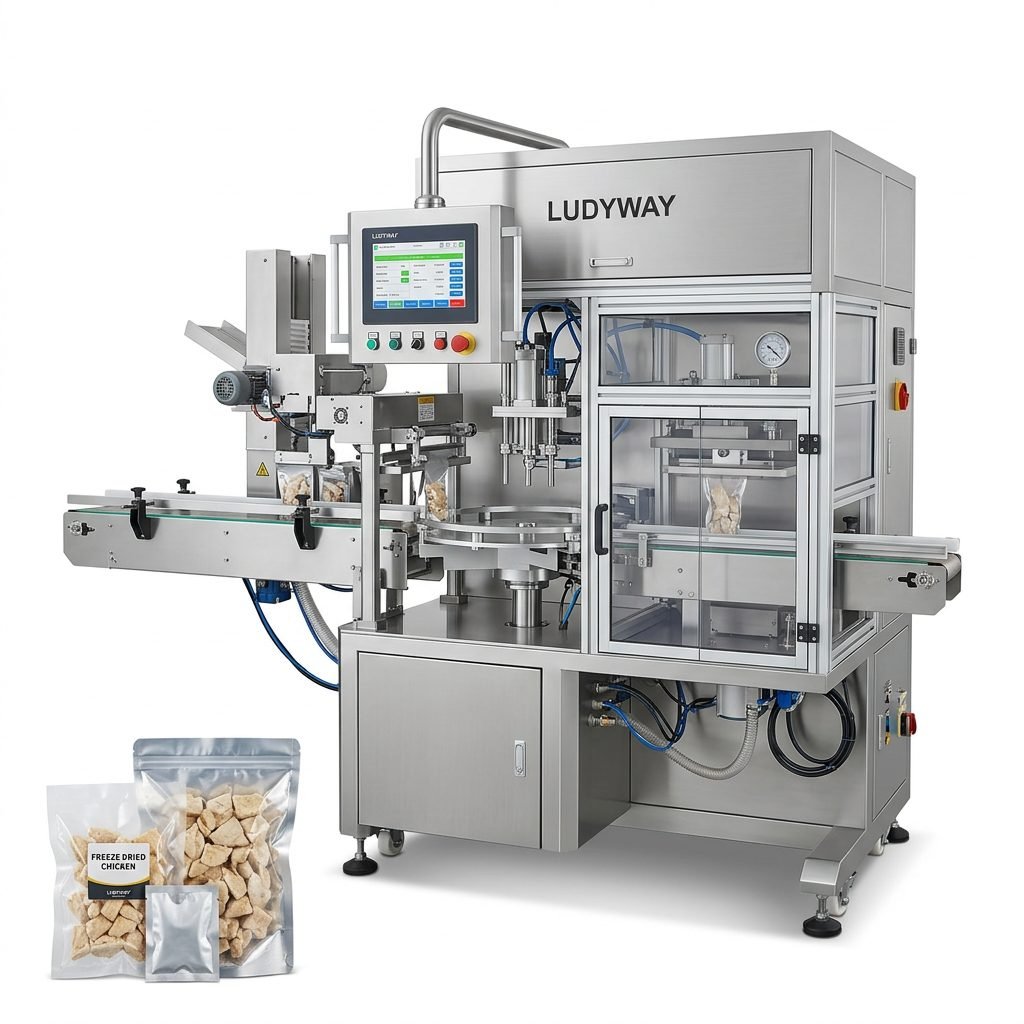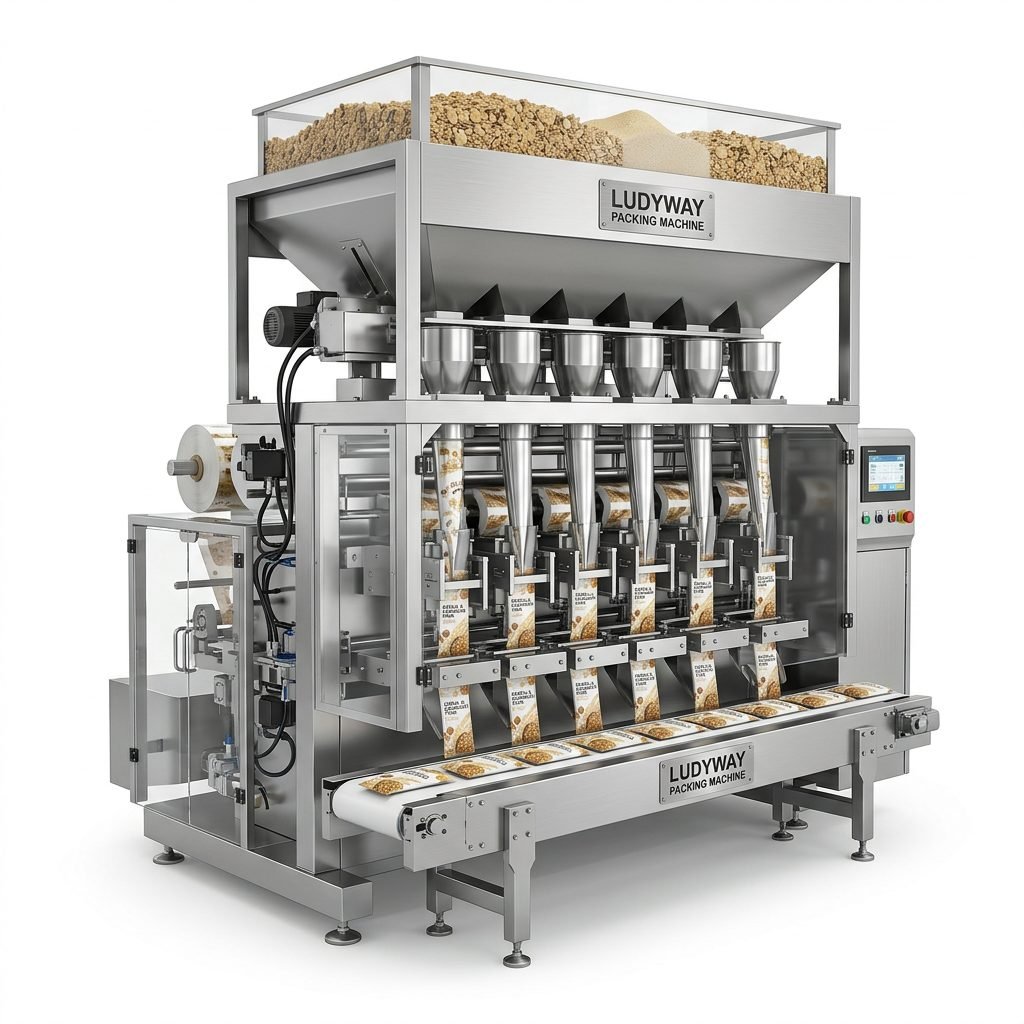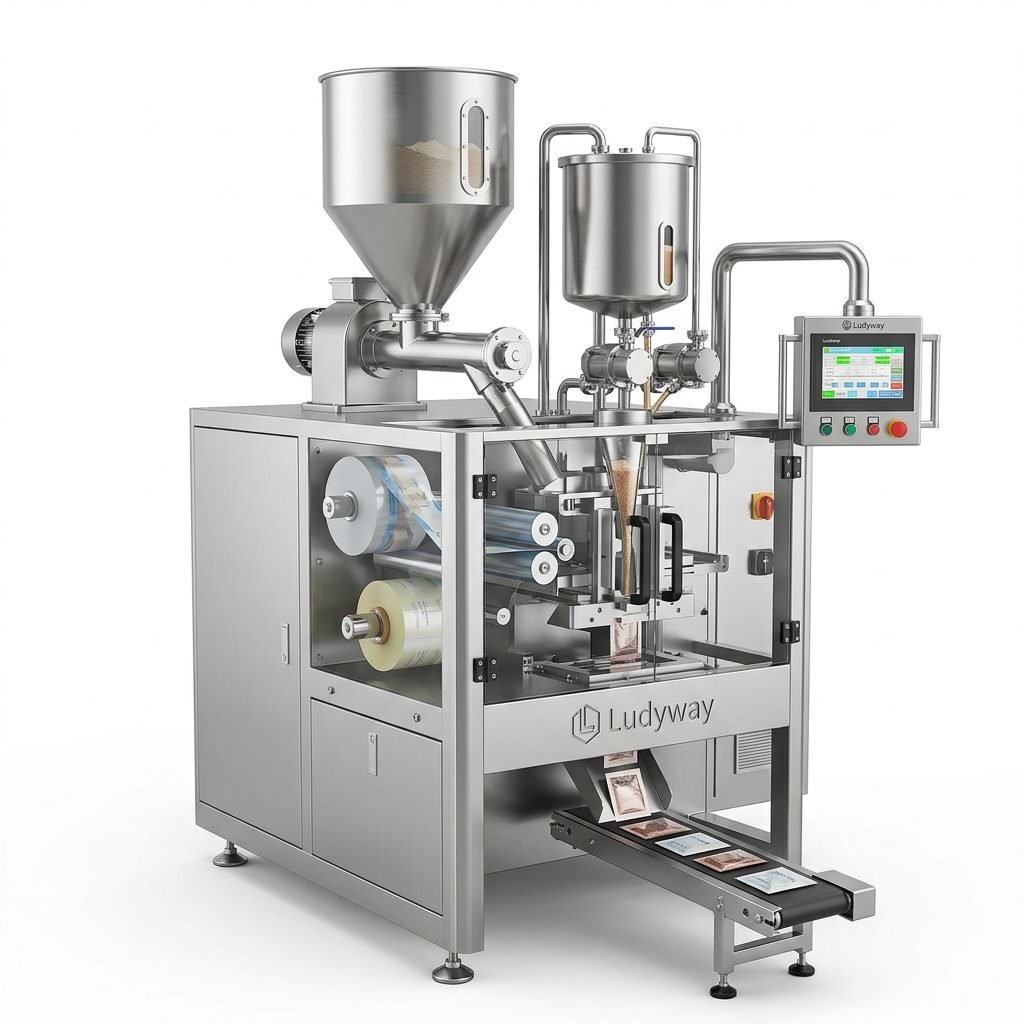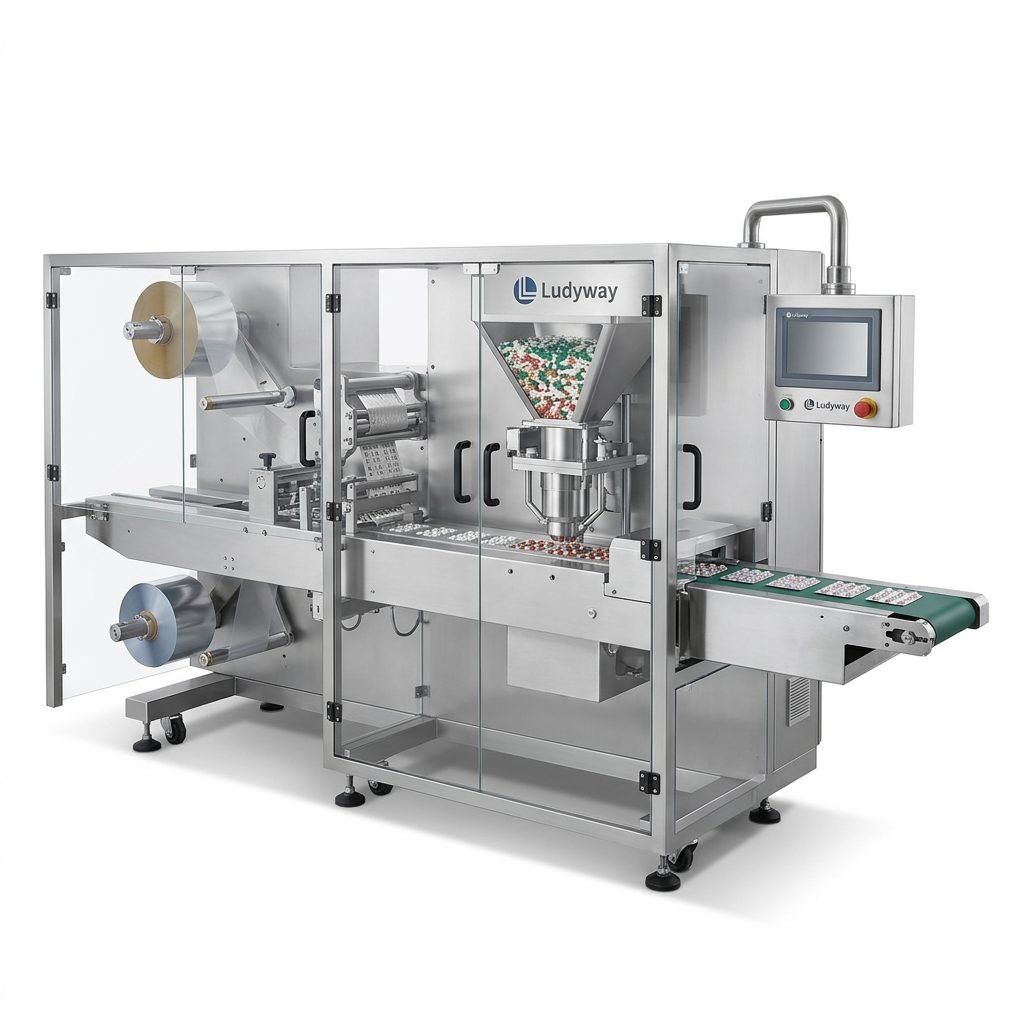
In modern manufacturing, packaging equipment must do more than simply fill and seal. It needs to support product safety, stable output, precise dosing, attractive presentation, and efficient changeovers across different packaging formats. For businesses in food, industrial, and retail sectors, choosing the right packing machine solution can directly affect labor costs, production speed, and brand consistency.
Today’s market demands flexible systems that can handle granules, powders, liquids, pastes, pouches, sachets, stick packs, bottles, and bulk bags with dependable performance. That is why many buyers look for manufacturers with proven engineering depth, export experience, and the ability to provide both standalone machines and complete turnkey lines.
Why Reliable Packaging Machinery Matters
Packaging is often the final and most visible step in production. A reliable machine helps manufacturers protect product quality while maintaining output targets. In food processing, this means better hygiene and seal integrity. In industrial products, it means accurate filling and safer handling. In retail packaging, it means shelf-ready presentation and more consistent pack appearance.
- Higher productivity through automated filling, sealing, counting, weighing, and labeling
- Lower waste with precise dosing and stable film or pouch control
- Better product protection through dependable sealing and contamination control
- Labor savings by reducing manual handling and repetitive operations
- Scalability for growing businesses that need line expansion later
When packaging performance is unstable, the result is usually downtime, customer complaints, material loss, and delayed shipment schedules. A reliable machine is therefore not just equipment—it is part of a company’s operational strategy.
Applications Across Food, Industrial, and Retail Products
Packing machines are used in a wide range of industries because products vary greatly in texture, density, flowability, package style, and compliance requirements. A well-designed system can be adapted to many applications without sacrificing precision.
Food Packaging
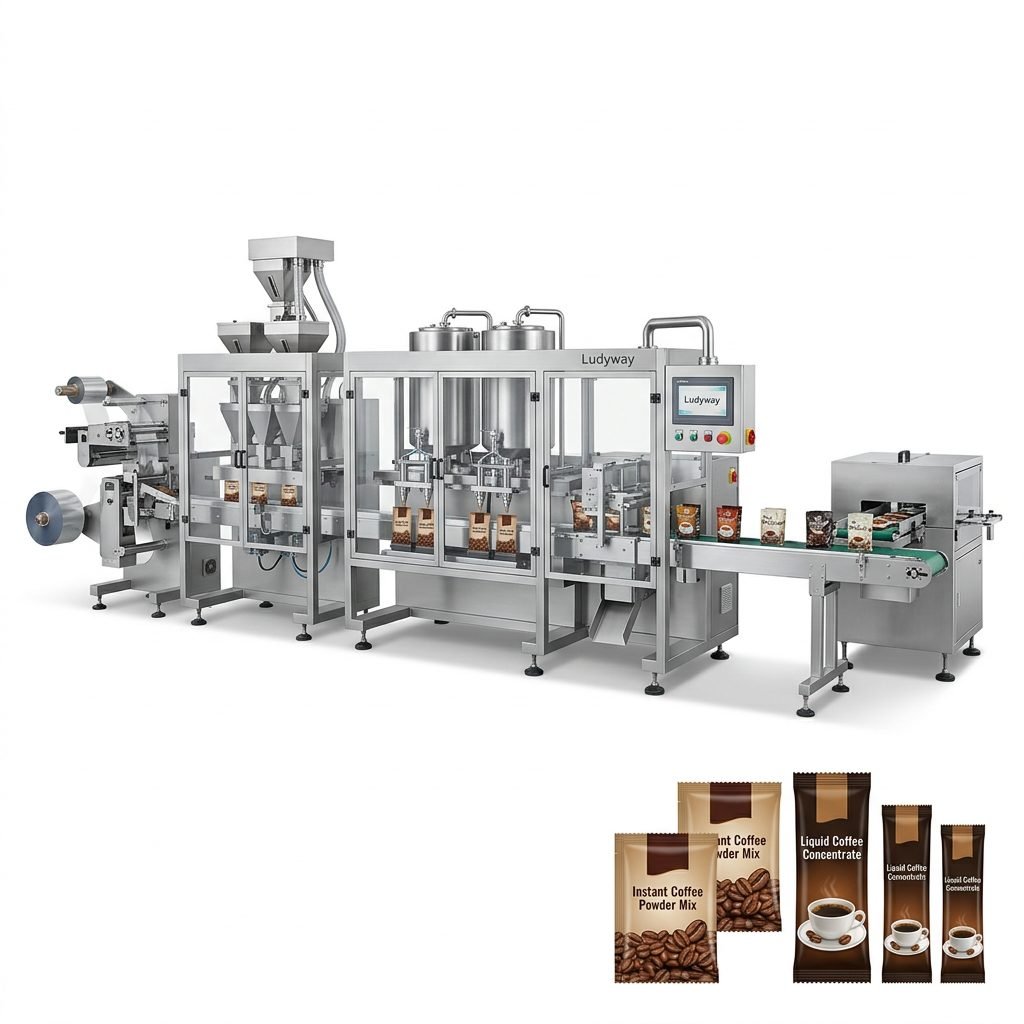
Food manufacturers often require machines for snacks, spices, sauces, drink powders, coffee, sugar, grains, instant mixes, pet food, and nutritional products. Depending on the product, the system may use auger filling, volumetric dosing, piston filling, multihead weighing, or counting technology.
Industrial Product Packaging
Industrial goods such as detergents, additives, solvents, powders, lubricants, and chemical granules demand robust construction, dosing stability, and compatibility with different materials. In many cases, leak prevention and corrosion resistance are especially important.
Retail and Consumer Pack Formats
Retail-ready products usually need visually consistent package shapes, clean seals, clear coding, and flexible pack sizes. Sachets, stick packs, pouches, bottles, and cartons are all common formats where automation improves both efficiency and product presentation.
Common Types of Packing Machines
The best packaging setup depends on product characteristics and final packaging requirements. Below are some of the most widely used machine categories.
| Machine Type | Typical Products | Main Benefits |
|---|---|---|
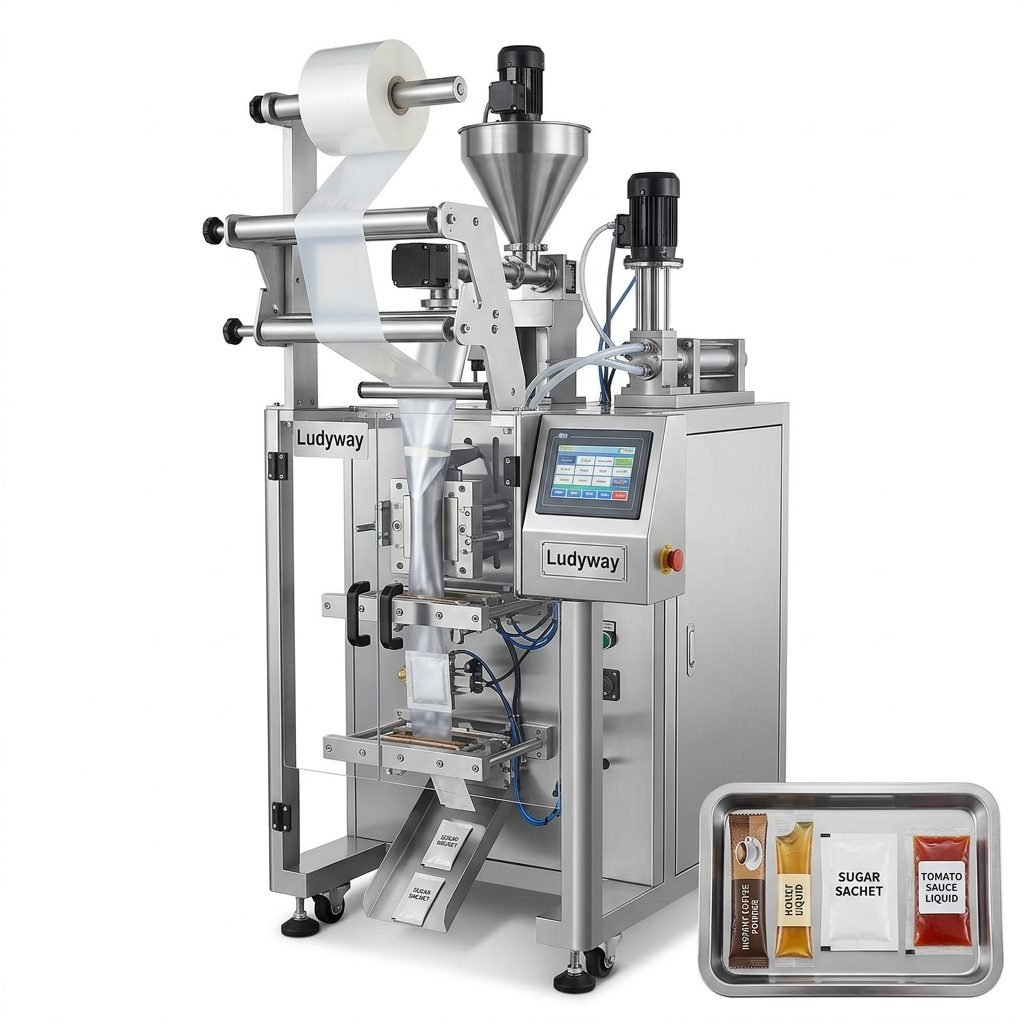
| Vertical Form Fill Seal Machines | Powders, granules, snacks, seeds | Compact layout, high efficiency, flexible bag styles |
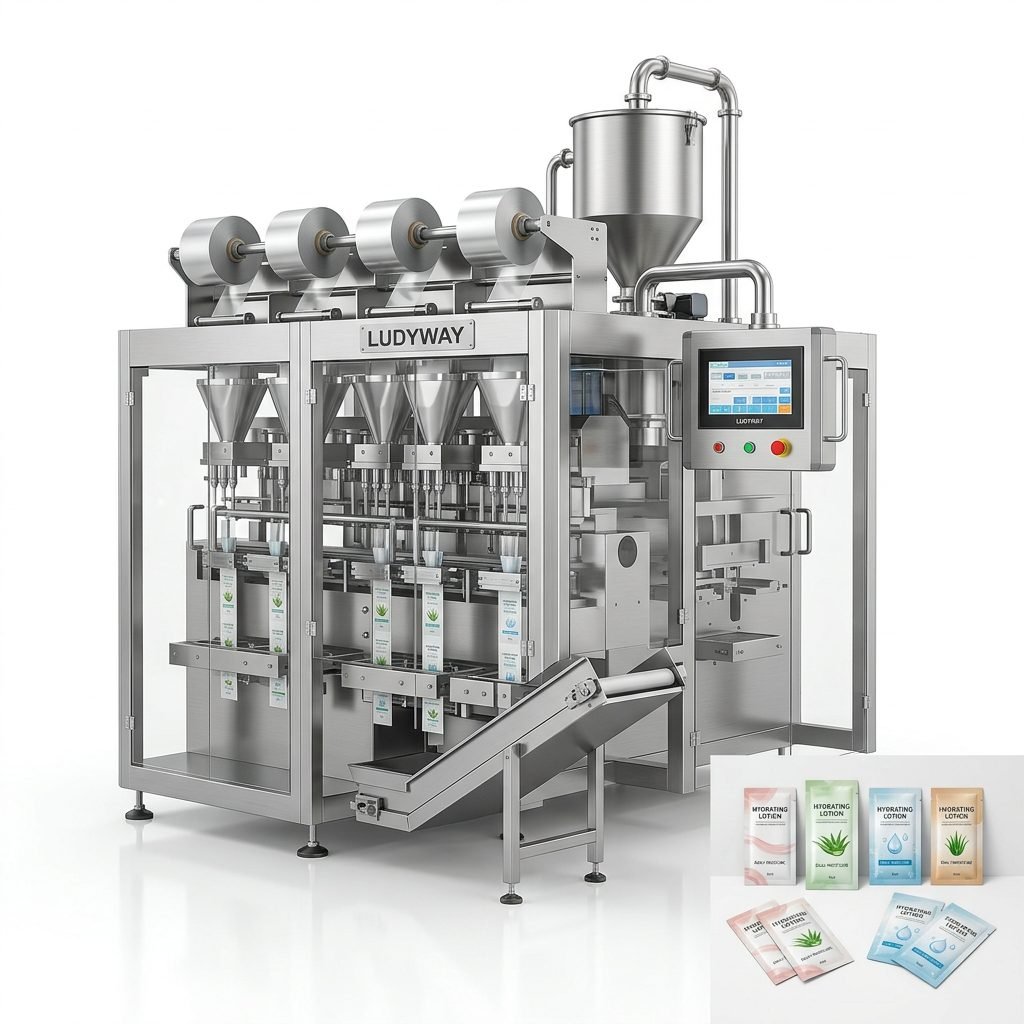
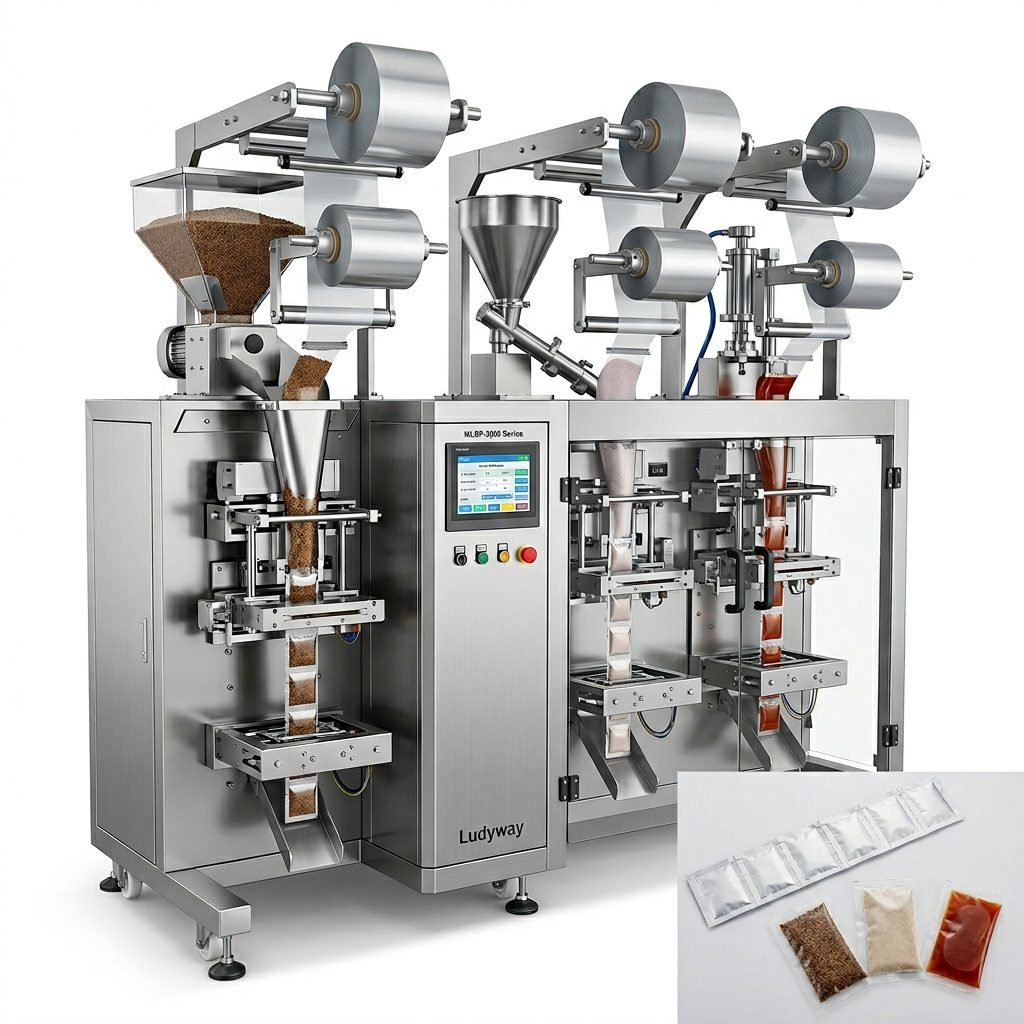
| Sachet Packing Machines | Sauces, seasonings, health products, detergents | Ideal for small-dose packaging and retail convenience |
| Stick Pack Machines | Drink mixes, sugar, coffee, supplements | Slim pack format, fast output, suitable for single-serve products |
| Liquid & Paste Filling Machines | Sauce, oil, cream, gel, solvent | Accurate filling, cleaner operation, strong sealing compatibility |
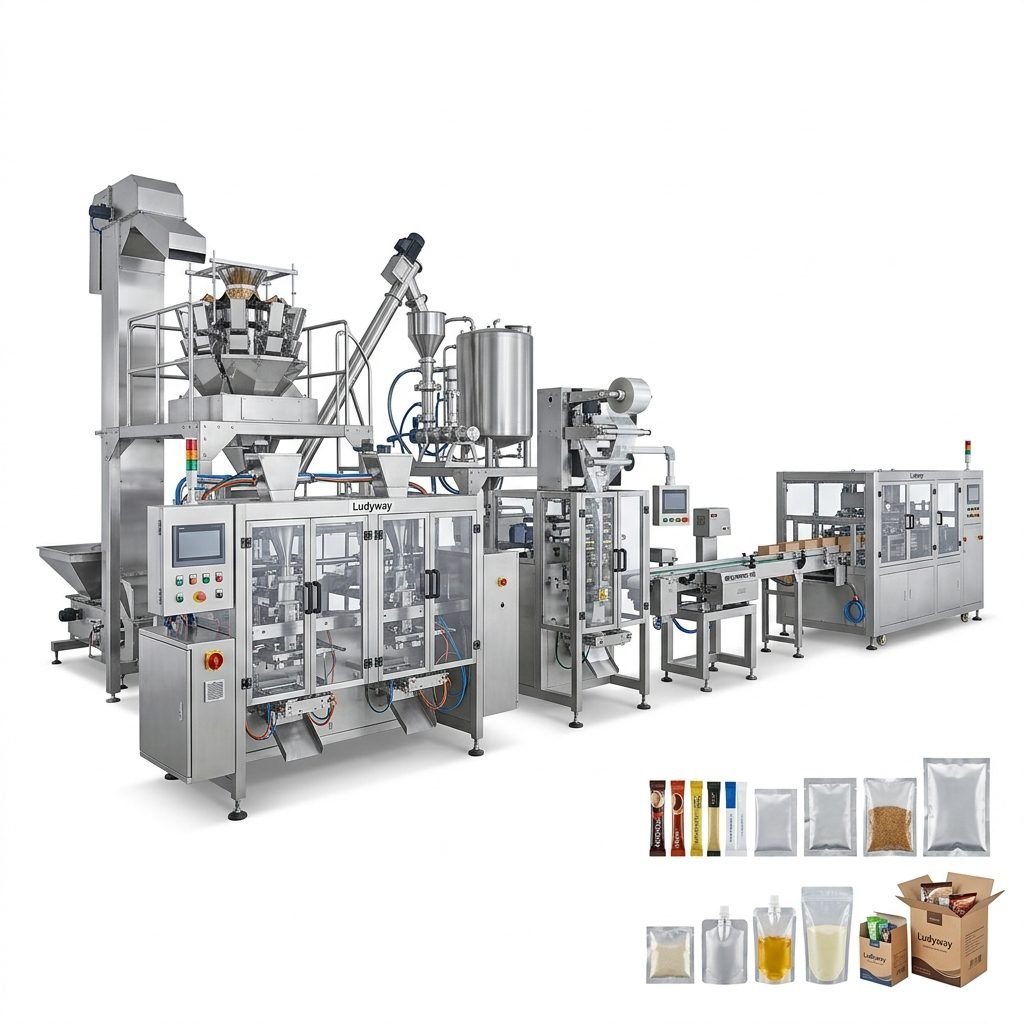
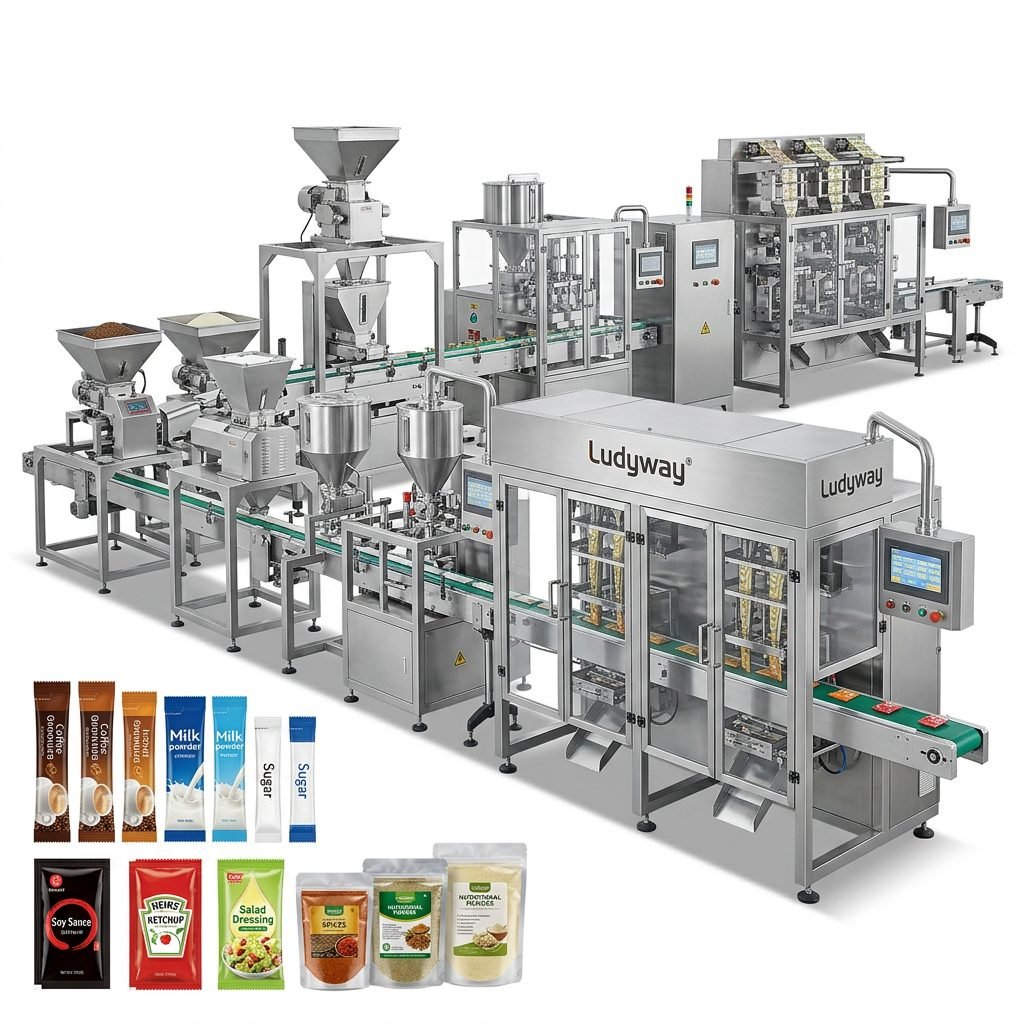
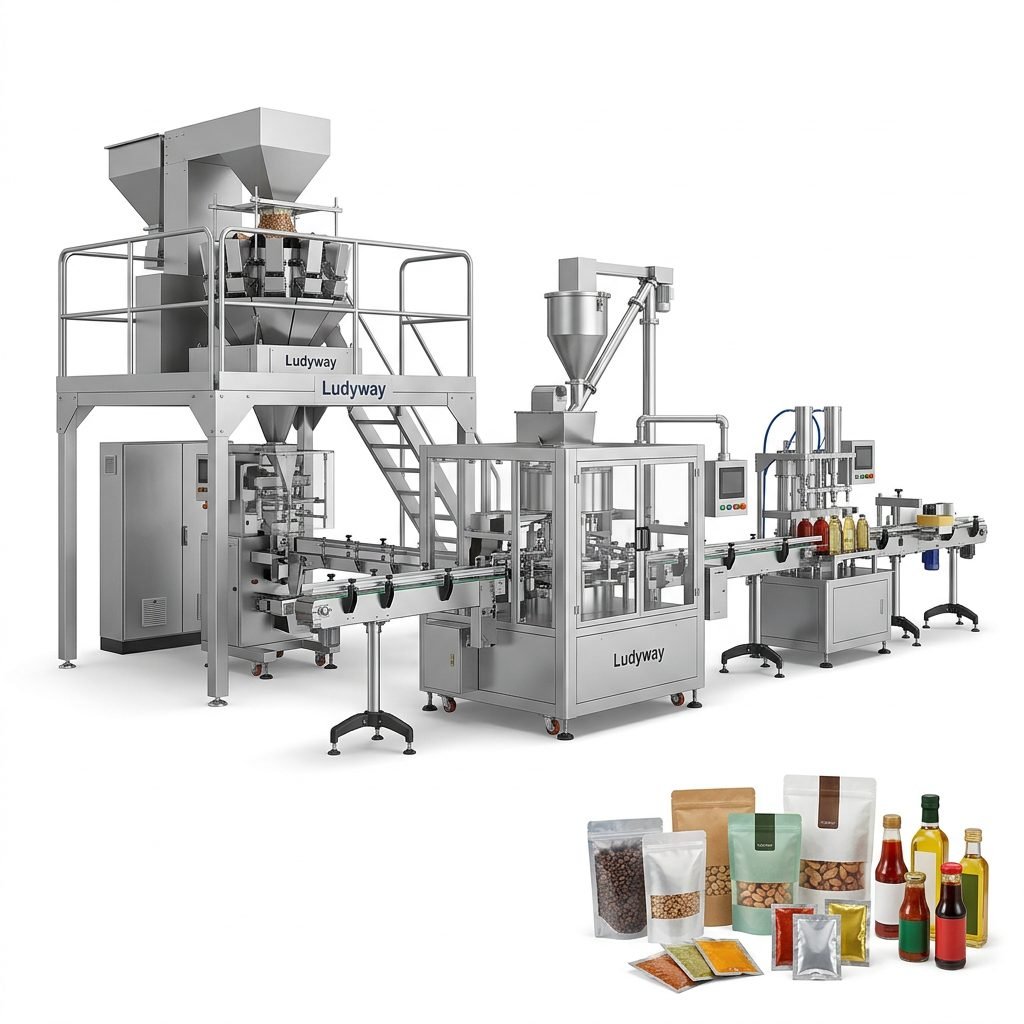
| Turnkey Packaging Lines | Food, pharmaceutical, cosmetic, chemical products | Integrated feeding, filling, sealing, coding, inspection, and end-of-line automation |
Key Features Buyers Should Look For
Not all packaging equipment offers the same long-term value. Buyers should evaluate machine performance beyond initial speed claims.
1. Dosing Accuracy
Accurate filling is essential for both regulatory compliance and cost control. Underfilling affects customer trust, while overfilling increases product giveaway and operating cost.
2. Stable Sealing Quality
Good sealing prevents leakage, moisture ingress, contamination, and transportation damage. This is particularly important for food, pharmaceuticals, and chemical products.
3. Material Compatibility
A machine should be matched to product characteristics, including powder fineness, granule size, viscosity, or corrosiveness. Stainless steel contact parts and application-specific configurations are often necessary.
4. Ease of Cleaning and Maintenance
Simple disassembly, accessible cleaning points, and organized mechanical structure reduce downtime and support more efficient production management.
5. Automation and Expandability
Many factories begin with a single machine and later add feeding systems, checkweighers, coding units, cartoners, case packers, or palletizers. Choosing scalable equipment protects future investment.
Benefits of Turnkey Packaging Line Solutions
For manufacturers planning medium- to high-volume production, a complete packaging line is often more efficient than buying separate machines from multiple suppliers. A turnkey solution helps align machine speed, control logic, material flow, and installation planning.
- Better line integration between feeding, filling, sealing, inspection, and secondary packaging
- Reduced communication gaps during project execution
- Faster commissioning and more coordinated after-sales support
- Improved factory layout planning and line balance
- More consistent operating standards across the whole packaging process
This approach is especially valuable for companies packaging multiple SKUs or managing growth across food, nutraceutical, pharmaceutical, cosmetic, and industrial product lines.
Choosing the Right Machine for Your Product
Before selecting equipment, manufacturers should clarify their production goals and technical requirements. A packaging machine that works perfectly for coffee powder may not be suitable for sauce, detergent liquid, or bulk granules.
Important Selection Factors
- Product form: powder, granule, liquid, paste, tablet, capsule, or pouch-based item
- Target output per minute or per shift
- Pack size range and packaging format
- Film or packaging material specification
- Required accuracy level
- Industry hygiene or compliance expectations
- Available installation space and plant utility conditions
It is also wise to assess whether your operation requires a standalone machine or a complete packaging line with upstream and downstream automation.
A Manufacturer with Broad Packaging Experience
For buyers seeking dependable automation, Ludyway packaging machine solutions offer a strong combination of manufacturing depth, export capability, and turnkey line experience. Established in 1993, the company operates a modern facility of over 20,000 square meters and serves customers in more than 100 countries and regions.
With more than 30 years of industry experience and a broad range of equipment for granules, powders, liquids, pastes, and pouch-based products, the manufacturer is well positioned for projects involving food, pharmaceutical, health supplement, cosmetic, chemical, nicotine pouch, and animal feed packaging. Its portfolio covers multi-lane stick pack machines, sachet packing machines, vertical packaging systems, filling and sealing equipment, as well as integrated automatic packaging lines.
Why Buyers Value Experienced Suppliers
| Capability | Buyer Advantage |
|---|---|
| Long manufacturing history | More mature process control and engineering know-how |
| Wide machine range | Better product matching for different industries and package formats |
| Turnkey line capability | Simplified project management and more efficient integration |
| Global export experience | Better understanding of international production requirements |
| Customization support | Solutions adapted to product type, output demand, and factory layout |
Industries That Benefit Most from Automated Packing Solutions
Food and Beverage
From powdered drinks and seasoning sachets to sauces, coffee, grains, and snack packs, automation improves fill accuracy, production hygiene, and shelf-ready appearance.
Pharmaceutical and Health Products
Granules, oral liquids, supplement powders, capsules, and stick packs require consistency, traceability, and carefully controlled packaging conditions.
Cosmetics and Personal Care
Creams, serums, lotions, shampoos, and facial care samples often rely on sachet, stick pack, tube, or bottle packaging systems with stable sealing and attractive finishing.
Chemical and Industrial Products
Detergents, cleaners, additives, lubricants, and treatment powders need durable systems that can handle diverse flow properties and maintain safe, repeatable filling.
Animal Feed and Pet Products
Pet food, feed premix, pellets, powders, and supplements benefit from automated weighing, filling, and bagging solutions that support higher throughput and consistent package weights.
How Automation Improves Long-Term Competitiveness
Packaging automation is not only about replacing manual work. It helps manufacturers respond to market pressure with faster product launches, better pack consistency, and stronger production control. In highly competitive sectors, these advantages can influence customer retention and distribution growth.
- Shorter lead times for packaged goods
- Improved packaging quality across batches
- Reduced dependence on manual labor availability
- Better data visibility through integrated control systems
- Greater readiness for export-oriented production standards
Reliable packing solutions support business growth by creating a more stable bridge between manufacturing output and market delivery.
Final Considerations for Buyers
When comparing packaging machine suppliers, it is important to look beyond the machine itself. Evaluate the supplier’s engineering experience, product range, project communication, customization capability, and long-term service support. A machine may look similar on paper, but practical operating stability often depends on design details, assembly quality, and application knowledge.
For food, industrial, and retail products, the most effective packaging solution is one that aligns product type, production target, package format, and future expansion plans. With the right equipment partner, manufacturers can improve efficiency today while building a packaging system ready for tomorrow’s growth.