In modern food packaging, shelf life is no longer improved by vacuum alone. Many manufacturers now use vacuum packing machines with nitrogen flushing to better protect products from oxygen, moisture influence, texture damage, and flavor loss. This packaging method is especially valuable for foods that are sensitive, fragile, oily, crispy, or easily oxidized.
By combining air removal with controlled nitrogen injection, manufacturers can create a more stable internal package environment. The result is often longer freshness, better appearance, improved taste retention, and lower spoilage risk.
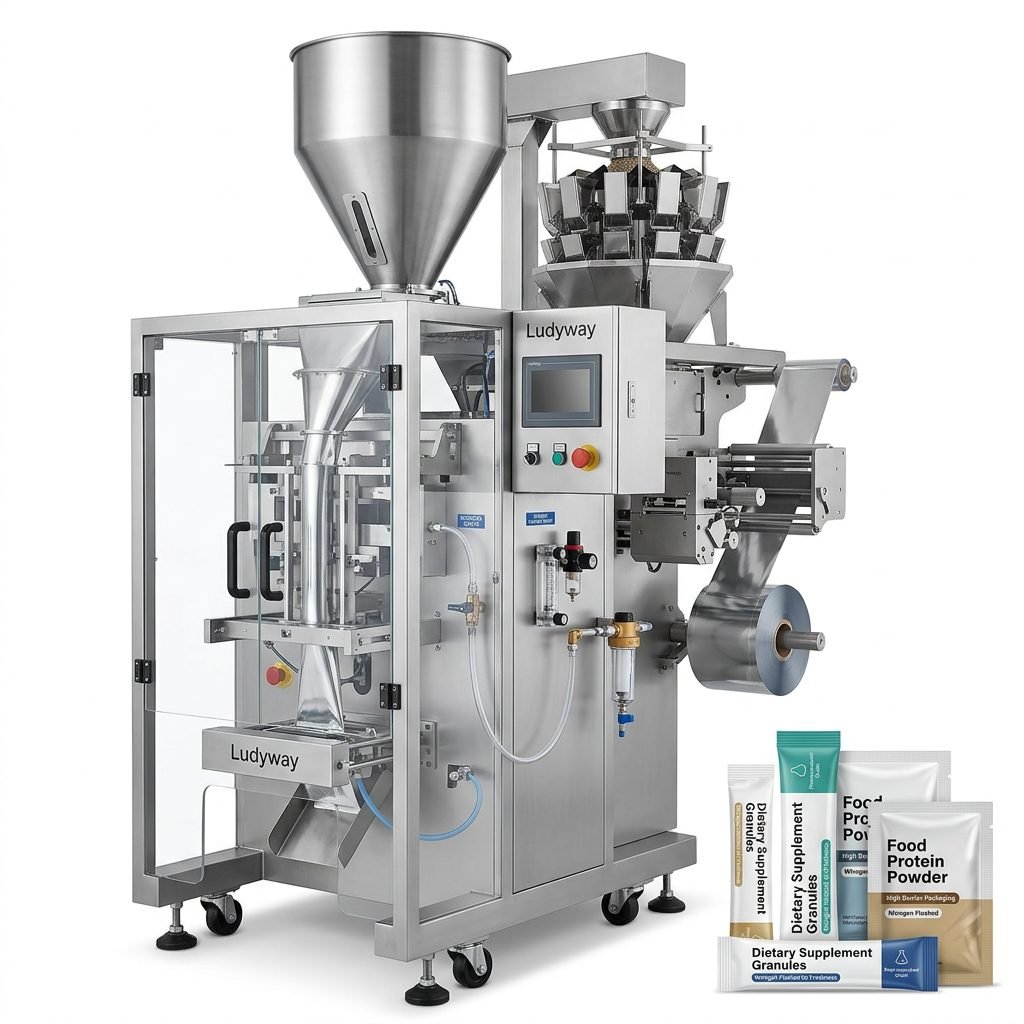
What Is a Vacuum Packing Machine with Nitrogen Flushing?
A vacuum packing machine with nitrogen flushing is a packaging system designed to remove most of the air inside a package and then replace part or all of the remaining atmosphere with nitrogen gas before sealing.
Nitrogen is an inert gas, which means it does not easily react with food. Since oxygen is one of the main causes of oxidation, rancidity, discoloration, and microbial growth, replacing oxygen with nitrogen helps preserve product quality more effectively.
In simple terms, the machine does two jobs:
- It reduces oxygen exposure by vacuuming out air.
- It adds protective nitrogen to create a safer internal package atmosphere.
How the Process Works
Although machine structures vary by product type and packaging format, the core process is usually similar.
- Product loading: Food is filled into a pouch, tray, bag, or container.
- Vacuum stage: The machine removes air from the package chamber or directly from the package.
- Nitrogen flushing stage: Nitrogen is introduced to displace residual oxygen.
- Sealing stage: The package is heat sealed under controlled conditions.
- Quality check: Seal integrity, gas retention, and appearance are inspected.
Why both vacuum and nitrogen are used together
Vacuum packaging alone is excellent for many products, but it may not be ideal for delicate foods that can be crushed under pressure. Nitrogen helps create a cushioning effect inside the pack. This is why foods like chips, roasted nuts, coffee, bakery products, and powdered nutritional items often benefit from nitrogen flushing.
| Step | What Happens | Main Benefit |
|---|---|---|
| Filling | Product enters pouch or container | Accurate portion control |
| Vacuuming | Air is removed from package | Lower oxygen content |
| Nitrogen flushing | Nitrogen replaces residual air | Oxidation protection |
| Sealing | Package is closed tightly | Maintains atmosphere stability |
| Inspection | Seal and gas level are checked | Consistent packaging quality |
Why Nitrogen Flushing Improves Food Preservation
1. Slows oxidation
Oxygen exposure can cause oils and fats to become rancid, colors to fade, and flavors to deteriorate. Nitrogen reduces the oxygen level inside the package, which helps slow these reactions.
2. Protects taste and aroma
Products such as coffee, tea, spices, snack foods, and nutritional powders can lose aroma quickly when exposed to air. Nitrogen helps preserve their original sensory profile for longer.
3. Helps maintain texture
Crunchy and fragile products can lose quality when packaging fails to protect them. Nitrogen can act as a buffer, helping reduce crushing and maintaining product shape during handling and transport.
4. Supports longer shelf life
When combined with proper sealing materials and hygienic processing, nitrogen flushing can significantly extend the marketable life of packaged foods.
5. Improves product presentation
A well-flushed package often looks fuller and more professional. This improves shelf appeal and supports stronger consumer confidence in product freshness.
Foods That Commonly Use Nitrogen Flushing
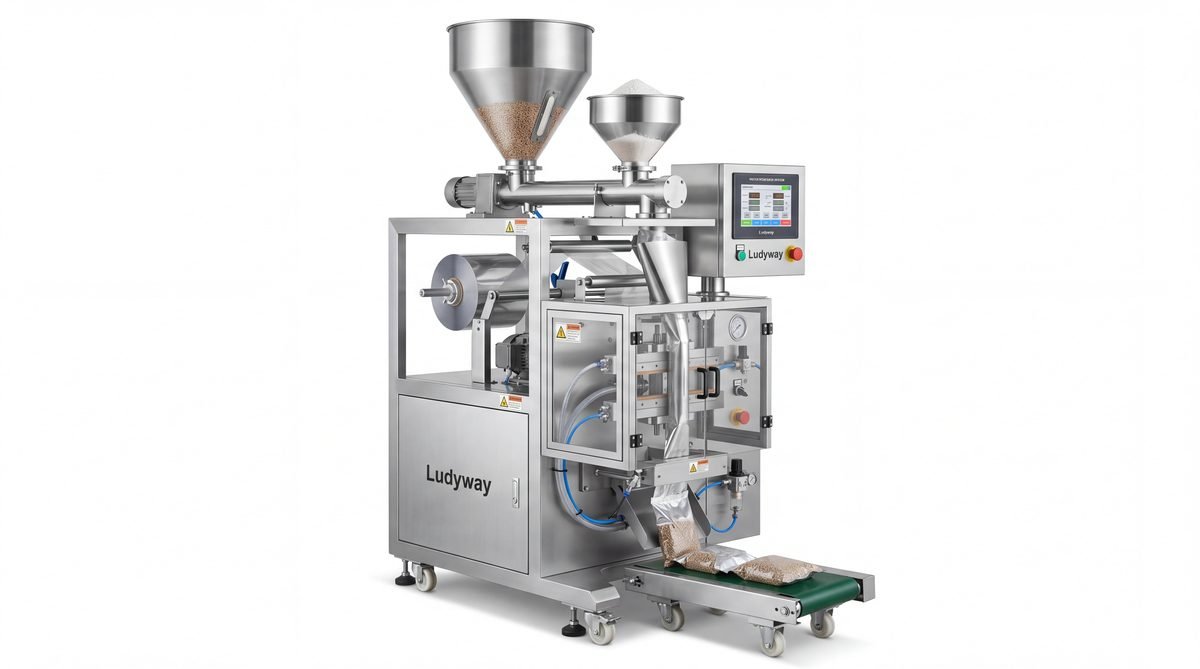
This packaging technology is widely used across the food industry, especially for products where oxygen control matters.
- Potato chips and puffed snacks
- Roasted nuts and seeds
- Coffee beans and ground coffee
- Milk powder and protein powder
- Spices and seasoning blends
- Bakery products and biscuits
- Dried fruits and freeze-dried foods
- Tea, instant beverages, and functional powders
Vacuum Packaging vs. Vacuum Packaging with Nitrogen Flushing
| Feature | Vacuum Only | Vacuum + Nitrogen Flushing |
|---|---|---|
| Oxygen reduction | Good | Better and more controlled |
| Fragile product protection | Limited | Excellent for delicate items |
| Flavor retention | Moderate to good | Strong |
| Package appearance | Often tight or compressed | More balanced and market-friendly |
| Best for | Meat, cheese, dense products | Snacks, powders, coffee, dry foods |
Key Machine Features to Look For
Not every nitrogen flushing packaging machine performs at the same level. The right machine should match the product, packaging material, production speed, and required gas control precision.
Important features include:
- Stable vacuum performance for consistent air removal
- Accurate nitrogen dosing to maintain target gas ratios
- Reliable sealing system to prevent leakage
- Compatible packaging materials with strong barrier properties
- Easy cleaning and maintenance for food safety compliance
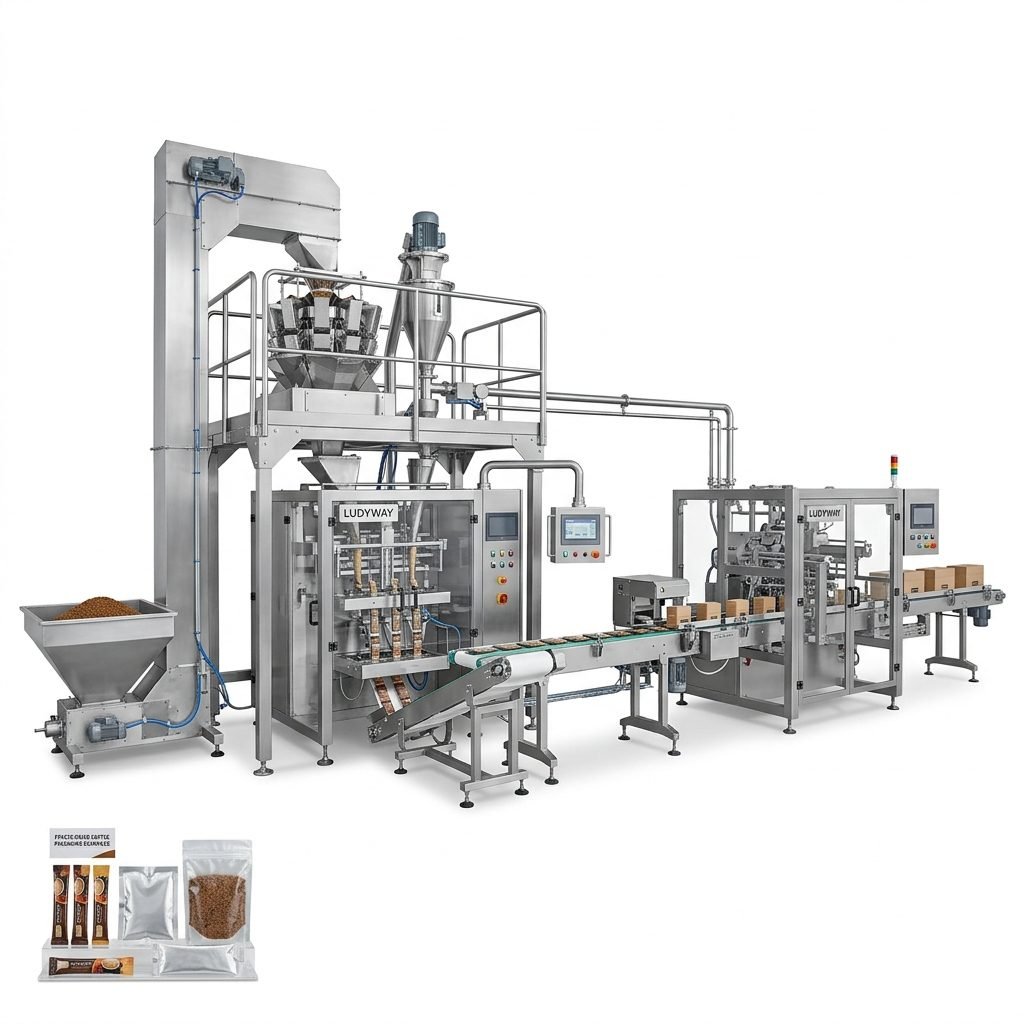
- Automation integration with fillers, conveyors, checkweighers, and coding systems
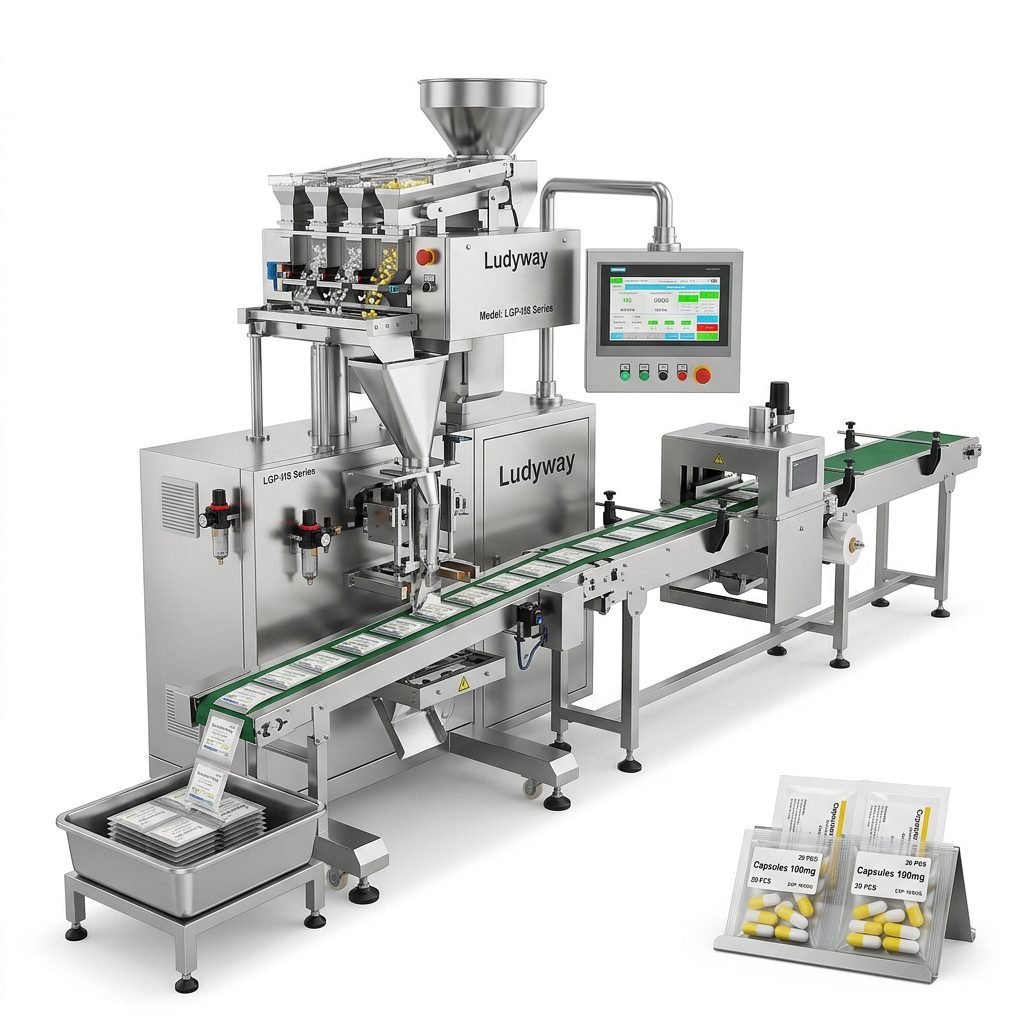
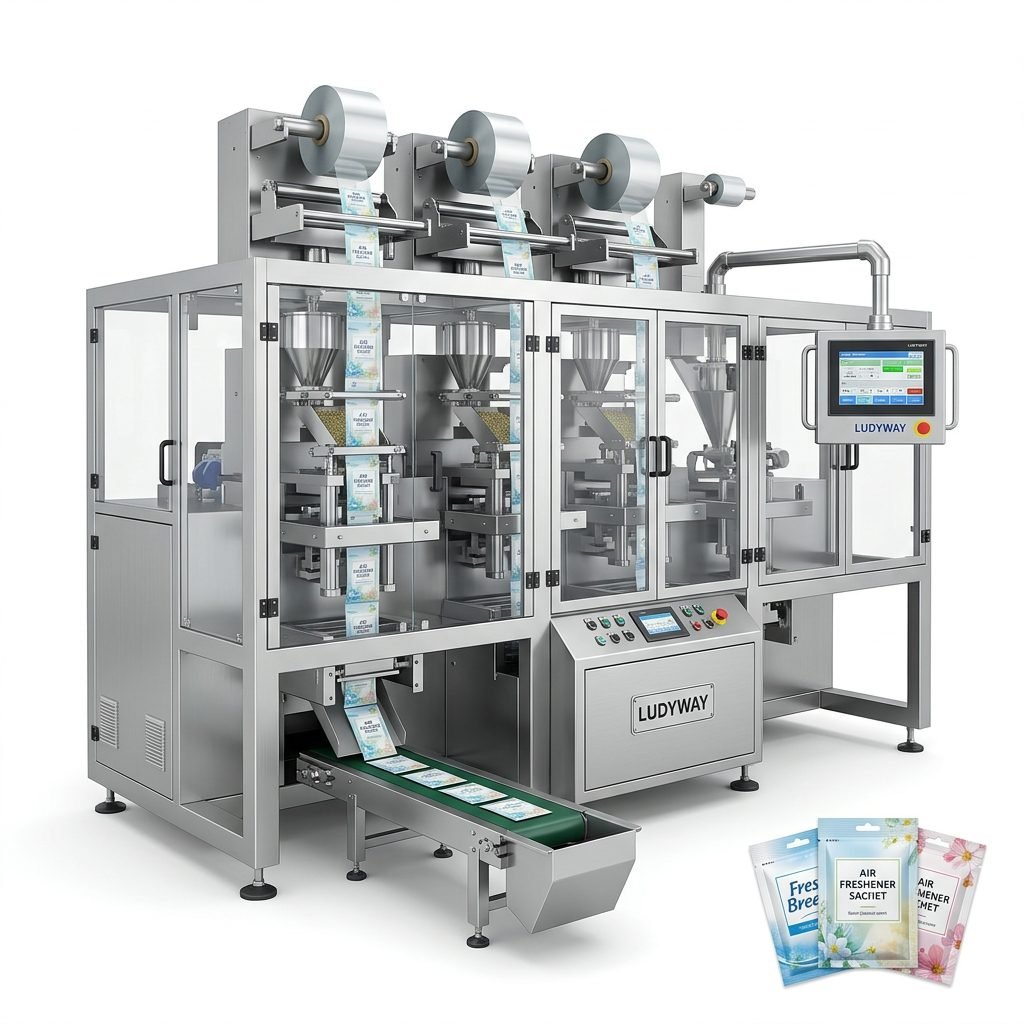
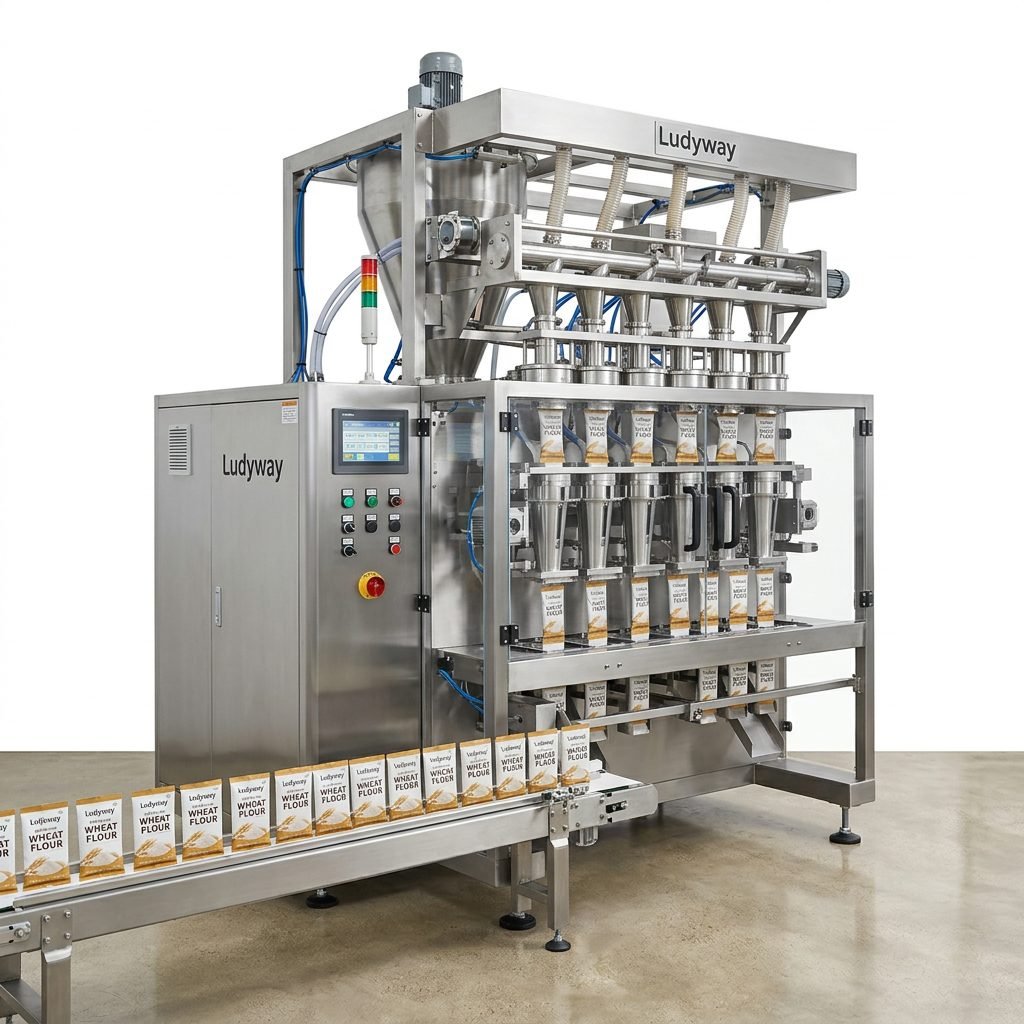
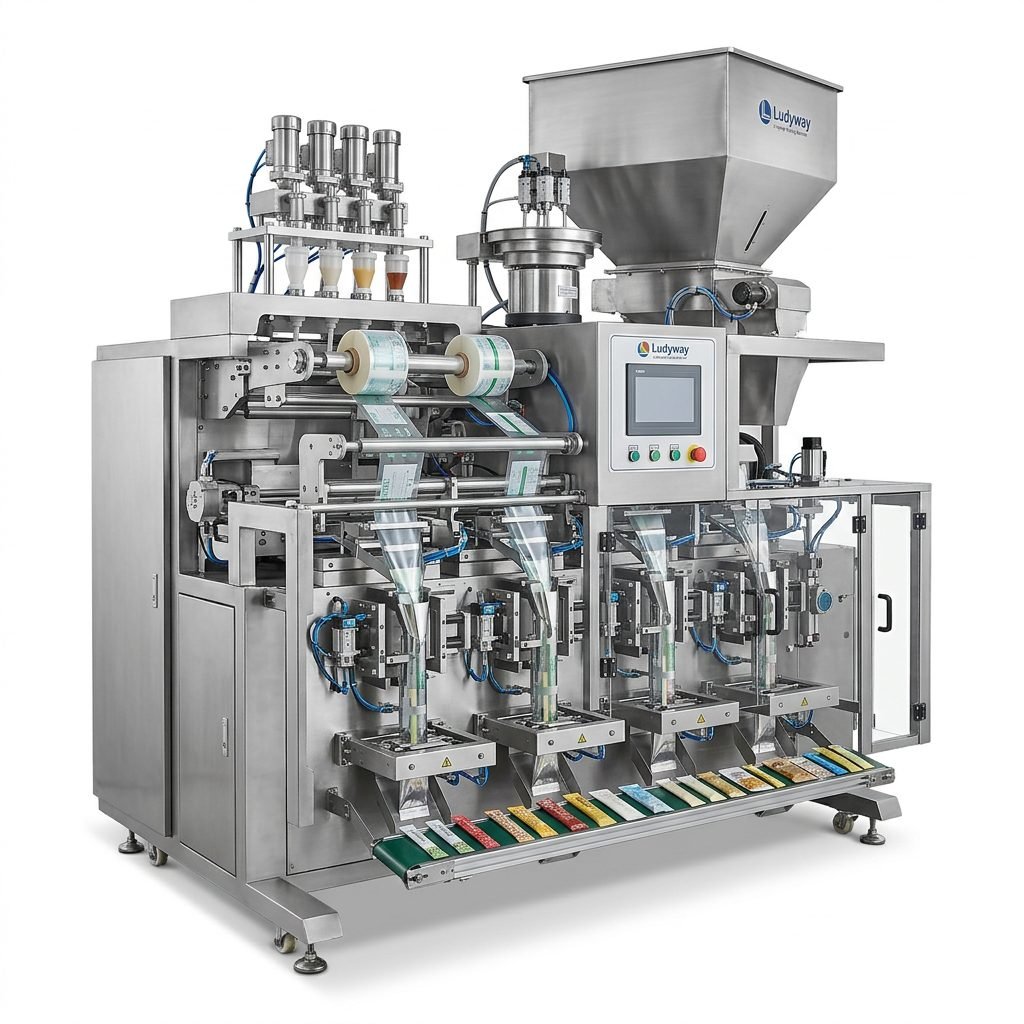
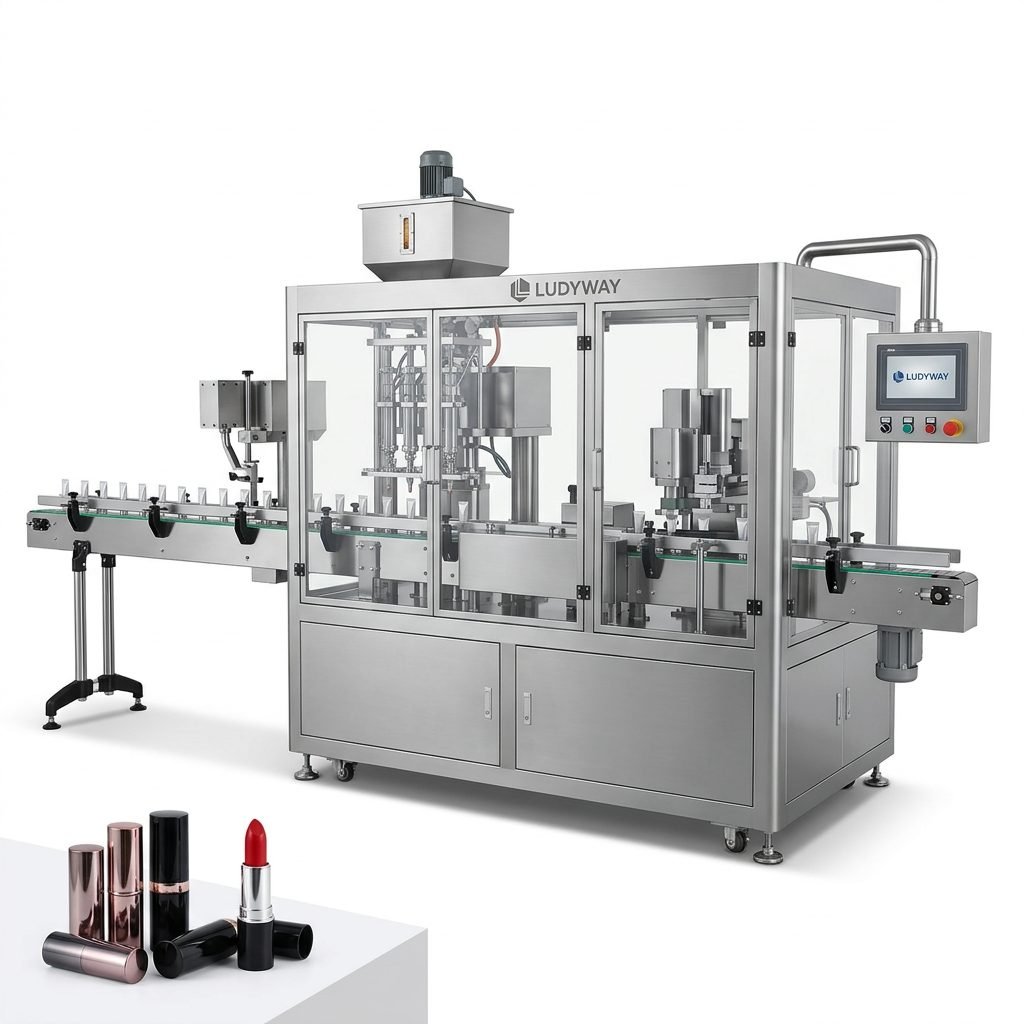
For manufacturers looking for scalable equipment and integrated automation, Ludyway packaging machine solutions are widely used in food, pharmaceutical, health supplement, and related industries, with extensive experience in turnkey packaging lines and customized systems.
Packaging Materials Matter Too
Even the best nitrogen flushing system cannot perform well if the packaging film has poor barrier properties. Oxygen transmission rate, moisture resistance, puncture strength, and sealing compatibility all influence the final preservation result.
For best performance, businesses should evaluate:
- Film structure and oxygen barrier level
- Heat sealing consistency
- Suitability for powders, granules, or fragile solids
- Storage and distribution conditions
Common Industries Benefiting from This Technology
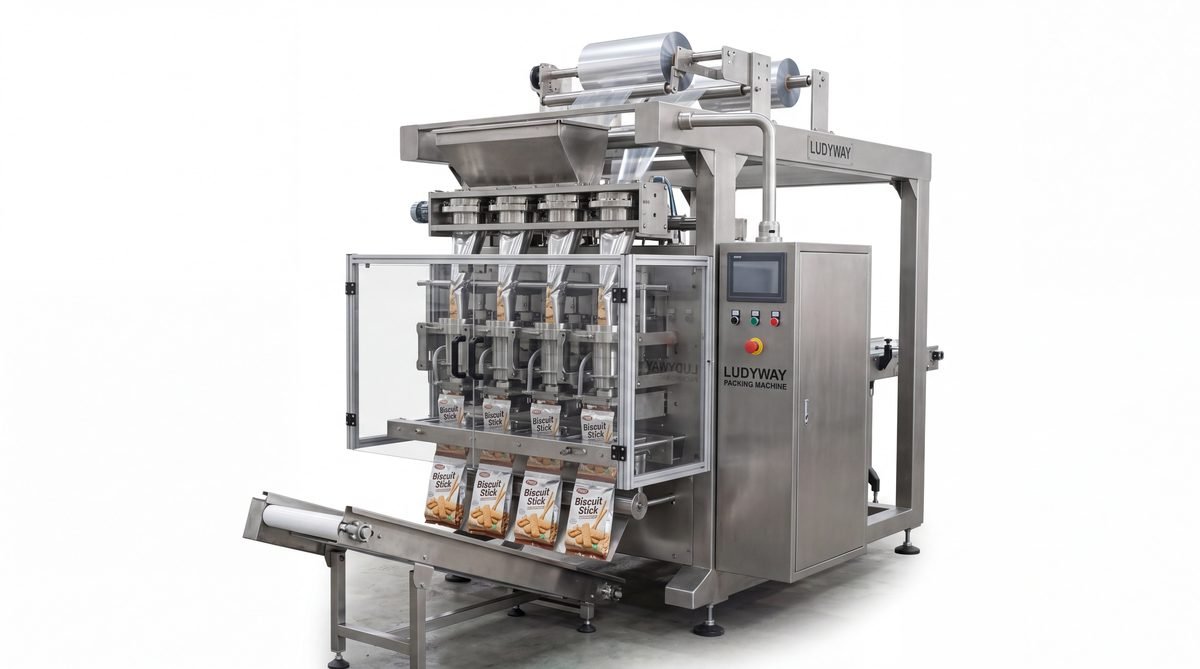
Although this method is strongly associated with food preservation, it is also useful in other sectors where product stability matters.
Typical applications include:
- Food processing
- Nutritional supplement manufacturing
- Coffee and beverage powder production
- Pharmaceutical granule and powder packaging
- Pet food and pet nutrition packaging
Operational Benefits for Manufacturers
Beyond product preservation, vacuum packing machines with nitrogen flushing offer important production advantages.
- Reduced product returns caused by stale flavor or poor seal performance
- Improved consistency across batches
- Stronger brand presentation on shelves
- Better suitability for export and longer logistics cycles
- Higher production automation and lower manual handling
How to Choose the Right System
Before investing in a nitrogen flushing vacuum packaging machine, businesses should assess the following:
- What product characteristics need protection: oxygen sensitivity, fragility, aroma, or moisture stability?
- What package format is required: sachet, pouch, tray, bag, or rigid container?
- What output speed is needed for current and future production?
- What gas purity and residual oxygen levels are acceptable?
- Will the machine need to integrate into a complete packaging line?
Final Considerations for Better Food Preservation
A vacuum packing machine with nitrogen flushing is more than a packaging upgrade. It is a strategic preservation solution for brands that want to protect quality, reduce oxidation, improve shelf appeal, and extend shelf life without compromising product integrity.
For snacks, powders, coffee, dry foods, and many sensitive packaged products, this technology delivers a practical balance between freshness protection and efficient automated production. When paired with the right film, sealing performance, and machine configuration, it can make a measurable difference in both product quality and business performance.