Selecting the right airtight food packaging machine is one of the most important equipment decisions a food manufacturer can make. Whether you are packaging coffee, spices, protein powders, dried fruits, or ready-to-drink mixes, an airtight seal directly affects product freshness, shelf life, and consumer safety. With so many machine types, configurations, and technical specifications available, the selection process can feel overwhelming. This guide breaks down everything you need to evaluate before investing in airtight packaging equipment.
Understanding Airtight Packaging Requirements
Not all food products require the same level of airtight protection. The first step in choosing the right machine is understanding what you are protecting against. Airtight packaging typically guards against four main threats: oxygen, moisture, light, and microbial contamination. Products with high fat content are particularly susceptible to oxidation, while hygroscopic powders like instant coffee or milk powder quickly absorb moisture from the air.
According to industry resources from the Flexible Packaging Association, barrier properties of packaging materials play a defining role in shelf-life extension. The machine you select must be compatible with these barrier films and capable of producing consistent, verifiable seals. For many manufacturers, this also means incorporating features like nitrogen flushing or vacuum sealing to actively remove oxygen before the package is closed.
Types of Airtight Food Packaging Machines
The packaging format you choose will largely determine the type of machine you need. Each format offers different levels of airtight protection, production speed, and cost efficiency. Below are the most common types used in food manufacturing:
Stick Pack and Sachet Machines
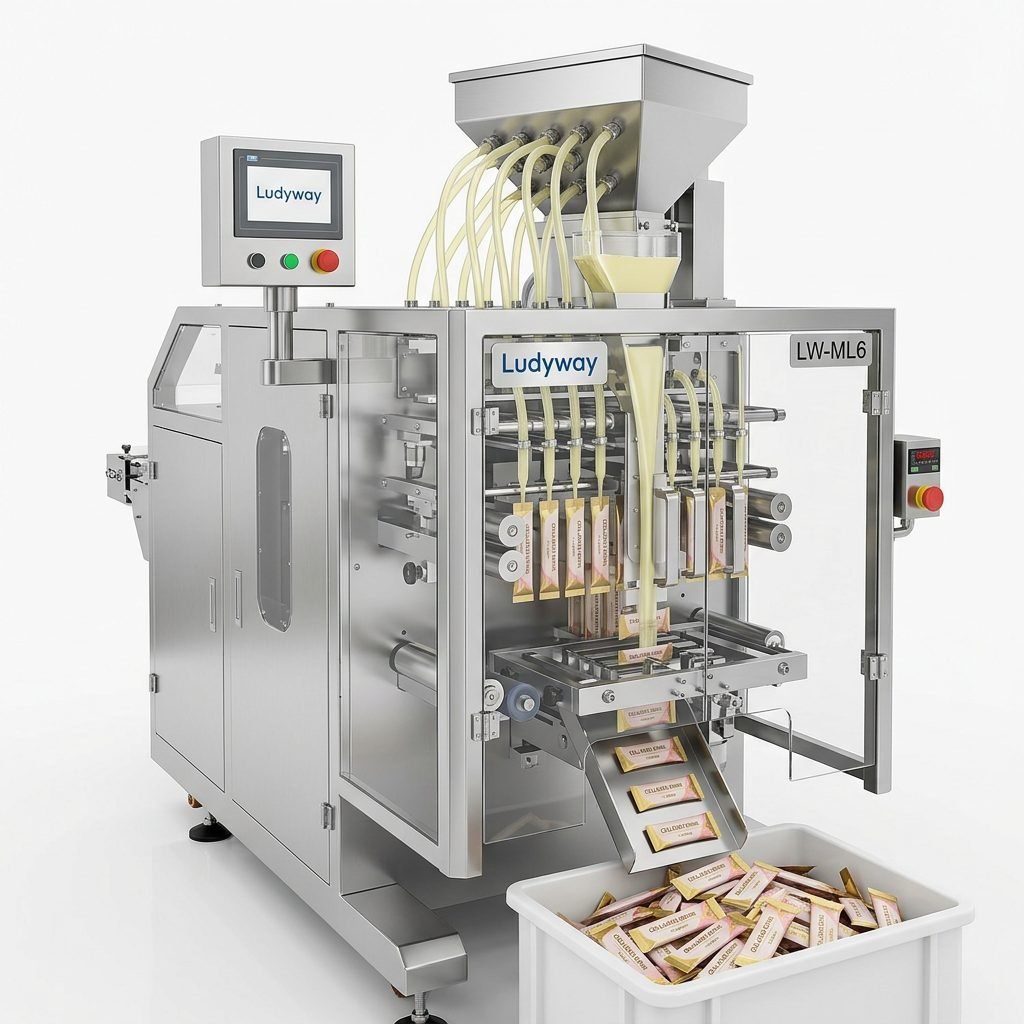
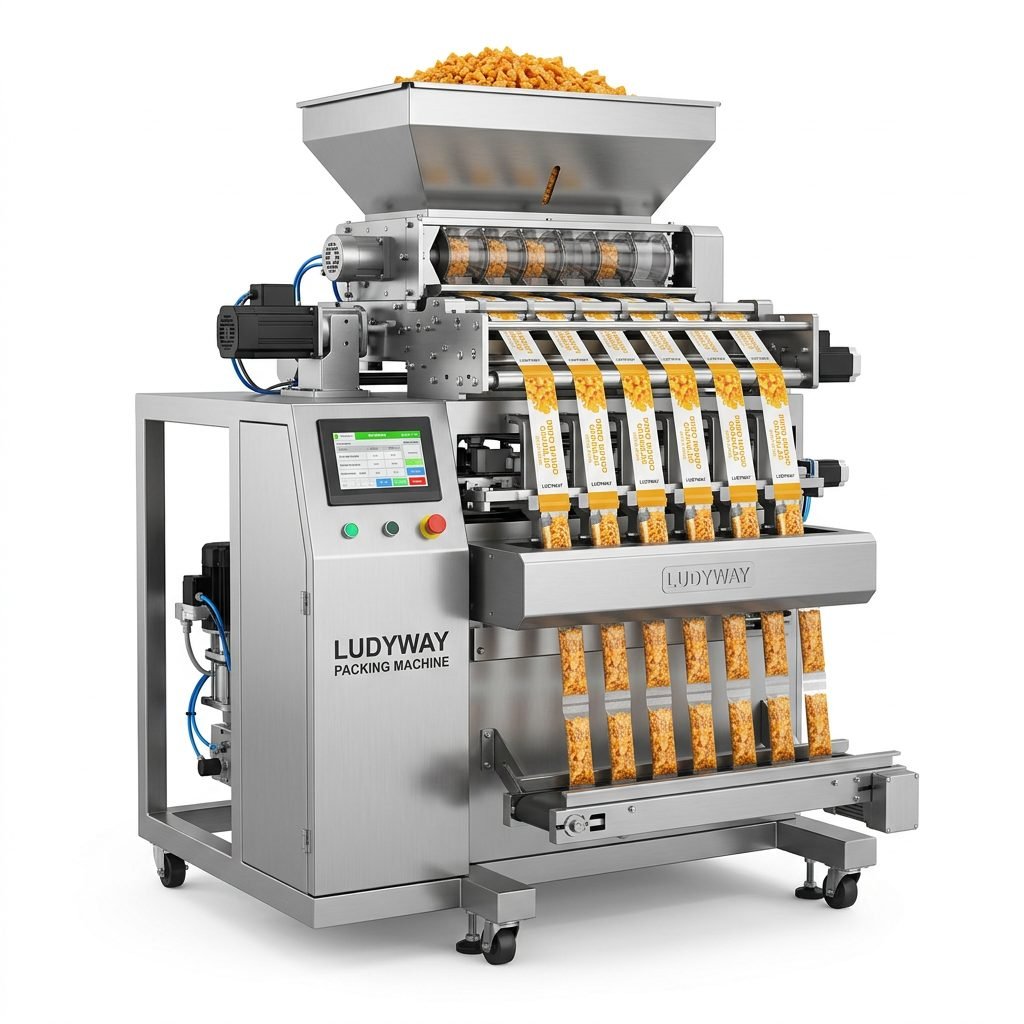
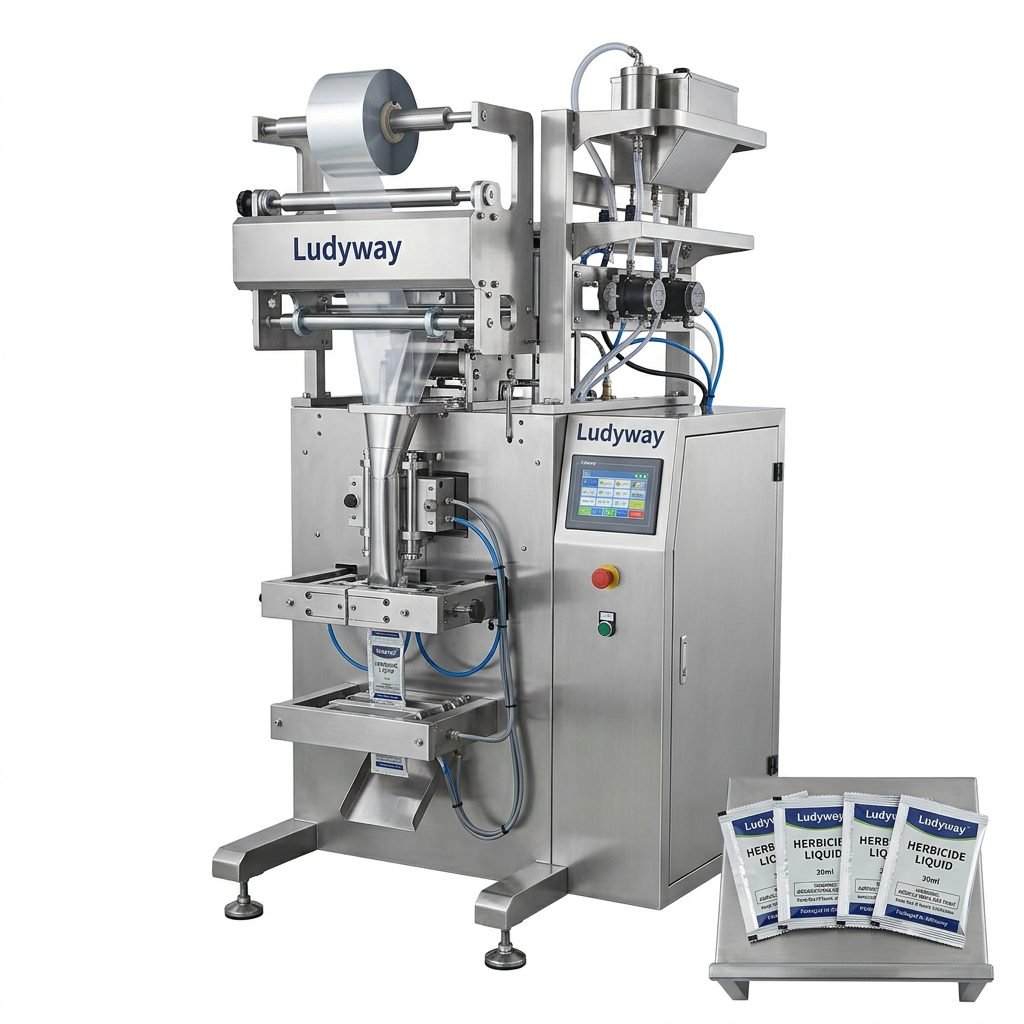
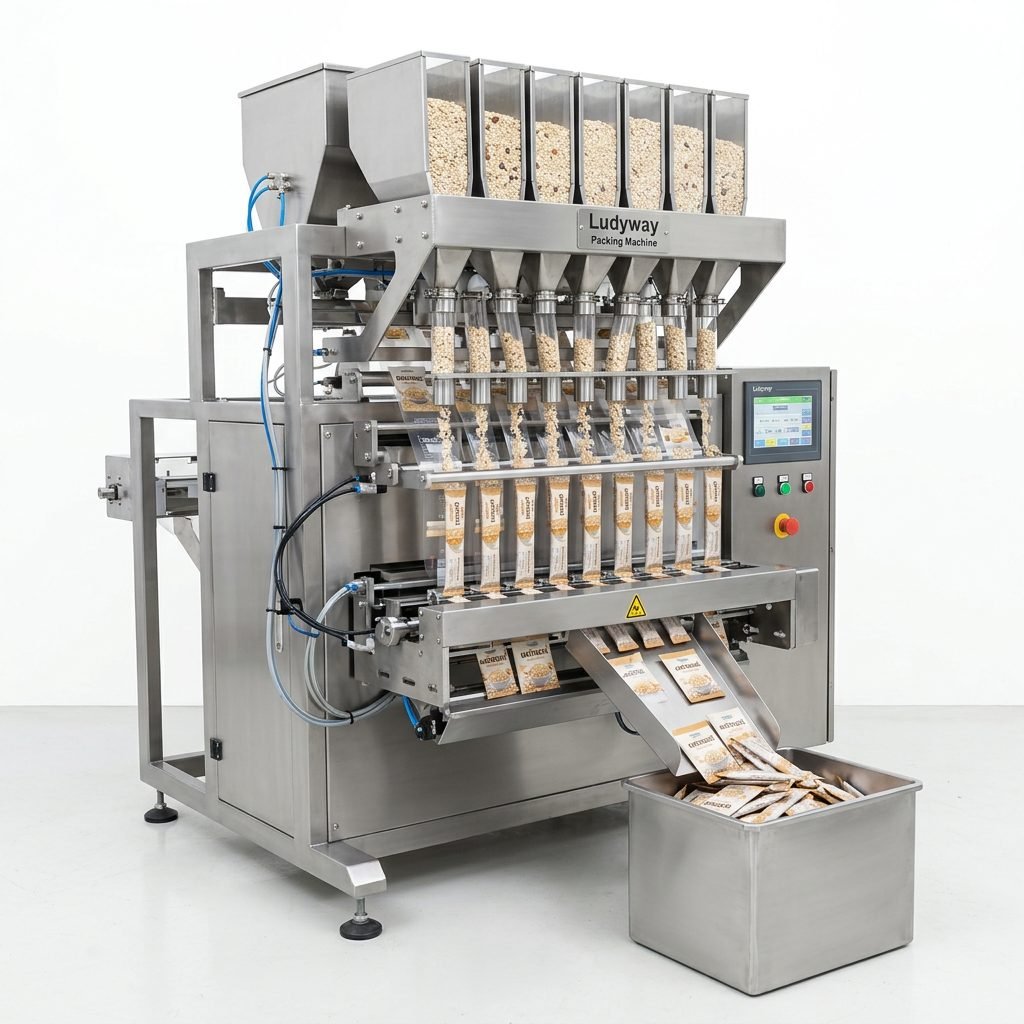
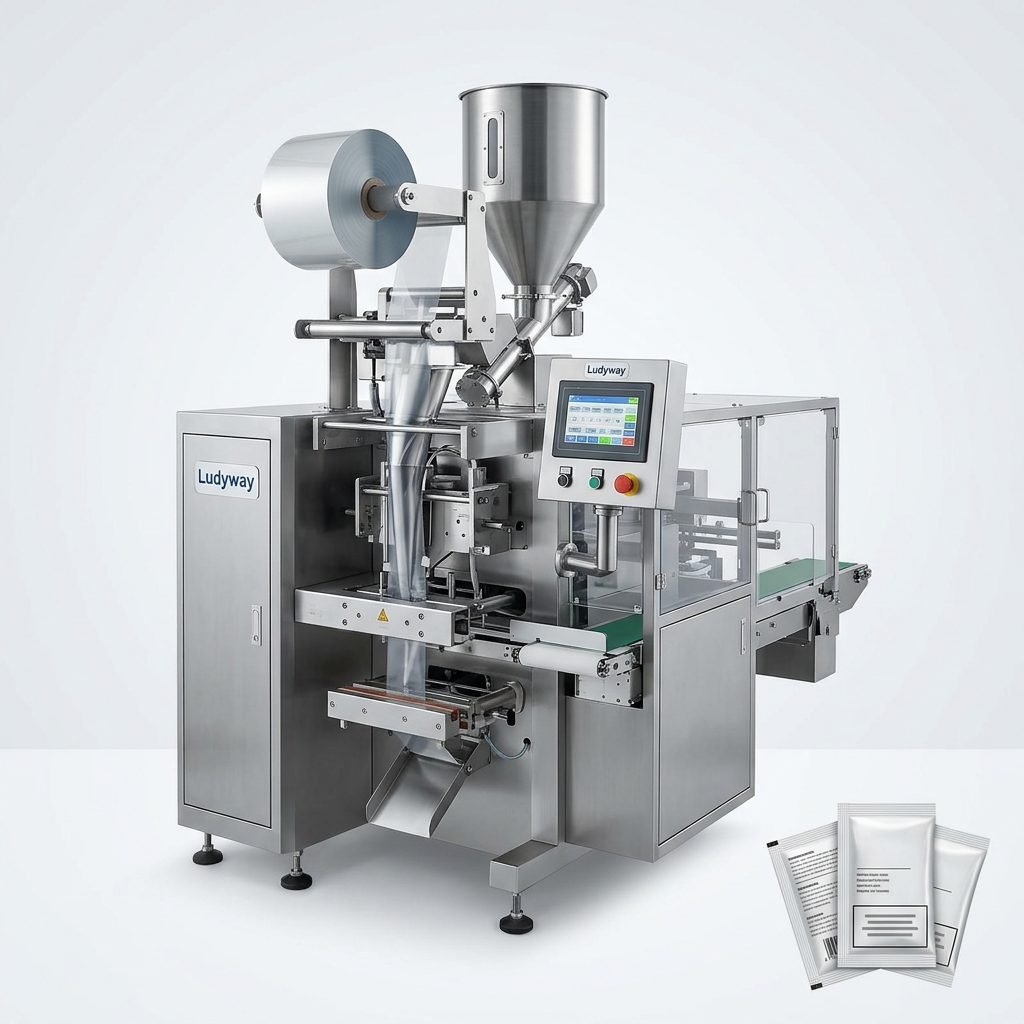
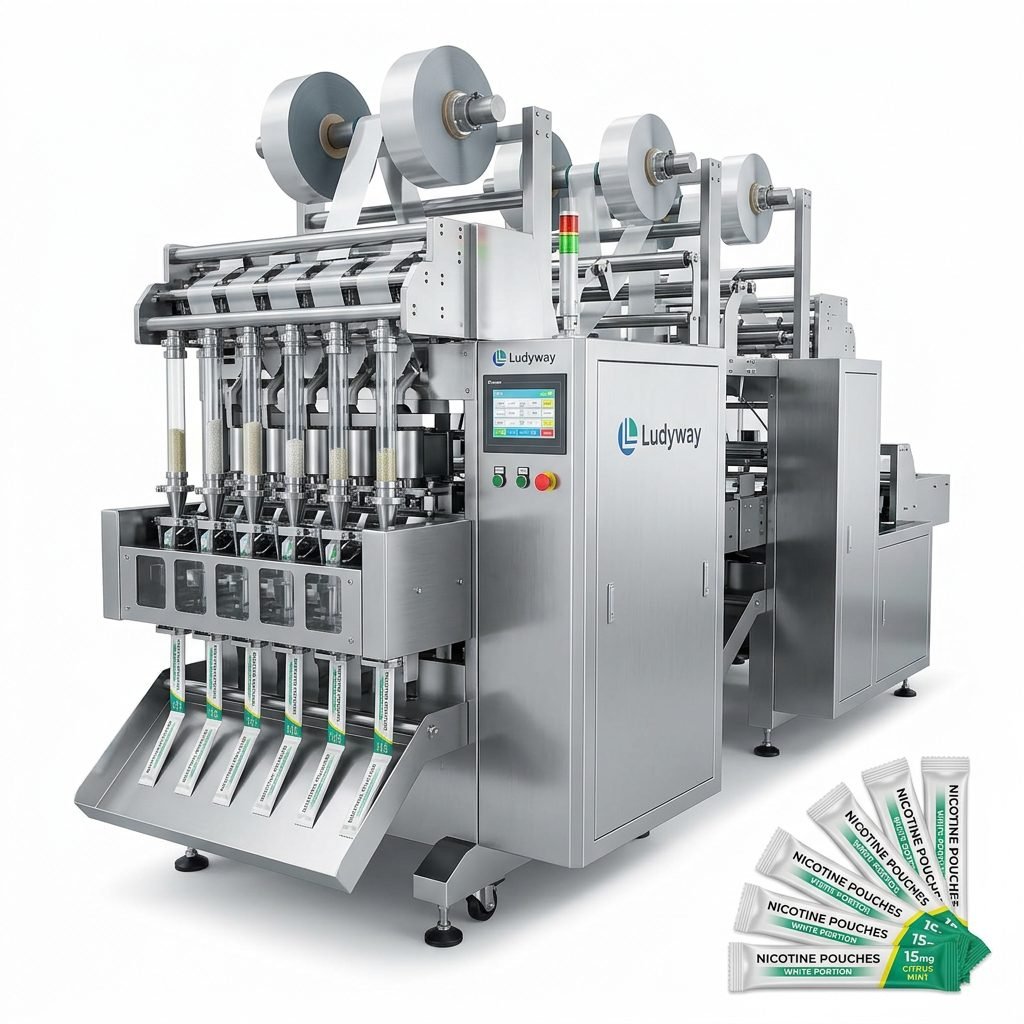
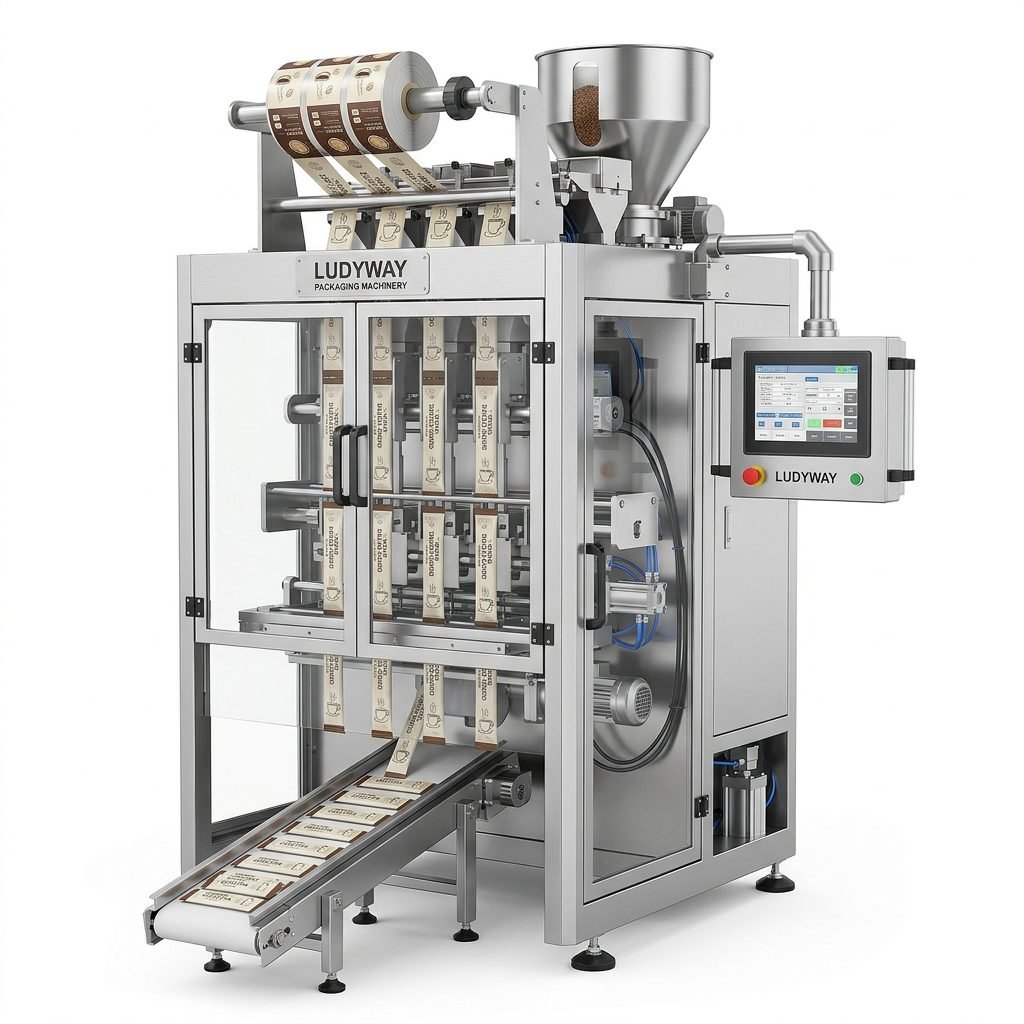
Stick pack machines produce narrow, tube-like packages ideal for single-serve powders, granules, and liquids. These machines are widely used for instant coffee, sugar, protein powder, and condiments. Multi-lane configurations can produce dozens of sticks simultaneously, achieving very high output rates. The vertical form-fill-seal (VFFS) process creates a triple-sealed package that provides excellent airtight protection when paired with appropriate barrier films.
Pouch Packaging Machines
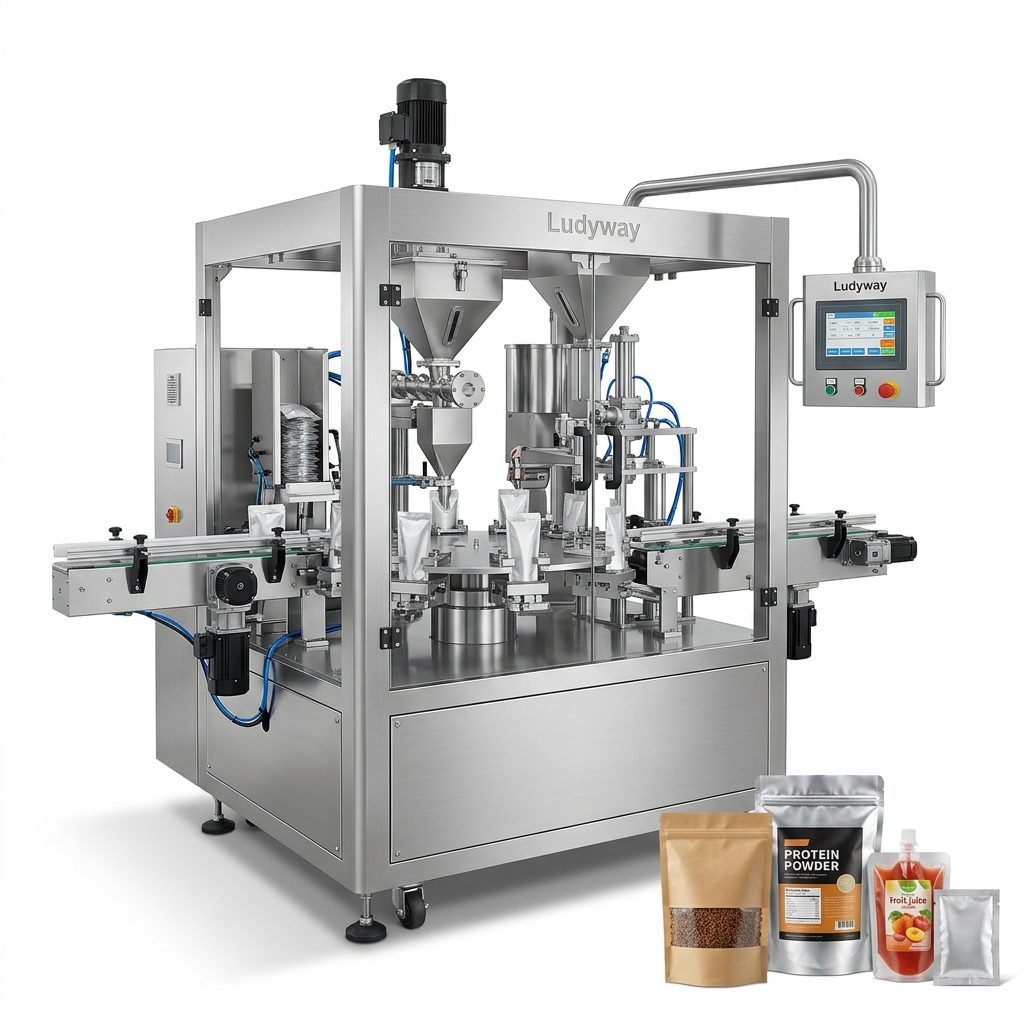
Premade pouch and form-fill-seal pouch machines handle larger package sizes, from small retail bags to bulk formats. Rotary and inline configurations offer different speed and flexibility trade-offs. Stand-up pouches with zipper closures are increasingly popular for products like nuts, dried fruits, and frozen foods, combining airtight sealing with consumer convenience. The PMMI packaging industry data shows continued growth in flexible pouch formats across multiple food categories.
Vacuum Packaging Machines
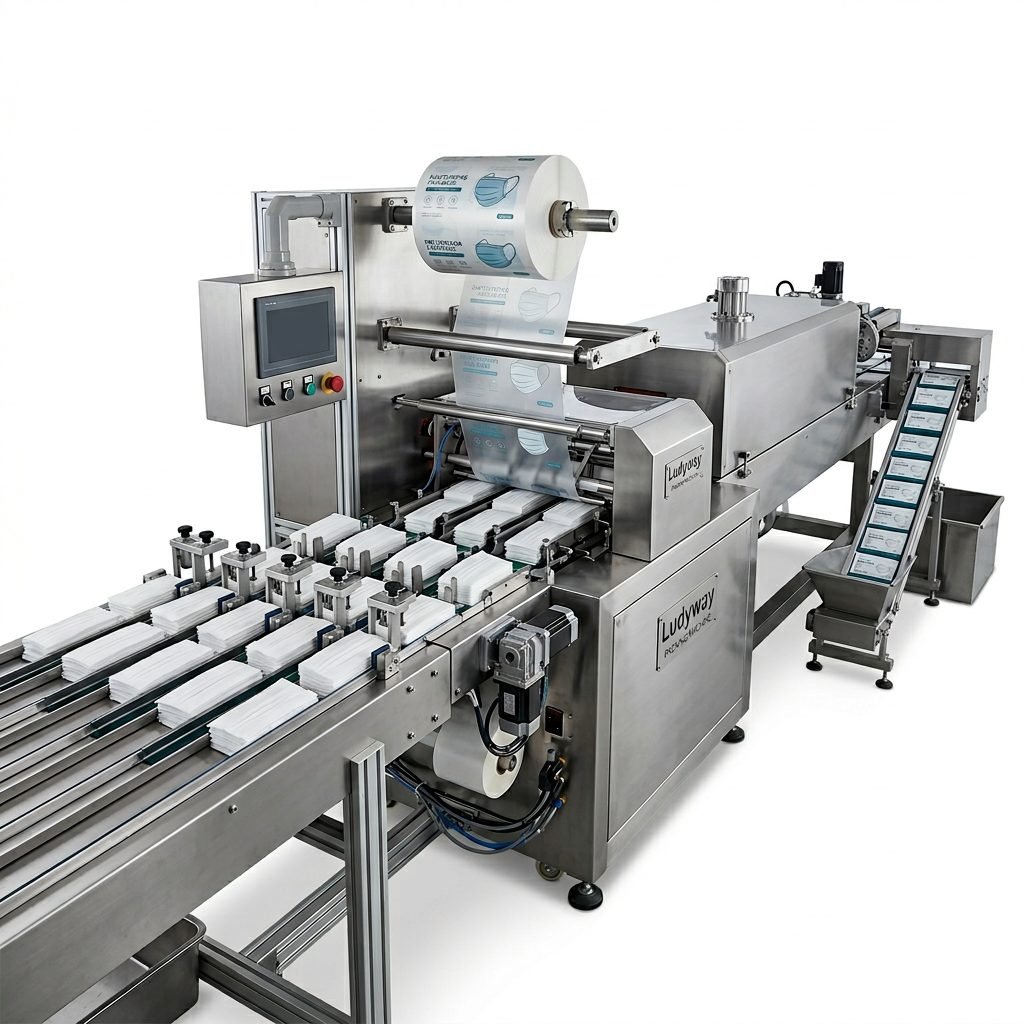
For products requiring the highest level of oxygen removal, vacuum packaging machines extract air from the package before sealing. These systems are essential for meat, cheese, and certain dried products where oxidation poses significant quality risks. Chamber vacuum machines, nozzle vacuum machines, and thermoforming systems each offer different capabilities depending on production volume and package format.

Key Features to Evaluate
Beyond the basic machine type, several technical features determine whether a packaging machine will meet your specific airtight requirements. Use the table below to compare critical factors across different machine options:
| Feature | Why It Matters | What to Look For |
|---|---|---|
| Sealing Technology | Determines seal integrity and airtight performance | Heat sealing with precise temperature control; ultrasonic options for sensitive products |
| Gas Flushing Capability | Displaces oxygen to extend shelf life | Nitrogen or CO₂ flushing systems with flow control and monitoring |
| Multi-Lane Configuration | Directly impacts production output | 4-12 lane options for sachet and stick pack formats |
| Film Compatibility | Must work with your chosen barrier materials | Support for aluminum laminates, metallized films, and multi-layer structures |
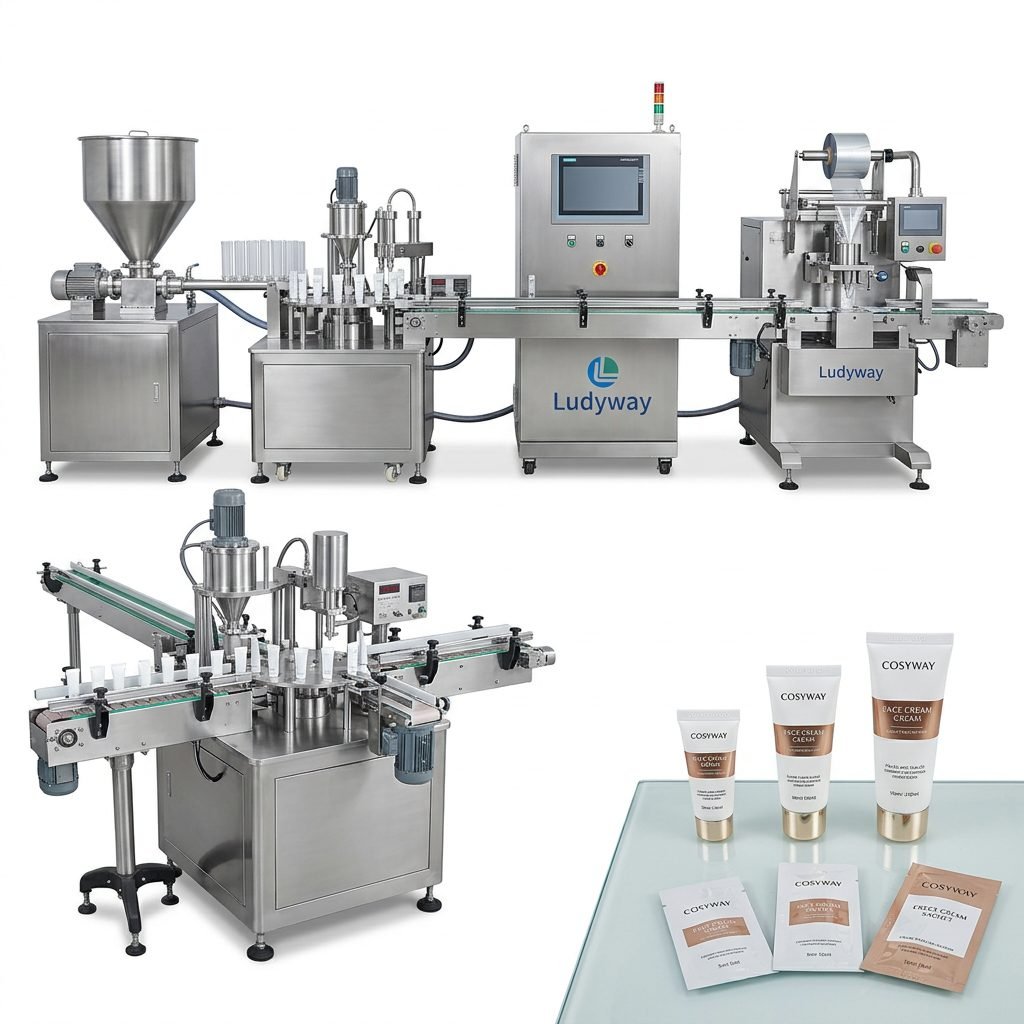
| Automation Level | Affects labor requirements and consistency | From semi-automatic to fully integrated turnkey lines |
| Quality Control Systems | Detects seal defects and fill errors | Checkweighers, vision inspection, metal detection integration |
Material Compatibility and Barrier Properties
The best packaging machine cannot compensate for the wrong film choice. Airtight food packaging typically relies on multi-layer laminates that combine strength, barrier properties, and sealability. Your machine should be tested with the specific film structure you intend to use. Key material characteristics to verify include oxygen transmission rate (OTR) and water vapor transmission rate (WVTR), both of which directly impact product shelf life.
Production Speed and Scalability
Production requirements vary dramatically from one manufacturer to another. A small-batch operation might need only 30-50 packages per minute, while high-volume producers often require 200-600+ packages per minute across multiple lanes. When evaluating speed, consider not just the machine’s maximum rated output but also its sustained production rate under real operating conditions. Also factor in changeover time between different product runs or package formats.
Industry-Specific Considerations
Different food sectors have unique airtight packaging needs. Understanding where your product fits can narrow down machine options considerably:
- Bakery and Snack Foods: Moisture barrier is often the priority. Modified atmosphere packaging (MAP) may be required for extended shelf life of products like bread, crackers, and pastries.
- Coffee and Tea: Oxygen and moisture protection are both critical. One-way degassing valves may be needed for freshly roasted coffee, while instant coffee requires complete moisture isolation.
- Dairy and Protein Powders: Hygroscopic products demand excellent moisture barrier films and often benefit from nitrogen flushing. Whey protein, milk powder, and nutritional supplements all fall into this category.
- Spices and Seasonings: Volatile oils and aromas require barrier films that prevent flavor loss. Small sachet formats are common for both retail and food service applications.
- Frozen Foods: Cold-temperature seal integrity is essential. Packaging must withstand freezing without seal failure or film cracking.
For regulatory guidance on food contact materials, manufacturers should reference FDA food packaging regulations to ensure compliance with applicable standards in their target markets.
Questions to Ask Before Buying
A systematic evaluation process helps avoid costly mistakes. Before contacting equipment suppliers, answer these questions about your production needs:
- What is your product’s sensitivity to oxygen, moisture, and light? This determines the barrier level required and whether gas flushing is necessary.
- What package format best serves your market? Stick packs, sachets, pouches, or vacuum bags each have different machine requirements.
- What is your target production volume? Daily or hourly output targets will guide lane count and automation level decisions.
- What packaging materials do you plan to use? Verify machine compatibility with your preferred film structures before committing.
- What level of automation does your facility need? Consider whether you need a standalone machine or a fully integrated line with filling, sealing, coding, and cartoning.
- What are your future growth plans? Choose equipment that can scale or be reconfigured as production volumes increase.
- What after-sales support is available? Technical support, spare parts availability, and operator training are critical for long-term success.
Making the Final Decision
After narrowing your options based on the factors above, the final selection often comes down to total cost of ownership, supplier capability, and real-world performance validation. Request sample runs with your actual product and packaging materials whenever possible. A machine that performs well in a demo may behave differently with your specific product characteristics, such as particle size distribution, bulk density, or oil content.
Pay close attention to seal integrity testing results from these trials. Even small inconsistencies in seal quality can lead to significant product waste, customer complaints, or food safety issues. Leading packaging machinery manufacturers provide comprehensive testing support before finalizing equipment specifications.
Conclusion
Choosing the right airtight food packaging machine requires careful evaluation of your product characteristics, packaging format, production volume, and long-term business goals. The investment extends beyond the initial equipment purchase to include operational efficiency, maintenance costs, and packaging material optimization. By systematically assessing the factors outlined in this guide—from sealing technology and gas flushing capability to material compatibility and automation level—you can select equipment that protects product quality, meets regulatory requirements, and supports your growth strategy.
With over 30 years of experience in the packaging industry, companies like Ludyway Machinery offer a broad range of automatic packaging equipment and integrated turnkey solutions designed for different products, packaging formats, and production requirements. Whether you need a single machine or a complete production line, working with an experienced packaging machinery partner can help ensure your investment delivers reliable, long-term performance. For further reading on packaging machinery standards and industry trends, explore resources available through the PMMI packaging industry resources portal.