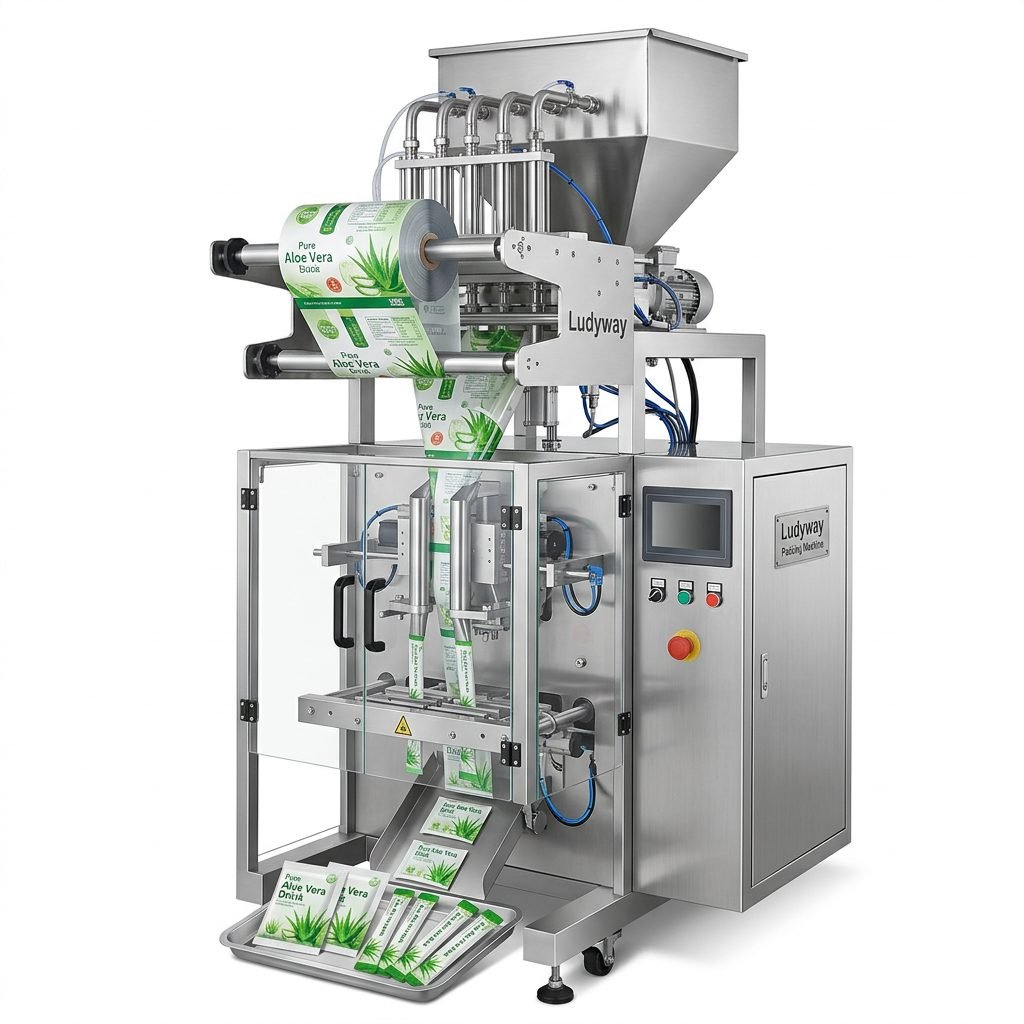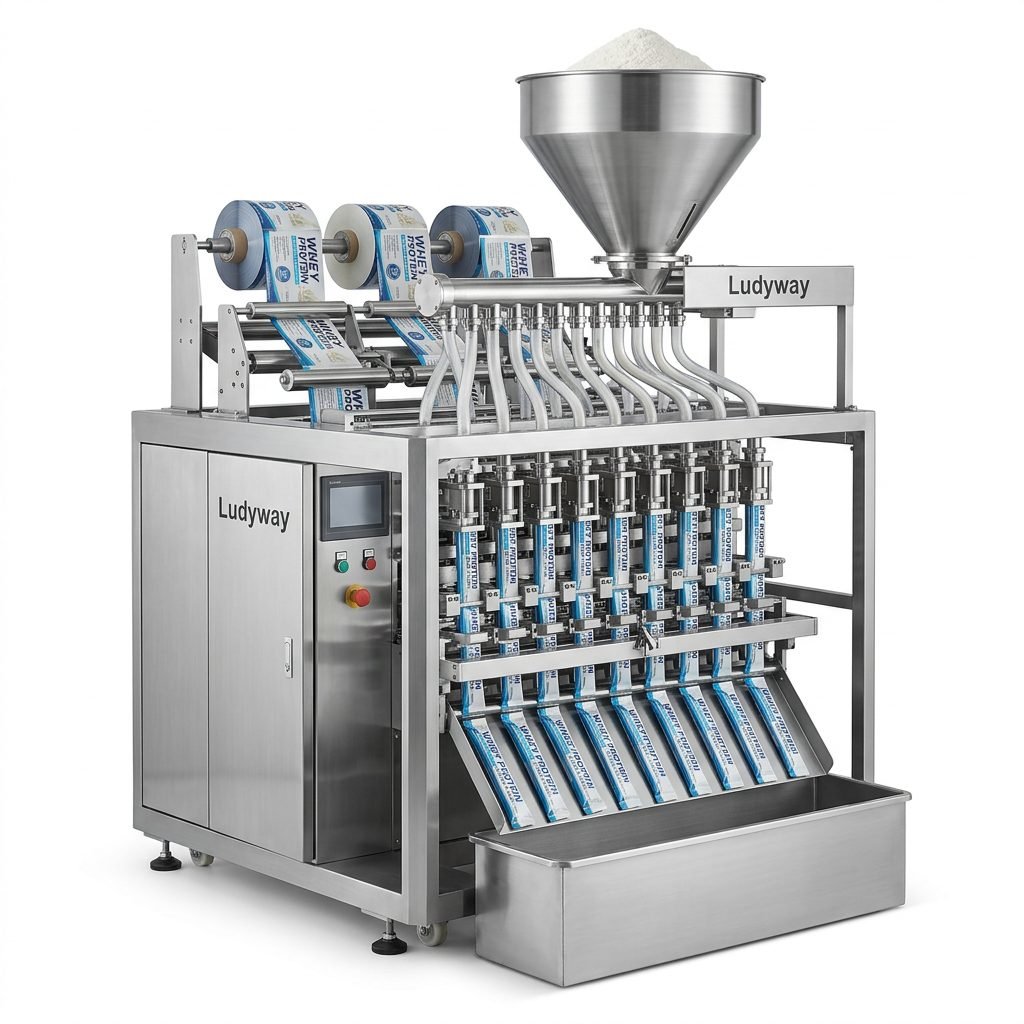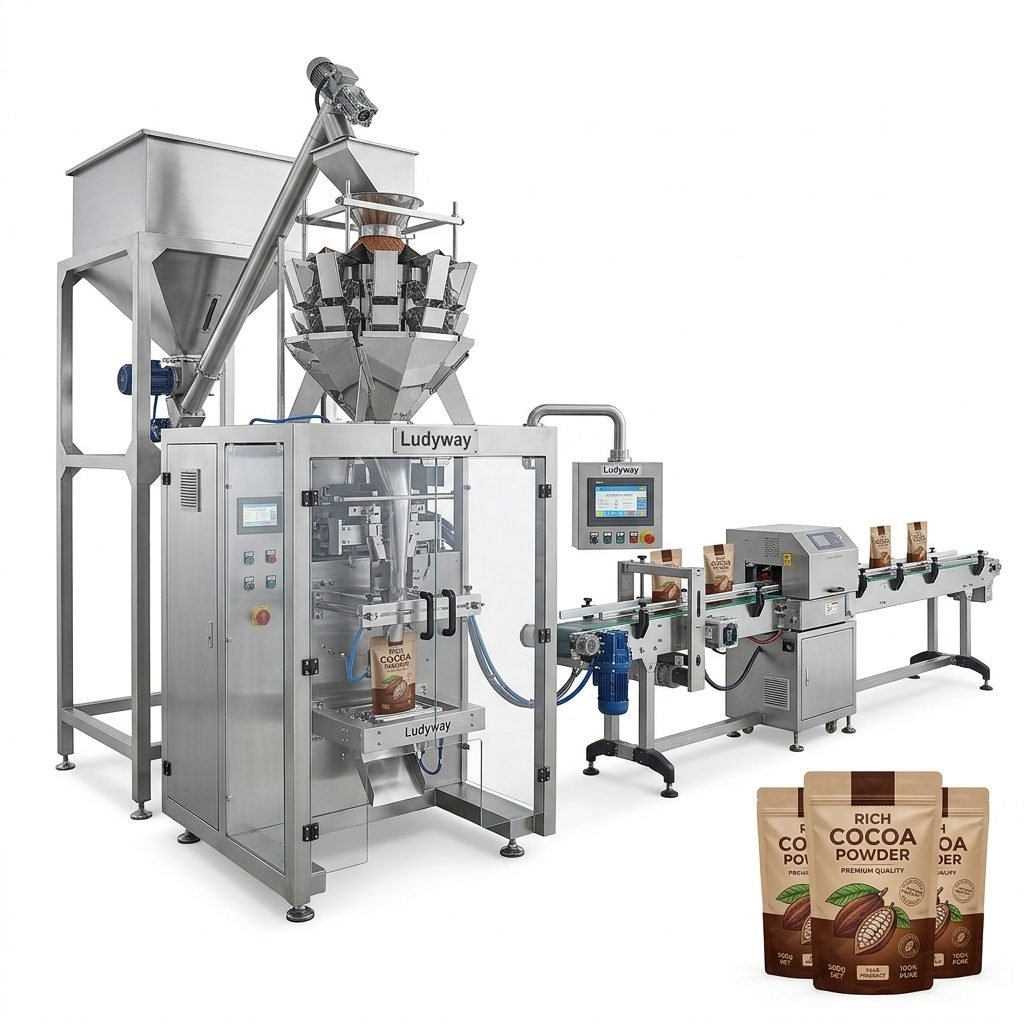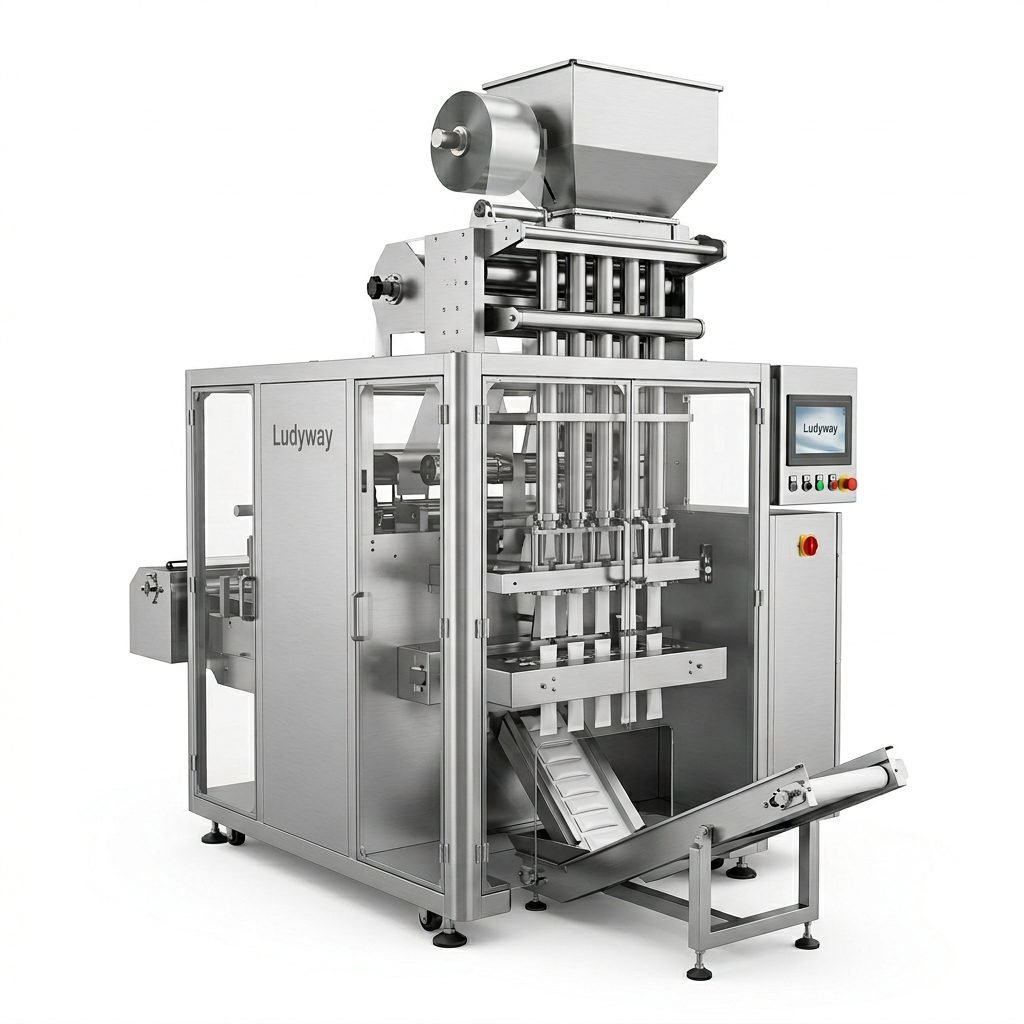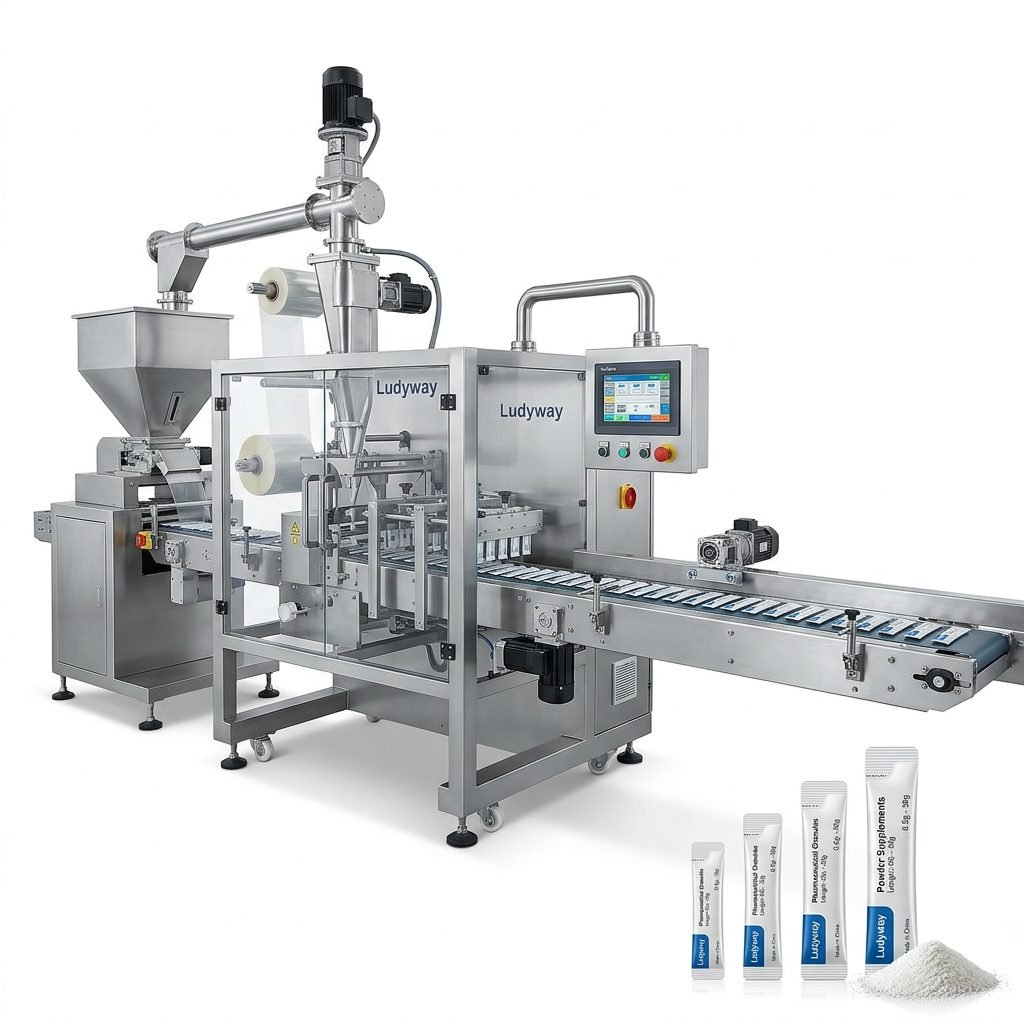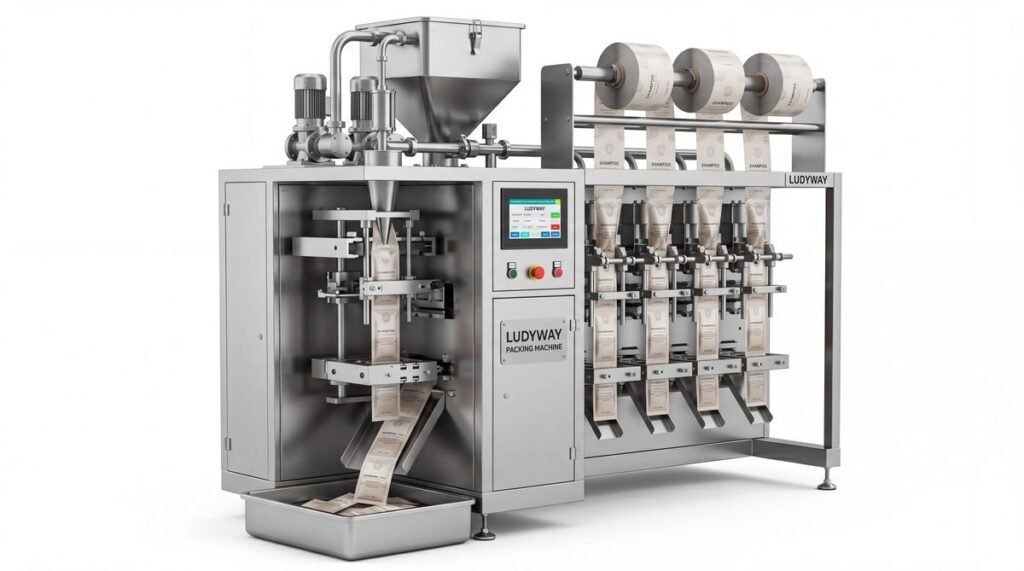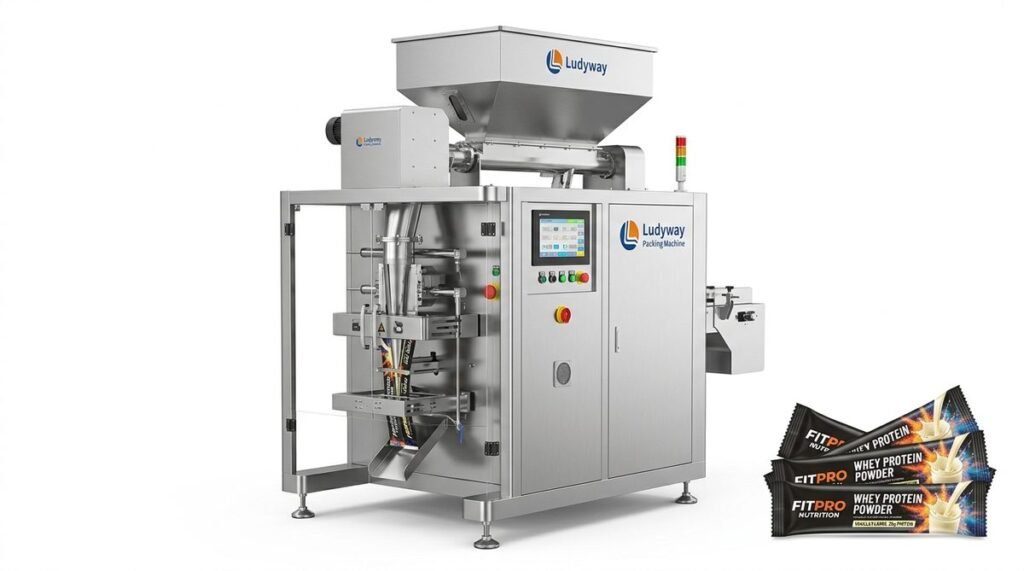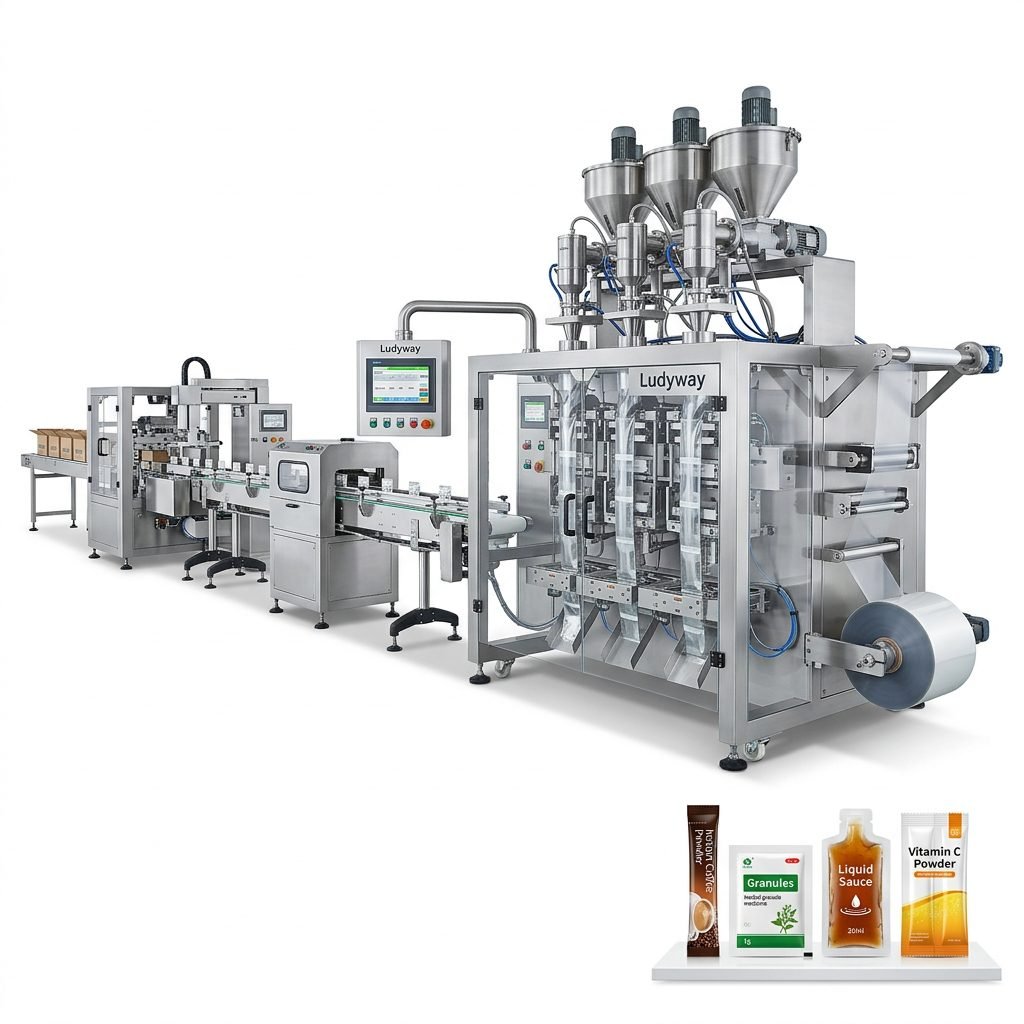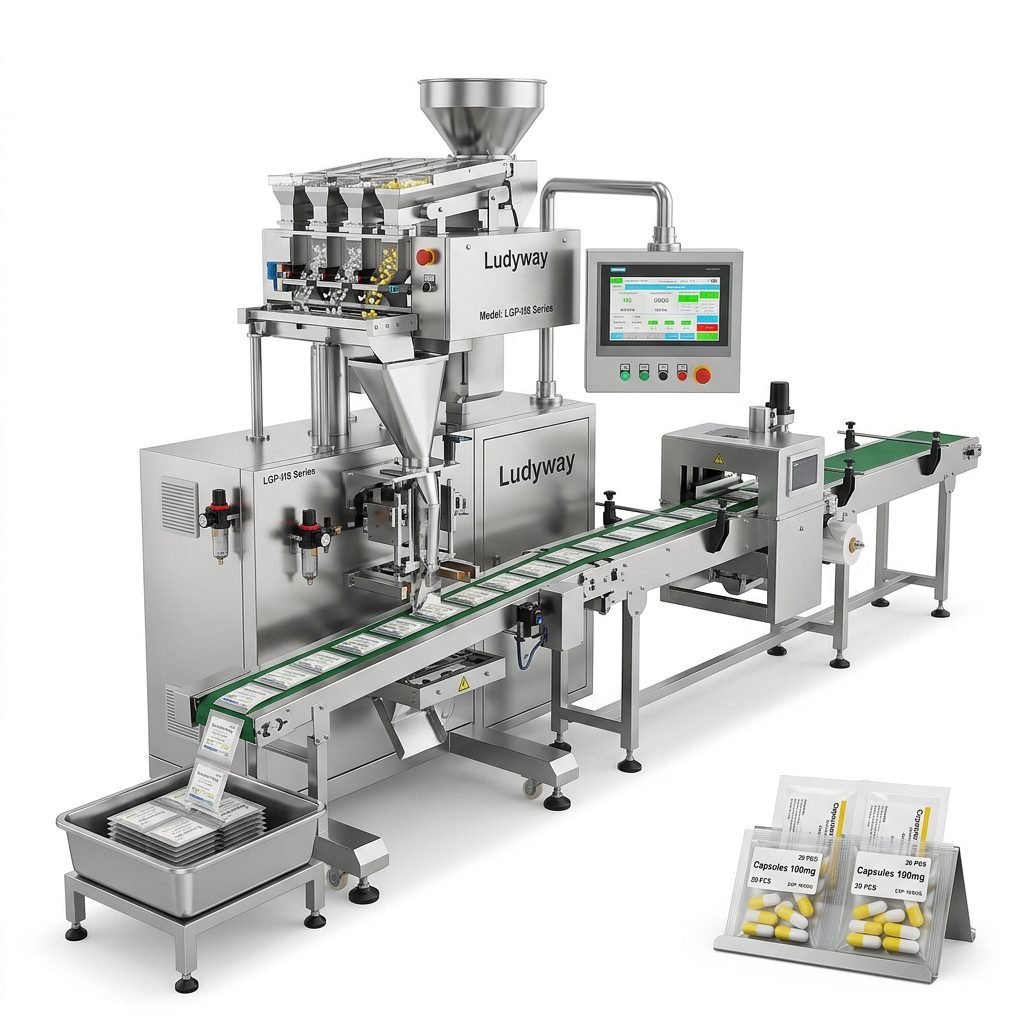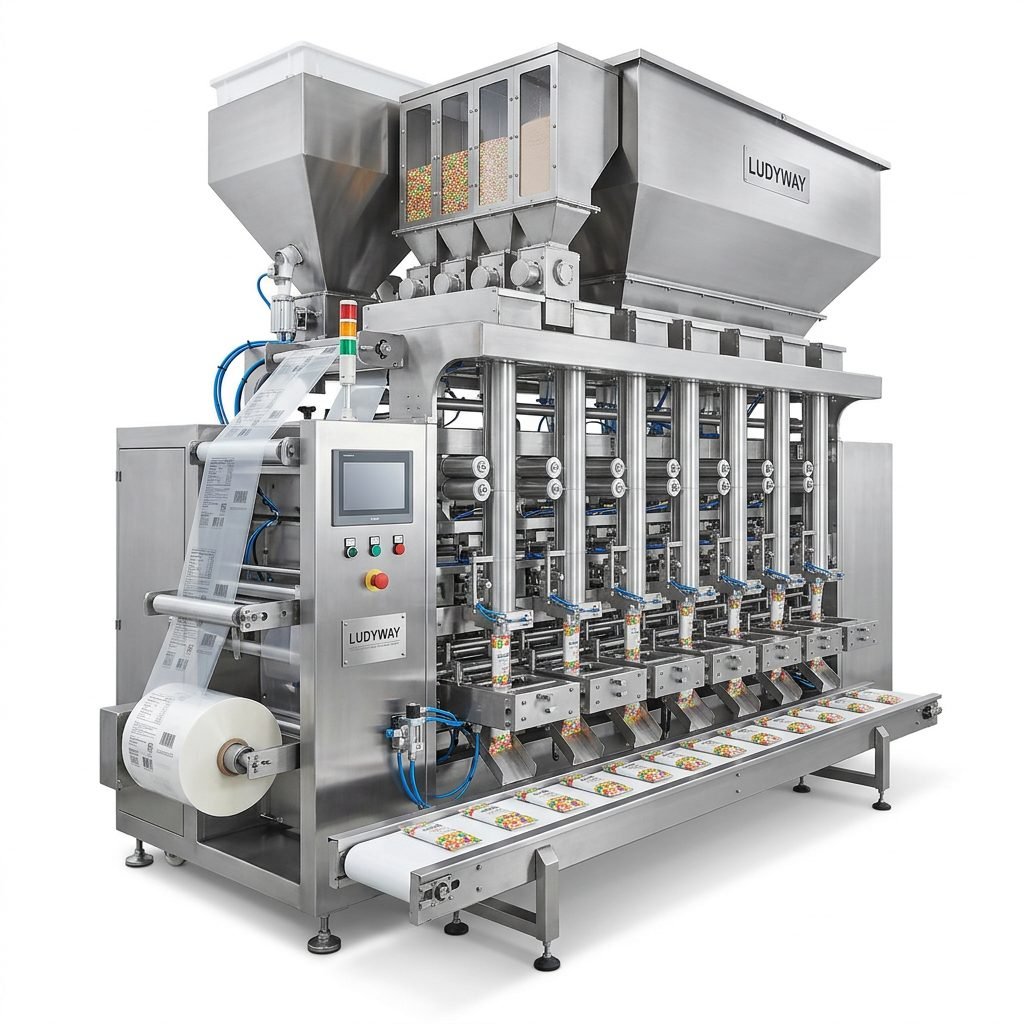
The confectionery industry in Asia is experiencing unprecedented growth, with global demand for packaged candies, chocolates, gummies, and snack bars rising sharply across both emerging and mature markets. As manufacturers scale up production to meet this demand, selecting the right confectionery packaging machine supplier becomes a critical business decision that directly impacts productivity, product quality, and long-term profitability. Among the many equipment providers in the region, one name consistently stands out for delivering reliable, high-performance packaging systems tailored to the unique needs of confectionery producers.
Choosing an Asian supplier for your confectionery packaging equipment offers distinct advantages — cost efficiency without compromising on engineering quality, shorter supply chains, faster after-sales support, and deep expertise in handling diverse product types ranging from sticky candies to delicate chocolate pieces. However, not all suppliers are equal. What truly sets a best-in-class supplier apart is the combination of manufacturing scale, technical innovation, international certifications, and a proven track record across multiple markets.
Unmatched Manufacturing Scale and Engineering Expertise
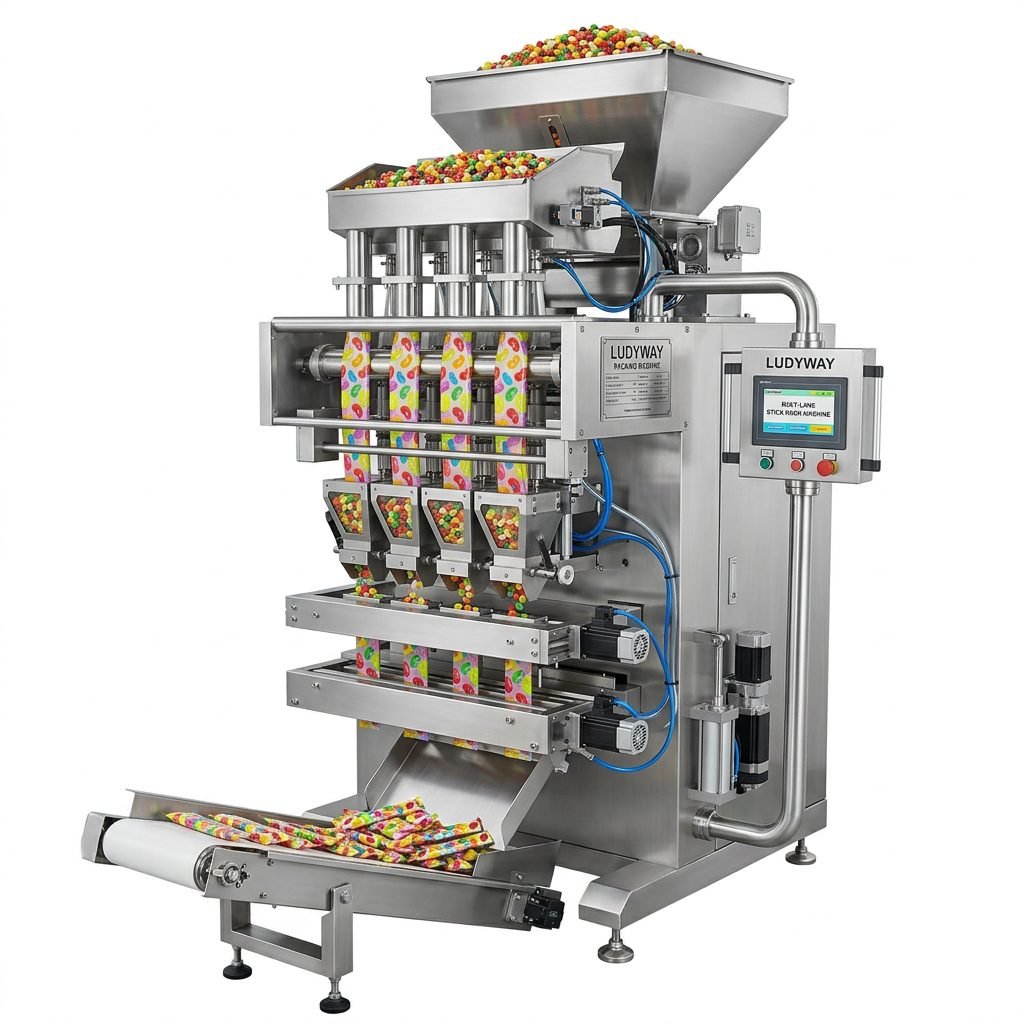
When evaluating a confectionery packaging machine supplier, manufacturing capability is one of the first factors to assess. A supplier with a 20,000㎡ modern production facility and over 200 manufacturing equipment units demonstrates the capacity to handle large-scale orders while maintaining consistent quality. Ludyway operates one of the largest packaging machinery manufacturing plants in China, supported by more than 30 years of industry experience and a team of 130+ professional packaging experts. This deep engineering bench ensures that every machine — from single-lane sachet packers to complex multi-lane stick pack systems — is designed, assembled, and tested to meet rigorous performance standards.
Comprehensive Product Range for Every Confectionery Application
Confectionery products come in an incredibly wide variety — hard candies, soft gummies, chocolate bars, lollipops, toffees, marshmallows, chewing gum, and many more. Each product type demands specific handling, feeding, and sealing technologies to ensure product integrity and packaging quality. A top-tier confectionery packaging machine supplier must offer a versatile range of equipment that can accommodate different product characteristics, packaging formats, and production speeds. The table below outlines key machine types and their applications:
| Machine Type | Best For | Packaging Format | Speed Range |
|---|---|---|---|
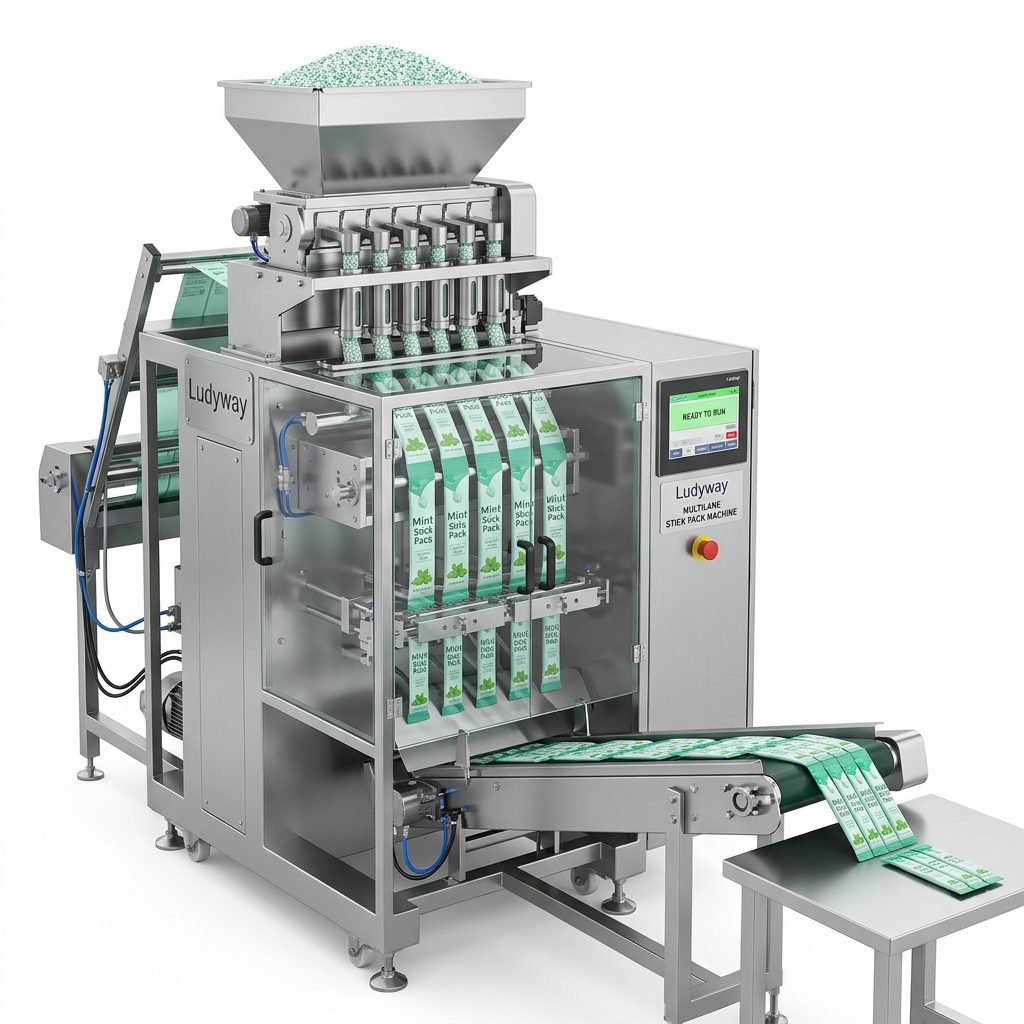
| Multi-Lane Stick Pack Machine | Powdered candies, drink mixes, sugar sticks | Stick packs (4-20 lanes) | Up to 800 packs/min |
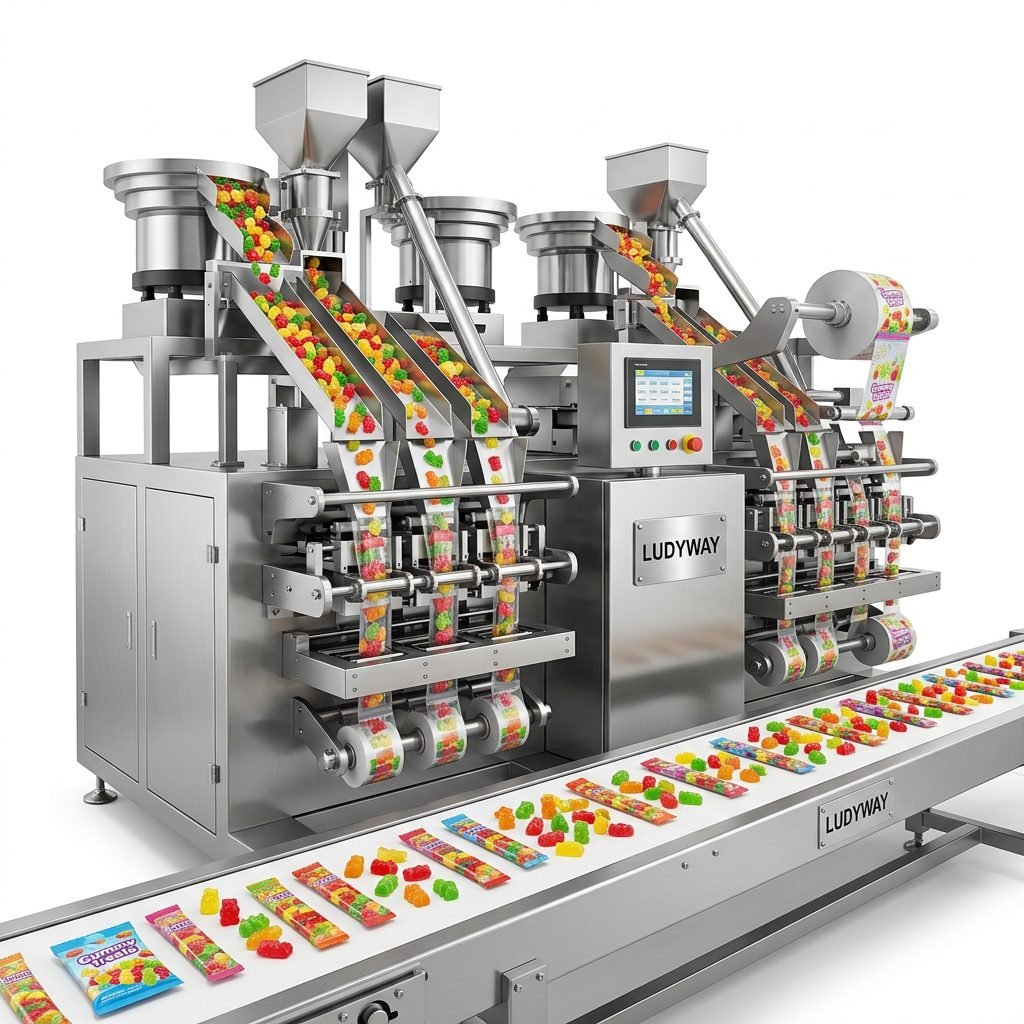
| Gummy & Jelly Packaging Line | Gummy bears, jelly beans, soft candies | Sachets, pouches, stick packs | Up to 600 packs/min |
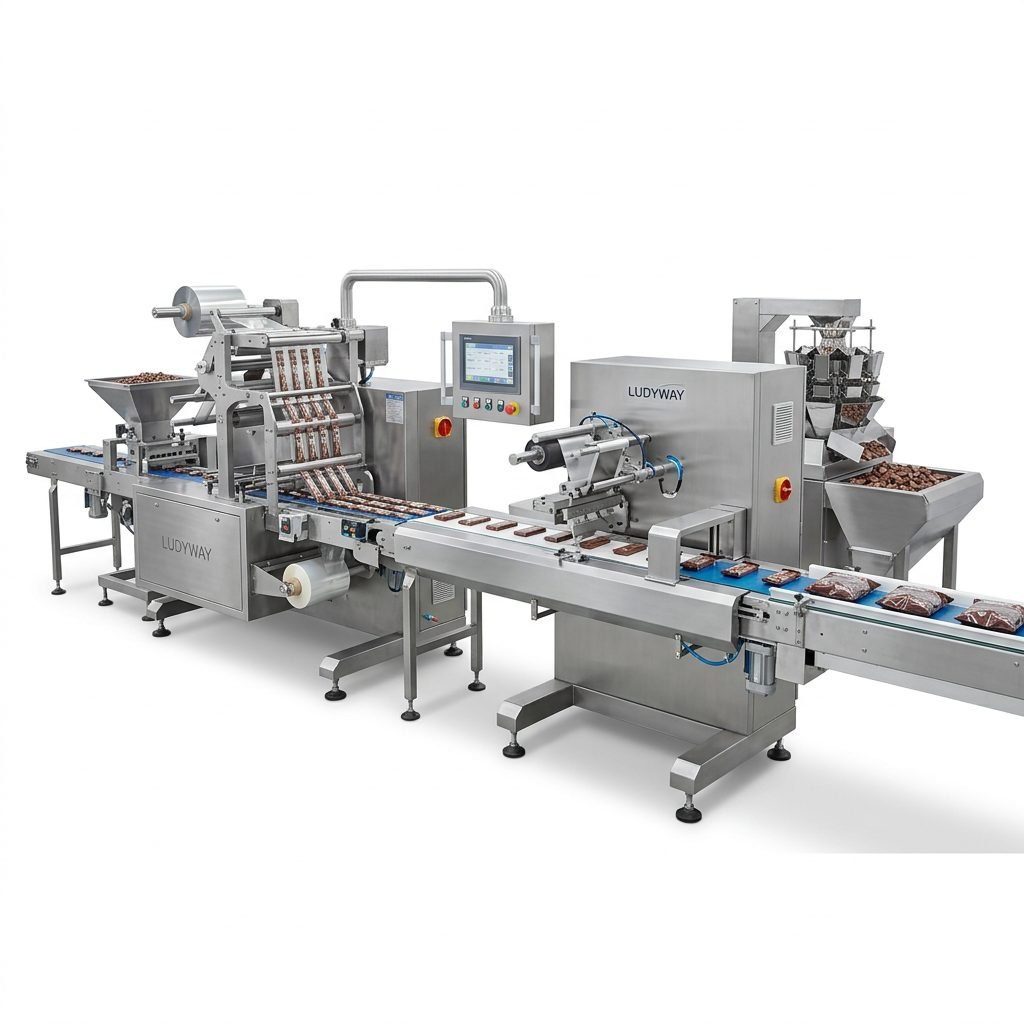
| Chocolate Bar Wrapping System | Chocolate bars, pieces, coated snacks | Flow wrap, sachet, stick pack | Up to 500 packs/min |
| Chewing Gum Packaging Machine | Gum sticks, pellets, coated gum | Stick packs, blister packs | Up to 700 packs/min |
| Hard Candy Sachet Packer | Mints, hard candies, lollipops | Sachets, stick packs | Up to 550 packs/min |
| Marshmallow Packaging System | Marshmallows, soft aerated confections | Pillow packs, sachets | Up to 400 packs/min |
Advanced Technology and Intelligent Automation
Modern confectionery packaging machine systems have evolved far beyond simple filling and sealing operations. Today’s intelligent packaging lines integrate precision weighing, automatic feeding, nitrogen flushing for extended shelf life, vision inspection for quality control, and robotic pick-and-place systems for secondary packaging. A supplier that offers turnkey solutions — from raw product handling through to cartoning and palletizing — provides significant value by reducing integration risks and ensuring seamless production workflows. Key technologies to look for include:
- Servo-driven multi-lane systems with independent lane control for maximum flexibility
- Automatic checkweighers and metal detectors integrated directly into the packaging line
- High-precision vibratory and auger fillers calibrated for confectionery granules and powders
- Gas flushing and modified atmosphere packaging capabilities for shelf-life extension
- Quick-changeover tooling that minimizes downtime between product runs
- IoT-enabled remote monitoring for predictive maintenance and real-time production analytics
International Quality Standards and Certifications
For confectionery manufacturers exporting to regulated markets such as the European Union, North America, and Japan, packaging equipment must comply with stringent food safety and machinery standards. A reputable Asian confectionery packaging machine supplier should hold relevant certifications and design equipment that meets or exceeds international requirements, including CE certification, ISO 9001 quality management standards, and FDA-compliant food contact materials. Equipment constructed with stainless steel frames, sanitary-grade conveyors, and easy-clean designs ensures compliance with GMP and HACCP protocols — essential requirements for any serious confectionery operation.
According to industry data from the PMMI State of the Industry Report, the global packaging machinery market continues to expand, with the confectionery and snack sectors showing particularly strong investment in automated packaging solutions. Similarly, the Flexible Packaging Association reports growing adoption of multi-lane stick pack and sachet formats for single-serve confectionery products — a trend that aligns perfectly with the capabilities of advanced Asian packaging machinery manufacturers.
Cost-Effectiveness Without Compromise
One of the most compelling reasons to choose an Asian confectionery packaging machine supplier is the significant cost advantage. However, cost-effectiveness should never come at the expense of quality or durability. The best suppliers leverage economies of scale, efficient supply chains, and deep manufacturing expertise to deliver equipment that competes with — and often exceeds — the performance of European counterparts at a fraction of the price. Key cost benefits include:
- Lower initial capital investment with faster ROI timelines
- Reduced shipping and logistics costs compared to long-distance overseas suppliers
- Competitive spare parts pricing with readily available inventory
- Affordable customization and application-specific engineering
- Lower total cost of ownership over the equipment lifecycle
Global Service Network and Responsive Support
Even the most reliable confectionery packaging machine requires professional installation, operator training, and occasional technical support throughout its service life. A supplier that serves customers in over 100 countries and regions demonstrates not only global reach but also the organizational capability to provide responsive after-sales service wherever your facility is located. Look for suppliers that offer remote video assistance, on-site commissioning by experienced engineers, comprehensive spare parts catalogs, and multilingual technical documentation. These support capabilities are just as important as the machine specifications themselves when evaluating long-term supplier partnerships.
Customization and Future-Proofing Your Investment
No two confectionery manufacturers have identical requirements. Your confectionery packaging machine supplier should be willing and able to customize equipment to your specific product characteristics, packaging material preferences, production layout constraints, and throughput targets. Whether you need a dedicated single-product line or a flexible multi-product system capable of handling various confectionery formats, the right supplier will engineer a solution that meets your current needs while allowing for future expansion. Modular machine designs that support additional lanes, upgraded feeding systems, and integration with downstream equipment protect your investment as your business grows.
Key Factors When Selecting Your Confectionery Packaging Machine Partner
- Manufacturing footprint and production capacity — can they deliver on time?
- Range of machine models and configurations — do they have the right solution for your product?
- International certifications and compliance documentation — will the equipment pass regulatory inspection?
- Customer references and case studies — what do other confectionery manufacturers say about their experience?
- After-sales support infrastructure — how quickly can you get help when you need it?
- Parts availability and lead times — are critical spares kept in stock?
- Warranty terms and service agreements — what level of protection is included?
For confectionery manufacturers seeking a reliable, high-performance packaging machinery partner in Asia, the combination of engineering depth, manufacturing scale, international experience, and customer-focused service makes all the difference. As the packaging machinery market continues its strong growth trajectory, partnering with an established and forward-thinking supplier positions your business for sustained success in the competitive global confectionery market. With exports projected to surpass RMB 500 million in 2025 and targeting RMB 1 billion by 2026, the trajectory speaks for itself — choosing the right supplier today is an investment in your production capabilities for years to come.
Learn more about industry standards and market trends from these authoritative resources: