Investing in a double chamber vacuum packing machine is a significant decision for food processors, pharmaceutical manufacturers, and industrial packaging operations. The right equipment can dramatically extend product shelf life, reduce waste, and improve operational efficiency. However, with numerous configurations, chamber sizes, and vacuum pump technologies available, selecting the optimal machine requires a clear understanding of your production needs, product characteristics, and long-term operational goals.
This guide walks you through the essential factors to evaluate before purchasing a double chamber vacuum packing machine, helping you make an informed investment that aligns with your packaging requirements.
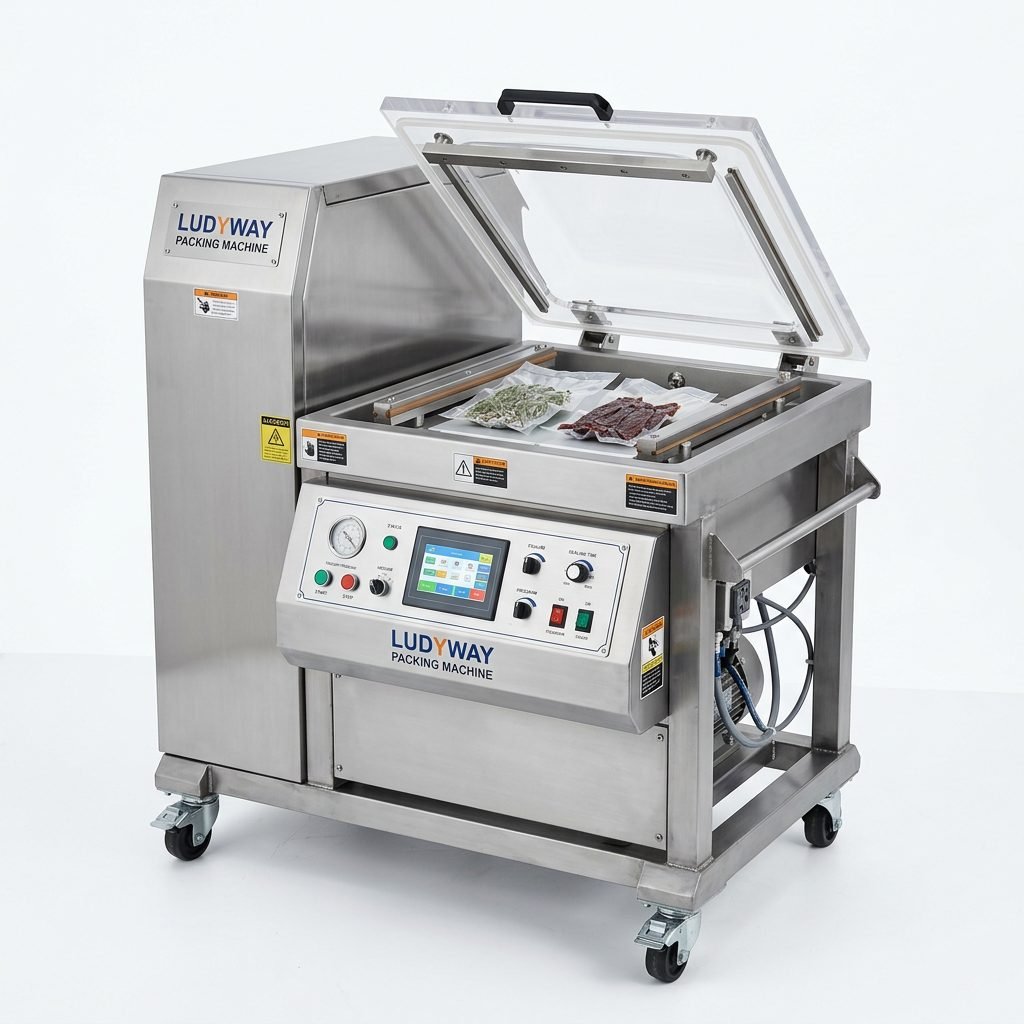
Understanding How a Double Chamber Vacuum Packing Machine Works
A double chamber vacuum packing machine operates by placing products into vacuum bags positioned inside one of two alternating chambers. When the lid closes, the vacuum pump extracts air from the chamber and the bag, creating a low-oxygen environment. Once the desired vacuum level is reached, the bag is heat-sealed, and air is reintroduced into the chamber. The dual-chamber design allows operators to load one chamber while the other is under vacuum, enabling near-continuous packaging cycles and significantly higher throughput compared to single-chamber models.
Key Factors to Evaluate Before Purchasing
Choosing the right machine involves more than comparing technical specifications. The following factors will help you narrow down the options and select equipment that matches your specific application.
1. Chamber Dimensions and Product Size Compatibility
The internal chamber dimensions directly determine the maximum bag size and product volume you can process. Measure your largest product and bag configuration, then add buffer space to ensure proper positioning and sealing. Chamber depth is particularly important for bulky or irregularly shaped items. A machine with insufficient chamber height may crush delicate products or prevent proper lid closure. Always verify the usable chamber area, as the sealing bar position can reduce the effective space within the chamber.
2. Vacuum Pump Type and Performance
The vacuum pump is the core component affecting cycle speed, ultimate vacuum level, and long-term reliability. Different pump technologies offer distinct advantages depending on your application:
| Pump Type | Advantages | Best Suited For |
|---|---|---|
| Oil Rotary Vane Pump | High vacuum level, fast pump-down time, durable | Heavy-duty production, high moisture products, continuous operation |
| Dry Scroll Pump | Oil-free operation, low maintenance, clean vacuum | Pharmaceutical, electronics, sensitive products requiring contamination-free environments |
| Oil Ring Pump | Handles moisture well, robust | Products with high liquid content, marinade packaging |
| Venturi System | Simple design, low cost, no moving parts | Low-volume applications, limited budget scenarios |
3. Sealing Bar Configuration and Quality
The sealing system determines package integrity and production speed. Look for machines with adjustable sealing time and temperature controls to accommodate different bag materials and thicknesses. Sealing bar length should match your widest bag size, and some models offer dual sealing bars per chamber to process multiple smaller bags simultaneously. Silicone or PTFE-coated sealing bars provide better release properties and longer service life, reducing maintenance frequency.
4. Control System and Programmability
Modern double chamber vacuum packing machines feature digital control panels that allow operators to store multiple programs for different products. This capability is valuable when packaging items with varying requirements—for example, delicate baked goods versus dense meat cuts. Key programmable parameters include vacuum time, gas flush duration (for modified atmosphere packaging), sealing time, and cooling time. Advanced models may include memory for storing and recalling dozens of preset programs, streamlining changeovers between production runs.
5. Construction Materials and Build Quality
Machine construction directly impacts hygiene, durability, and compliance with industry regulations. Stainless steel chambers and body construction are standard for food and pharmaceutical applications due to corrosion resistance and ease of cleaning. 304 or 316L stainless steel grades offer superior chemical resistance for harsh cleaning agents. Examine the quality of welds, hinge mechanisms, and lid construction, as these components experience significant mechanical stress during daily operation.
6. Production Volume and Duty Cycle
Estimate your daily or hourly packaging volume to determine the required machine capacity. A double chamber machine’s throughput depends on chamber size, pump speed, and operator efficiency. Cycle times typically range from 20 to 60 seconds, influenced by the vacuum pump capacity and chamber dimensions. For higher-volume operations, consider machines with larger chambers, faster pumps, or the ability to use multiple bags per cycle. Understanding your duty cycle requirements helps prevent premature wear from overloading the equipment beyond its design specifications.
Comparing Machine Specifications: What the Numbers Mean
When reviewing technical datasheets, certain specifications carry more practical weight than others. Here is how to interpret the key metrics:
| Specification | What to Look For | Impact on Operation |
|---|---|---|
| Ultimate Vacuum Pressure | 0.5 – 5 mbar typical | Lower pressure means better air removal; critical for extended shelf life |
| Pump Flow Rate | 16 – 300 m³/h depending on size | Higher flow rate reduces cycle time; match to chamber volume |
| Sealing Bar Width | 3 – 10 mm | Wider seals provide stronger closure; narrow seals suit lightweight pouches |
| Chamber Volume | Measured in liters | Must accommodate product plus bag with clearance for proper vacuum action |
| Power Requirements | Single-phase or three-phase options | Verify compatibility with facility electrical infrastructure |
Modified Atmosphere Packaging (MAP) Capability
Many double chamber machines offer gas flush or modified atmosphere packaging functionality. This feature injects an inert gas mixture—typically nitrogen, carbon dioxide, or a blend—into the bag after vacuum extraction and before sealing. MAP is essential for products that would be crushed under a hard vacuum or that benefit from protective gas atmospheres. If your application involves fresh produce, baked goods, or delicate prepared foods, verify that the machine includes a gas flush port and compatible control system. The ability to precisely regulate gas flow and timing ensures consistent package quality across production runs.
Industry-Specific Considerations
Different industries impose unique requirements on vacuum packaging equipment. Understanding your sector’s standards will help narrow the selection:
- Food Processing: Prioritize stainless steel construction, easy-to-clean surfaces, and compliance with HACCP principles. Machines should support washdown environments and include sanitary design features such as sloped surfaces and minimal crevices.
- Pharmaceutical Packaging: Look for oil-free vacuum pumps to prevent contamination risk, validated sealing parameters, and documentation supporting GMP compliance. Integration with ISO 11607 standards for sterile barrier systems may be required.
- Industrial and Chemical Products: Chemical-resistant sealing gaskets and compatible materials are essential. Verify compatibility with the specific bag materials required for chemical resistance or barrier properties.
- Electronics and Components: ESD-safe configurations and moisture-sensitive device packaging require specific vacuum and sealing characteristics to protect components during storage and transport.
Evaluating Total Cost of Ownership
Purchase price alone does not reflect the true cost of a double chamber vacuum packing machine. Consider these ongoing operational expenses that accumulate over the equipment’s service life:
- Vacuum pump oil and filter changes – oil-sealed pumps require regular maintenance every 500–2,000 operating hours
- Sealing bar and Teflon tape replacement – consumable wear items that affect seal quality
- Gasket and lid seal replacement – worn seals compromise vacuum performance and increase cycle times
- Energy consumption – pump motor power directly impacts electricity costs over thousands of cycles
- Spare parts availability – reliable access to replacement components minimizes downtime
- Technical support and service – remote assistance and on-site service capabilities protect your investment
Machines designed for easier maintenance and supported by responsive technical service providers typically demonstrate lower long-term ownership costs. Examining specifications from established manufacturers like Flexible Packaging Association resource guides can help identify quality benchmarks when evaluating suppliers.
Installation and Facility Requirements
Before finalizing your selection, confirm that your facility can accommodate the machine’s physical and utility requirements. Verify electrical supply compatibility—some high-capacity vacuum pumps require three-phase power that may not be available in all locations. Consider compressed air availability if the machine uses pneumatic controls or gas flush systems. Adequate ventilation around the equipment is necessary for proper cooling, particularly for oil-sealed pumps that generate heat during continuous operation. Adequate clearance for loading and unloading, as well as maintenance access, should be factored into your floor plan.
Selecting a Reliable Packaging Machinery Partner
The longevity and performance of your vacuum packaging equipment depend significantly on the manufacturer’s engineering capabilities and support infrastructure. A manufacturer with comprehensive in-house manufacturing, engineering expertise, and global technical service can provide integrated solutions rather than simply delivering a machine. When evaluating suppliers, consider their project lifecycle support—from initial machine selection and packaging solution design through installation, commissioning, operator training, and ongoing spare parts availability.
Ludyway Machinery, with over 30 years of experience and a 20,000-square-meter manufacturing facility, develops automated packaging equipment and complete packaging systems for manufacturers across more than 100 countries. The company’s approach combines mechanical design, automation technology, and application engineering to configure machines according to specific product characteristics and production requirements, ensuring that your double chamber vacuum packing machine investment aligns with your operational goals.
Making the Final Decision
After evaluating chamber dimensions, pump technology, sealing capabilities, construction quality, and total cost factors, you can create a shortlist of machines that meet your core requirements. Whenever possible, request product samples processed on the actual machine model under consideration. Evaluating sealed packages for vacuum integrity, seal strength, and appearance provides insight that technical specifications cannot capture. This practical step helps confirm that the equipment delivers the packaging quality your products and customers demand.
For additional guidance on packaging machinery selection and industry best practices, resources from organizations such as PMMI’s State of the Industry reports and FDA food contact substance regulations offer valuable perspectives on packaging compliance and market trends that may influence your equipment requirements.