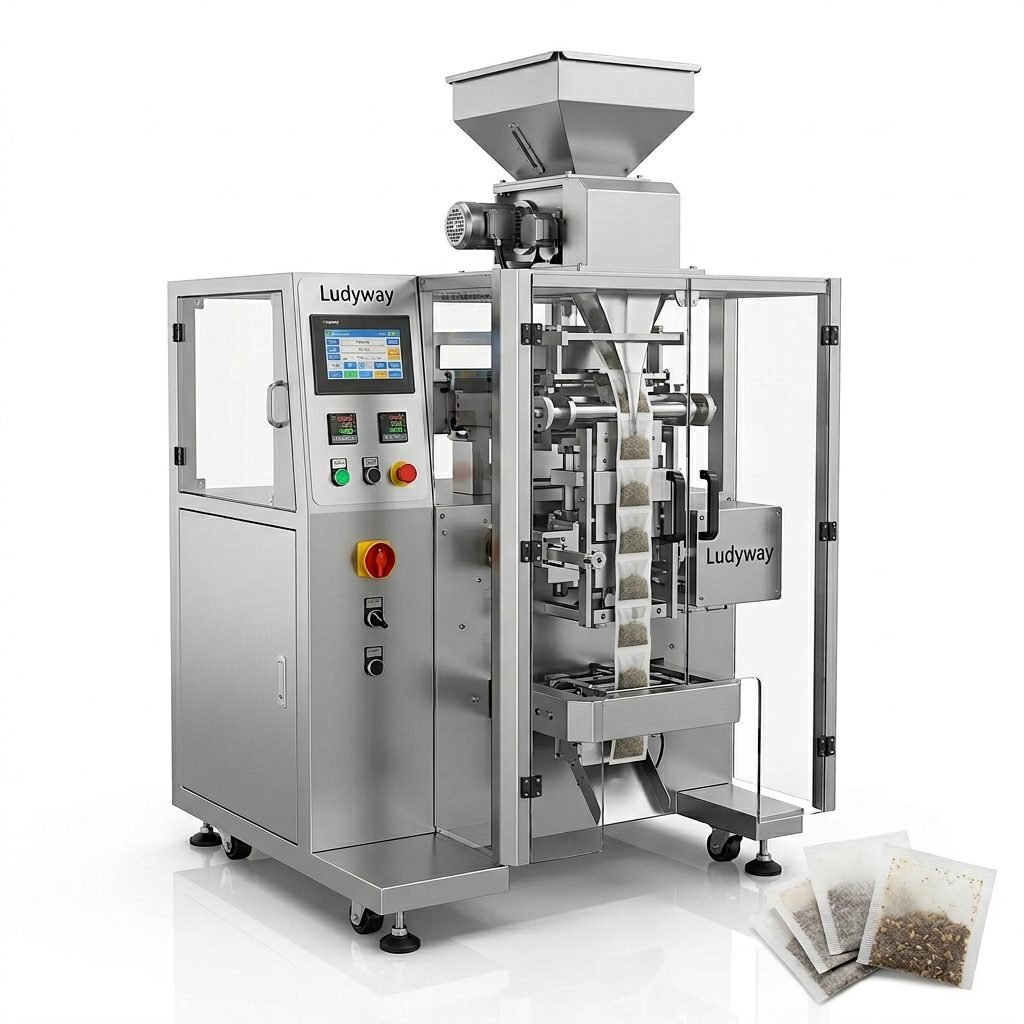
Investing in a pharmacy pill packaging machine is a strategic decision that directly impacts production efficiency, product integrity, and regulatory compliance. Whether you are upgrading an existing line or building a new facility, understanding the key selection criteria is essential. This guide walks you through the critical factors to evaluate before making your purchase.
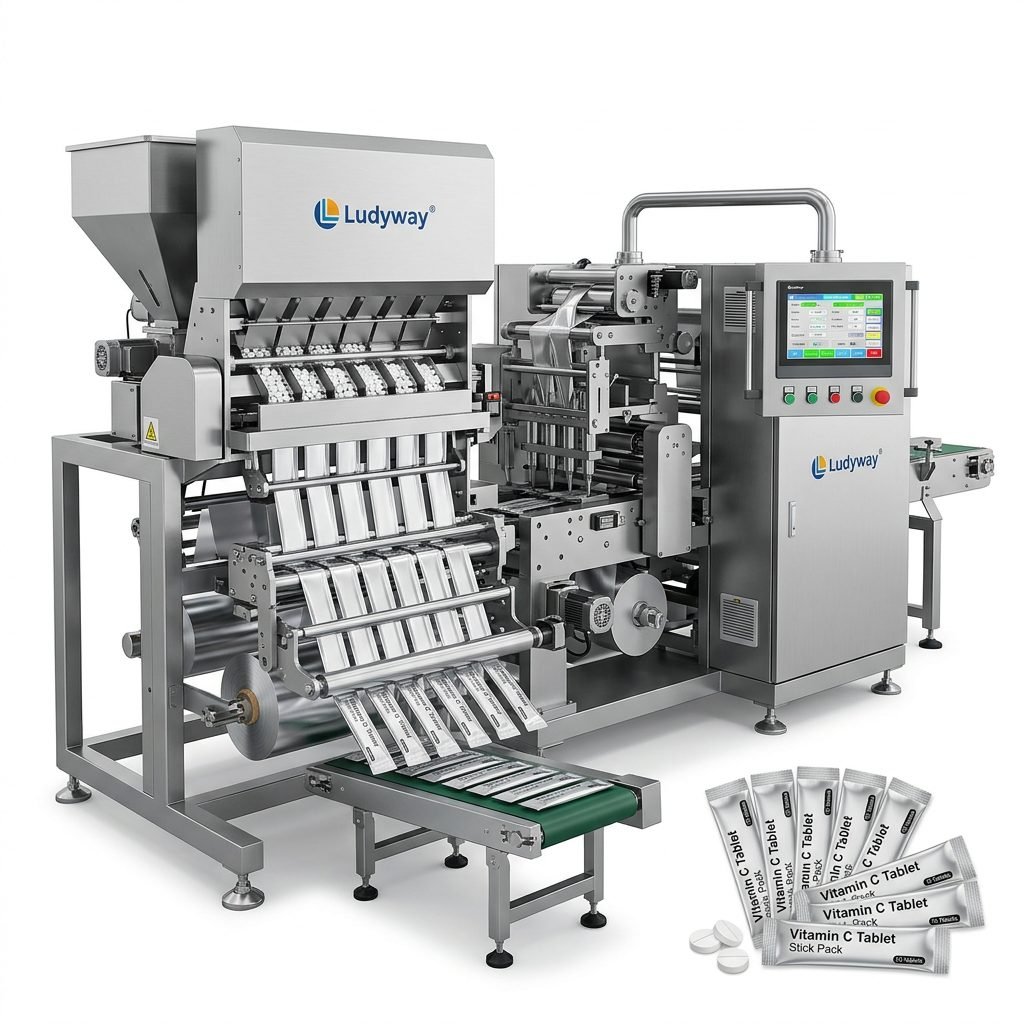
1. Understand Your Product and Packaging Format Requirements
Before evaluating machinery, define your product characteristics and desired packaging format. Pharmaceutical products come in diverse forms — tablets, capsules, pills, granules, and powders — each requiring specific handling and filling mechanisms.
- Product type: Tablets and capsules demand gentle handling to prevent breakage, while powders require precise dosing and dust control.
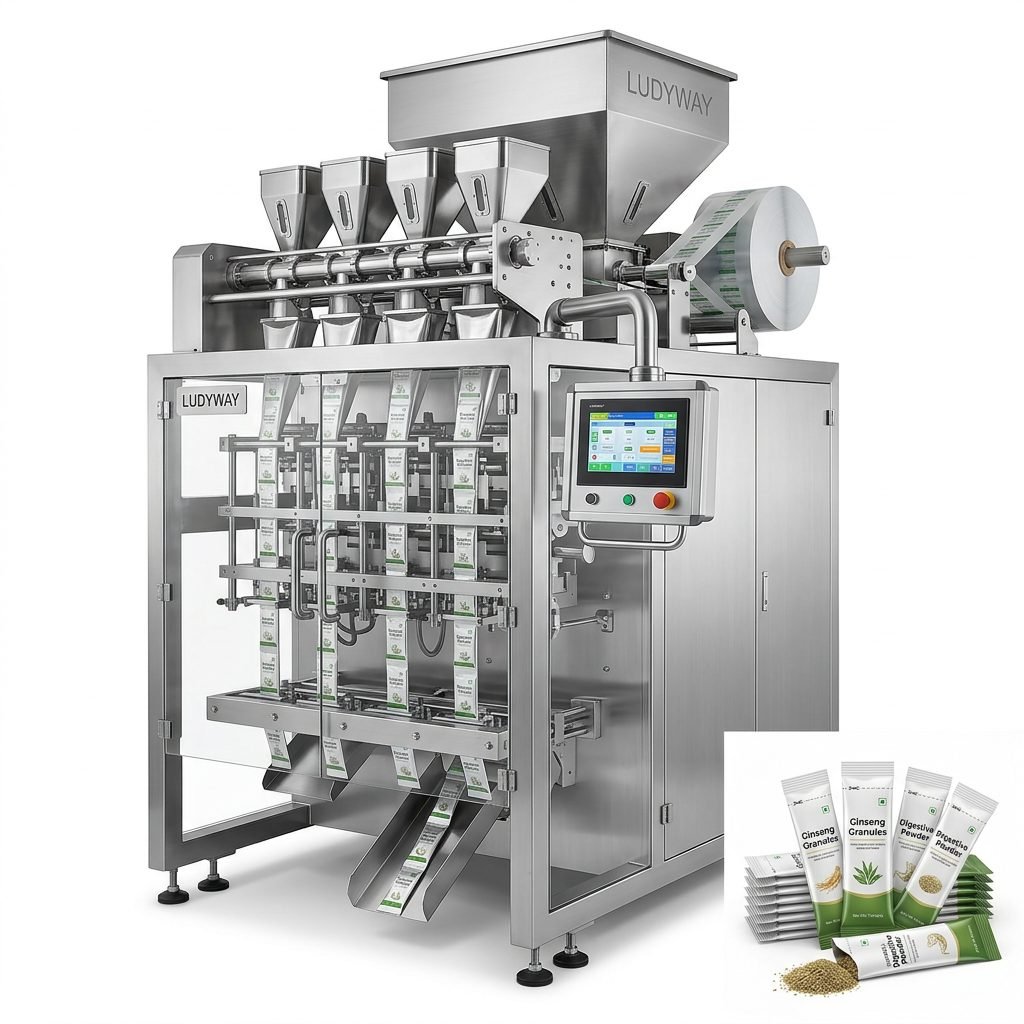
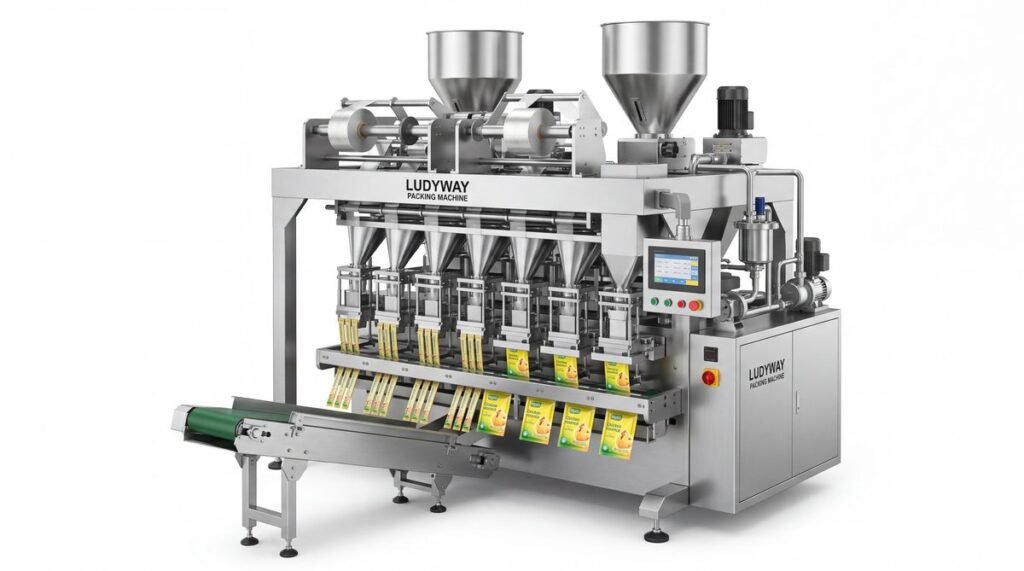
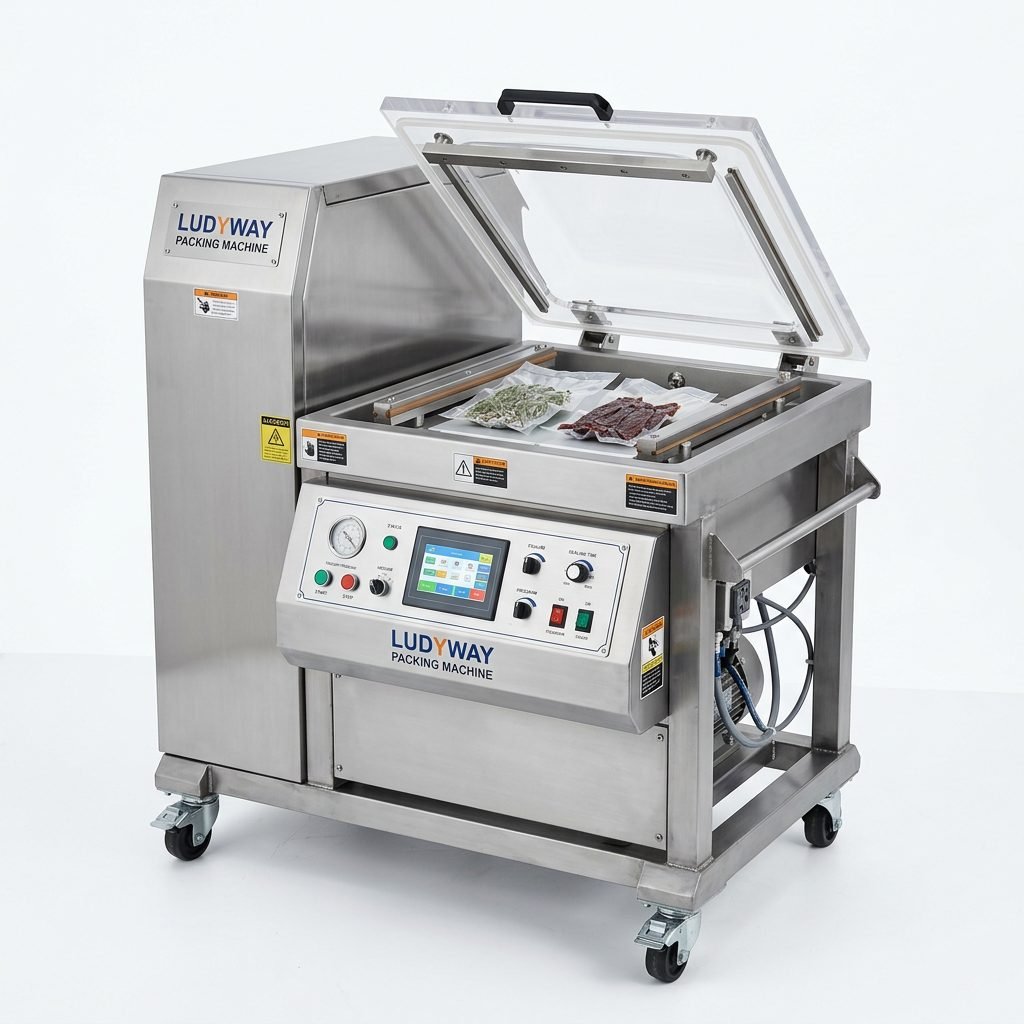
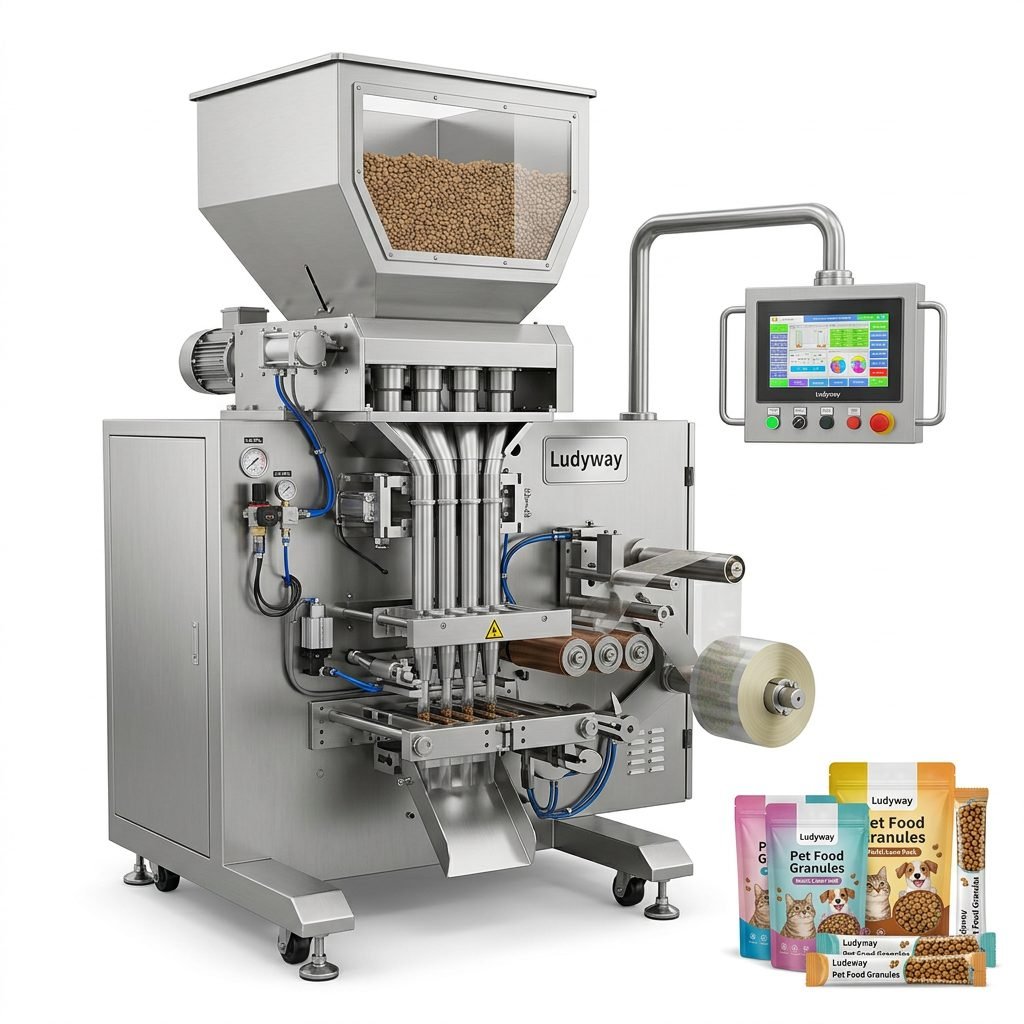
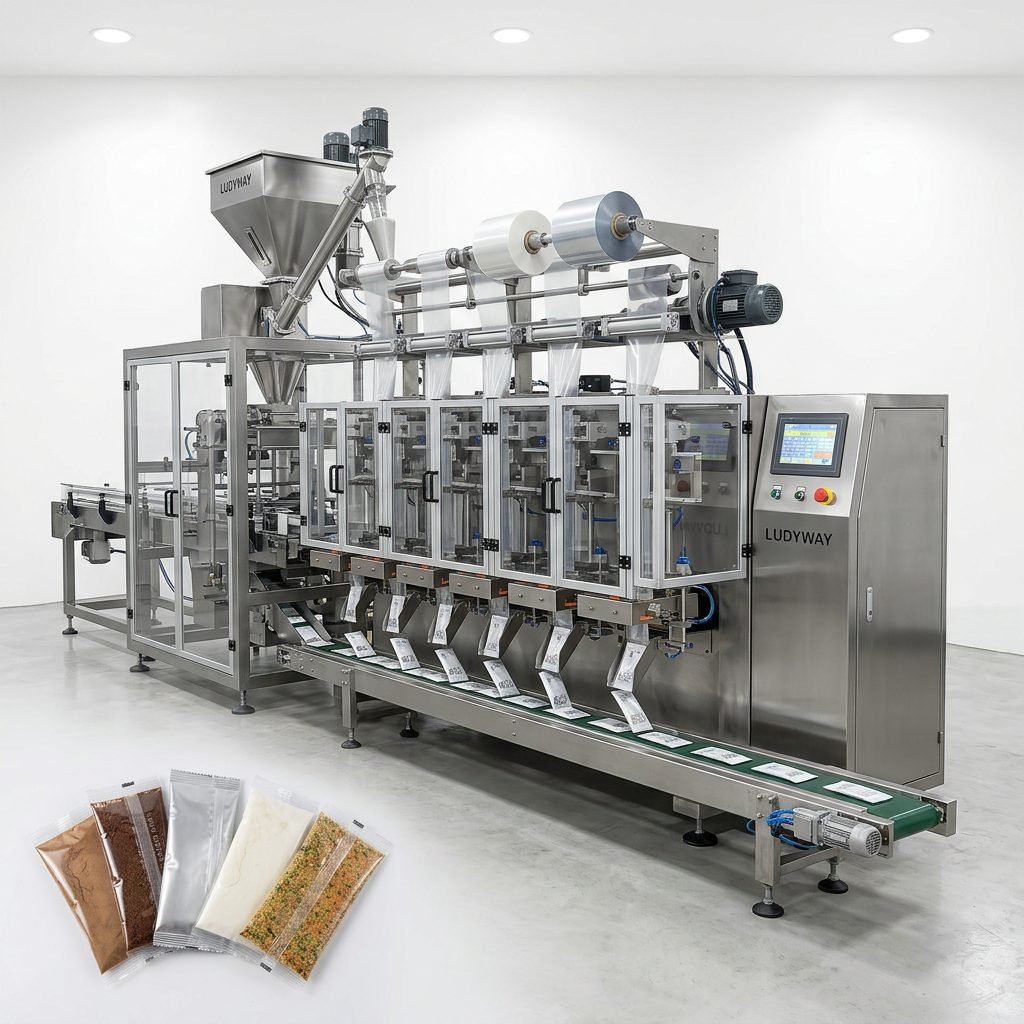
- Packaging format: Common formats include stick packs, sachets, blister packs, bottles, and pouches. Multi-lane stick pack machines are increasingly popular for single-dose pharmaceutical applications.
- Packaging material: Verify that the machine is compatible with your chosen materials — foil laminates, paper-based structures, or pharmaceutical-grade films.
According to ISO 11607 standards for terminally sterilized medical devices, packaging must maintain sterility and product protection throughout the supply chain. Your equipment selection should align with these requirements from the start.
2. Evaluate Filling Accuracy and Dosing Technology
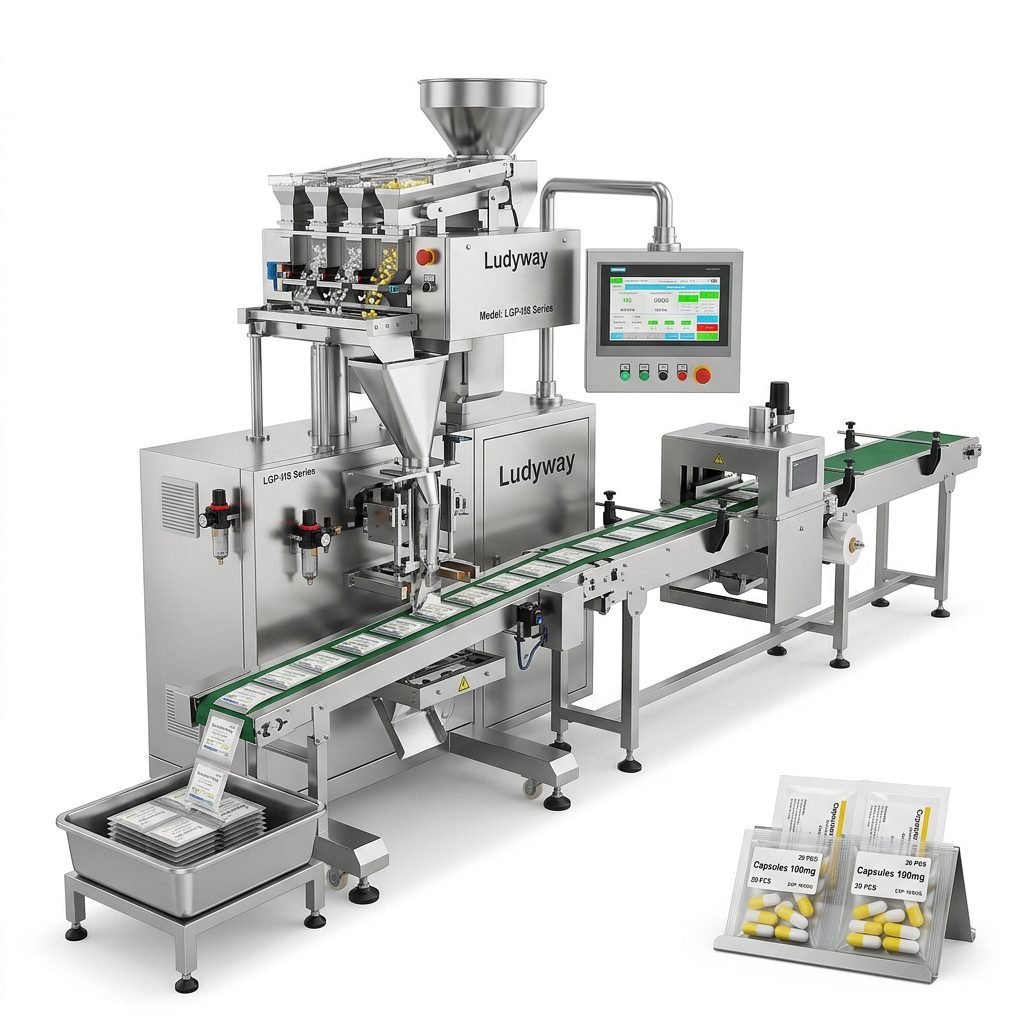
In pharmaceutical packaging, dosing precision is non-negotiable. Regulatory bodies such as the FDA enforce strict tolerances on fill weights and content uniformity. The right pill packaging machine should incorporate advanced dosing systems tailored to your product.
| Dosing Technology | Best Suited For | Accuracy Level |
|---|---|---|
| Auger Filler | Powders, fine granules | ±0.5% to ±1% |
| Volumetric Cup Filler | Free-flowing granules, pellets | ±1% to ±2% |
| Electronic Counting | Tablets, capsules, softgels | >99.9% count accuracy |
| Multi-Head Weigher | High-speed granule packaging | ±0.1% to ±0.5% |
Speed and Accuracy Balance
While higher speeds improve throughput, ensure the machine maintains dosing accuracy at your target production rate. A machine capable of 400 stick packs per minute is only valuable if every pack meets pharmaceutical weight specifications.
3. Compliance with Pharmaceutical Regulations and Standards
Pharmaceutical packaging equipment must comply with Good Manufacturing Practice (GMP) requirements and applicable regulatory frameworks. Key considerations include:
- Material traceability: All product-contact parts should be certified and documented.
- Clean-in-place (CIP) capability: Equipment should facilitate thorough cleaning and sanitization.
- Validation documentation: IQ/OQ/PQ protocols should be available from the manufacturer.
- Data integrity: Modern machines should support electronic batch recording and audit trails.
Refer to PMMI packaging machinery standards and resources for the latest industry benchmarks on pharmaceutical packaging compliance.
4. Production Speed and Scalability
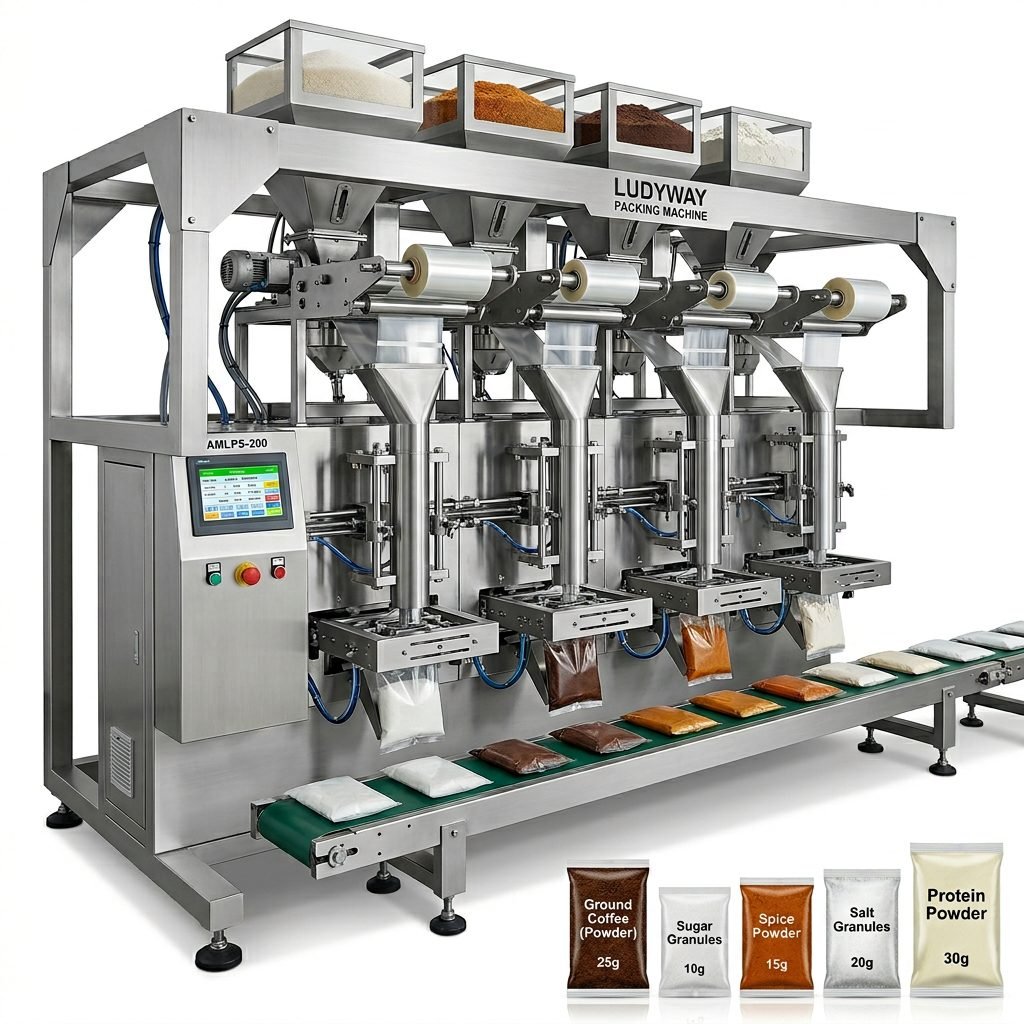
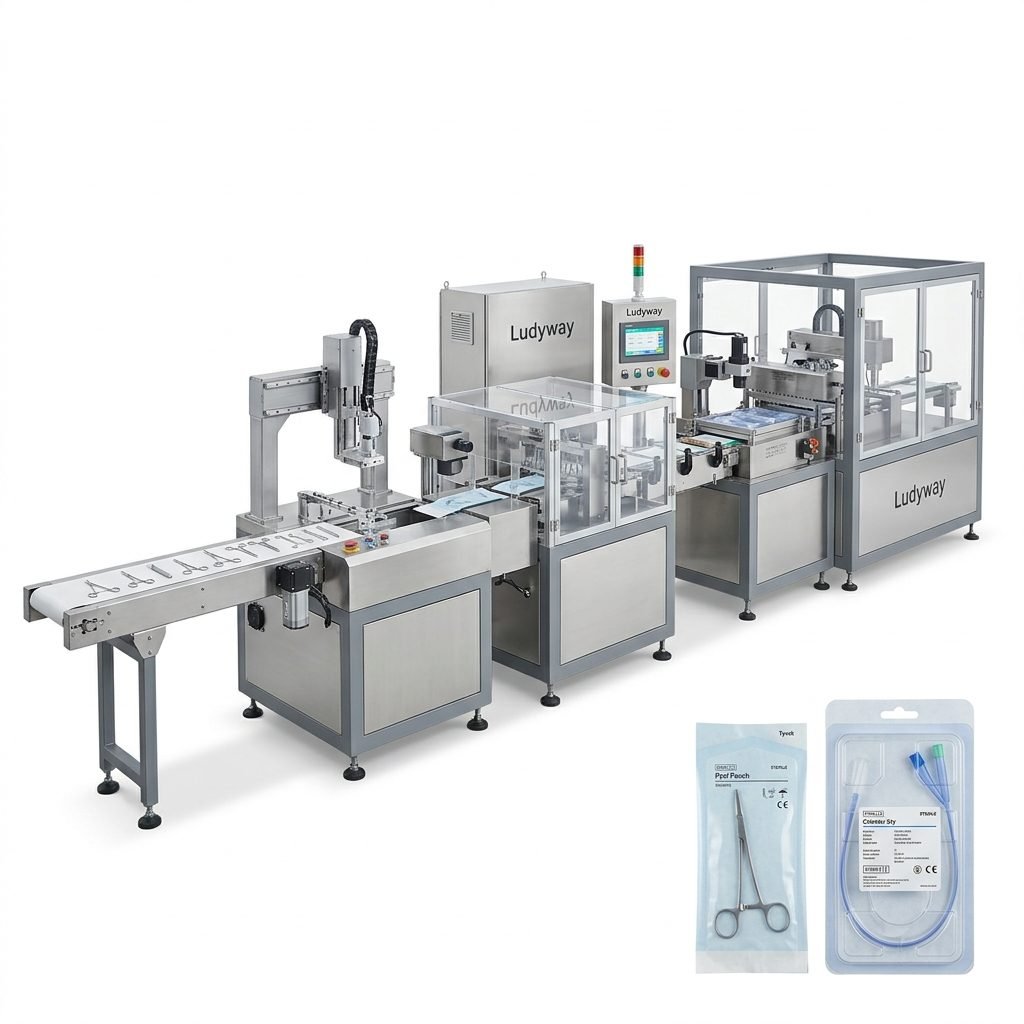
Your current and projected production volumes should guide equipment selection. Multi-lane stick pack machines offer scalable output — from 4-lane configurations for moderate production to 12-lane or more for high-volume pharmaceutical manufacturing.
| Production Scale | Recommended Configuration | Typical Output Range |
|---|---|---|
| Small Batch / R&D | Single-lane or 2-lane | 30-80 packs/min |
| Medium Volume | 4-lane to 6-lane | 120-300 packs/min |
| High Volume | 8-lane to 12-lane | 400-800+ packs/min |
Select a machine that can grow with your business. Modular designs allow you to add lanes or upgrade components without replacing the entire system.
5. Machine Build Quality and Component Reliability
Pharmaceutical environments demand equipment built for longevity and consistent performance. Evaluate the following build quality indicators:
- Frame construction: Stainless steel SUS304 or SUS316L for corrosion resistance and cleanability.
- Control systems: PLC-based controls with HMI touchscreen interfaces from established automation brands.
- Pneumatic and electrical components: Sourcing from globally recognized suppliers ensures spare parts availability and reliable operation.
- Sealing technology: Precision temperature control for consistent hermetic seals on pharmaceutical packaging.
Manufacturers with in-house engineering and manufacturing capabilities typically offer better quality control and customization options. Ludyway Machinery, for instance, combines in-house manufacturing with engineering expertise across its 20,000-square-meter facility, serving customers in more than 100 countries with configurations tailored to pharmaceutical applications.
6. Integration with Existing Production Lines
A pharmacy pill packaging machine rarely operates in isolation. Consider how the equipment will integrate with upstream and downstream processes:
- Feeding systems: Vibratory feeders, bucket elevators, or vacuum conveyors for product infeed.
- Inspection systems: Checkweighers, metal detectors, and vision inspection for quality assurance.
- Coding and marking: Thermal transfer printers, inkjet coders, or laser markers for batch coding and serialization.
- Secondary packaging: Cartoning, case packing, and palletizing systems for end-of-line automation.
7. Total Cost of Ownership (TCO)
Beyond the initial purchase price, evaluate the total cost of ownership over the machine’s expected lifespan. Key cost factors include:
- Spare parts availability and cost: Confirm lead times and pricing for wear components like sealing jaws, cutting blades, and belts.
- Energy consumption: Energy-efficient motors and heating systems reduce long-term operational costs.
- Maintenance requirements: Machines with accessible design and clear documentation reduce downtime and technician costs.
- Technical support: Remote assistance capabilities and local service availability minimize production disruptions.
Warranty and After-Sales Support
A comprehensive warranty and responsive after-sales service are critical. Look for manufacturers that offer installation, commissioning, operator training, and ongoing technical support throughout the equipment lifecycle. Remote troubleshooting capabilities have become increasingly important for international pharmaceutical operations.
8. Customization and Flexibility
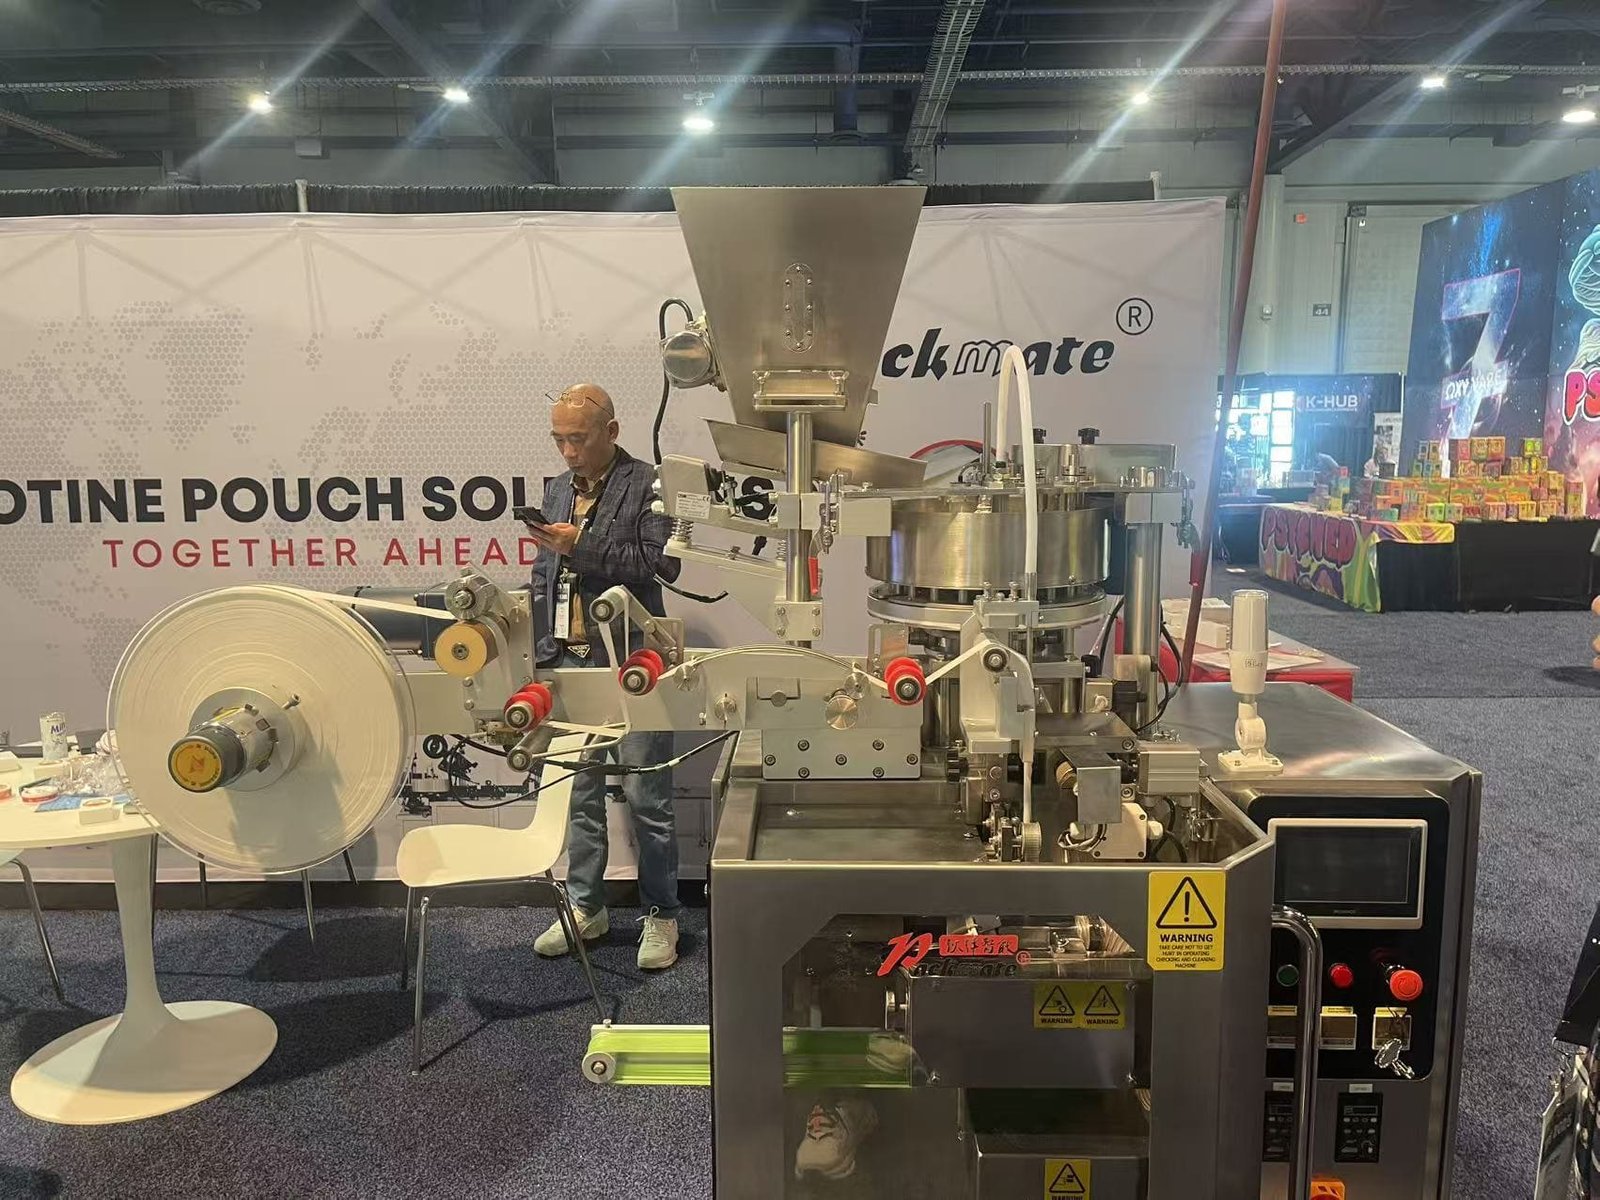
Pharmaceutical manufacturers often require customized packaging solutions to accommodate unique product characteristics, packaging formats, or factory layouts. Consider a manufacturer that offers engineering customization rather than off-the-shelf machines only.
Flexible machines capable of handling multiple packaging formats — such as switching between sachet, stick pack, and pouch formats — provide greater operational versatility. According to Flexible Packaging Association industry data, the demand for flexible pharmaceutical packaging continues to grow, making format flexibility a valuable asset.
9. Documentation and Validation Support
Pharmaceutical packaging operations require extensive documentation for regulatory compliance. Confirm that your equipment supplier can provide:
- Design Qualification (DQ) documentation
- Installation Qualification (IQ) protocols
- Operational Qualification (OQ) protocols
- Performance Qualification (PQ) support
- Material certificates for product-contact components
- Equipment manuals and maintenance schedules
10. Making the Final Decision: Key Takeaways
Selecting the right pharmacy pill packaging machine requires balancing multiple factors — product compatibility, dosing accuracy, regulatory compliance, production speed, integration capability, and total cost of ownership. To summarize the decision-making process:
- Start with your product: Define its physical characteristics and packaging requirements first.
- Map your regulatory path: Ensure the equipment can be validated for your target markets.
- Think long-term: Choose scalable equipment that supports future growth and new product introductions.
- Partner with experienced manufacturers: Work with suppliers who understand pharmaceutical packaging requirements and can provide ongoing technical support.
For more industry insights, visit PMMI State of the Industry reports and ISO packaging standards for the latest regulatory and technology developments in pharmaceutical packaging.