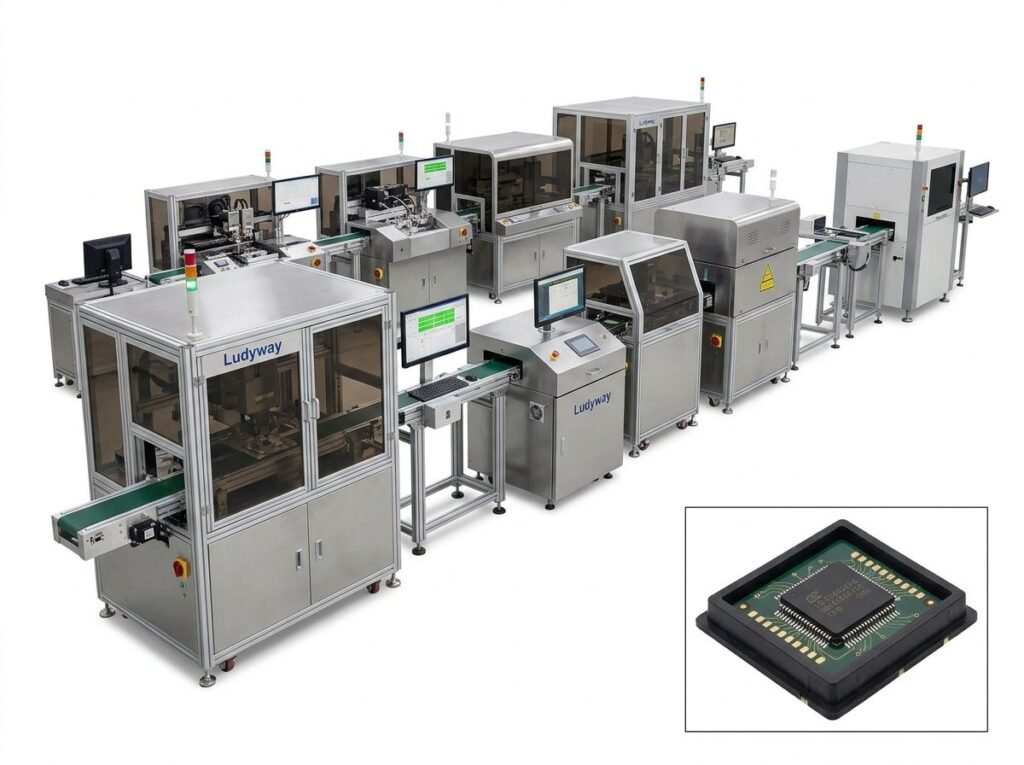
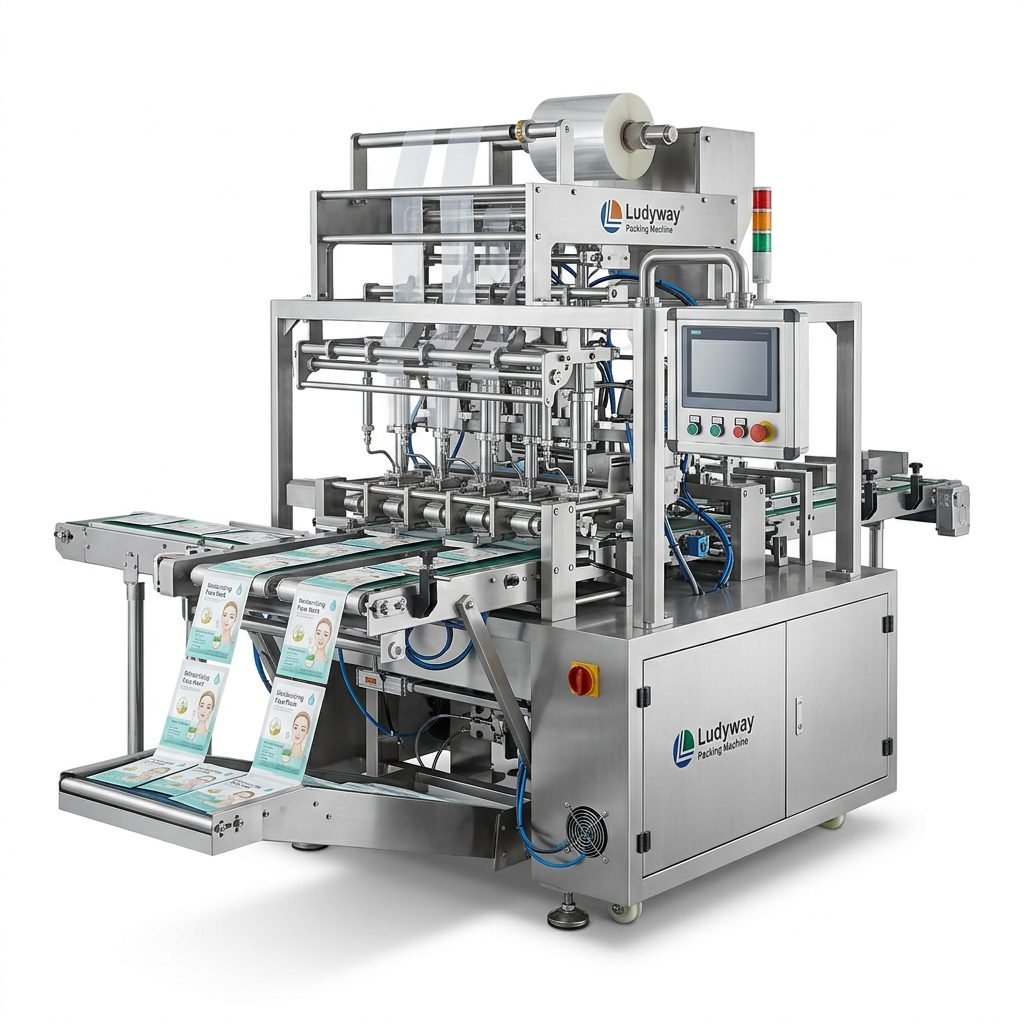
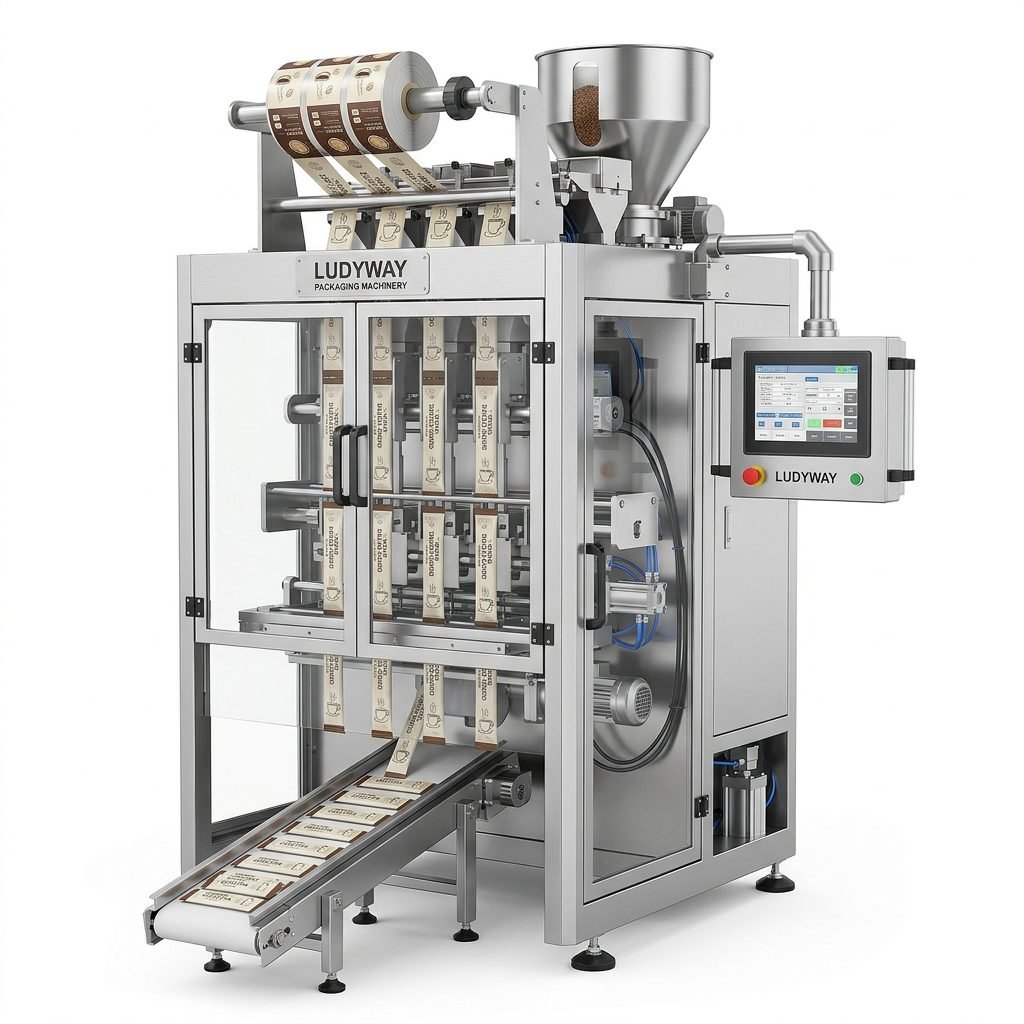
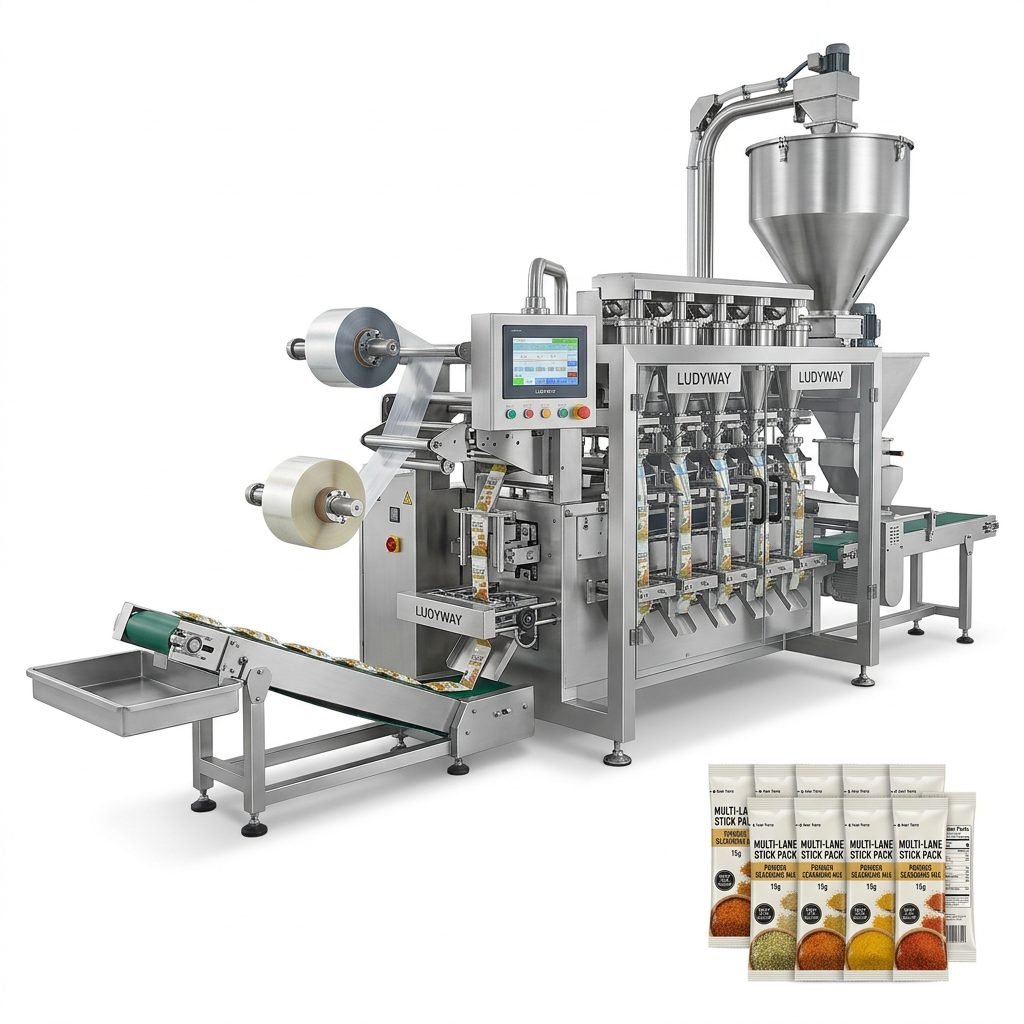
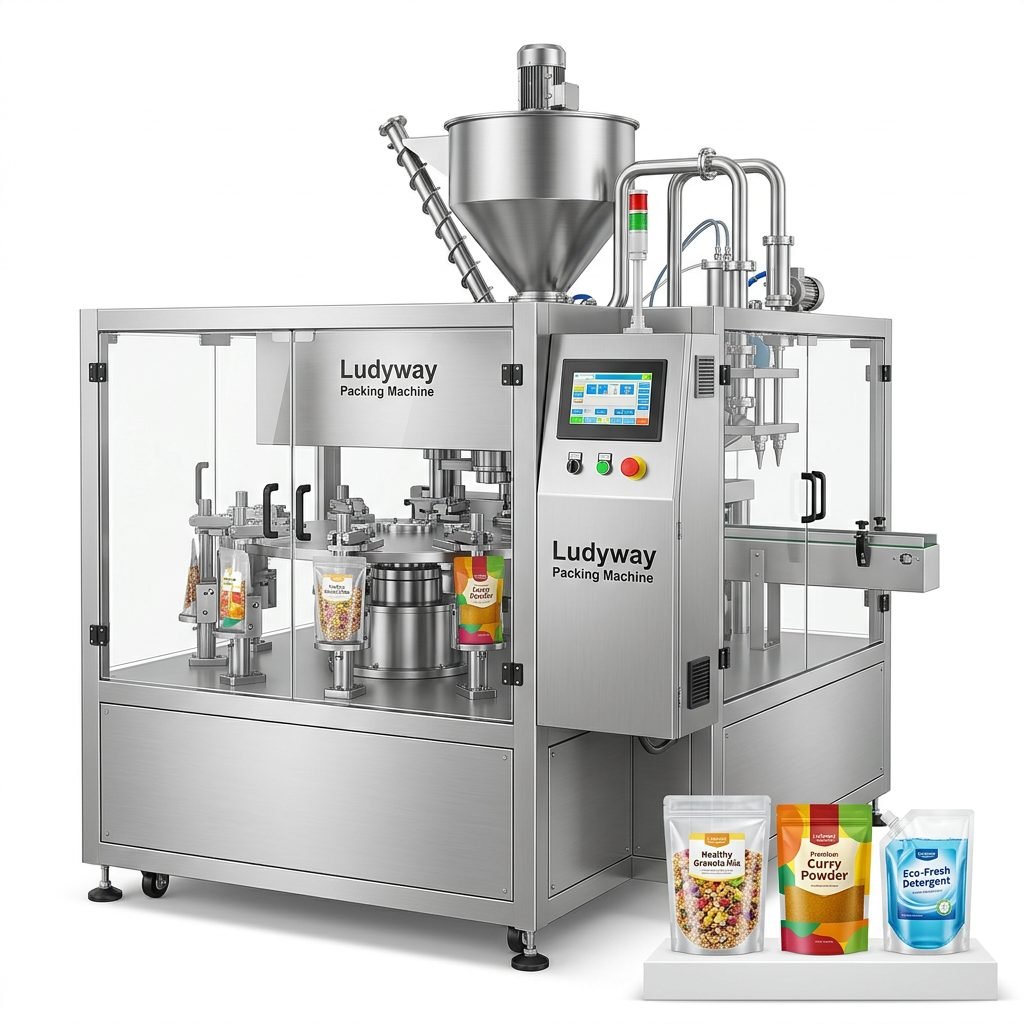
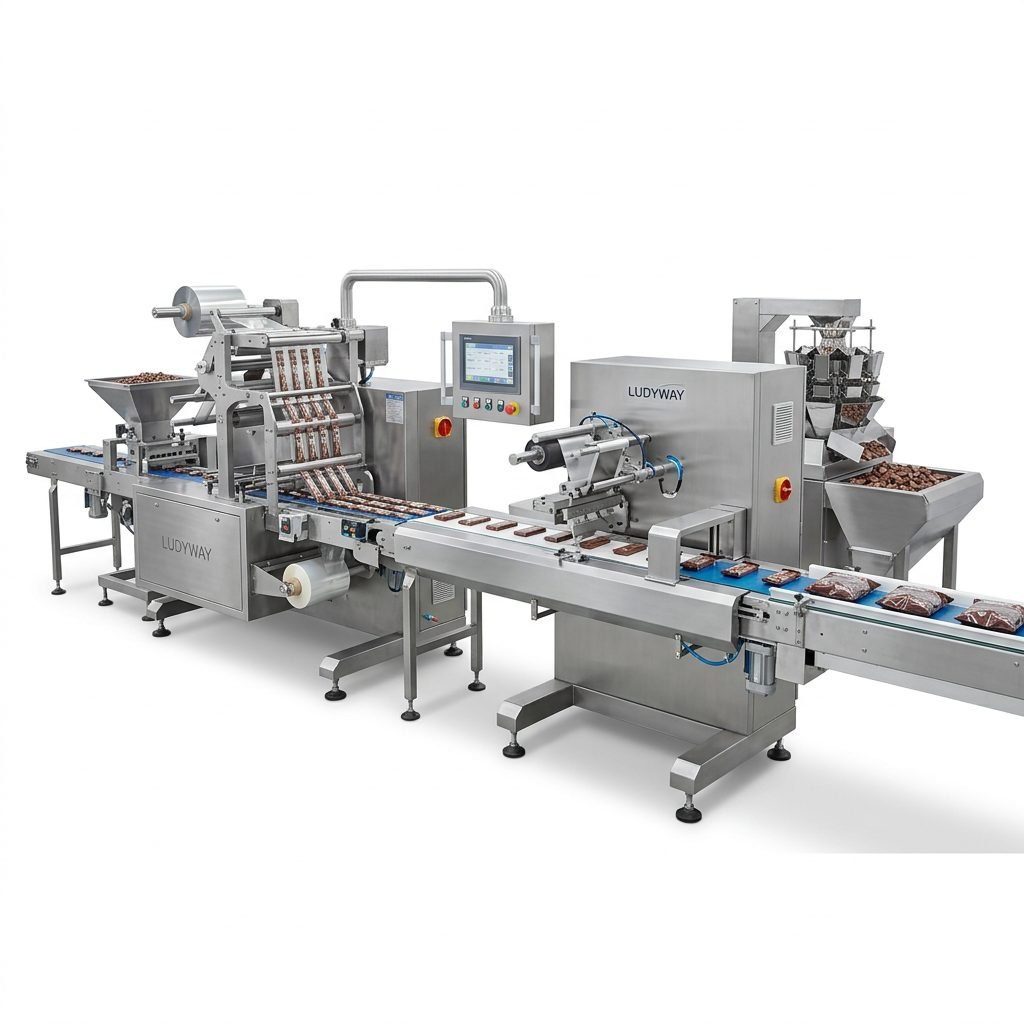
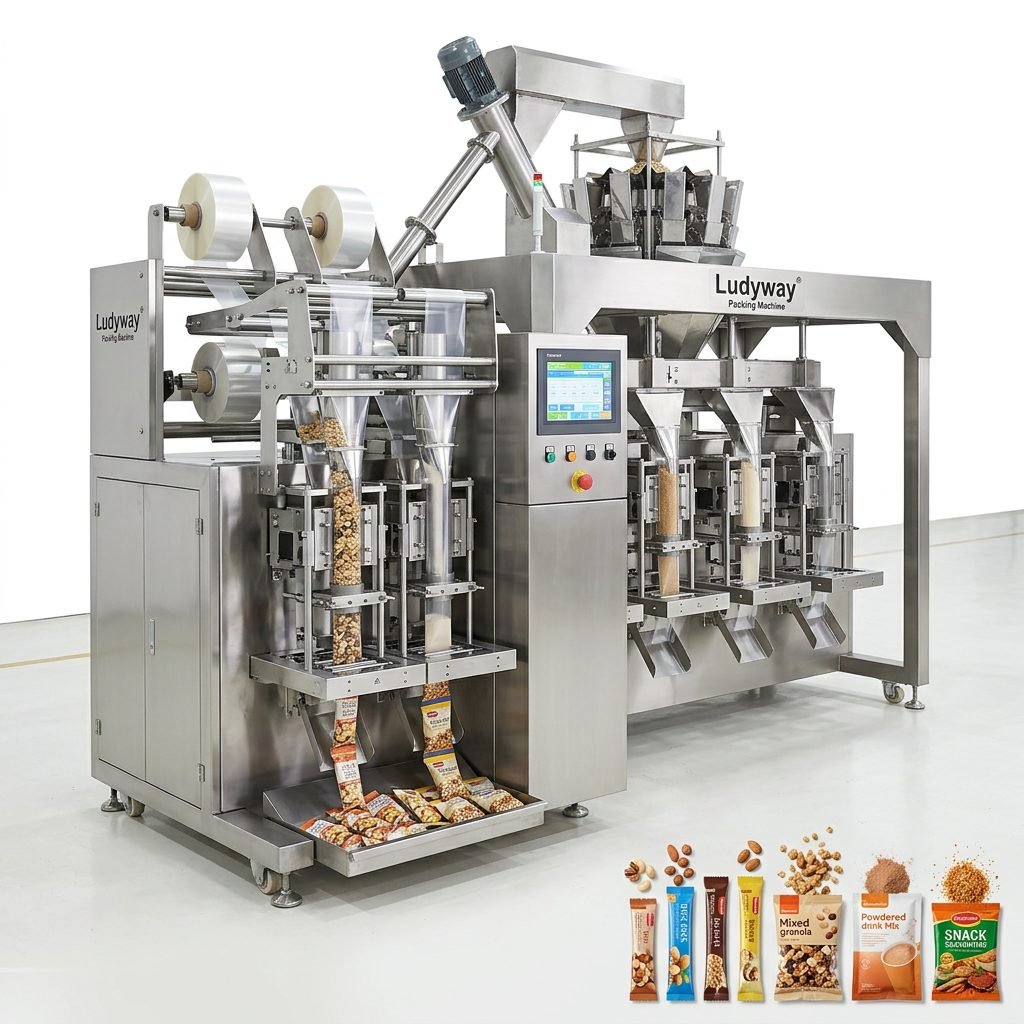
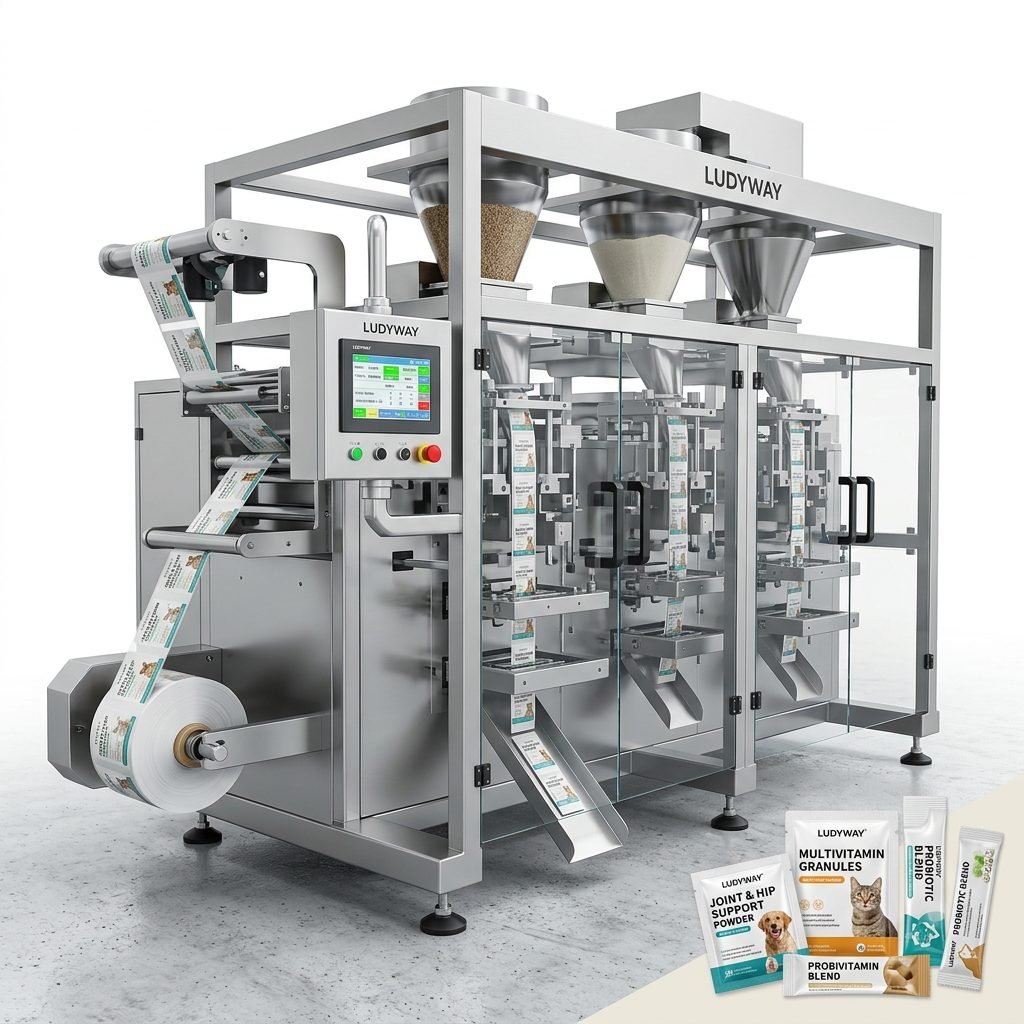
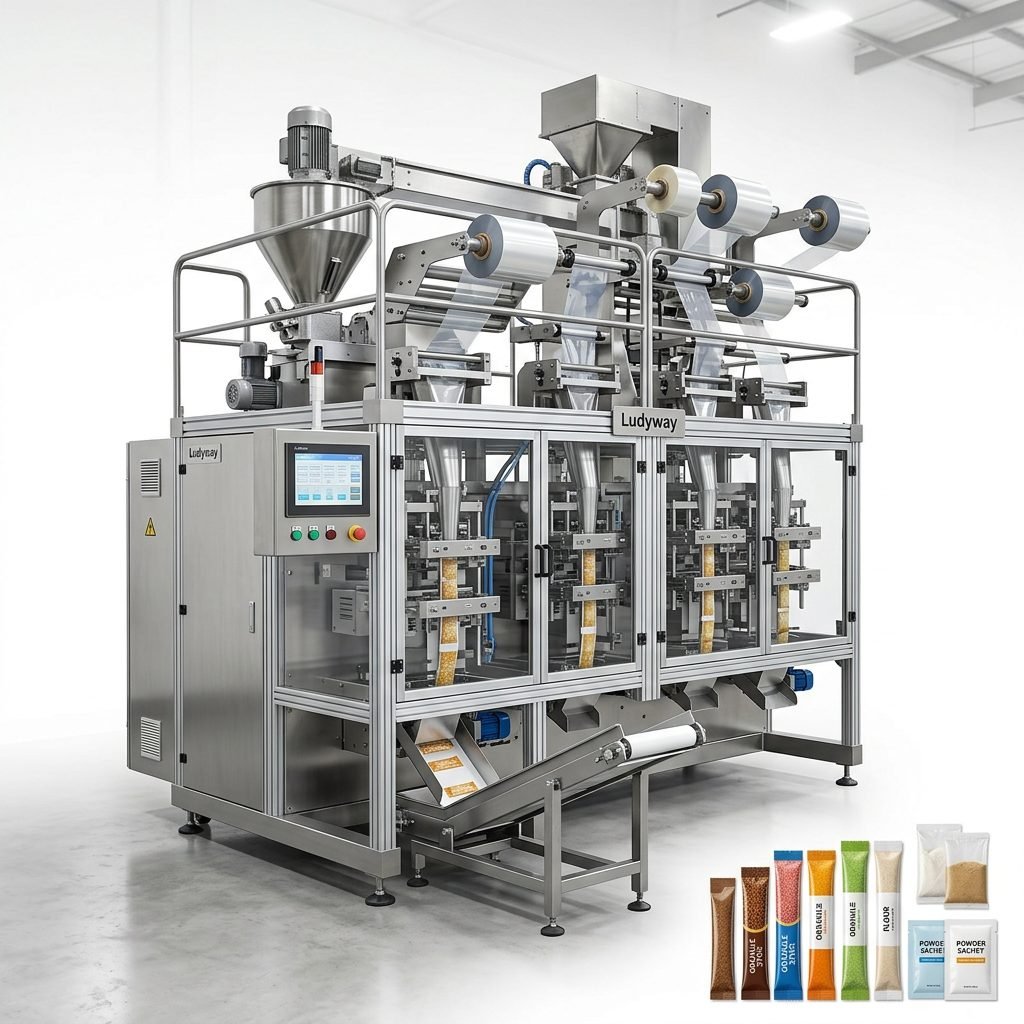
In today’s competitive food industry, selecting the right food tray packaging machine is critical to ensuring product freshness, extending shelf life, and maintaining operational efficiency. As global demand for packaged foods continues to rise, manufacturers need reliable, high-speed packaging solutions that can adapt to diverse production requirements. Among the many packaging equipment suppliers worldwide, one name stands out for its engineering excellence, comprehensive product range, and commitment to quality — Ludyway, a premier food tray packaging machine manufacturer in China.
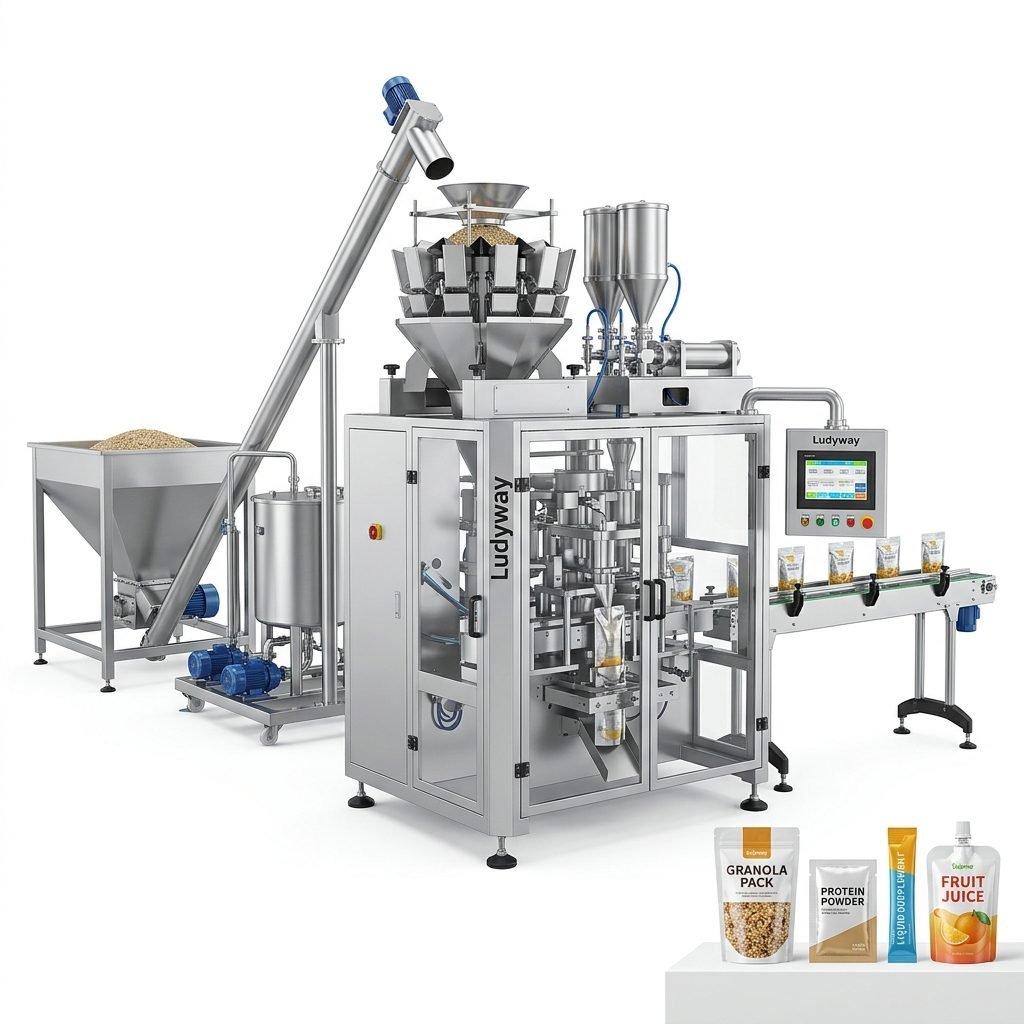
Unmatched Manufacturing Scale and Expertise
When evaluating a food tray packaging machine supplier, manufacturing capacity is a fundamental consideration. Operating from a modern 20,000㎡ production facility with over 200 manufacturing equipment units, the company possesses the infrastructure needed to deliver high-quality machinery at scale. With 30+ years of industry experience and a team of 130+ professional packaging experts, every machine is engineered with precision and built to perform reliably in demanding production environments. According to the PMMI State of the Industry Report, global packaging machinery demand continues to grow, making manufacturer stability and capacity more important than ever.
Comprehensive Product Portfolio for Diverse Applications
What distinguishes a top-tier food tray packaging machine manufacturer is the breadth of its product offerings. The ideal supplier provides solutions across multiple packaging formats:
- Tray sealing and lidding systems — for ready meals, fresh produce, and bakery products
- Modified atmosphere packaging (MAP) solutions — extending shelf life for perishable goods
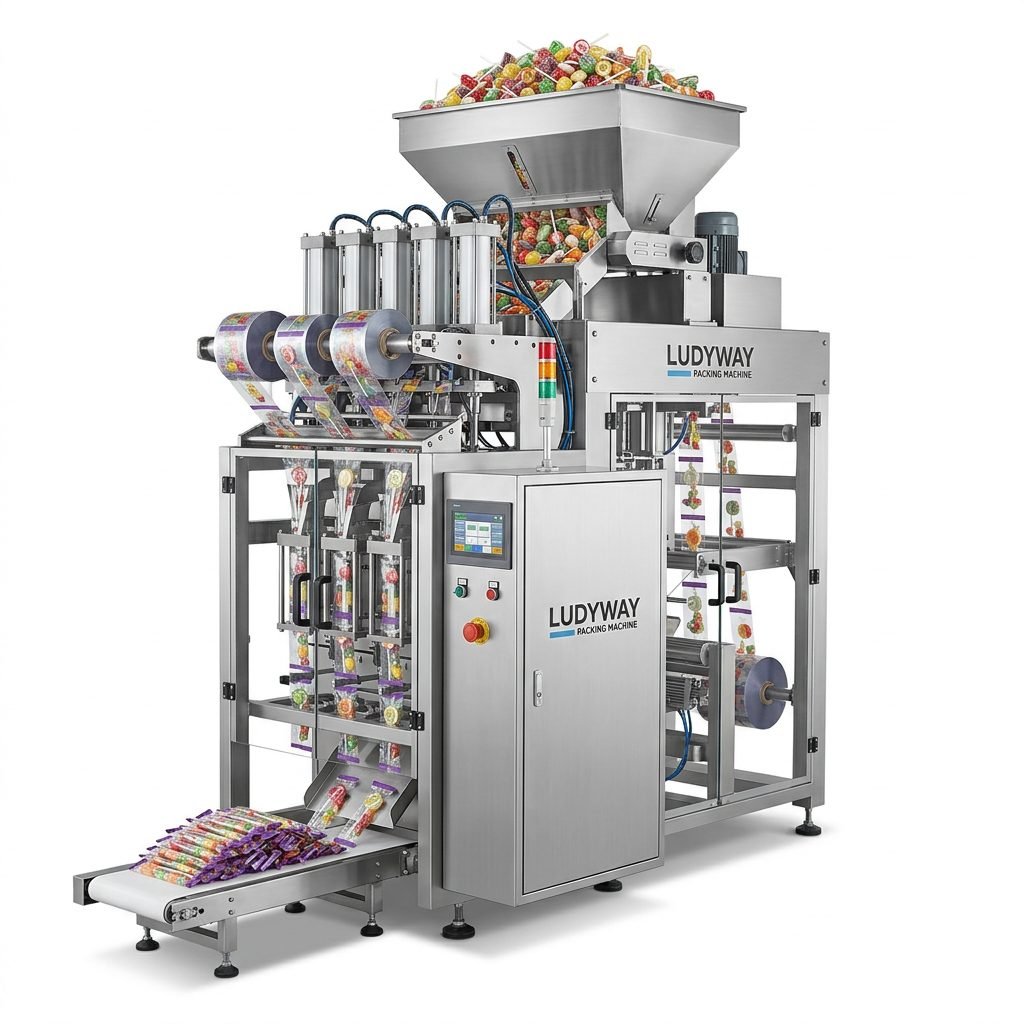
- Multi-lane stick pack and sachet machines — for powders, granules, and liquid condiments
- Fully automated turnkey packaging lines — integrating filling, sealing, labeling, and cartoning
- Custom OEM packaging solutions — tailored to unique product specifications and factory layouts
This versatility ensures that food manufacturers can find the right machine configuration for their specific tray packaging needs, whether for frozen foods, snack items, or fresh meal kits. The Flexible Packaging Association highlights how advanced packaging formats continue to reshape the food industry landscape.
Advanced Technology and Intelligent Automation
Modern food tray packaging machines must deliver more than just basic functionality. The best manufacturers incorporate intelligent features that boost productivity while minimizing waste:
- Servo-driven control systems for precise tray positioning and sealing accuracy
- Automated tray denesting and loading to reduce manual labor requirements
- Multi-head weighing and filling integration for consistent portion control
- Inline quality inspection systems including checkweighers and metal detection
- User-friendly HMI touchscreen interfaces with recipe management capabilities
These technological advantages translate directly to improved production efficiency and reduced downtime — critical factors for food processors operating on tight margins.
Global Quality Standards and Compliance
Food safety regulations demand that packaging equipment meets stringent hygiene and quality standards. A reliable food tray packaging machine manufacturer ensures compliance with international norms including ISO packaging standards and FDA requirements for food contact materials. Key quality attributes include:
- Stainless steel construction on all food-contact surfaces for easy sanitation
- IP65/IP66 rated components suitable for washdown environments
- CE certification ensuring conformity with European safety and quality directives
- Rigorous factory acceptance testing (FAT) before equipment shipment
- Comprehensive after-sales support and technical service worldwide
Key Specifications Comparison
| Feature | Standard Configuration | Advanced Configuration |
|---|---|---|
| Tray Material | PP, PET, Aluminum | Biodegradable, CPET, Multi-layer |
| Sealing Method | Heat seal with film lidding | MAP gas flushing + heat seal |
| Production Speed | 30-60 trays per minute | 80-120+ trays per minute |
| Automation Level | Semi-automatic operation | Fully automatic inline system |
| Inspection Systems | Basic tray presence detection | Vision inspection + checkweighing |
| Changeover | Manual adjustment (15-30 min) | Servo-driven automatic (under 5 min) |
Cost-Effectiveness and ROI Optimization
Investing in a food tray packaging machine represents a significant capital decision. The most competitive Chinese manufacturers offer compelling value through:
- Lower initial equipment cost compared to European counterparts without sacrificing quality
- Reduced spare parts expenses due to standardized component sourcing
- Energy-efficient designs that lower ongoing operational costs
- High machine uptime backed by robust engineering and reliable support
- Faster delivery lead times from well-stocked production facilities
Global Reach with Localized Support
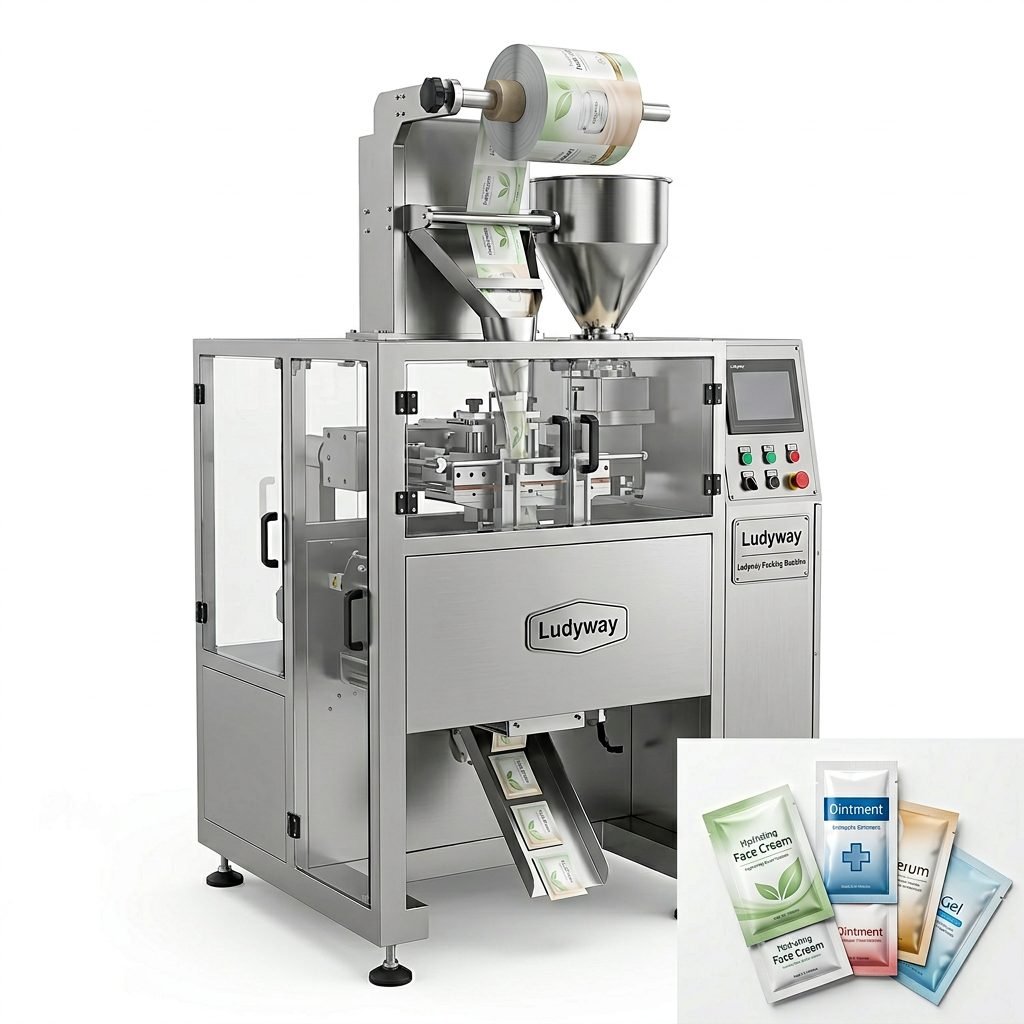
Serving customers in over 100 countries and regions, a truly global food tray packaging machine manufacturer must provide localized technical assistance. This includes pre-sales consultation, factory layout planning, installation and commissioning, operator training, and ongoing maintenance support. The PMMI packaging industry resources emphasize that supplier reliability and after-sales service are among the top criteria for equipment purchasing decisions.
Why Tray Packaging Matters for Modern Food Production
Food tray packaging continues to gain market share due to several advantages:
- Product visibility — clear lidding films allow consumers to inspect contents
- Extended shelf life — MAP technology preserves freshness without preservatives
- Portion control — pre-portioned trays reduce food waste at the consumer level
- Brand differentiation — custom tray shapes and printed lidding films enhance shelf appeal
- Retail convenience — stackable, microwaveable, and freezer-ready formats
Common Questions About Food Tray Packaging Machines
What types of food products are suitable for tray packaging?
Tray packaging is ideal for fresh meat, poultry, seafood, ready meals, fresh-cut fruits and vegetables, bakery items, cheese, snacks, and frozen foods. The versatility of tray sealing technology accommodates both solid and liquid-containing products.
How does Modified Atmosphere Packaging (MAP) work in tray sealers?
MAP technology replaces the air inside the tray with a precisely controlled gas mixture — typically nitrogen, carbon dioxide, and oxygen — before sealing. This significantly extends shelf life by slowing microbial growth and oxidation, which is essential for fresh protein products and prepared meals.
What should manufacturers consider when choosing a tray packaging machine?
Critical factors include production volume requirements, tray dimensions and materials, desired automation level, available factory floor space, cleaning and sanitation requirements, and budget constraints. Working with an experienced manufacturer ensures these factors are properly addressed during equipment selection.
Can tray packaging machines handle eco-friendly materials?
Yes, modern food tray packaging equipment is increasingly compatible with sustainable materials including recyclable mono-material trays, biodegradable films, and fiber-based alternatives. Equipment can be configured to accommodate the specific sealing parameters required by these innovative materials.
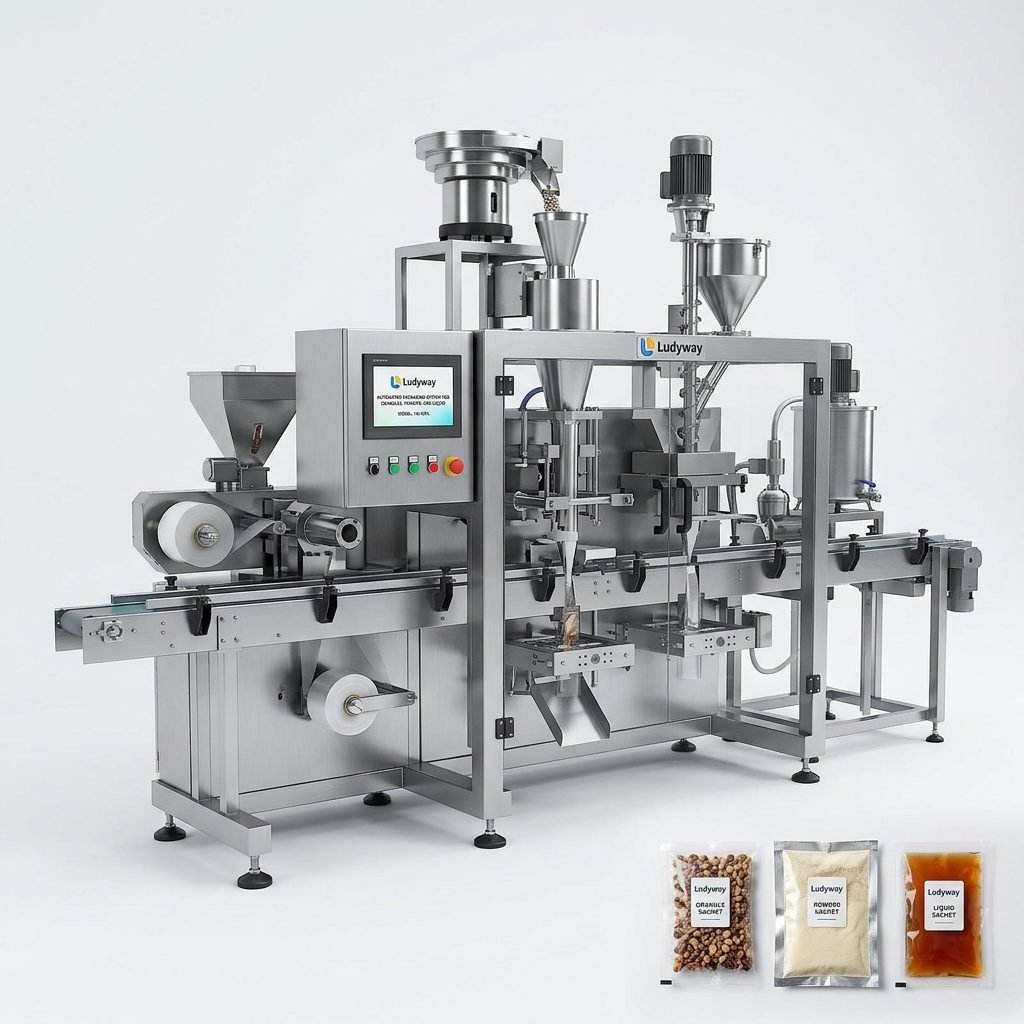
The Strategic Advantage of Choosing a Specialized Manufacturer
Partnering with a dedicated food tray packaging machine manufacturer offers distinct benefits over general equipment suppliers. Specialized manufacturers bring deep domain knowledge, proven machine designs refined through years of field experience, and a focused commitment to innovation in tray packaging technology. With export revenues projected to exceed RMB 500 million (approximately US$69 million) by 2025, the leading Chinese manufacturers demonstrate both financial stability and sustained market trust. As noted in recent industry analysis, the growth trajectory of top packaging machinery exporters reflects the increasing global recognition of Chinese engineering capabilities.
In conclusion, selecting the right food tray packaging machine partner requires careful evaluation of manufacturing capability, technological sophistication, quality standards, global service support, and overall value proposition. Manufacturers that combine decades of experience with modern production infrastructure and a customer-focused approach represent the optimal choice for food companies seeking to enhance their packaging operations and compete effectively in the global marketplace.