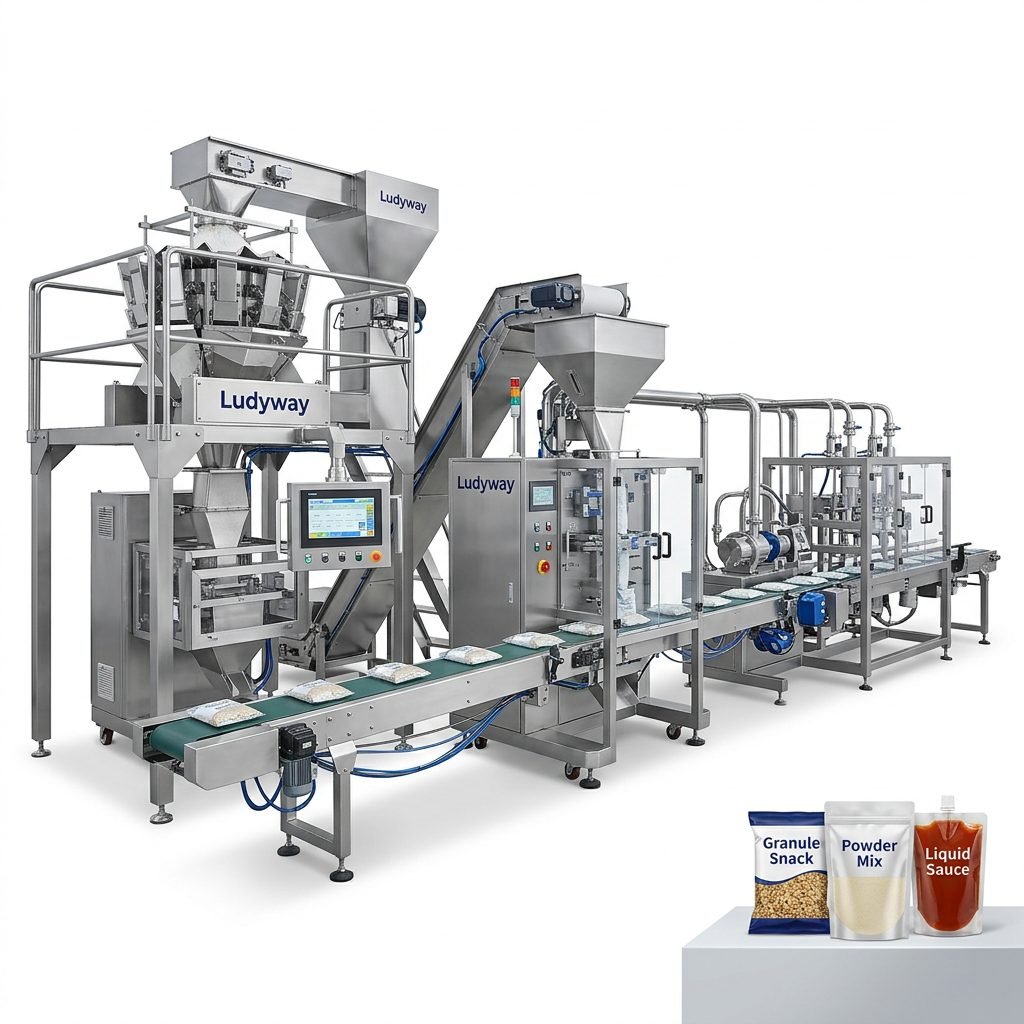
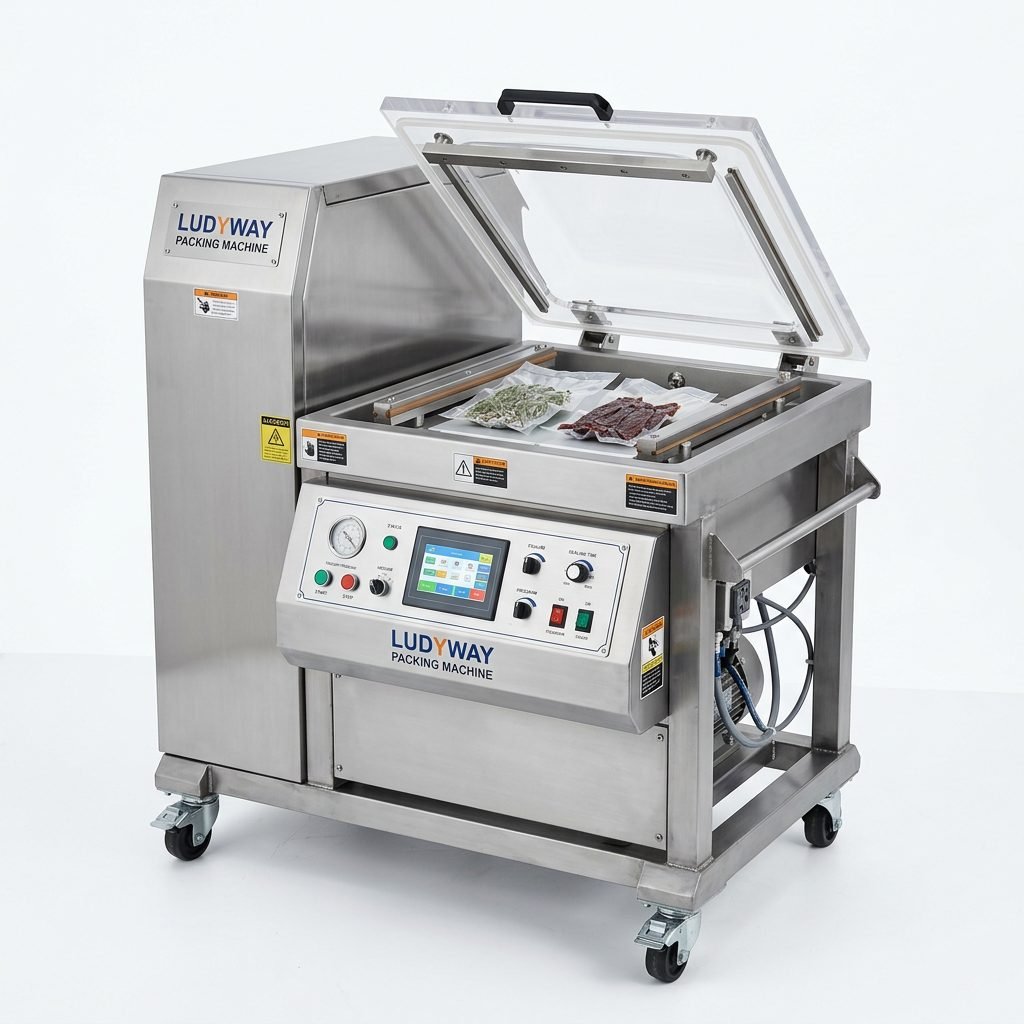
Investing in a water purification and packaging machine is a significant decision for manufacturers across industries, including food and beverage, pharmaceuticals, cosmetics, and chemical processing. The right equipment ensures product safety, extends shelf life, and optimizes production efficiency. This comprehensive buyer’s guide covers the essential factors to evaluate before making a purchase.
Understanding Your Product and Production Goals
Before comparing machine specifications, you must clearly define your requirements. The type of water purification technology and packaging format you need depends on several variables: the source water quality, desired purity level, production volume, and final packaging presentation. A common mistake is selecting a machine based solely on price without aligning it with operational goals.
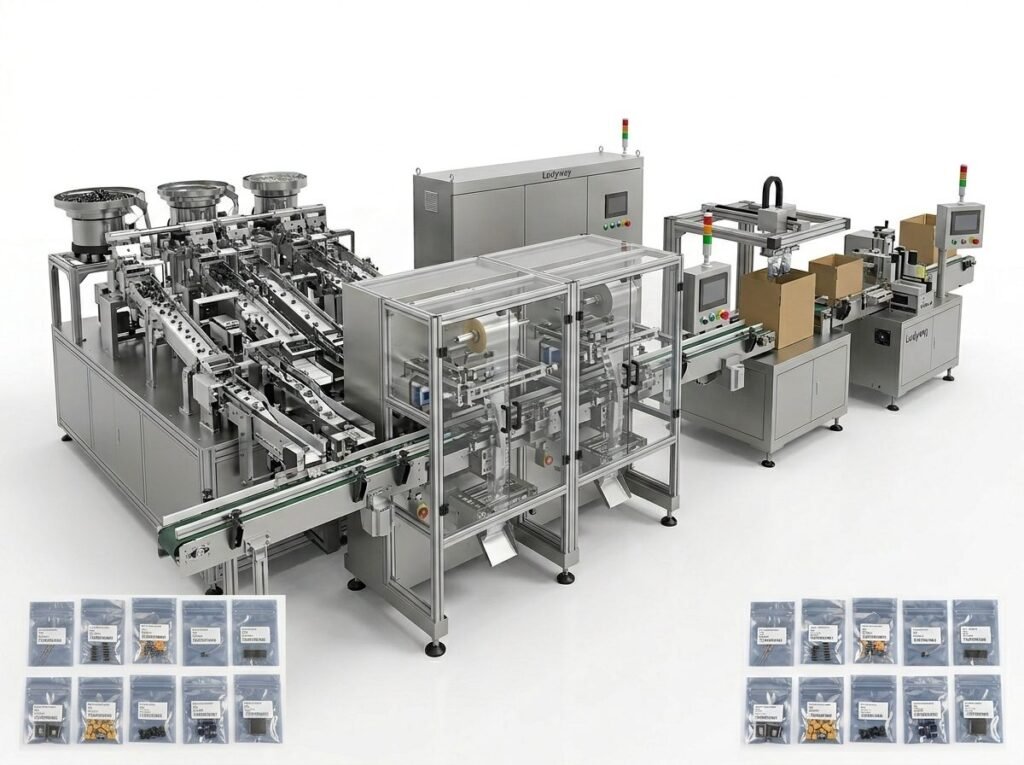
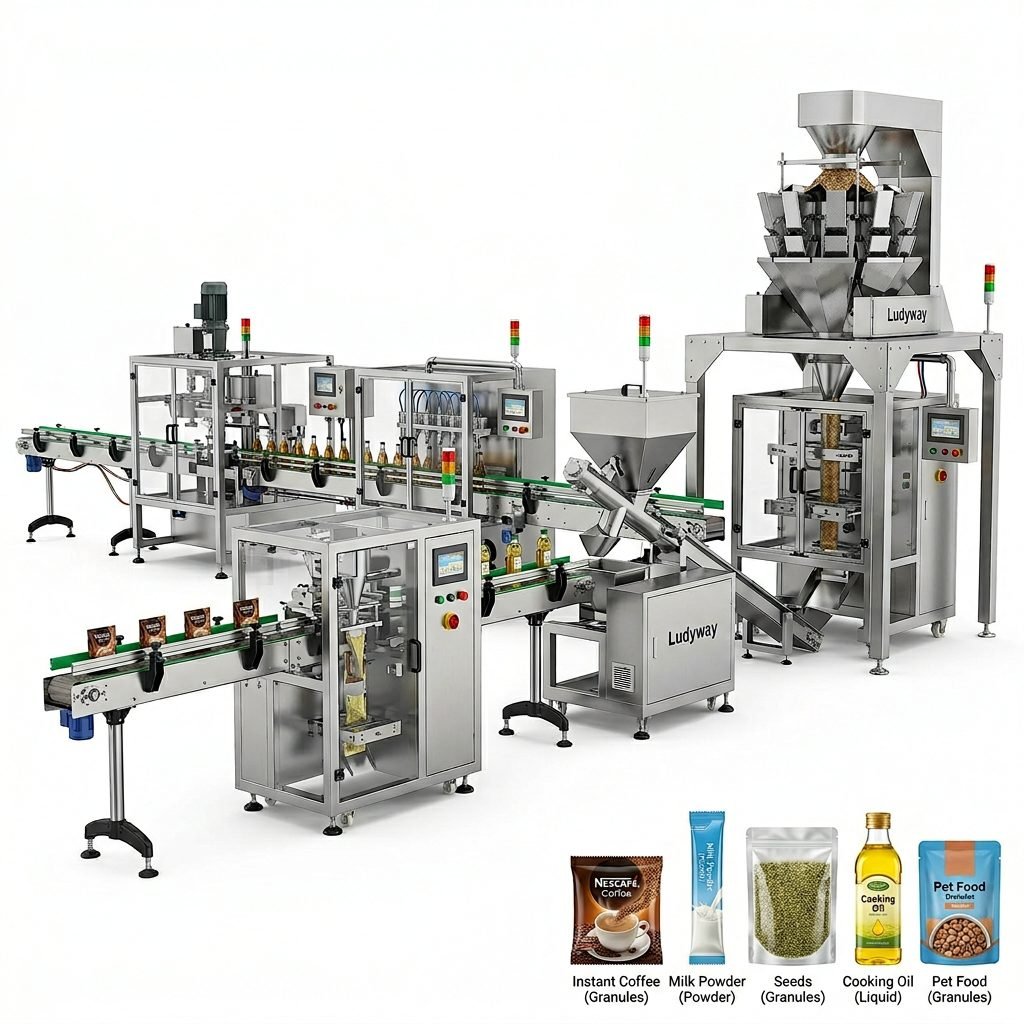
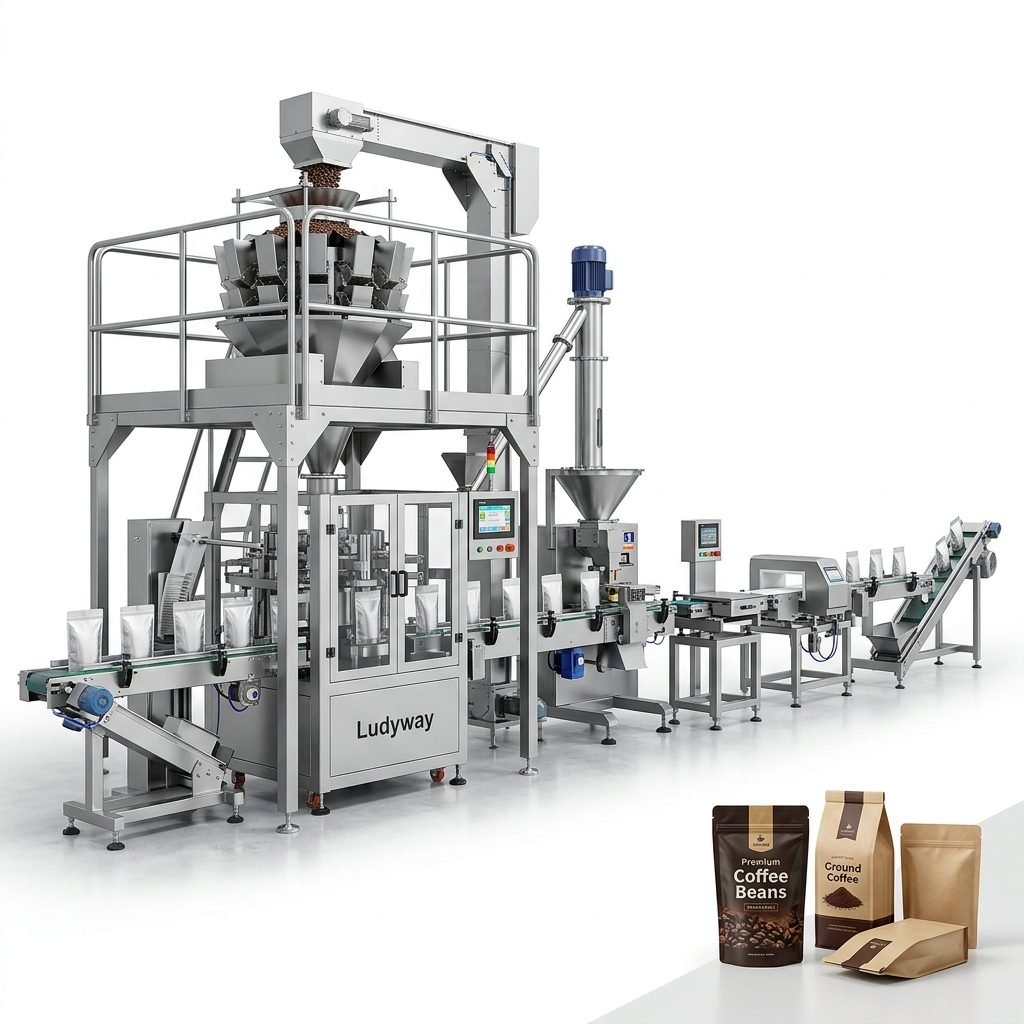
Consider whether you need a complete turnkey packaging line or a standalone unit. For high-volume operations, integrated systems that combine water treatment, filling, capping, and labeling into one automated workflow can significantly reduce labor costs and human error.
Key Factors in Selecting Water Purification Technology
Water purification is not a one-size-fits-all process. The appropriate technology depends on your input water analysis and the purity standards your final product must meet. Common technologies include reverse osmosis (RO), ultraviolet (UV) sterilization, ultrafiltration (UF), and electrodeionization (EDI). Many packaging industry standards now require rigorous purification documentation for regulated products.
| Purification Technology | Best For | Key Consideration |
|---|---|---|
| Reverse Osmosis (RO) | High-purity pharmaceutical water | Requires pre-treatment for optimal membrane life |
| UV Sterilization | Microbial control for beverage and food | No chemical addition, but water clarity matters |
| Ultrafiltration (UF) | Particle and colloid removal | Lower energy consumption than RO |
| EDI (Electrodeionization) | Ultra-pure water without chemicals | Often paired with RO for final polishing |
Packaging Machine Formats and Configurations
Once purified, water must be packaged efficiently. The packaging format you choose—sachets, stick packs, pouches, bottles, or bulk containers—will determine the type of filling and sealing equipment required. Flexible packaging materials have become increasingly popular for single-serve water and liquid concentrate applications due to reduced material usage and extended shelf life.
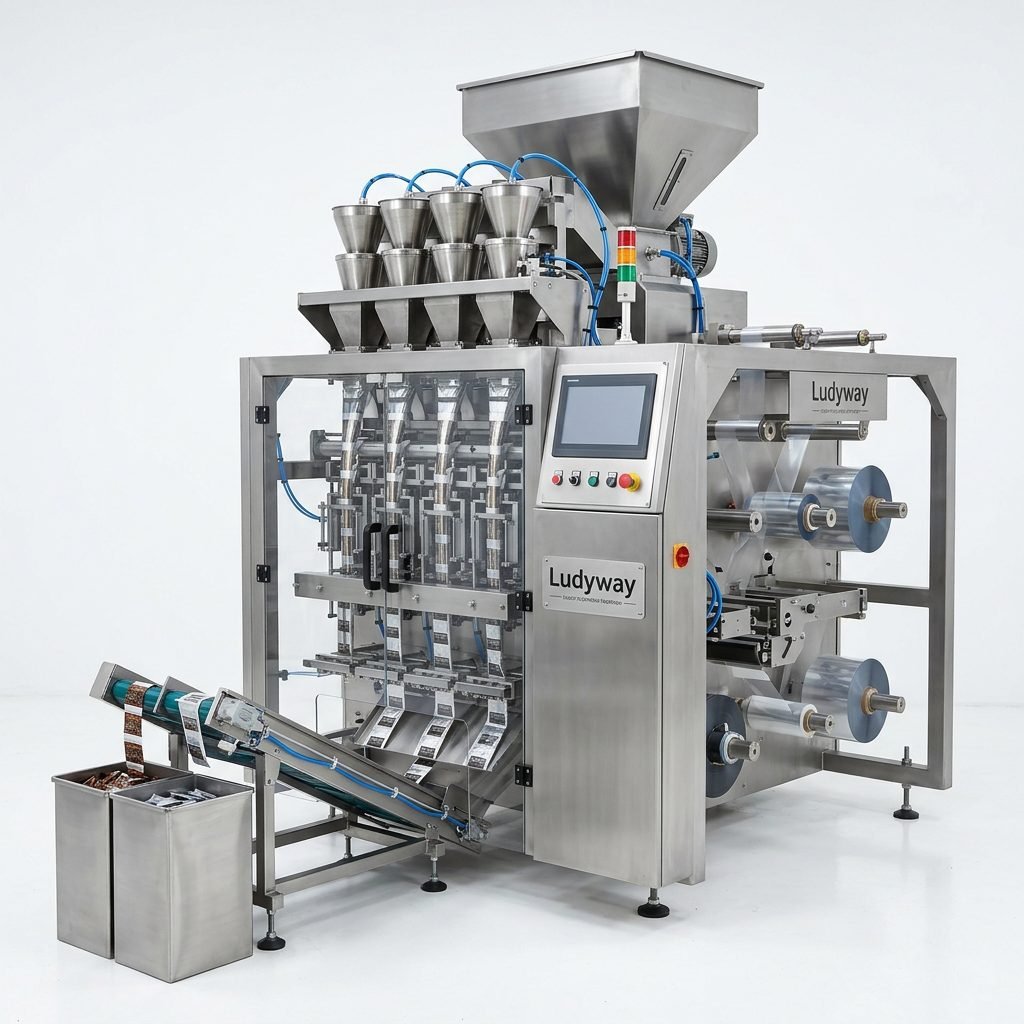
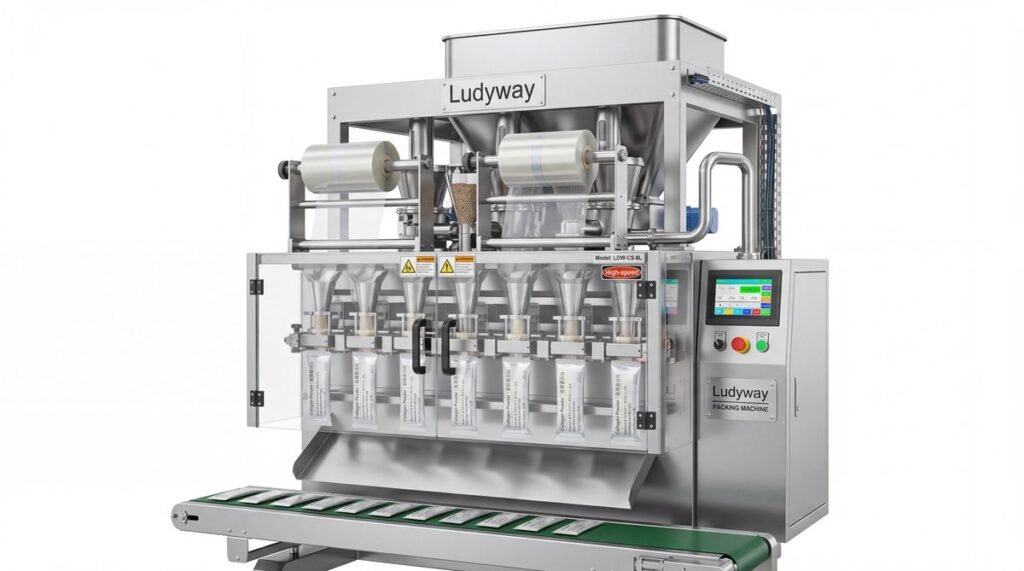
- Sachet and stick pack machines – Ideal for single-use purified water or liquid concentrates, offering high-speed multi-lane options.
- Bottle filling and capping lines – Suitable for retail water products, requiring precise volumetric or gravity filling systems.
- Pouch packaging systems – Increasingly used for larger volumes, with spout and zipper closure options.
- Bag-in-box and bulk filling – Designed for commercial and industrial purified water distribution.

Matching Machine Capacity to Production Demand
Production speed is a critical specification. Machines are rated by pouches per minute, bottles per hour, or liters per day. Underestimating capacity can create bottlenecks, while overestimating leads to unnecessary capital expenditure. Analyze your current and projected demand over the next three to five years.
For manufacturers entering water purification and packaging, a modular approach often works best. Start with a mid-range system that can be scaled with additional filling heads, lane expansions, or upgraded purification modules as demand grows.
Automation Level and Integration
Modern water packaging machines offer varying degrees of automation. Semi-automatic systems require operator intervention for some steps, while fully automatic lines handle everything from bottle feeding to palletizing. Consider your labor availability and consistency requirements. Integrated CIP (Clean-in-Place) systems are essential for maintaining hygiene in water processing equipment, particularly for FDA-regulated food and beverage applications.
Material Compatibility and Packaging Sustainability
The packaging material you select must be compatible with both the purified water and the sealing technology of your machine. Common materials include PET, HDPE, multi-layer laminates, and aluminum foil composites. With increasing regulatory focus on packaging waste, many manufacturers are evaluating sustainable packaging options that maintain product integrity while reducing environmental impact.
| Material Type | Typical Application | Sealing Temperature Range |
|---|---|---|
| PET Bottles | Still and sparkling water | N/A (cap sealing) |
| Multi-layer laminates | Sachets and stick packs | 120°C – 180°C |
| Aluminum foil composite | High-barrier liquid packaging | 140°C – 200°C |
| HDPE Containers | Bulk purified water | Induction or cap sealing |
Regulatory Compliance and Certifications
Water purification and packaging equipment must meet applicable regulatory standards for your target markets. For pharmaceutical-grade water, compliance with USP, EP, or JP pharmacopeia standards is mandatory. Food-grade water packaging requires adherence to FDA, EU, or local food safety regulations. Machines should be constructed from 316L stainless steel for product contact parts, with sanitary design principles applied throughout.
Look for equipment that supports IQ/OQ/PQ validation protocols if you operate in regulated industries. Documentation packages, including material certificates, electrical schematics, and maintenance manuals, should be available as part of the equipment purchase.
After-Sales Support and Long-Term Partnership
A packaging machine is a long-term investment. Evaluate the manufacturer’s technical support, spare parts availability, and service network before committing. Remote troubleshooting capabilities, operator training programs, and preventive maintenance plans contribute significantly to equipment uptime and operational efficiency.
Experienced manufacturers like Ludyway Machinery provide comprehensive support throughout the project lifecycle, from initial machine selection and packaging solution design to installation, commissioning, and ongoing technical assistance. With a global footprint serving customers in more than 100 countries, reliable after-sales service ensures your equipment continues performing optimally in the long term.
Key Questions to Ask Your Equipment Supplier
- What purification technology is best suited for my source water quality?
- Can the machine handle multiple packaging formats if my product line expands?
- What are the total cost of ownership projections, including consumables and maintenance?
- Is remote diagnostic support available after installation?
- What lead time should I expect for critical spare parts?
Integration with Existing Production Infrastructure
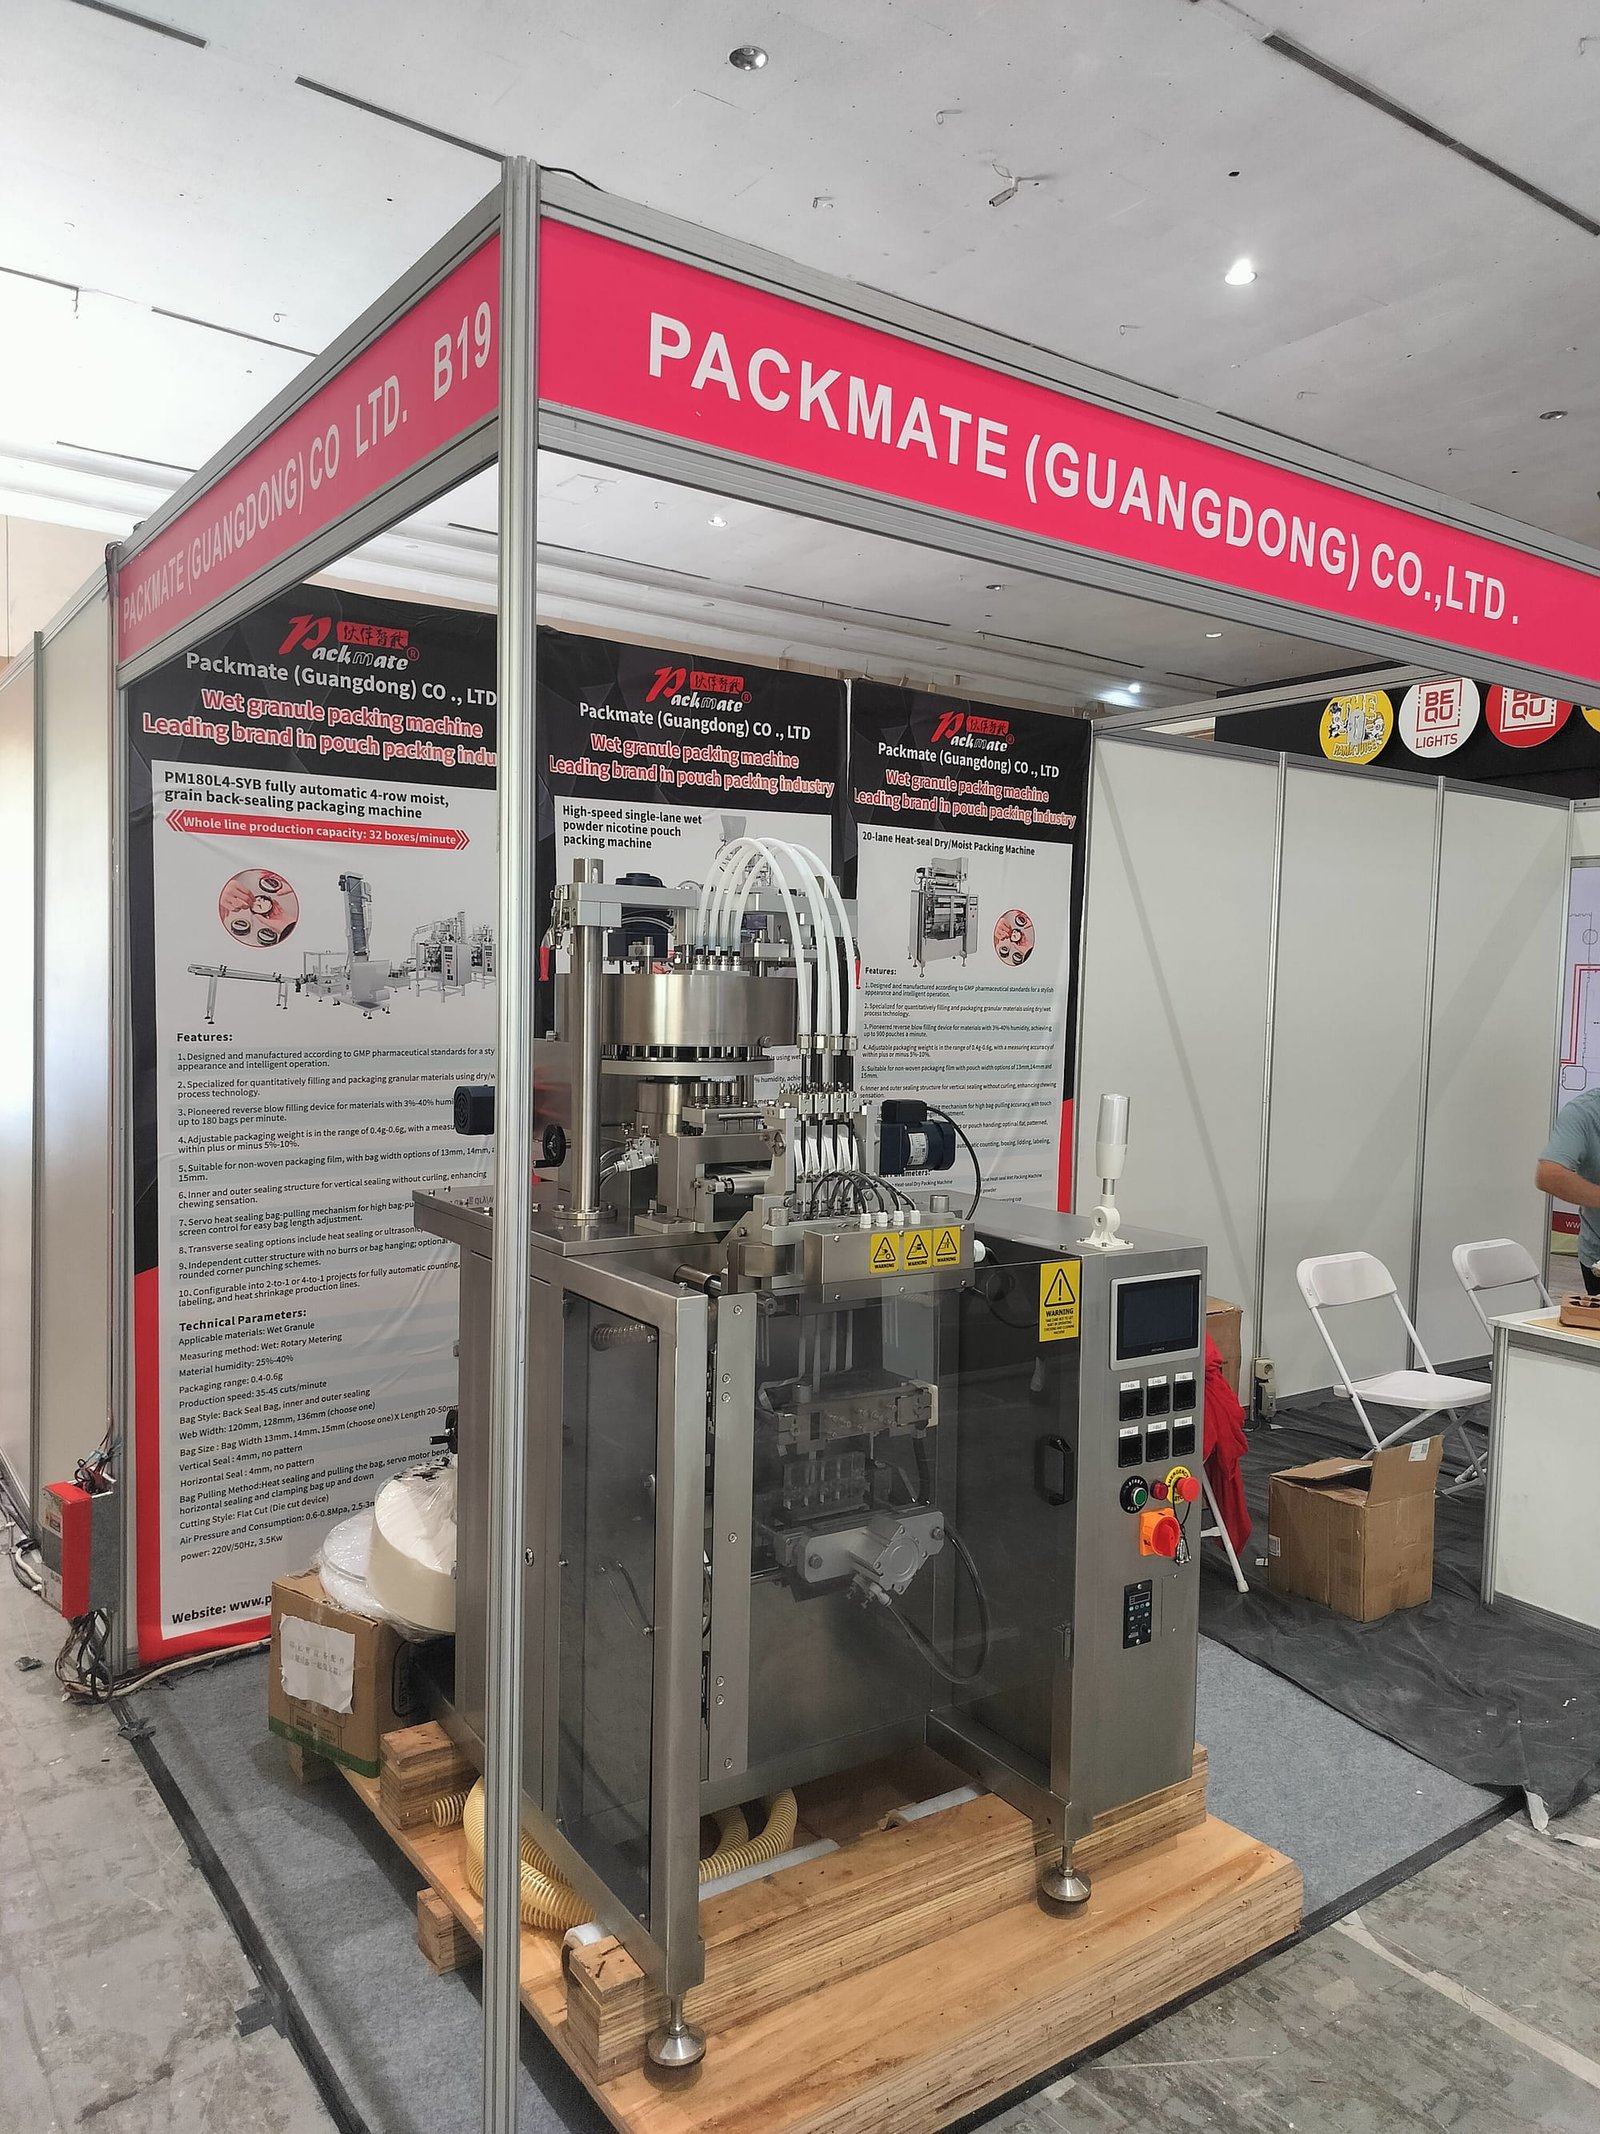
Your new water purification and packaging machine must integrate seamlessly with upstream and downstream processes. Consider conveyor connections, water supply lines, compressed air requirements, and electrical specifications. A well-designed system will include buffer tanks, product accumulators, and rejection systems to maintain line efficiency during minor interruptions.
For facilities with limited floor space, compact vertical designs or monobloc configurations can combine multiple processing steps in a single machine footprint. Always request a detailed layout drawing and utility requirements list during the quotation phase to avoid costly installation modifications later.
Budget Planning and ROI Analysis
Beyond the initial purchase price, factor in installation, training, validation, and ongoing operational costs. A higher upfront investment in a quality machine often translates to lower total cost of ownership through reduced downtime, less material waste, and longer service life. Calculate your expected return on investment (ROI) based on labor savings, increased throughput, and reduced product loss.
| Cost Category | Percentage of Total Investment | Annual Maintenance Estimate |
|---|---|---|
| Equipment purchase | 65% – 75% | 2% – 5% of equipment cost |
| Installation and commissioning | 10% – 15% | N/A (one-time) |
| Training and validation | 5% – 10% | Optional refresher training |
| Consumables and spare parts | 5% – 10% | Varies by production volume |
Testing and Validation Before Final Decision
Whenever possible, conduct factory acceptance testing (FAT) with your actual product and packaging materials. This allows you to verify machine performance, fill accuracy, seal integrity, and overall equipment effectiveness before shipment. Many manufacturers offer trial runs and sample production services to demonstrate machine capabilities.
Review the warranty terms carefully. A standard warranty typically covers 12 to 24 months from installation or shipment, but extended warranties and service contracts may be available. Clarify whether the warranty includes on-site service, parts replacement, and travel expenses for technicians. Reference industry packaging machinery market data can help benchmark performance expectations and pricing norms.
Making the Final Selection
Choosing the right water purification and packaging machine requires balancing technical specifications, regulatory compliance, production requirements, and long-term support. A methodical evaluation process that includes product testing, supplier assessment, and total cost analysis will yield the best results. Engage with experienced packaging machinery partners who understand your specific industry challenges and can provide customized solutions rather than off-the-shelf equipment that may not fully meet your needs.
For manufacturers seeking a reliable long-term partner, Ludyway Packaging Machinery offers comprehensive water purification and packaging solutions backed by over 30 years of industry experience. The company provides customized machine configurations, turnkey production line integration, and ongoing technical support to help manufacturers achieve efficient, scalable, and compliant packaging operations worldwide.