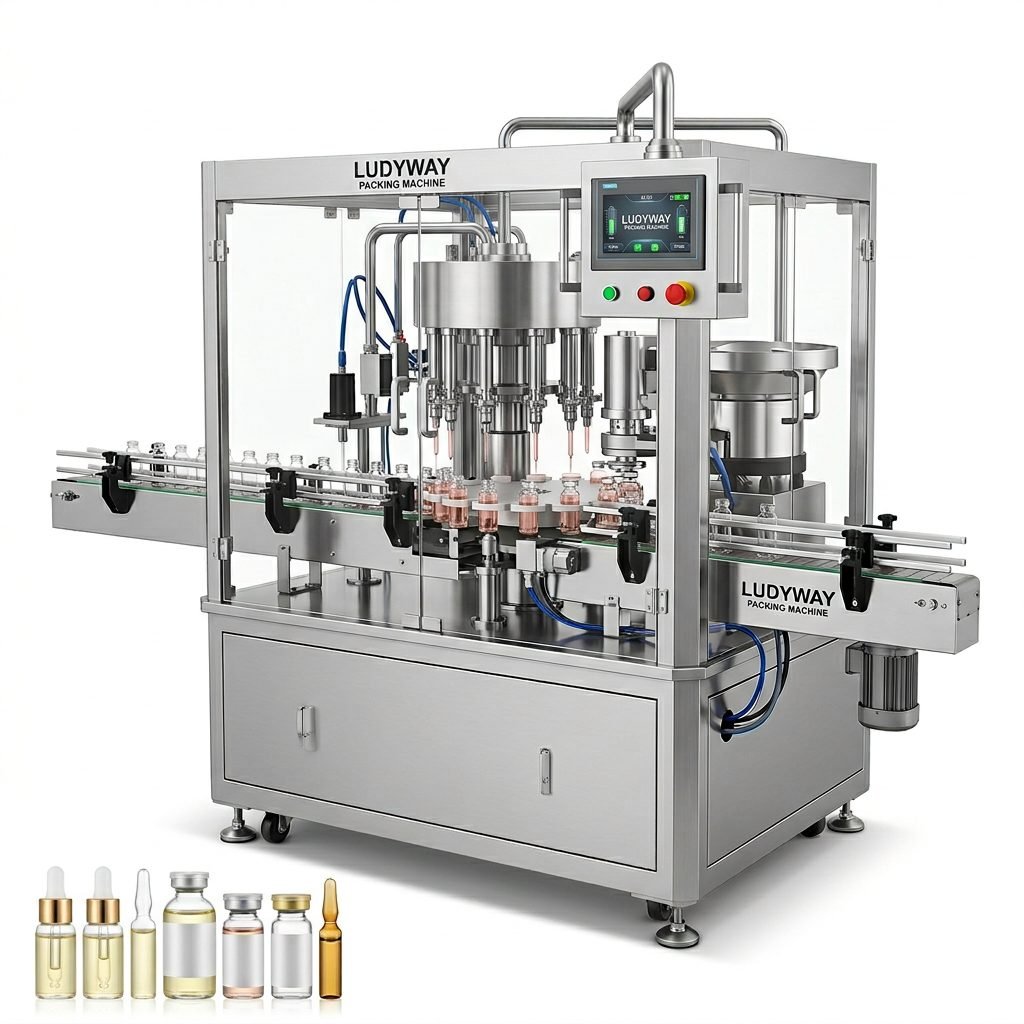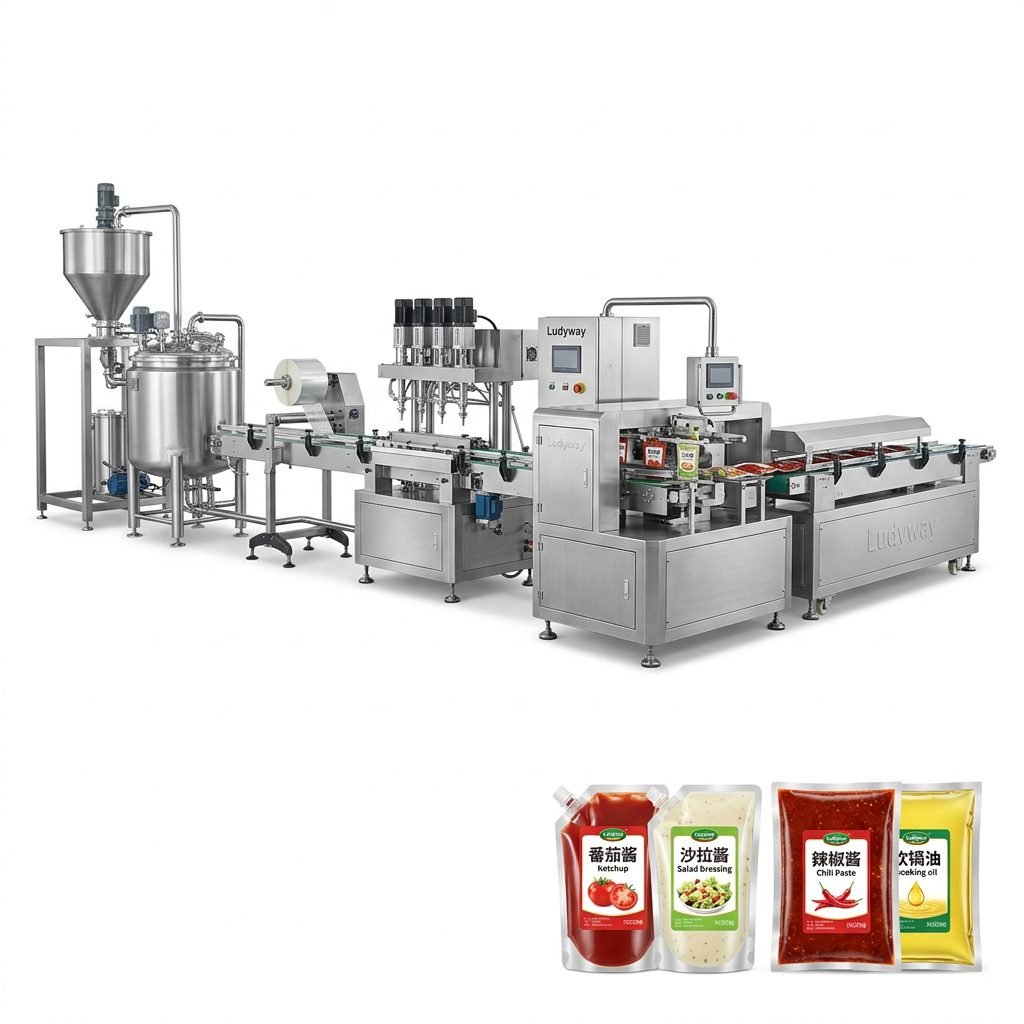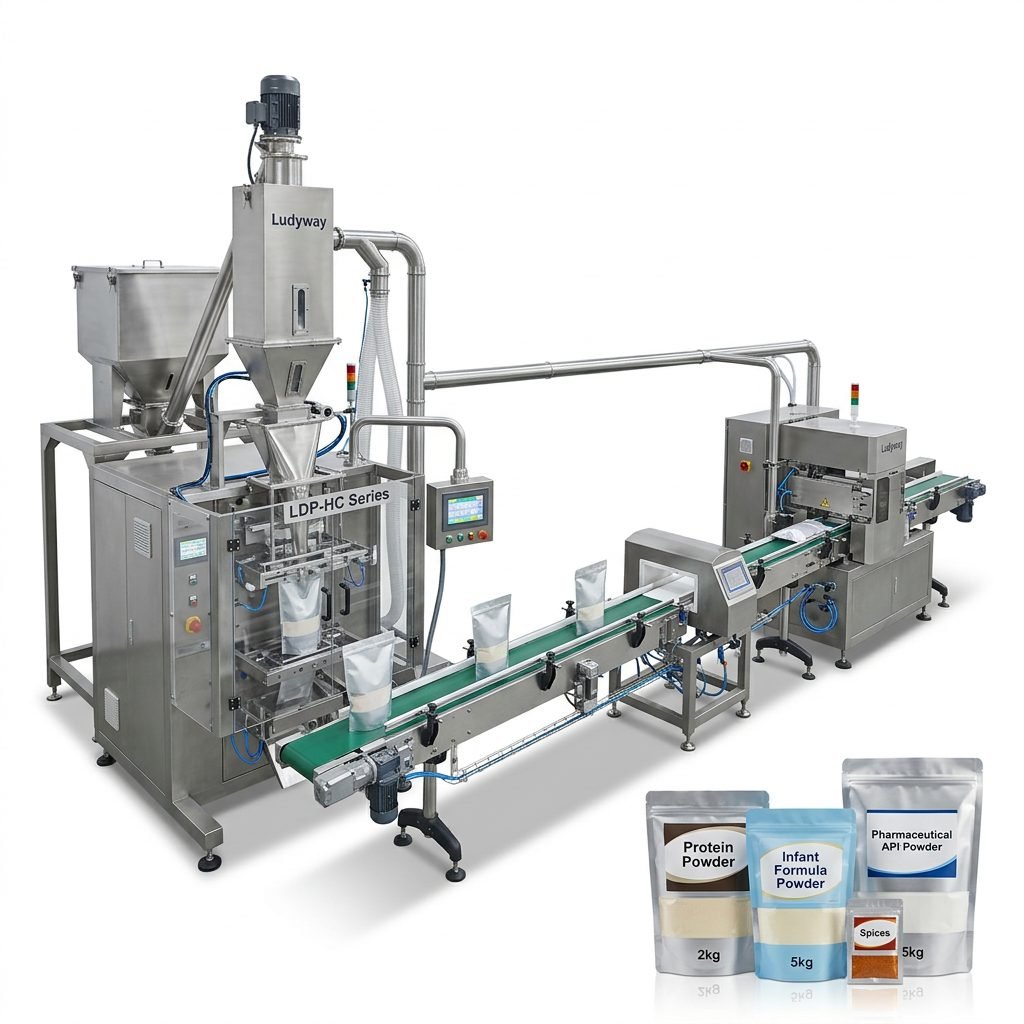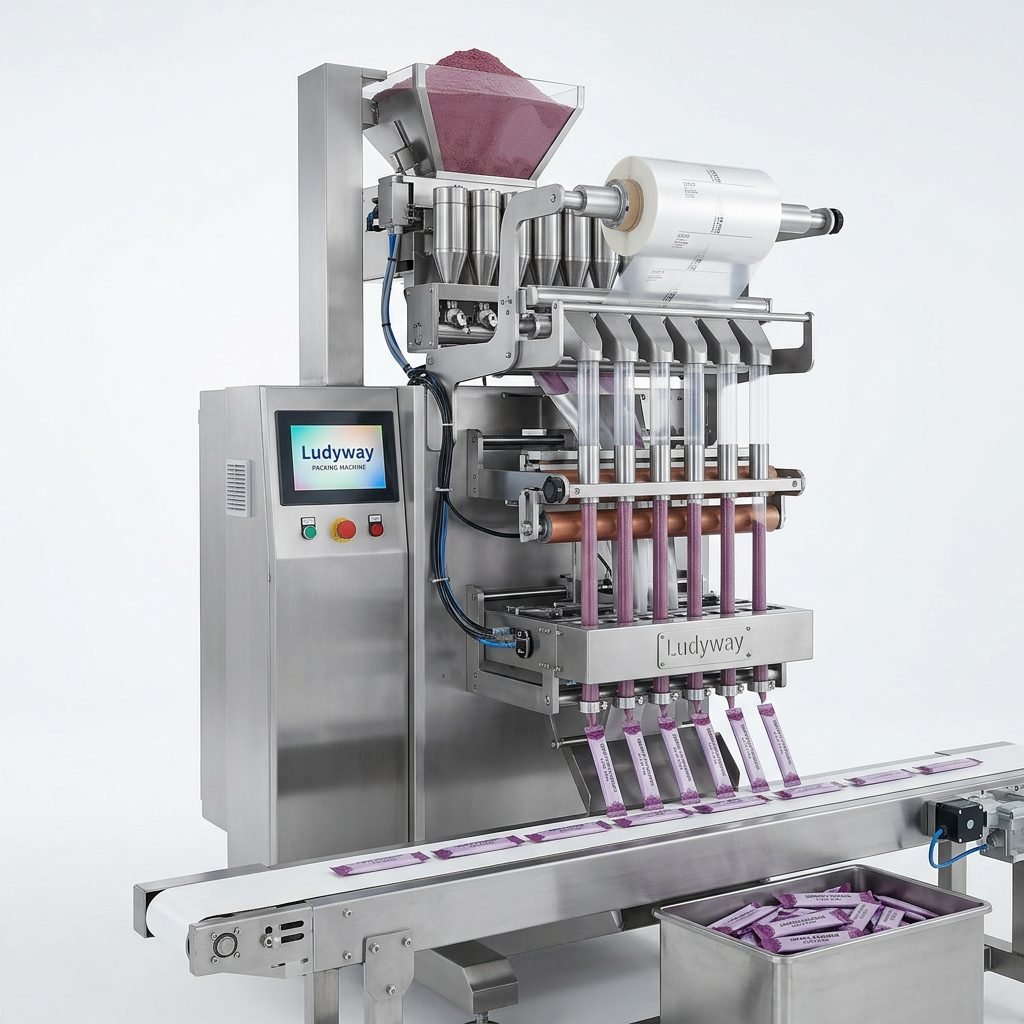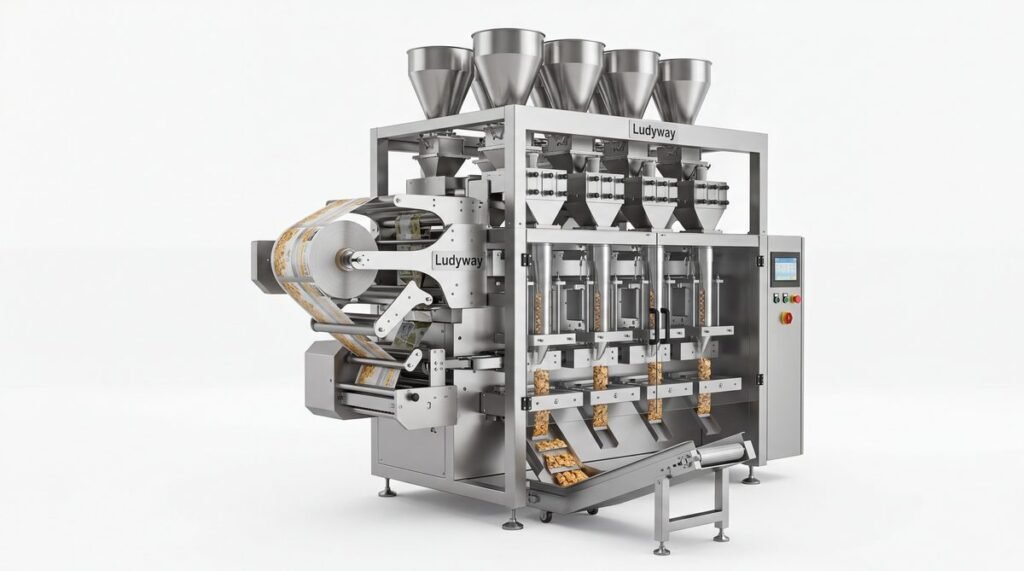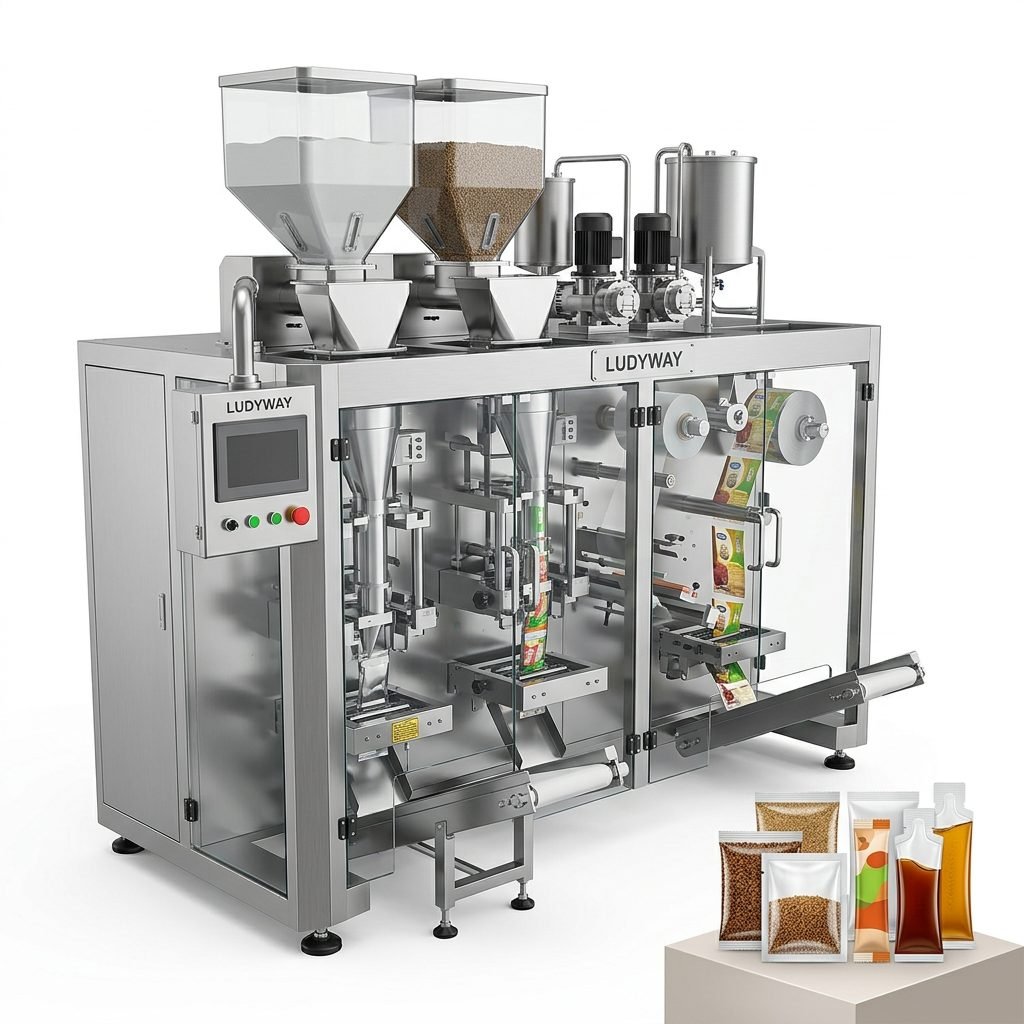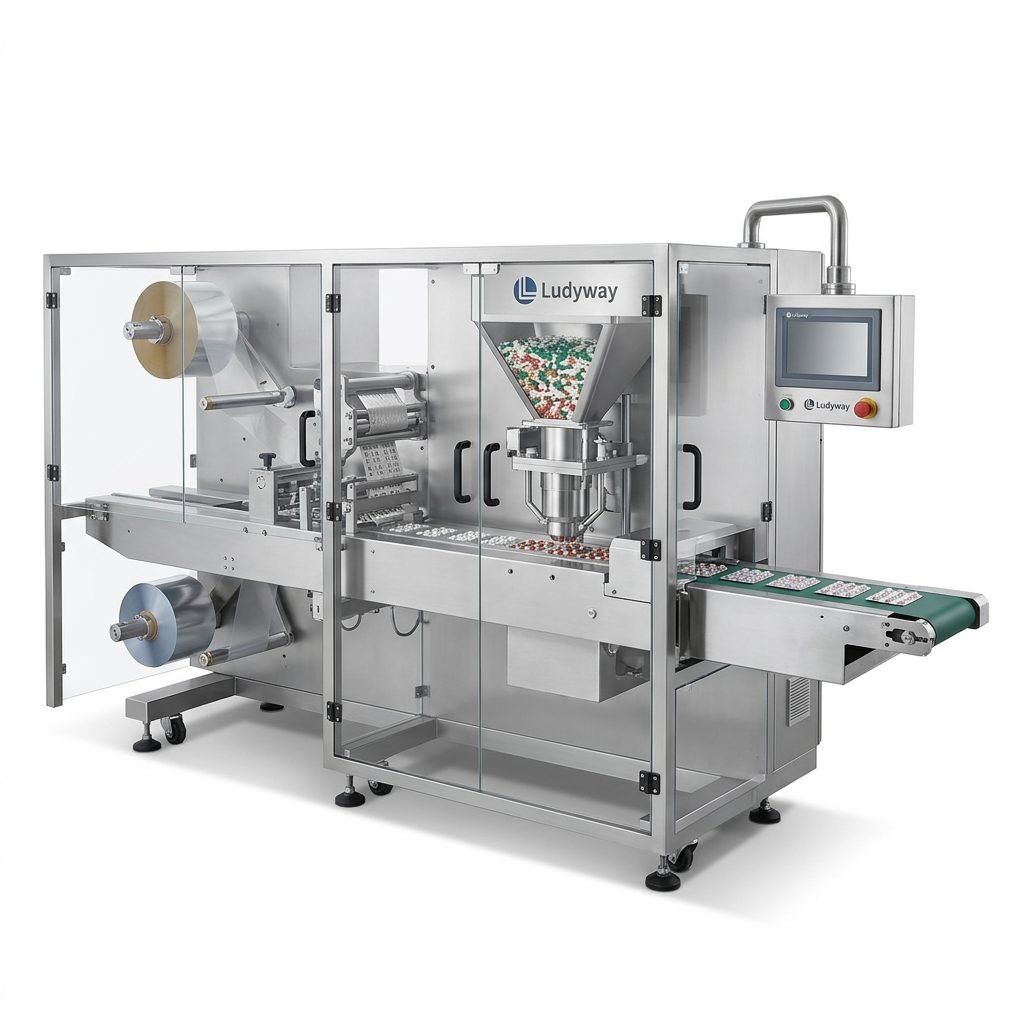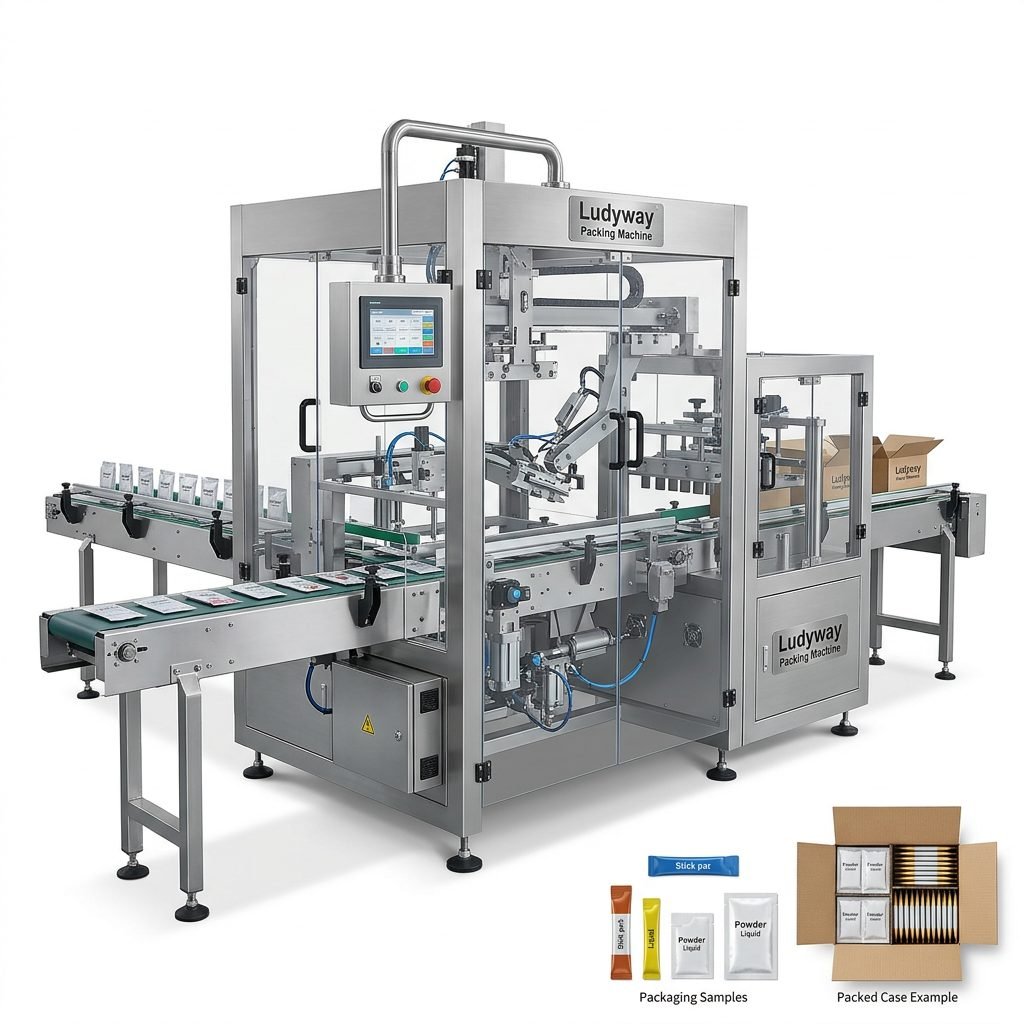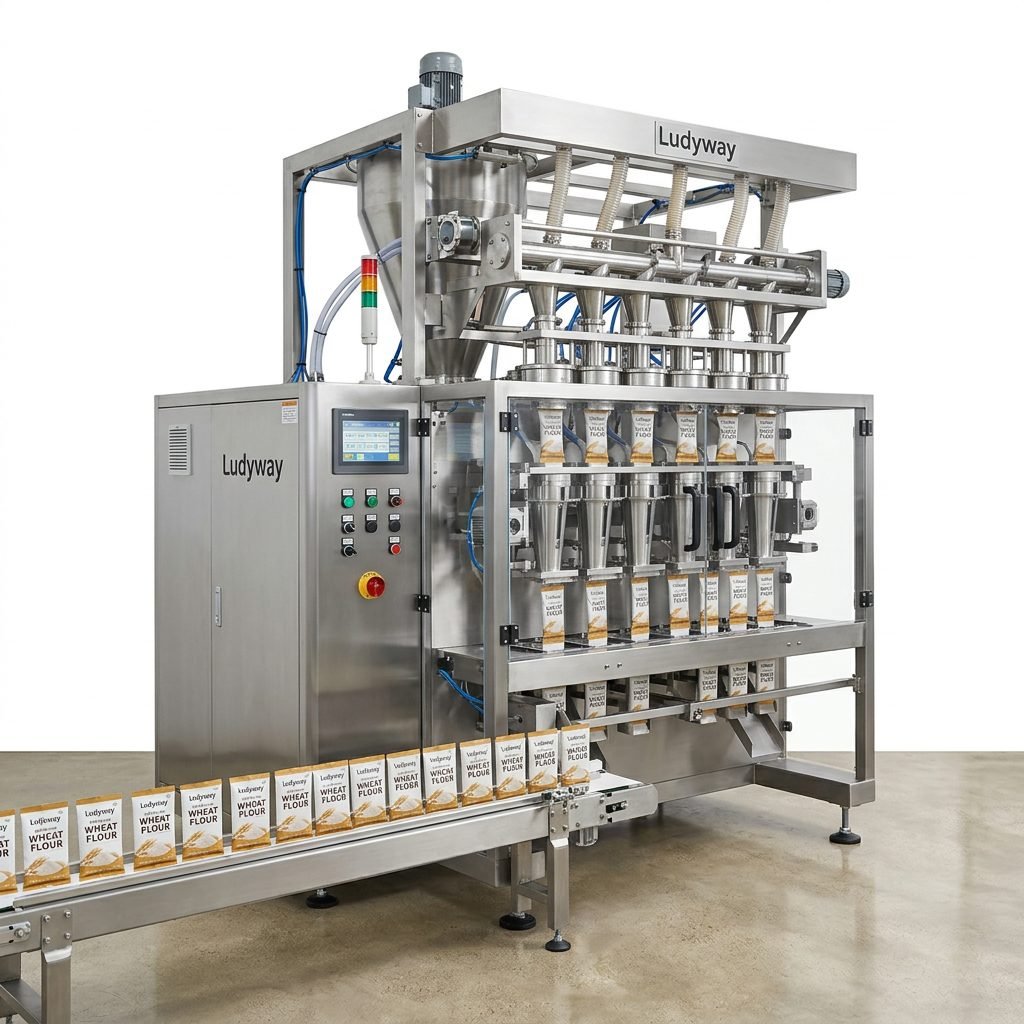
In today’s competitive global marketplace, selecting the right packaging equipment can make the difference between operational efficiency and costly downtime. For businesses handling food, pharmaceuticals, cosmetics, or industrial goods, small vacuum packaging machines have emerged as a critical investment. These compact yet powerful systems offer precise sealing, extended product shelf life, and remarkable versatility across diverse industries. Understanding why certain models outperform others requires a closer look at engineering quality, customization capabilities, and long-term reliability—areas where Ludyway small vacuum packaging machines consistently deliver exceptional value.
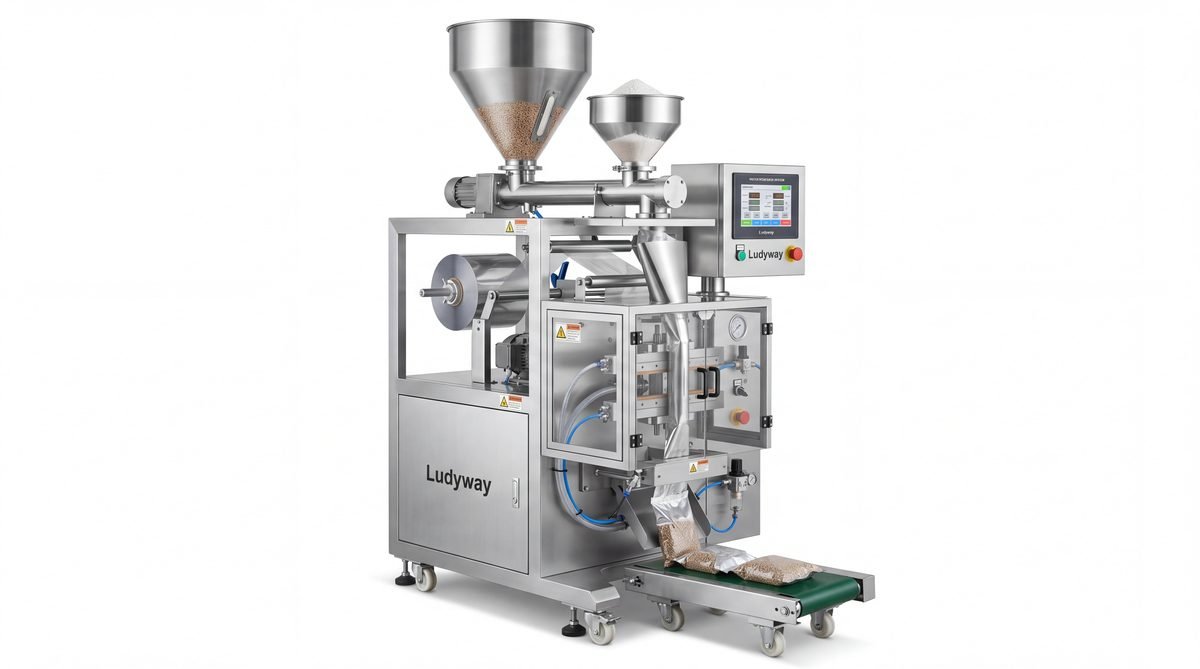
Understanding the Global Demand for Compact Vacuum Packaging
The global packaging machinery market continues to expand rapidly, driven by increasing consumer demand for convenience, food safety, and extended product freshness. Small and medium-sized enterprises, in particular, require equipment that balances footprint with performance. Unlike massive industrial lines that demand extensive floor space and infrastructure, compact vacuum packaging solutions enable businesses to achieve professional-grade results without overwhelming their production facilities.
According to industry data from the PMMI Business Intelligence Library, the demand for flexible packaging machinery has seen consistent year-over-year growth, with vacuum sealing technologies playing an increasingly vital role across multiple sectors. This trend underscores the importance of choosing equipment that can adapt to evolving market needs.
Key Industries Benefiting from Small Vacuum Packaging Machines
- Food processing — preserving freshness in coffee, nuts, dried fruits, spices, and snack products
- Pharmaceutical manufacturing — ensuring product integrity for powders, granules, and medical devices
- Cosmetics and personal care — safeguarding serums, creams, and single-use formulations
- Pet food and nutrition — maintaining quality in kibble, treats, and supplement packaging
- Industrial and chemical products — protecting moisture-sensitive materials and additives
What Sets Premium Small Vacuum Packaging Machines Apart
Not all vacuum packaging equipment is created equal. When evaluating options for your production line, several critical factors determine whether a machine will deliver consistent results over years of operation. The most successful global businesses prioritize build quality, automation capabilities, and after-sales support above initial price considerations.
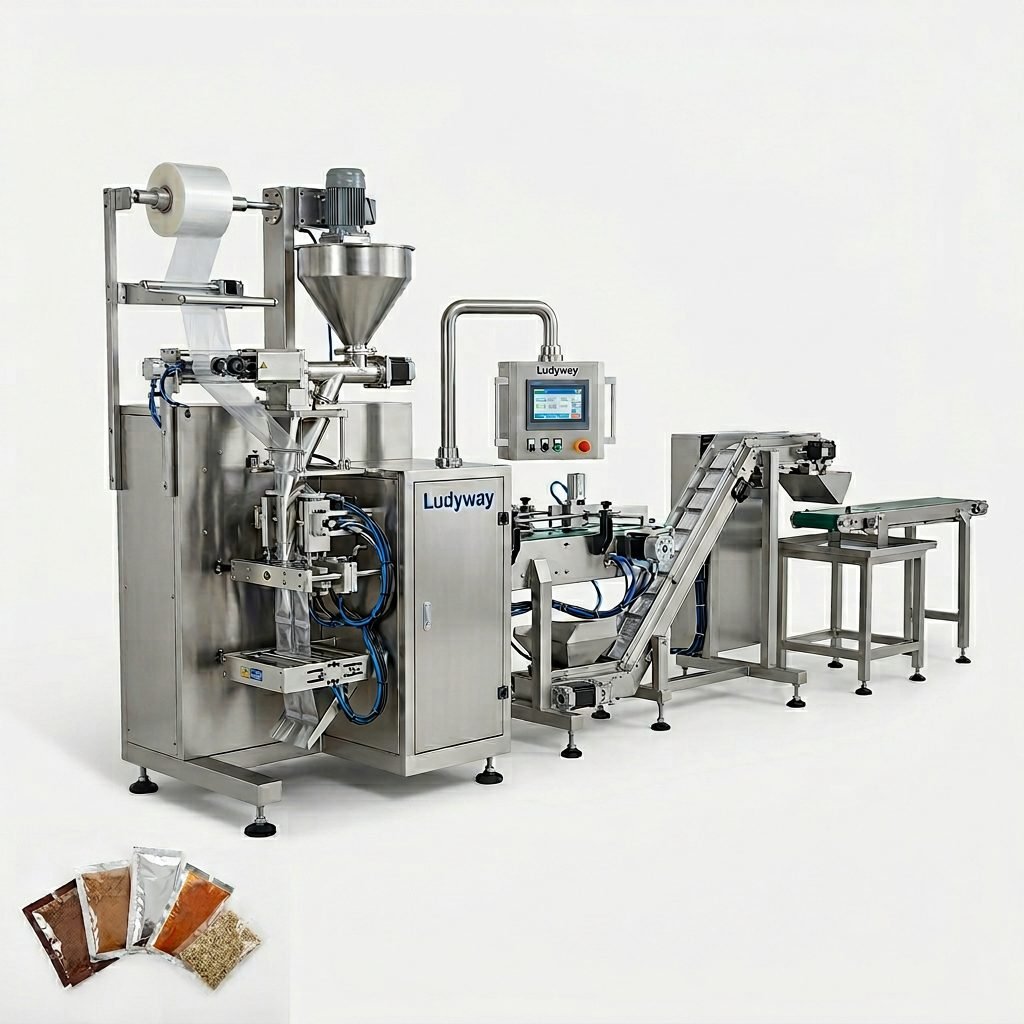
Precision Engineering and Material Quality
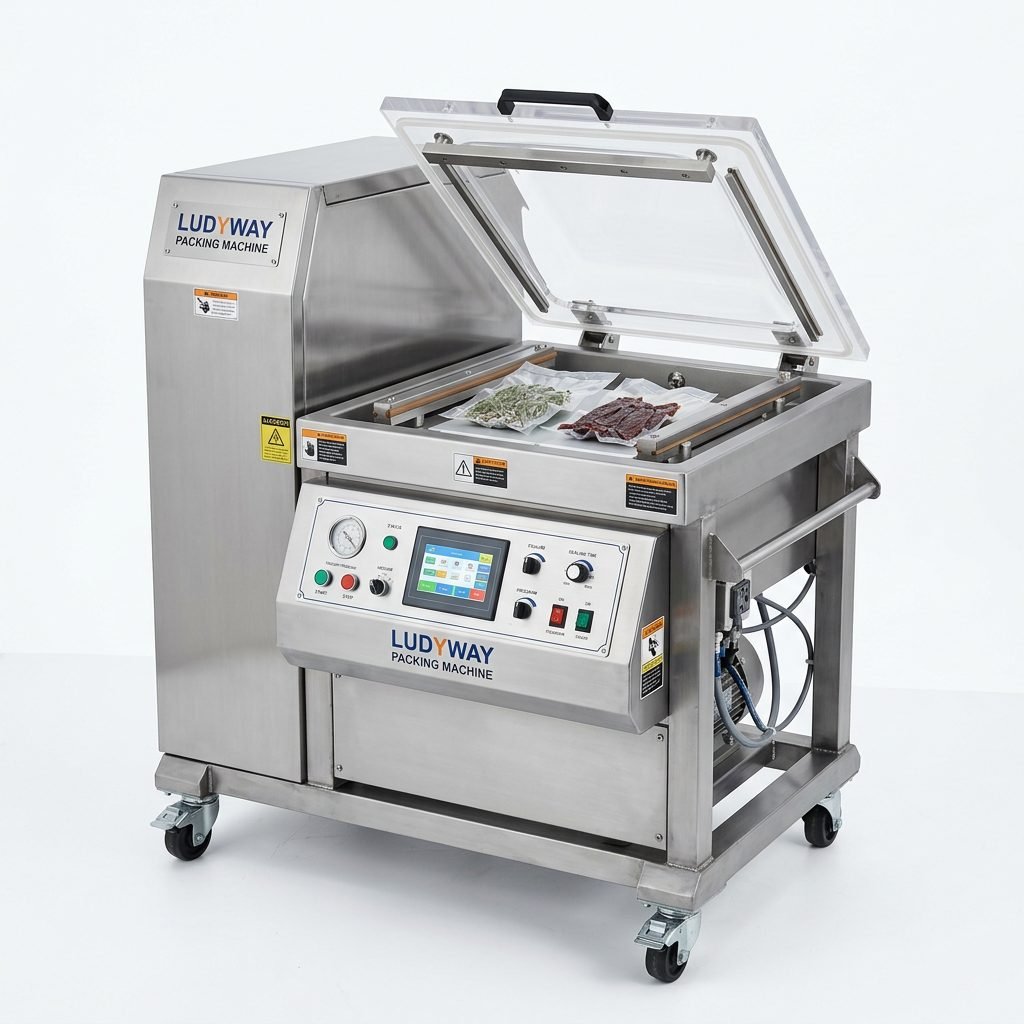
Top-tier manufacturers utilize stainless steel construction, precision-machined components, and industry-standard electrical systems to ensure durability in demanding production environments. The chamber design, sealing bar configuration, and vacuum pump specifications directly impact performance. Equipment built with food-grade materials and compliant with international safety standards provides peace of mind for exporters serving regulated markets.
Automation and Control Features
Modern packaging equipment incorporates intelligent control systems that allow operators to fine-tune vacuum levels, sealing times, and temperature parameters. PLC interfaces with touchscreen operation reduce training requirements while improving consistency across production batches. Programmable recipe storage enables quick changeovers between different product types and packaging formats—a crucial advantage for contract packagers and multi-product manufacturers.
Cost-Effectiveness and Return on Investment
While the initial purchase price of a small vacuum packaging machine represents a significant consideration, forward-thinking businesses evaluate total cost of ownership. Factors such as energy efficiency, maintenance requirements, spare parts availability, and expected service life all contribute to the true economic picture. Premium machines may command higher upfront investment but typically deliver lower lifetime costs through reduced downtime and consistent output quality.
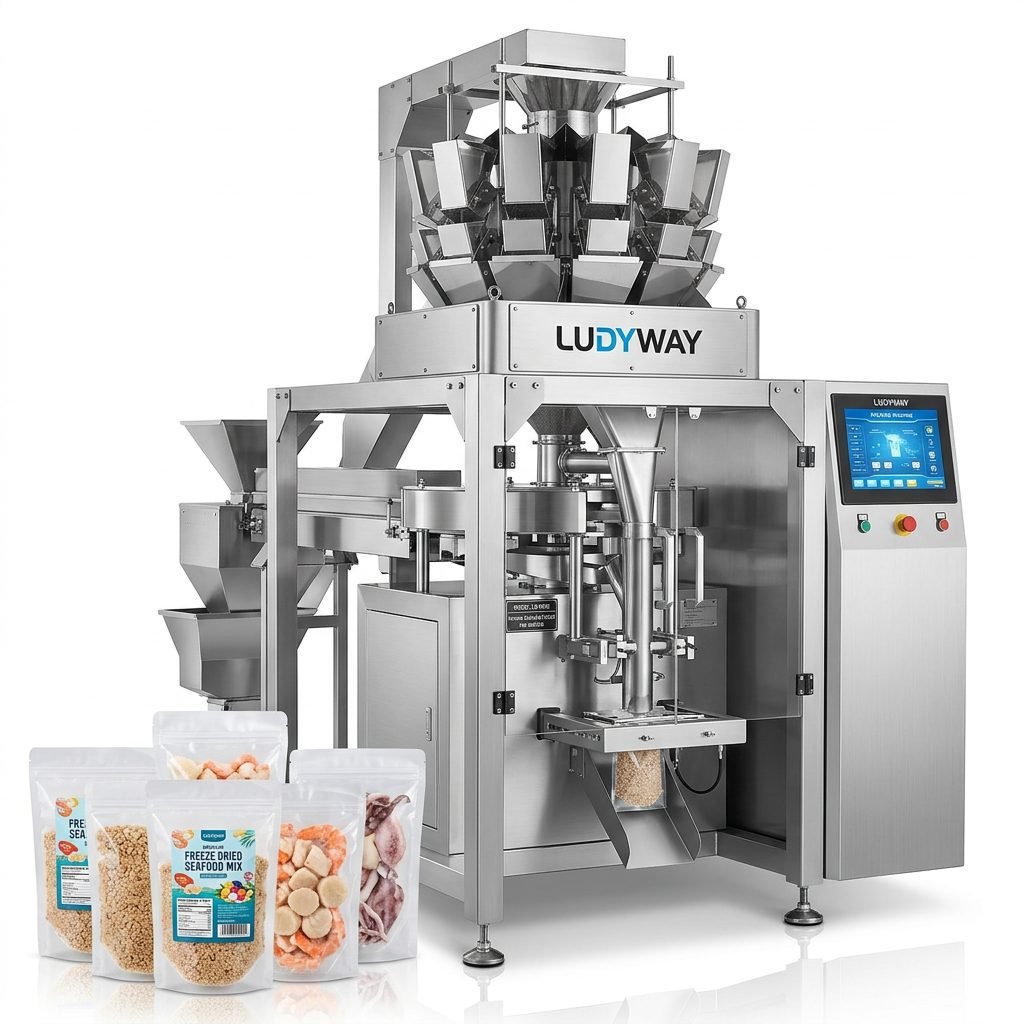
Comparing Small Vacuum Packaging Machine Specifications
| Feature | Entry-Level Machines | Professional-Grade Machines |
|---|---|---|
| Chamber Material | Aluminum or basic steel | 304/316 stainless steel |
| Vacuum Pump | Standard oil pump | High-efficiency Busch or equivalent |
| Control System | Manual or basic digital | PLC with touchscreen HMI |
| Sealing Quality | Single-bar heating | Dual-bar with temperature control |
| Compliance | Limited certifications | CE, ISO, FDA-compatible design |
| Warranty & Support | 1 year, limited coverage | Extended warranty with global support |
Application Versatility Across Product Categories
One of the most compelling advantages of modern small vacuum packaging systems is their ability to handle an extraordinary range of products. Whether you are sealing moisture-sensitive powders, oxygen-reactive food products, or sterile medical components, the right equipment configuration ensures optimal results. This versatility explains why businesses across diverse packaging industry segments continue to invest in vacuum technology.
Granule and Powder Packaging Excellence
Free-flowing products such as coffee grounds, protein powders, spices, and nutritional supplements benefit tremendously from vacuum packaging. By removing ambient air before sealing, these machines prevent oxidation, preserve volatile flavor compounds, and inhibit moisture absorption. The result is a product that maintains its original quality from the production facility to the end consumer, even across extended international supply chains.
Liquid and Semi-Liquid Product Protection
Vacuum sealing technology extends well beyond dry products. Small vacuum packaging machines equipped with appropriate chamber configurations effectively seal liquids, gels, and pastes without compromising product integrity or creating messy spills. This capability proves invaluable for cosmetics manufacturers, food producers packaging sauces and marinades, and pharmaceutical companies handling liquid formulations.
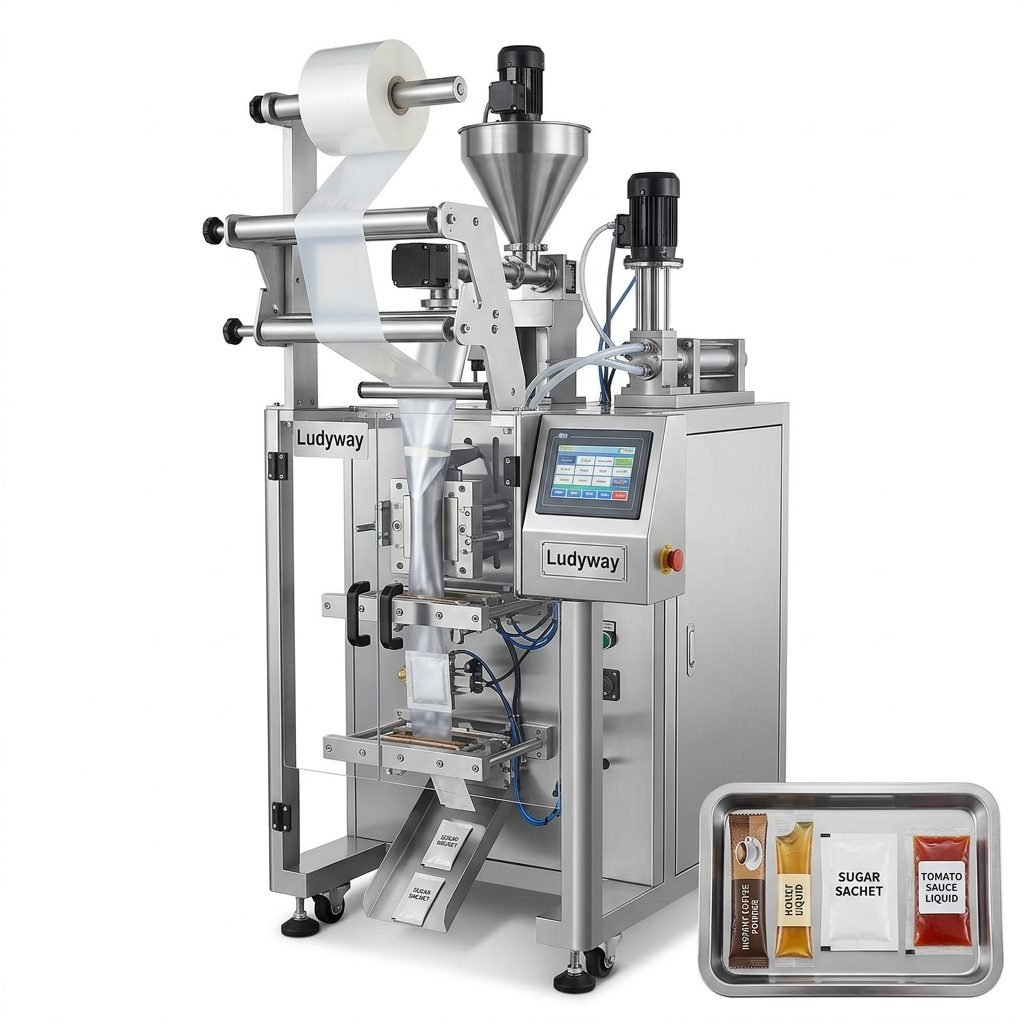
Global Supply Chain and Support Infrastructure
For international buyers, the decision to invest in packaging machinery extends beyond the equipment itself. Reliable technical support, accessible spare parts, and responsive service form the backbone of a successful long-term partnership. Manufacturers with established global distribution networks and multilingual support teams provide significant advantages for businesses operating across multiple regions.
Why Manufacturing Excellence Matters
Ludyway operates one of the largest packaging machine manufacturing facilities in China, spanning over 20,000㎡ with more than 50 intelligent packaging machine models serving customers in over 100 countries. This scale enables rigorous quality control, continuous innovation, and competitive pricing that directly benefits global buyers seeking turnkey packaging solutions. According to recent industry analysis published by EIN Presswire, packaging machinery exports from leading manufacturers continue to demonstrate strong growth trajectories.
Integration with Complete Production Lines
While standalone small vacuum packaging machines serve many applications effectively, forward-thinking businesses often consider future scalability. Equipment that integrates seamlessly with upstream and downstream processes—including weighers, conveyors, labeling systems, and cartoning machines—protects your initial investment while creating a clear path for production expansion.
Key Integration Considerations
- Communication protocols — ensuring compatibility with existing PLC and SCADA systems
- Physical footprint — optimizing floor layout for efficient material flow
- Changeover speed — minimizing downtime between product runs
- Data collection — enabling traceability and quality documentation for regulated industries
Energy Efficiency and Sustainability
Modern packaging operations increasingly prioritize environmental responsibility alongside productivity. Advanced vacuum pump technology, intelligent standby modes, and optimized sealing cycles reduce energy consumption without compromising output quality. These features not only lower operational costs but also support corporate sustainability initiatives—an increasingly important factor for brands serving environmentally conscious consumers and retailers.
Making the Right Choice for Your Business
Selecting the ideal small vacuum packaging machine requires a thorough assessment of your current needs and future growth plans. Consider the range of products you will package, your target production volumes, available facility space, and the regulatory requirements of your destination markets. Engaging with manufacturers who offer comprehensive consultation and customization services ensures that your equipment investment aligns perfectly with your business objectives.
Additional Resources for Packaging Professionals
For further research on packaging industry standards and trends, the following authoritative resources provide valuable insights:
- PMMI Packaging Industry Resources — comprehensive guides and market research
- Flexible Packaging Association Industry Data — sector-specific reports and regulatory updates
- ISO Packaging Standards — international packaging and distribution standards
- FDA Food Packaging and Food Contact Substances — regulatory compliance guidance
Investing in the right vacuum packaging technology today positions your business for sustained growth, operational excellence, and competitive advantage in the global marketplace.