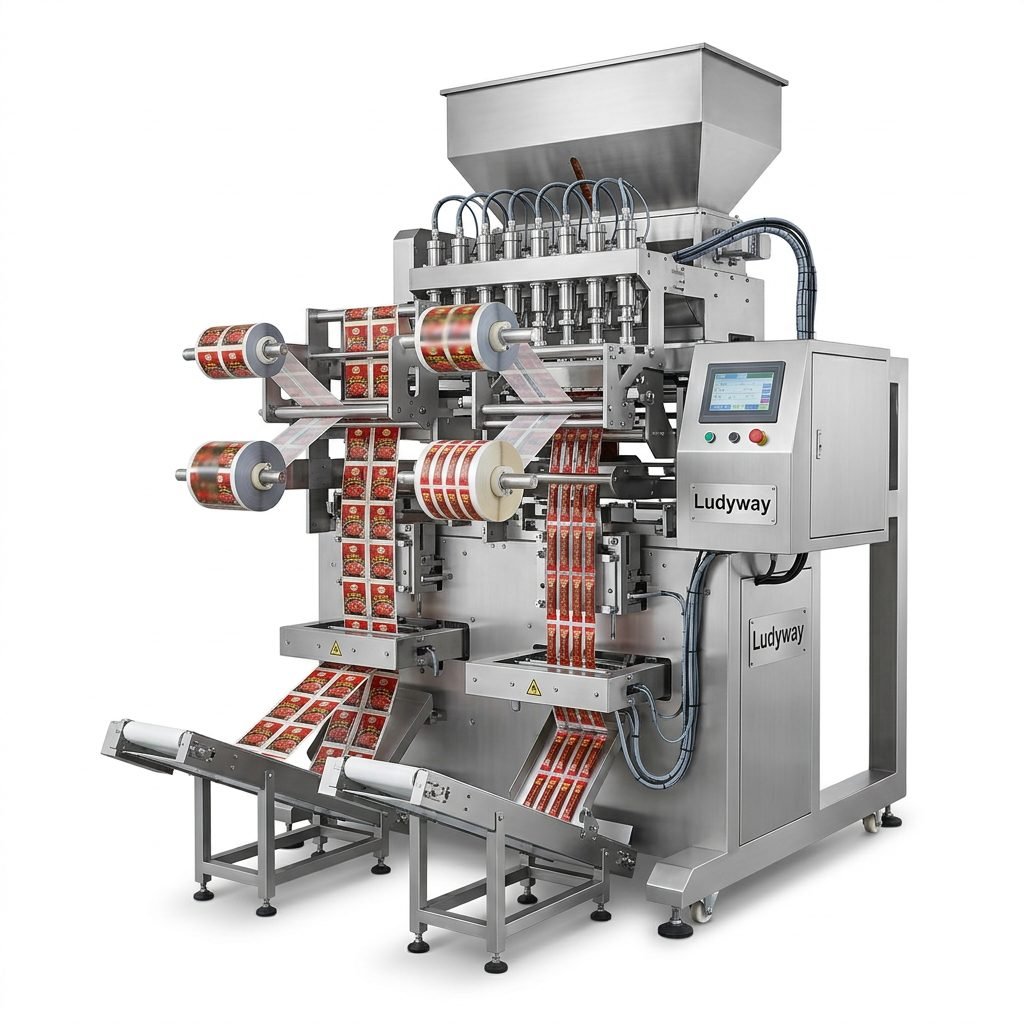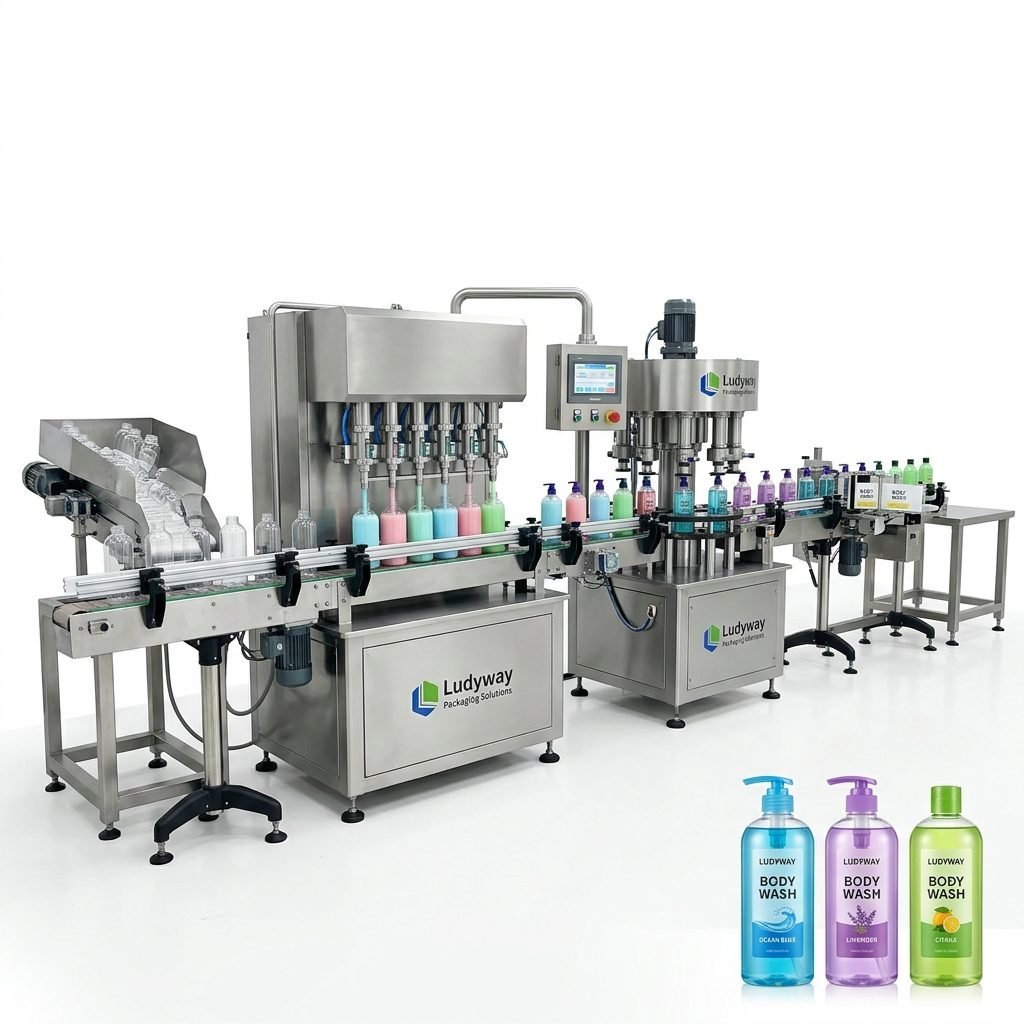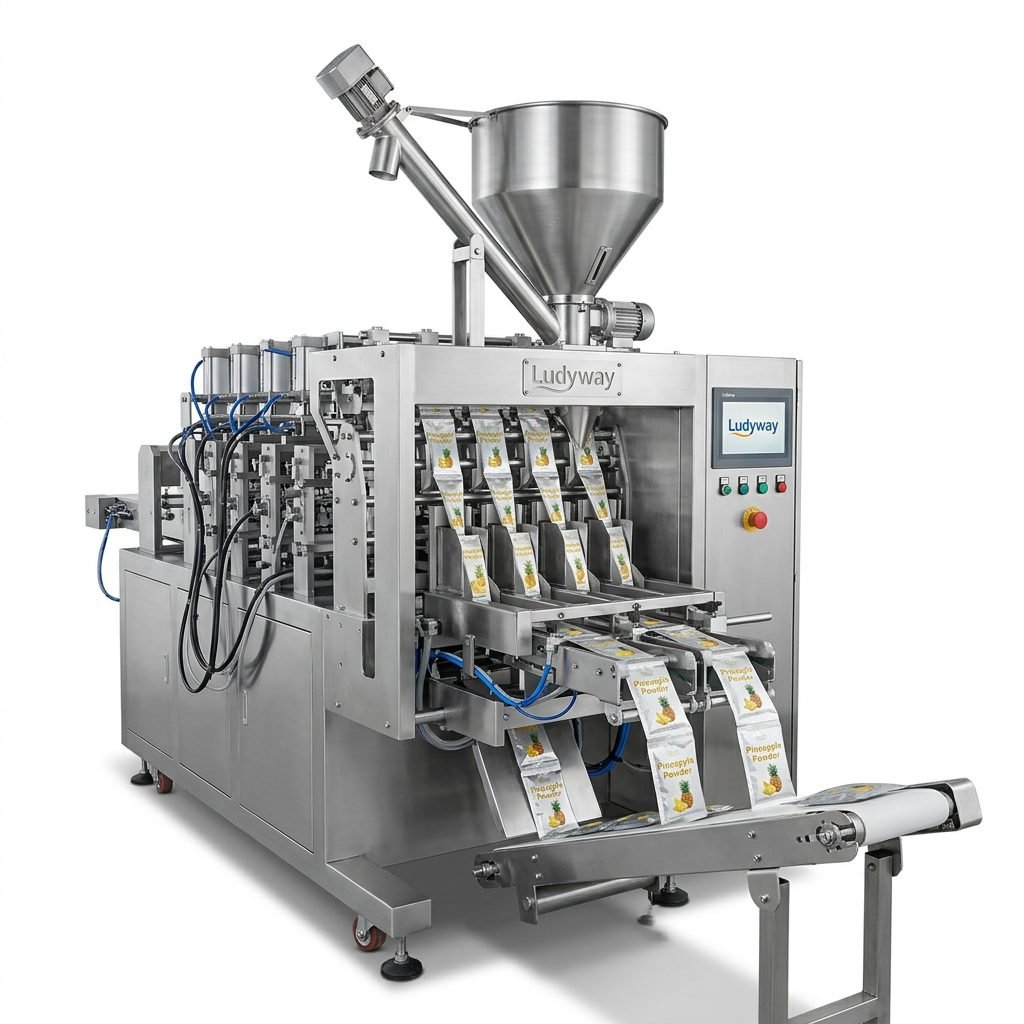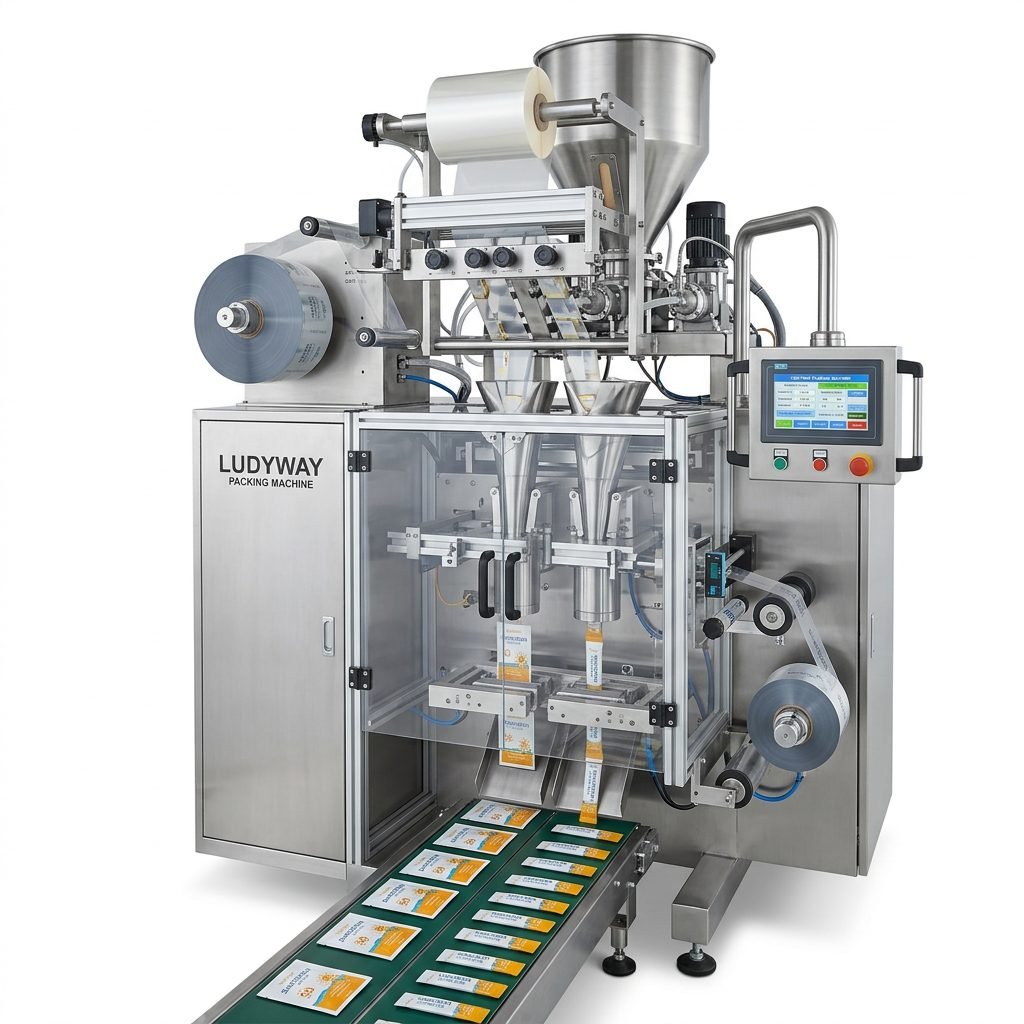
Setting up a small vacuum packaging machine production line in North America can be a transformative investment for food processors, pharmaceutical manufacturers, and industrial suppliers. Whether you are looking to extend product shelf life, improve hygiene standards, or enter new markets, a well-planned vacuum packaging system is essential. This guide walks you through every stage — from initial planning and equipment selection to installation, compliance, and ongoing optimization.
Why North American Manufacturers Are Investing in Vacuum Packaging
The North American vacuum packaging market continues to grow, driven by demand for extended shelf life, reduced food waste, and compliance with FDA and CFIA standards. Vacuum-sealed products retain freshness up to five times longer than non-vacuum alternatives, making this technology indispensable for FDA-regulated food packaging operations. Small to mid-sized producers are increasingly adopting in-house vacuum lines to reduce outsourcing costs and maintain quality control.
Key Components of a Small Vacuum Packaging Line
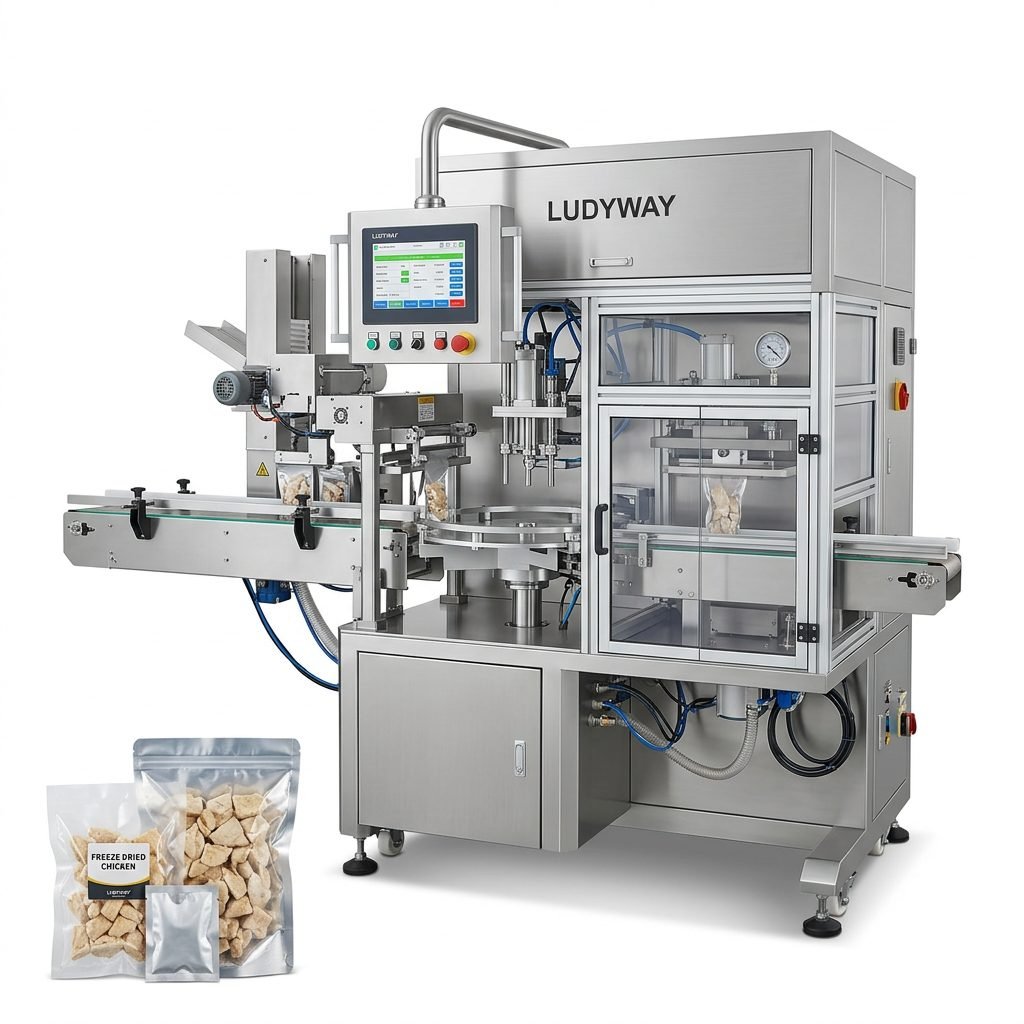
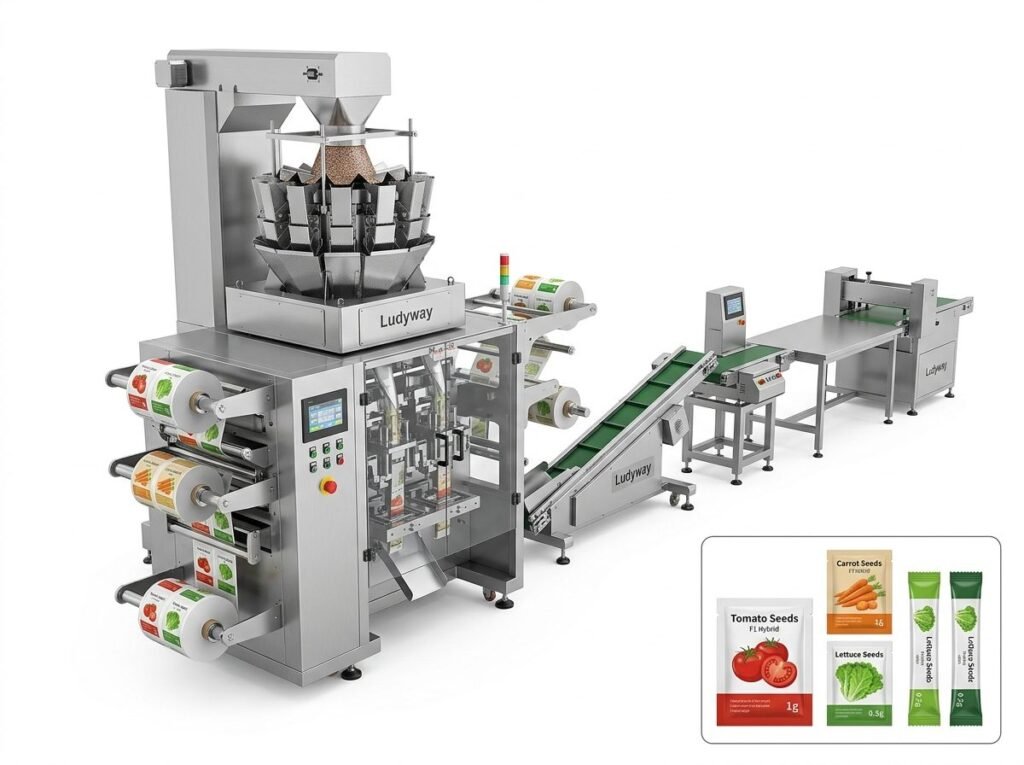
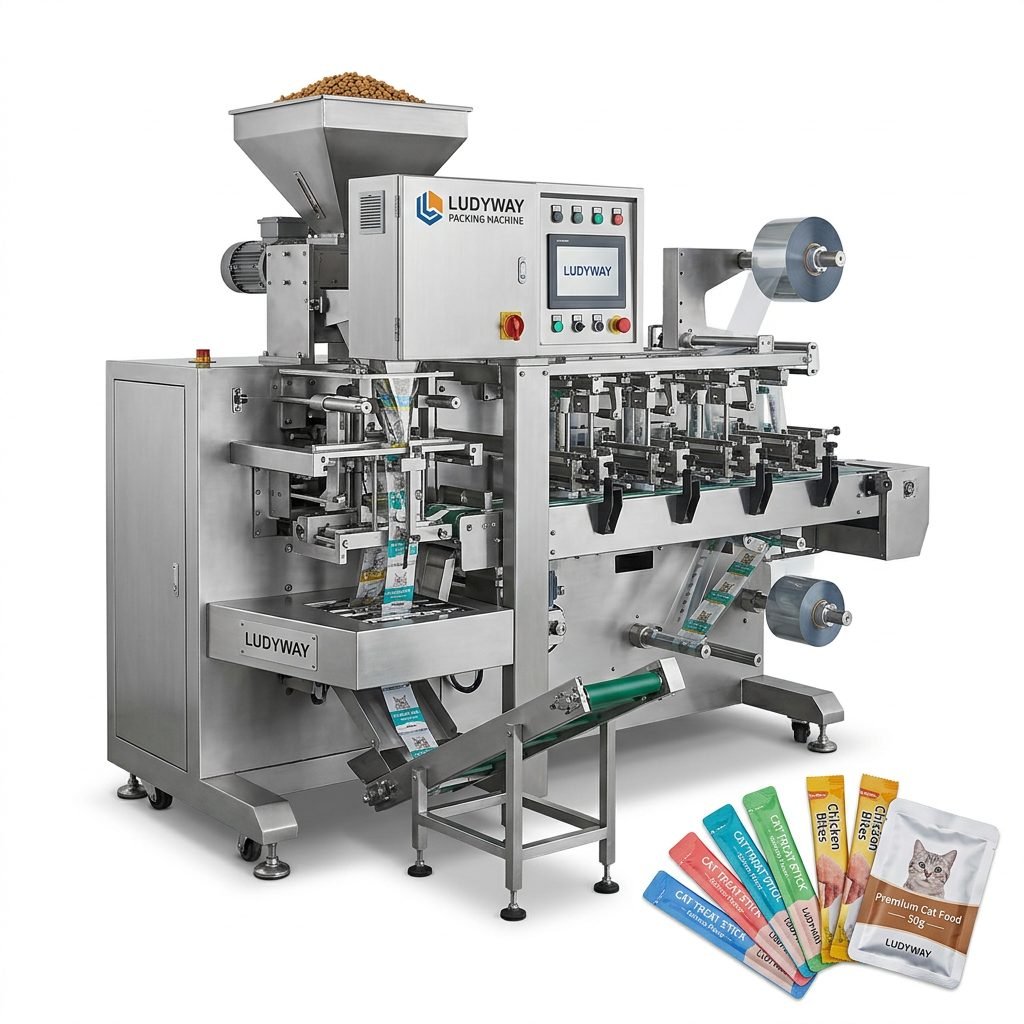
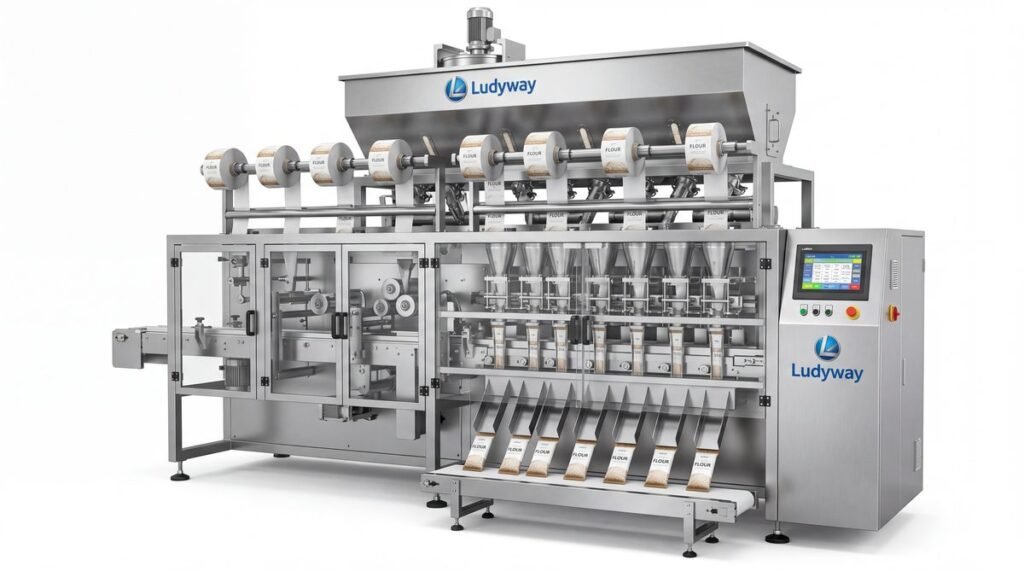
A complete small vacuum packaging production line typically integrates several core modules. Understanding each component helps you make informed procurement decisions and avoid costly bottlenecks. Below are the primary elements to consider:
| Component | Function | Selection Tips |
|---|---|---|
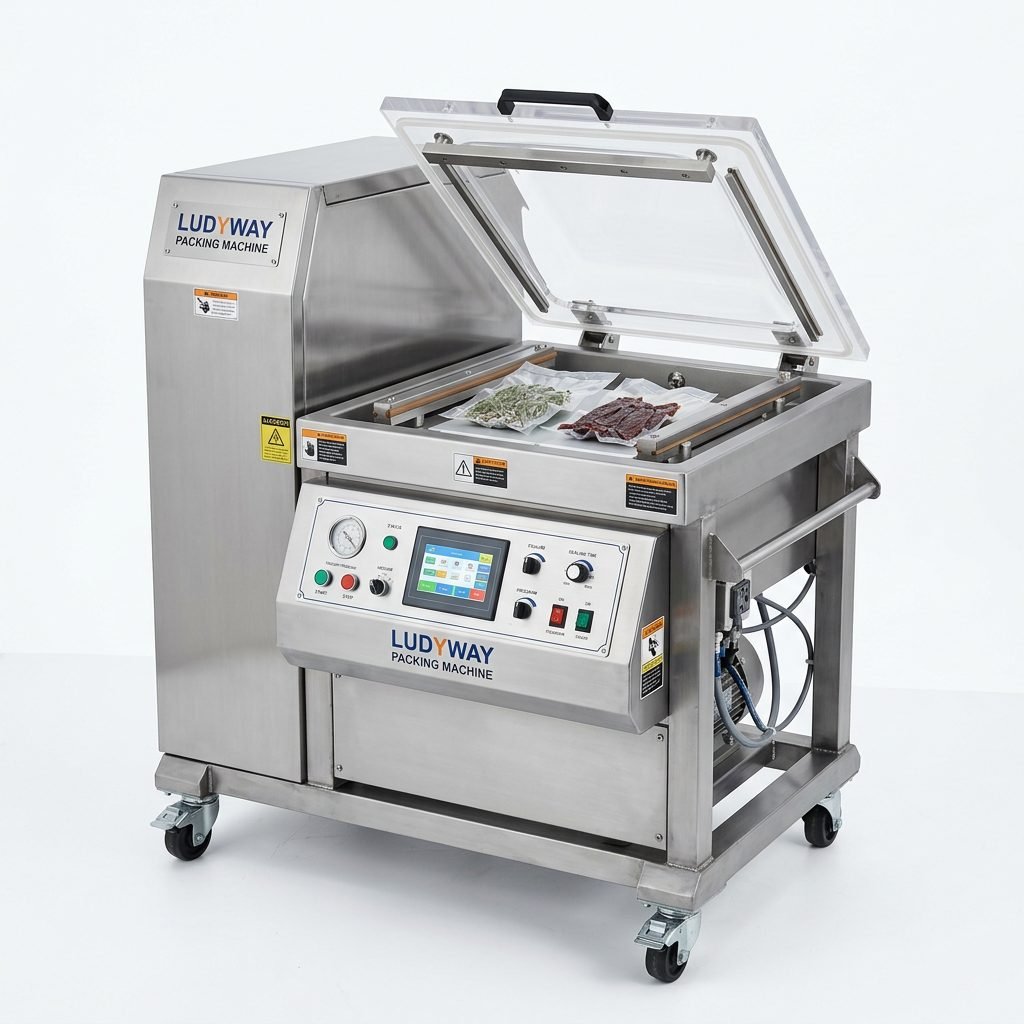
| Vacuum Chamber Machine | Removes air from the package and heat-seals the bag | Choose single or double chamber based on throughput needs |
| Conveyor Belt System | Transports products between stations | Stainless steel construction for food-grade compliance |
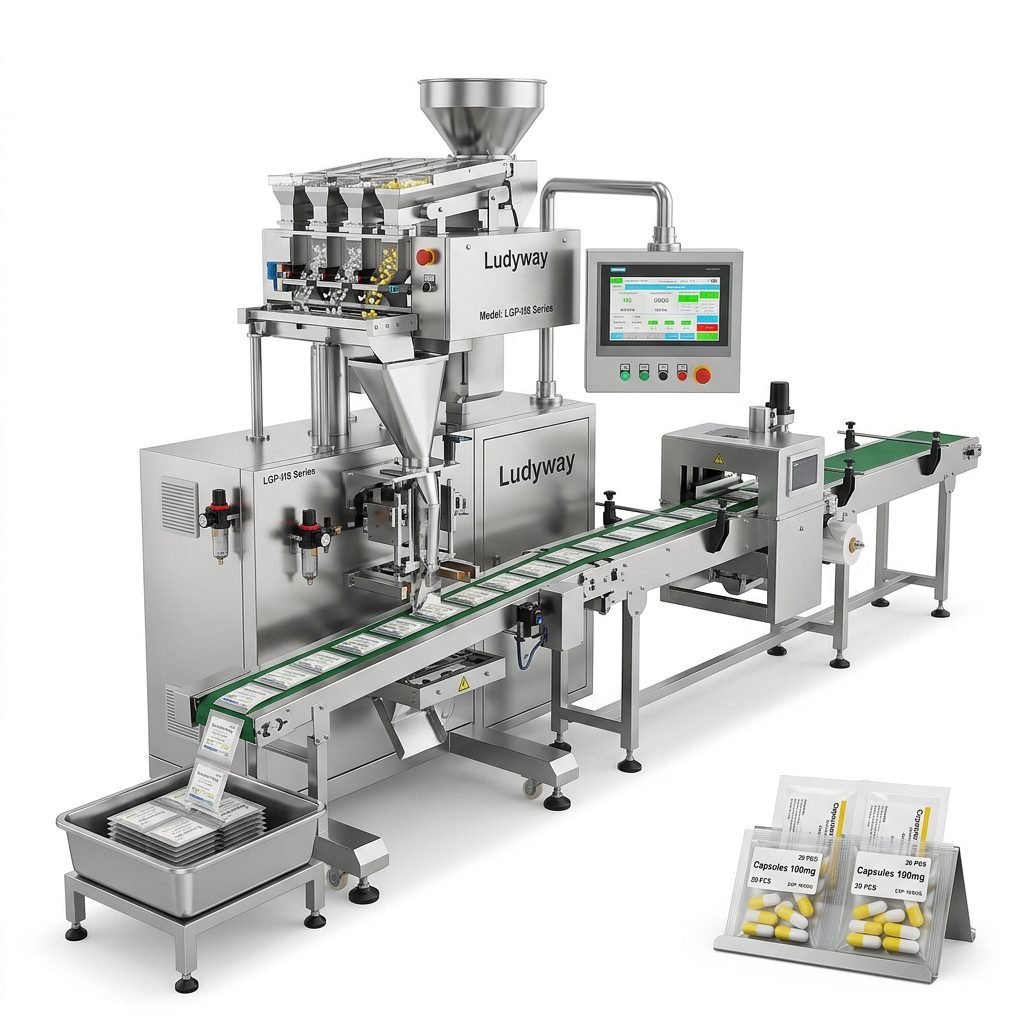
| Weighing & Filling Station | Ensures precise portion control before sealing | Multi-head weighers for granular or powder products |
| Labeling & Coding Unit | Applies date codes, batch numbers, and barcodes | Thermal transfer or inkjet systems depending on substrate |
| Inspection & Reject System | Detects seal defects, metal contaminants, or weight errors | Integrate checkweighers and metal detectors in-line |
Step 1: Define Your Production Goals and Capacity
Before purchasing any equipment, clearly define your target output, package sizes, and product characteristics. Are you packaging granular powders, liquid sachets, solid cuts of meat, or medical devices? Each product type requires different vacuum levels, bag materials, and sealing temperatures. A realistic capacity target — measured in packages per minute (ppm) — will guide the entire line configuration.
- Low-volume artisan producers: 5–15 ppm, single-chamber batch systems
- Mid-scale regional packagers: 20–40 ppm, double-chamber or rotary systems
- High-growth co-packers: 50+ ppm, automated multi-lane vacuum lines
Step 2: Evaluate Facility and Utility Requirements
Vacuum packaging equipment demands specific electrical, pneumatic, and spatial conditions. Most North American facilities operate on 208V or 480V three-phase power. Confirm voltage compatibility before ordering machinery. Compressed air requirements typically range from 6 to 8 bar, and clean, dry air is essential to prevent contamination. Floor space allocation should account for material inflow, operator walkways, and maintenance access per PMMI packaging industry standards.
Step 3: Choose the Right Vacuum Packaging Machine
The market offers several machine types, each suited to different applications. Here is a comparison to help narrow your search:
- Nozzle Vacuum Machines: Ideal for large bags and bulk solids; lower initial investment but slower cycle times
- Chamber Vacuum Machines: Best for liquid-rich or moist products; consistent seal quality and versatile bag sizes
- Thermoforming Vacuum Machines: Form, fill, and seal in one continuous process; high throughput for retail-ready packs
- Tray Sealing Machines: Popular for fresh proteins and ready meals; modified atmosphere packaging (MAP) compatible
For small to medium operations, a double-chamber vacuum machine often provides the best balance of cost, flexibility, and output. Many North American businesses also source high-quality packaging machinery from global manufacturers to access advanced features while managing capital expenditure.
Step 4: Integrate Ancillary Equipment for a Complete Line
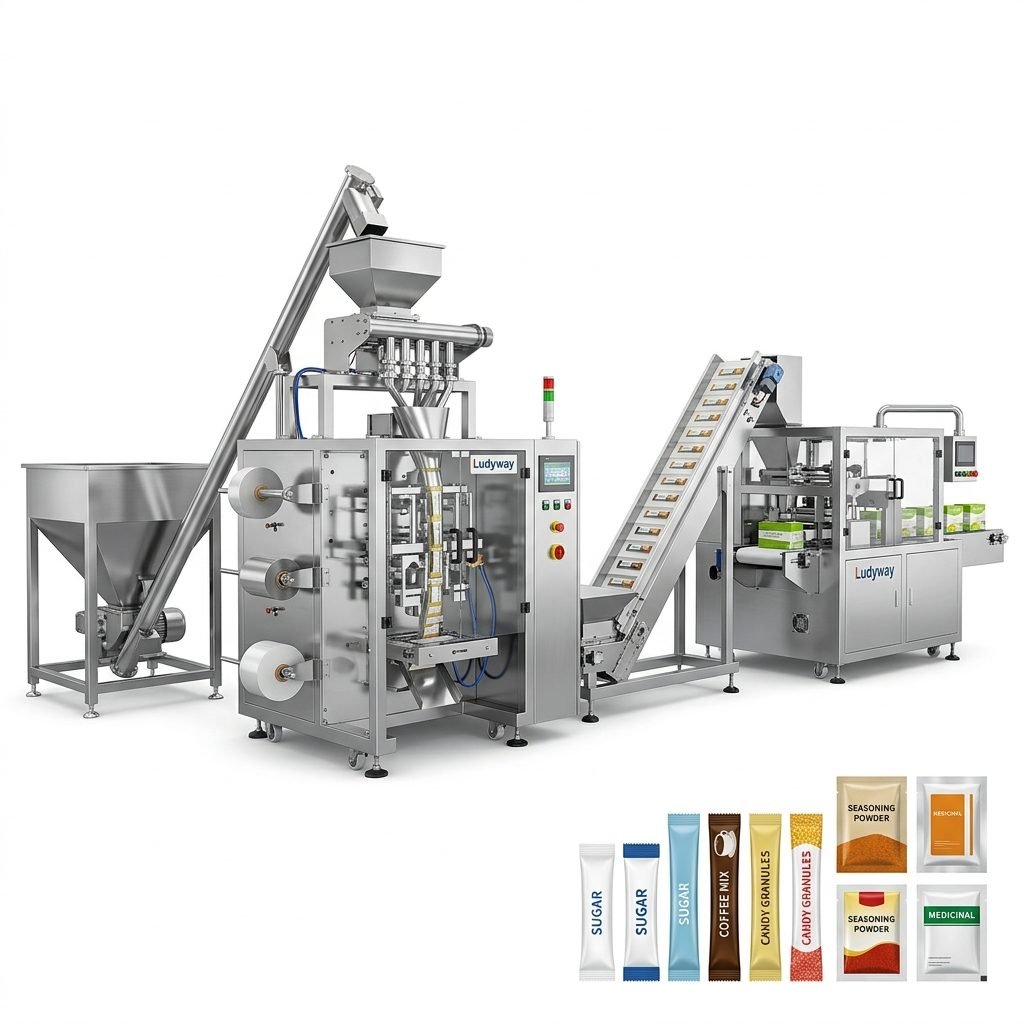
A standalone vacuum machine alone does not constitute a production line. Integrating supporting equipment dramatically improves efficiency. Consider adding:
Material Handling & Feeding Systems
Bucket elevators, inclined conveyors, and vibratory feeders ensure consistent product flow into the weighing and filling station. For powder and granule applications, vacuum conveying systems minimize dust and product loss.
Checkweighing & Metal Detection
Inline checkweighers verify package weight compliance, while metal detectors safeguard against physical contaminants. These are critical for FDA food contact substance compliance and retailer audit requirements.
Cartoning & Palletizing
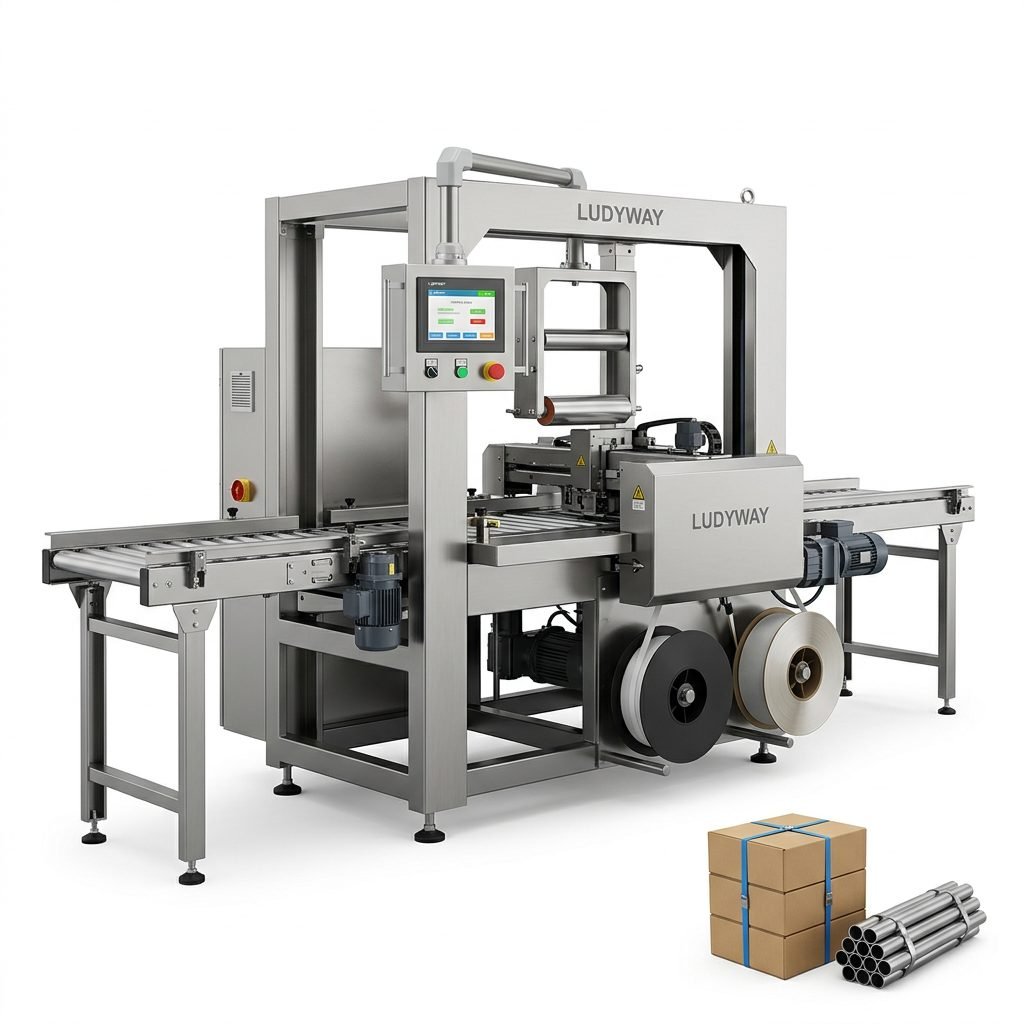
Automated carton erectors, case packers, and robotic palletizers reduce manual labor and standardize case presentation for distribution centers across the U.S. and Canada.
Step 5: Navigate North American Regulatory Compliance
Regulatory compliance is non-negotiable for North American vacuum packaging operations. Key frameworks include:
- FDA 21 CFR Part 110: Good manufacturing practices for food contact surfaces and sanitation
- CFIA Safe Food for Canadians Regulations: Mandatory for any product entering the Canadian market
- ISO 11607: Standards for terminally sterilized medical device packaging — relevant for pharma and healthcare sectors
- UL and CSA Certification: Electrical safety certifications required by most North American facility insurers
Work with equipment suppliers who provide documentation packages including IQ/OQ protocols, material certifications, and preventive maintenance schedules. These documents will expedite your facility’s internal audit and customer qualification processes.
Step 6: Installation, Training, and Ramp-Up
Proper installation sets the foundation for long-term reliability. Schedule a factory acceptance test (FAT) before shipment and a site acceptance test (SAT) after installation. Allocate at least two weeks for operator training, covering:
- Machine startup, shutdown, and emergency procedures
- Film threading, seal temperature calibration, and vacuum level adjustment
- Cleaning-in-place (CIP) and sanitation workflows
- Basic troubleshooting for common faults such as incomplete seals or vacuum leaks
- Changeover procedures for different bag sizes and materials
Step 7: Maintenance and Continuous Improvement
A structured maintenance program prevents unplanned downtime, which is particularly costly for small production lines with limited backup capacity. Implement the following schedule:
| Frequency | Maintenance Tasks |
|---|---|
| Daily | Clean sealing bars, inspect vacuum pump oil level, check air filter |
| Weekly | Lubricate moving parts, verify sensor calibration, inspect electrical connections |
| Monthly | Replace vacuum pump oil, test emergency stops, deep-clean conveyor belts |
| Quarterly | Full system audit, software updates, seal bar replacement if wear exceeds tolerance |
Common Challenges and How to Overcome Them
Even well-planned lines encounter operational hurdles. Below are frequent issues and practical solutions:
- Inconsistent Vacuum Levels: Check for leaks in hoses or gasket deterioration; recalibrate vacuum sensors quarterly
- Seal Failure: Verify seal bar temperature uniformity; contamination on seal area is the most common cause — ensure product is not spilling into the seal zone
- Film Wrinkling: Adjust film tension and tracking guides; wrinkled packages can indicate misaligned rollers
- Low Throughput: Review cycle time settings; sometimes a small reduction in vacuum time yields significant throughput gains without compromising seal quality
Sourcing Equipment: Domestic vs. International Suppliers
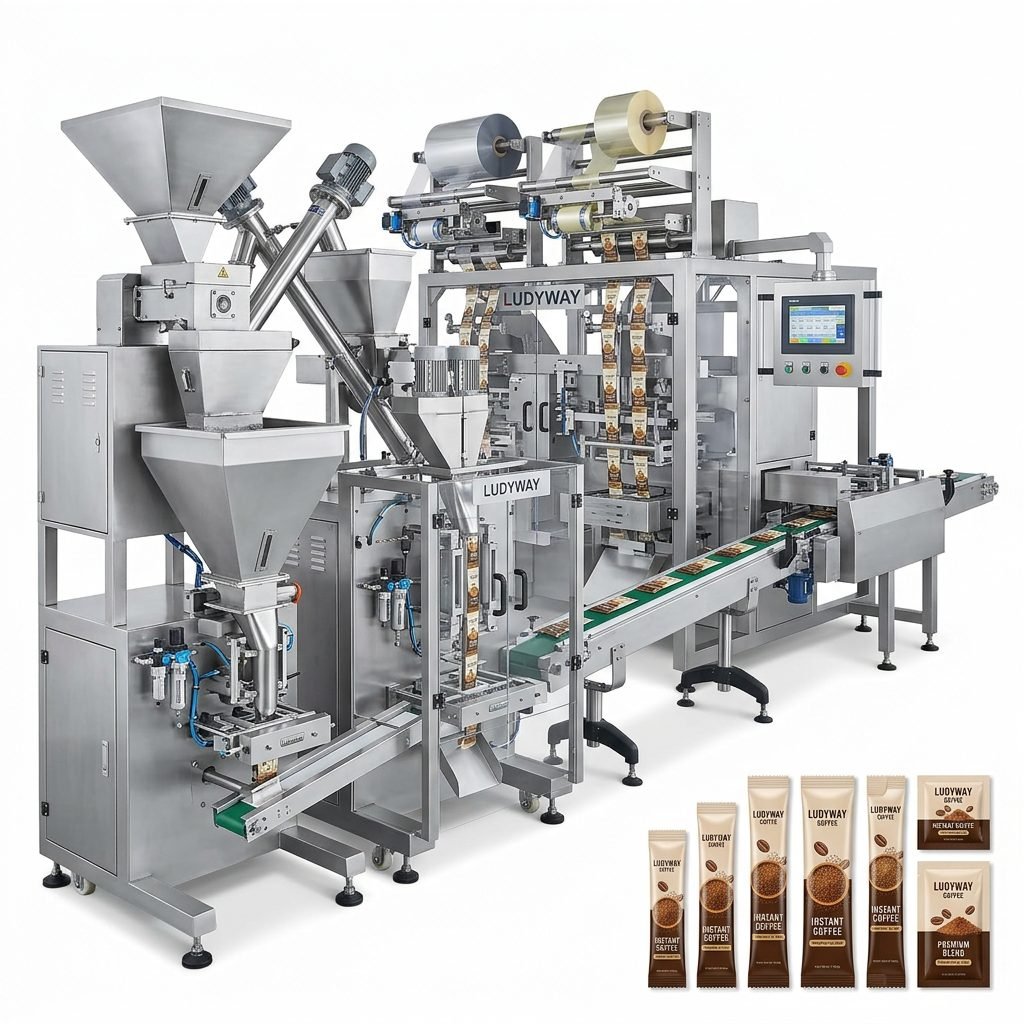
North American buyers increasingly evaluate both domestic and international equipment sources. Domestic suppliers offer proximity for service and spare parts, often at a premium. International manufacturers — particularly those with established export experience — can deliver high-quality machinery at competitive price points. When evaluating an international supplier, verify their compliance with flexible packaging standards, North American voltage configurations, and availability of local service support. One notable manufacturer in this space is Ludyway, which specializes in advanced packaging equipment and turnkey production solutions for the food, pharmaceutical, and health industries. With a modern 20,000㎡ manufacturing facility and over 50 intelligent packaging machine models, the company serves customers in more than 100 countries and regions — including a growing base across North America.
Budgeting and ROI Considerations
A small vacuum packaging line in North America typically requires an investment ranging from $50,000 to $350,000, depending on automation level and throughput. Key cost factors include:
- Machine type and chamber configuration
- Ancillary equipment — conveyors, weighers, printers, inspection systems
- Installation, training, and freight costs
- Facility modifications — electrical upgrades, compressed air lines, ventilation
- Initial consumables inventory — vacuum bags, films, spare parts kits
Most small to mid-sized operations achieve payback within 12 to 24 months through reduced labor, lower material waste, and the ability to command premium pricing for vacuum-sealed products. For the latest market data on packaging machinery investment trends, consult the PMMI business intelligence reports.
Future-Proofing Your Vacuum Packaging Line
As your business grows, your packaging line should scale with minimal disruption. When selecting equipment, prioritize:
- Modular designs that allow additional lanes or stations to be added later
- IoT-enabled controls for remote monitoring, predictive maintenance, and OEE tracking
- Multi-format capability — machines that handle both vacuum and MAP applications provide flexibility as product lines evolve
- Energy-efficient vacuum pumps — variable-speed drive pumps reduce electricity consumption by up to 30% compared to fixed-speed models
Final Checklist Before Launching Your Line
Use this checklist to ensure your small vacuum packaging production line is ready for commercial operation:
- All equipment installed, leveled, and anchored per manufacturer specifications
- Electrical connections verified by a licensed electrician; phase rotation confirmed
- Compressed air supply tested for pressure stability and moisture content
- SOPs documented for startup, operation, cleaning, and emergency shutdown
- Operators trained and assessed on all core tasks; training records maintained
- Initial production run validated; seal integrity and vacuum levels tested
- Regulatory documentation compiled — FDA registration, CFIA permits, material certifications
- Spare parts inventory stocked — seal bars, gaskets, filters, vacuum pump oil
- Service contract or local technical support arranged for breakdown response
- Continuous improvement plan established with monthly KPI reviews
Setting up a small vacuum packaging machine production line in North America requires careful planning, but the rewards — improved product quality, extended shelf life, and access to premium retail channels — make it a compelling investment. By following this guide and partnering with reliable packaging industry resources, you can build a line that meets today’s demands while adapting to tomorrow’s growth opportunities.