Expanding into international markets with a vacuum packaging machine production line requires strategic planning, technical precision, and a deep understanding of global compliance standards. Whether you are packaging food, pharmaceuticals, or industrial components, a well-designed line can dramatically extend product shelf life and improve operational efficiency.
Understanding Vacuum Packaging Technology for Export Markets
Vacuum packaging removes oxygen from the package prior to sealing, creating an anaerobic environment that inhibits the growth of aerobic bacteria and fungi. For manufacturers targeting global markets, this technology must meet varied regional standards, from FDA packaging requirements in the United States to ISO packaging standards recognized internationally.
The global vacuum packaging market continues to expand, driven by demand for extended shelf life and reduced food waste. Key sectors include processed meats, dairy products, ready-to-eat meals, and medical device packaging. Selecting the right machinery starts with understanding your target market’s specific requirements.
Key Components of a Vacuum Packaging Production Line
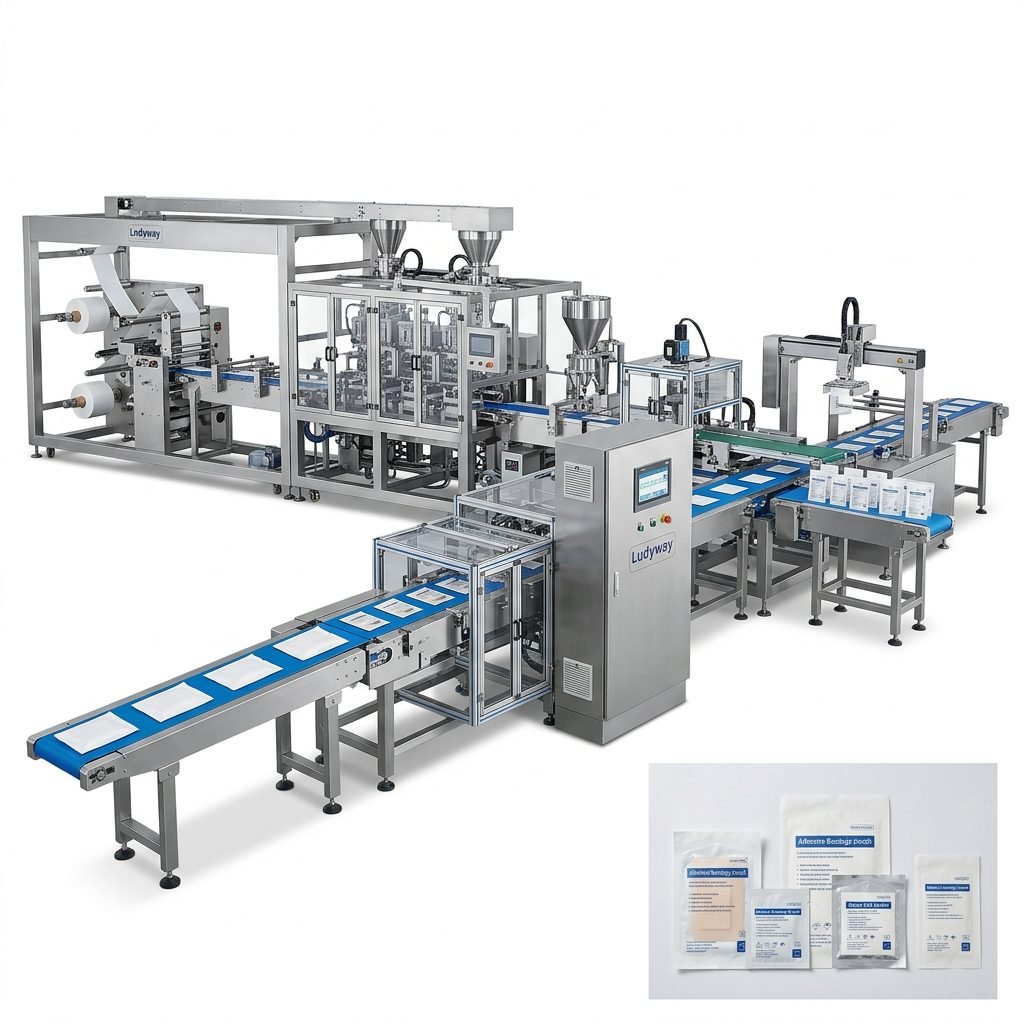
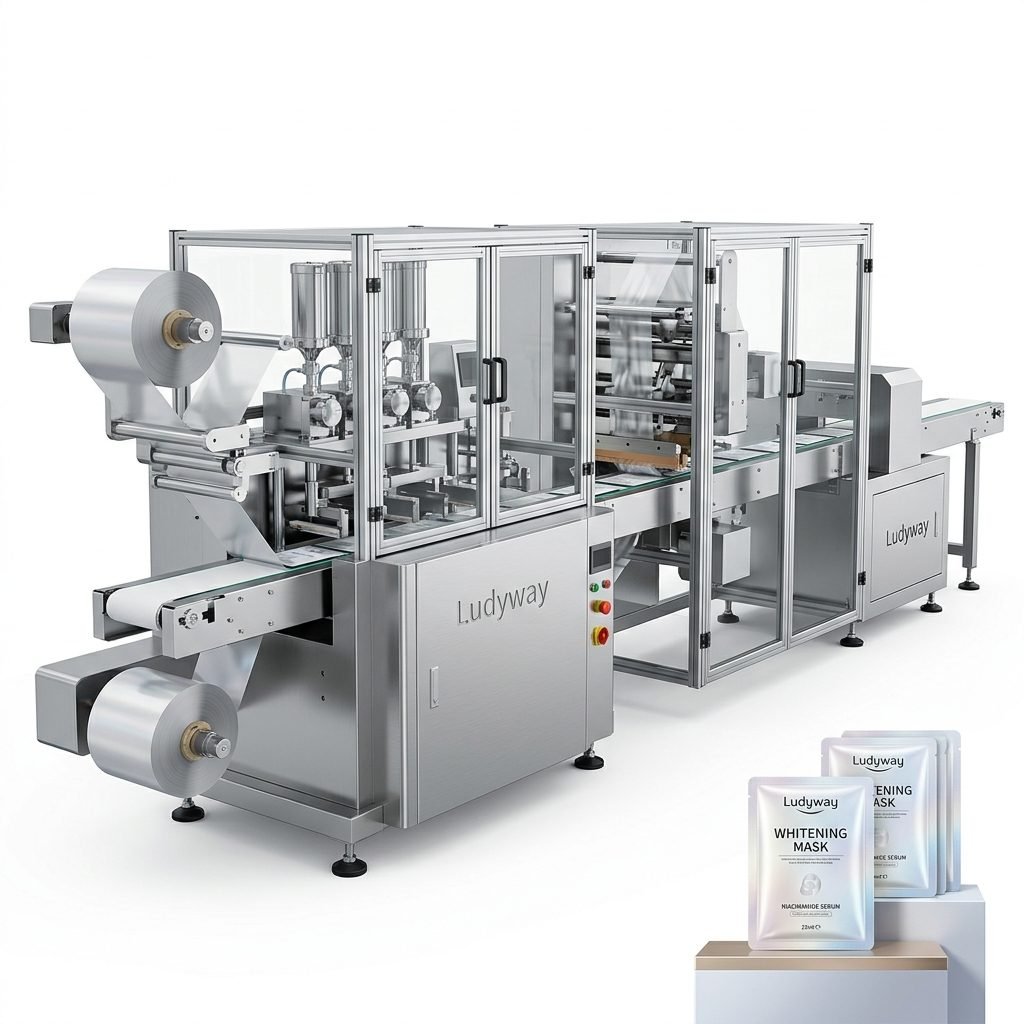
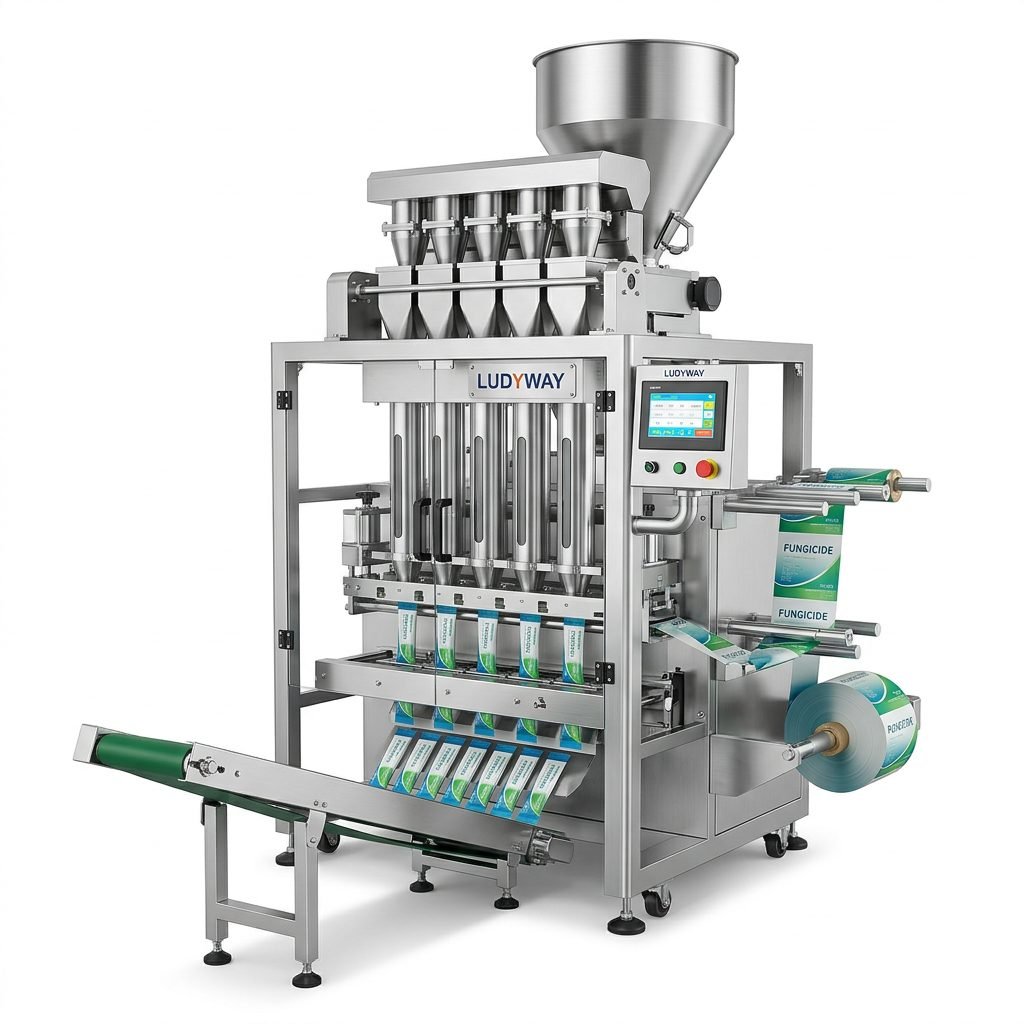
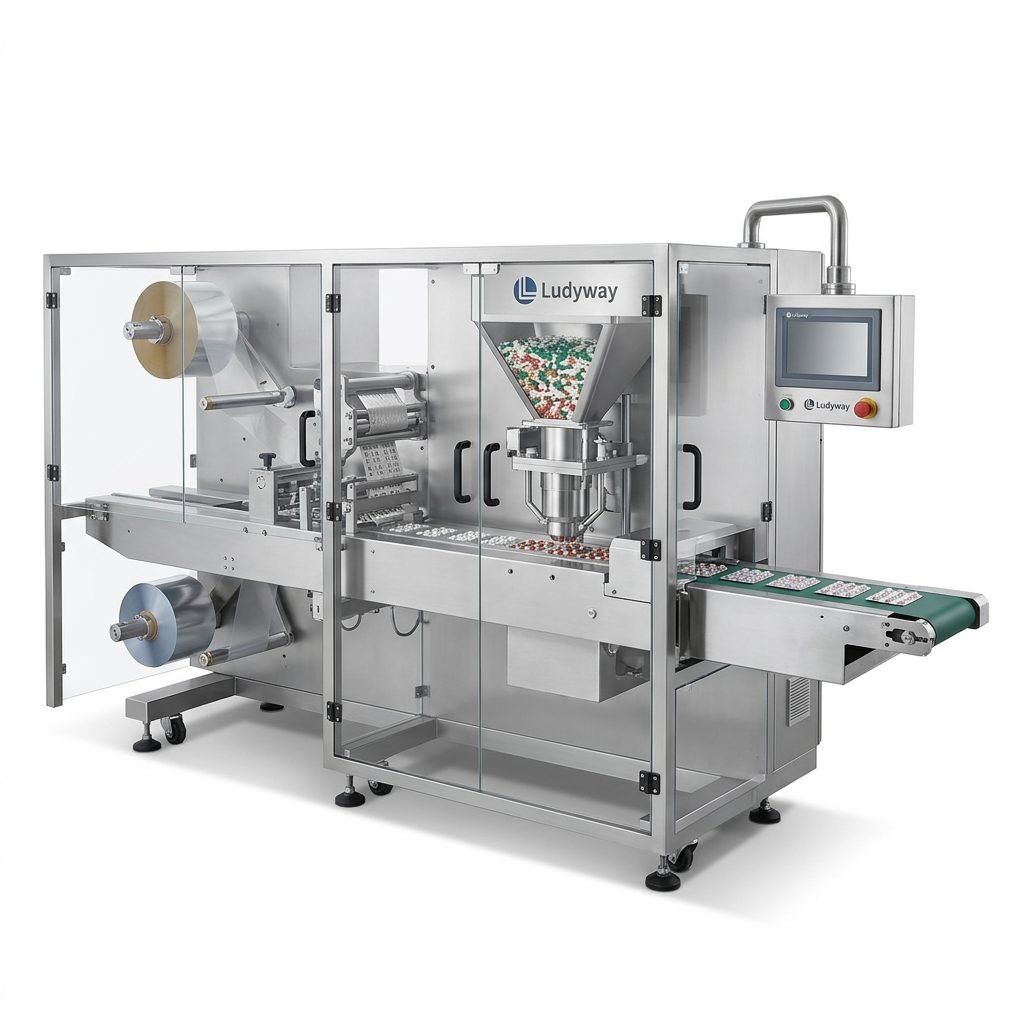
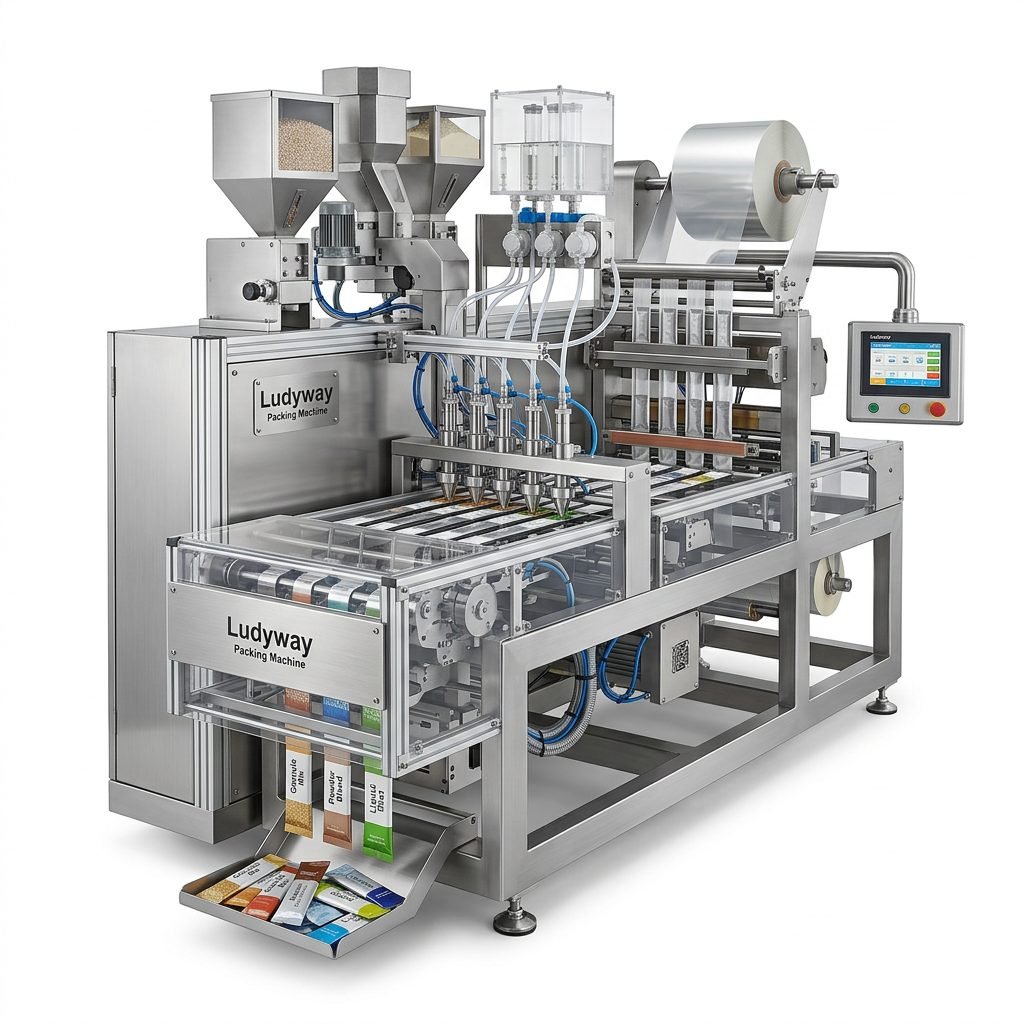
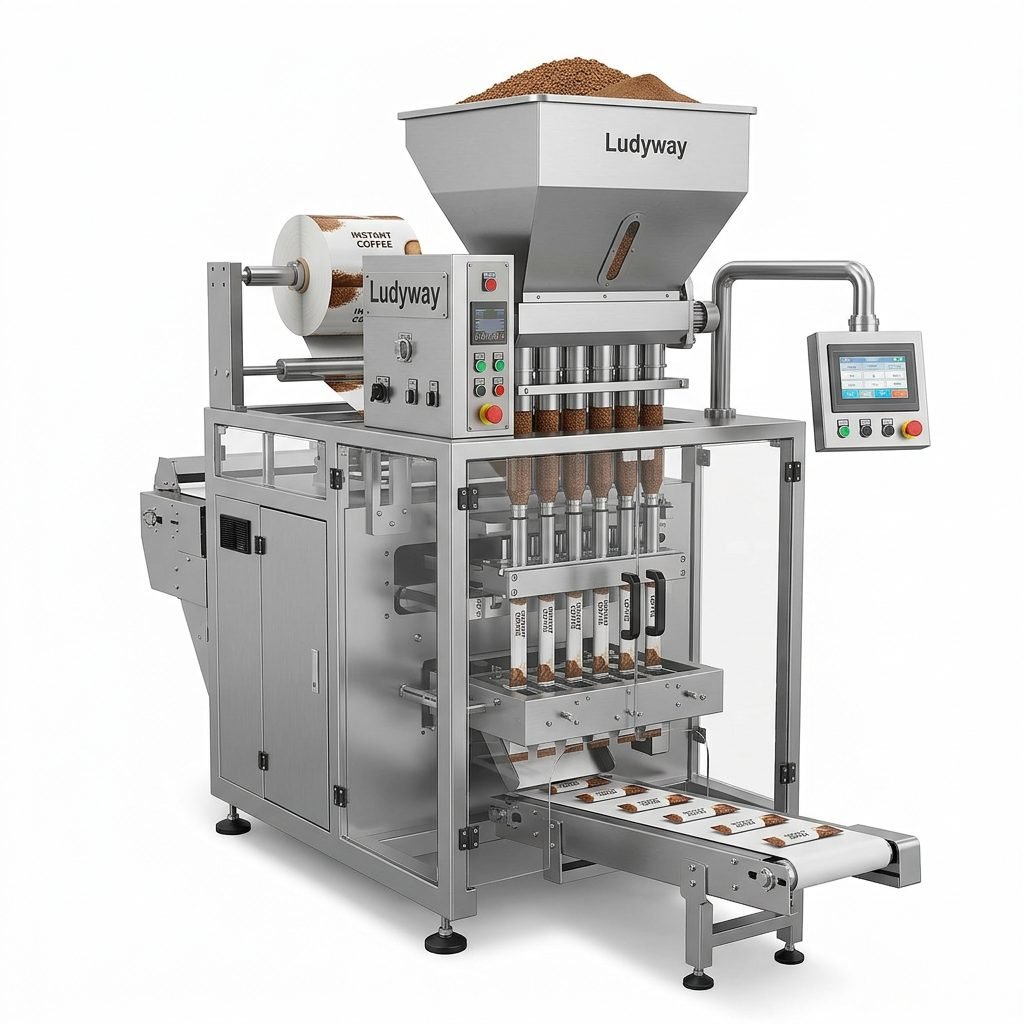
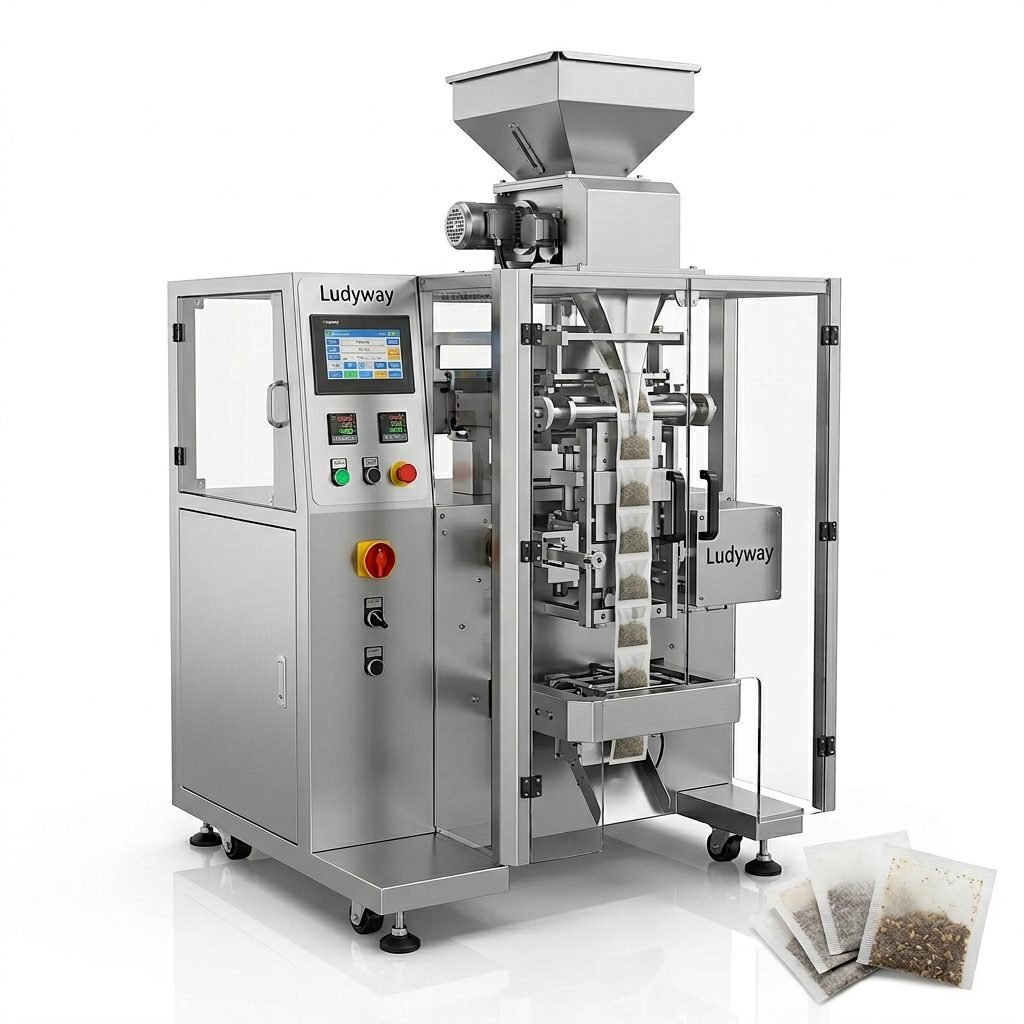
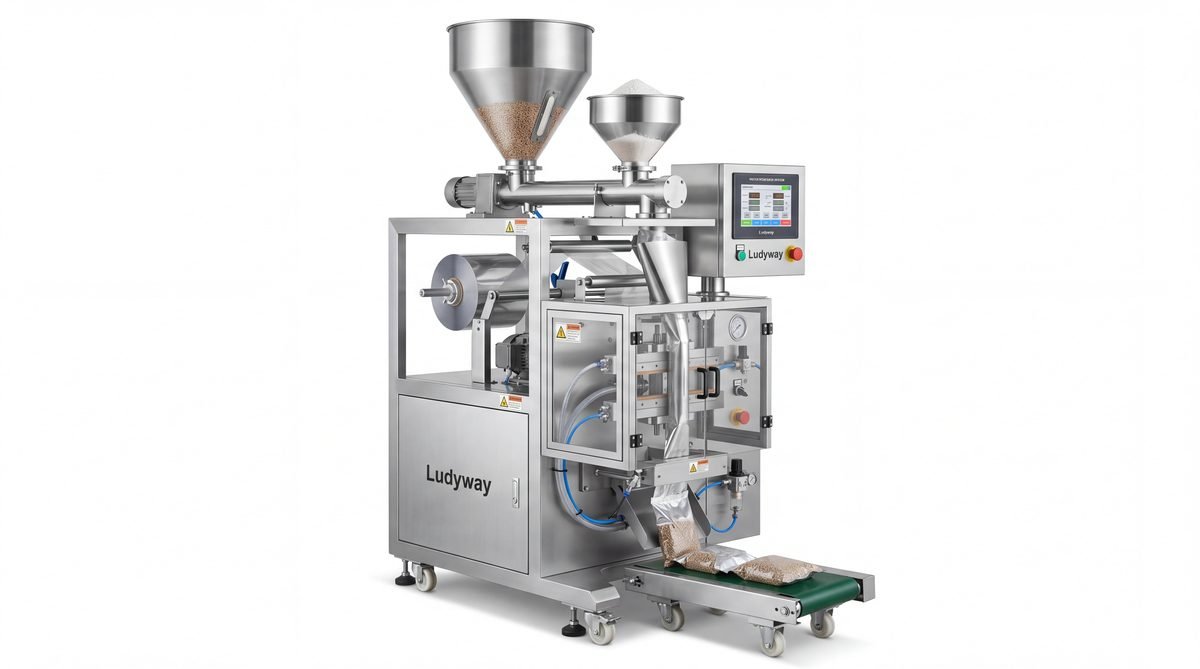
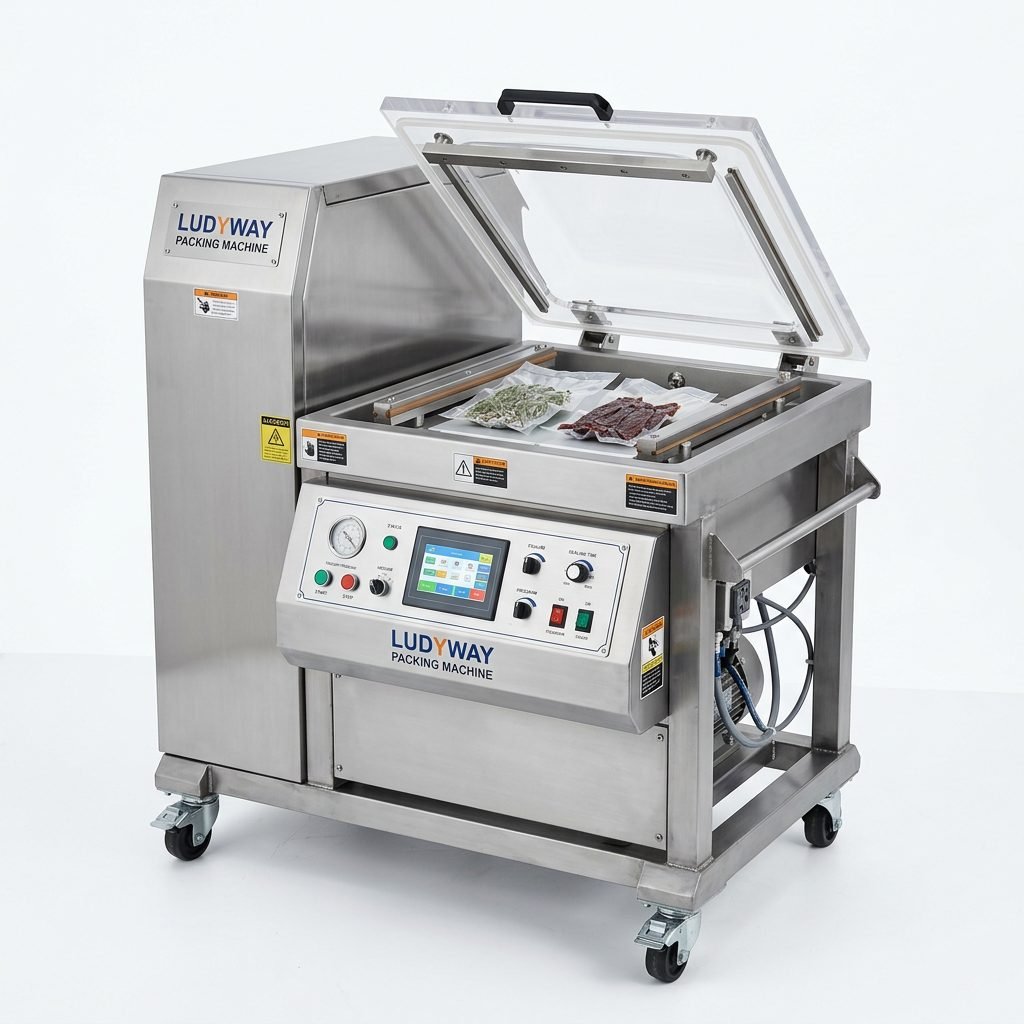
A complete vacuum packaging machine production line consists of several integrated modules. Each component plays a critical role in maintaining throughput and product integrity. Understanding these elements helps you make informed procurement decisions when sourcing equipment for international operations.
- Vacuum Chamber or Nozzle System – The core mechanism that extracts air from the package. Chamber machines are ideal for solid products, while nozzle systems work well for delicate or liquid items.
- Sealing Mechanism – Heat-sealing bars create an airtight closure. Impulse sealing technology ensures consistent results across varying film thicknesses.
- Conveyor and Feeding System – Automated conveyor systems synchronize product flow, reducing manual handling and improving line speed.
- Gas Flushing Module – Modified atmosphere packaging (MAP) replaces oxygen with inert gases like nitrogen or CO₂, further preserving product freshness.
- Control and Monitoring Systems – PLC-based controls with HMI touchscreens allow operators to adjust parameters for different products and packaging materials.
- Quality Inspection Station – Checkweighers, metal detectors, and vision systems ensure each package meets weight and seal integrity standards.
Selecting Equipment Based on Product Type and Market Requirements
Different products demand different vacuum packaging approaches. The table below outlines common product categories and the recommended machine configurations for optimal results in international markets.
| Product Category | Recommended Machine Type | Key Features for Global Markets |
|---|---|---|
| Fresh Meat & Poultry | Double Chamber Vacuum Machine | High vacuum pressure, MAP capability, FDA-compliant materials |
| Processed Foods | Continuous Belt Vacuum Machine | High throughput, consistent seal integrity, CE certification |
| Pharmaceutical Products | Nozzle Vacuum with Sterile Chamber | ISO 11607 compliance, validation documentation, cleanroom compatibility |
| Industrial Components | External Vacuum Sealer | Heavy-duty construction, corrosion-resistant seals, large chamber options |
| Coffee & Dry Goods | Single Chamber with Gas Flush | Nitrogen flushing, degassing valves, aroma preservation |
Compliance and Certification Considerations
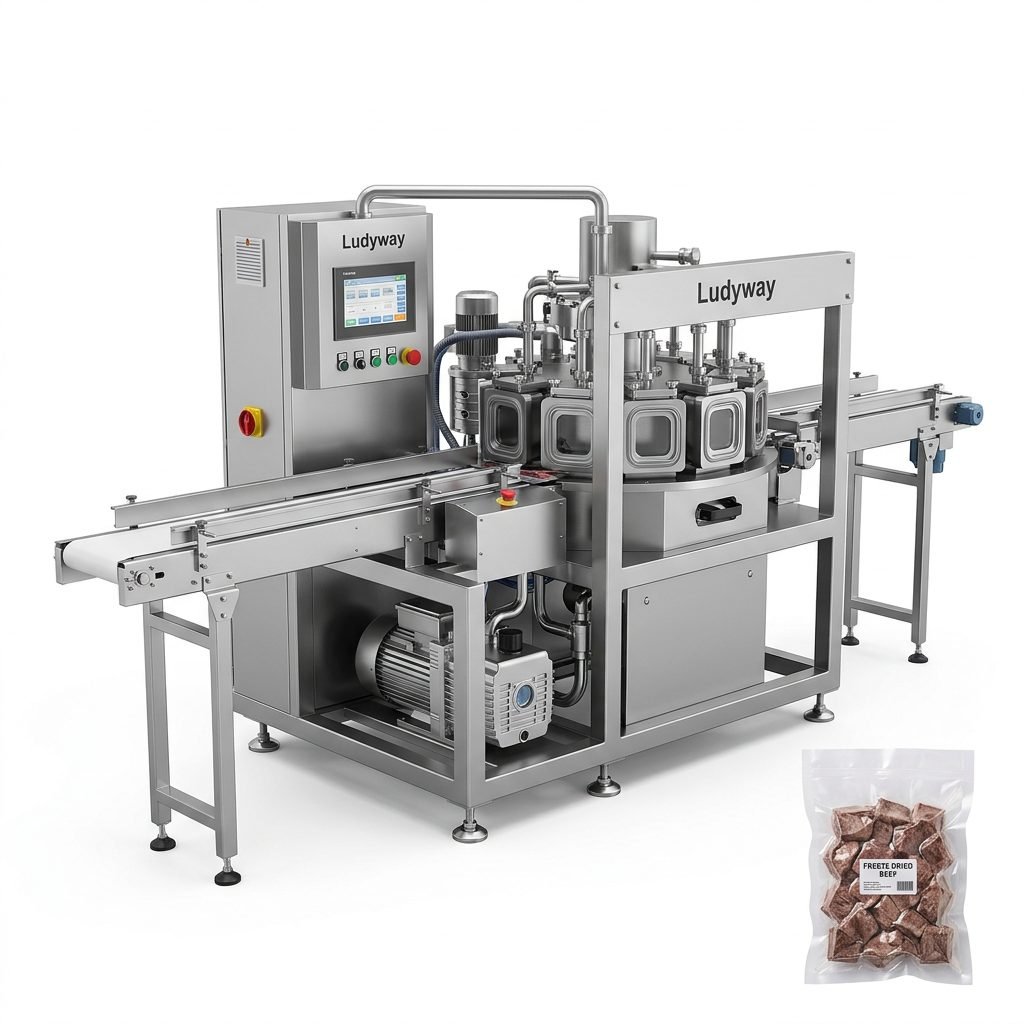
When setting up a vacuum packaging line for global distribution, regulatory compliance cannot be an afterthought. Different regions enforce distinct standards that directly impact equipment design, material selection, and operational procedures.
- CE Marking (European Union): Mandatory for machinery sold in the EU, covering safety, health, and environmental protection requirements under the Machinery Directive.
- FDA Compliance (United States): Food contact materials must meet 21 CFR regulations; pharmaceutical packaging requires adherence to current Good Manufacturing Practices (cGMP).
- ISO 11607 (Global): Specifies requirements for materials, sterile barrier systems, and packaging systems for terminally sterilized medical devices.
- HACCP Integration: Equipment should support Hazard Analysis Critical Control Point protocols, particularly for food-grade vacuum packaging lines.
Optimizing Line Layout for Export Production Efficiency
The physical arrangement of your vacuum packaging line significantly impacts throughput and labor costs. For manufacturers aiming at international competitiveness, line layout should prioritize flow efficiency and scalability. Consider these layout principles when planning your facility:
A U-shaped configuration minimizes operator movement and allows one person to manage both loading and unloading stations. For high-volume operations, a linear inline layout with automated infeed and outfeed conveyors maximizes throughput. Always leave space for future expansion — global demand patterns shift, and your production capacity should adapt accordingly.
Integration with Upstream and Downstream Systems
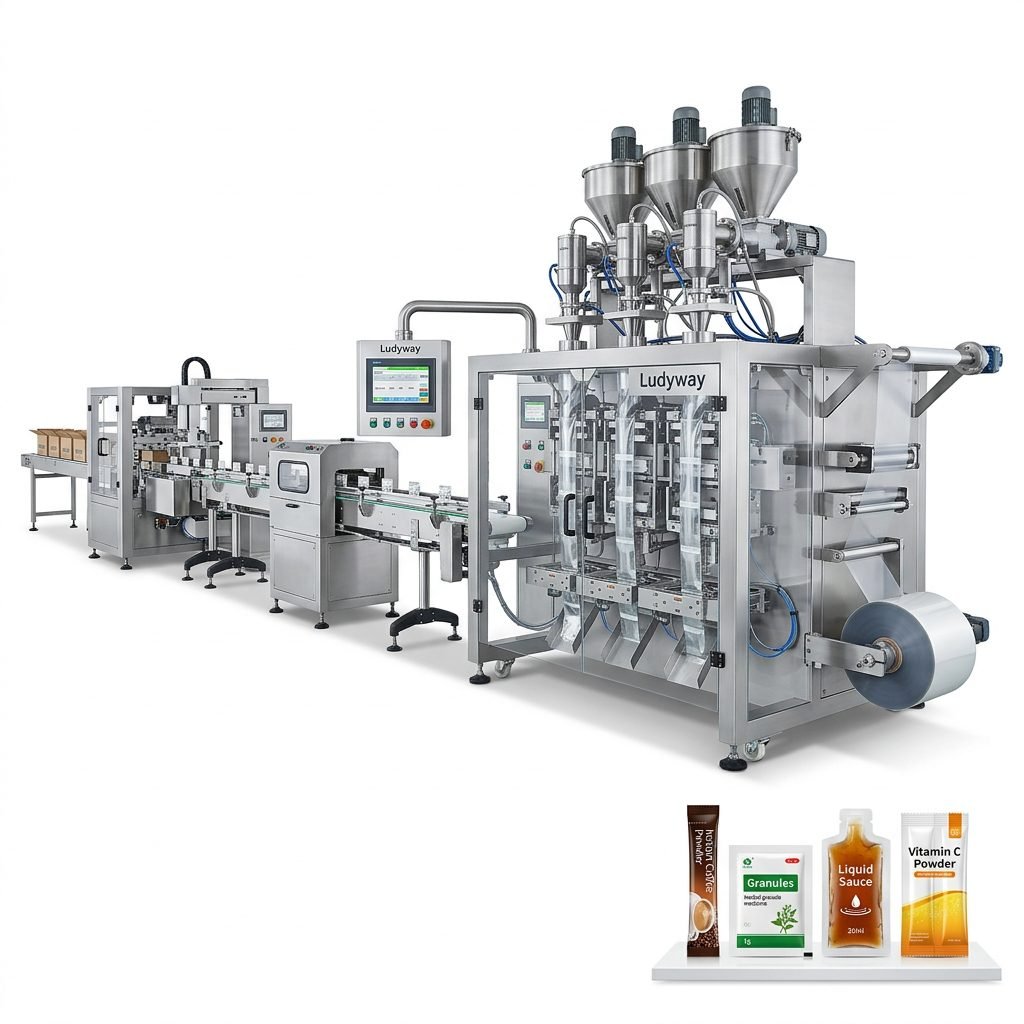
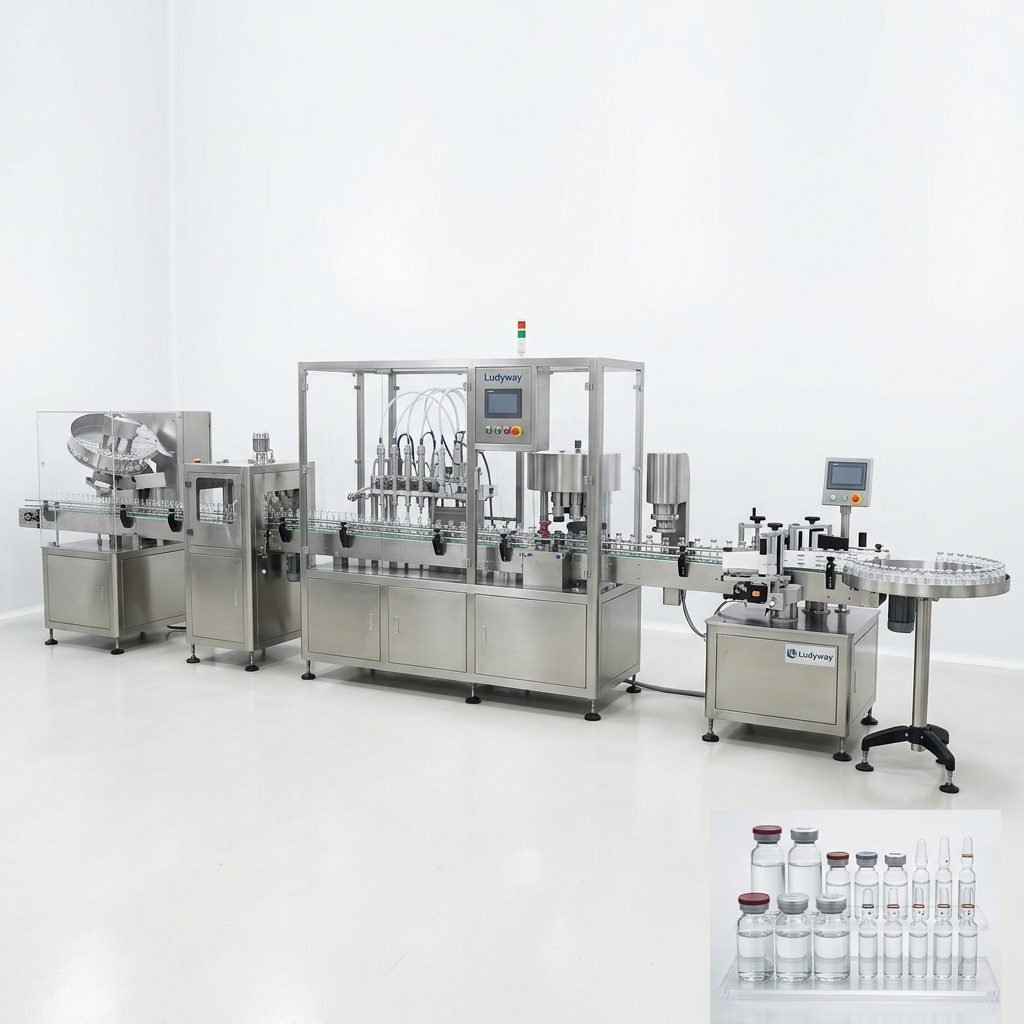
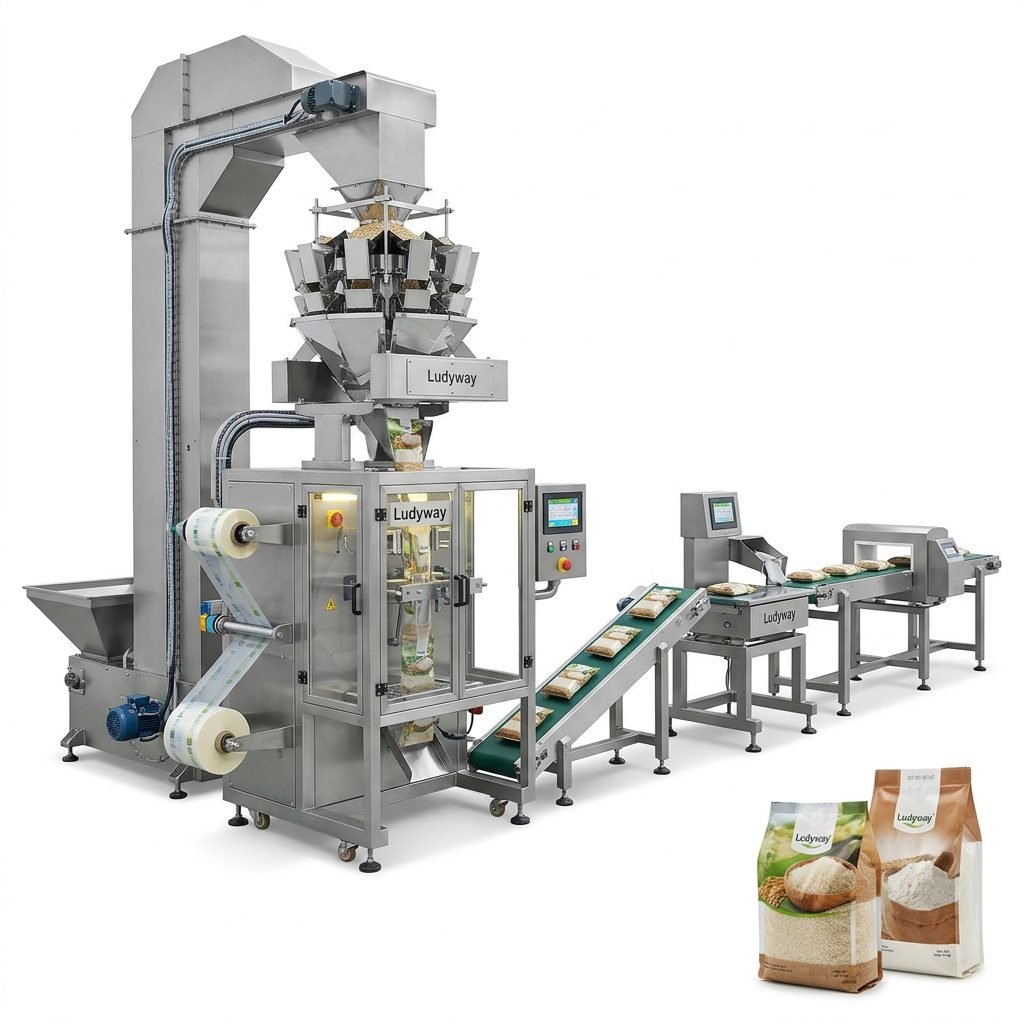
A truly effective vacuum packaging production line does not operate in isolation. Integration with filling systems, labeling equipment, cartoning machines, and palletizing solutions creates a seamless workflow. For companies serving global customers, this integration reduces lead times and ensures consistent package quality across batches.
Modern packaging lines increasingly incorporate IoT sensors and cloud-based monitoring, enabling real-time performance tracking across multiple production sites. This connectivity is particularly valuable for manufacturers managing packaging operations across different countries and time zones.
Material Selection for International Distribution Channels
Vacuum packaging films must withstand the rigors of international shipping while maintaining barrier properties. The choice of material depends on product sensitivity, shelf life requirements, and destination market regulations.
| Material Type | Barrier Properties | Best Application |
|---|---|---|
| PA/PE (Polyamide/Polyethylene) | High oxygen barrier, good puncture resistance | Fresh meat, cheese, processed foods |
| EVOH Multilayer | Superior oxygen barrier, moisture resistant | Coffee, nuts, pharmaceutical products |
| Aluminum Foil Laminate | Complete light and gas barrier | Medical devices, sensitive electronics |
| Biodegradable PLA Films | Moderate barrier, compostable | EU markets with strict sustainability mandates |
Automation Levels and Labor Considerations
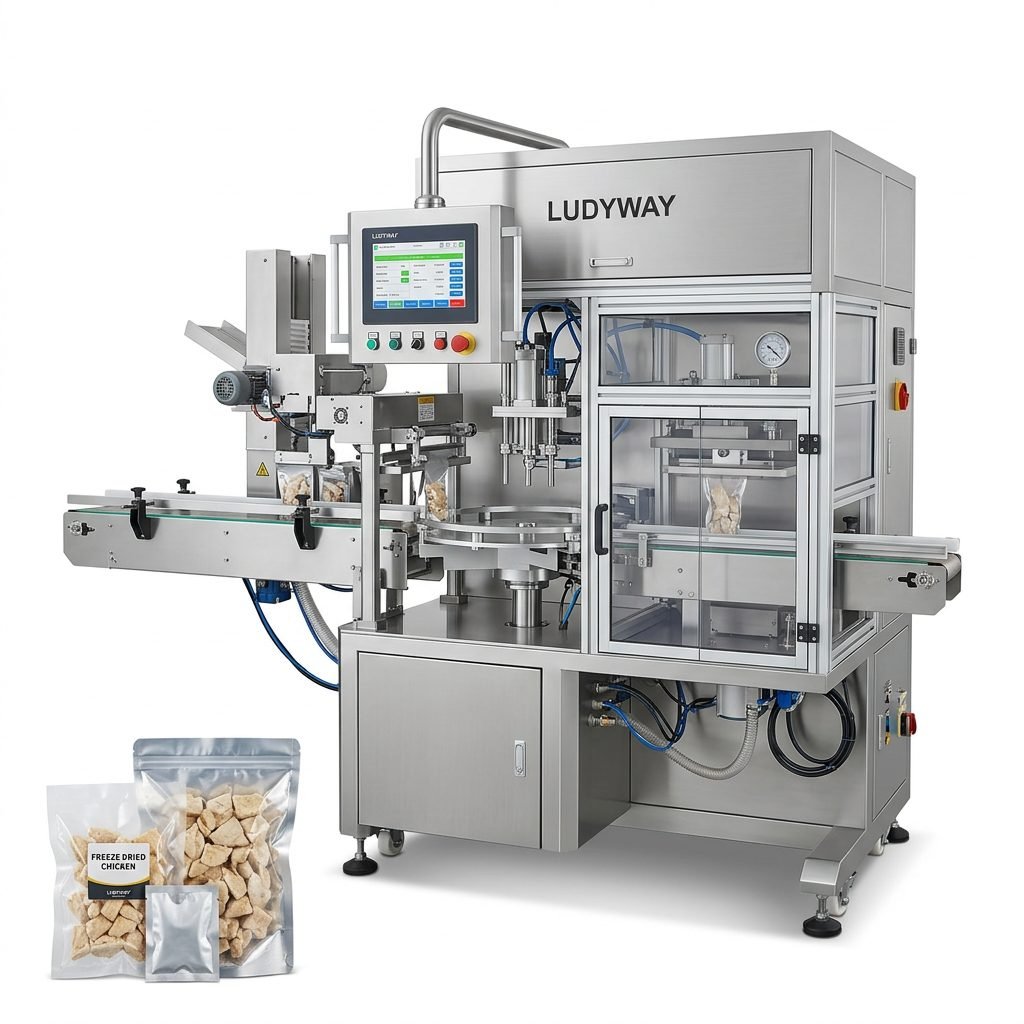
The degree of automation in your vacuum packaging line should align with your target market’s labor costs and production volume expectations. Fully automated systems reduce dependency on skilled labor and deliver consistent output — critical for markets with high wage structures. Semi-automatic configurations offer flexibility for smaller batch production and emerging market operations.
Key automation features to evaluate include automatic film feeding, programmable recipe management, self-diagnostic systems, and robotic pick-and-place integration. These capabilities not only improve efficiency but also enhance traceability — a growing requirement in regulated global markets.
Energy Efficiency and Sustainability Compliance
European and North American markets increasingly mandate energy-efficient equipment and sustainable packaging practices. Modern vacuum packaging machines incorporate servo-driven motors, intelligent standby modes, and optimized heating elements that reduce power consumption by up to 30% compared to older pneumatic systems.
Sustainability considerations extend beyond energy use. Equipment designed for EU packaging waste regulations should accommodate recyclable and mono-material films, supporting circular economy goals while maintaining packaging performance.
Testing and Validation for Export Readiness
Before shipping products internationally, your vacuum packaging line must undergo rigorous validation. This process verifies that the equipment consistently produces packages that meet seal strength, residual oxygen, and integrity standards across all operating conditions.
- Seal Strength Testing: Measures the force required to separate sealed layers, ensuring packages withstand transportation stresses.
- Burst Testing: Evaluates package resistance to internal pressure changes during altitude variations in air freight.
- Dye Penetration Testing: Detects microscopic leaks in seals that could compromise product sterility or freshness.
- Residual Oxygen Analysis: Confirms that vacuum levels meet specified thresholds for product shelf life requirements.
- Accelerated Aging Studies: Simulates long-term storage conditions to validate packaging performance over the product’s intended shelf life.
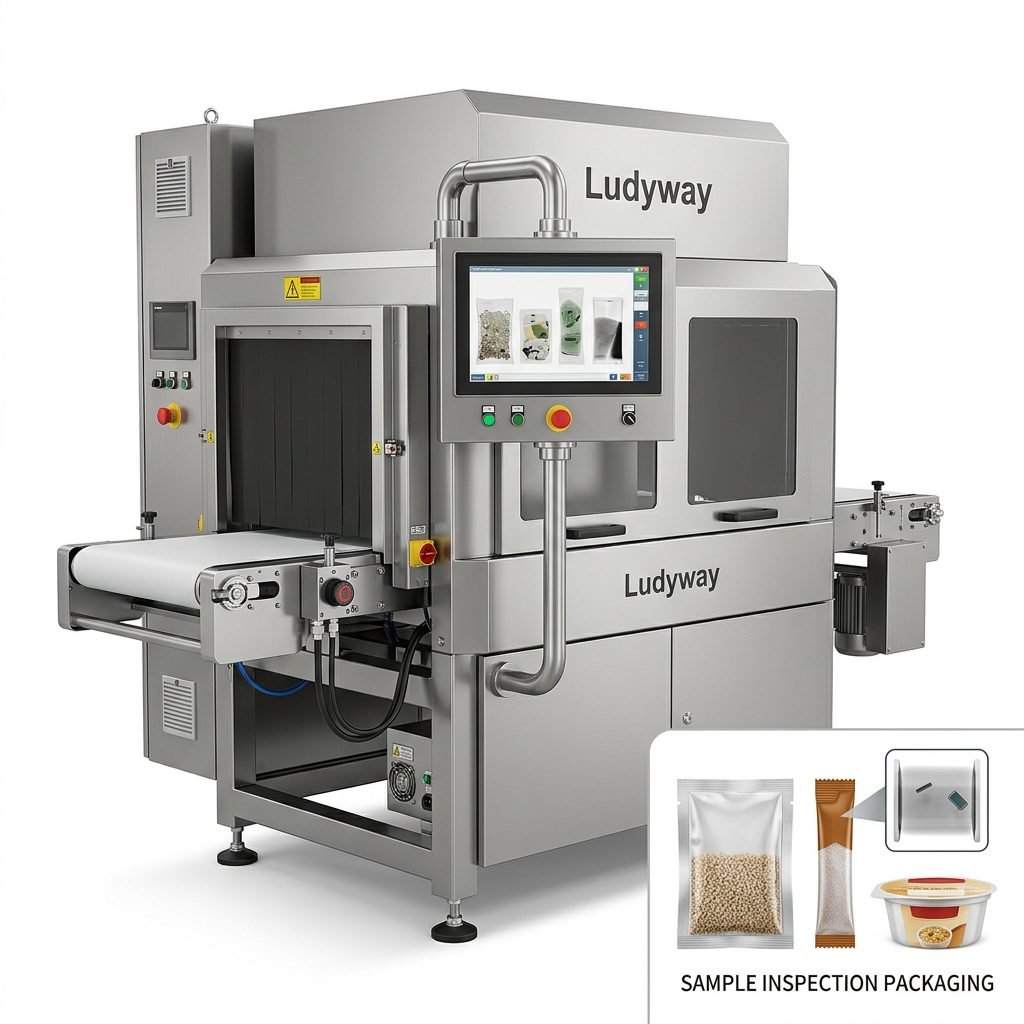
Partnering with Experienced Equipment Manufacturers
Selecting the right equipment partner is crucial for success in global markets. Look for manufacturers with proven export experience, international certifications, and comprehensive after-sales support. The supplier should offer installation and training services that bridge language and cultural differences, ensuring your team can operate and maintain the line effectively regardless of location.
As a leading packaging machine manufacturer, Ludyway has supported clients in over 100 countries with customized vacuum packaging solutions that meet diverse regulatory requirements. With a modern 20,000㎡ manufacturing facility and more than 50 intelligent packaging machine models, the company provides turnkey production lines engineered for international markets.
After-Sales Support and Spare Parts Availability
Global operations demand reliable access to spare parts and technical support. Establish clear service level agreements covering response times, remote diagnostics, and on-site technician availability. Many leading manufacturers now offer cloud-connected equipment that enables predictive maintenance, reducing unplanned downtime and protecting your export commitments.
Cost Analysis and ROI Projections for Export Operations
Investing in a vacuum packaging machine production line for global markets requires careful financial planning. Beyond the initial equipment cost, factor in installation, training, validation, and ongoing maintenance expenses. The return on investment typically comes from reduced product waste, extended shelf life enabling wider distribution, and premium pricing opportunities in markets that value extended freshness.
For manufacturers targeting both developed and emerging markets, modular line designs offer the flexibility to scale capacity incrementally. This approach reduces upfront capital requirements while maintaining the ability to expand as market demand grows. A well-planned vacuum packaging line should deliver positive ROI within 18 to 36 months, depending on production volume and market pricing strategies.
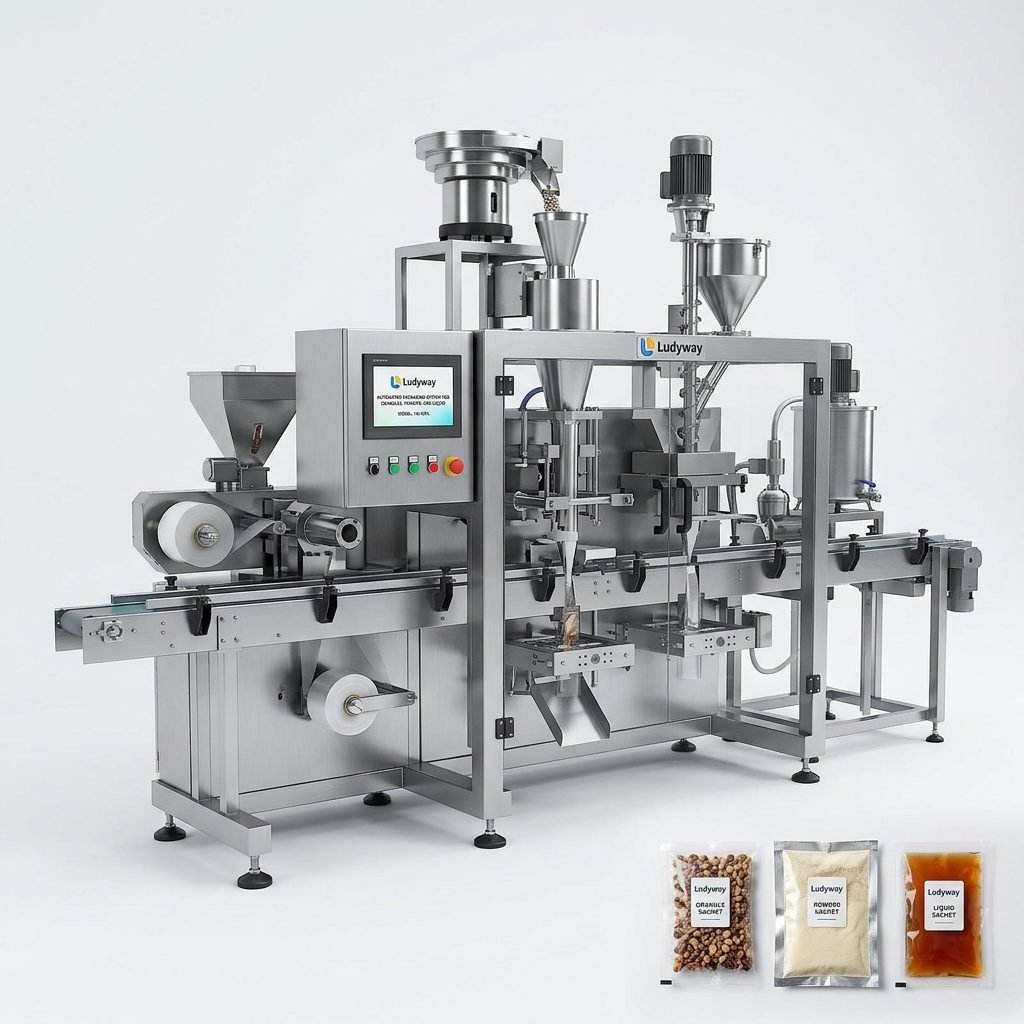
Future Trends in Global Vacuum Packaging
The vacuum packaging industry continues to evolve with advancements in smart packaging, active packaging technologies, and sustainable materials. Manufacturers targeting international markets should stay informed about trends such as intelligent indicators that monitor package integrity, antimicrobial films that extend shelf life beyond traditional vacuum methods, and fully recyclable barrier materials that meet tightening environmental regulations worldwide.
Investing in flexible, upgradeable equipment positions your operation to adapt to these changes without complete line replacement. This forward-thinking approach is essential for maintaining competitiveness in the dynamic global packaging landscape. For further insights, explore resources from flexible packaging industry associations and stay connected with international packaging trade exhibitions where the latest technologies are showcased.