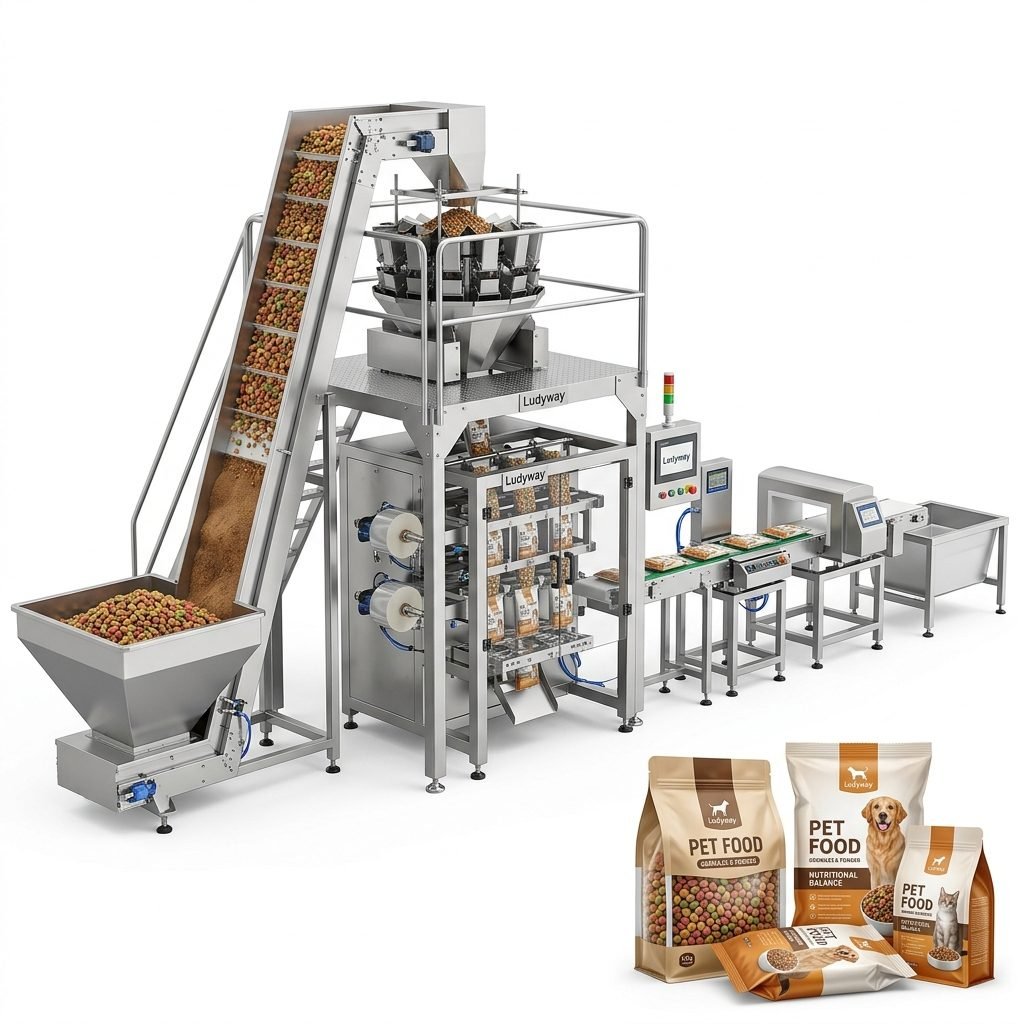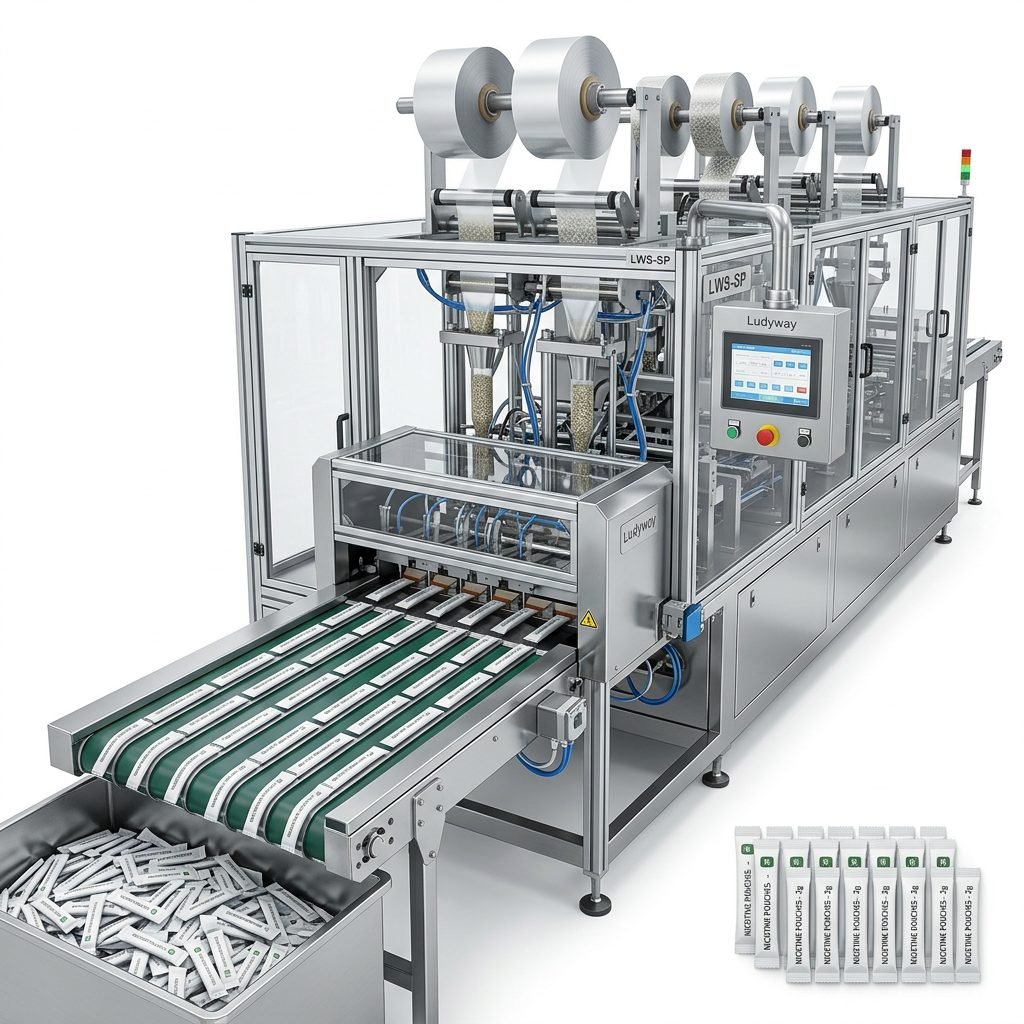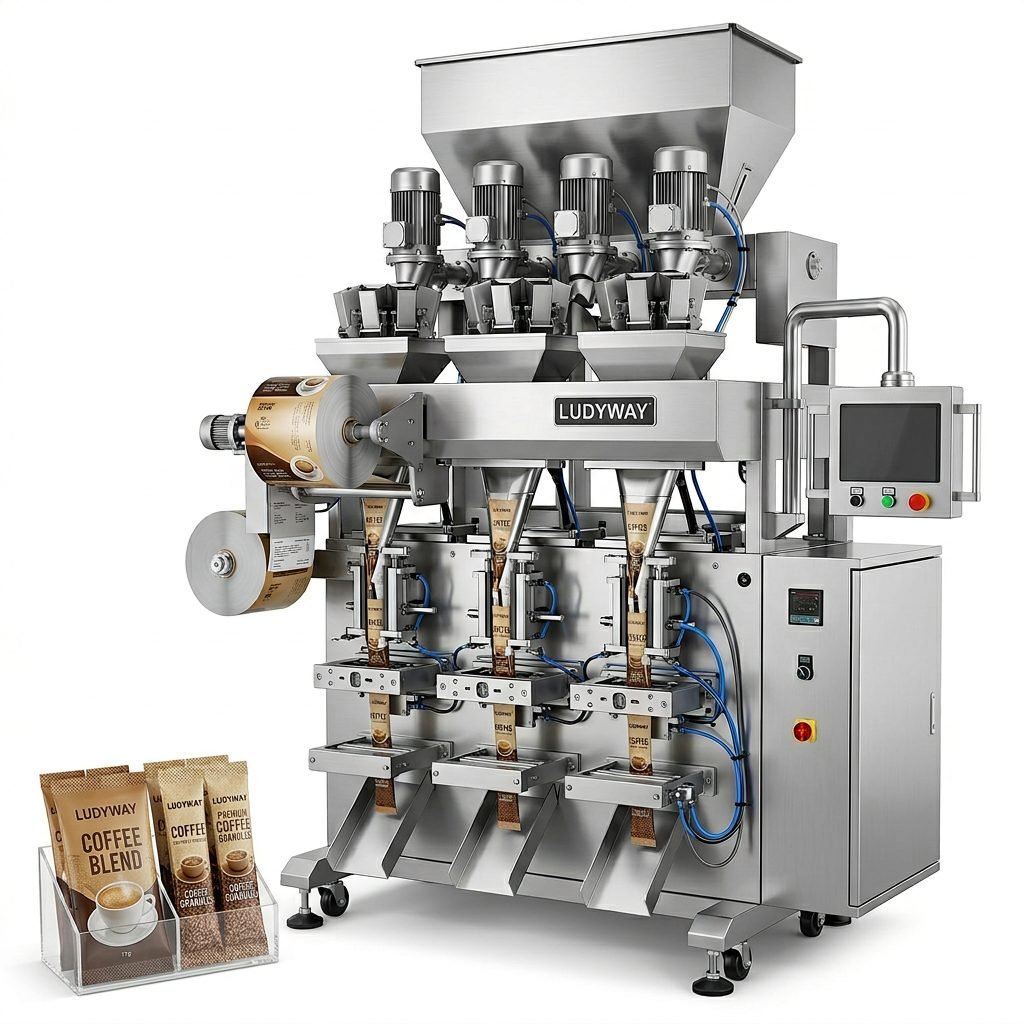
In the competitive animal food manufacturing sector, packaging efficiency directly impacts product quality, shelf life, and profitability. Whether producing dry kibble, wet pet food, nutrition powders, or mineral supplements, manufacturers need robust, high-speed packaging systems that can handle diverse product types while maintaining precision and hygiene standards. The Ludyway animal food packaging machine has emerged as a leading solution for businesses seeking to optimize their production lines.
Understanding the Demands of Animal Food Packaging
Animal food products present unique packaging challenges. Unlike human food, pet and livestock feed often involves irregular granule sizes, oily powders, sticky pastes, and moisture-sensitive formulations. A reliable animal food packaging machine must deliver consistent filling accuracy across varying product densities while preventing contamination and ensuring seal integrity. According to the Flexible Packaging Association, the global trend toward convenient single-serve and multi-lane sachet formats is reshaping how animal nutrition products reach consumers.
Multi-Lane Technology: The Efficiency Breakthrough
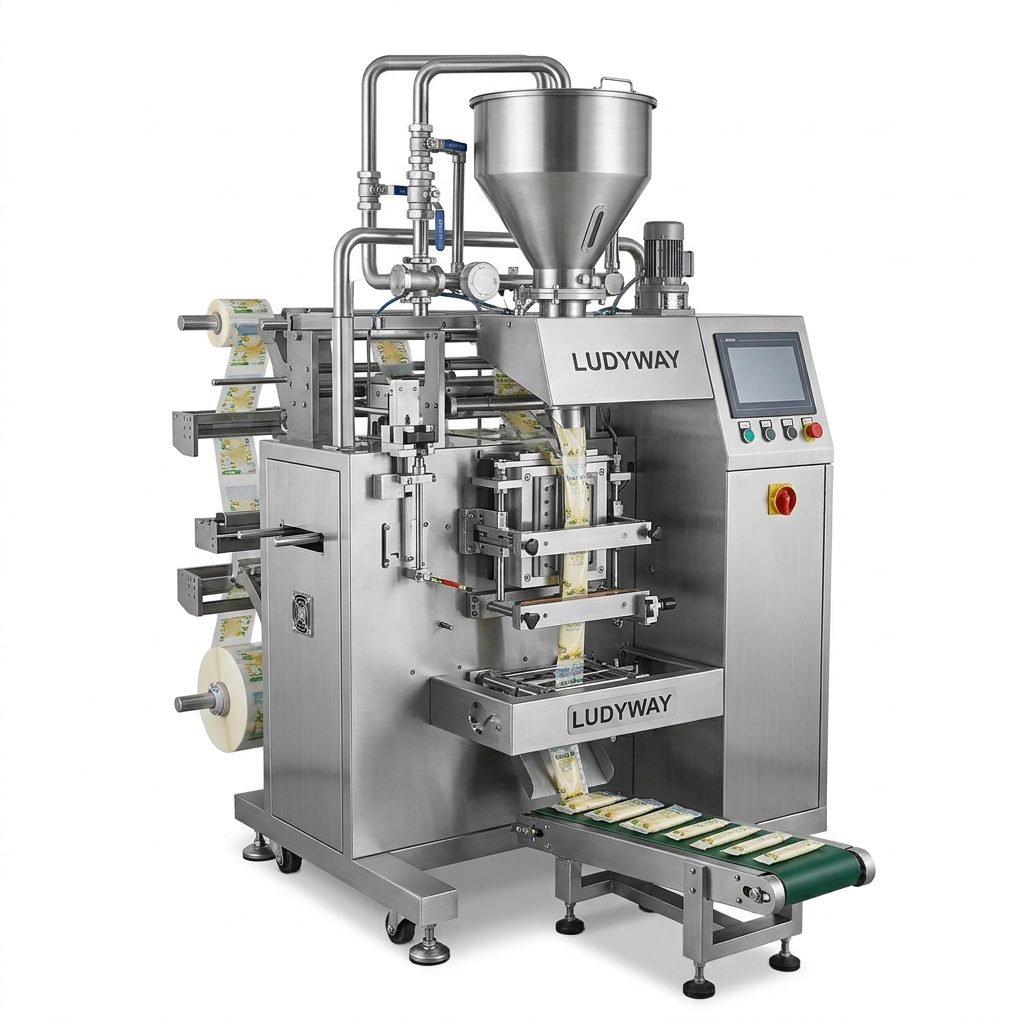
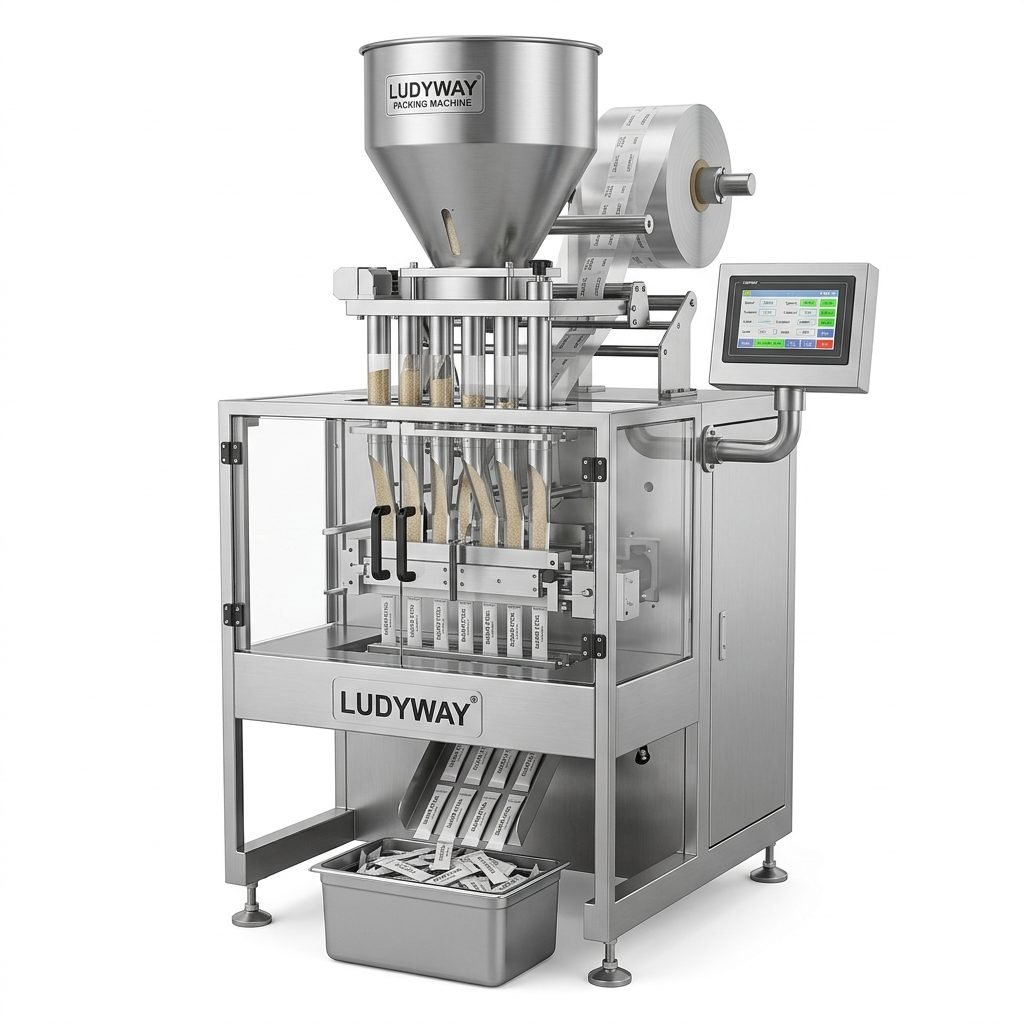
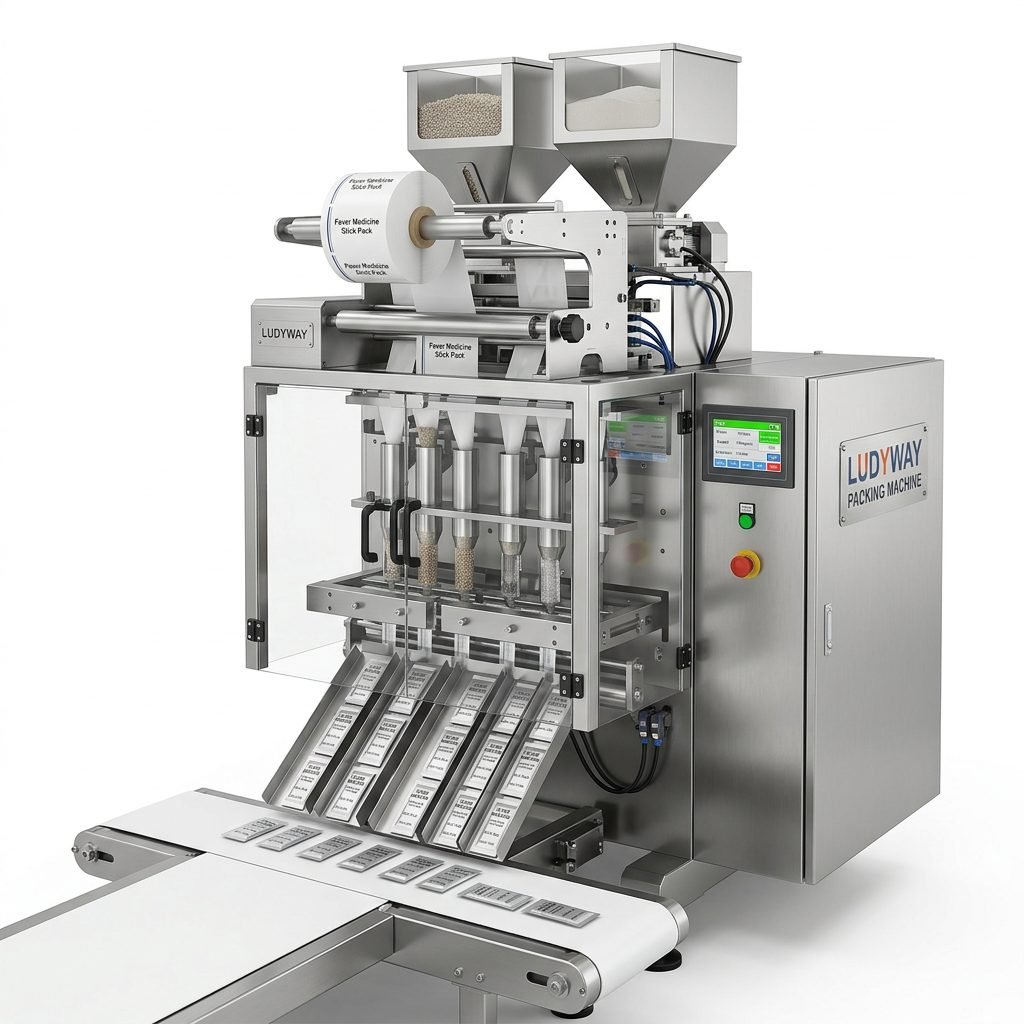
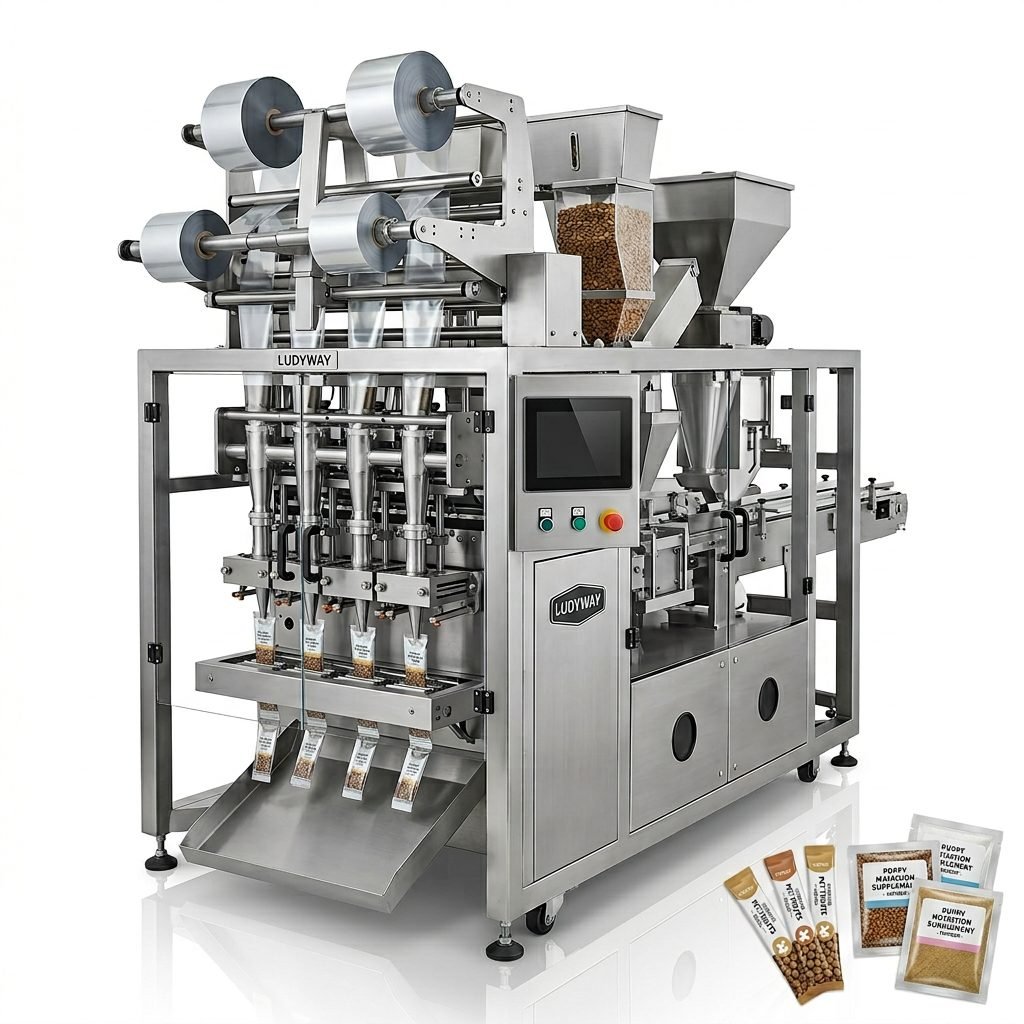
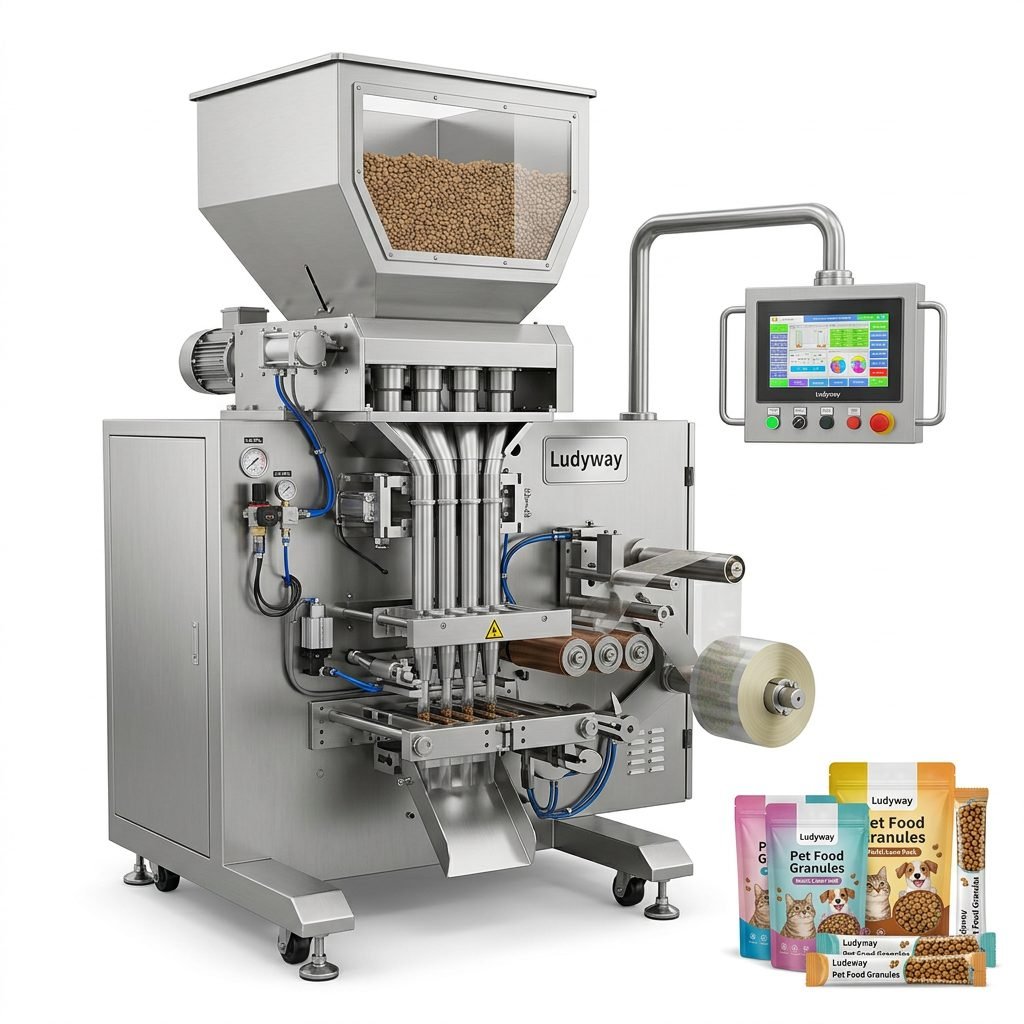
The core advantage of a modern animal food packaging machine lies in multi-lane stick pack and sachet technology. Traditional single-lane machines produce one pouch per cycle, severely limiting throughput. Multi-lane systems, by contrast, can run 4 to 12 lanes simultaneously, dramatically increasing output without proportional increases in floor space or labor. This architecture is particularly valuable for:
- High-volume pet treat manufacturers requiring rapid turnaround on bulk orders
- Private-label producers managing multiple SKU formats on the same line
- Export-oriented businesses needing consistent package quality for international distribution
- Co-packers serving diverse clients with varying granule and powder specifications
Precision Weighing and Filling for Diverse Product Types
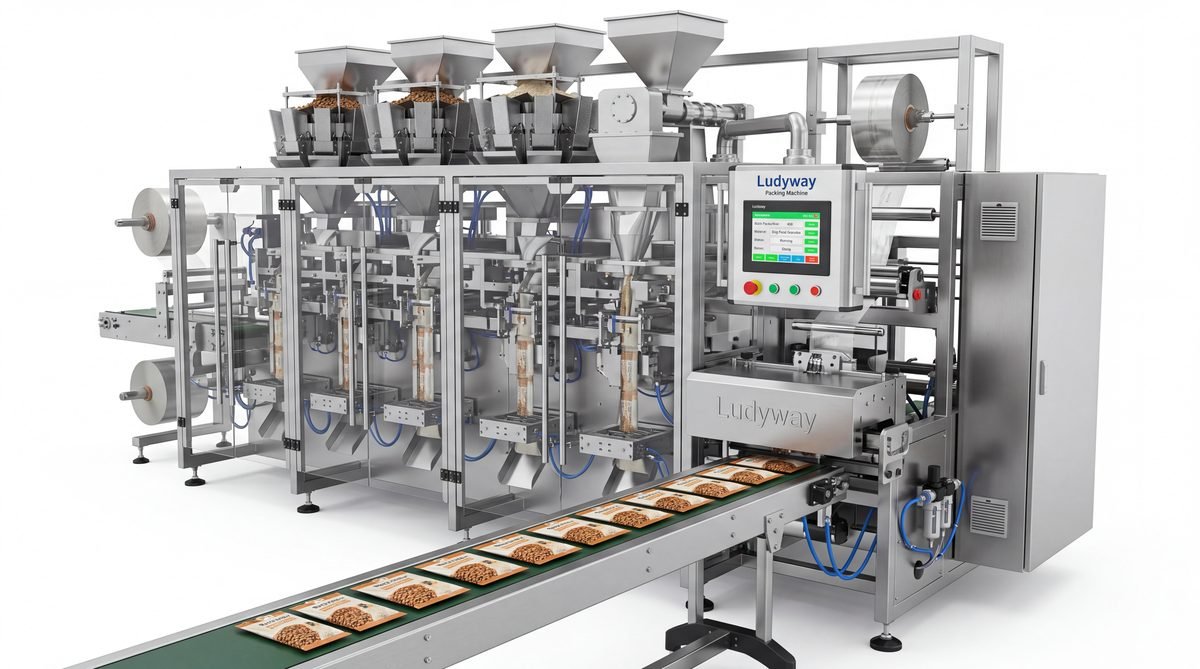
Animal food formulations range from free-flowing granules like dry kibble to cohesive powders such as protein supplements and mineral premixes. A high-performance packaging machine must adapt seamlessly. Advanced servo-driven auger fillers and multi-head weighers integrated into the packaging line ensure each sachet or stick pack receives the exact target weight. The FDA food packaging regulations emphasize the importance of accurate net weight compliance, especially for products destined for regulated markets.
Sealing Integrity and Product Freshness
Oxygen and moisture ingress are primary enemies of animal food shelf stability. Fat oxidation in dry pet foods can lead to rancidity, while moisture absorption causes powder caking and microbial growth. A superior animal food packaging machine incorporates precision heat-sealing jaws with digital temperature control, creating hermetic seals that lock in freshness. Many models also support nitrogen flushing and vacuum-assisted sealing for sensitive formulations such as freeze-dried raw pet foods and probiotic-enriched supplements.
Material Compatibility and Sustainable Packaging Trends
Today’s packaging landscape demands machines that work with a wide spectrum of film materials. From traditional multi-layer laminates to emerging recyclable mono-material films and biodegradable substrates, the equipment must handle varying seal temperatures, slip characteristics, and tensile strengths. Leading systems are designed with adjustable film tension control and multi-zone temperature profiling, allowing operators to fine-tune parameters for each material type. The PMMI packaging machinery market research indicates that flexibility in material handling is now a top purchasing criterion for food manufacturers worldwide.

Key Technical Specifications to Evaluate
When selecting an animal food packaging machine, manufacturers should evaluate several critical parameters. The table below outlines key performance indicators and their operational significance:
| Feature | Benefit | Ideal Application |
|---|---|---|
| Multi-Lane Configuration (4-12 lanes) | Exponential output increase with minimal footprint | High-volume pet food and supplement sachets |
| Servo-Driven Dosing System | ±0.5g precision for consistent portion control | Nutritional supplements and veterinary products |
| Digital Temperature Control | Hermetic seal integrity across variable film types | Moisture-sensitive and oxygen-sensitive products |
| Quick-Change Format Parts | Reduced downtime between product changeovers | Contract packagers and multi-SKU manufacturers |
| Stainless Steel Construction | Full washdown capability and corrosion resistance | Wet food, raw pet food, and high-moisture products |
Versatility Across Animal Food Categories
A truly efficient packaging machine should handle the full spectrum of animal nutrition products. From livestock feed premixes and aquaculture pellets to premium cat treats and veterinary supplement powders, the equipment must transition smoothly between product types. The ability to package granules, powders, and even liquid animal nutrition supplements on a single platform reduces capital expenditure and simplifies operator training. This versatility is particularly valuable for manufacturers expanding their product portfolios in response to evolving market demands.
Automation and Smart Factory Integration
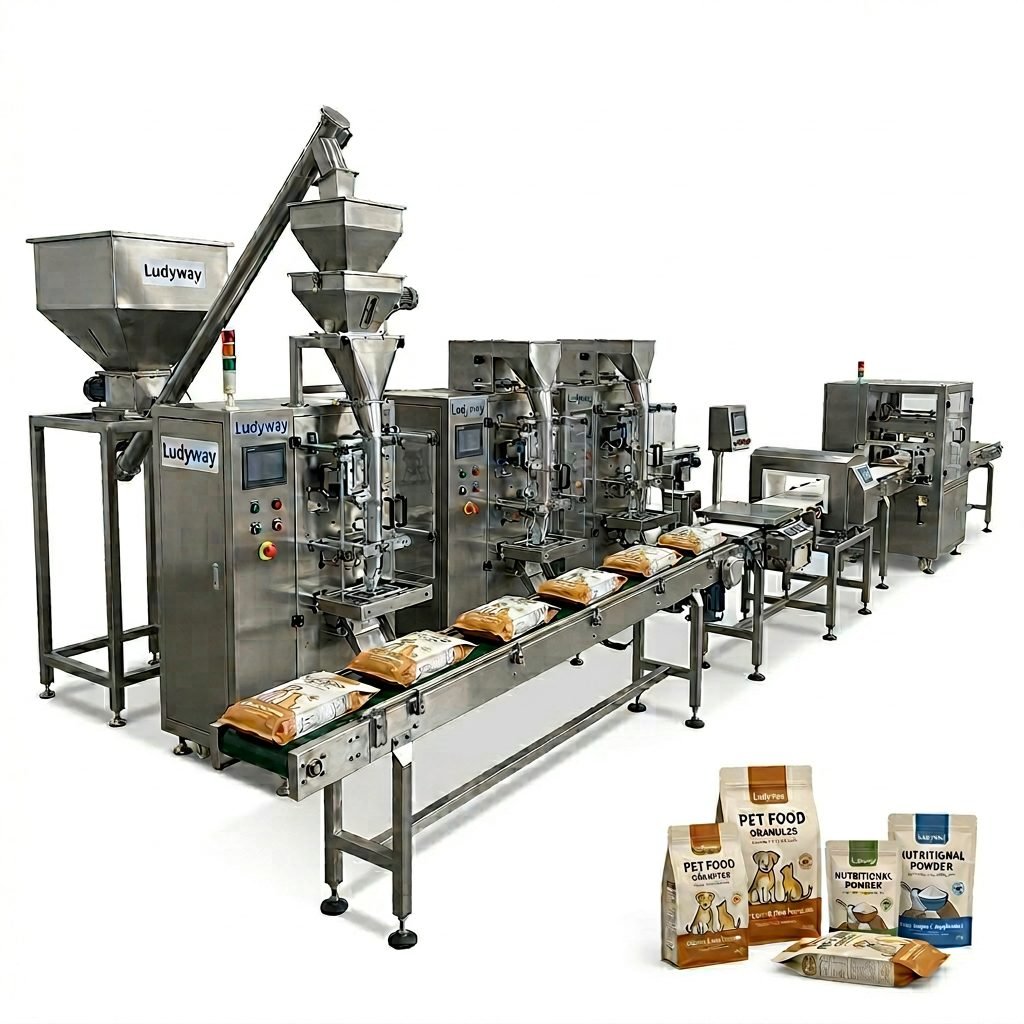
Modern production environments increasingly demand seamless integration with upstream and downstream equipment. An advanced animal food packaging machine should communicate with weighing systems, cartoning machines, case packers, and palletizing robots through standardized industrial protocols. Real-time production monitoring, remote diagnostics, and predictive maintenance alerts further enhance operational efficiency. These smart features align with Industry 4.0 principles and help manufacturers achieve consistent output with minimal unplanned downtime.
Hygiene and Sanitary Design Considerations
Animal food safety standards are increasingly aligned with human food regulations, particularly in markets such as the European Union and North America. A packaging machine designed with tool-free disassembly, sloped surfaces, and sealed electrical enclosures facilitates thorough cleaning and sanitation. Compliance with ISO packaging standards and GMP guidelines ensures that manufacturers can meet the stringent requirements of international retailers and regulatory bodies without costly retrofits.
Cost Efficiency and Return on Investment
While the initial capital outlay for a high-quality packaging system represents a significant investment, the long-term operational savings are compelling. Key factors contributing to rapid ROI include:
- Reduced labor costs through full automation of filling, sealing, and cutting operations
- Lower film waste due to precision film registration and minimal mis-seal rates
- Decreased product giveaway from accurate servo-driven dosing systems
- Extended product shelf life resulting in fewer returns and less spoilage
- Higher throughput per square meter of factory floor space compared to single-lane alternatives
About the Manufacturer
Ludyway is one of the largest packaging machine manufacturers in China, specializing in advanced packaging equipment and turnkey production solutions for the food, pharmaceutical, and health industries. Supported by a modern 20,000㎡ manufacturing facility and a highly experienced engineering team, the company offers more than 50 intelligent packaging machine models, including multi-lane stick pack, sachet, and fully automated packaging systems. Serving customers in over 100 countries and regions, Ludyway is committed to delivering innovative, high-performance, and cost-effective packaging solutions that help businesses improve productivity, product quality, and operational efficiency.

Why Efficiency Matters More Than Ever
The global animal food market continues to expand, driven by rising pet ownership rates, increasing livestock production, and growing consumer demand for premium and functional animal nutrition products. In this dynamic environment, manufacturers cannot afford packaging bottlenecks, inconsistent product quality, or excessive material waste. A well-engineered animal food packaging machine serves as the cornerstone of a competitive production strategy, enabling businesses to scale operations while maintaining the quality standards that build brand loyalty.
For operations managers and business owners evaluating packaging technology investments, the combination of multi-lane productivity, precision dosing accuracy, material flexibility, and hygienic design makes the Ludyway animal food packaging machine a compelling choice for efficient, future-ready production.